
More Articles
Published 14 September 2026
The short version
High-frequency welding (HFW) runs a strip straight through forming stands and closes a longitudinal seam. Spiral welding (SSAW) feeds the strip in at an angle and winds it into a helix, closing a spiral seam.
Both make welded pipe. They are not interchangeable lines, and they suit different businesses.
How an HFW line forms a pipe
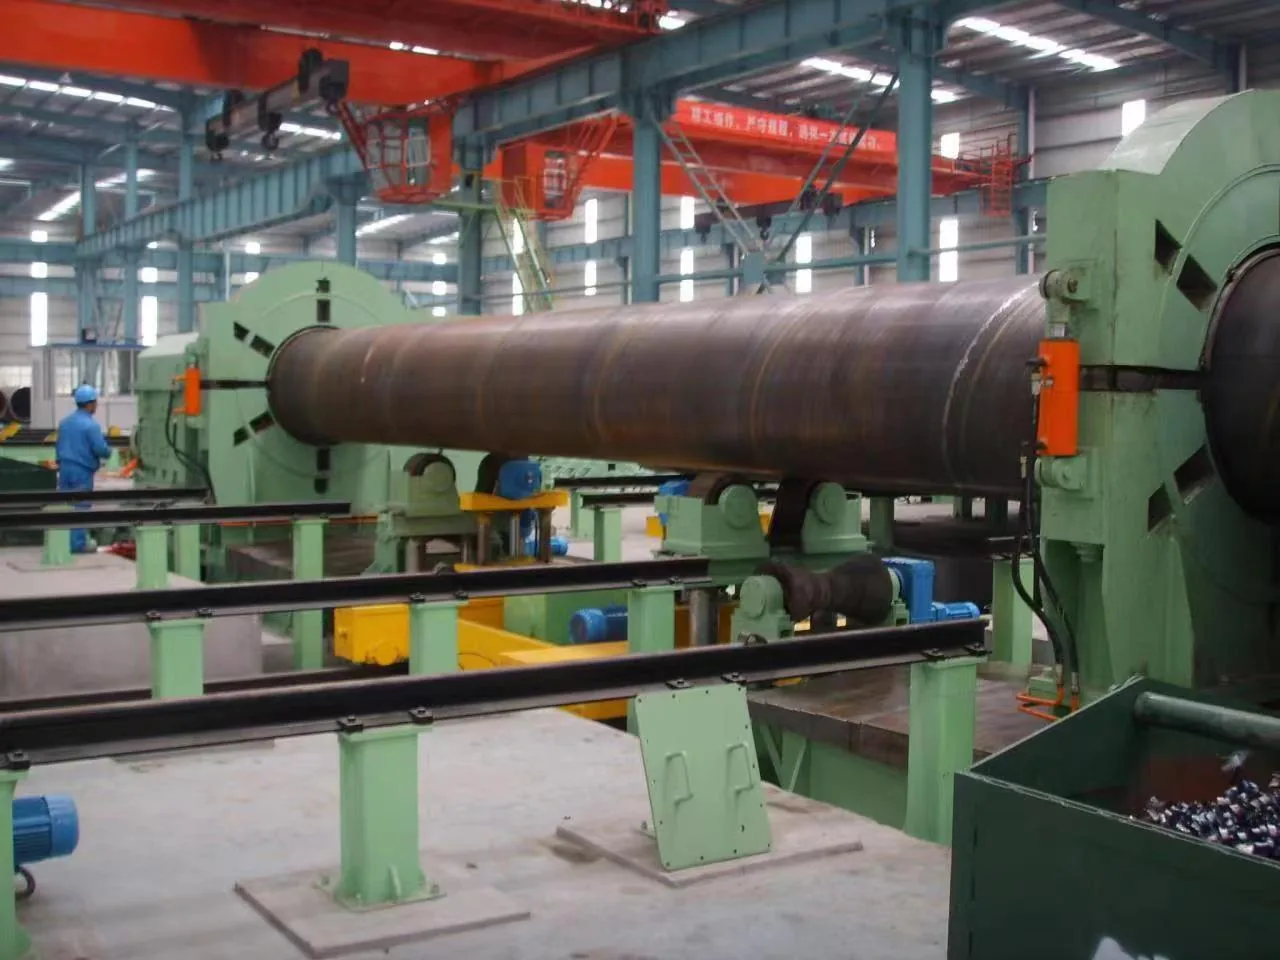
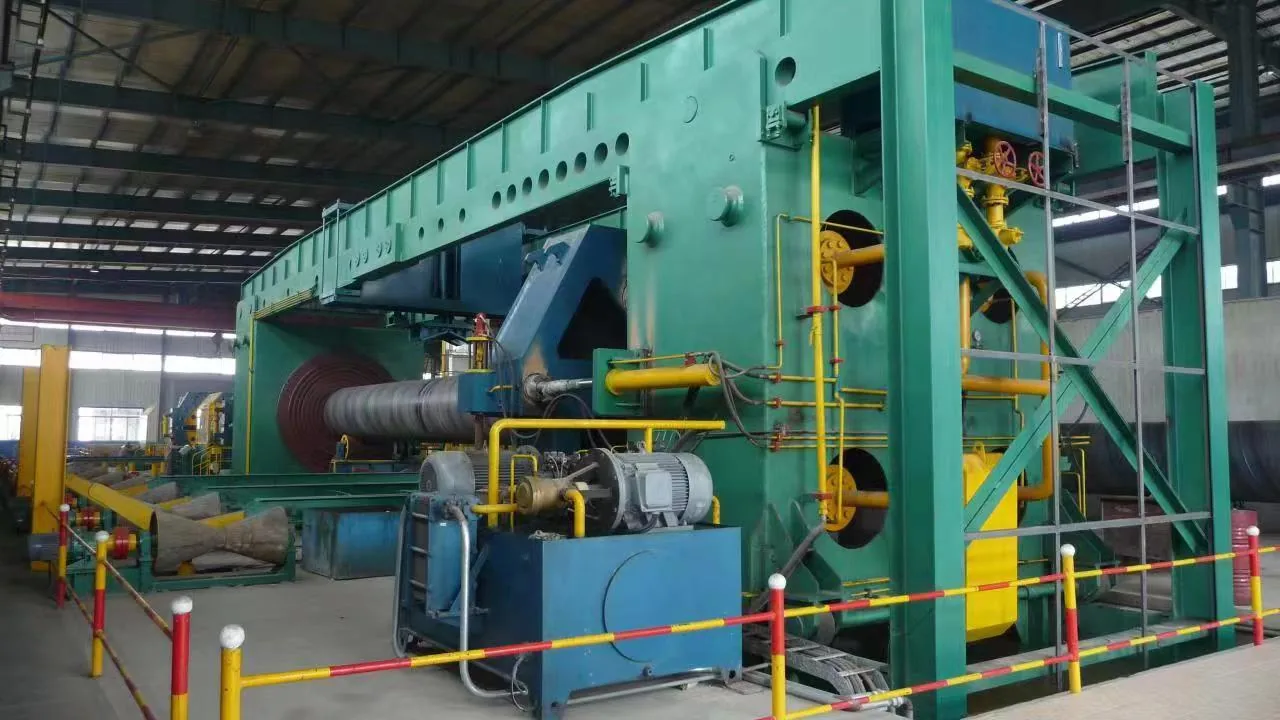
A coil is uncoiled, levelled, and fed into a forming section that bends the flat strip progressively into a circle. The two edges arrive at the weld box, are heated by high-frequency current, and are pressed together. The bead is scarfed, the pipe is sized and cut to length.
The strip width is fixed by the diameter you want. Change the diameter and you change the strip width and the roll set. That is the central fact about an HFW line: diameter changes mean roll changes.
How an SSAW line forms a pipe
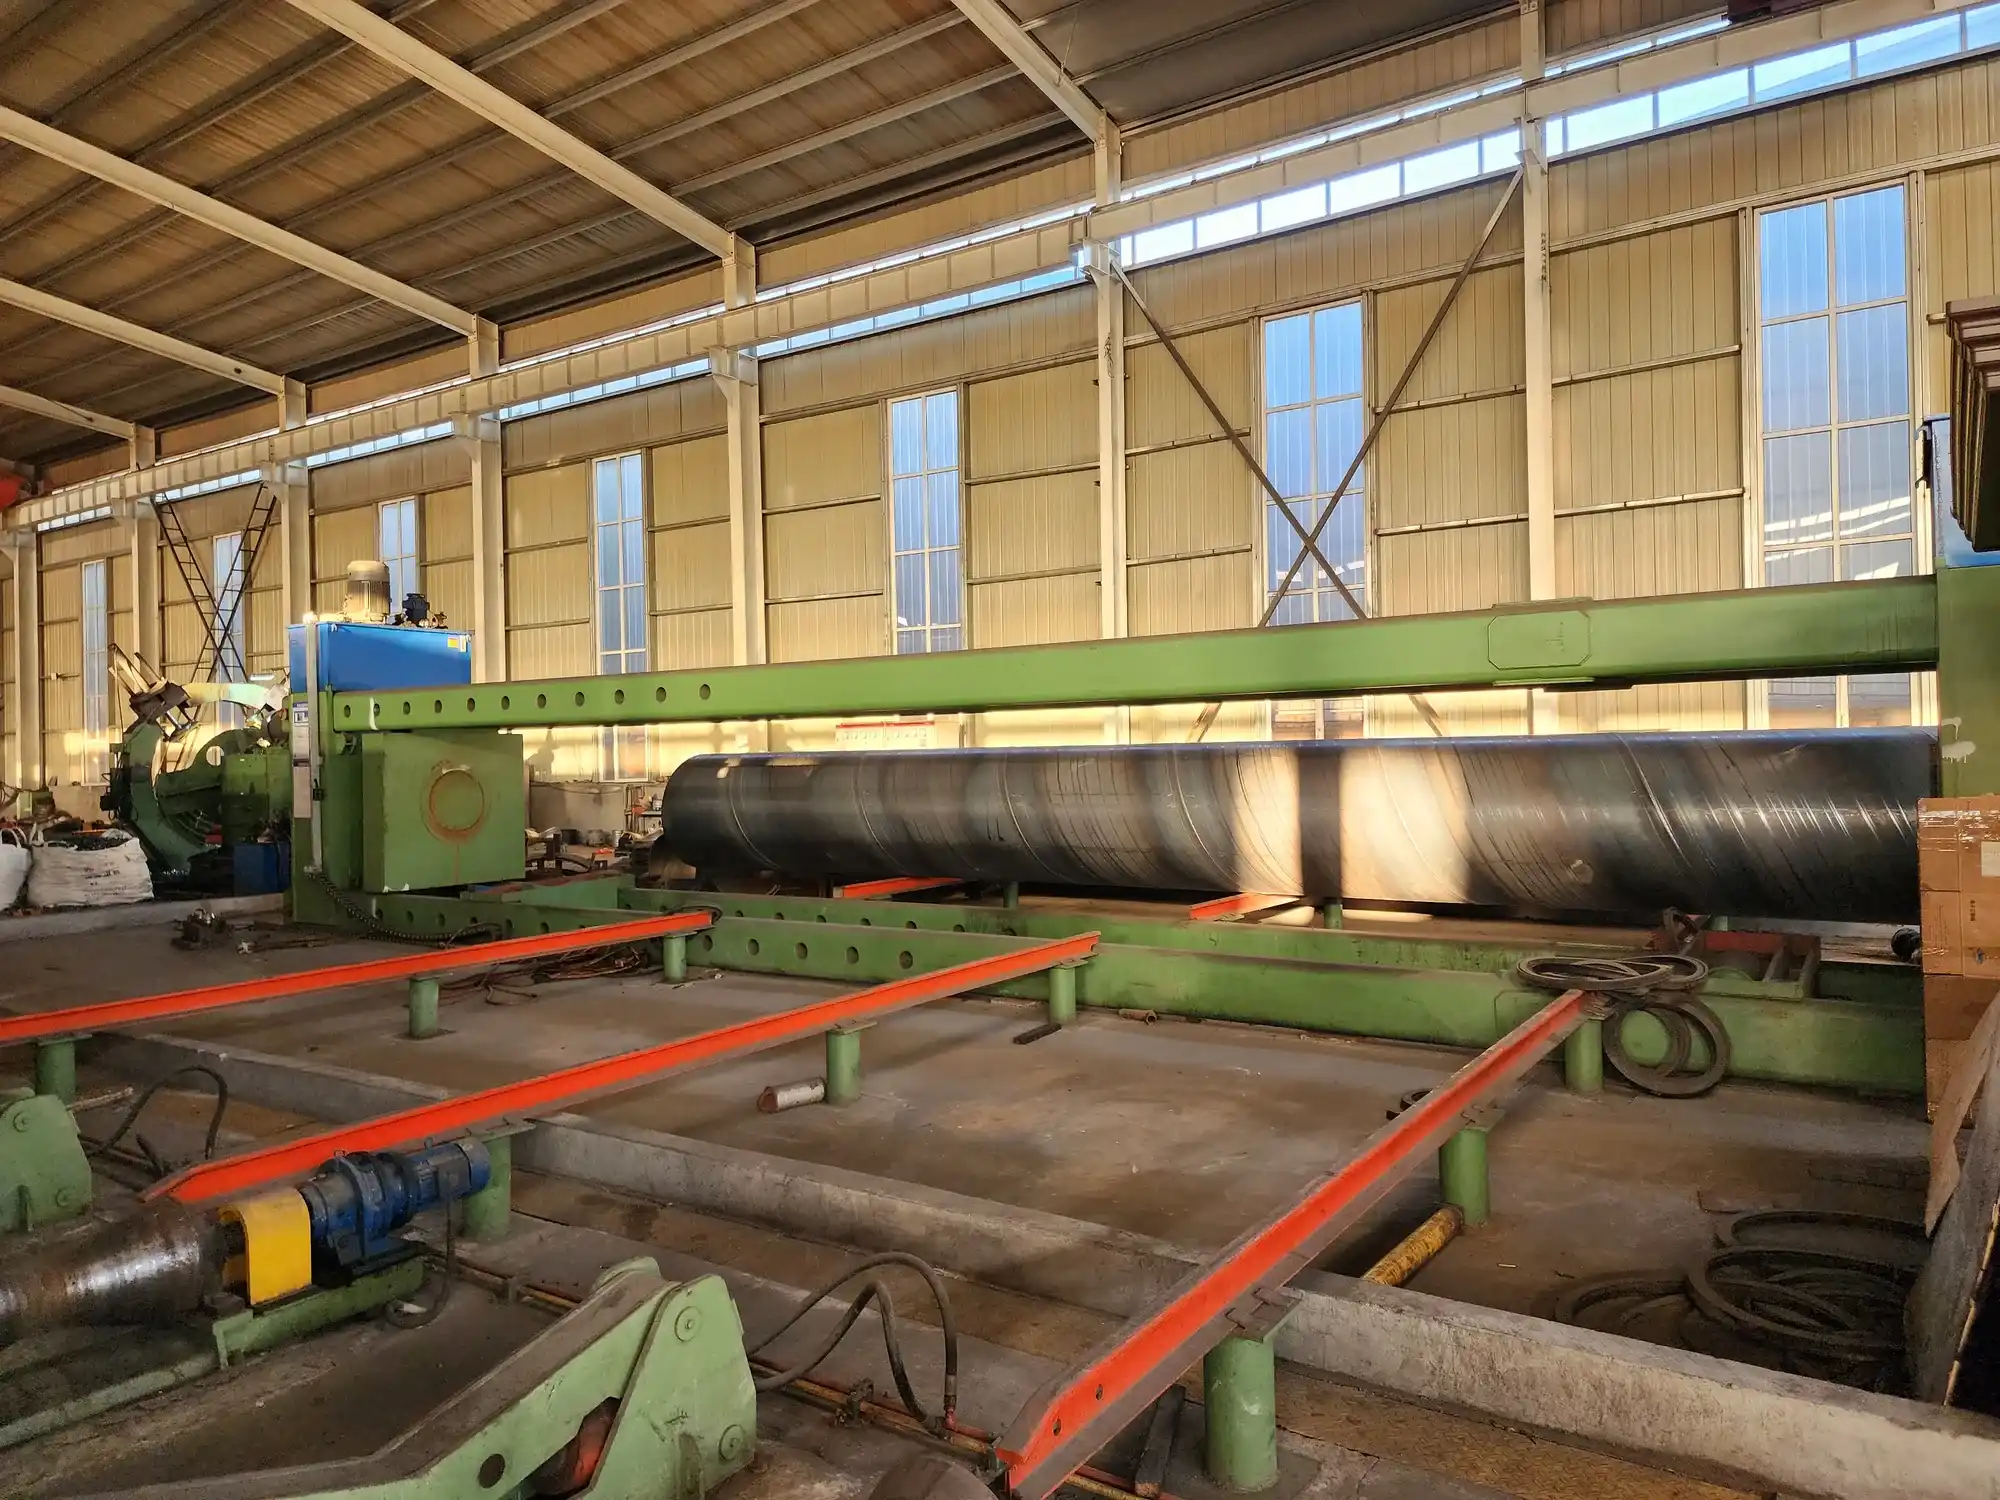
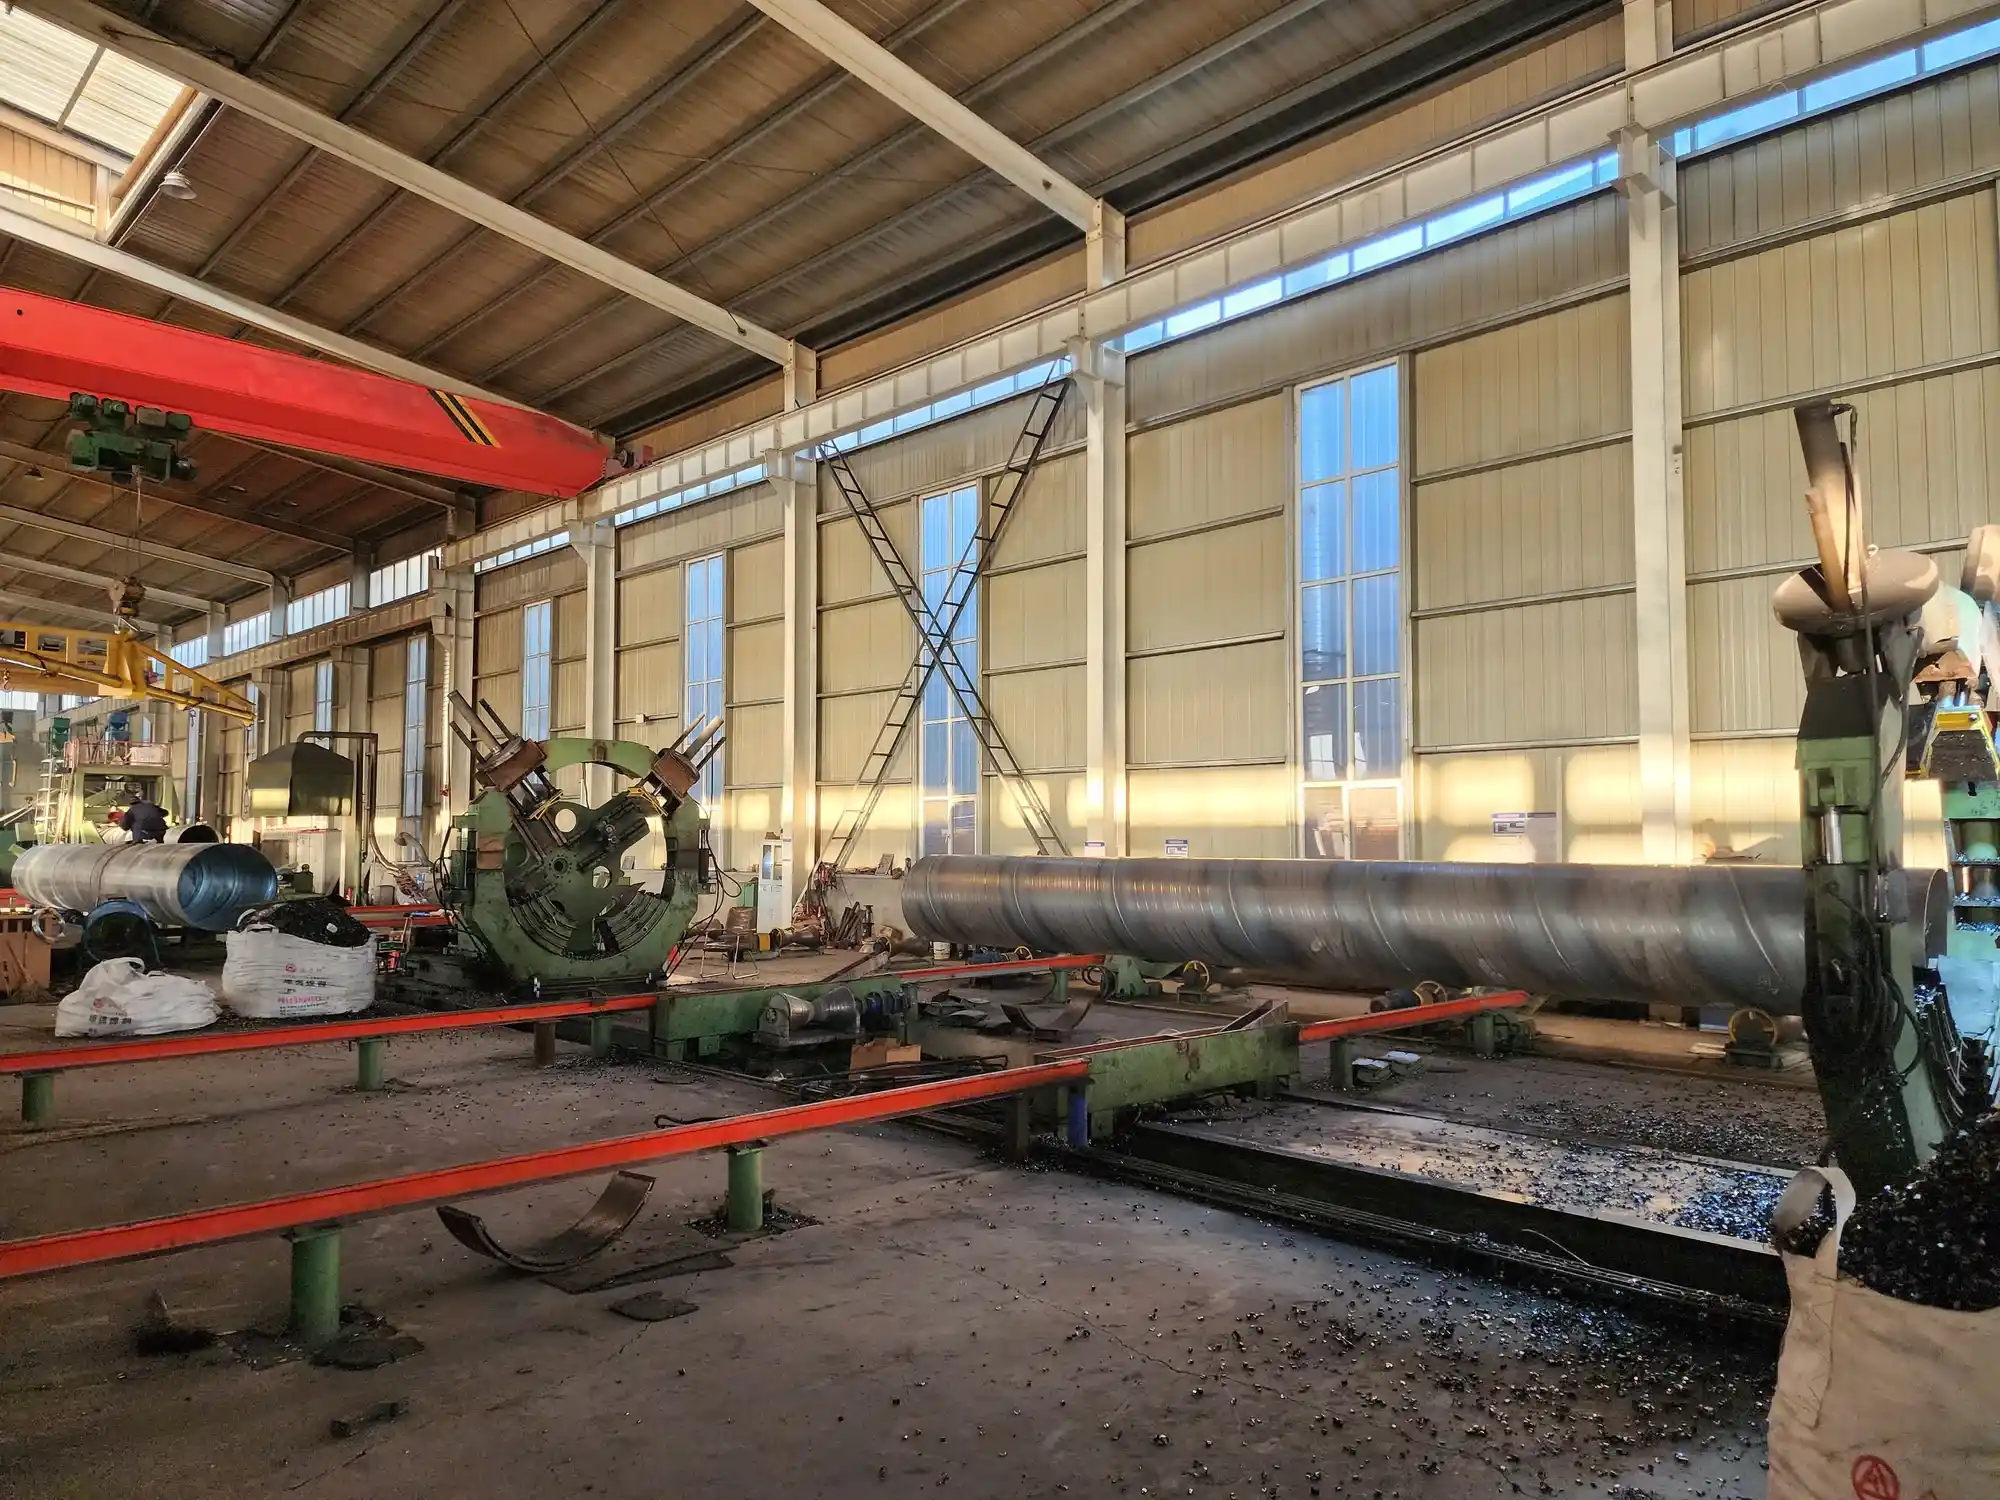
The strip enters the forming head at an angle. As it advances, it wraps into a helix and the edges meet along a spiral seam, which is welded — typically by submerged arc, inside and outside.
Because the diameter is a function of the forming angle and the strip width, one line can produce a wide span of diameters from a limited number of strip widths. That is the central fact about an SSAW line: diameter changes are largely an angle change, not a roll change.
Side by side
| HFW | SSAW | |
|---|---|---|
| Seam | longitudinal, one straight seam | helical, running the length of the pipe |
| Feedstock | strip width tied to the target diameter | one strip width covers several diameters |
| Diameter change | roll set change | forming angle change |
| Diameter reach | suited from small bore upward, in steps | favoured where diameter is large relative to strip width |
| Product profile | high volume of one or a few sizes | varied diameters, larger sizes, project quantities |
| Typical use | standard sizes in steady volume | pipeline, piling and structural projects |
Which one should you quote?
Ask what your order book looks like, not what the machine can do.
- If you sell a small number of standard sizes in continuous volume — scaffold tube, furniture tube, fluid pipe in fixed diameters — an HFW line is usually the answer. The roll change is a known cost, and you will not be making it often.
- If your orders arrive as projects, each with its own diameter, and the diameters are large, an SSAW line will spend less time in changeover and will cover the range with less tooling.
- If you supply line pipe to a specification, the specification itself may decide the process before either argument applies. Start from the standard your customer names.
If you serve both markets, the question becomes which line to install first, and that comes back to which order book is already paying.
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.