
Home › Pipe Production Applications › Structural & Scaffolding Tube Production
A scaffolding tube mill or structural steel tube mill is chosen by section: high-frequency welded lines for round, square and rectangular tube, direct forming lines where square sizes change often, and an H-beam line where the section is a beam.
In This Line
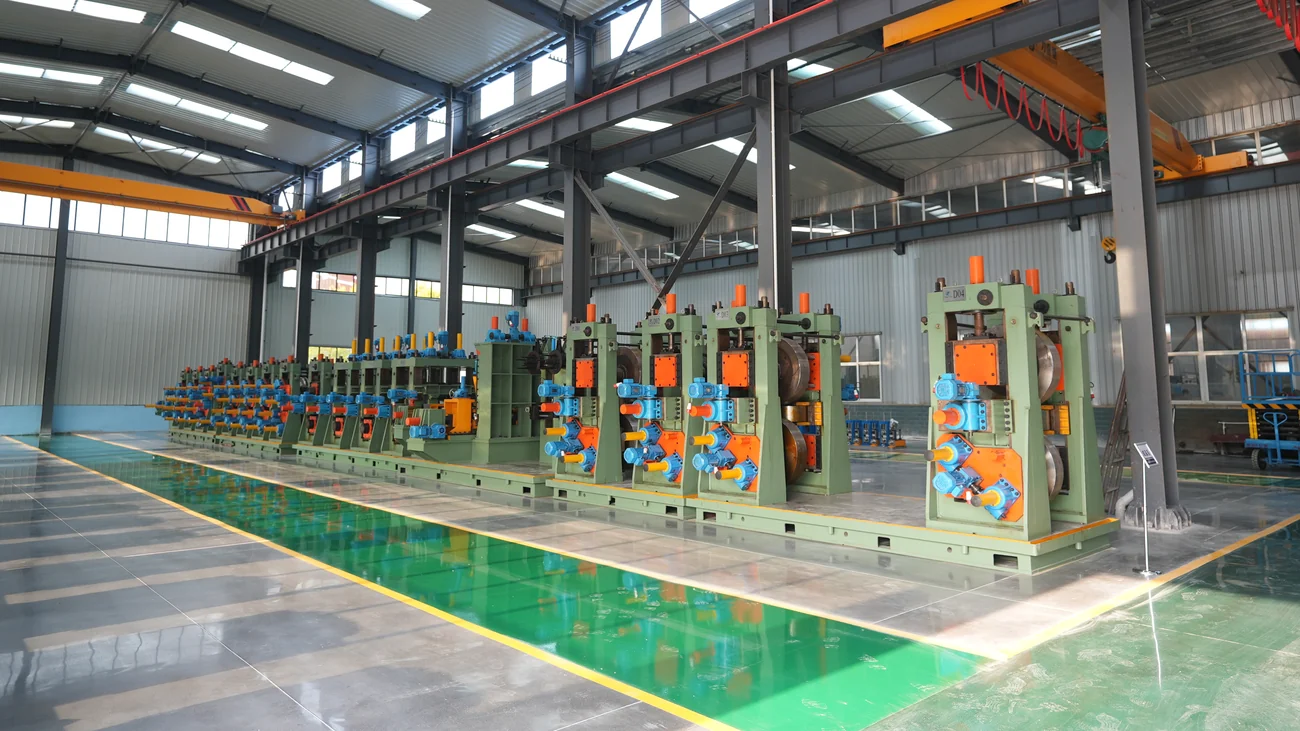
Most of our reference deliveries make construction tube.
What Is Structural & Scaffolding Tube Production
Structural and scaffolding tube production lines make round, square and rectangular tube for building frames, steel structures and scaffolding. What this work asks of the mill differs from fluid pipe: frequent size changes, stable forming on square and rectangular section, sharp corners, and good straightness and surface.
Target Pipe Sizes and Wall Thickness for This Application
High-frequency welded tube mill — twelve steps from HG32 to HG630, finished outside diameter Φ10 to Φ630 mm, wall 0.5 to 16 mm, in round, square and rectangular section on most steps.
Direct forming square tube mill — square section from 30 × 30 mm to 500 × 500 mm in seven bands, wall 1.5 to 20 mm; within each band one combined roll set covers the size range, so a size change is a servo adjustment rather than a roll change. Details are on the direct forming square tube mill page.
H-beam production line — welded H-beam to GOST R 58966-2020, 147 to 450 mm high with 80 to 350 mm flanges and 4 to 16 mm web and flange (20 mm as an option). The full specification is on the h-beam production line page.
| Mill step | Finished outside diameter | Wall thickness | Welder power |
|---|---|---|---|
| HG32 | Φ10–32 mm | 0.5–1.5 mm | 150 kW |
| HG50 | Φ16–50.8 mm | 0.8–2.0 mm | 200 kW |
| HG76 | Φ25–76 mm | 1.5–3.0 mm | 250 kW |
| HG89 | Φ32–89 mm | 1.0–4.0 mm | 300 kW |
| HG114 | Φ45–114 mm | 1.5–5.0 mm | 300 kW |
| HG165 | Φ60–165 mm | 3.0–7.0 mm | 400 kW |
| HG219 | Φ114–219 mm | 4.0–8.0 mm | 500 kW |
| HG273 | Φ114–273 mm | 4.0–10.0 mm | 600 kW |
| HG325 | Φ165–325 mm | 4.0–10.0 mm | 600 kW |
| HG426 | Φ165–426 mm | 4.0–10.0 mm | 800 kW |
| HG508 | Φ219–508 mm | 4.0–16.0 mm | 1000 kW |
| HG630 | Φ325–630 mm | 4.0–16.0 mm | 1500 kW |
Mill Model and Welder Power Band
Welder power follows the mill step: 150 kW on HG32 up to 1500 kW on HG630 for round-based lines, and 300 kW up to 2000 kW across the seven direct forming bands.
| Band | Finished square section | Wall thickness | Welder power |
|---|---|---|---|
| 1 | 30 × 30 – 100 × 100 mm | 1.5–4.0 mm | 300 kW |
| 2 | 70 × 70 – 150 × 150 mm | 2.0–6.0 mm | 600 kW |
| 3 | 100 × 100 – 200 × 200 mm | 2.0–6.0 mm | 600 kW |
| 4 | 100 × 100 – 250 × 250 mm | 2.0–8.0 mm | 800 kW |
| 5 | 150 × 150 – 300 × 300 mm | 5.0–13 mm | 1000 kW |
| 6 | 150 × 150 – 400 × 400 mm | 5.0–14 mm | 1000 kW |
| 7 | 200 × 200 – 500 × 500 mm | 10–20 mm | 2000 kW |
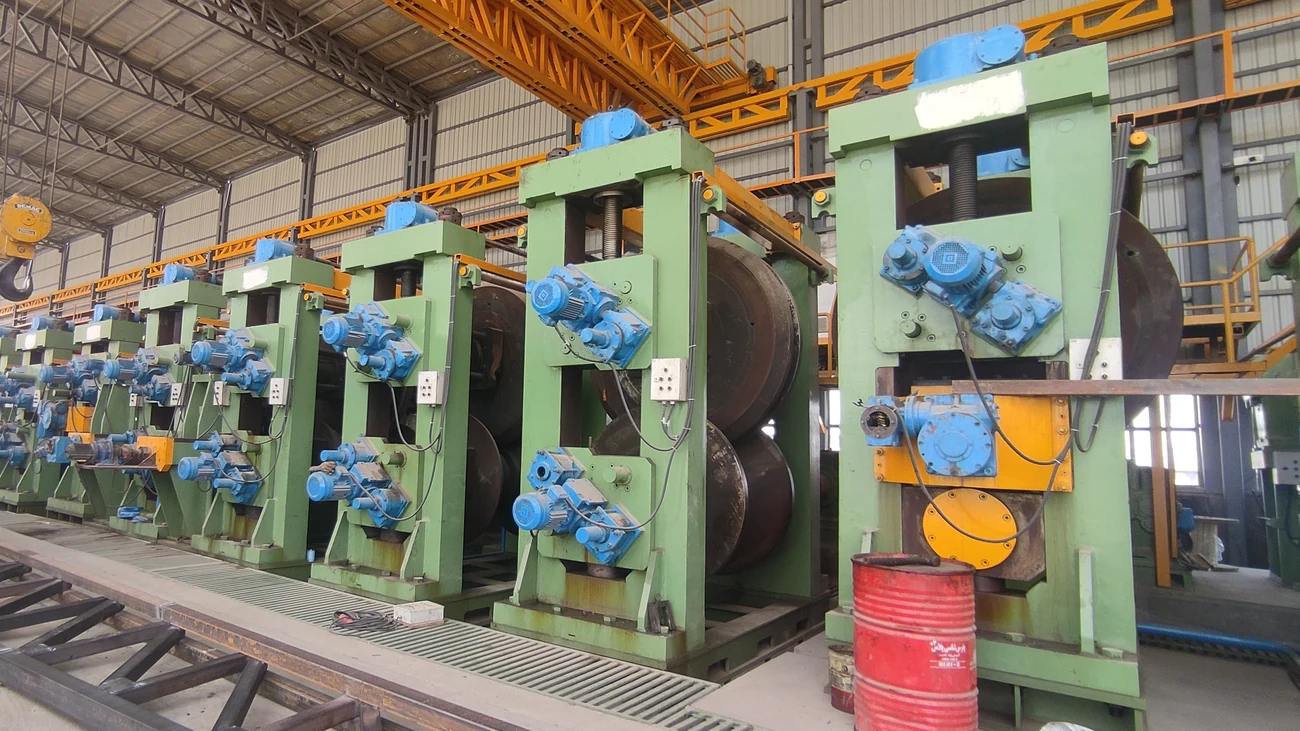
Two Forming Routes for Square Section
Square and rectangular section dominates structural work, so the forming route is the key decision. Conventional roll forming makes a round tube, welds it and sizes it down to square. Direct forming takes the strip straight to the square section, so a size change within a band is a servo adjustment rather than a roll change.
The direct route means fewer forming passes, fewer roll changes, point contact that reduces roll wear, and a roll saving of more than 90%. One exception applies: making 100 × 100 mm tube needs the upper roll on the final open stand changed. It suits a plant that changes size often across the 30 × 30 to 500 × 500 range and pays for that in roll cost and changeover downtime.
Applicable Standards and Inspection Requirements
The H-beam line produces beams to GOST R 58966-2020, the Russian welded H-beam standard, which applies to the beam rather than the tube. Structural and scaffolding tube is made to the buyer’s own project specification. An ordinary high-frequency welded line carries no in-line NDT, with final inspection as the catching step; structural tube is accepted on corner definition, straightness and appearance rather than through a test chain.
Worked Output Example
- Line speed — confirmed at quotation for the chosen line, against tube size, steel grade and cut length.
- Output — H-beam line: not less than 20 tonnes per hour, and not less than 100,000 tonnes a year on two 12-hour shifts.
- Material yield — 93% or more achievable on high-end configurations of the welded tube family, with actual yield also depending on the plant’s operation.
Standard lines ship within 90 working days of the deposit, with plant-level customisation scheduled from our own manufacturing base.
The line is dismantled into units and shipped in containers: heavy frames are braced and secured, while precision parts and wear items travel in wooden cases together with a spare-parts pack.
Our engineers travel to site to guide installation, commissioning and operator training; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance, and support continues online after handover. Our after-sales team handles enquiries.
Payment is 30% by T/T on signing, 65% by T/T before shipment and 5% after installation and commissioning, or by L/C at sight; prices are quoted ex-works (EXW).
Importers buying one of these lines for a local plant can start from the page for importers & trading companies.
Scaffolding tube making machine
A scaffolding tube making machine is a high-frequency welded line from the HG range rather than a separate machine type, and a scaffolding tube mill is chosen by the diameter and section to be made and by how often the size changes. Scaffolding tube is bought by the tonne against a repeated specification, so batch-to-batch consistency matters more than the largest diameter a mill can reach.
Structural steel tube mill
A structural steel tube mill for square and rectangular section is either a high-frequency welded line that forms round and sizes to square, or a direct forming line that goes straight to the square section. The choice follows how often the plant changes size, since corner definition and straightness are reached on both routes.
Field Evidence for This Application
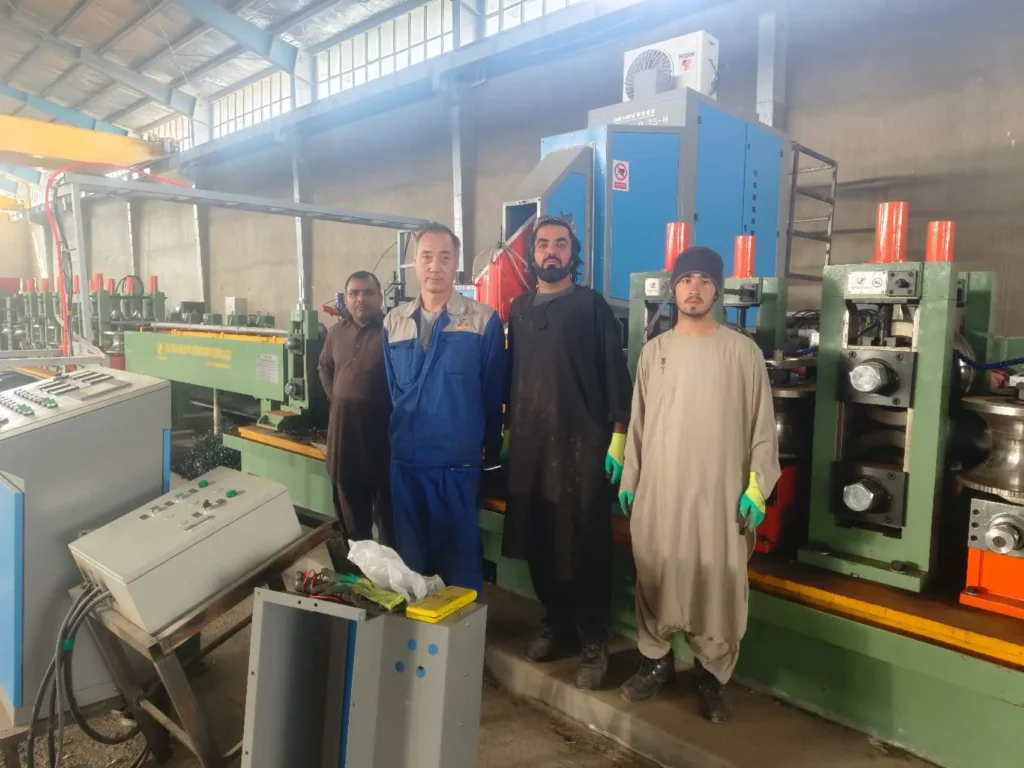
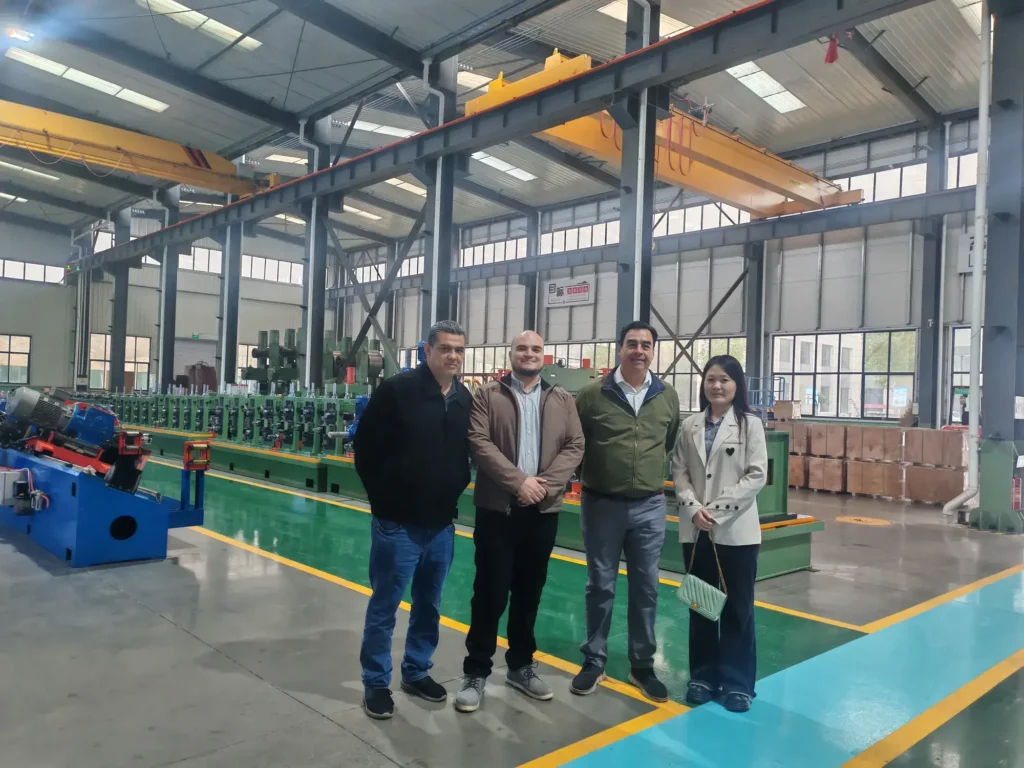
Structural work accounts for most of our reference deliveries.
Square sections include 250 × 250 in Afghanistan, 200 × 200 × 12 in South Korea, 150 × 150 × 6 in Kenya, 200 × 200 in Türkiye and 150 × 150 in Italy.
Round sections include HG165 × 6 in Russia, 165 × 6 in Thailand, 254 × 8 in South Korea, 127 × 6 in Pakistan and Mexico, HG114 × 4 in Mexico, 127 × 3 in Uzbekistan, 168 × 5 in Kyrgyzstan, 89 × 5 in Sri Lanka, HG76 × 3 in Egypt, 76 × 3 in India and 165 × 5 in Afghanistan.
From the Workshop
 Water Supply, Drainage & Urban Gas Pipe Production Lines
 Oil & Gas Line Pipe Mill
 Furniture & Fence Tube Production
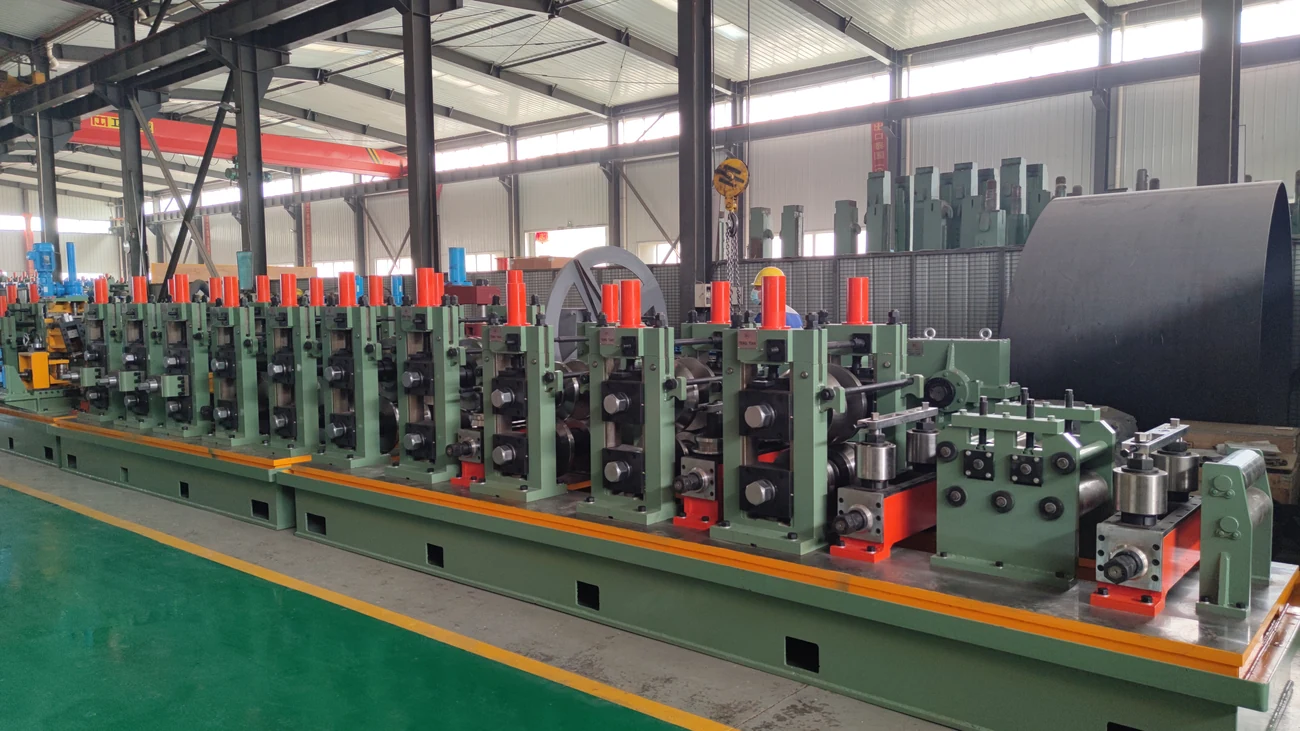 Direct Forming Square Tube Mill
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.