
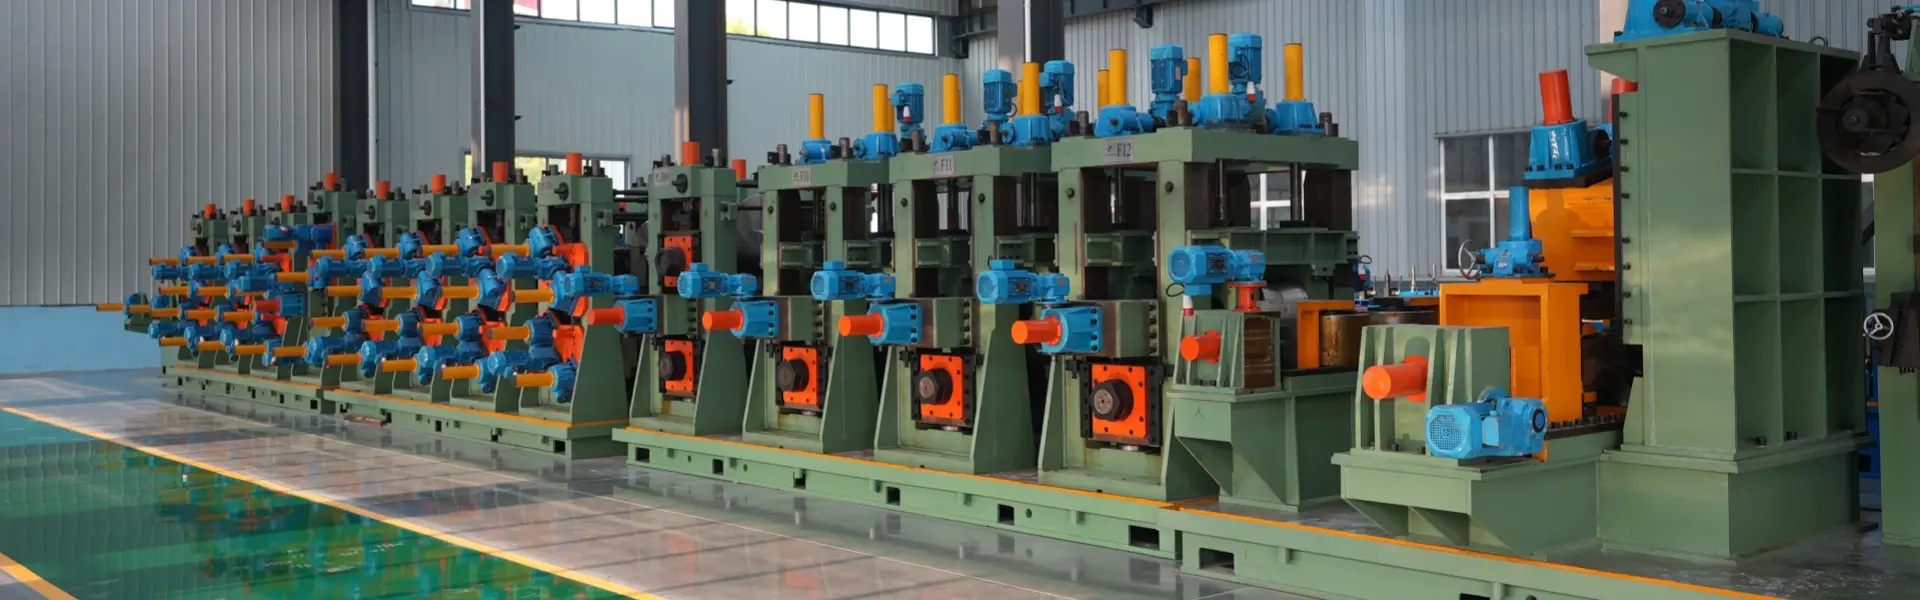
High-Frequency Welded Pipe Mill
In This Line
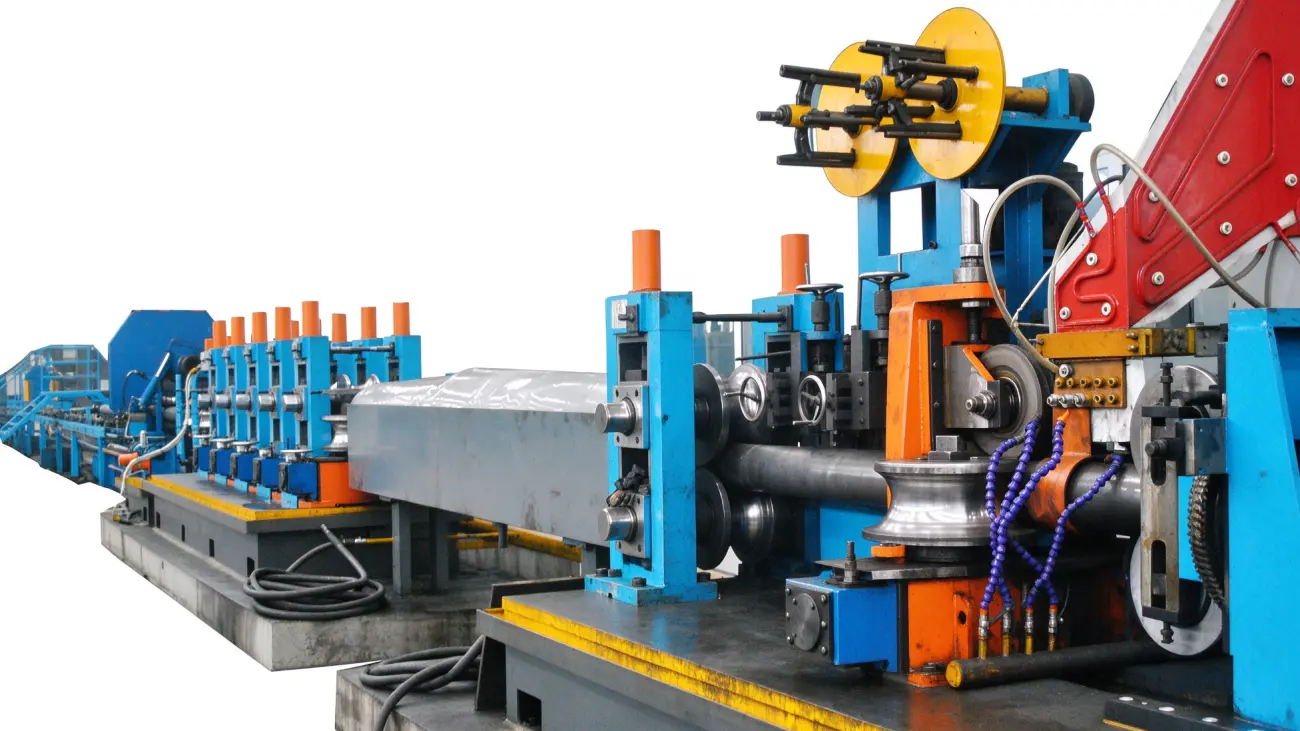
High-frequency induction welding is the step that turns formed strip into pipe, and the HF welding machine at the weld box is what supplies the heat. How it heats the strip edges, what the welder has to be matched to, and what that means when choosing a mill are the same across all twelve HFW model steps.
What Is a High-Frequency Welded Pipe Mill?
High-frequency current is concentrated at the seam by skin and proximity effects, the edges are heated to welding temperature, and squeeze rolls press them together. High-frequency welding is a pressure weld, not a fusion weld with filler. No filler metal is involved.
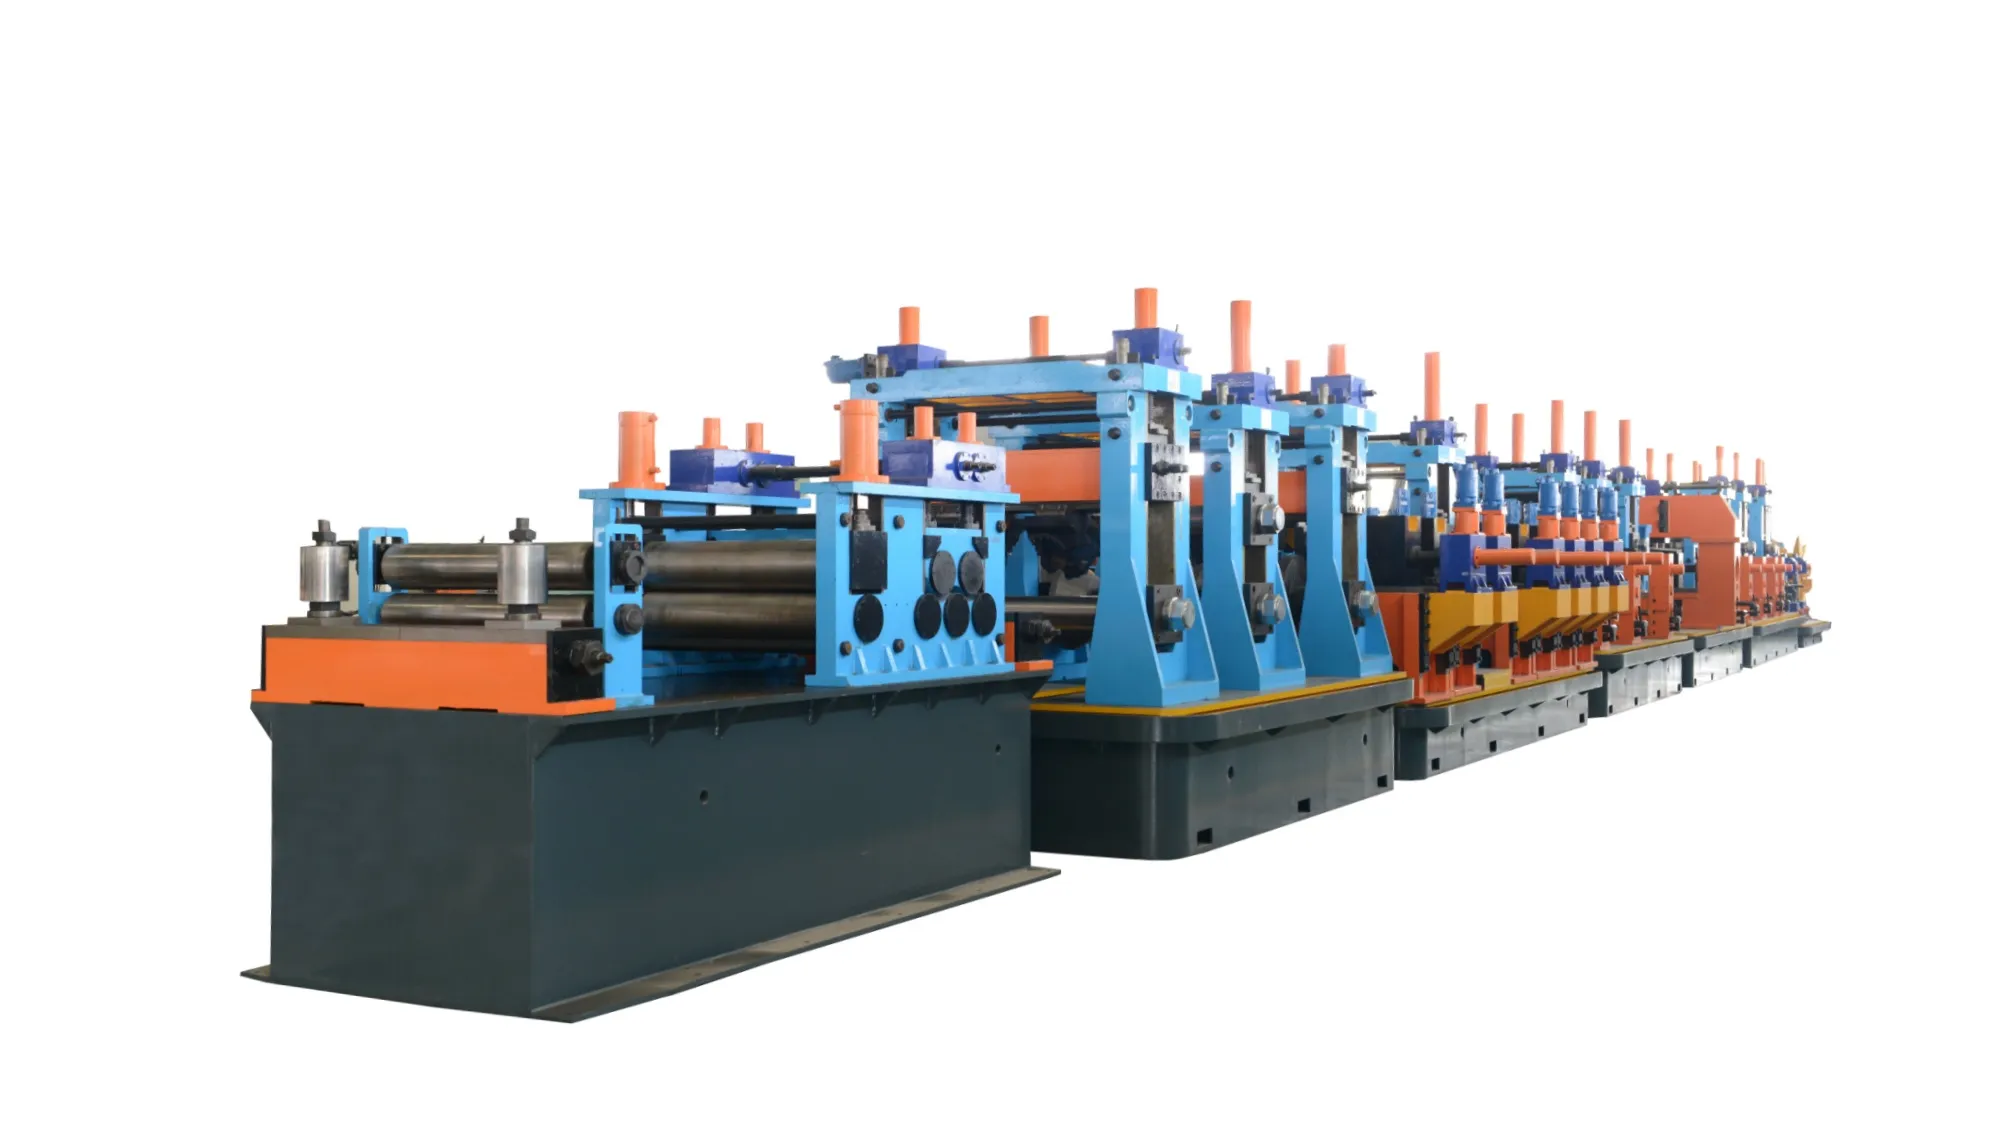 How the Weld Seam Heats: Skin and Proximity EffectThe two heated edges are brought together under pressure from the squeeze rolls and forged into a continuous seam; the result is solid-state or fusion pressure welding.See the line →
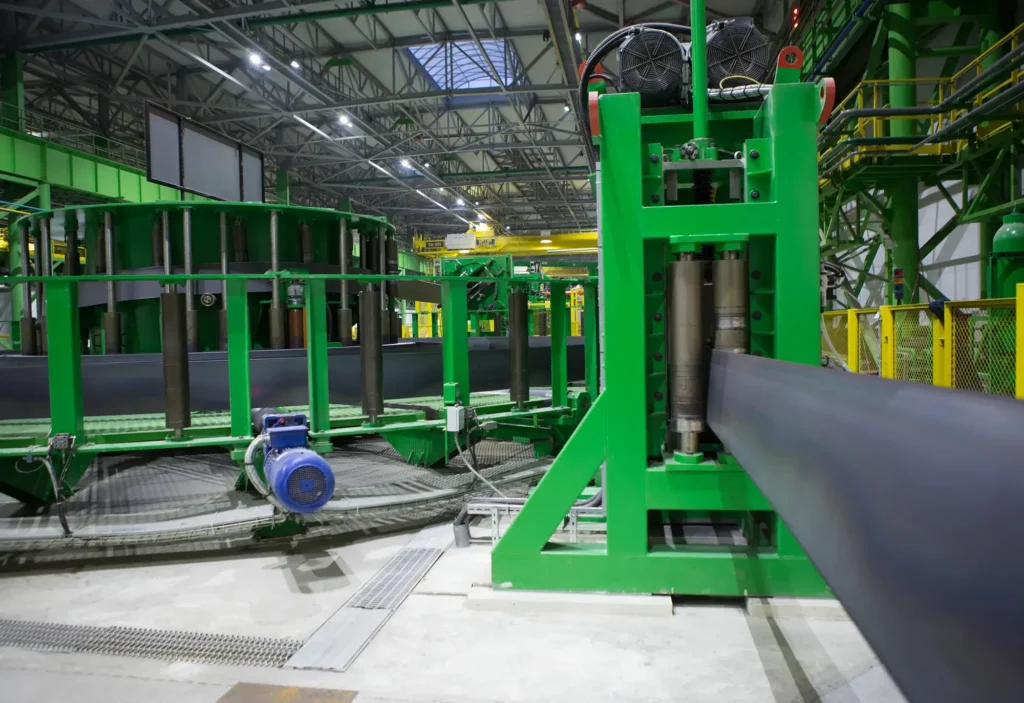 Sizing the Welder to the Pipe DiameterWelder rating on our HF tube mills is stepped with pipe diameter across a range of 150 to 1500 kW.See the line →
That single fact settles several things at once. There is no welding wire on this line and no consumable electrode; the consumables that matter are the impeder and the induction coil, which shape where the current goes.
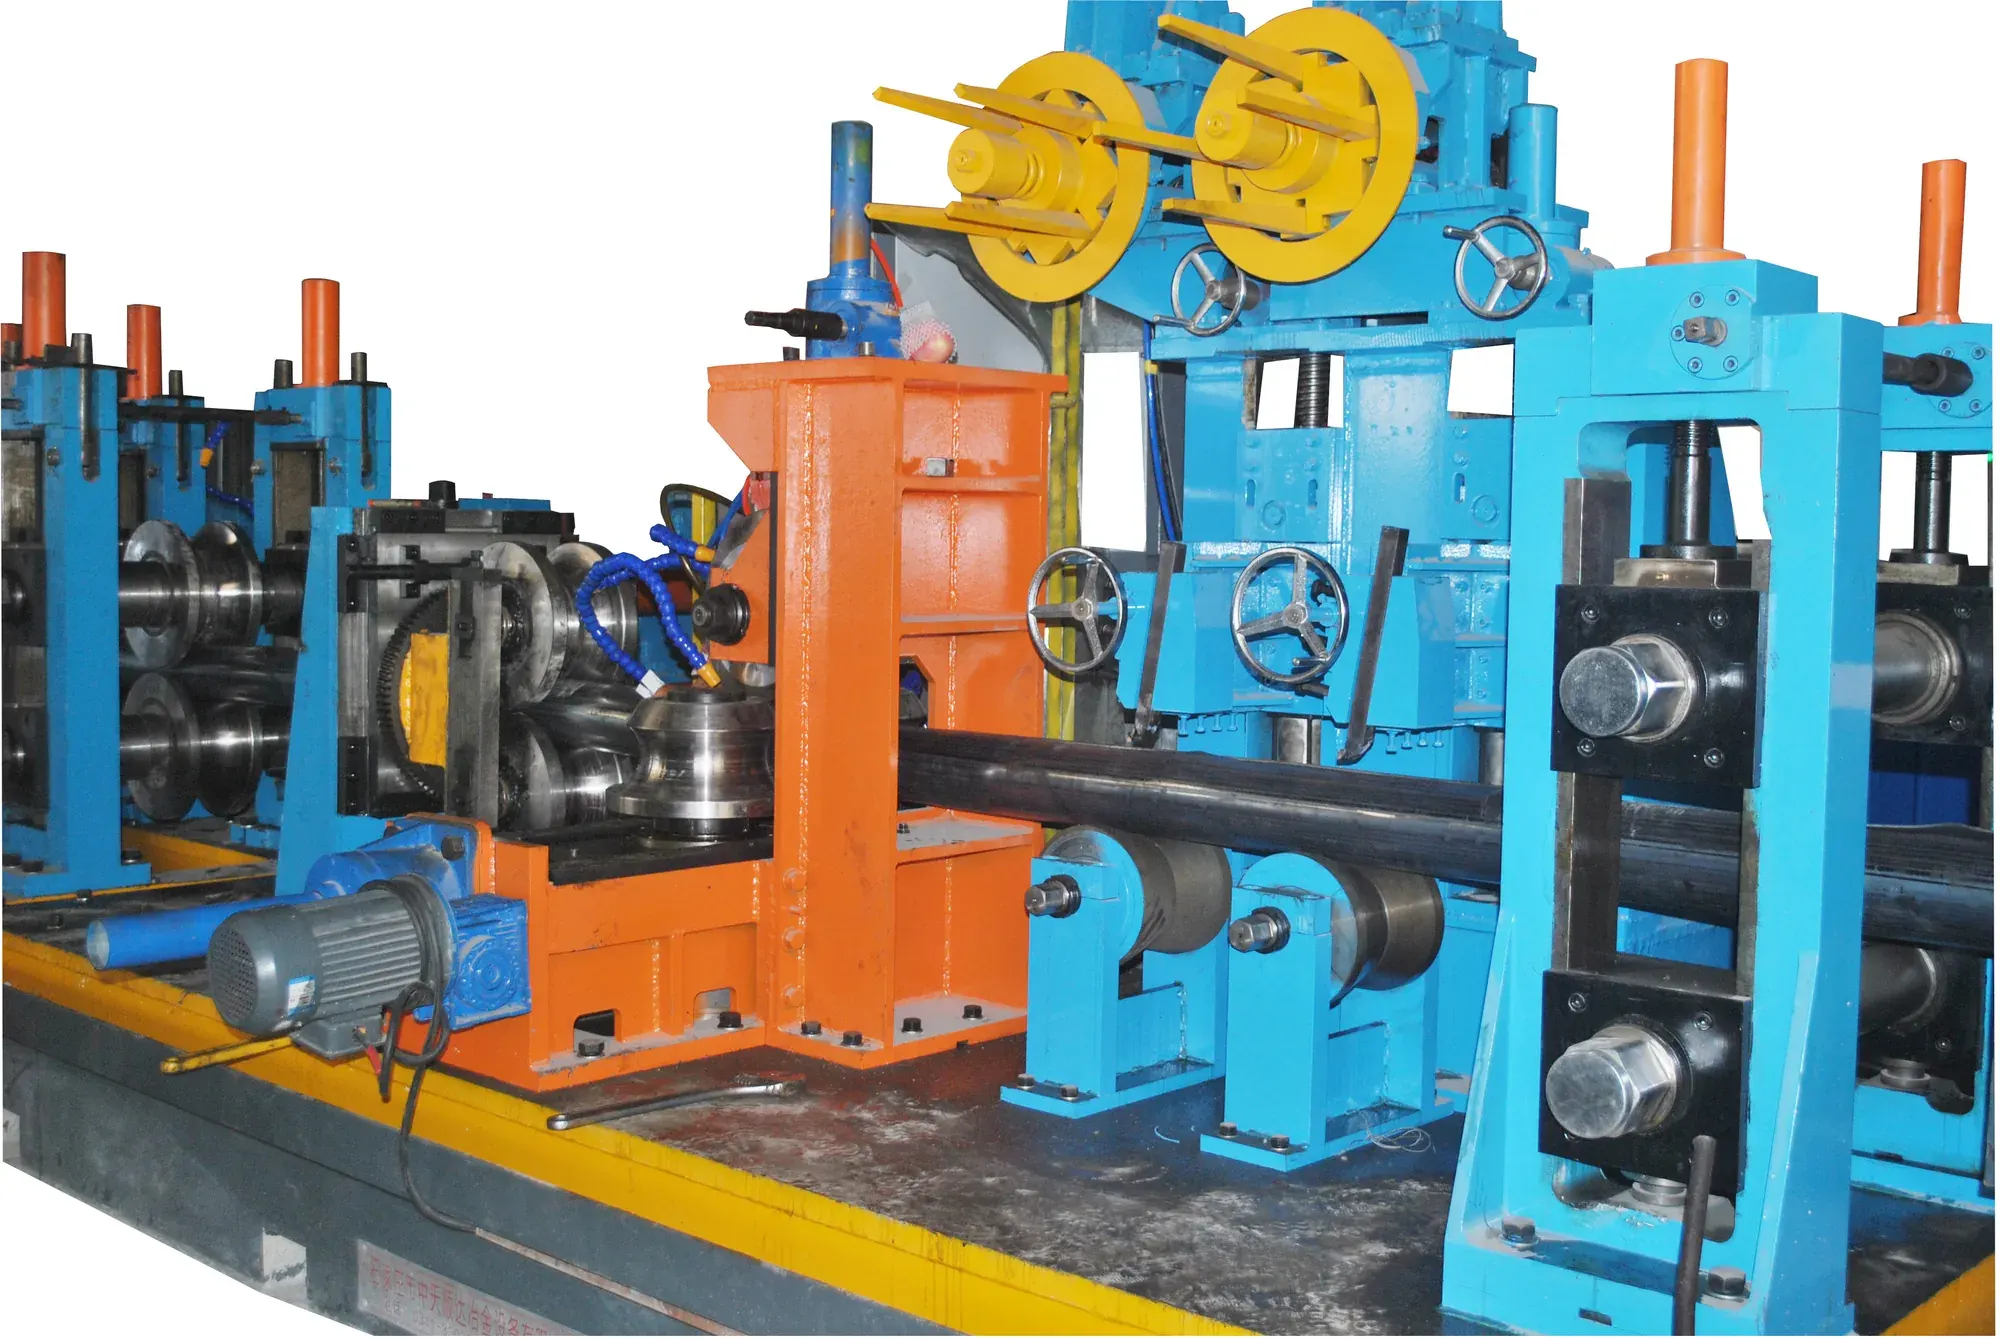
Three Units at the Weld Box: Coil and Impeder, Forming Section, HF Welding Machine
The whole HFW series uses HF induction welding, across all twelve steps from HG32 to HG630.
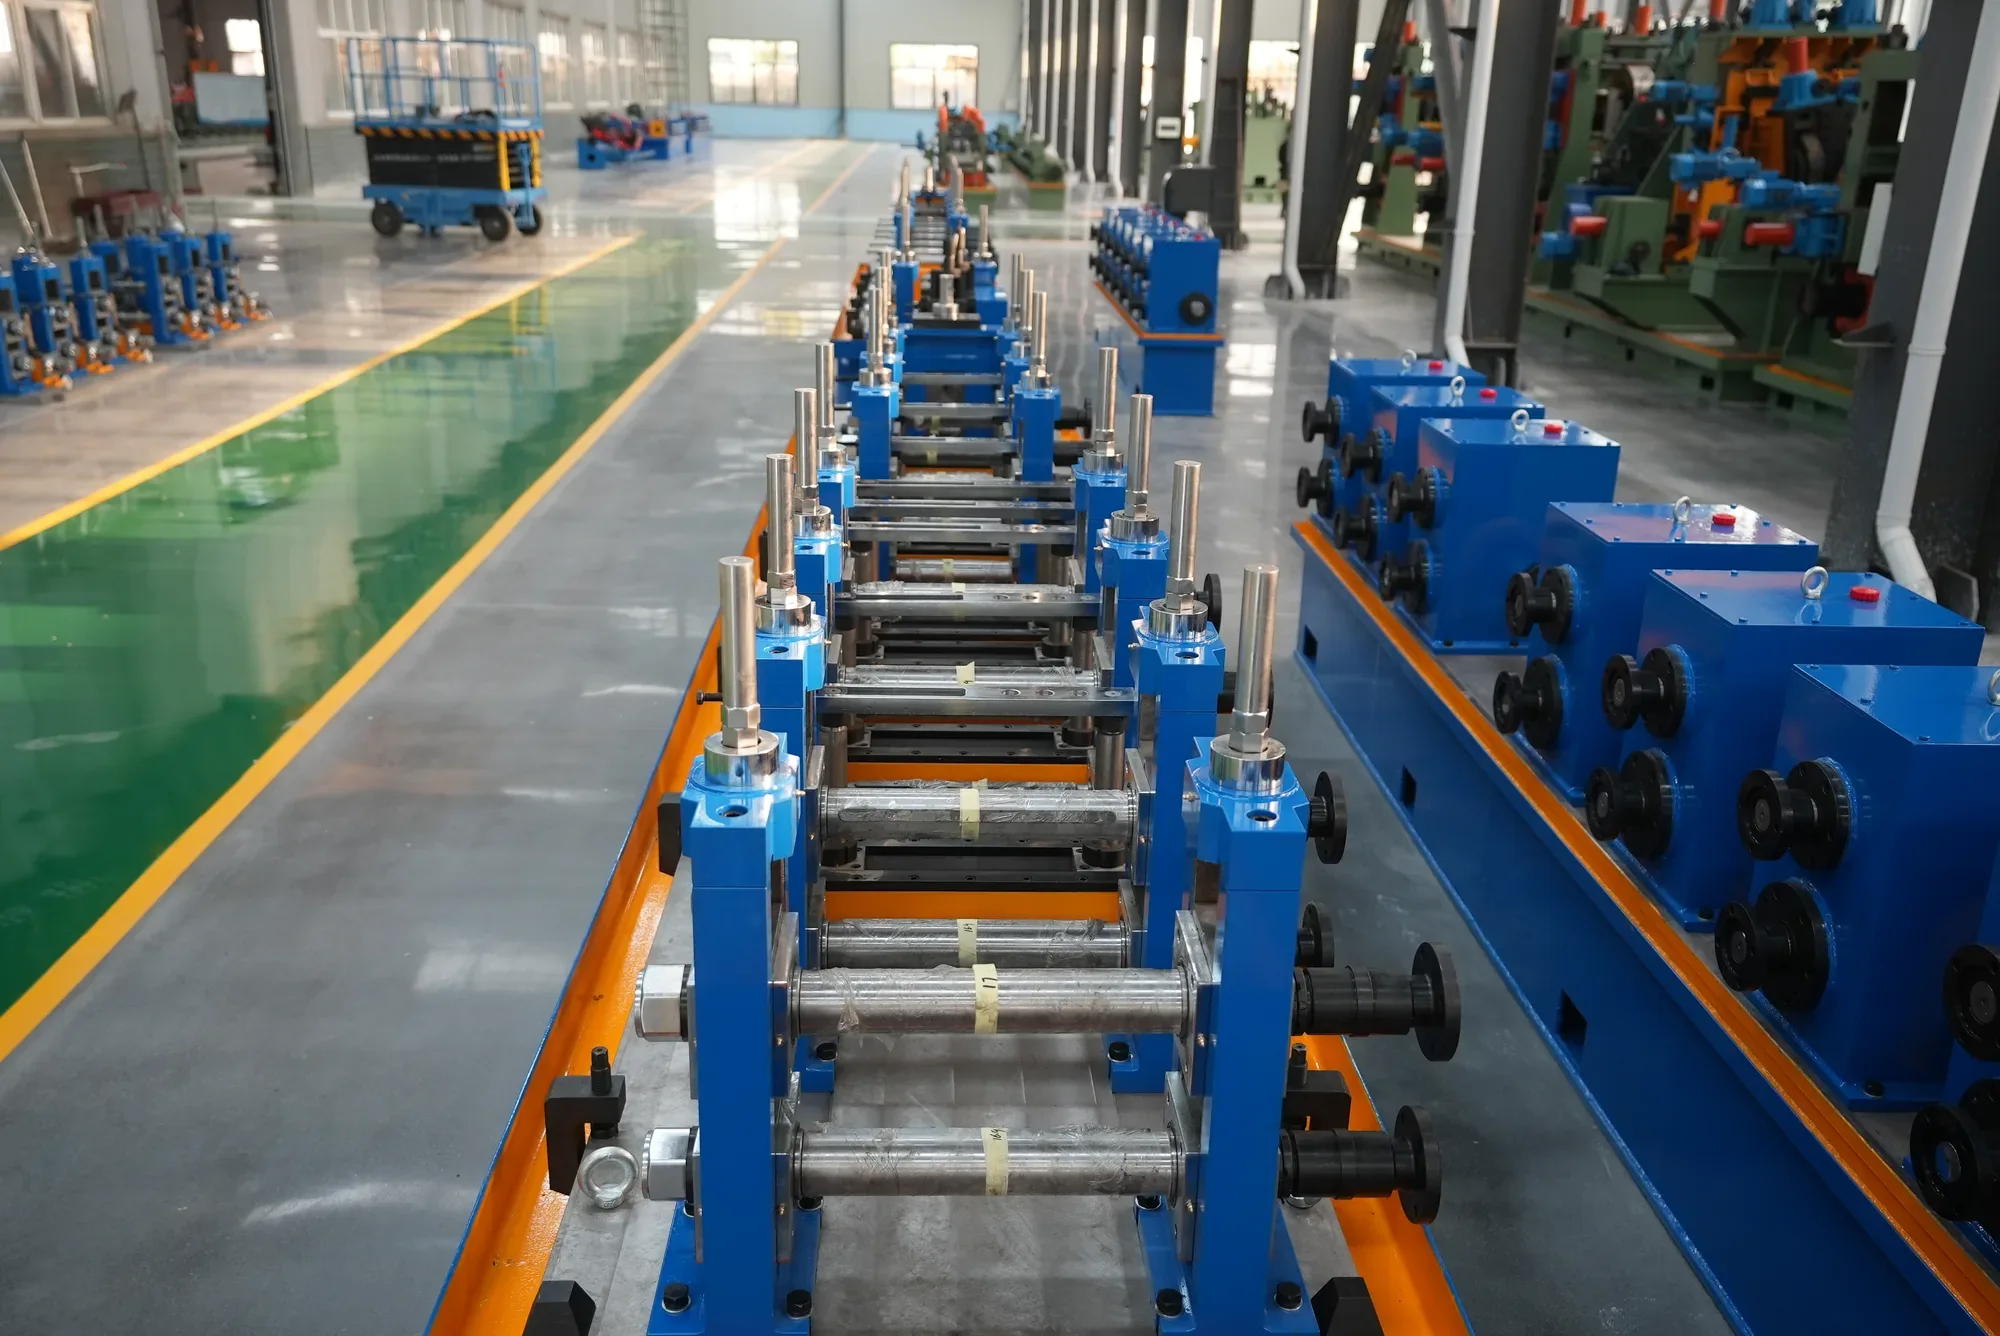
Three units around the weld box decide the result:
The impeder and induction coil concentrate the current at the seam. As they wear, weld energy spreads, seam quality drifts and energy consumption rises — which is why they are treated as wear parts with continuous supply rather than as fixed parts.
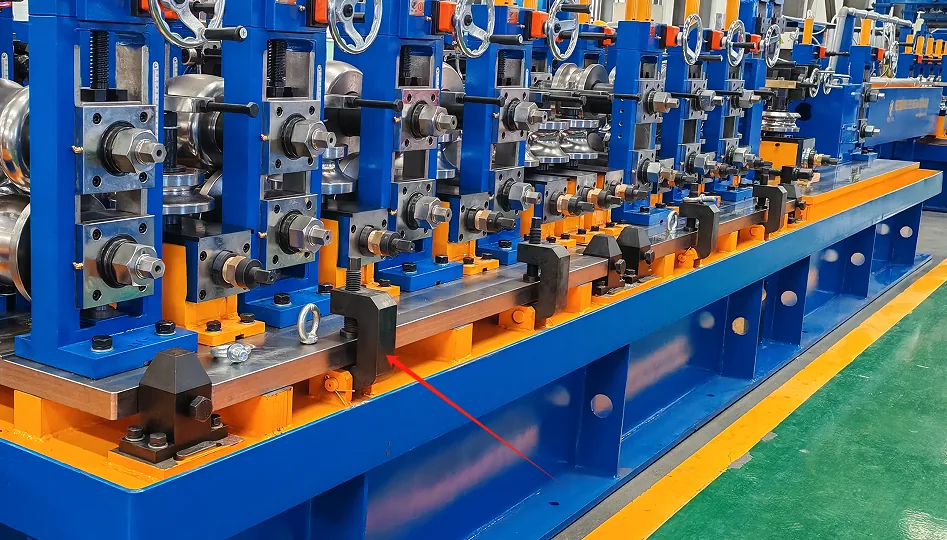
The forming section ahead of the weld box sets whether the edges arrive aligned at all. If the forming passes or roll gaps are set wrong, the open seam is uneven, the pipe shape is off, and the weld goes off-centre no matter what the welder is doing.
The HF welding machine supplies the energy and therefore decides fusion quality and welding speed. Power is matched to the pipe range. If power or frequency is unstable the seam shows lack of fusion, cold welds or burn-through, and the pipe fails pressure and inspection testing.
Key Parameters: Size Range, Wall Thickness and Welder Power Band
- Size range: Φ10–630 mm outside diameter across twelve model steps, HG32 to HG630.
- Process: high-frequency induction welding across the whole series.
- HF welding machine type: solid-state or thyristor.
- Power band: 150 kW to 1500 kW, matched by pipe range.
- The two endpoints: HG32 = 150 kW and HG630 = 1500 kW.
Wall thickness across the series is 0.5–16 mm; per-step windows are available on request.
Forming on these lines uses the W, FFX and FF forming methods. Roll passes are designed in COPRA, the German roll-forming design software, and every pass is checked in COPRA again before the rolls are machined.
How to Choose the Right Model
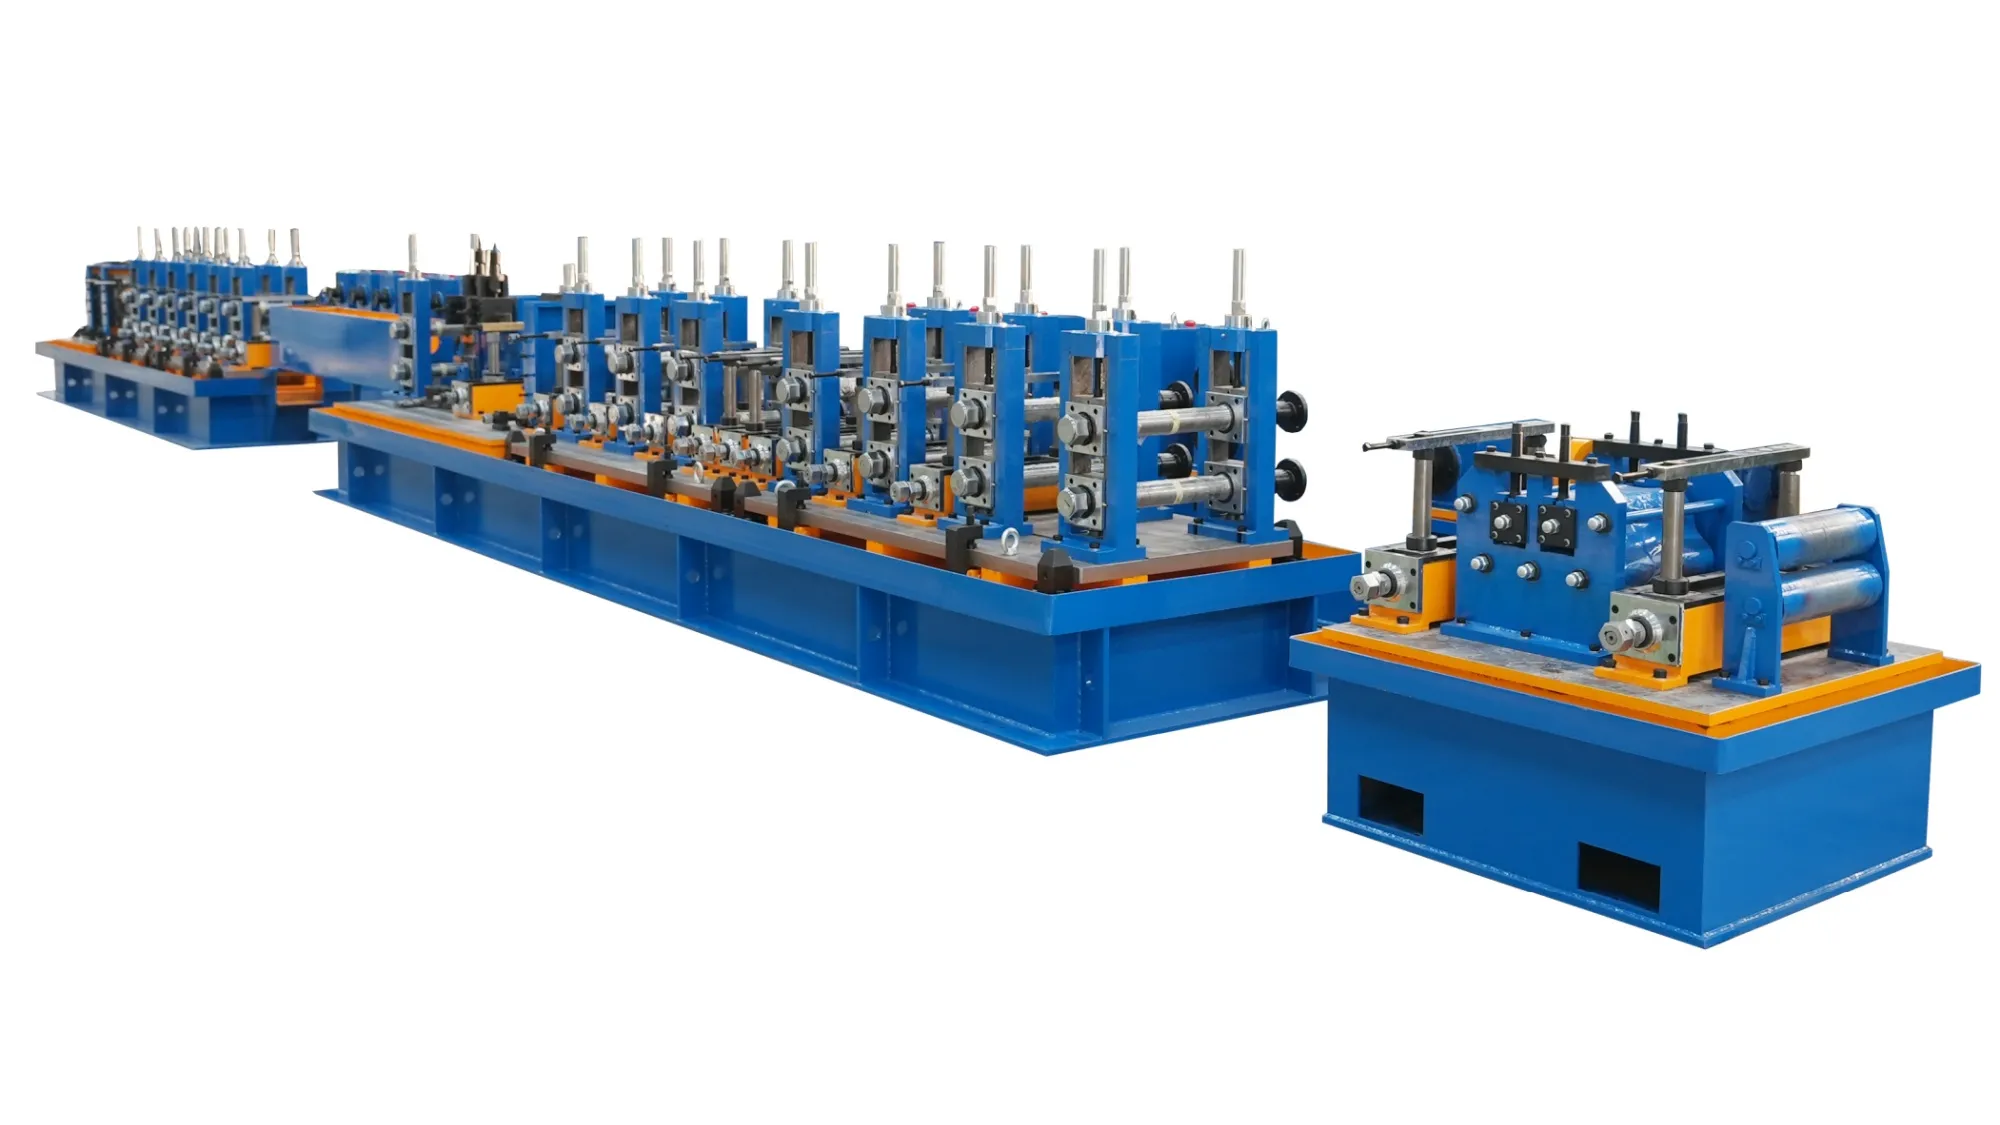
Because power is matched to diameter rather than chosen separately, choosing the model step is what chooses the welder. Read your largest finished diameter against the twelve steps and the power follows from the step.
Where a real decision remains is automation and inspection. Automation changes the grade of the line, not the mill itself. In-line NDT is a different matter: ultrasonic and eddy-current inspection belong to the API line, which adds intermediate annealing, straightening, end facing and hydrostatic testing on top of the tube mill.
Scope of Supply, Installation and Commissioning
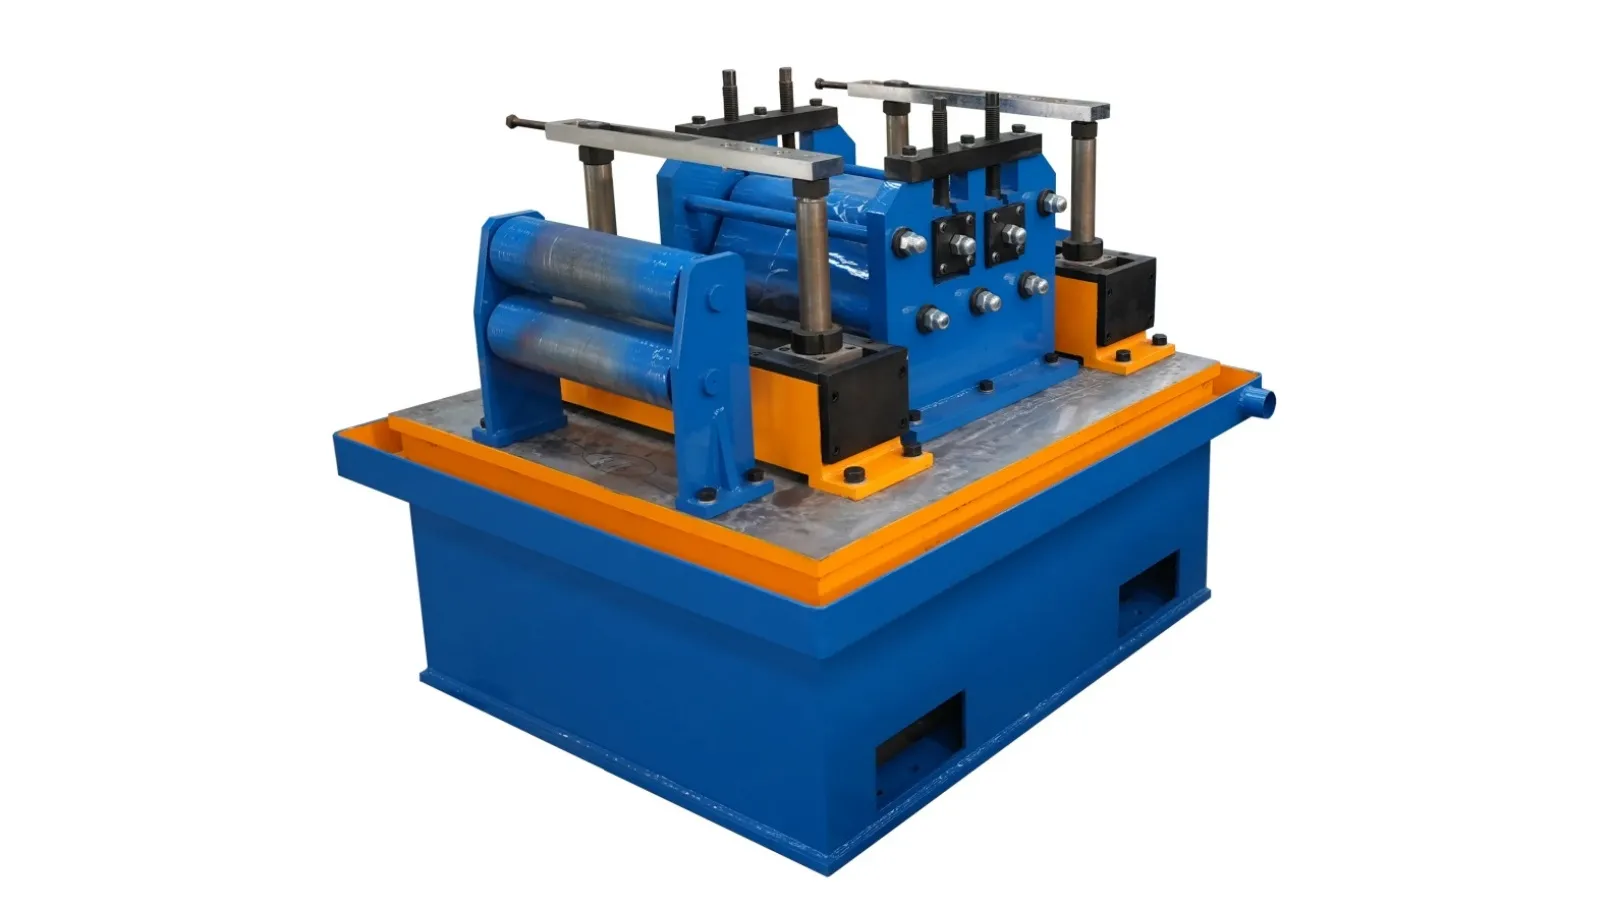
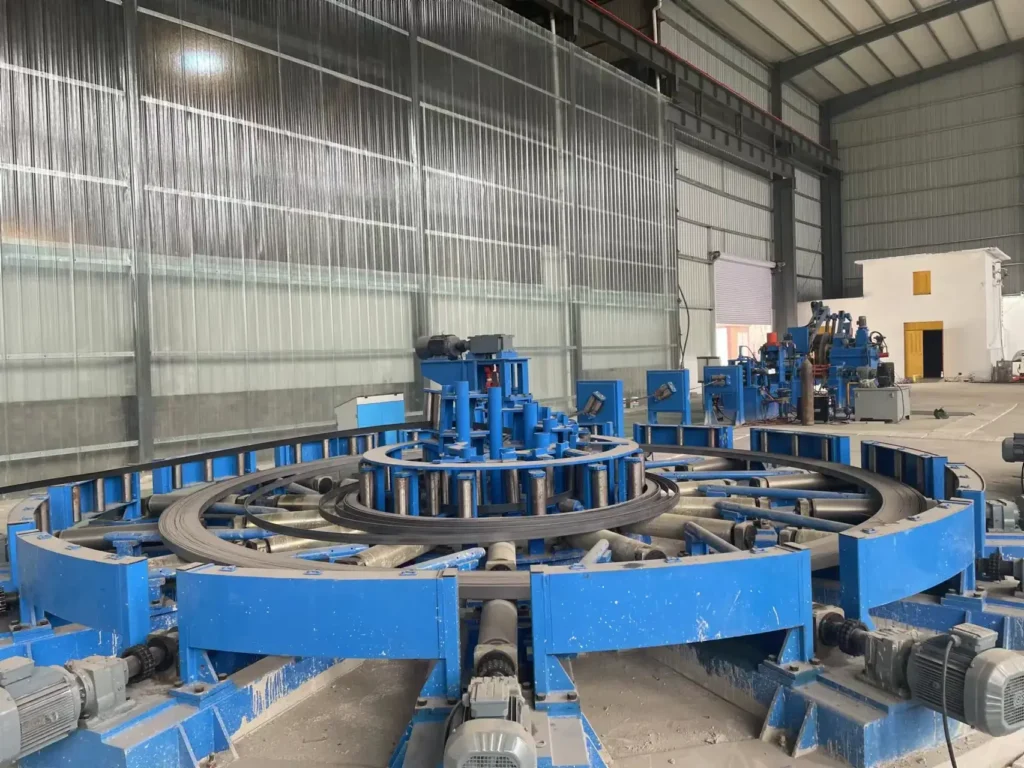
Two units in the line address what can be addressed: the five-roller leveller flattens strip before forming, and the shear-welder plus spiral accumulator keep feed continuous so the forming section is not repeatedly restarted.
The HF welding machine arrives as part of the line, matched to the step, with impeders and induction coils available as ongoing supply.
Responsibility is split clearly. Weld fusion quality is on the equipment side through power matching, seam alignment and squeeze control; strip quality and operating practice are on the buyer’s side. Impeder and coil service lives are available on request.
What goes wrong at the weld box, and where it comes from
Each weld defect can be traced to a specific cause.
Unstable welder power or frequency produces lack of fusion, cold welds or burn-through, and the pipe then fails pressure testing and inspection. Worn impeders or induction coils spread the welding energy instead of concentrating it, so seam quality drifts and energy consumption rises.
Misadjusted forming passes or roll gaps leave the open seam uneven, so the pipe shape is off and the weld goes off-centre before the welder is even involved. Mismatched power, welding speed or squeeze produces the same fusion defects from the process side rather than the equipment side.
That ordering matters when a plant is diagnosing: two of the four causes sit upstream of the weld box, so a seam problem is not automatically a welder problem.
What the strip brings with it
Incoming strip is the buyer’s responsibility, with the line offering levelling and incoming checks rather than correction of grade or flatness. For high-frequency welding, steel strip brings three quality factors on the raw-material side: grade, thickness tolerance and shape.
Automation, and what it does and does not change
On the HG series, control comes as semi-automatic or full PLC; the fully automatic HGF150 is a separate direct-forming line for square and rectangular tube. What PLC and variable-frequency control change is repeatability: line speed and cut length stop being operator-dependent. What they do not change is the physics at the seam.
Power still has to match diameter, edges still have to arrive aligned, and squeeze still has to be right.
Certification, and what each certificate actually covers
ISO 9001 is held under certificate number 18524Q11269R2S, issued by National Standard Integration (Beijing) Certification Co., Ltd. under IAF MLA and CNAS accreditation.
CE certificates are held from UDEM under three separate numbers, and each covers a different line type: welded pipe equipment under M.2022.206.C72171, cold roll forming equipment under M.2022.206.C72172, and slitting lines under M.2022.206.C72173. A fourth CE certificate for cold forming is held from Ente Certificazione Macchine in Italy under 0P250616.HTWTT37.
Each number can be checked at the issuing body rather than taken on trust, which is why each certificate is listed with its number and the route to verify it.
An enterprise standard, Q/GYL TT01-2023 for HGF150 high-frequency welded pipe equipment, is published on the national enterprise-standard platform. High-Tech Enterprise certificate GR202413001148 is held. The Madrid international trademark for TENGTIAN is registered under number 1 707 606. The patent portfolio is 30 granted utility model patents, with 7 invention patents applied for.
Delivery, payment and after-sales
Lines are dismantled into units and shipped in containers: heavy frames braced bare on cradles with designated lifting points and rust protection, precision and wear items in moisture-protected wooden cases with a spare-parts pack. Standard lines ship within 90 working days of the deposit.
Installation and commissioning are guided on site by our engineers, with online support; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance. Our after-sales team handles enquiries. Payment is 30% by T/T on signing, 65% by T/T before shipment and 5% after installation and commissioning, or L/C at sight; prices are quoted ex-works (EXW).
Anonymised reference deliveries
Our lines have gone to 25 countries — most make construction tube, and others run fire-extinguisher tube, furniture tube and other sections. Commissioning dates are available on request.
The five operating steps where the welder is involved
The line has five operating steps, and three of them touch the weld directly.
Loading and threading: the coil car feeds, the uncoiler tensions, and the operator guides the strip head through levelling into the mill. Training is required.
Shear-weld coil joining: before a coil runs out, head and tail are cut and joined, coordinated with the accumulator so the mill does not stop. Training is required, because a poor joint means a broken strip and scrap.
Setting the size and changing tooling: the line is set to the target diameter — a conventional line changes rolls, a direct-forming line adjusts servos without changing rolls. The tooling-change crew needs training, because a poor setup means shape drift and scrap.
Setting and running weld parameters: set welder power and welding speed, then start and monitor the continuous forming, welding and sizing sequence. Operating and process training is required, because errors here cause lack of fusion, burn-through and dimensional drift.
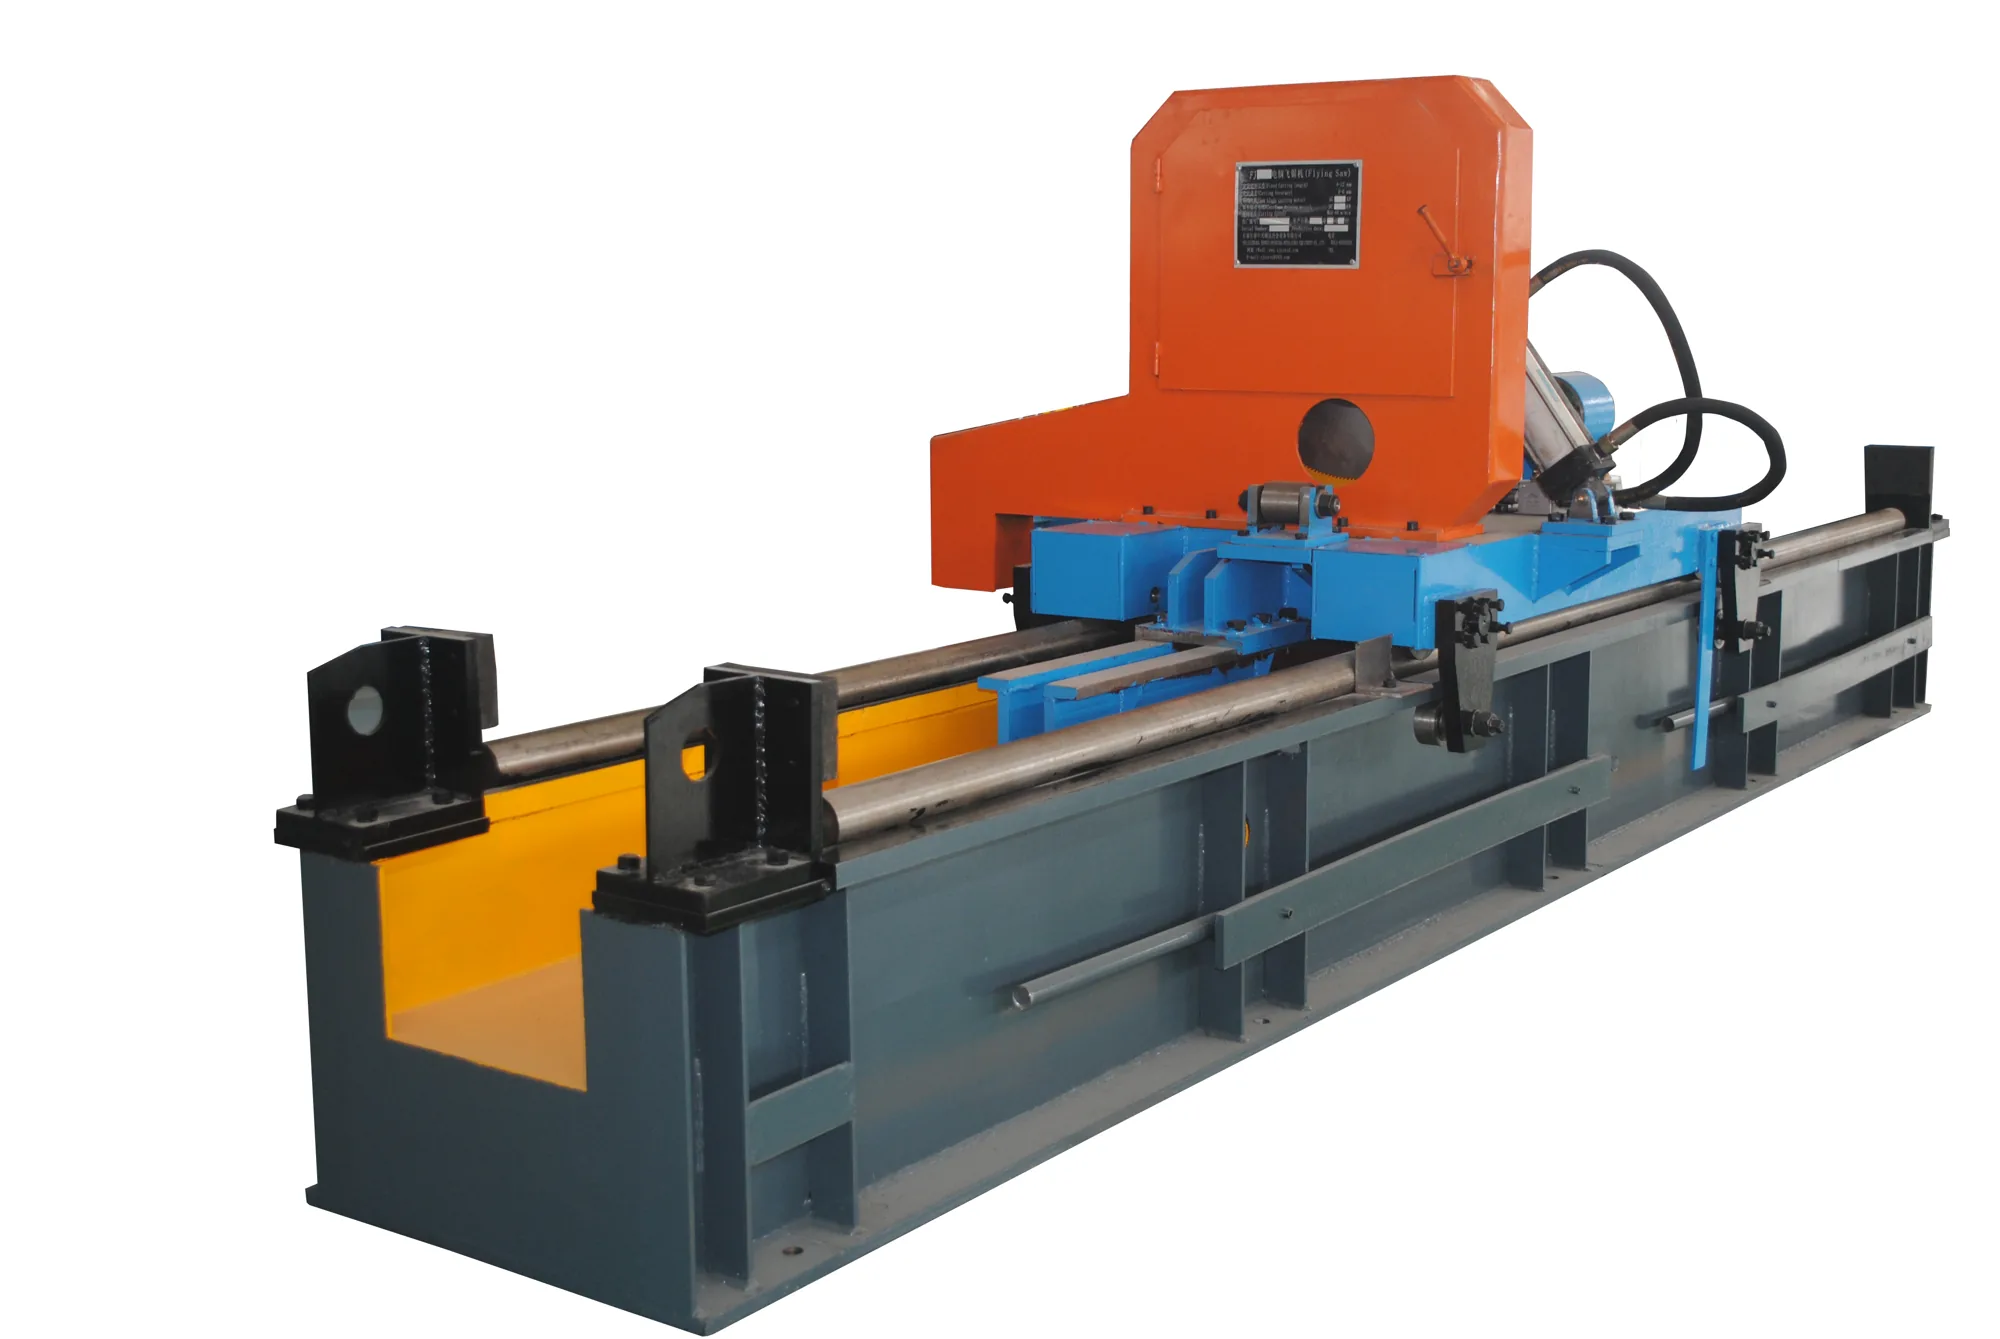
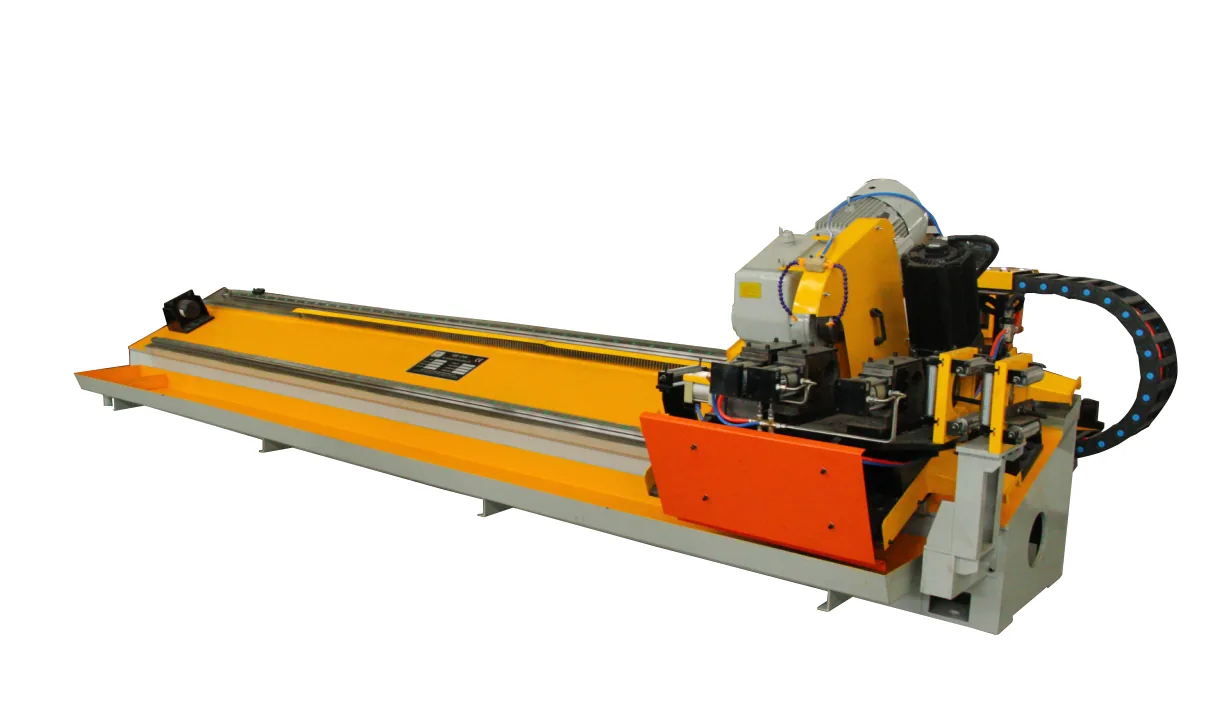
Cutting and collecting: the flying saw cuts to the set length and the run-out table collects the pipe. Routine operation.
Post-weld cooling, and why it belongs here
Post-weld cooling is its own quality factor: it stabilises the seam structure and has to be matched to welding speed. When it is not, the outcome is poor seam structure and distortion. The cooling medium — water or emulsion — is a process medium: we give the specification, the plant sources it locally.
That pairing is worth spelling out because it is where a plant most often looks last: a seam problem that survives power and alignment checks is often a cooling-versus-speed mismatch rather than a welder fault.
What the API line adds, and what it does not change
The API configuration adds medium-frequency annealing, straightening, end facing, hydrostatic testing, ultrasonic and eddy-current inspection on top of the tube mill. What it does not change is the welding process itself — it is the same high-frequency weld, with post-weld treatment and inspection added around it.
What to send when you enquire about the welder
The step, the wall thickness, the steel grade and the welding speed you expect to run. Power is matched to the pipe range, but power, frequency and welding speed together are what set fusion, so a power number on its own does not answer the question.
From the Workshop
 H-Beam Production Line
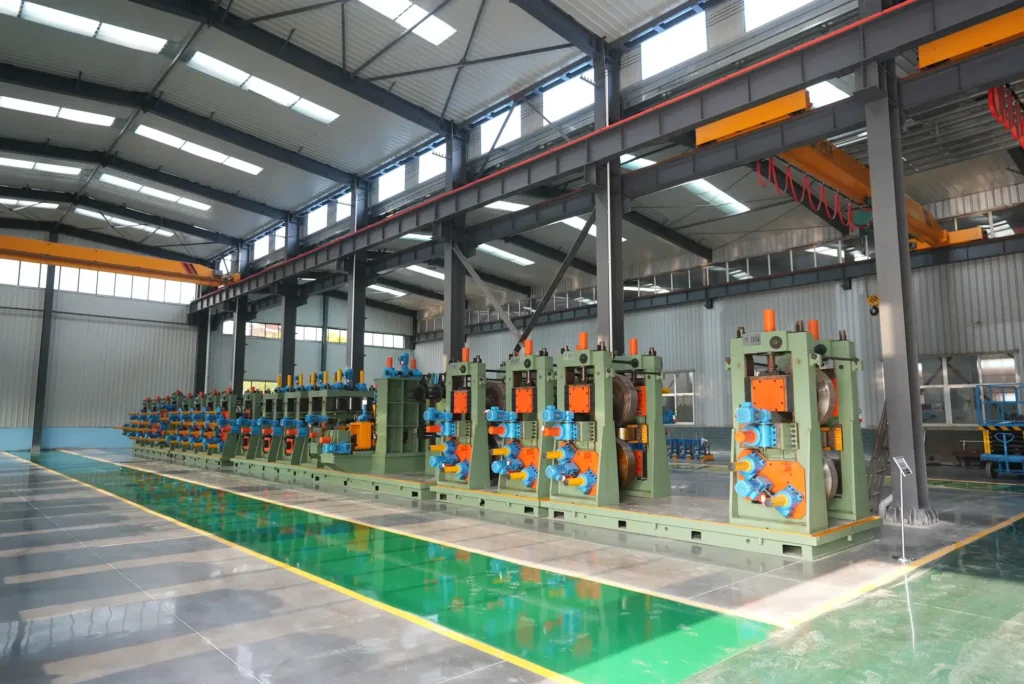 Direct Forming Square Tube Mill
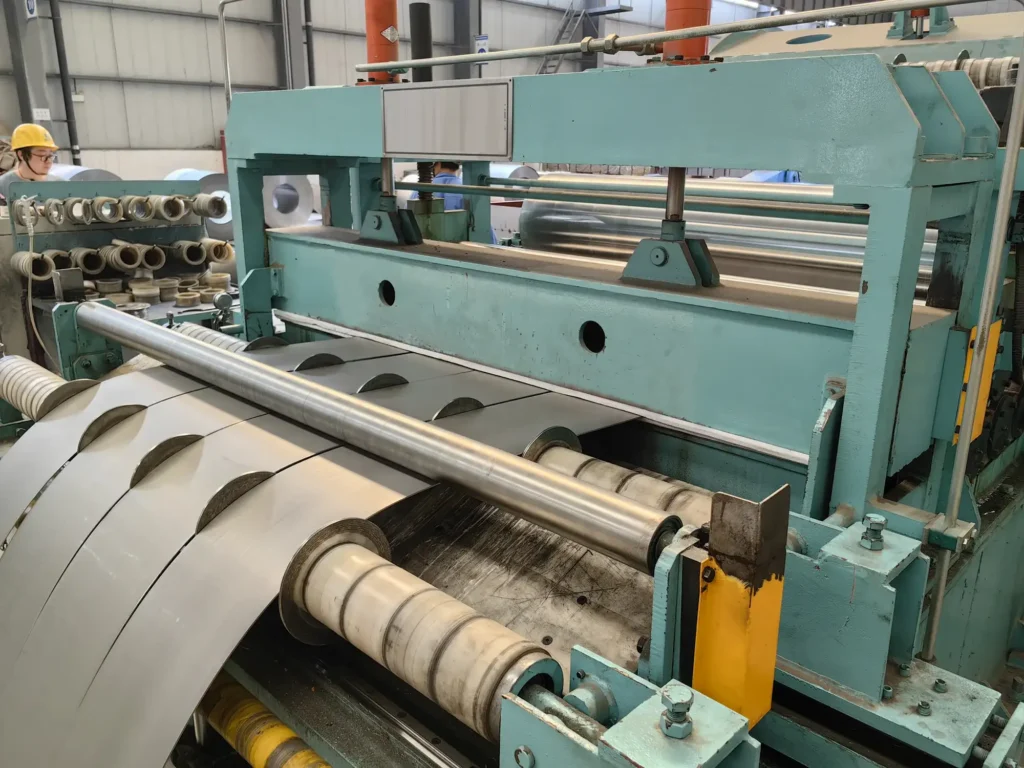 Cut-to-Length Line
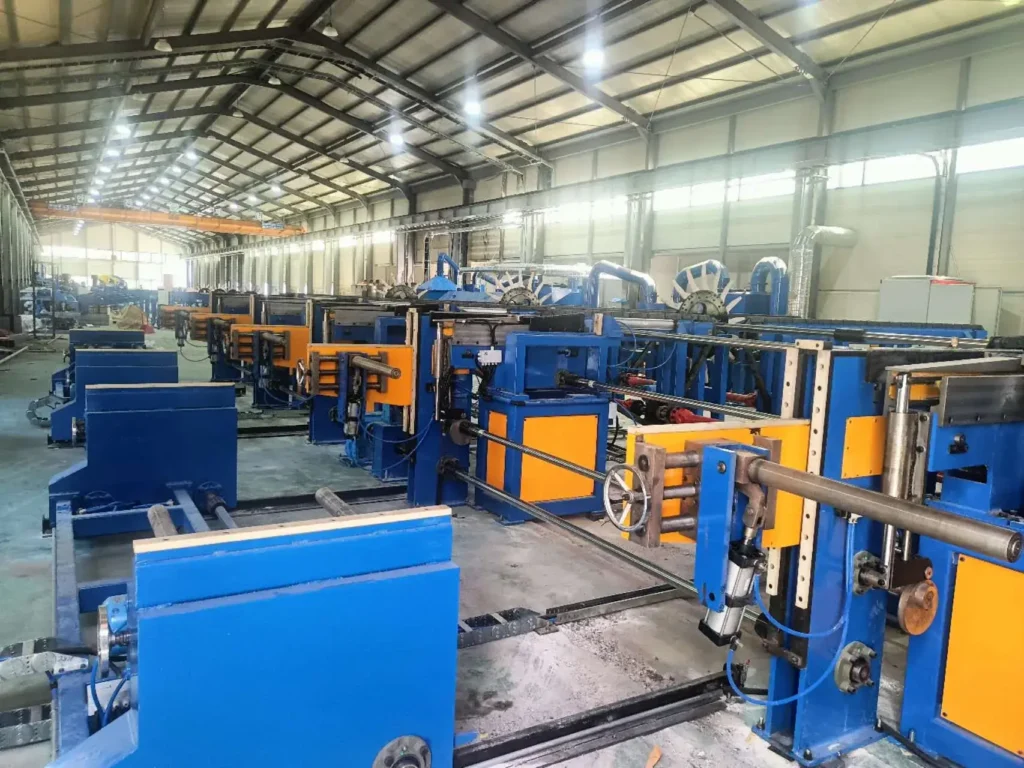 Auto Spray Paint Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.