
Home › Pipe Production Applications › Oil & Gas Line Pipe Mill
Which line pipe mill makes oil and gas transmission pipe, from Φ114 mm on an API-configured HFW line up to Φ1620 mm on a spiral line.
In This Line
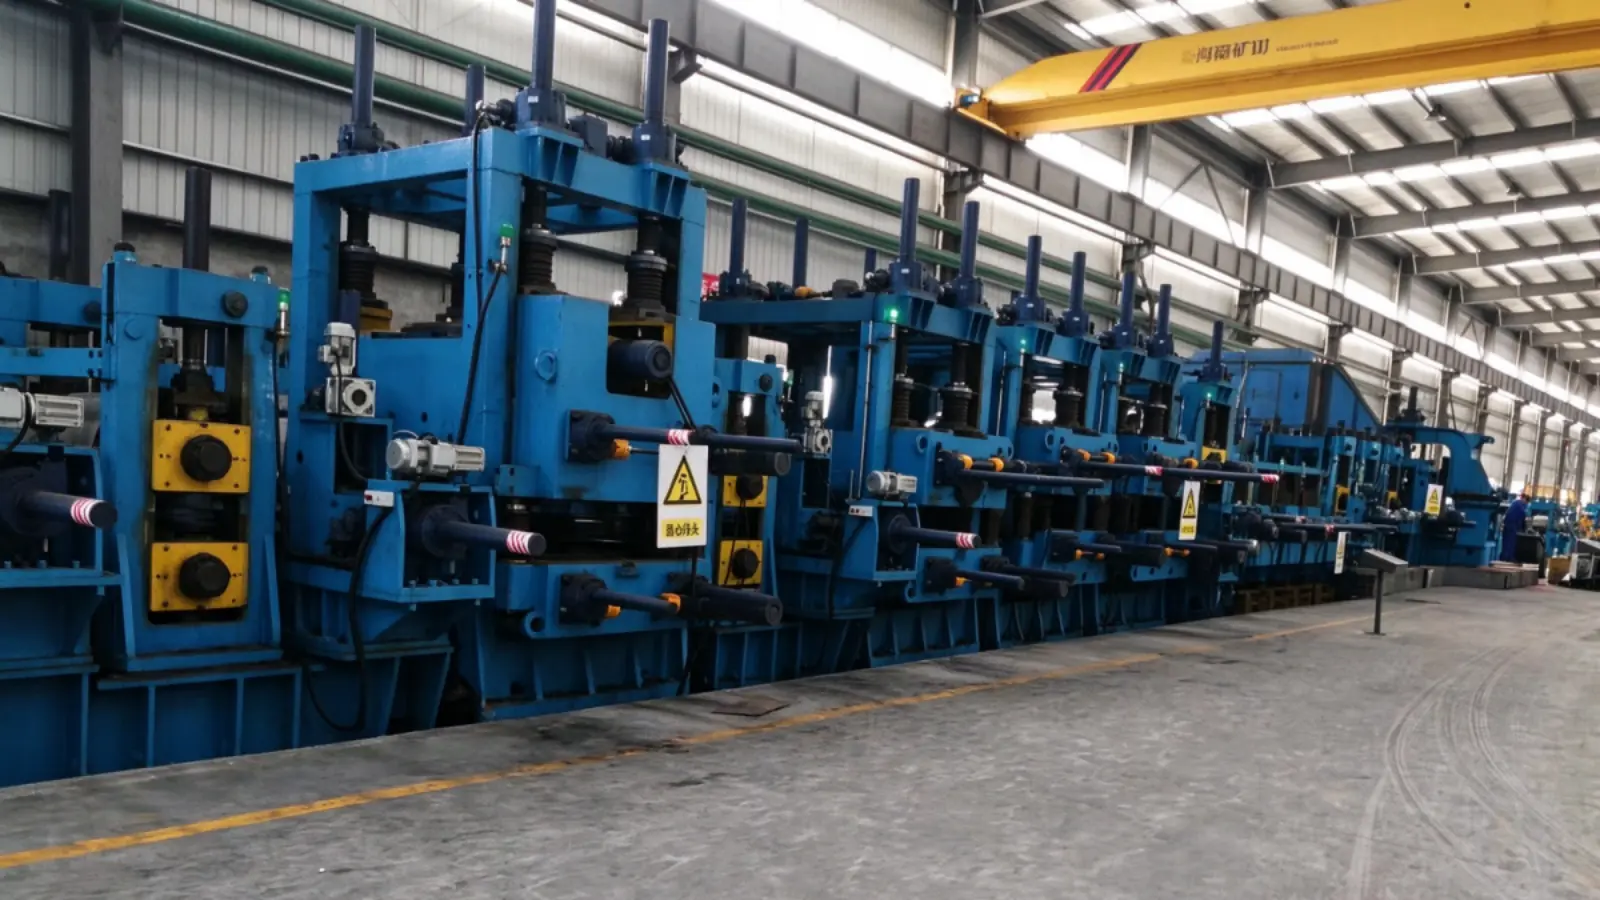
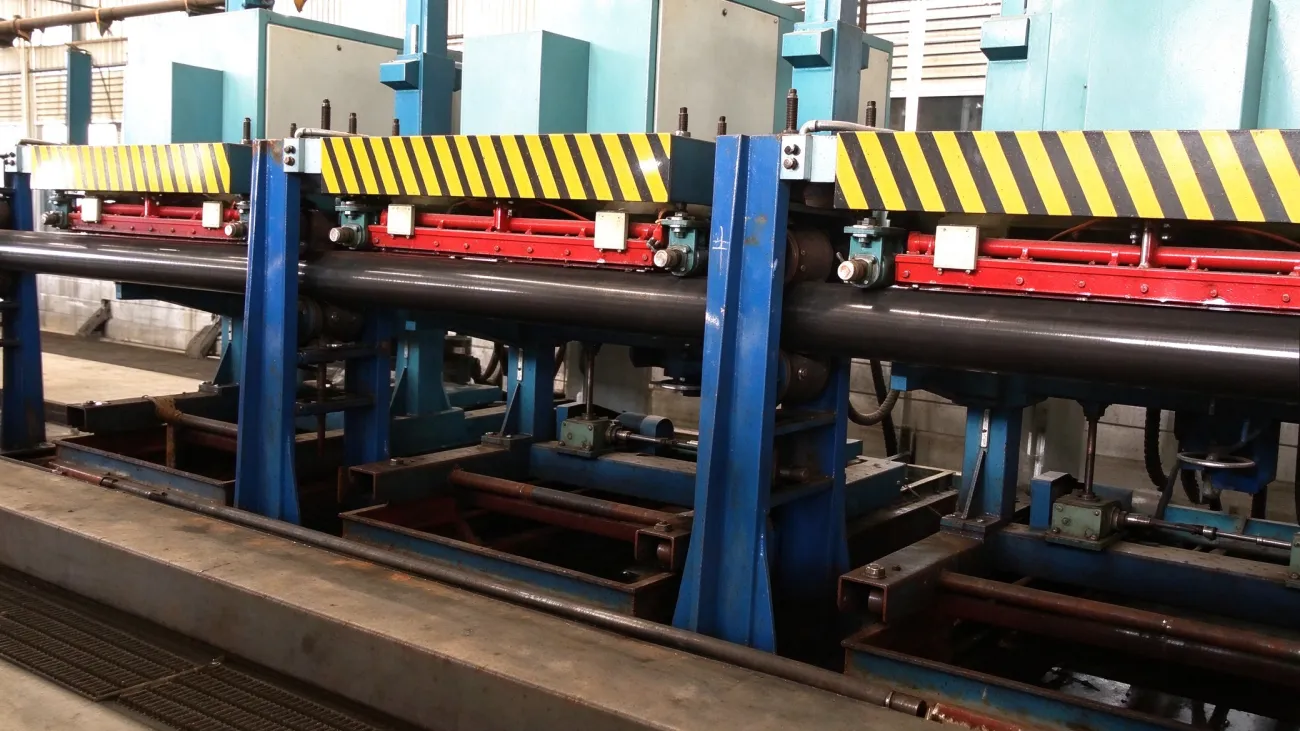
On the HFW-API route, annealing, hydrostatic testing, ultrasonic and eddy-current inspection are stations on the line, not a separate laboratory.
What Is Oil & Gas Line Pipe Production
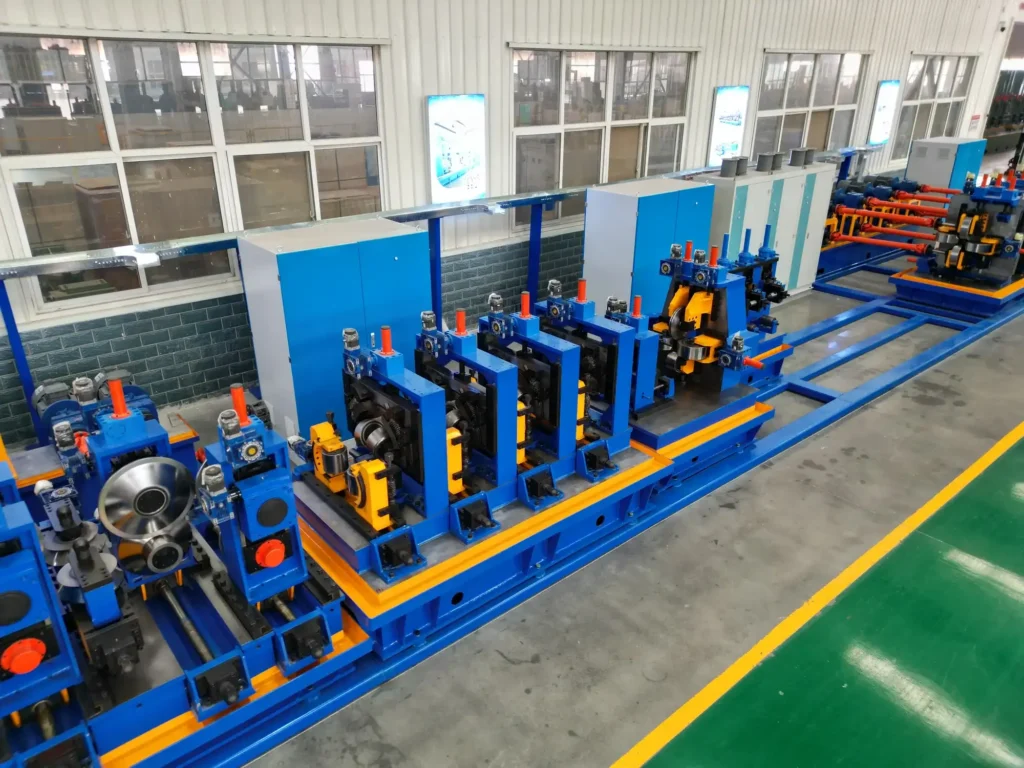
An oil and gas line pipe mill is a welded pipe line with a compliance chain attached: the same forming and welding as a standard mill, plus medium-frequency annealing, straightening, end facing, hydrostatic testing, ultrasonic and eddy-current inspection. For larger diameters, an oil and gas pipe mill is a spiral line instead, with X-ray, hydrostatic and ultrasonic stations.
Annealing comes first and is metallurgical rather than dimensional. High-frequency welding leaves the weld zone harder and less tough than the parent material; medium-frequency heating followed by natural cooling improves the structure and toughness of the seam and its heat-affected zone, which is why annealing is part of the line rather than an option.
The inspection stations run in line, testing seam and pipe body as the pipe is produced, so the result is traceable pipe by pipe. How the stations are set up is covered under the API pipe mill inspection chain.
Straightening and end facing follow, and they are what make the pipe usable on a pipeline rather than merely sound. A pipe that is metallurgically perfect but bowed, or square-cut but not bevelled, cannot be laid and welded in the field.
Then the three inspection stations, and their order is not arbitrary. Hydrostatic testing proves pressure integrity of body and seam under internal pressure. Ultrasonic inspection finds internal discontinuities the pressure test would not reveal. Eddy-current inspection covers surface and near-surface defects that ultrasonic is poorly placed to see.
Target Pipe Sizes and Wall Thickness for This Application
Line pipe for oil and gas spans a diameter range no single welding technology covers, so this application is served by two mill routes: our API line pipe mill and our SSAW spiral welded pipe mill.
HFW route with API post-weld chain — API 219 / 406 / 426 / 508 models, outside diameter Φ114–508 mm, wall 3–20 mm across the four models, pipe length 4–6 m.
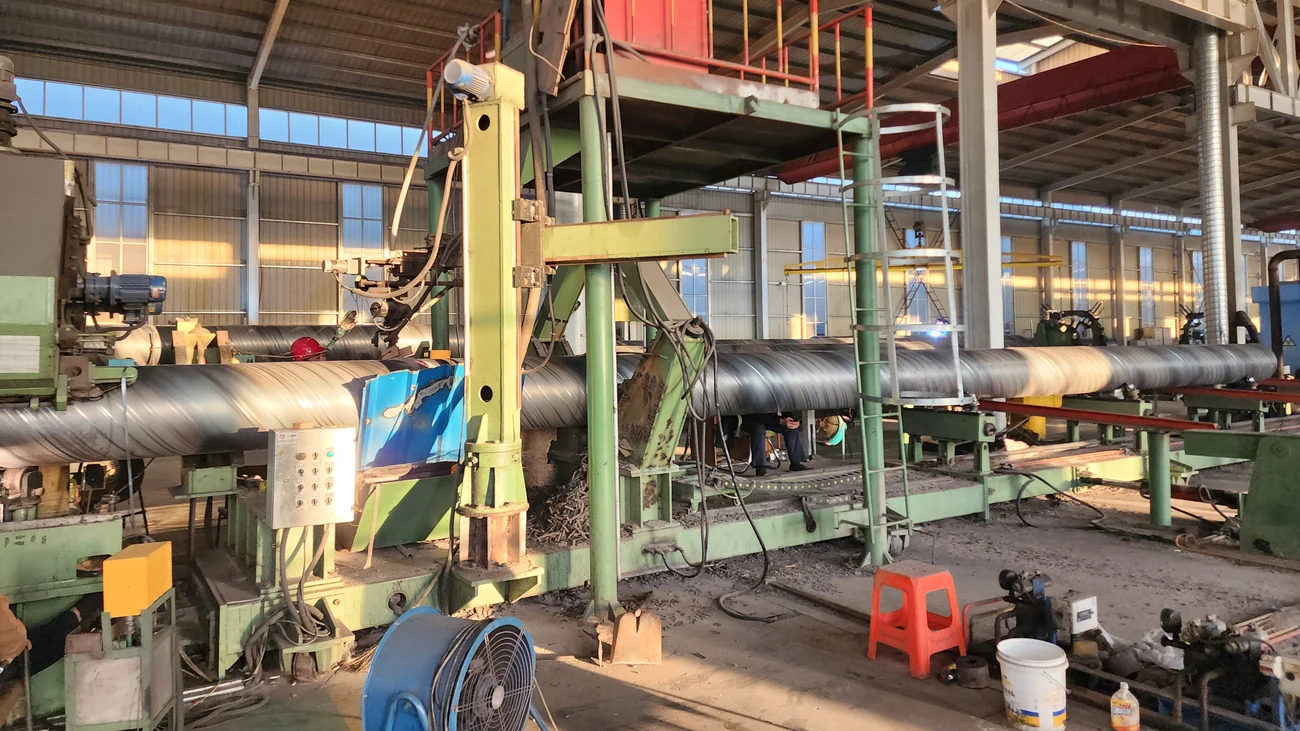
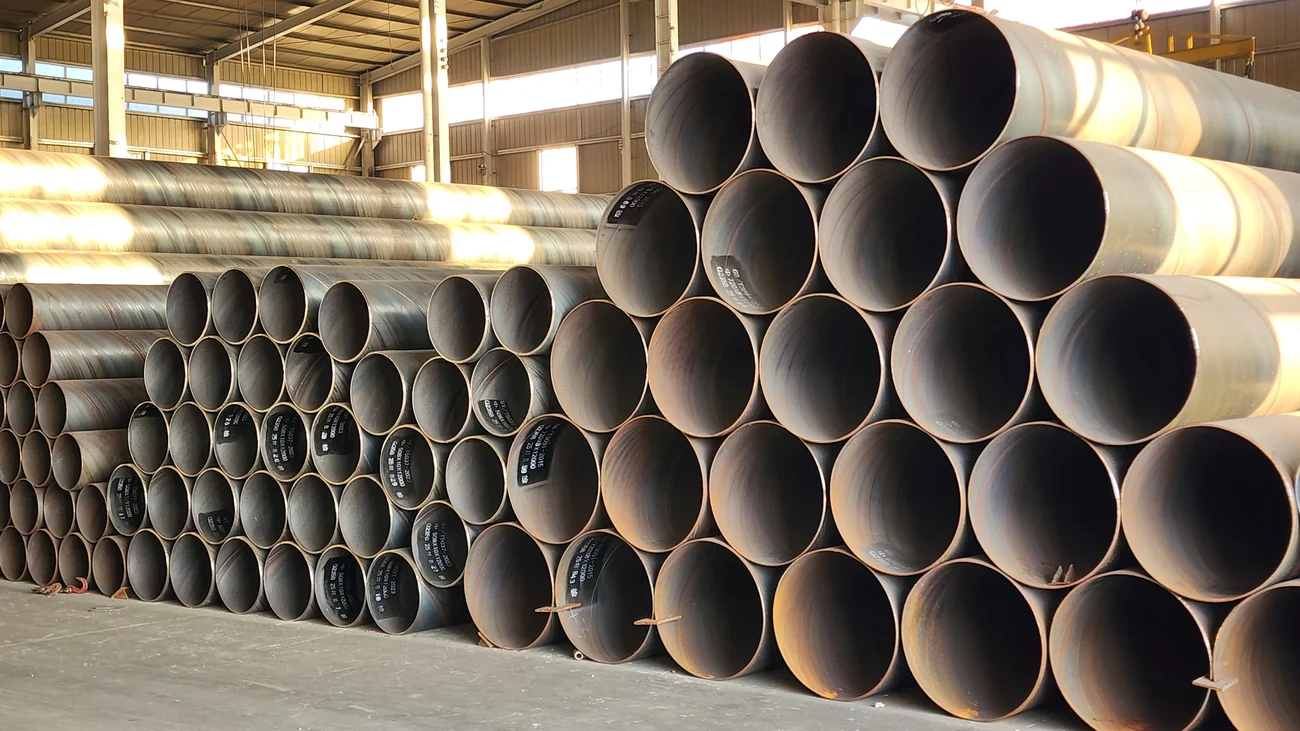
Spiral submerged-arc route — two classes, Φ219–820 mm × 3–12 mm and Φ219–1620 mm × 5–16 mm, pipe 8–12 m, single-pipe weight to 7.5 t. Diameter is changed by forming angle (39°–80°) rather than by roll change.
Both spiral classes list oil and gas pipelines among their uses. The Φ1620 class adds API SPEC 5L to GB/T 9711 and runs X-ray, hydrostatic testing and off-line ultrasonic on every pipe.
Wall thickness is where the two routes diverge most sharply. The HFW-API route carries 3–20 mm across its four models, at diameters up to Φ508 mm. The spiral route carries 3–12 mm on the Φ820 class and 5–16 mm on the Φ1620 class, across a much wider diameter band.
So a requirement for heavy wall at moderate diameter points one way, and thin-to-medium wall at large diameter points the other.
Pipe length and handling matter more on line pipe than on general tube, because the pipe is laid rather than cut down. On the spiral route pipe is produced at 8–12 m with single-pipe weight to 7.5 t on the Φ1620 class — figures that decide site handling equipment before they decide anything about the mill.
| Route and class | Outside diameter | Wall thickness | Also covered |
|---|---|---|---|
| HFW, API models 219 / 406 / 426 / 508 | Φ114–508 mm | 3–20 mm | Post-weld annealing, hydrostatic, ultrasonic and eddy-current as line stations; pipe length 4–6 m |
| Spiral submerged-arc, class 1 | Φ219–820 mm | 3–12 mm | Pipe length 8–12 m |
| Spiral submerged-arc, class 2 | Φ219–1620 mm | 5–16 mm | Single-pipe weight to 7.5 t; diameter set by forming angle 39°–80° |
Mill Model and Welder Power Band
Above Φ508 mm the HFW-API route runs out and the spiral route is what makes the pipe. Which route fits is decided by the largest diameter the plant intends to sell, then by wall thickness, then by the standard the finished pipe must satisfy.
Batch size deserves its own line here because the two routes behave differently under it. The spiral route is discontinuous — pipe by pipe, at 0.5–3 m/min welding speed — which suits large diameter in medium batches. The high-frequency route is continuous, running across coil changes without stopping, which suits volume in a narrower diameter band.
For a line-pipe project measured in kilometres of a single specification, that difference usually decides more than diameter does.
The standard the finished pipe must satisfy is the third input, and on this application it is often the first one the buyer states. The spiral Φ1620 class is built against GB/T 9711 and API SPEC 5L; the Φ820 class against GB/T 9711 and GB/T 5037; the HFW-API route against API 5L.
On the HFW-API route the high-frequency welder is 600 kW on the API 219, 406 and 426 models and 1000 kW on the API 508, with medium-frequency annealing of 600 or 1000 kW depending on the model. The spiral route welds by submerged arc, so it has no high-frequency welder rating.
Between Φ219 and Φ508 mm both routes can make the pipe, and the decision moves to wall, batch size and which inspection chain the buyer’s specification names.
Applicable Standards and Inspection Requirements
| HFW-API route | Spiral (SSAW) route | |
|---|---|---|
| Diameter × wall | Φ114–508 mm × 3–20 mm | Φ219–820 mm × 3–12 mm (Φ820 class); Φ219–1620 mm × 5–16 mm (Φ1620 class) |
| Model classes | API 219 / 406 / 426 / 508 | Φ820 class and Φ1620 class |
| Post-weld treatment | Medium-frequency annealing + straightening + end facing | Weld repair + end facing / bevelling |
| Inspection chain | Hydrostatic + UT + ECT, in line | X-ray + hydrostatic + off-line ultrasonic |
| X-ray capability | — (not on this route) | 225 kV / 8 mA, 40 mm Fe, sensitivity 0.8–1.2% |
| Hydrostatic | In-line hydrostatic test unit | 1200 t frame, Φ800 cylinder, 31.5 MPa, printed record |
| Ultrasonic | In-line UT | Off-line, 0.5–15 MHz, weld 100%, HAZ 25 mm each side, body ≥35% |
| Eddy current | ECT in line | — (not on this route) |
| Operative standard | API 5L | GB/T 9711; API SPEC 5L (Φ1620 class) |
X-ray runs at 225 kV / 8 mA with 40 mm Fe penetration and static sensitivity 0.8–1.2%, at 0.5–10 m/min, against GB/T 26830-2011, ISO 10893-7 single-wall class B, GB/T 9711-2017 and API SPEC 5L (46th edition).
Hydrostatic testing uses a 1200-tonne frame with a Φ800 mm main cylinder and a 31.5 MPa pump, four tension beams at safety factor 4, PLC and computer monitoring with a printed record.
Off-line ultrasonic runs 0.5–15 MHz, covering the weld 100%, the heat-affected zone 25 mm each side and pipe body base material at 35% or better, with false calls at or below 2% and zero missed calls on the sample pipe. Weld tracking uses laser image capture.
Finishing on the spiral Φ1620 class runs slag removal, weld repair, pipe-end alignment, X-ray, hydrostatic test, off-line ultrasonic, then end facing and bevelling; repaired welds are re-inspected, and the pipe-end dead zone of 300 mm or less is handled by the operator’s own procedure. The Φ820 class runs a shorter chain: weld repair, X-ray, end facing, hydrostatic.
Worked Output Example
The example below is for the spiral route; on the HFW-API route, output is confirmed at quotation.
Spiral route, Φ1620 class — output is set at approximately 120 tonnes per 8-hour shift; the Φ820 class at approximately 62 tonnes per 8-hour shift.
Manufacturing lead time on the spiral route is 120 days for the Φ820 class and 150 days for the Φ1620 class.
Plant requirements for the spiral route: workshop 36 × 24 m with a 32 t crane at 6.5 m hook height for the Φ1620 class, or 32 × 18 m with a 20 t crane at 7 m for the Φ820 class; supply 220 / 380 V 50 Hz and compressed air at 0.6 MPa. Feed direction can be set left or right to suit an existing building.
Commercially, terms are the same as across the range: tiered configuration mapped to a written scope of supply, payment by T/T in three stages (30% / 65% / 5%) or L/C at sight, and ex-works (EXW) pricing. Our engineers travel to site to guide installation, commissioning and operator training, with support continuing online after handover; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance.
Acceptance on the spiral route is defined as continuous production of two different pipe sizes.
Importers and trading companies can see our page for importers & trading companies.
Oil and gas transmission pipe mill
An oil and gas transmission pipe mill is chosen by the largest diameter you will sell and the standard your buyers write into the order: up to Φ508 mm, an API-configured HFW line with in-line annealing, hydrostatic, ultrasonic and eddy-current stations; above that, a large diameter line pipe mill on the spiral route, built to GB/T 9711 and, on the Φ1620 class, API SPEC 5L.
From the Workshop
 Water Supply, Drainage & Urban Gas Pipe Production Lines
 Structural & Scaffolding Tube Production
 Furniture & Fence Tube Production
 API Line Pipe Mill
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.