
Home › Resources › Watch the Lines Running › Process Videos
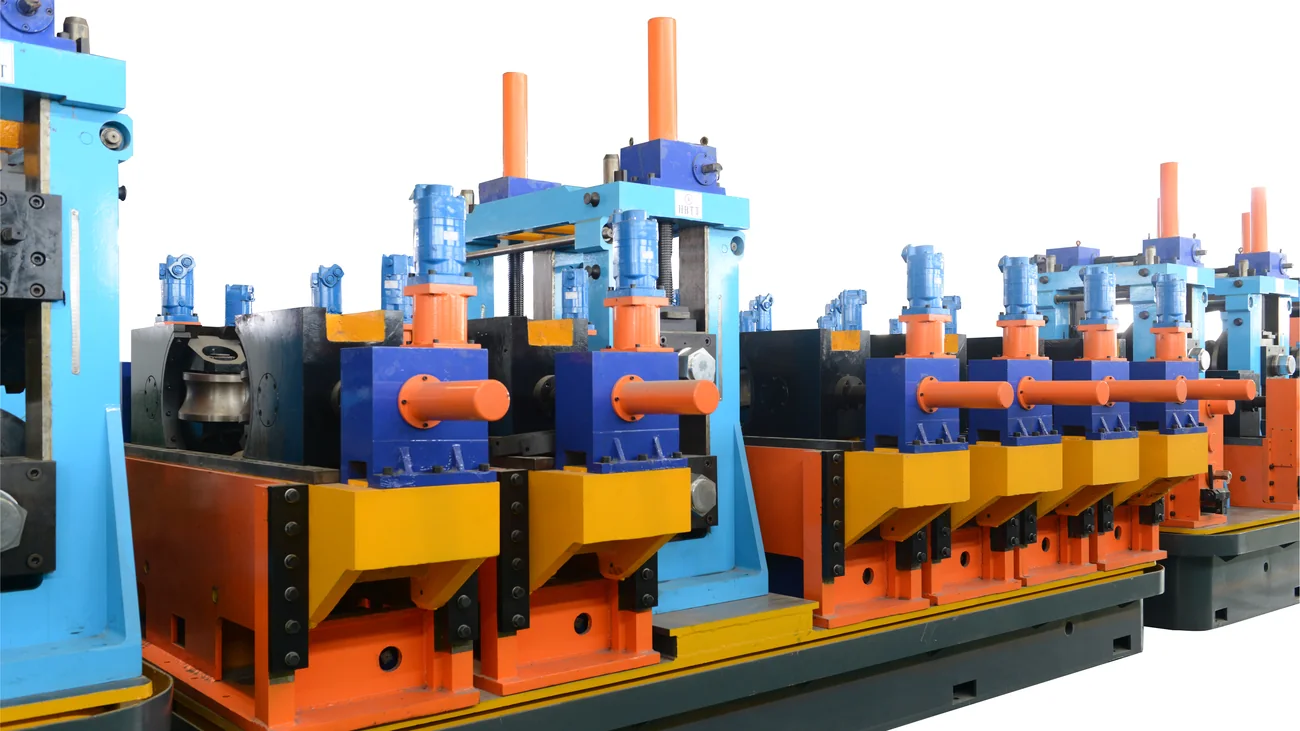
These films follow a high-frequency welded tube line from coil to cut length: uncoiling, strip joining, roll forming, HF induction welding, sizing, straightening and flying-saw cut-off, without stopping between coils. The full line is set out under the tube mill & welded pipe production line, and more films are in the video library.
Process Films
How a Tube Mill Line Runs, Stage by Stage
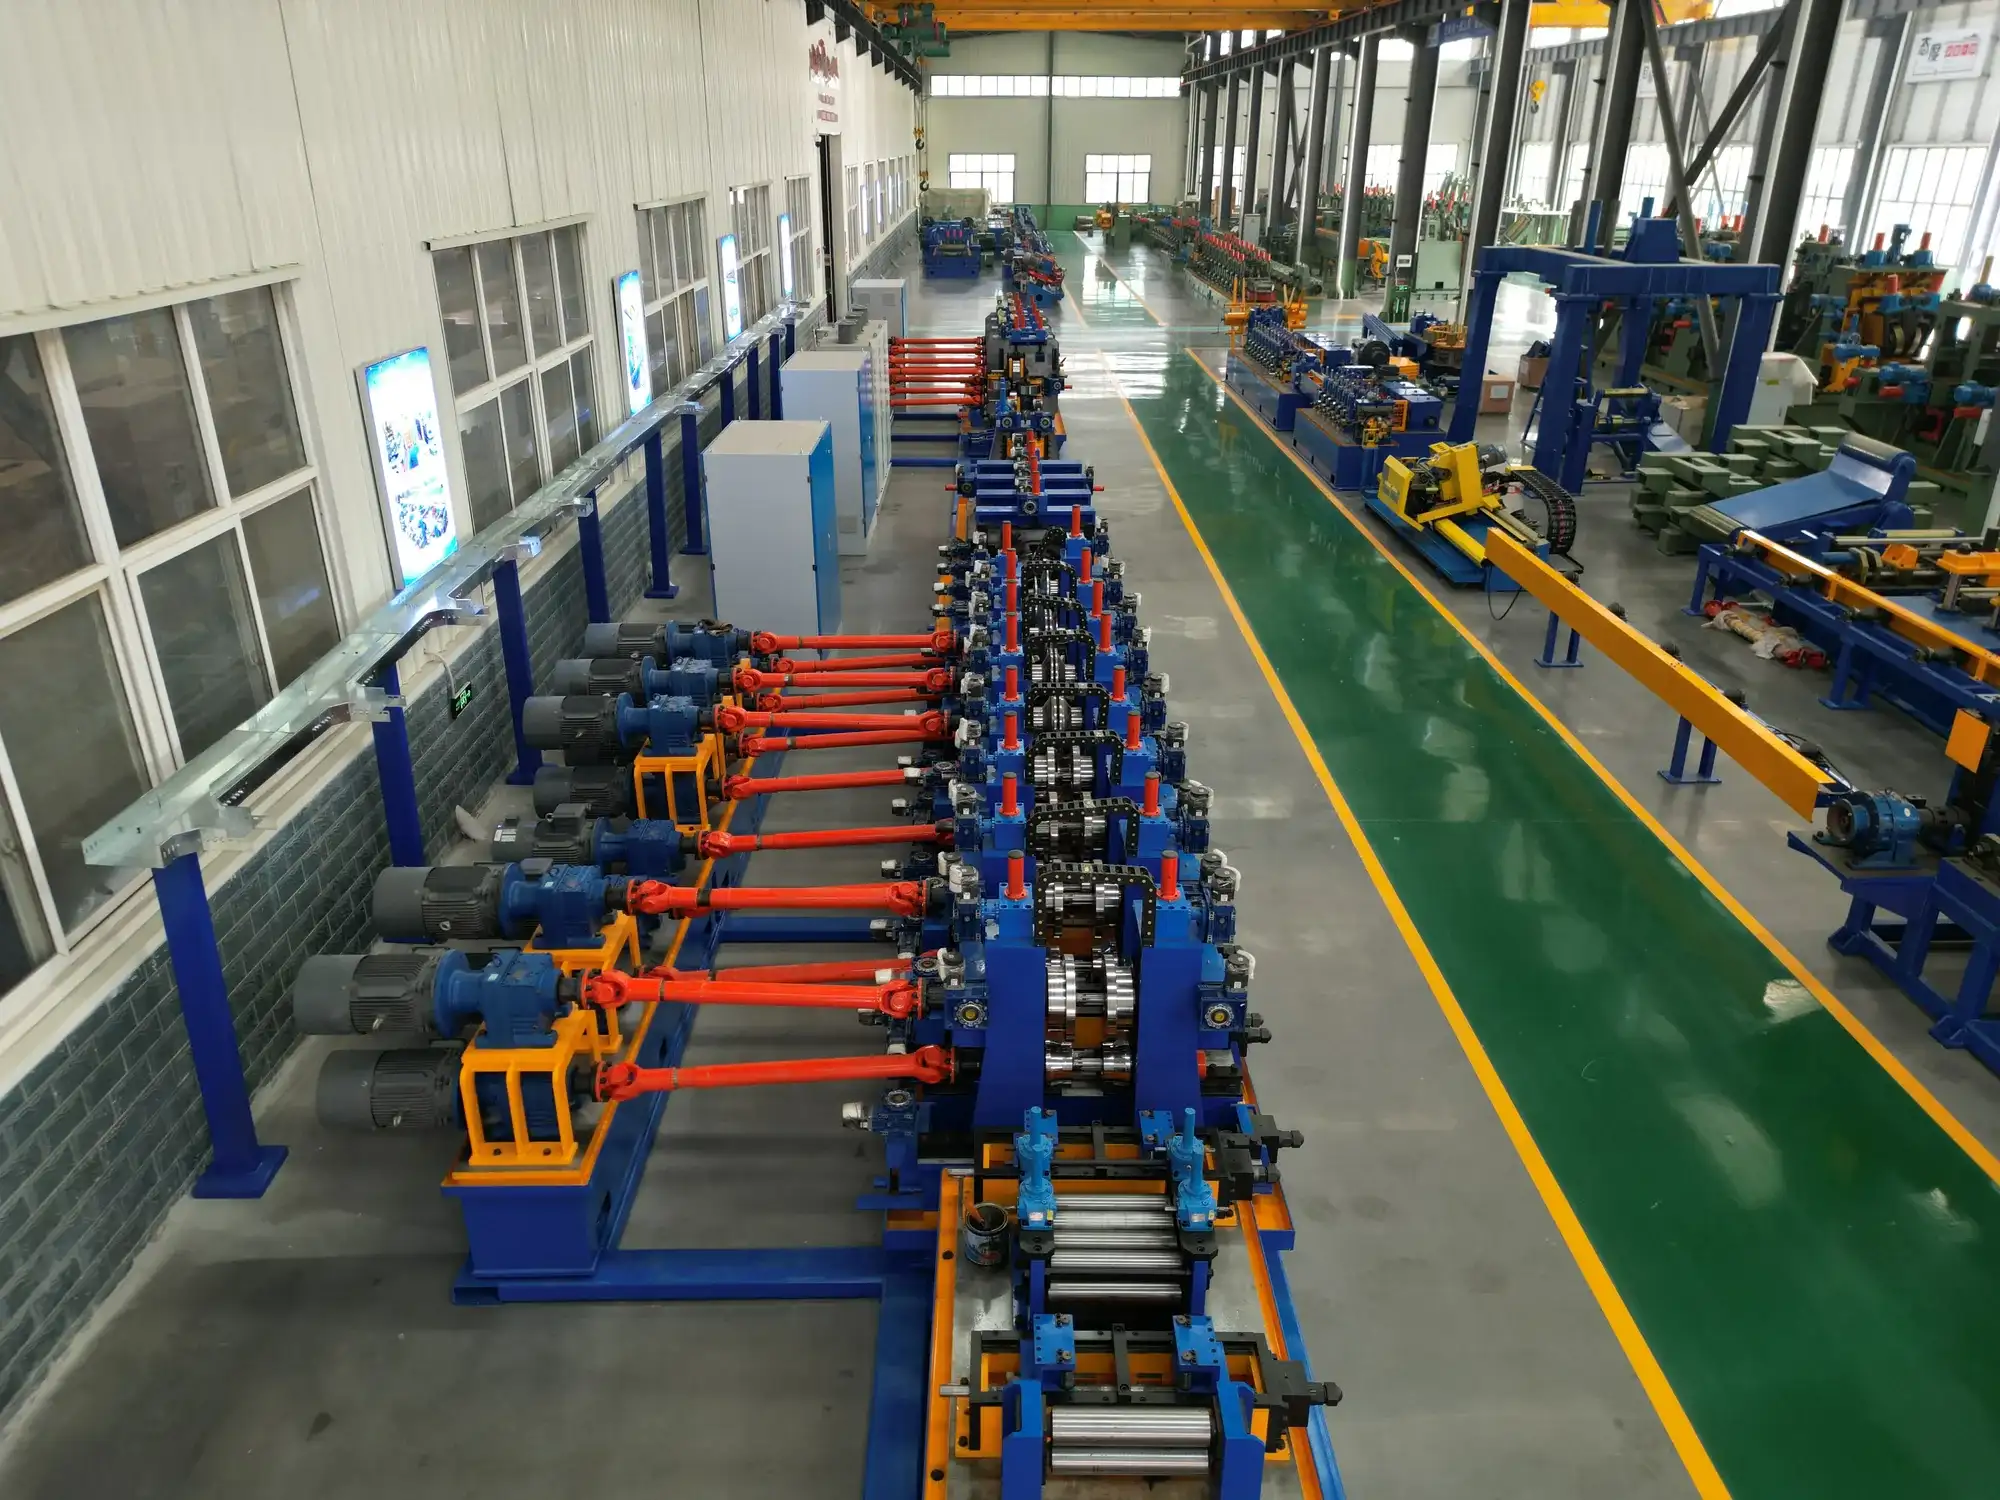
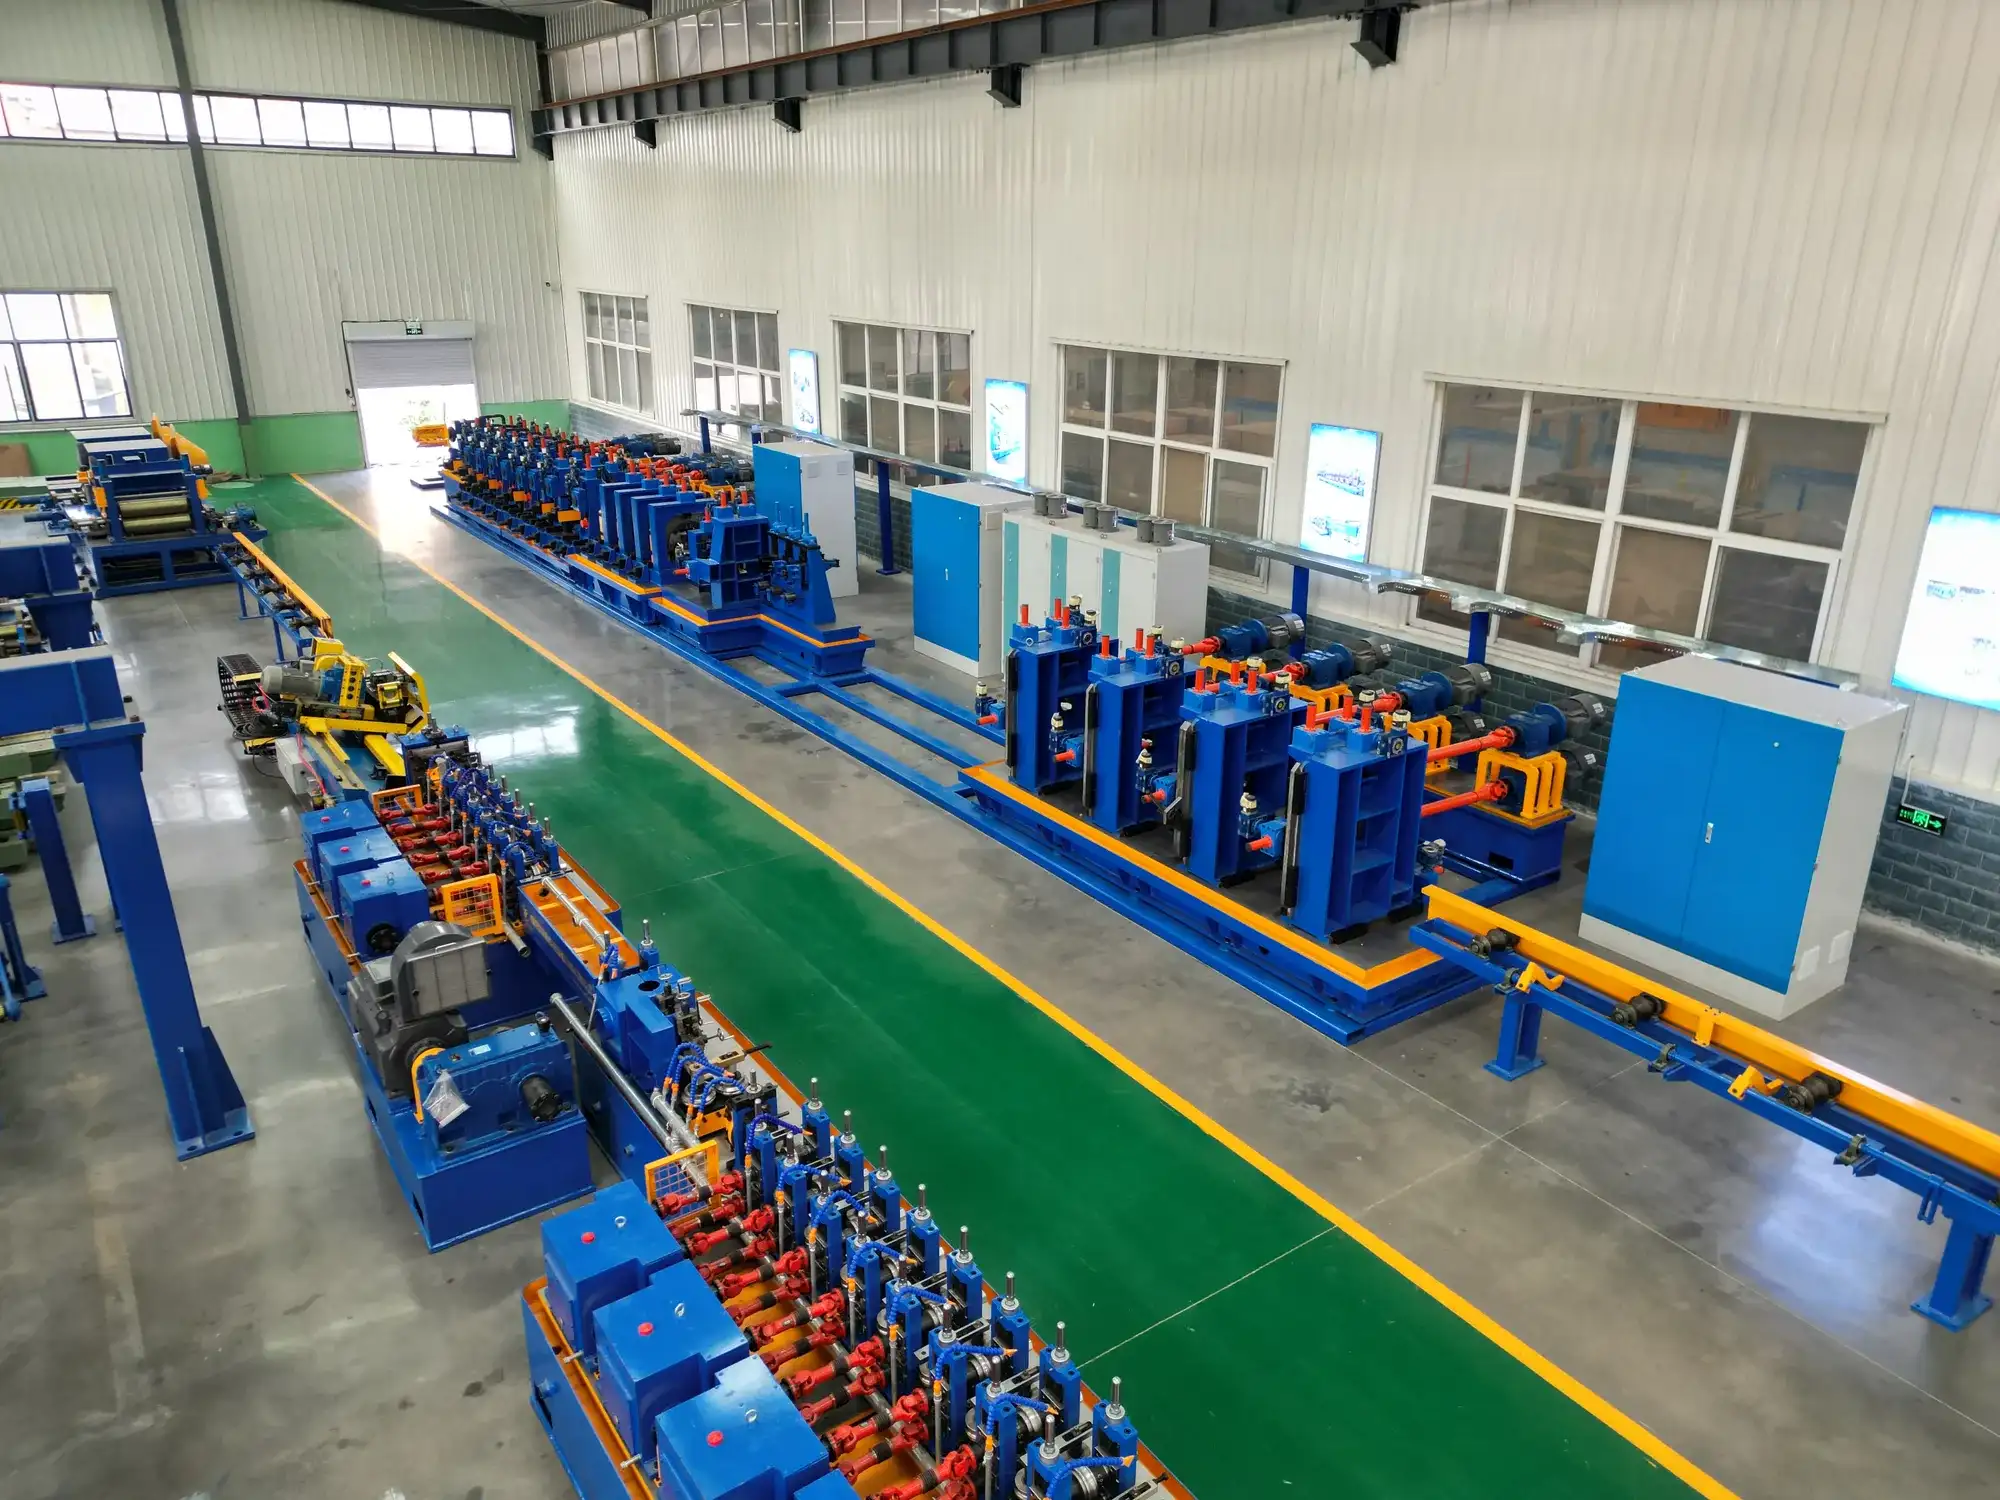
A high-frequency welded tube mill is a continuous line: flat strip enters at one end and cut lengths of welded pipe leave at the other, without the mill stopping when one coil runs out. Two preparation stages and two continuity units make that possible.
The coil is loaded by coil car onto an expanding-mandrel uncoiler and tensioned pneumatically. On the HG89 and larger lines, a five-roller leveller then flattens the strip before it goes forward.
An automatic shear-welder cuts off the irregular head and tail of each coil and joins one strip to the next; a spiral accumulator stores strip between that unit and the mill, feeding the mill while the next coil is being prepared.
Without the accumulator the mill stops at every coil change; with it, the joint passes through as part of a continuous run.
HF Induction Welding on the Line
High-frequency welding closes the seam without filler: the HF current concentrates at the edges through skin and proximity effect, heats them to welding temperature, and squeeze rolls press them together.
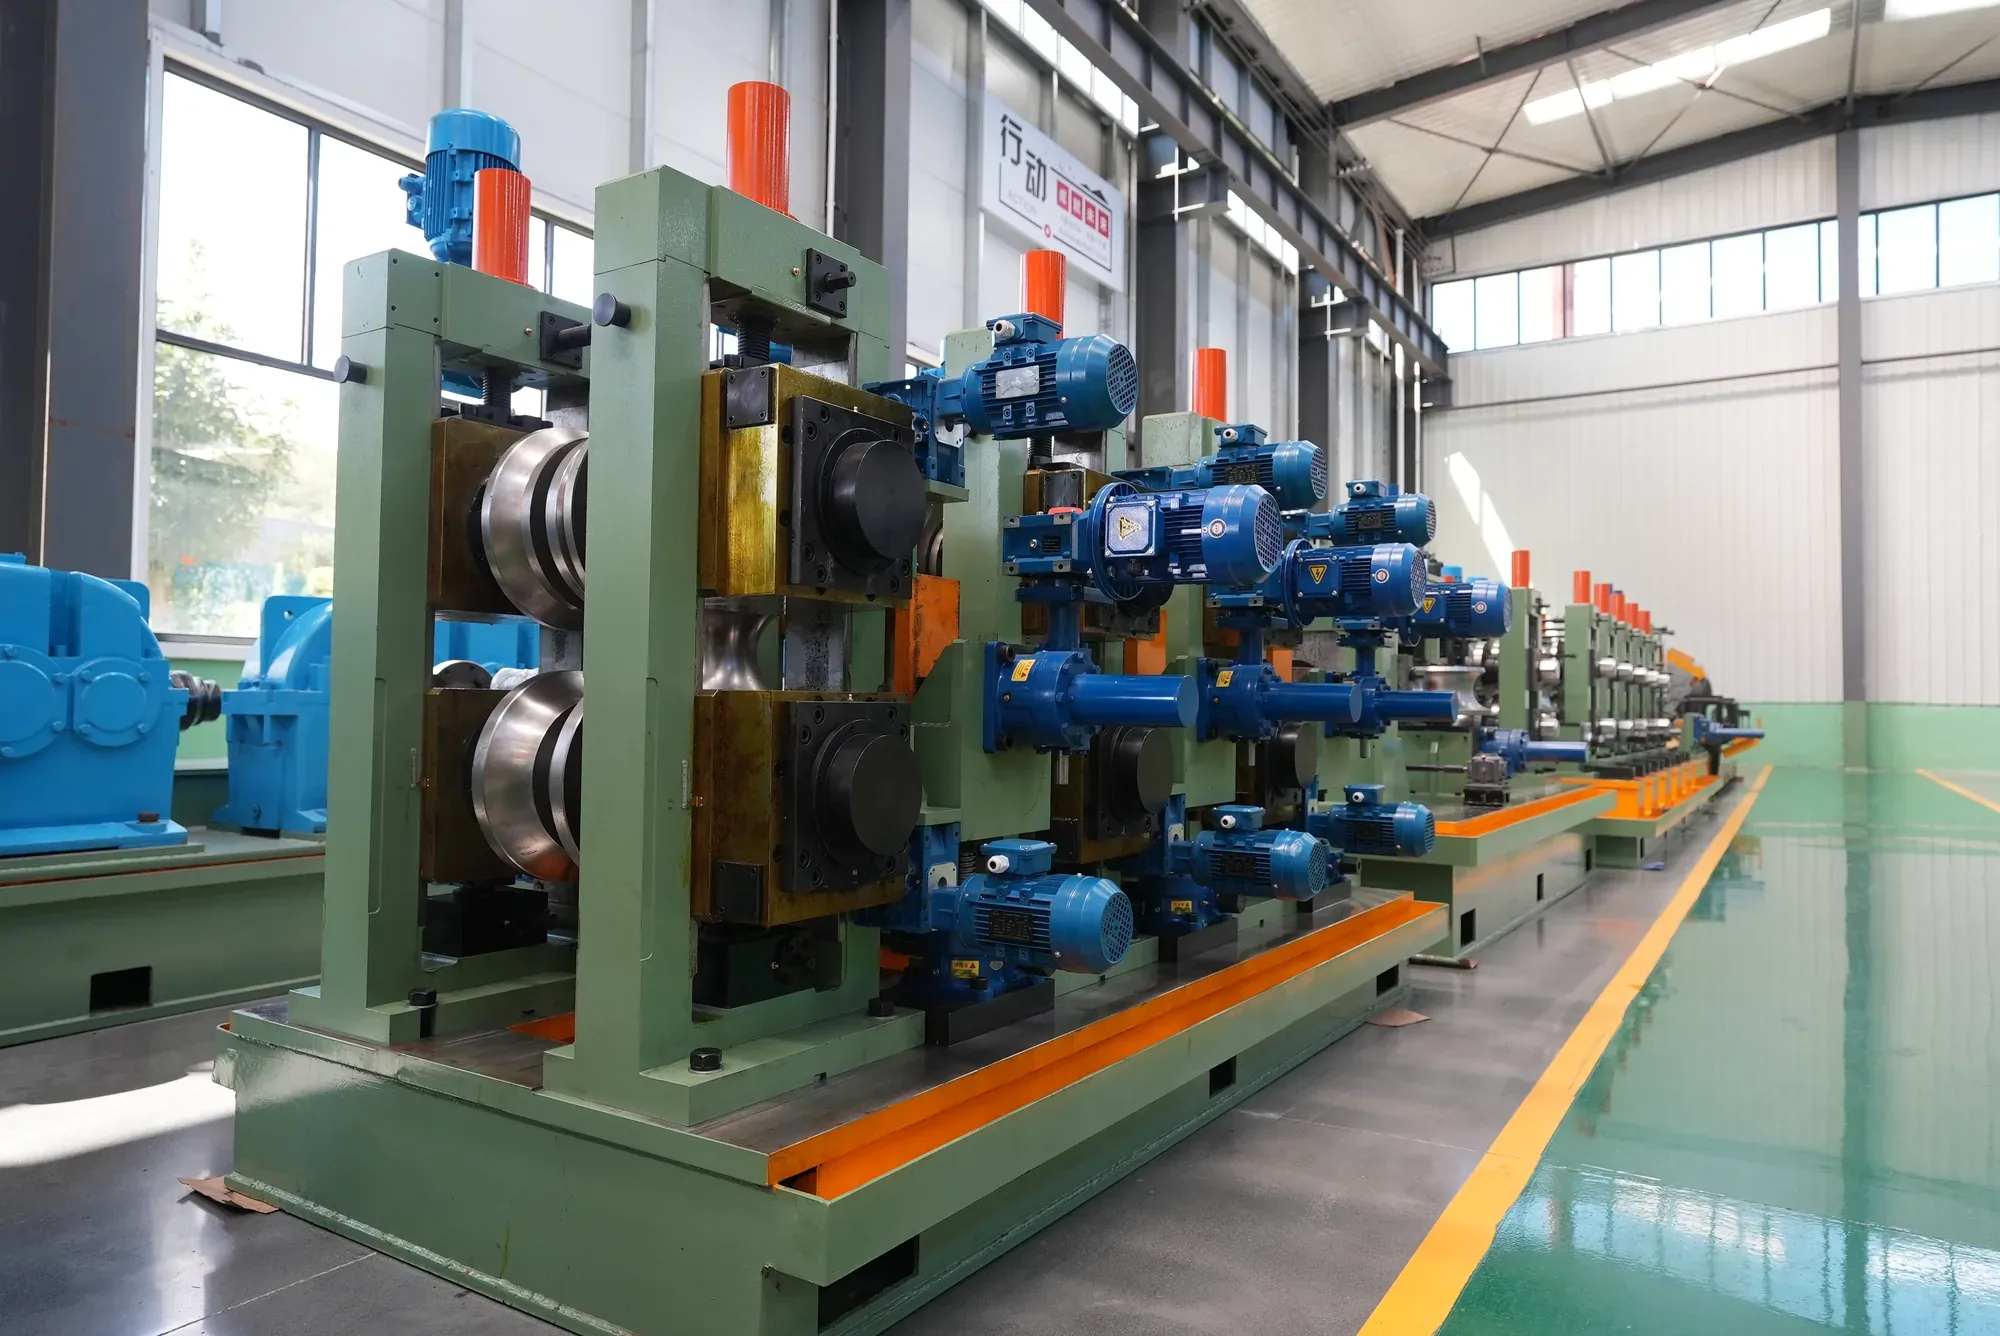
Forming comes first and decides whether the seam can be welded well at all: forming rolls bring the flat strip progressively to the required round or square section, setting both tube shape and seam alignment before the strip reaches the weld box.
Welder power is matched to diameter in steps across the twelve sizes of the high-frequency welded pipe mill, from 150 kW on the HG32 to 1500 kW on the HG630; the sizes in between are set per project.
What the video shows that a diagram cannot is how tightly three variables have to stay matched — welder power, line speed and squeeze. Mismatch does not produce a slightly worse weld; it produces a specific and recognisable defect. Too little energy gives lack of fusion or a cold weld; too much gives burn-through. Either one fails a pressure or NDT check downstream.
Sizing, Straightening and Flying-Saw Cut-Off
After the weld cools, sizing rolls bring the tube to final outside diameter and straighten it; a flying saw then cuts to length at full line speed without stopping the mill.
Underneath all of it sits the control layer — PLC industrial computer with variable-frequency drive — which is what keeps line speed and cut length repeatable run after run.
Two further things show up clearly on film: size change and yield.
The first is size change. On direct-square-forming lines, size is changed by combined dies rather than by changing rolls, and roll consumption falls by more than 90%; servo adjustment and quick die change carry the rest. For a plant running several sizes this is the difference between a shift lost to changeover and an hour lost to it — and it is far more convincing watched than tabulated. One exception is worth stating: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
The second is yield. On our high-end lines fitted with digital-twin production monitoring, material yield can reach 93% or more; roll wear and changeover speed are the two things that move it.
The eight stages, in order:
- Uncoiling — coil car and expanding-mandrel uncoiler, pneumatic tensioning
- Head straightening and levelling — five-roller leveller on the HG89 and larger lines
- Shear and strip welding — automatic shear-welder joins coil to coil
- Spiral accumulator — strip buffer for non-stop running
- Roll forming — progressive forming to round or square section
- HF induction welding — skin and proximity heating, squeeze rolls close the seam
- Sizing and straightening — final dimension and straightness after cooling
- Flying-saw cut-off — cut to length at line speed
Ask an Engineer — Talk to Our After-Sales Team →
More in Watch the Lines Running
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.