
Home › Purlin Machine Lines › CZ Purlin Roll Forming Machine
In This Line
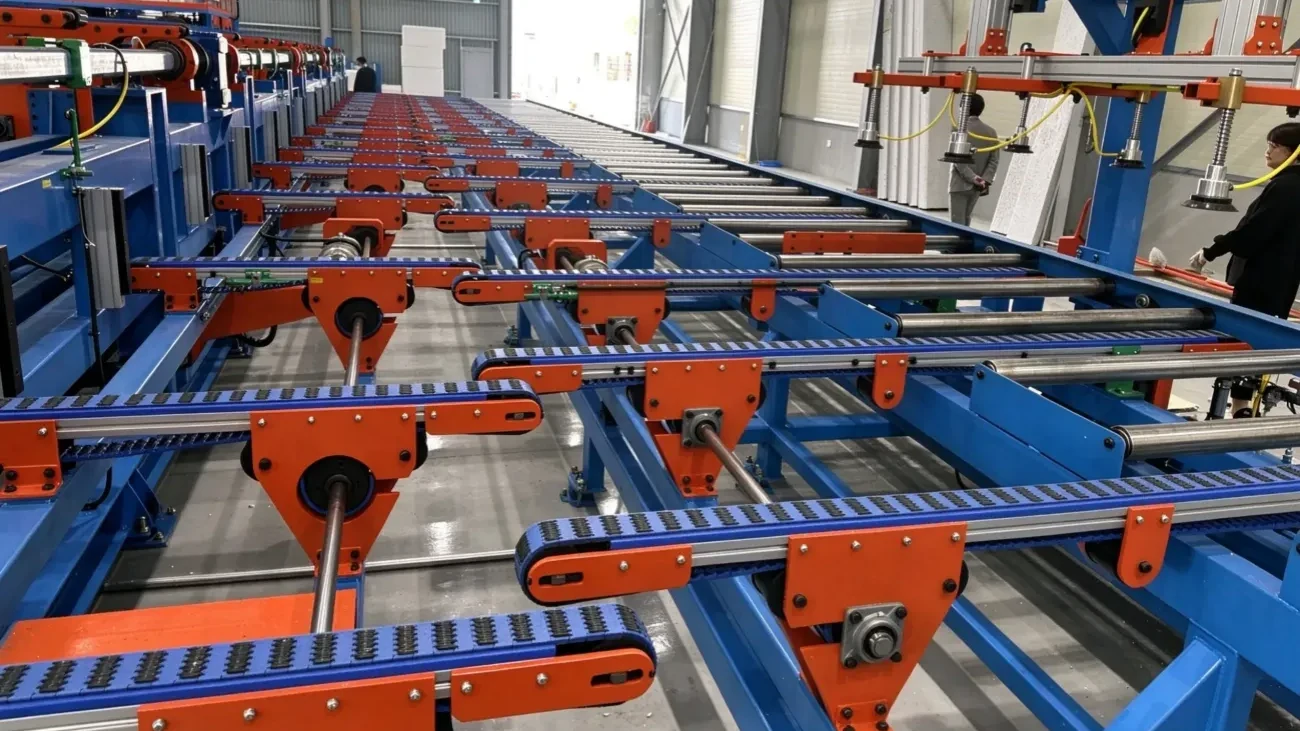
The C/Z/Ω purlin line cold-forms steel strip 2–4 mm thick into C, Z and Ω sections on one machine, at forming speeds up to 20 m/min, punching and cutting automatically from an entered length, hole pitch and quantity.
Technical Specification Table
| Parameter | Value |
|---|---|
| Line type | Semi-automatic C/Z interchangeable purlin line |
| Sections produced | C / Z / Ω on one machine |
| Strip thickness | 2–4 mm |
| Forming passes | 18 passes |
| Forming speed | up to 20 m/min |
| Size change | Stepless adjustment — no roll change |
| Punching & cut-off | Hydraulic, automatic from entered length / hole pitch / quantity |
| Forming roll material | Bearing steel, finished after quenching |
| Die & cutter material | Cr12, hardened |
| Forming principle | Room-temperature progressive bending; no phase change, purely plastic deformation |
| Tooling supplied | One set of dies and cutters with the line |
| Control | Industrial PLC with variable-frequency drive |
| Section dimension range (web / flange / lip) | C: web 100–400 mm; Z: web 120–400 mm; flange 50–100 mm; lip 10–25 mm |
The full specification of the line is on the cold roll forming machine page.
Our cold roll forming equipment is CE marked under the EC Machinery Directive 2006/42/EC; the certification covers C, Omega, Zeta and Z purlin sections as well as other open and closed profiles.
Line Configuration and Scope of Supply
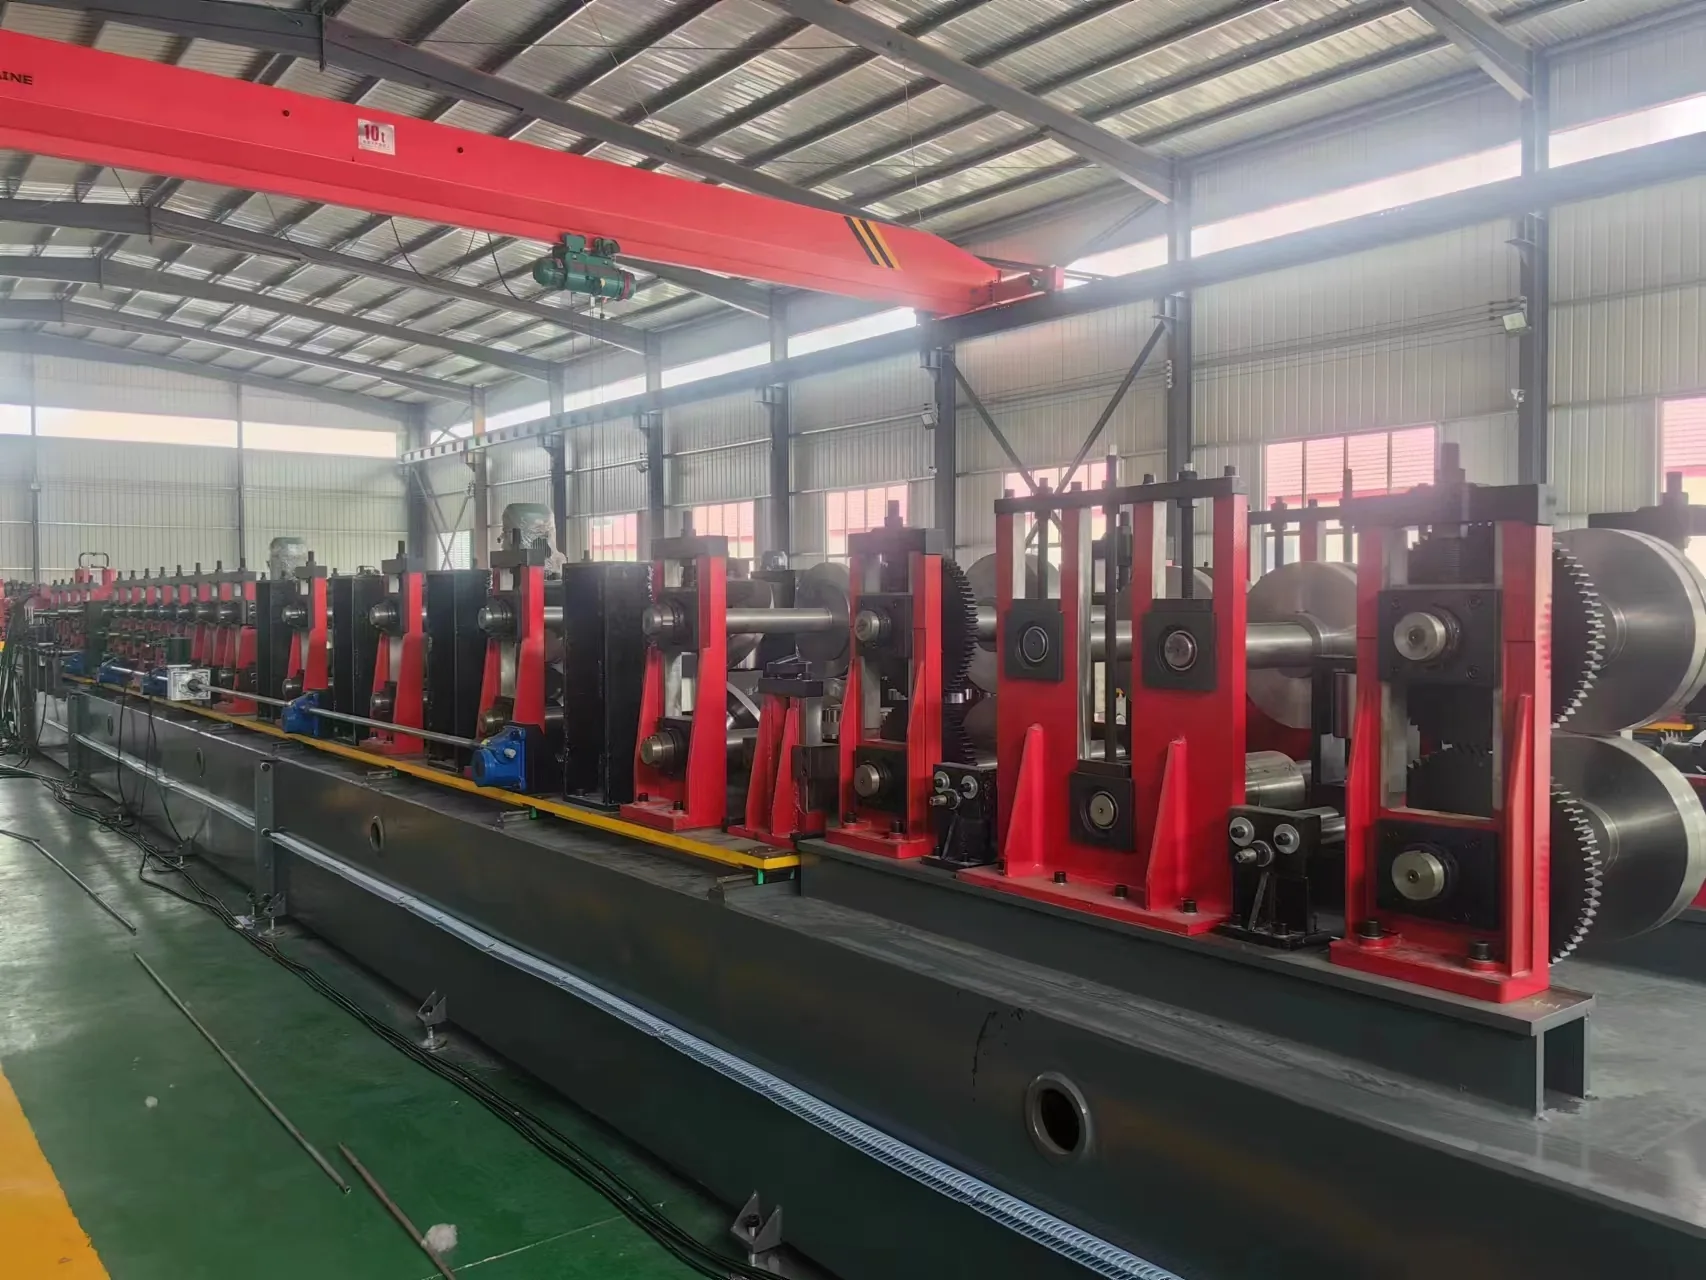
The line consists of a strip guide, a leveling unit, the roll former, two hydraulic punching units, a hydraulic stepless-adjustment and cutting unit, and the electrical and hydraulic systems. Three of these decide what comes off the line:
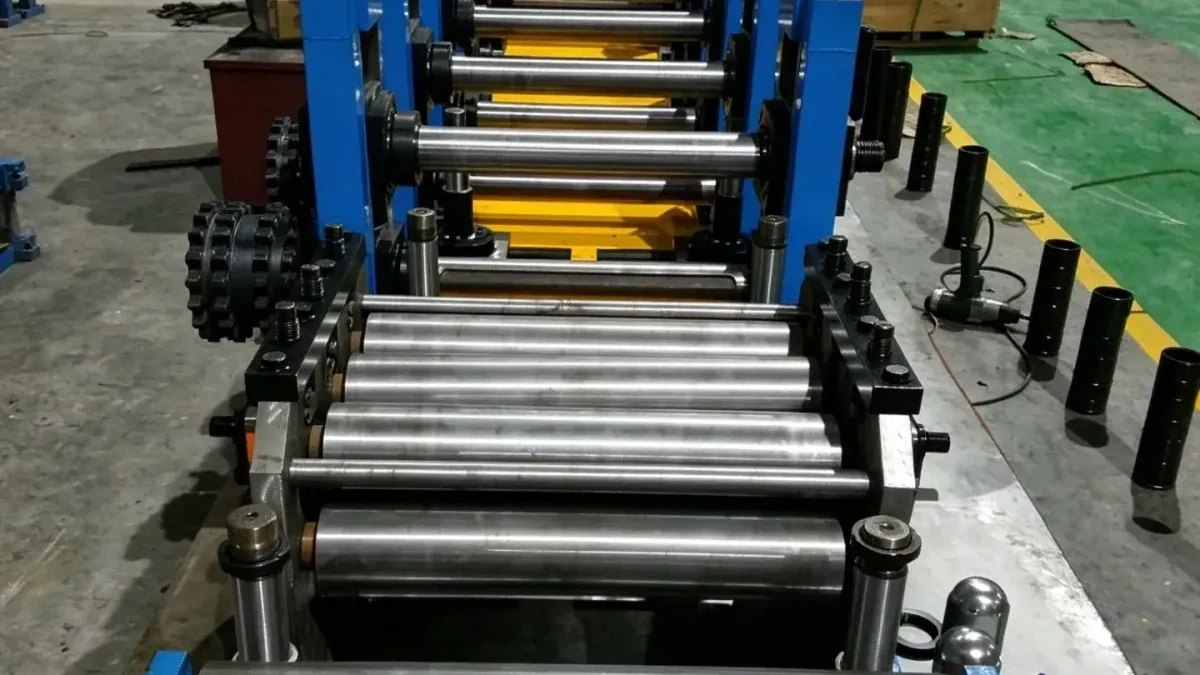
Forming rolls. Eighteen passes bend the flat strip step by step into the C, Z or Ω section. The rolls are bearing steel, finished after quenching.
Hydraulic punching and cutting. Holes are punched and the section is cut to length hydraulically after forming; dies and cutters are quenched Cr12.
Parameter entry and control. The operator enters length, hole pitch and quantity, and the line punches, forms and cuts automatically. Control is by an industrial PLC with variable-frequency drive.
One set of dies and cutters ships with the line, so tooling is in place for commissioning.
Cold roll forming bends the strip a little at each pass, so pass count, roll profile and the yield strength of the strip together set the accuracy of the finished section and how much springback has to be allowed for. The section stays open, so there is no welding stage: what comes off the last pass is the finished purlin.
The line is quoted complete, or as individual machines where the plant already has part of the chain.
Size Change, Roll Wear and Running Cost
Sizes are changed by stepless adjustment, with no roll change: C and Z purlins of different sizes come off the same machine, and the stand positions are set hydraulically for each size. A section outside the C, Z and Ω family needs its own tooling. For the changeover itself, see purlin line size change.
Material thickness, line speed and output are confirmed against your profile section, steel grade and finished length at quotation.
Send us those three and we will state the figures.
What wears:
- Forming rolls — wear parts, replaced according to output volume. Machined at the works on its own CNC equipment, so a replacement set years later matches the set delivered with the line.
- Punching dies and cutters (Cr12) — wear parts, reground or replaced according to punch count.
Where quality is decided, in order: roll, die and cutter hardness; the entered parameters; and the stepless-adjustment alignment at setup. Failure shows as hole-position offset, twisted section, or a blunt cut edge — and all three surface downstream as assembly problems rather than as visible machine faults.
Responsibility boundary. The equipment holds hydraulic punch positioning and roll profile accuracy; the plant sets the entered parameters and the setup, and supplies strip of the right grade and flatness. Hole position and section geometry on the finished purlin depend on both.
Applications and Output Examples
C and Z purlins from this line go into steel-structure buildings and photovoltaic mounting frames; length, hole pitch and quantity change from order to order, and the line handles that from the control panel without changing rolls. The Ω section comes off the same machine under the same stepless adjustment.
PV bracket purlin machine
Used as a PV bracket purlin machine, the line forms the C, Z and Ω sections that carry the panels on solar mounting frames, with the fixing holes punched automatically from the hole pitch entered at the control panel.
CZ purlin making machine
As a CZ purlin making machine, the line runs in this order: the strip is guided and leveled, formed through 18 passes, then punched and cut to length by the hydraulic units after forming, all from the length, hole pitch and quantity entered at the control panel.
Delivery, Installation and Training
Standard lines ship within 90 working days of the deposit, with plant-level customisation scheduled from our own manufacturing base.
The line is dismantled into units and shipped in containers: heavy frames are braced and secured, while precision parts and wear items travel in wooden cases together with a spare-parts pack.
Our engineers travel to site to guide installation, commissioning and operator training; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance, and support continues online after handover.
Payment is 30% by T/T on signing, 65% by T/T before shipment and 5% after installation and commissioning, or by L/C at sight; prices are quoted ex-works (EXW).
Our after-sales team handles enquiries.
Watch This Line Running
C/Z/Ω Purlin Roll Forming Machine — 18-Pass, 20 m/min
 Changing Section Size on a Purlin Roll Forming Machine
 Roll Forming Machines & Cold Roll Forming Lines
 Purlin Machine Price — Reading It Against the Supply Scope
 H-Beam Production Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.