
Home › Purlin Machine Lines › Changing Section Size on a Purlin Roll Forming Machine
In This Line
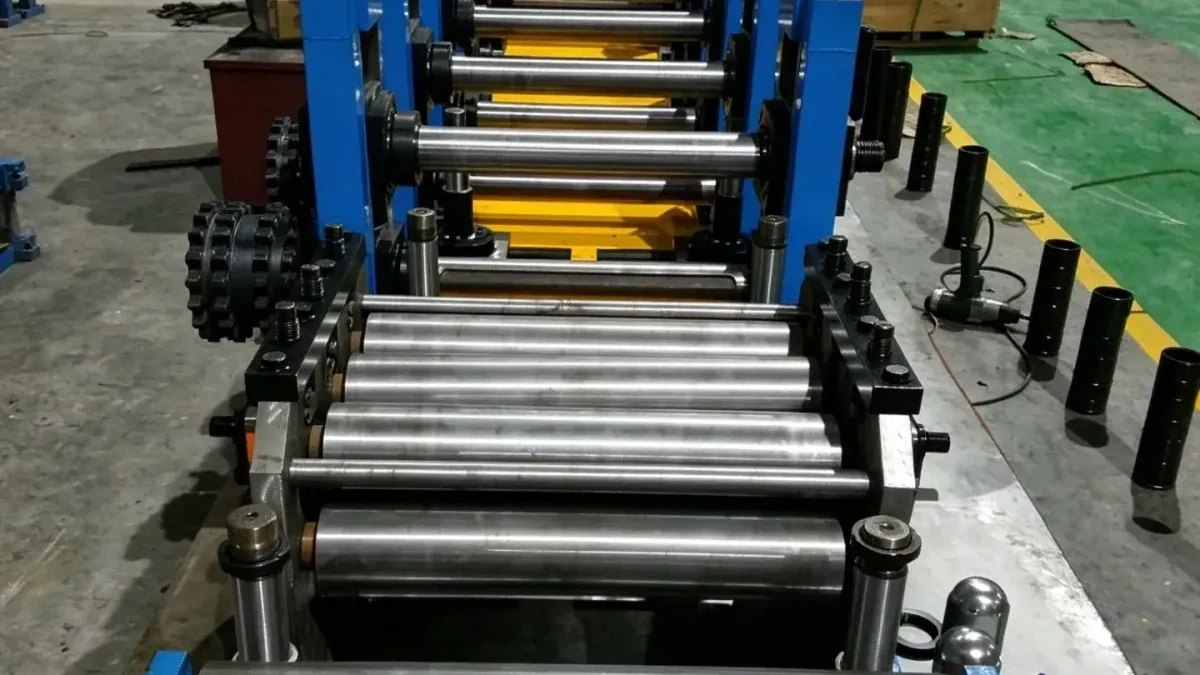
One machine produces multiple purlin sizes through stepless adjustment; length, hole pitch and quantity are entered as parameters and the line punches, forms and cuts automatically. Forming is 18 passes at up to 20 m/min on 2 to 4 mm material.
What Is Purlin Line Size Change
A purlin roll former is a cold forming line, not a welding line. It takes strip and bends it progressively into an open C, Z or omega section, punching and cutting it as it goes; unlike a tube mill, this is roll forming plus hydraulic punching and shearing, producing an open section, with no welding involved.
On this line the same machine produces multiple C and Z purlin sizes through stepless adjustment, so a size change does not require a roll change.
- A size change needs no roll change — the machine is adjusted steplessly.
- One machine produces C, Z and omega sections.
- Forming is 18 passes, with hydraulic punching and cutting.
- Forming speed: up to 20 m/min.
- Material thickness: 2 to 4 mm.
- Length, hole pitch and quantity are entered as parameters; punching, forming and cutting run automatically.
Purlin roll forming machine size change
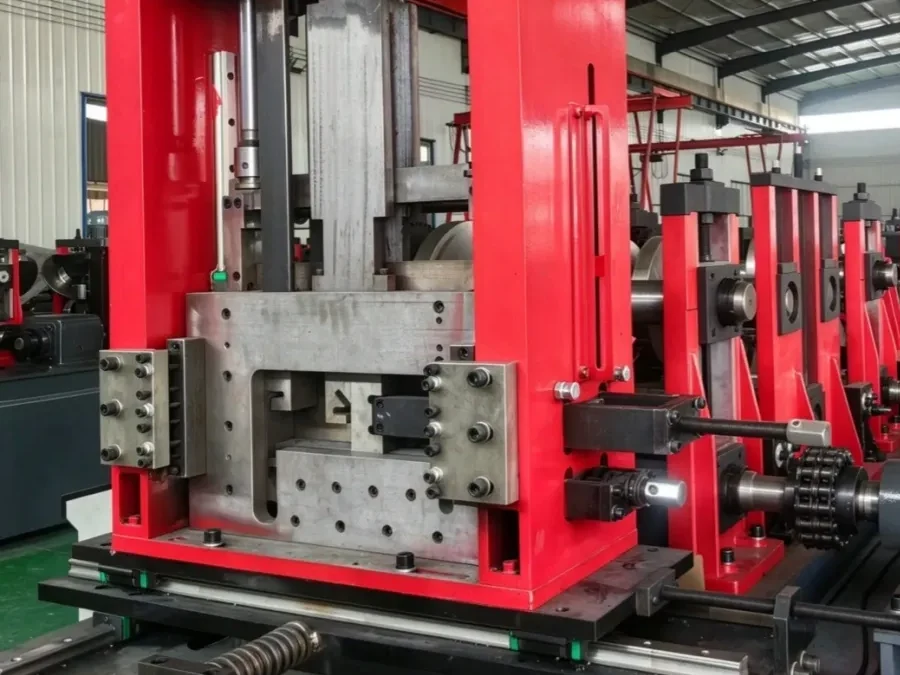
On a purlin roll forming machine of this type, a size change is a stepless adjustment of the existing forming stands rather than a roll change. The operator aligns the adjustment to the target section, enters the purlin length, hole pitch and quantity, and the machine then punches, forms and cuts automatically.
Purlin Line Size Change — Method and Measured Values
Forming runs through 18 passes, with hydraulic punching and cutting after forming. These are the limits for a size change on this machine:
- Section range: C purlins with a 100–400 mm web and Z purlins with a 120–400 mm web; flange 50–100 mm; lip 10–25 mm.
- Strip thickness: 2–4 mm.
- Hole spacing: adjustable from 45 to 650 mm.
- Width adjustment: hydraulic stepless adjustment, with adjustment motors of 2 × 0.75 kW and 1 × 1.5 kW.
- Forming speed: up to 20 m/min.
The forming principle explains why stepless adjustment is possible at all. Cold roll forming bends the strip progressively through 18 passes at ambient temperature into the open C, Z or omega section — pure plastic deformation with no phase change.
Forming rolls are bearing steel, finished after quenching; punch dies and cutters are quenched Cr12, so the same roll set holds its profile across every size the line is adjusted to.
C/Z purlin machine changeover
Moving between C and Z, or between sizes within them, follows the same steps, and Ω sections come off the same machine. Closed square tube is a different case: there sizes are changed by servo adjustment of a combined mould, as on our direct forming square tube mill.
Sources and Standards Referenced in Our Records
Our cold roll forming equipment is CE marked under the EC Machinery Directive 2006/42/EC. The section range, strip thickness, hole spacing, adjustment motors and speed given on this page are taken from the technical specification of our C/Z purlin roll forming line.
Step-by-Step Procedure
- Enter the purlin length, hole pitch and quantity for the new size at the control panel.
- Align the hydraulic stepless adjustment to the target section; no rolls are changed.
- Feed 2–4 mm strip through the guide and leveling unit.
- Form the section through 18 passes at up to 20 m/min.
- Punch the holes hydraulically after forming, at the entered hole pitch.
- Cut each purlin to length hydraulically after forming.
Worked Example — What Is On File and What Is Not
On file: a plant running 3 mm strip is inside the 2–4 mm range and can move between C, Z and Ω sections, and between C web heights of 100–400 mm or Z web heights of 120–400 mm, by stepless adjustment without changing rolls. Hole spacing is reset at the control panel anywhere from 45 to 650 mm.
Not given as fixed figures: the changeover time from the last piece of one size to the first good piece of the next, and punching position accuracy in millimetres. Both depend on the section and the setup, so we state them against your drawing when we quote.
Why cold forming behaves differently from welding
Nothing is melted: the strip is bent at room temperature through 18 passes, so the variables are pass count, roll profile and the yield strength of the strip, which together set section accuracy and springback. A different steel grade at the same thickness springs back differently, which is why the grade belongs in the enquiry.
What “semi-automatic” means here
Punching, forming and cutting run automatically from the entered parameters; the setup is manual — aligning the stepless adjustment to the target section and checking the entered length, hole pitch and quantity against the order. The equipment holds punch positioning and roll profile accuracy; errors at setup show as hole-position error, length error or a twisted section, so operator training is part of commissioning.
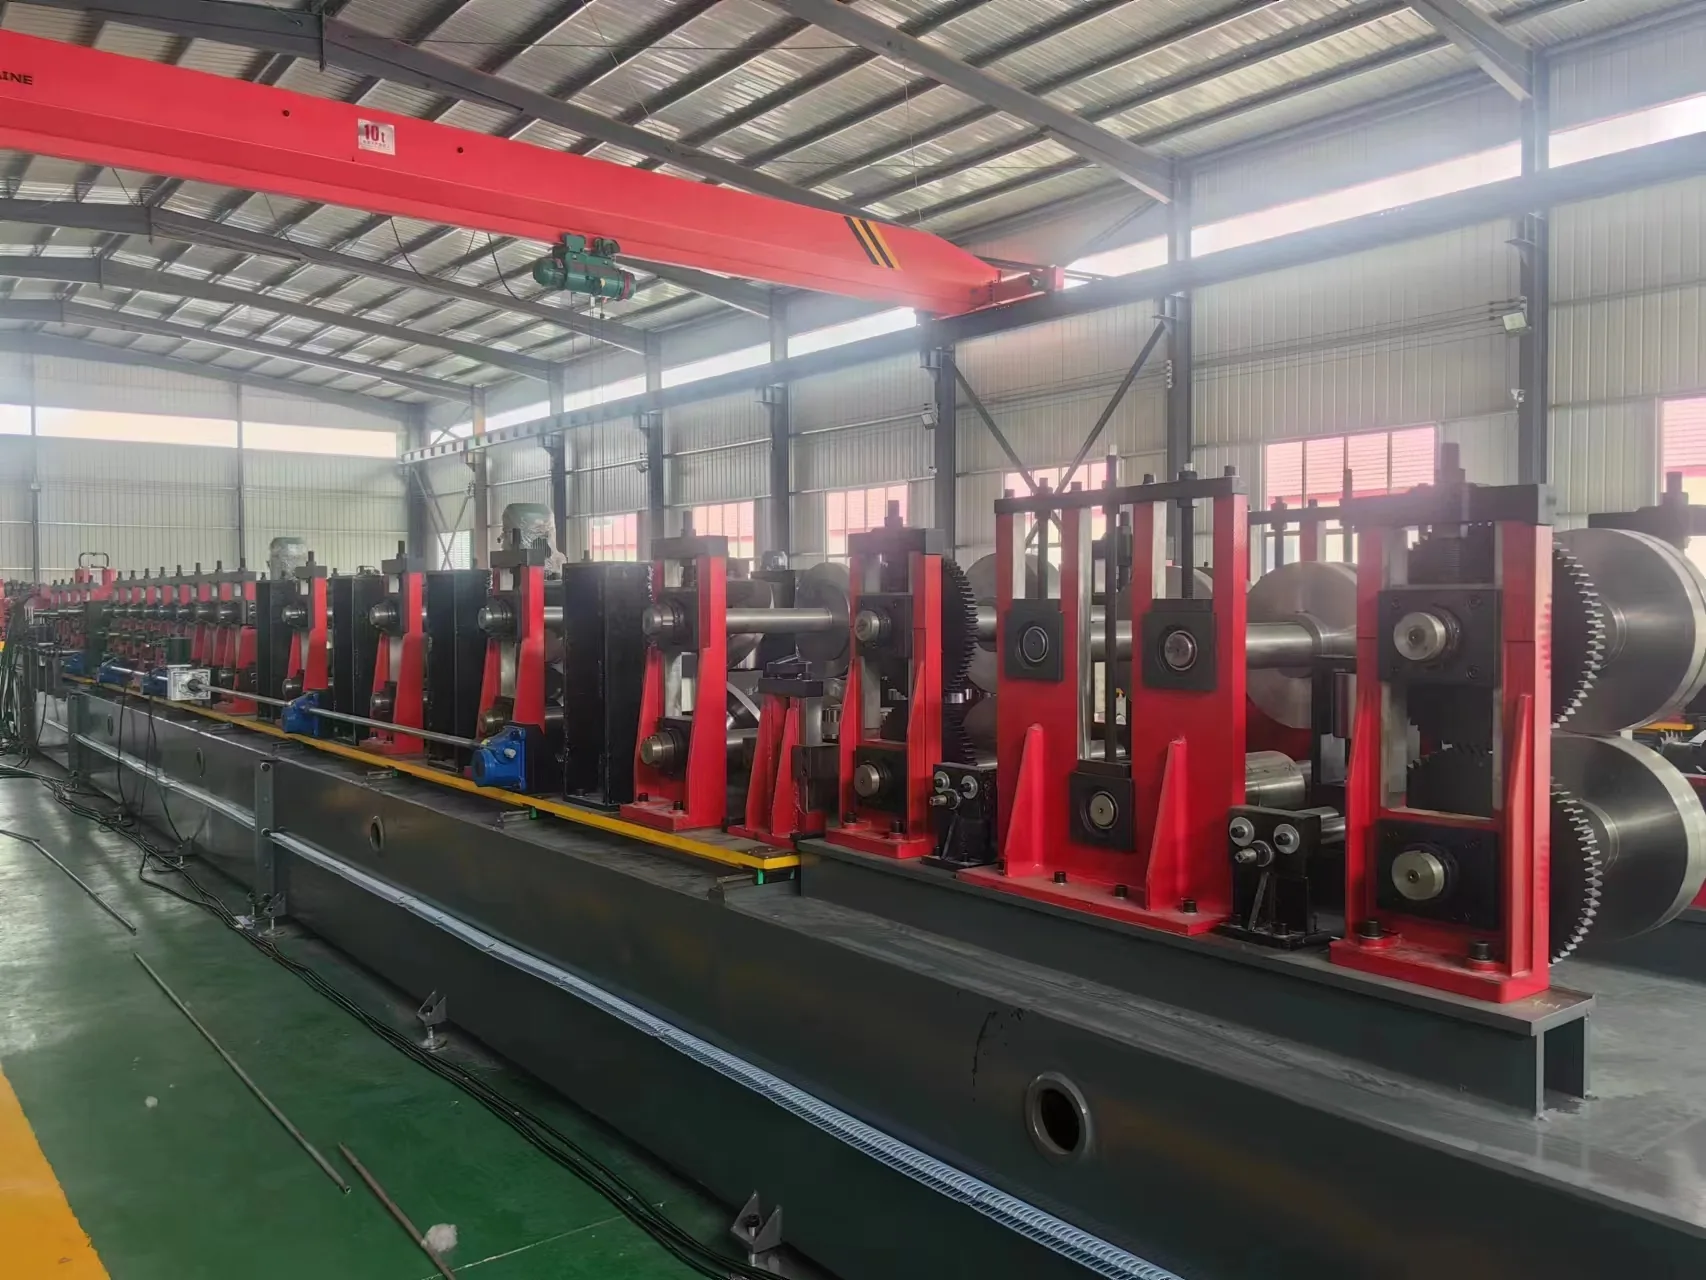
 CZ Purlin Roll Forming Machine
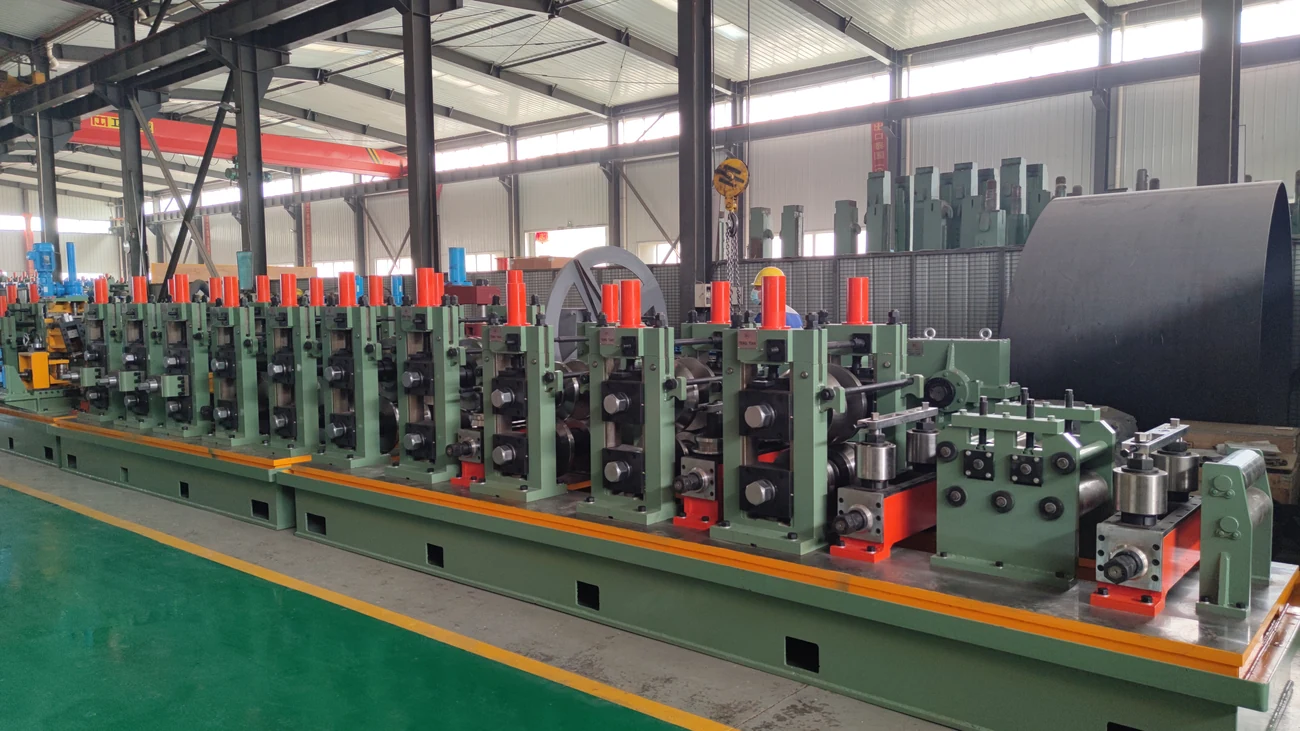 Direct Forming Square Tube Mill
 Purlin Machine Price — Reading It Against the Supply Scope
 Purlin Machine Lines
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.