
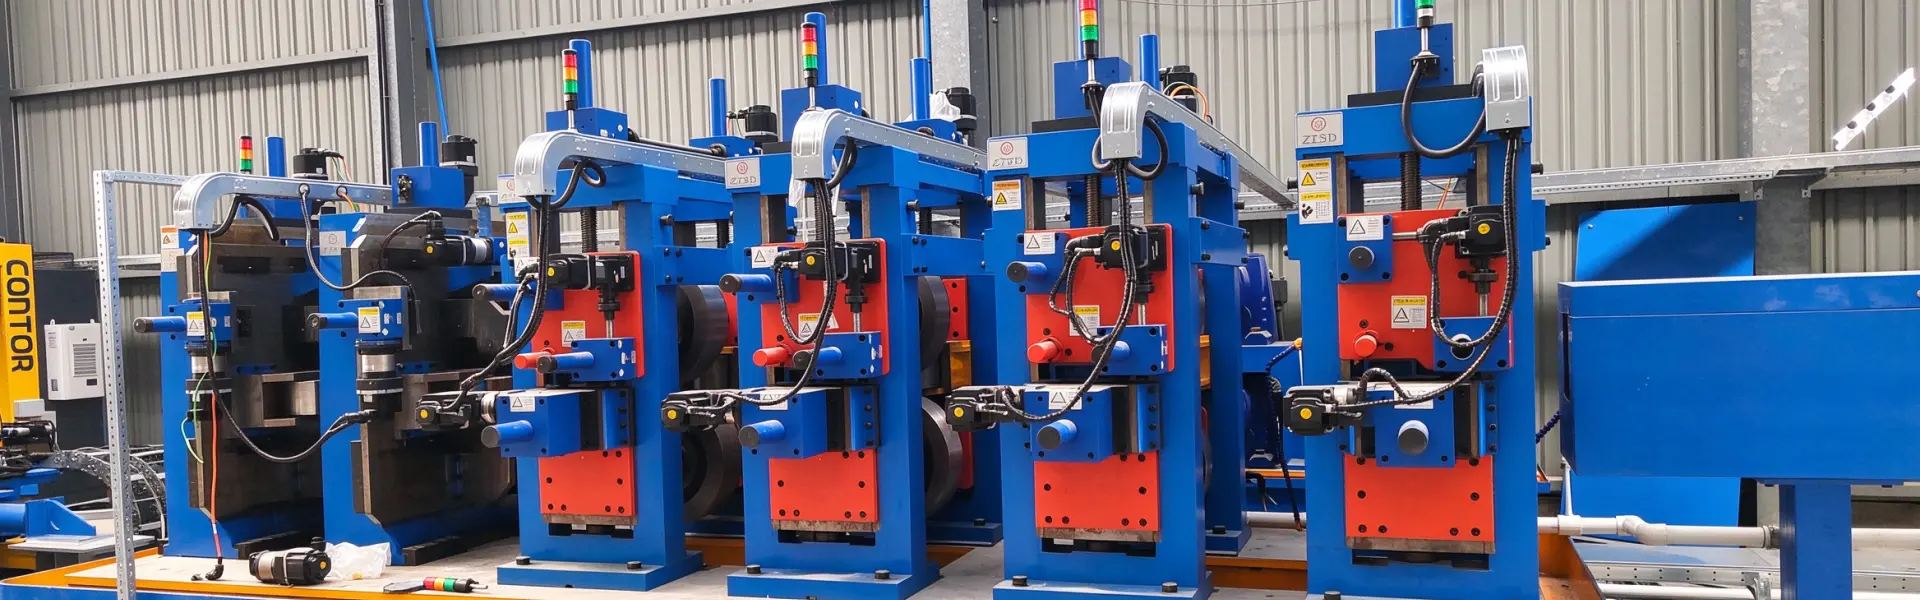
Tube Mill Rolls and Spares
Tube mill rolls and spare parts are what keep a line running after the commissioning engineers have gone home.
In This Line
Tengtian machines forming and sizing rolls in-house on its own CNC equipment and supplies the wear parts and consumables for every line it builds: saw blades, induction coils and impedors on high-frequency mills; wire, flux, torch tips and milling inserts on spiral submerged arc lines; knives and spacers on slitting lines.
We supply the wear items, consumables and replacement parts for every line we build — high-frequency welded tube mills, spiral submerged arc lines, slitting lines and the API inspection train. They are listed line by line below, because the part lists are not interchangeable.
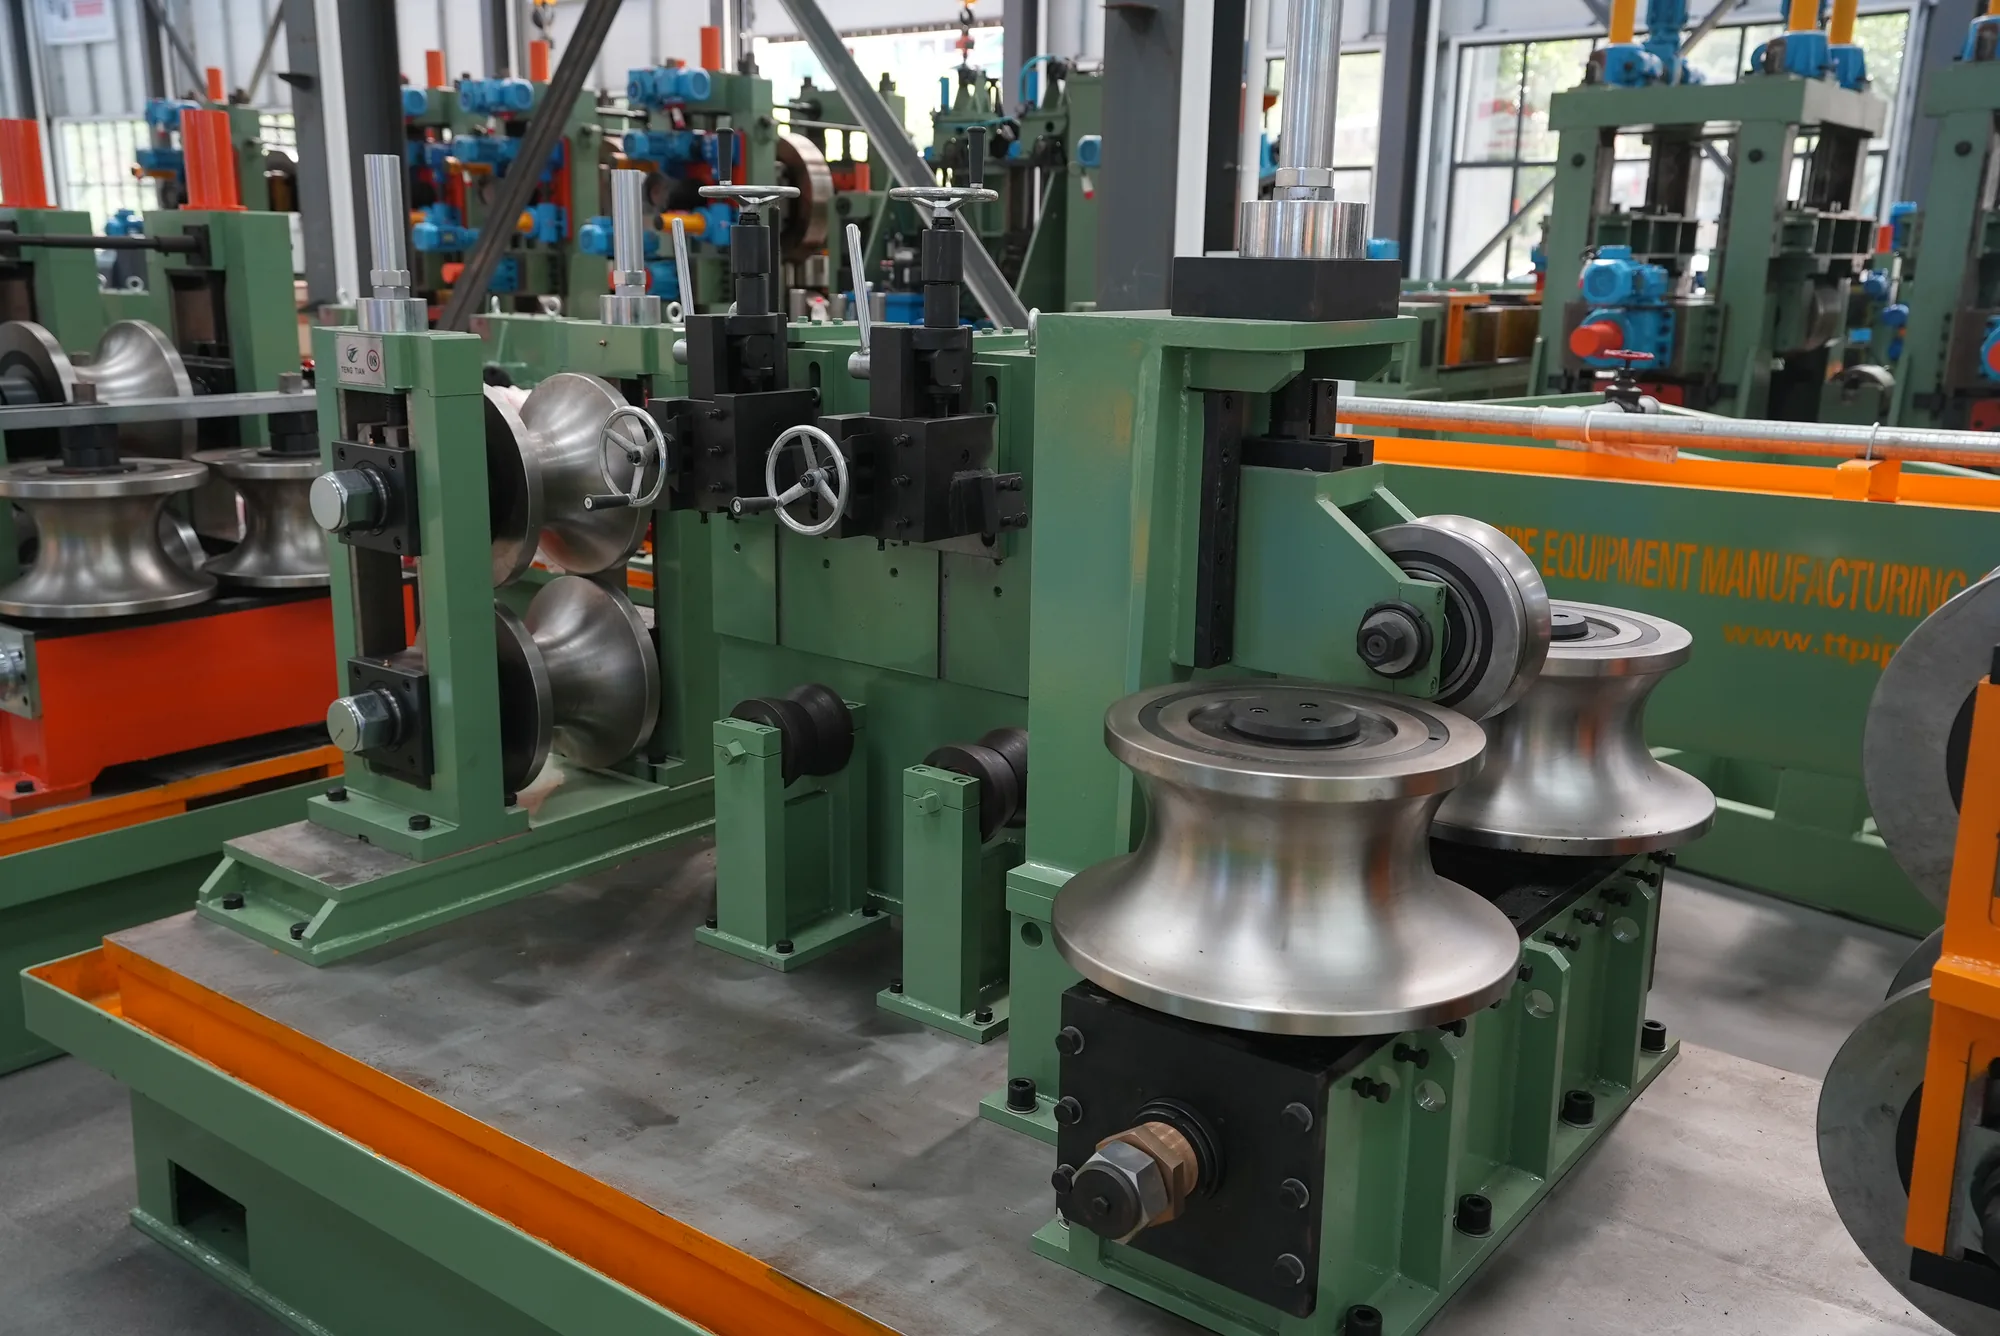 What Wears and What Gets ReplacedDifferent welded-pipe lines wear out different parts.See the line →
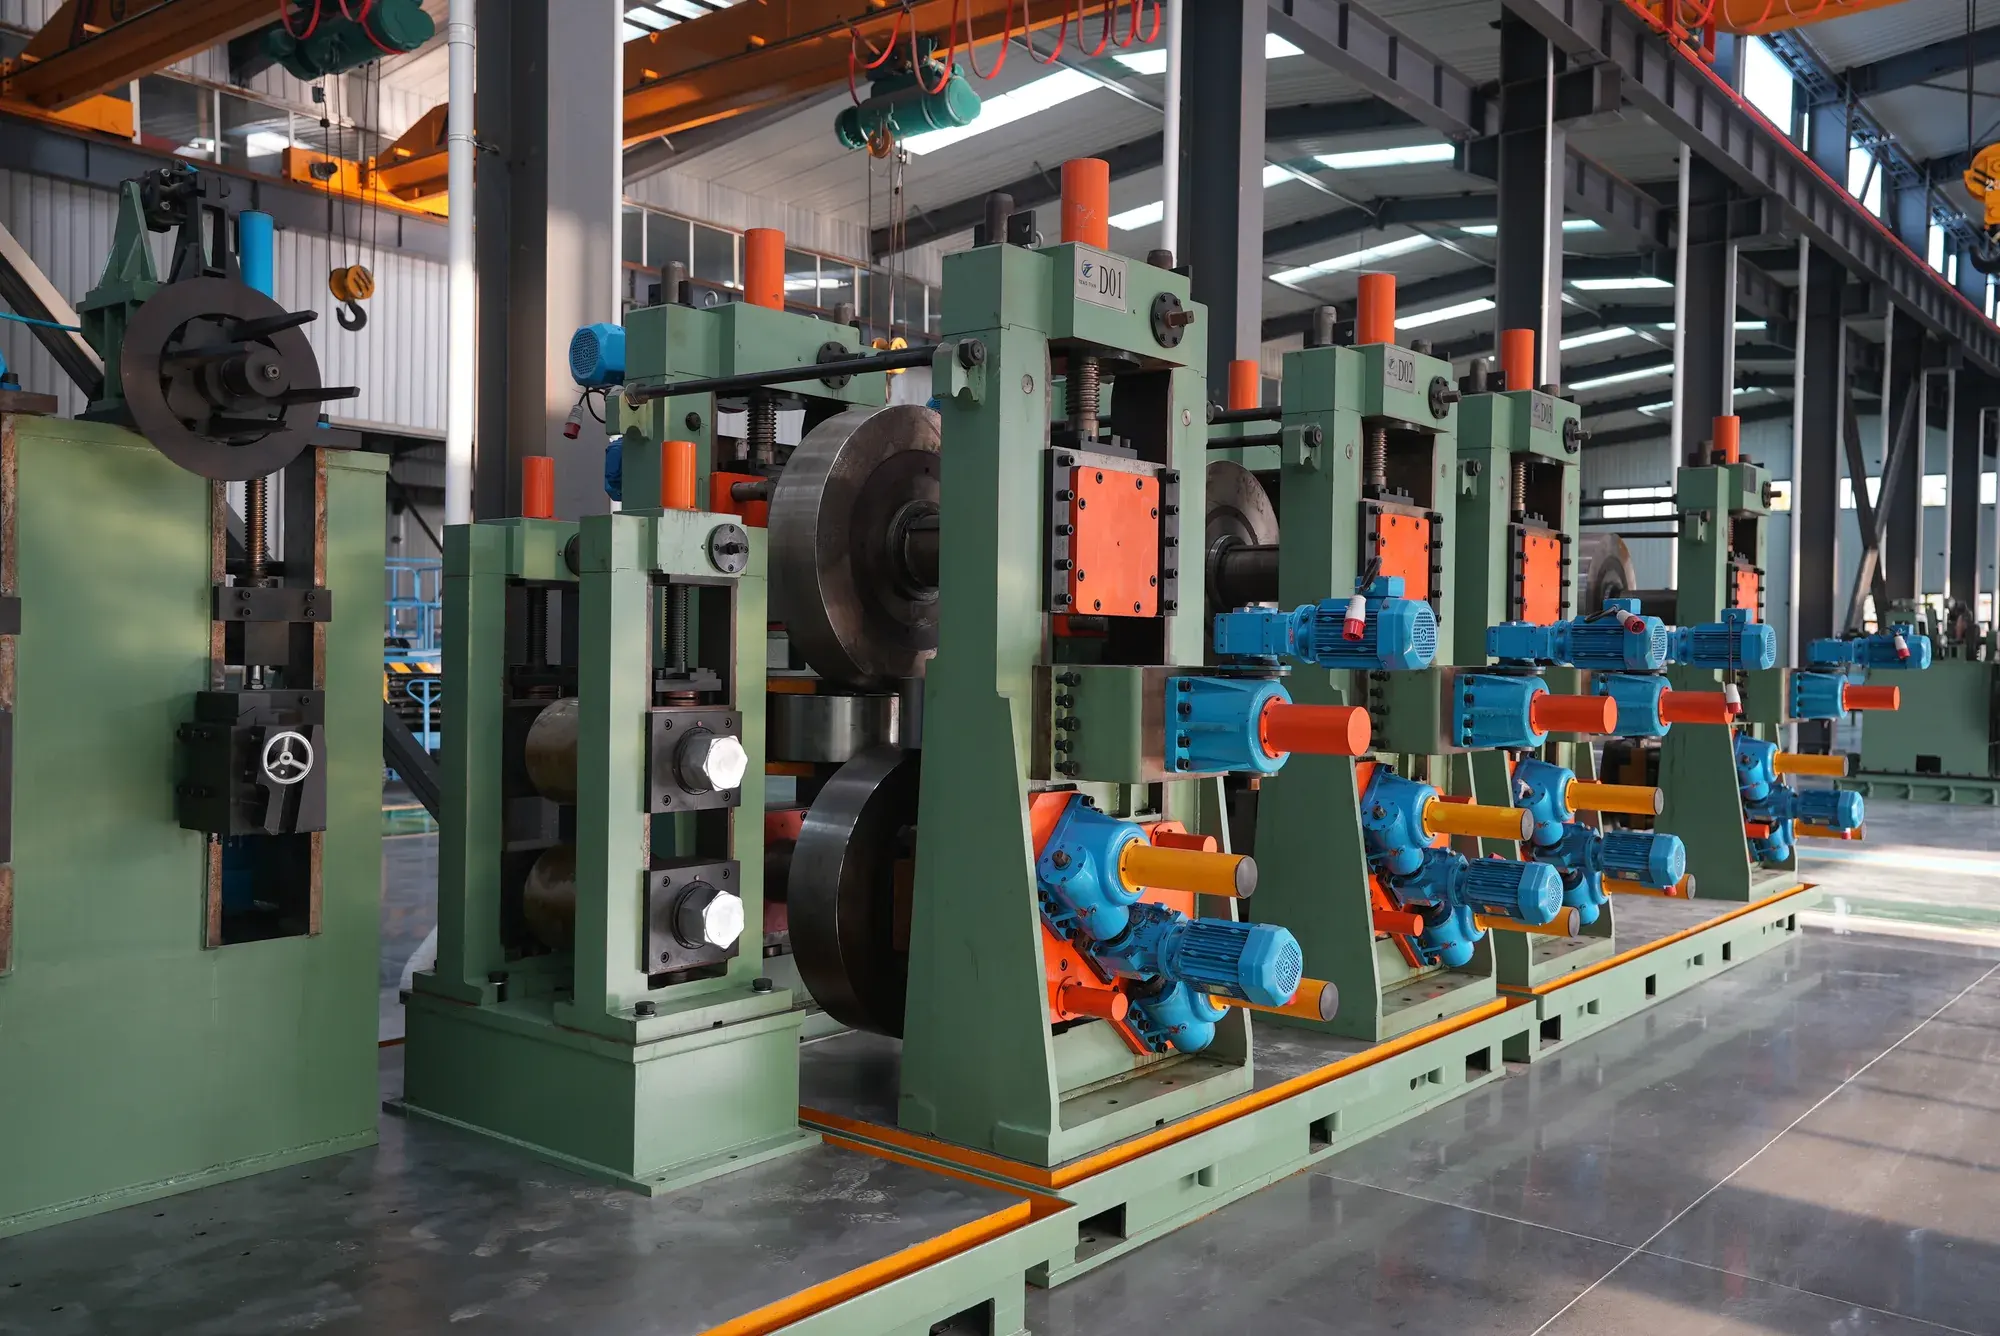 Roll Forming RollersRolls are where a tube mill’s accuracy is either created or lost.See the line →
What Tube Mill Rolls and Spare Parts Cover
A tube mill wears in three different ways at once, and the parts list follows that split rather than a single catalogue. Tube mill rolls — the forming and sizing rolls — are contact parts: they shape the strip, they wear by production volume, and they are replaced rather than consumed.
Consumables are the second group. On a high-frequency line these are the saw blades and cutting tools that cut the finished pipe to length, the induction coil and impeder that concentrate the welding current at the seam, and the process media — cooling water or emulsion for post-weld cooling and forming lubrication, plus hydraulic oil and grease for the power pack and bearings.
The third group is line-specific tooling that only exists on one family of machine: slitting knives with their spacers and rubber sleeves on a slitting line, plasma torch tips and electrodes on a spiral line’s flying cutter, milling inserts for the edge miller, and NDT couplant and calibration blocks on an API inspection train.
Buyers often ask whether a Chinese supplier can keep spares flowing after delivery. The answer depends on the part: some we machine ourselves, and others we source or specify for local purchase.
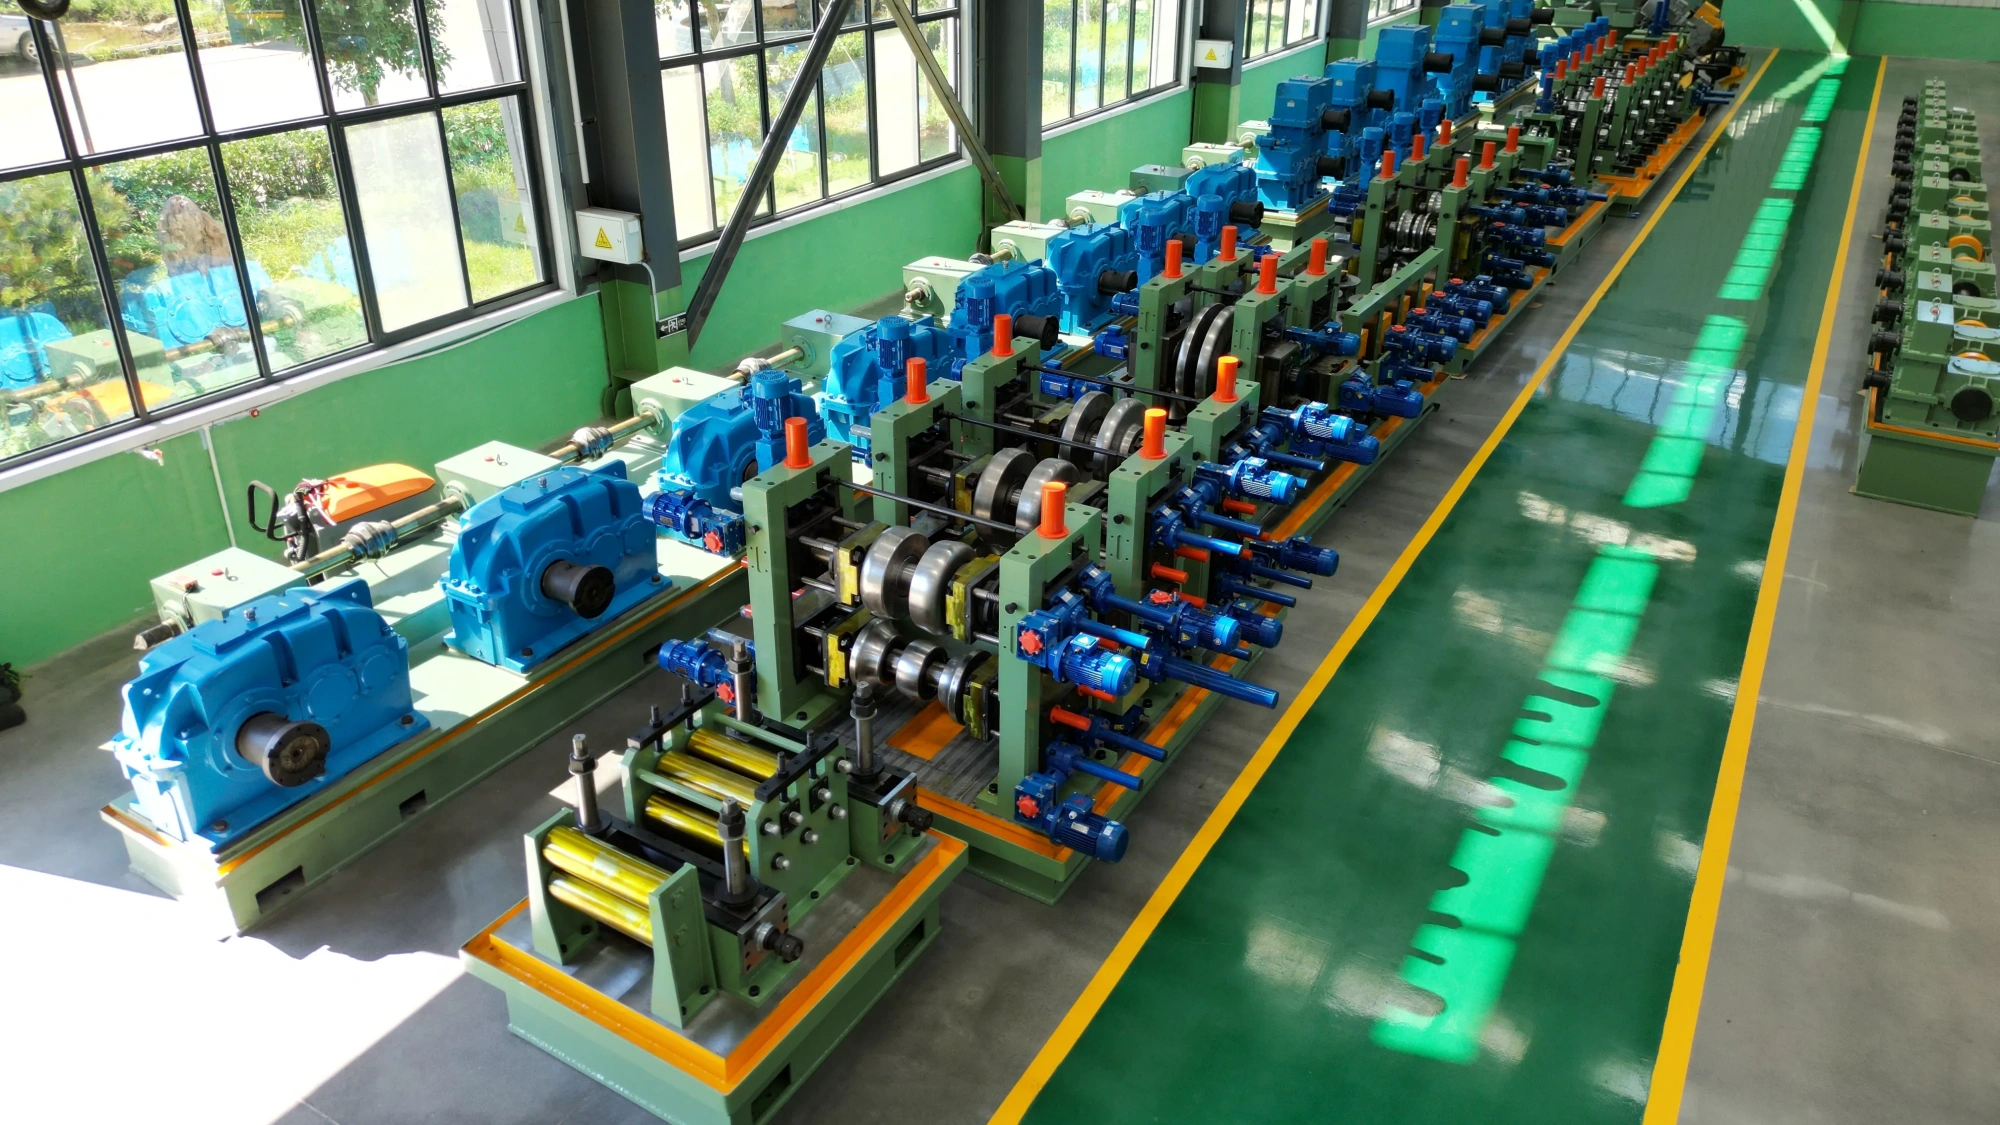
Tube Mill Rolls and Spare Parts, Line by Line
High-frequency welded tube mill. Five categories apply. Saw blades and cutting tools are consumed by cutting volume and normally ship with an initial batch. The induction coil and impeder are fast-wearing consumables replaced by welding hours, and can be ordered as line spares.
Cooling water or emulsion and hydraulic oil or grease are process media: we give the specification, the buyer purchases locally. Forming and sizing rolls are wear-replacement spares, and a changeover set of tube mill roll tooling is supplied with the line.
Spiral submerged arc line. Eight categories apply, and they are a different list because the process is different. Submerged arc welding consumes filler wire and flux; the line ships with two wire spools and with flux drying, magnetic separation and recovery equipment, while the flux itself is bought locally to our specification.
Forming, pressure, pre-bending and levelling rolls are wear-replacement spares: the Φ130 pressure rolls are GCr15 bearing steel hardened to HRC 56–60, and the feeding, straightening, vertical and pre-bending rolls are 42CrMo hardened to HRC 52–58. Edge-milling inserts and the Φ500 cutter head are re-ground or replaced by milling volume, and the plasma torch tips and electrodes are consumed by the flying cutter. Facing tools and twelve sets of clamping dies serve the end-facing machine.
Ultrasonic probes and reference blocks — with Φ1.6 and Φ3.2 radial through holes, an N5 rectangular notch and a Φ6 flat-bottom hole — are the calibration set. The X-ray tube and its cooling parts are life-limited items replaced by cumulative exposure time.
Slitting line. Slitting knives, spacers, rubber sleeves and separator discs are the tooling that decides slit-width tolerance, burr and edge quality. The knife set is configured to strip thickness — roughly fifteen strips at 2 mm down to four strips at 8 mm — and holds width to ±0.2 mm with burr no more than 4% of thickness.
API inspection train. This is a consumable and calibration category — couplant and calibration blocks for the NDT stations — replenished according to inspection volume.
Key Figures for Wear Parts and Tooling
- Slit width tolerance held by the knife set: ±0.2 mm; burr ≤ 4% of strip thickness; knife configuration by strip thickness.
- Spiral pressure rolls: Φ130, bearing steel, quench hardened HRC 56–60; feeding, straightening and pre-bending rolls 42CrMo, HRC 52–58.
- Spiral edge-milling cutter head: Ф500 mm.
- Ultrasonic reference block features: Φ1.6 / Φ3.2 radial through holes, N5 notch, Φ6 flat-bottom hole.
- X-ray tube cooling: water, flow > 4 L/min, inlet temperature ≤ 35 °C.
- Spiral line spares supplied with the machine: two welding wire spools, twelve clamping dies for the facing machine.
Why Roll Consumption Differs So Much Between Lines
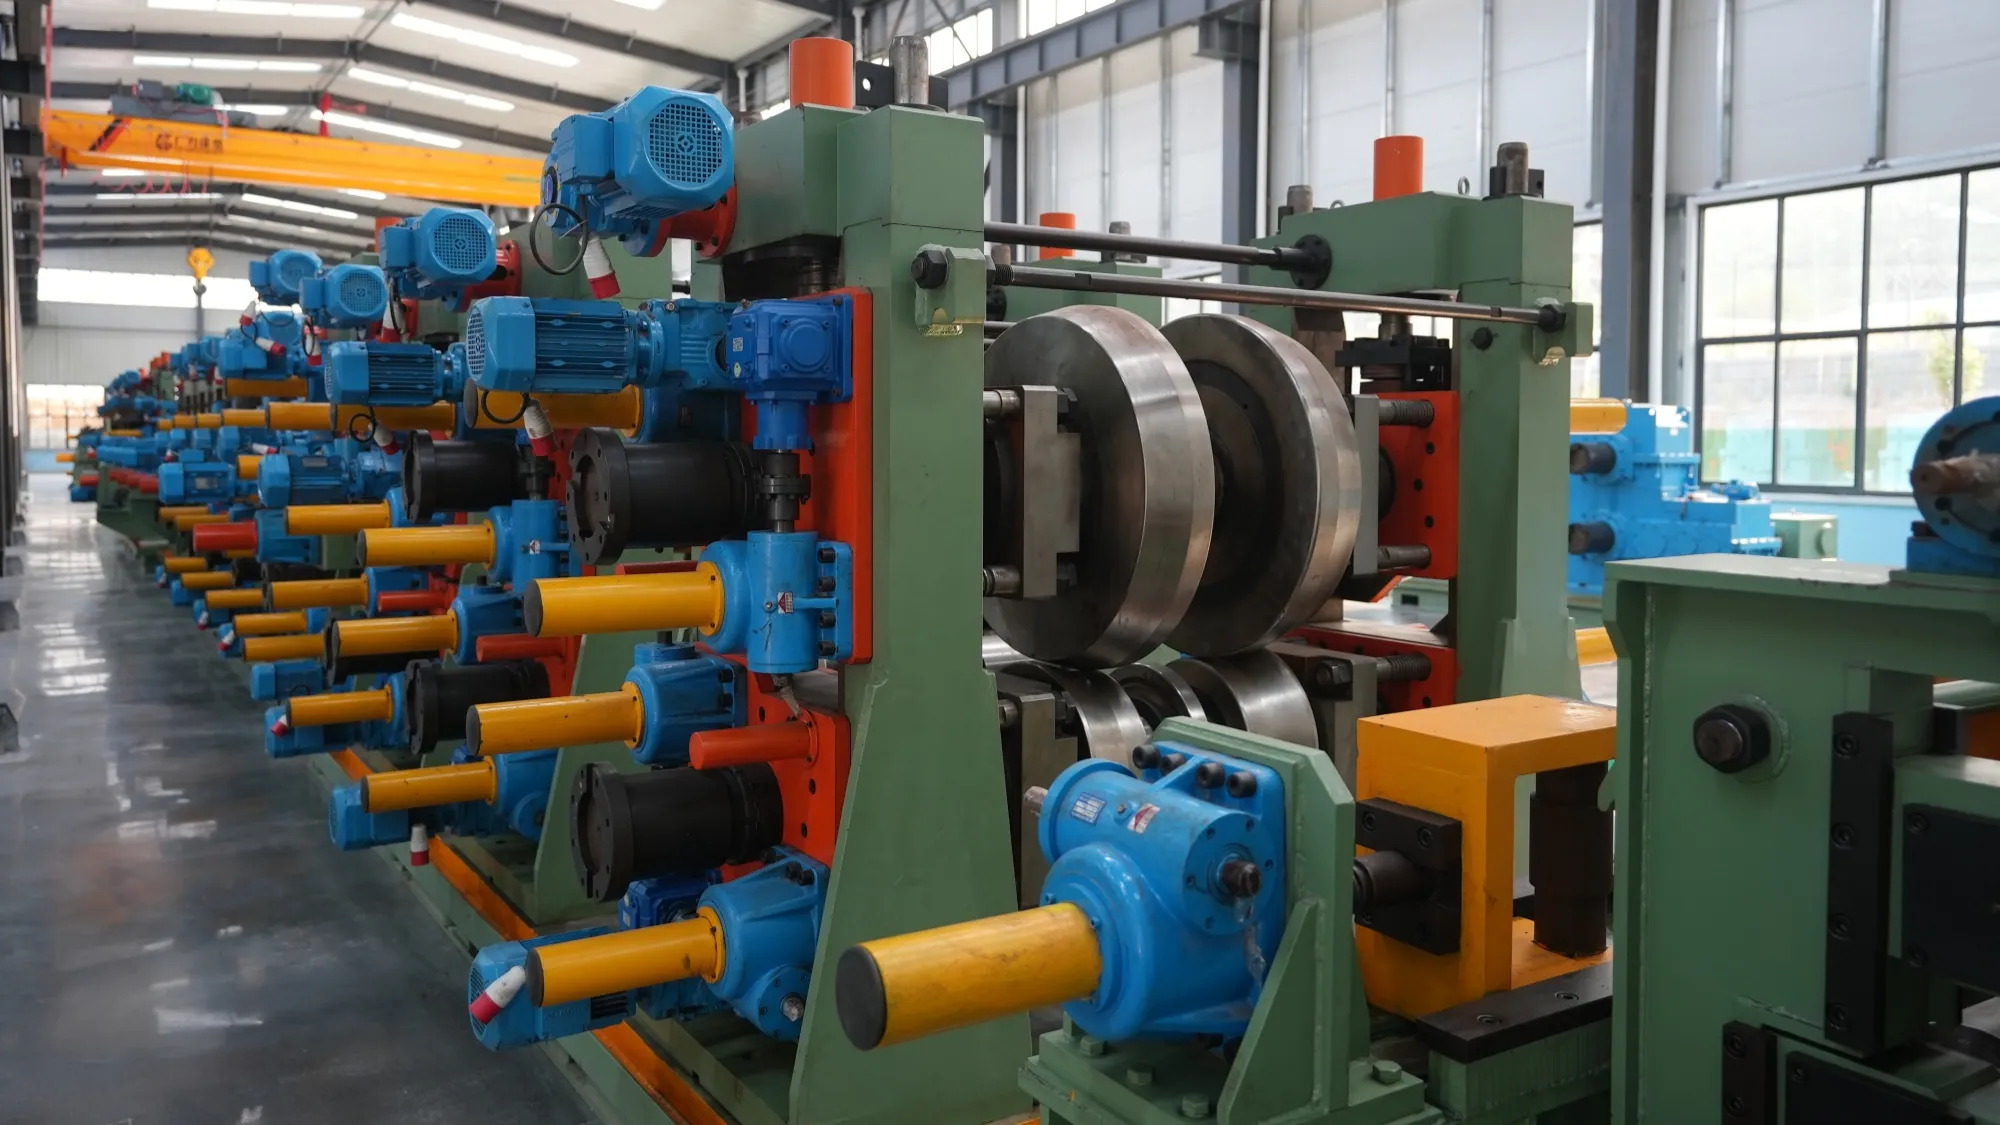
Two lines with the same output can have completely different roll bills. A conventional tube mill changes size by changing rolls, so every size in the production plan is a set of tube mill rolls that has to be bought, stored, fitted and eventually re-machined.
A direct-forming square line changes size through a combined mould and a servo adjustment instead, and the consequence is a roll saving of more than 90% together with longer tooling life. There is one exception: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
The operating step matters too. Setting a new size means adjusting roll gap and servo parameters and re-centring — with a roll change on a conventional line, without one on a direct-forming line. If it is done badly, the profile drifts and trial pipes are scrapped.
That is why the spares conversation cannot be separated from the line-selection conversation.
What In-House Roll Machining Actually Changes
We machine rolls ourselves rather than buying them in. When rolls come from an outside tool shop, lead time, cost and consistency depend on that shop; machining them on our own CNC equipment keeps all three under our control.
Our manufacturing base is our own and open to visits, and our twenty R&D engineers average twenty years of experience.
The service side is separate from the manufacturing side: our after-sales team, online support, engineers dispatched to site, and spares shipped direct rather than routed back through the original project channel.
Where Our Lines Run
The sizes span from small round tube at 76 × 3 mm up to square section at 250 × 250 mm and 200 × 200 × 12 mm. Our lines have gone to 25 countries — most make construction tube, and others run fire-extinguisher tube, furniture tube and other sections.
How to Choose Spares
Choosing spares comes down to three questions.
Which line is it for? The part lists above do not overlap. Filler wire belongs to the submerged arc process; a high-frequency line has no filler wire at all, because the seam is made by high-frequency induction welding of the strip edges themselves. Asking for “welding wire for pipe mill” therefore has two different answers depending on which mill is meant.
How long will it last? Service life depends on material, throughput and operating practice, so it is best assessed against your own production conditions.
Is it a wear part or a consumable? Rolls, cutter heads, probes and X-ray tubes are replaced on condition and are worth stocking as a set. Blades, torch tips, wire, flux, couplant, oil and emulsion are consumed continuously and are better handled as a standing order sized to throughput.
Scope of Supply, Installation and Commissioning
Precision and wear items travel in wooden cases. Electrical cabinets, induction coils and impeders, forming rolls and cutting tools are crated with moisture protection, the main frames are braced, and a spare-parts pack ships with the container.
Tube Mill Spare Parts Supply After Delivery
After delivery, we stay your tube mill spare parts supplier: rolls come from our own CNC shop, engineers can be sent to site, and spare parts ship to you directly rather than back through the original project channel.
Do Tube Mills Use Welding Wire?
High-frequency welded tube mills use no filler wire. The seam is formed by high-frequency induction heating and forge pressure on the strip edges, so the consumable that plays the equivalent role is the induction coil and impeder, not wire.
From the Workshop
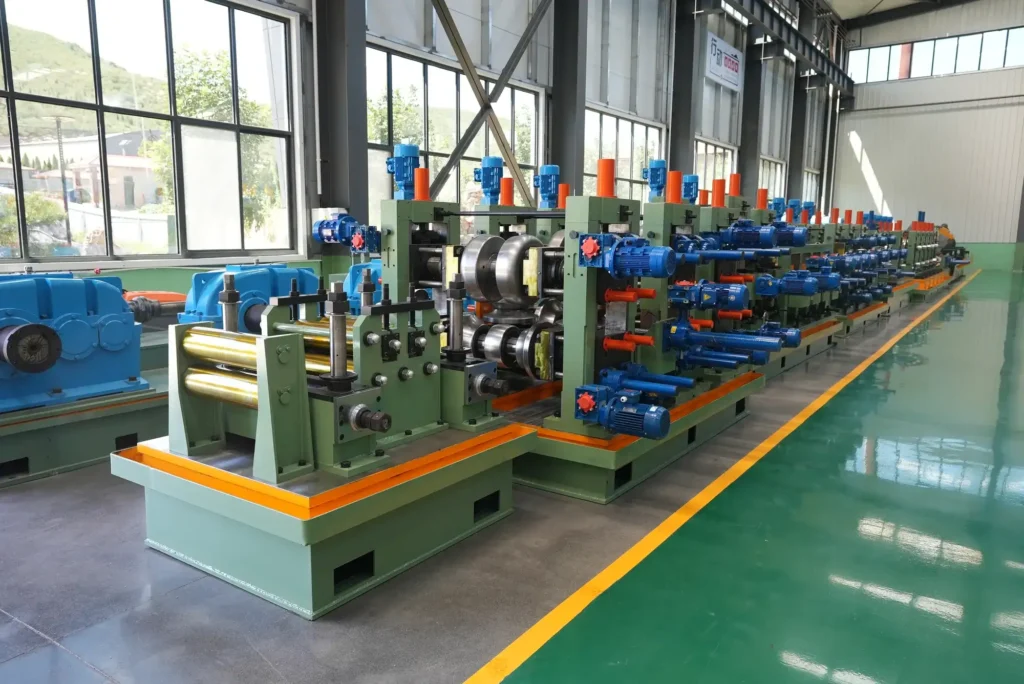 Tube Mill Manufacturer
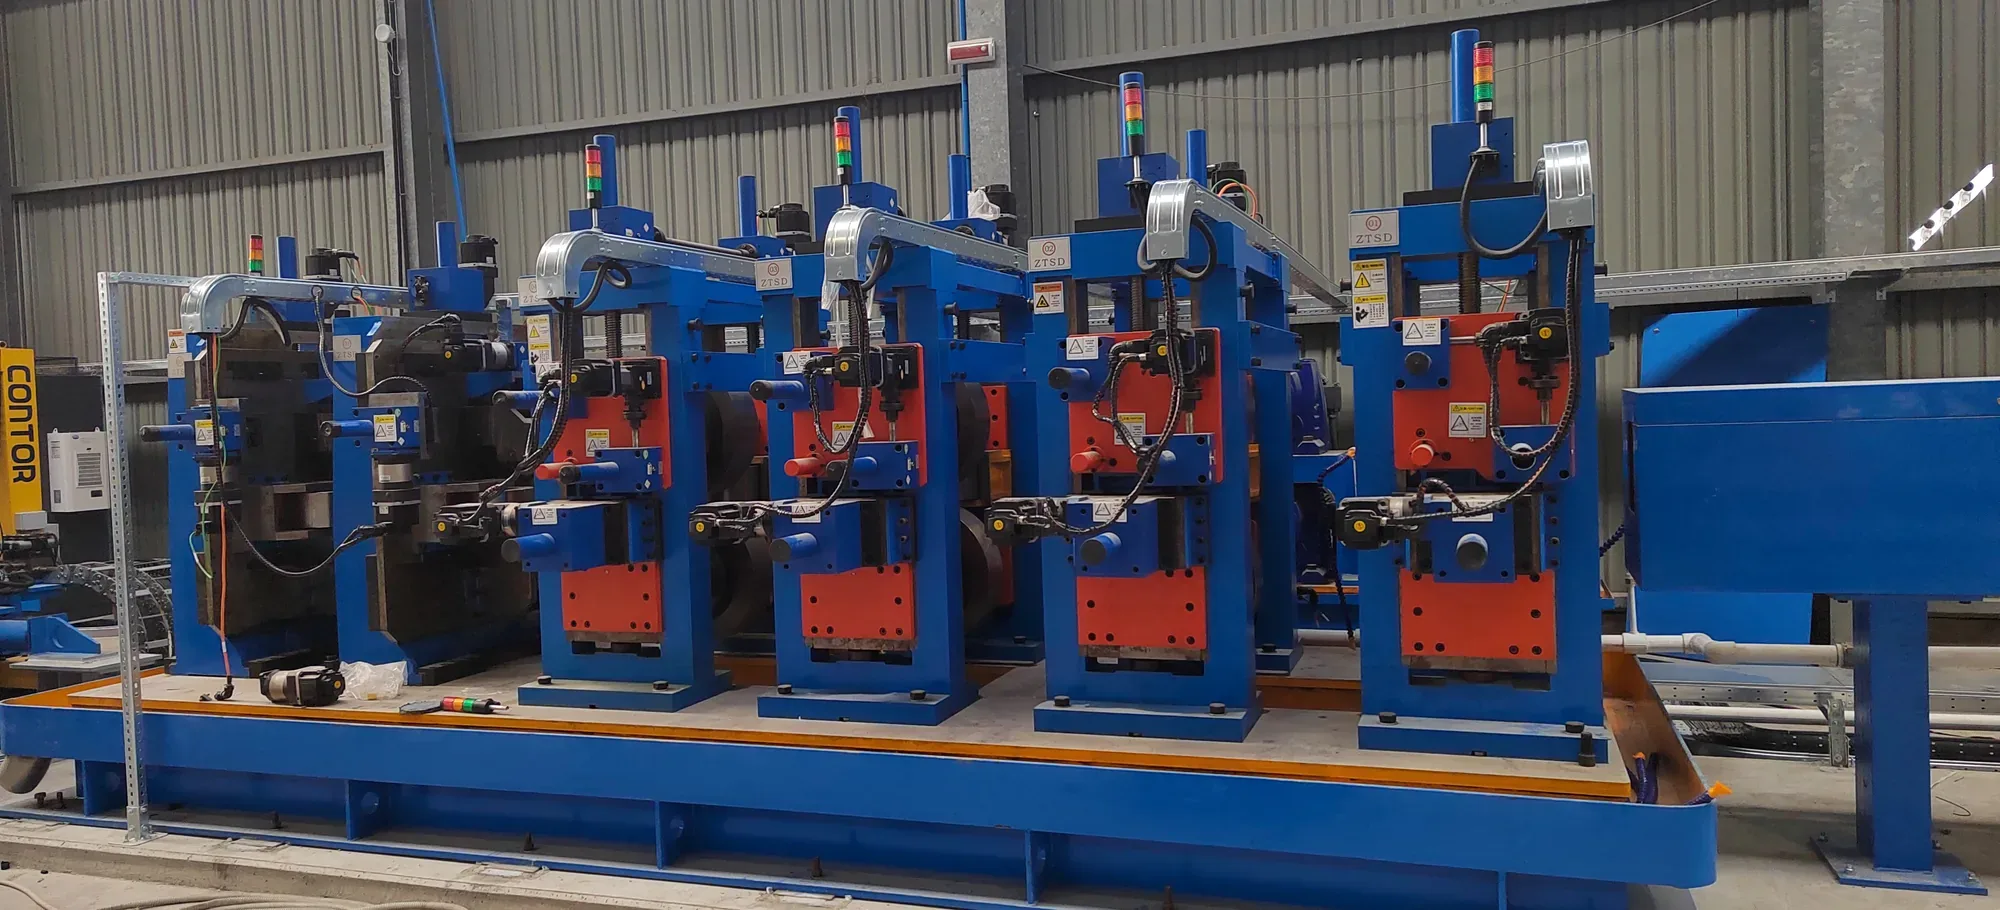
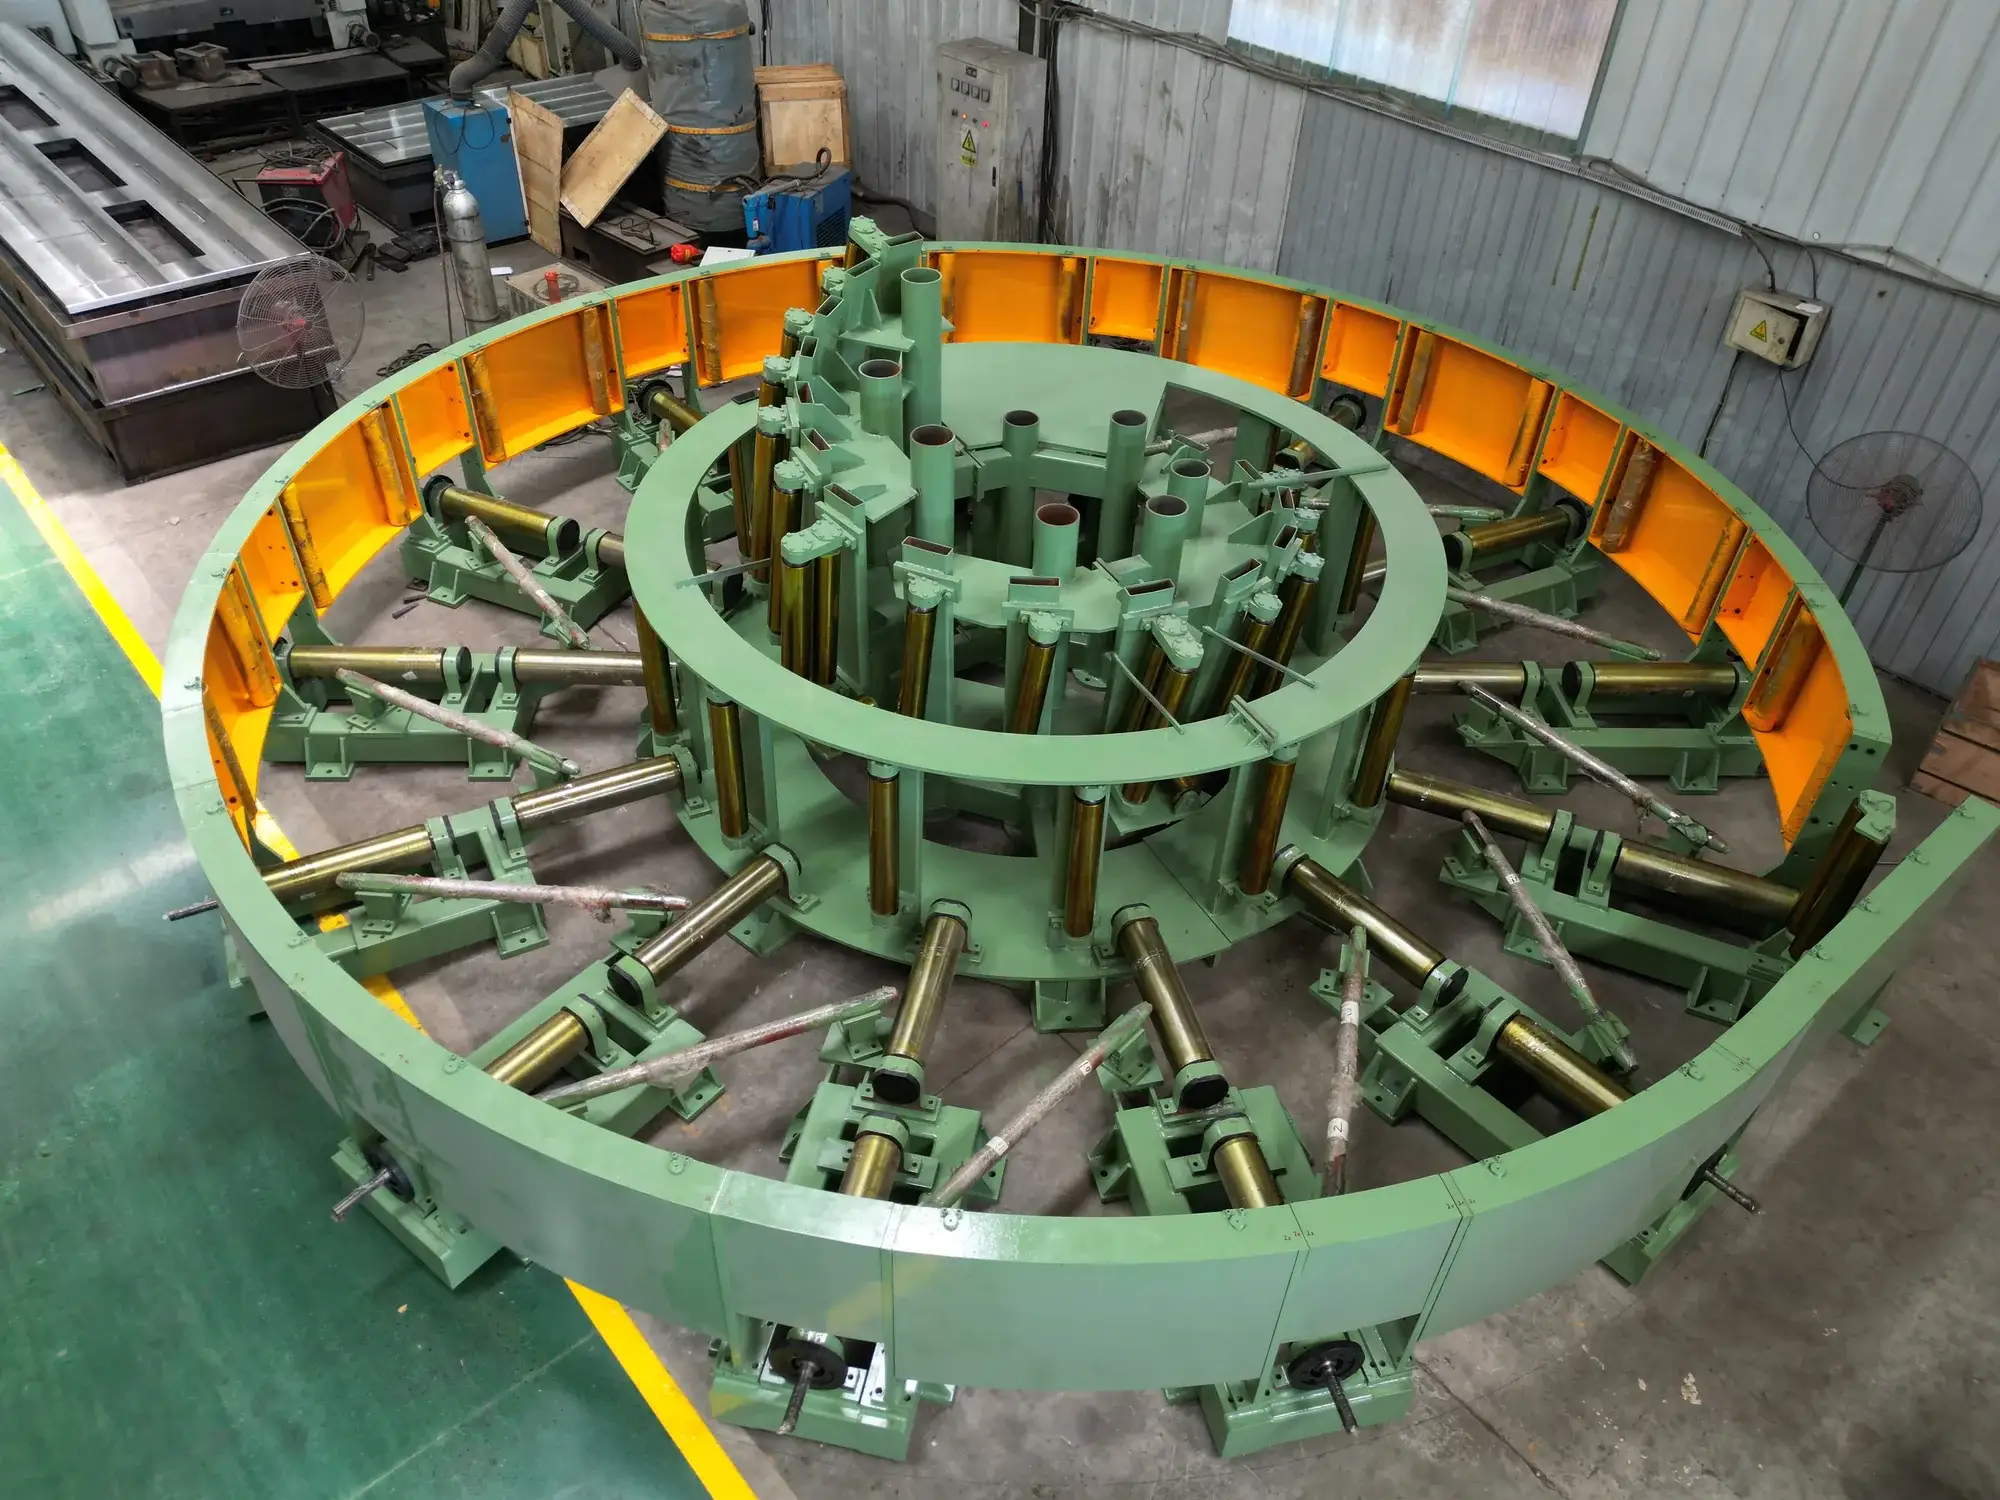
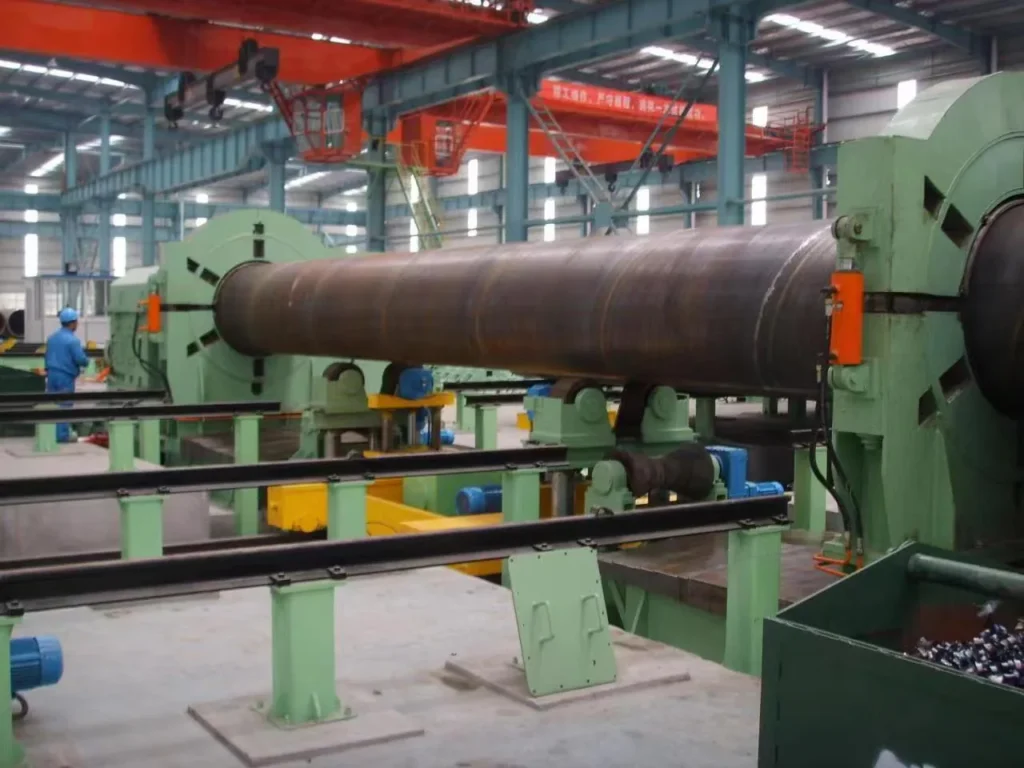 SSAW Spiral Welded Pipe Mill
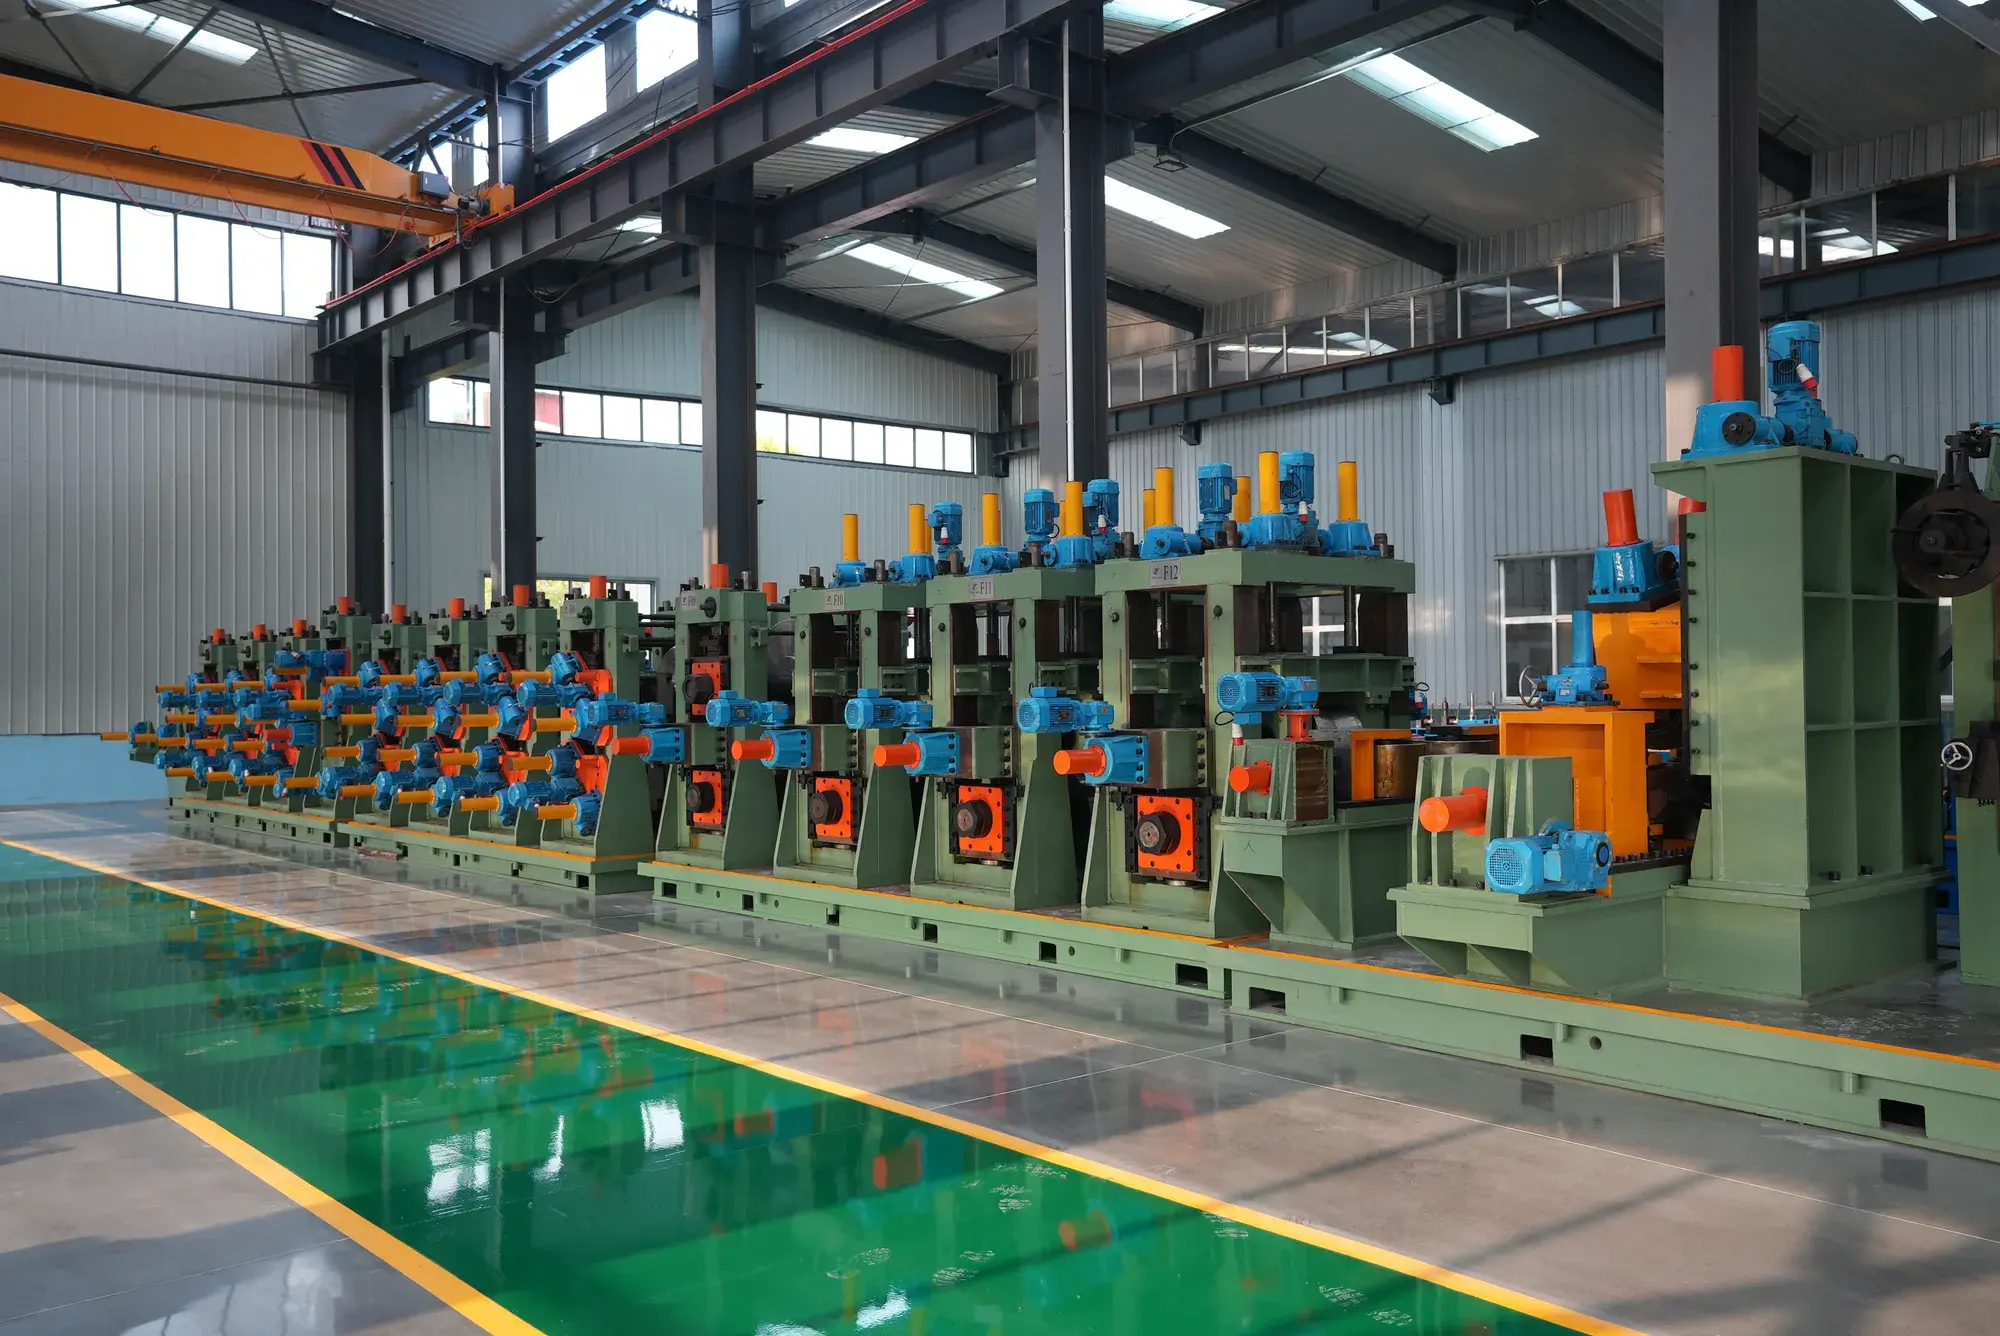
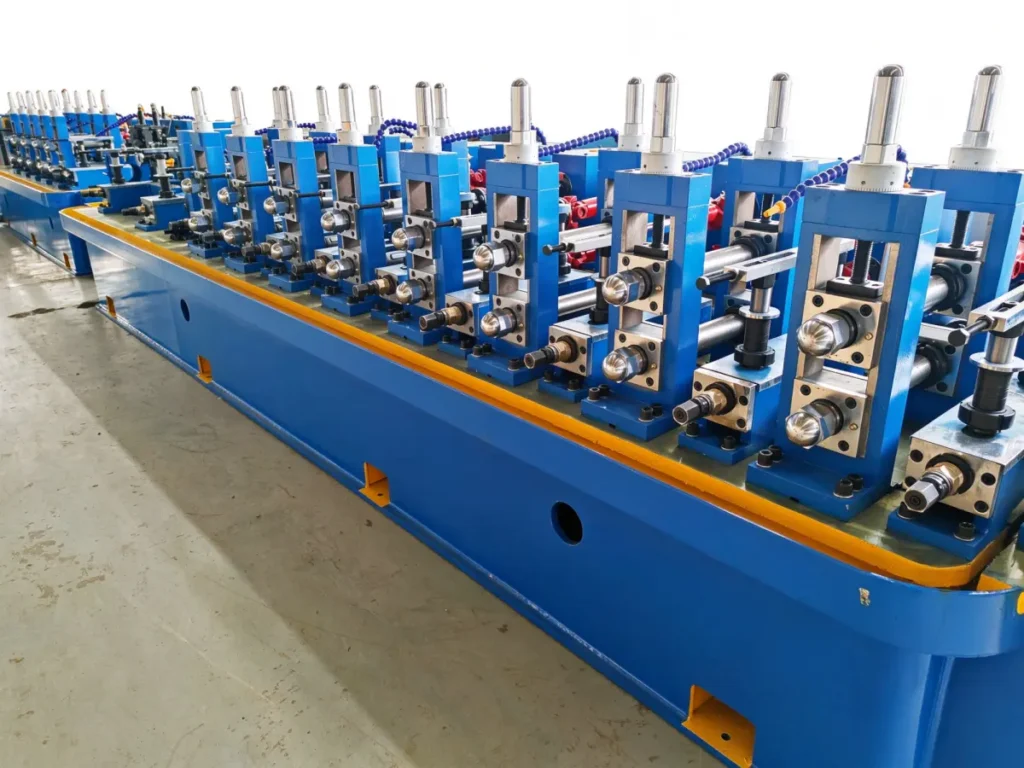 Small Diameter Tube Mill
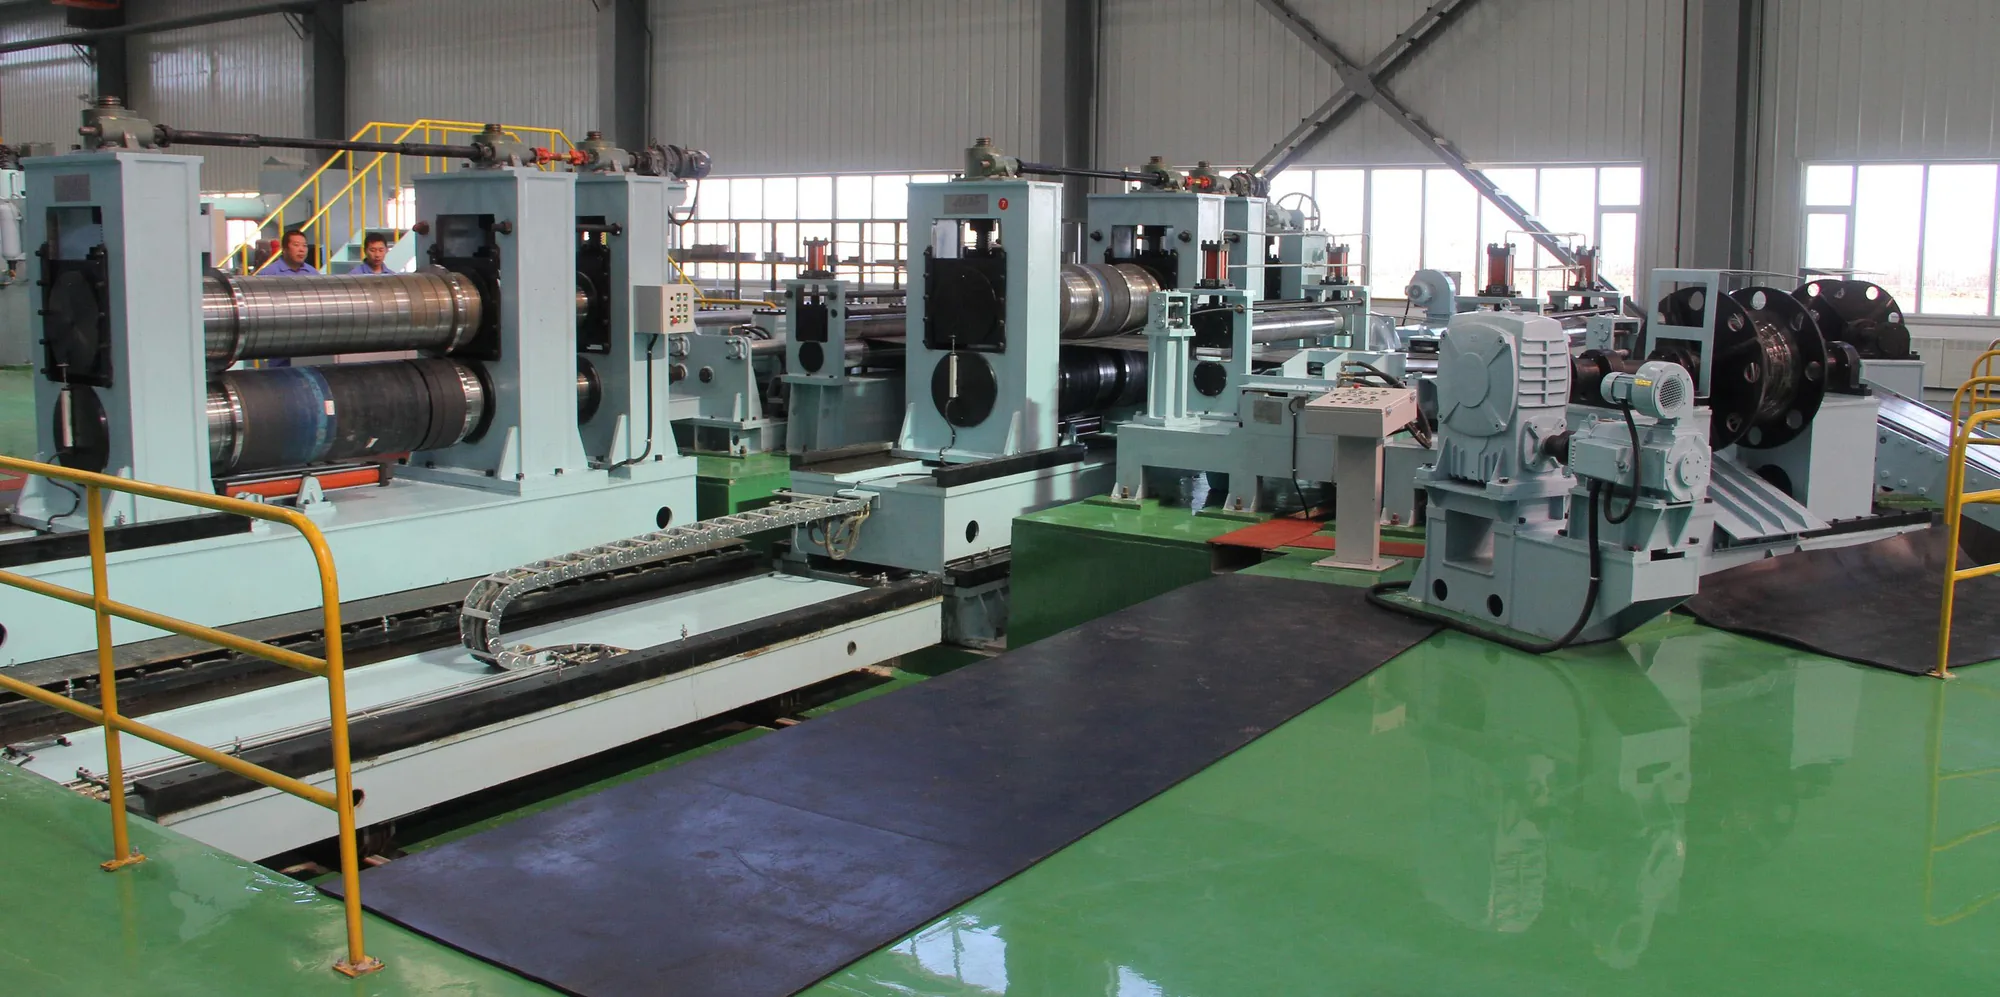 Steel Coil Slitting Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.