
Home › Resources › Welded Pipe Guide › How a Tube Mill Works
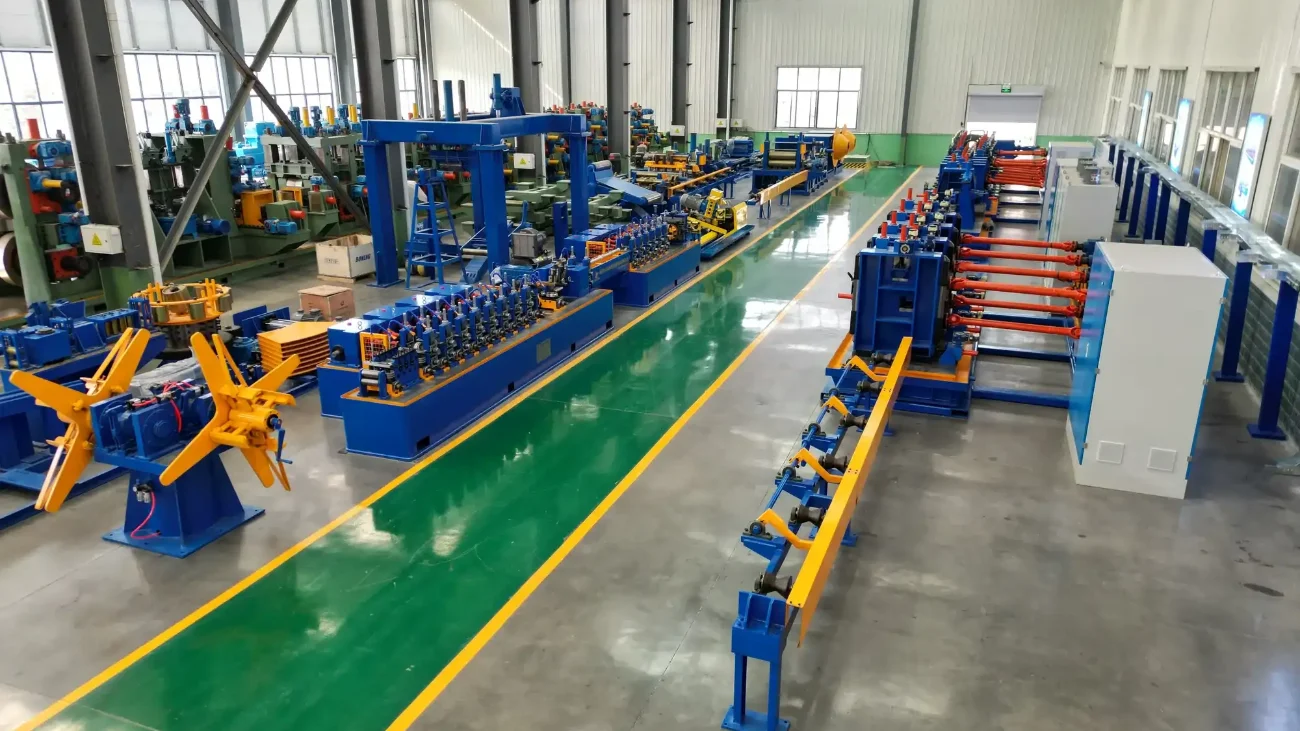
A tube mill turns a steel coil into welded pipe in one continuous line: uncoil, level on the larger sizes, shear and joint-weld, accumulate, roll form, high-frequency weld, size and straighten, then cut to length. Tengtian’s tube mill & welded pipe production line covers Φ10 to Φ630 mm in twelve bands, and the terms used along the way are explained in the tube & pipe mill glossary.
From Coil to Cut Pipe, Stage by Stage
- The line runs eight stages, from uncoiling to flying-saw cut-off.
- A spiral accumulator lets the mill keep forming while the next coil is shear-welded on.
- Welding heat comes from skin and proximity effect concentrating HF current at the open seam.
- Welder power is banded by diameter, from 150 kW to 1500 kW.
- On high-end configurations, material yield can reach 93% or more.
How a Tube Mill Works
A tube mill is a complete forming-welding-sizing set that takes coil as its raw material and produces straight-seam welded pipe, round or square, across twelve bands from HG32 to HG630, covering outside diameters of Φ10 to Φ630 mm at wall thicknesses of 0.5 to 16 mm. It is one continuous machine train, not a sequence of separate operations.
Uncoiling loads and tensions the coil on an expanding-mandrel uncoiler. On HG89 and larger lines a five-roller leveller then flattens the strip, because strip flatness is the precondition for forming quality.
An automatic shear-welder joins the tail of one coil to the head of the next, and a spiral accumulator stores strip so the mill never stops while that joint is made. Forming rolls then work the flat band progressively into the required round or square open tube blank.
How a Tube Mill Works — Method and Measured Values
High-frequency current concentrates at the open edges of the blank through skin effect and proximity effect, heating just that line to welding temperature; squeeze rolls then press the two heated edges together and the seam is made under pressure rather than by filler. The welder and its power bands are set out under high-frequency welded pipe mill.
After welding the tube is cooled, sized to final outside diameter and straightened, and a flying saw cuts it to length while the line keeps running.
Two figures apply at line level. Welder power is matched to the diameter range and banded from 150 to 1500 kW, so heat input stays consistent across the range. And on high-end configurations material yield can reach 93% or more, though actual yield also depends on how the buyer runs the plant.
Tube mill manufacturing process
The key stages each have their own governing parameters. For roll forming they include pass count, roll gap and roll form, which decide shape accuracy and seam alignment. For HF welding they include current frequency, power and welding speed. For pressure welding they include squeeze amount, temperature and alignment.
For the cooling, sizing and straightening stage they include sizing roll gap, straightening amount and cooling.
Operating the Line, Step by Step
The operating sequence has five steps, each calling for a defined level of skill.
- Load the coil and thread the strip. This needs operator training; the failure modes are strip wander, a loose coil and a failed thread.
- Join coils by shear-welding, timed against the accumulator. This also needs training; the failure modes are a broken-strip stoppage and scrap pipe at the joint.
- Set the size. On a conventional line the target diameter is set by changing rolls; on the direct-forming square line it is a servo adjustment with no roll change at all.
- Set welder power and speed, then run the line. This needs specialist process training, with under-fusion, burn-through and dimensional drift as the failure modes to guard against.
- Cut to length and collect the pipe. This is ordinary operation.
From the Workshop
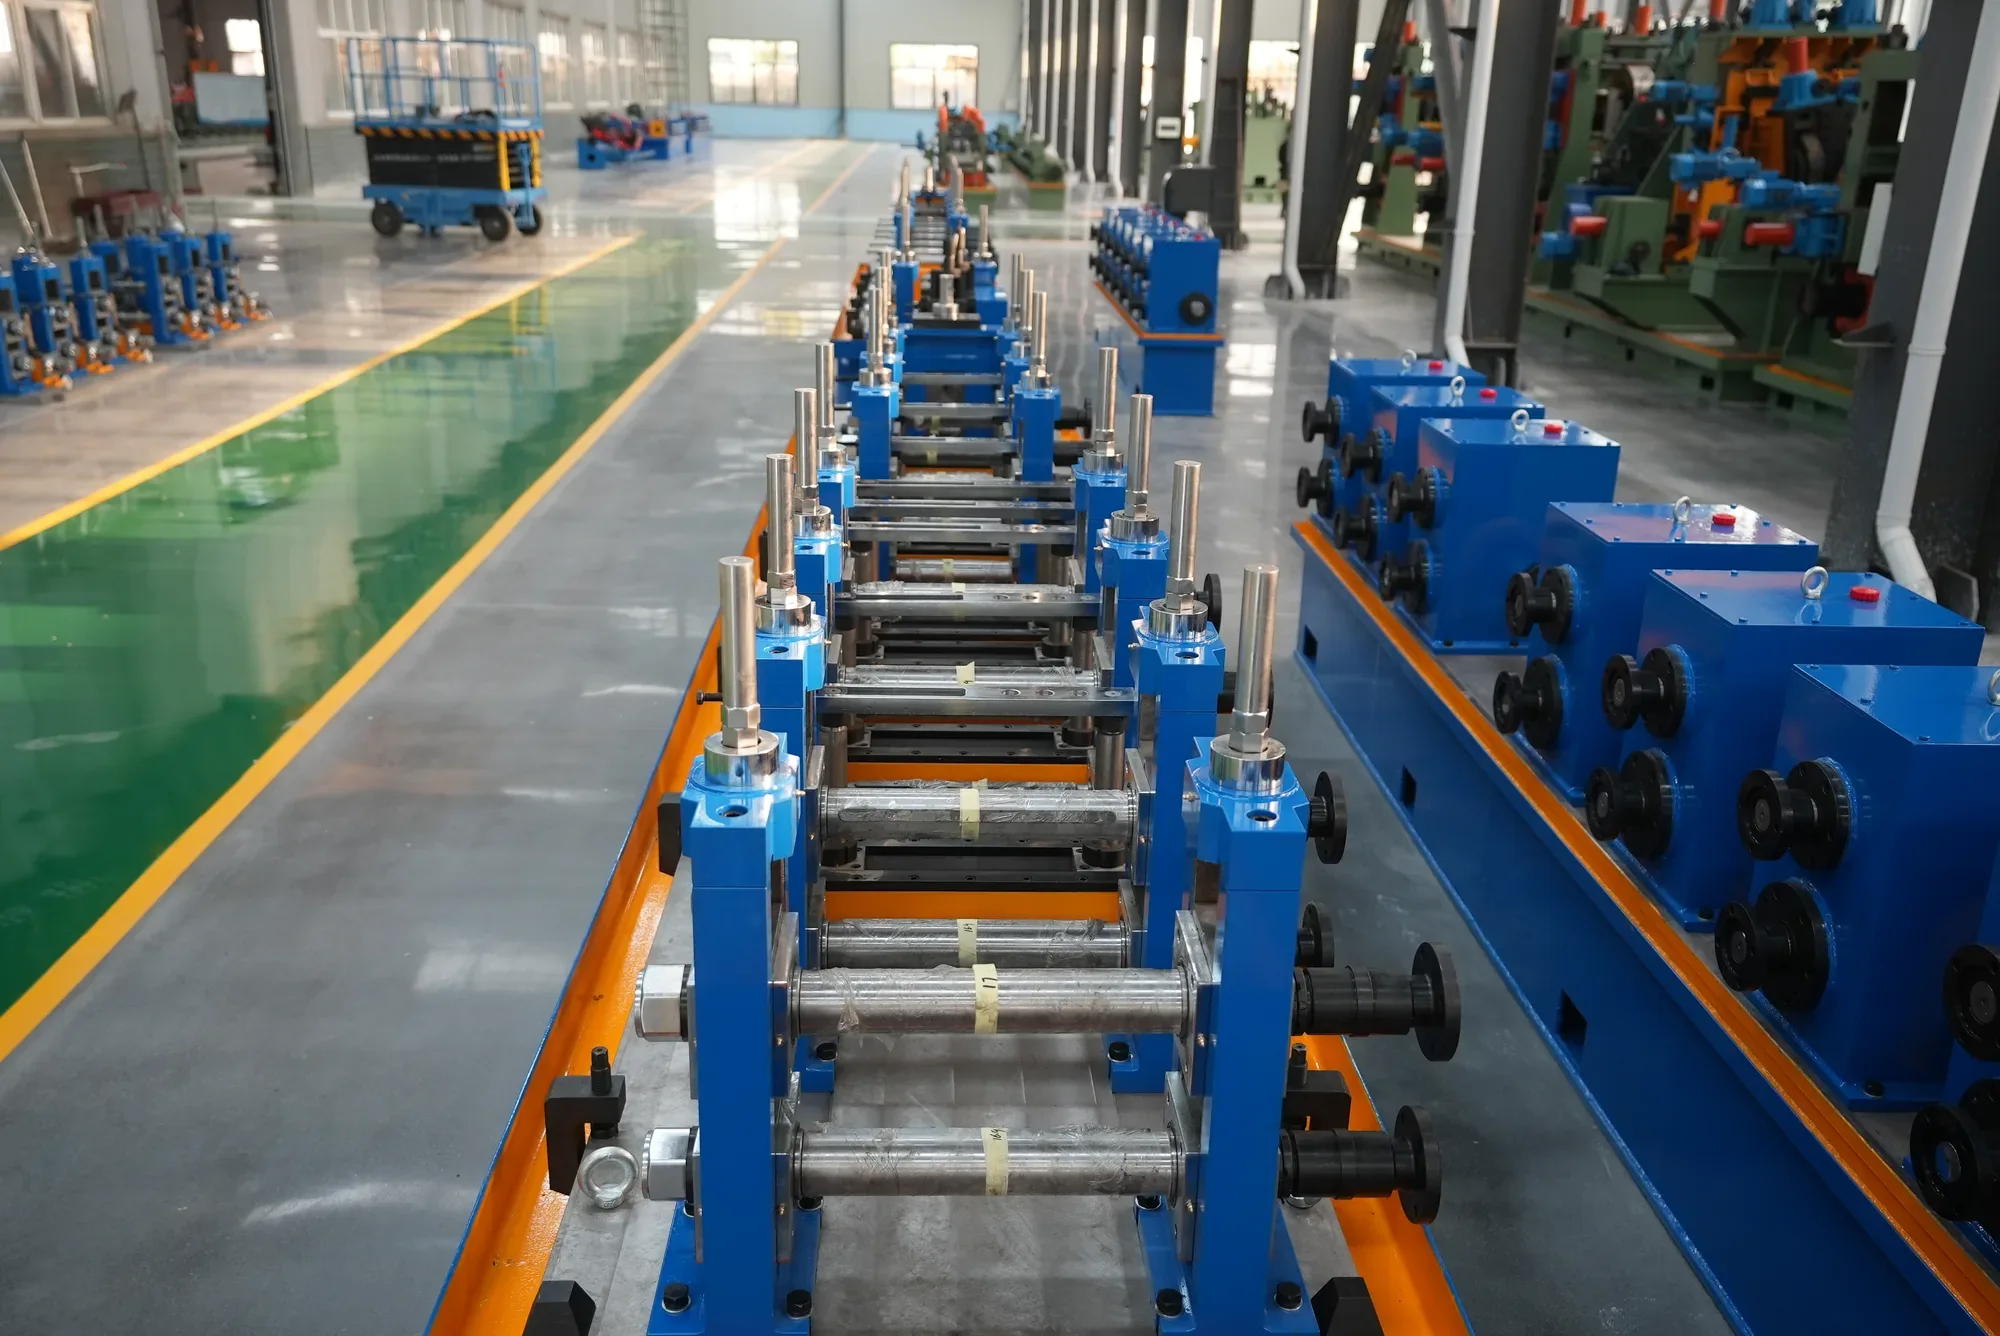
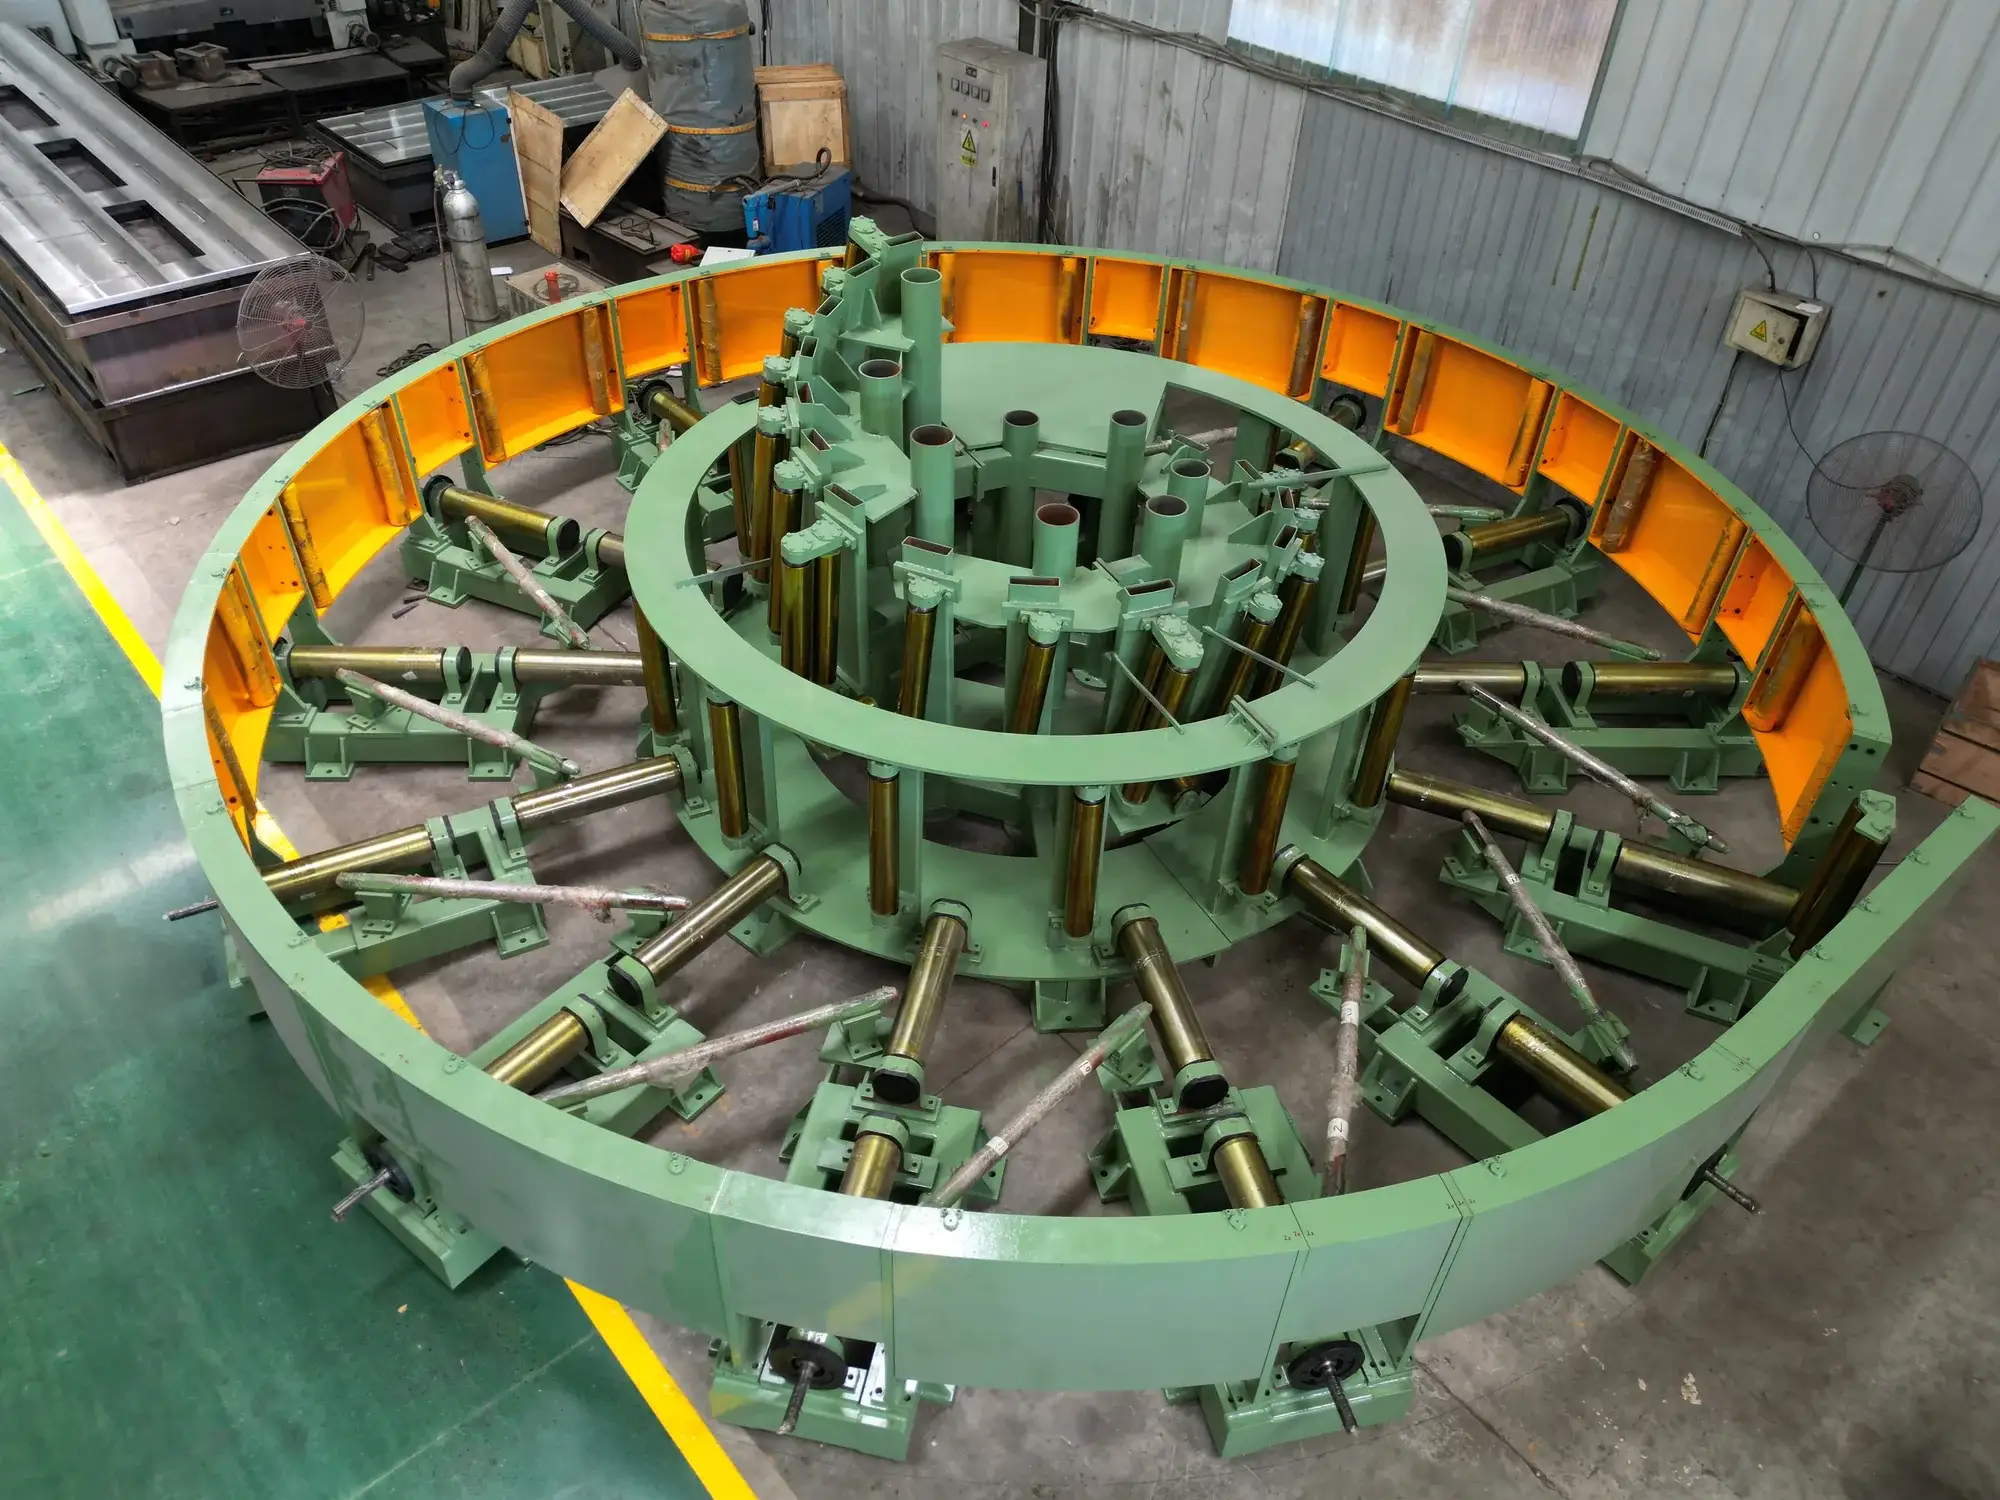
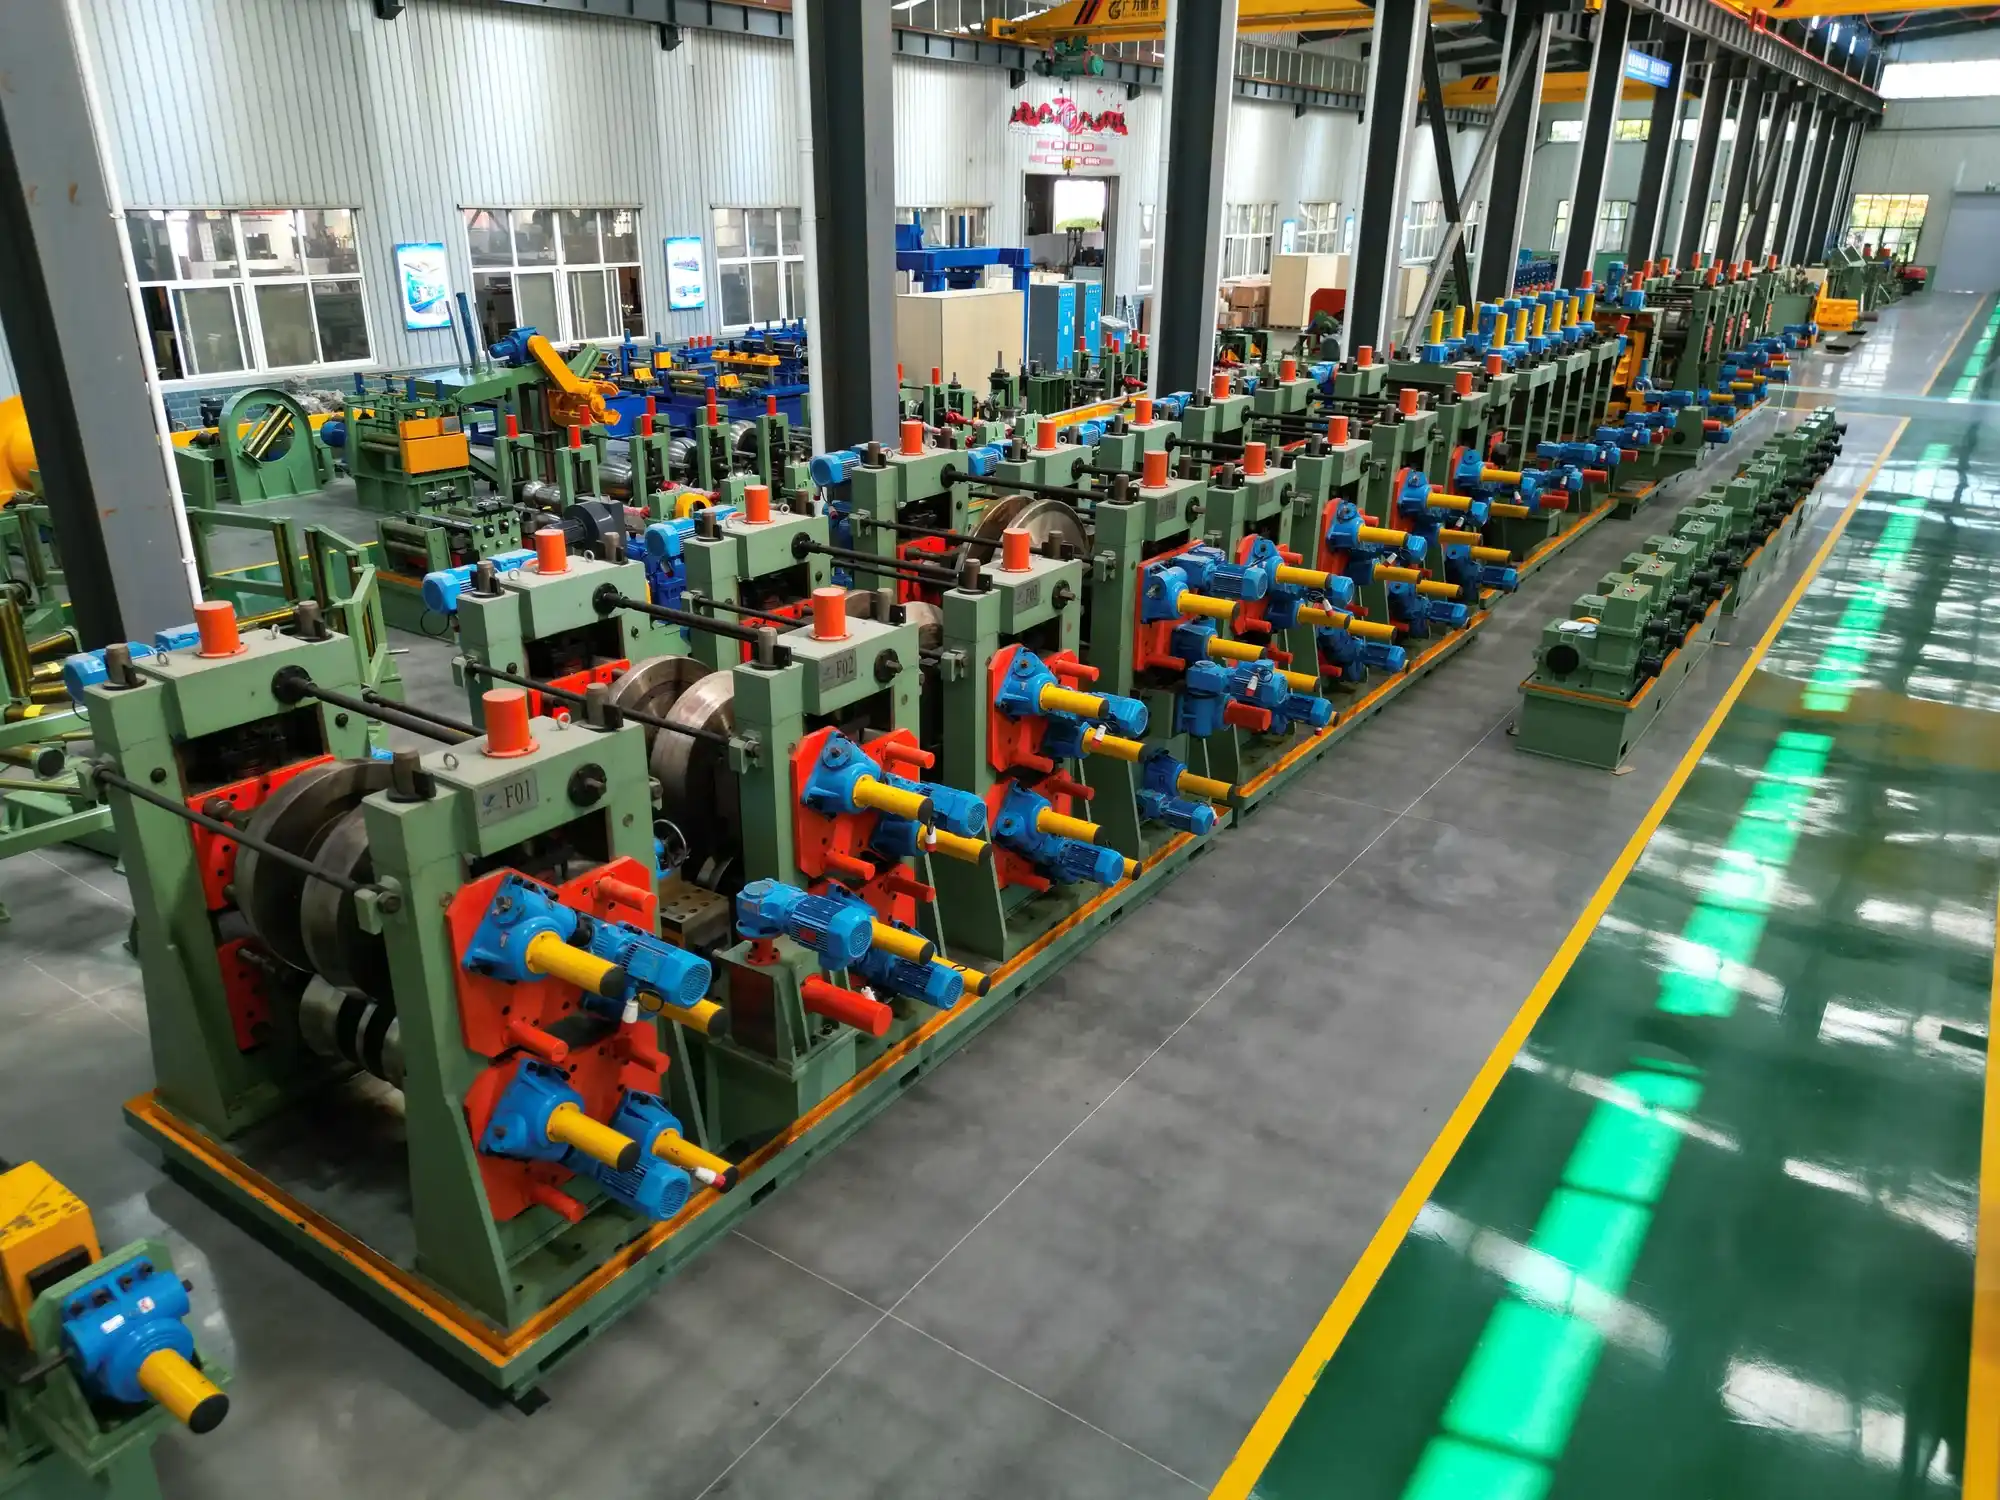
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.