
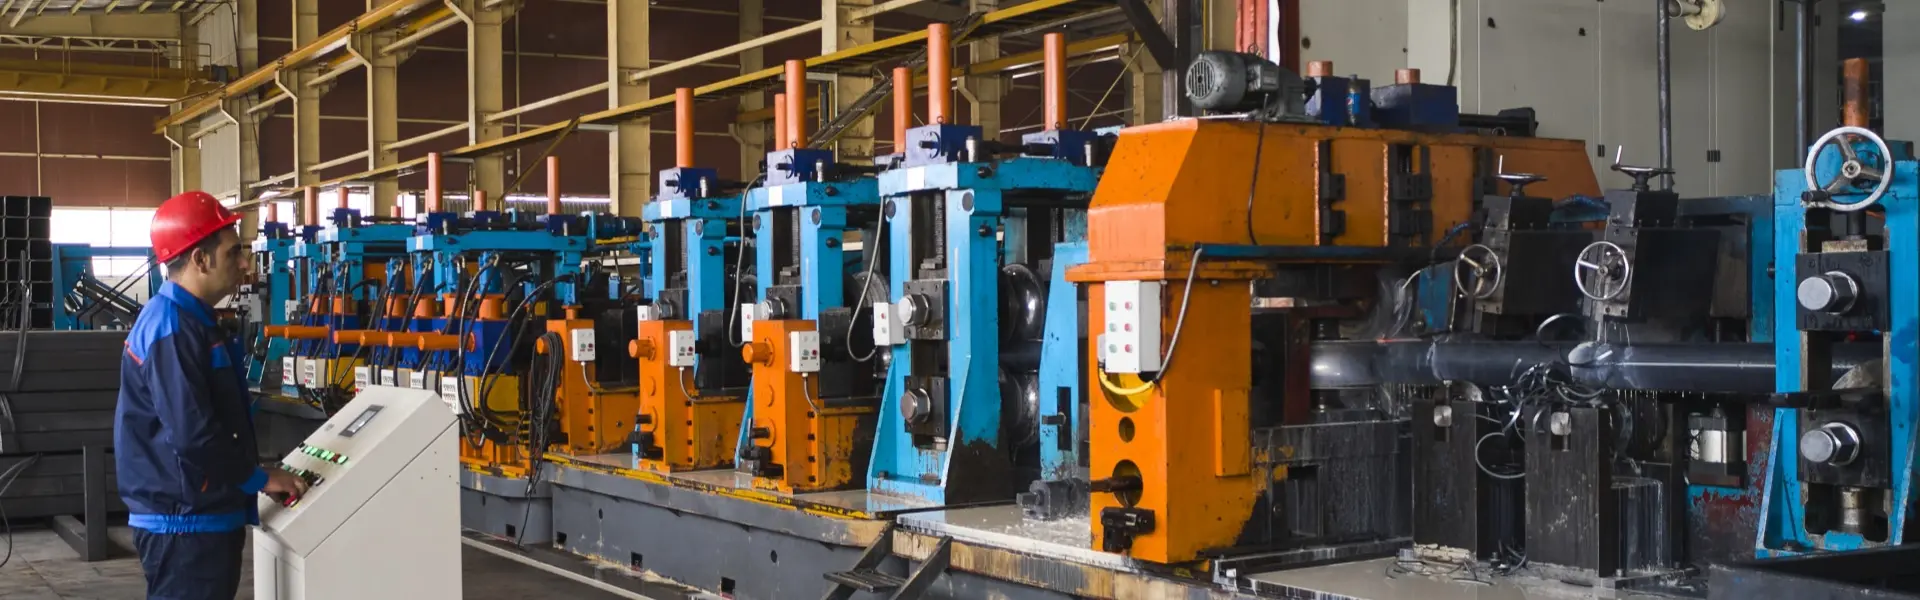
Large Diameter Tube Mill
In This Line
A large diameter pipe mill from Tengtian is one of the upper seven of our twelve HFW diameter steps, HG165 through HG630, covering finished pipe from Φ60 up to Φ630 mm with walls from 3.0 to 16 mm. Each step is a separate machine size with its own specification. The five smaller steps are on our small-diameter HFW tube mill page, and all twelve are set out under tube mill & welded pipe production line.
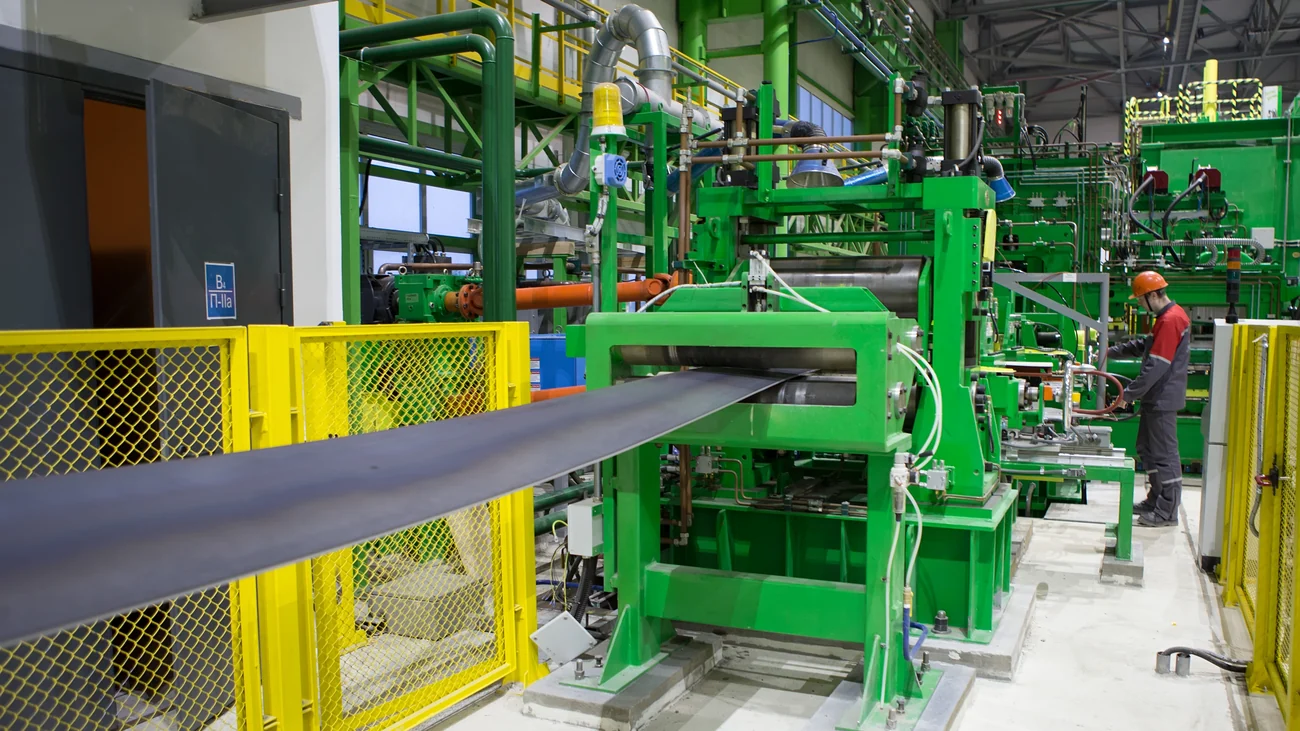
What Is Large-Diameter HFW Tube Mill
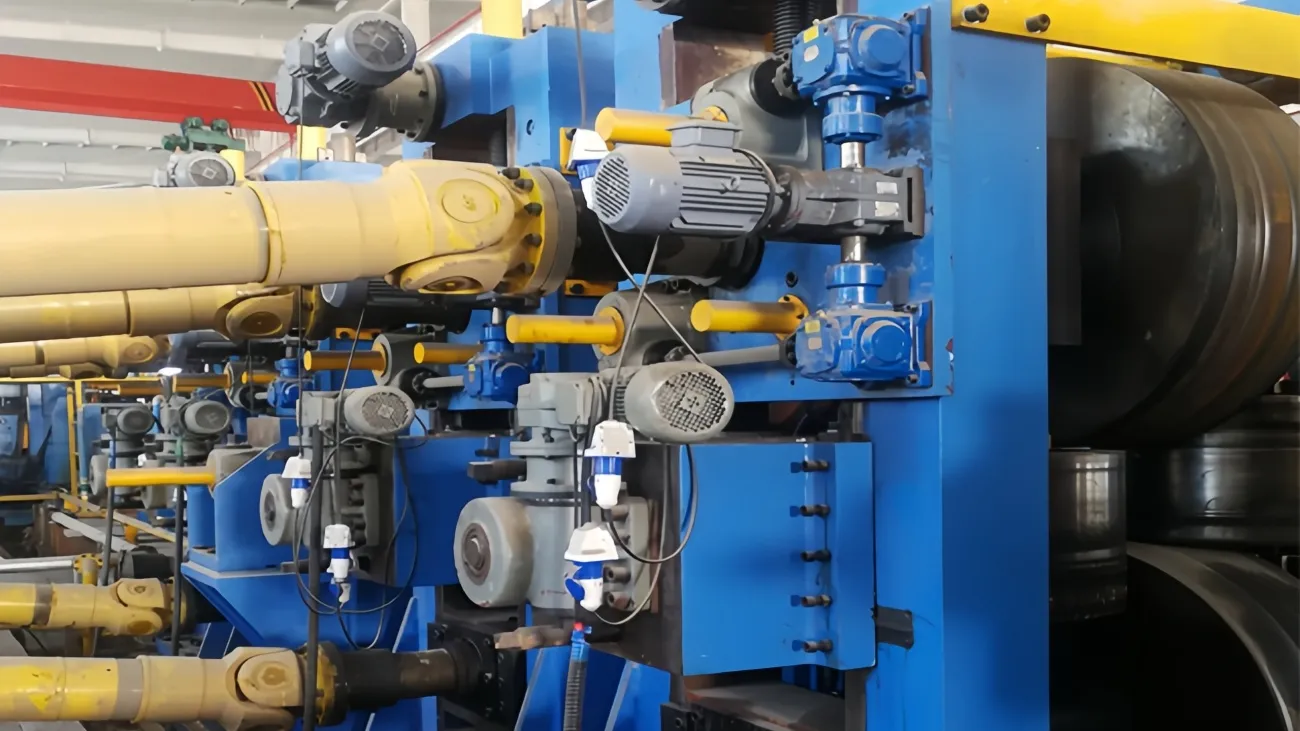
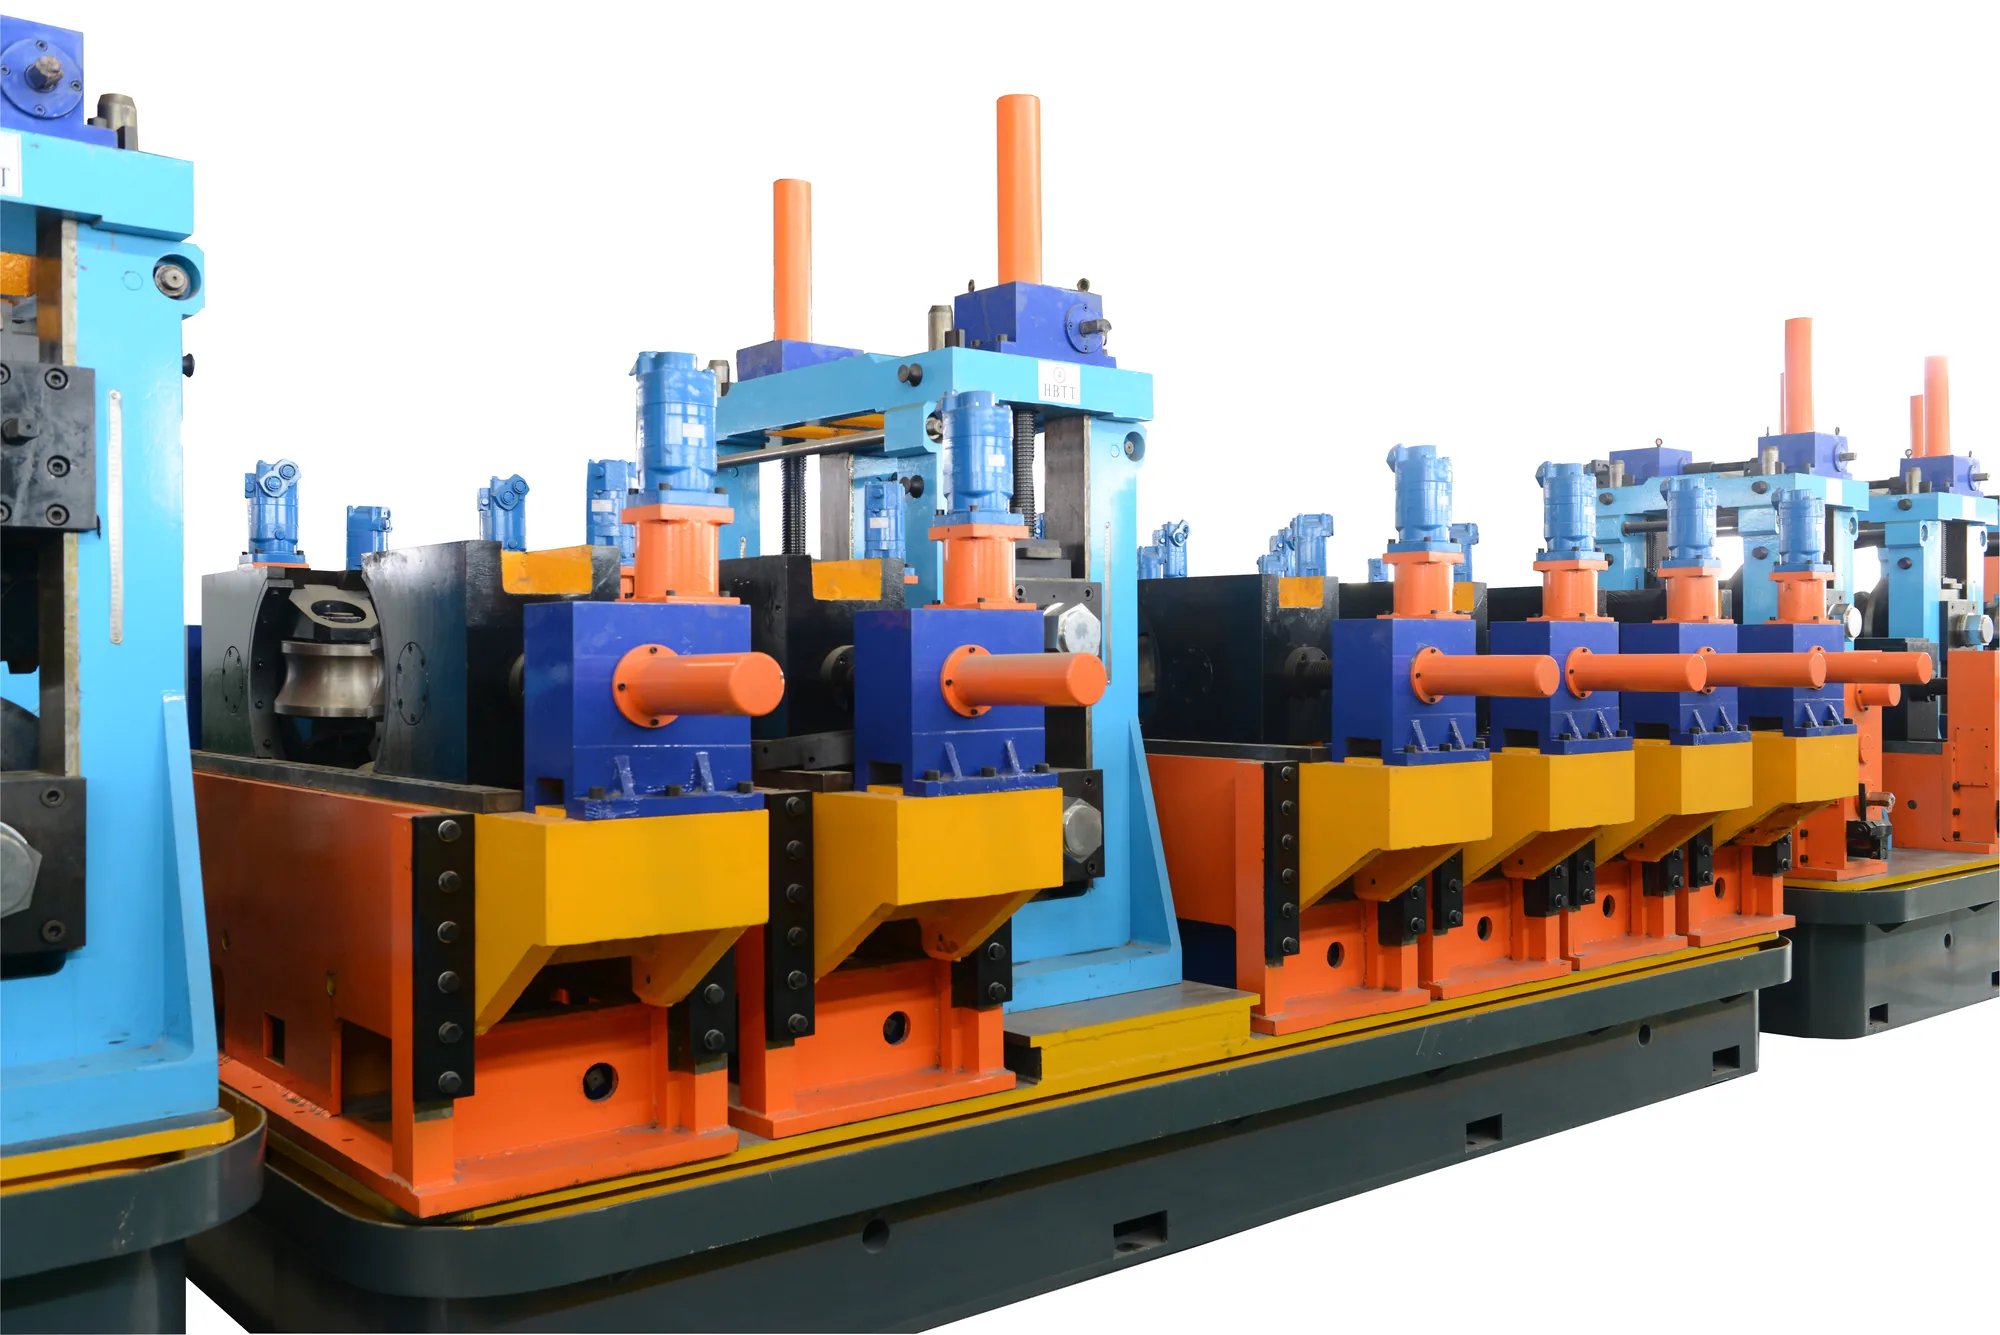
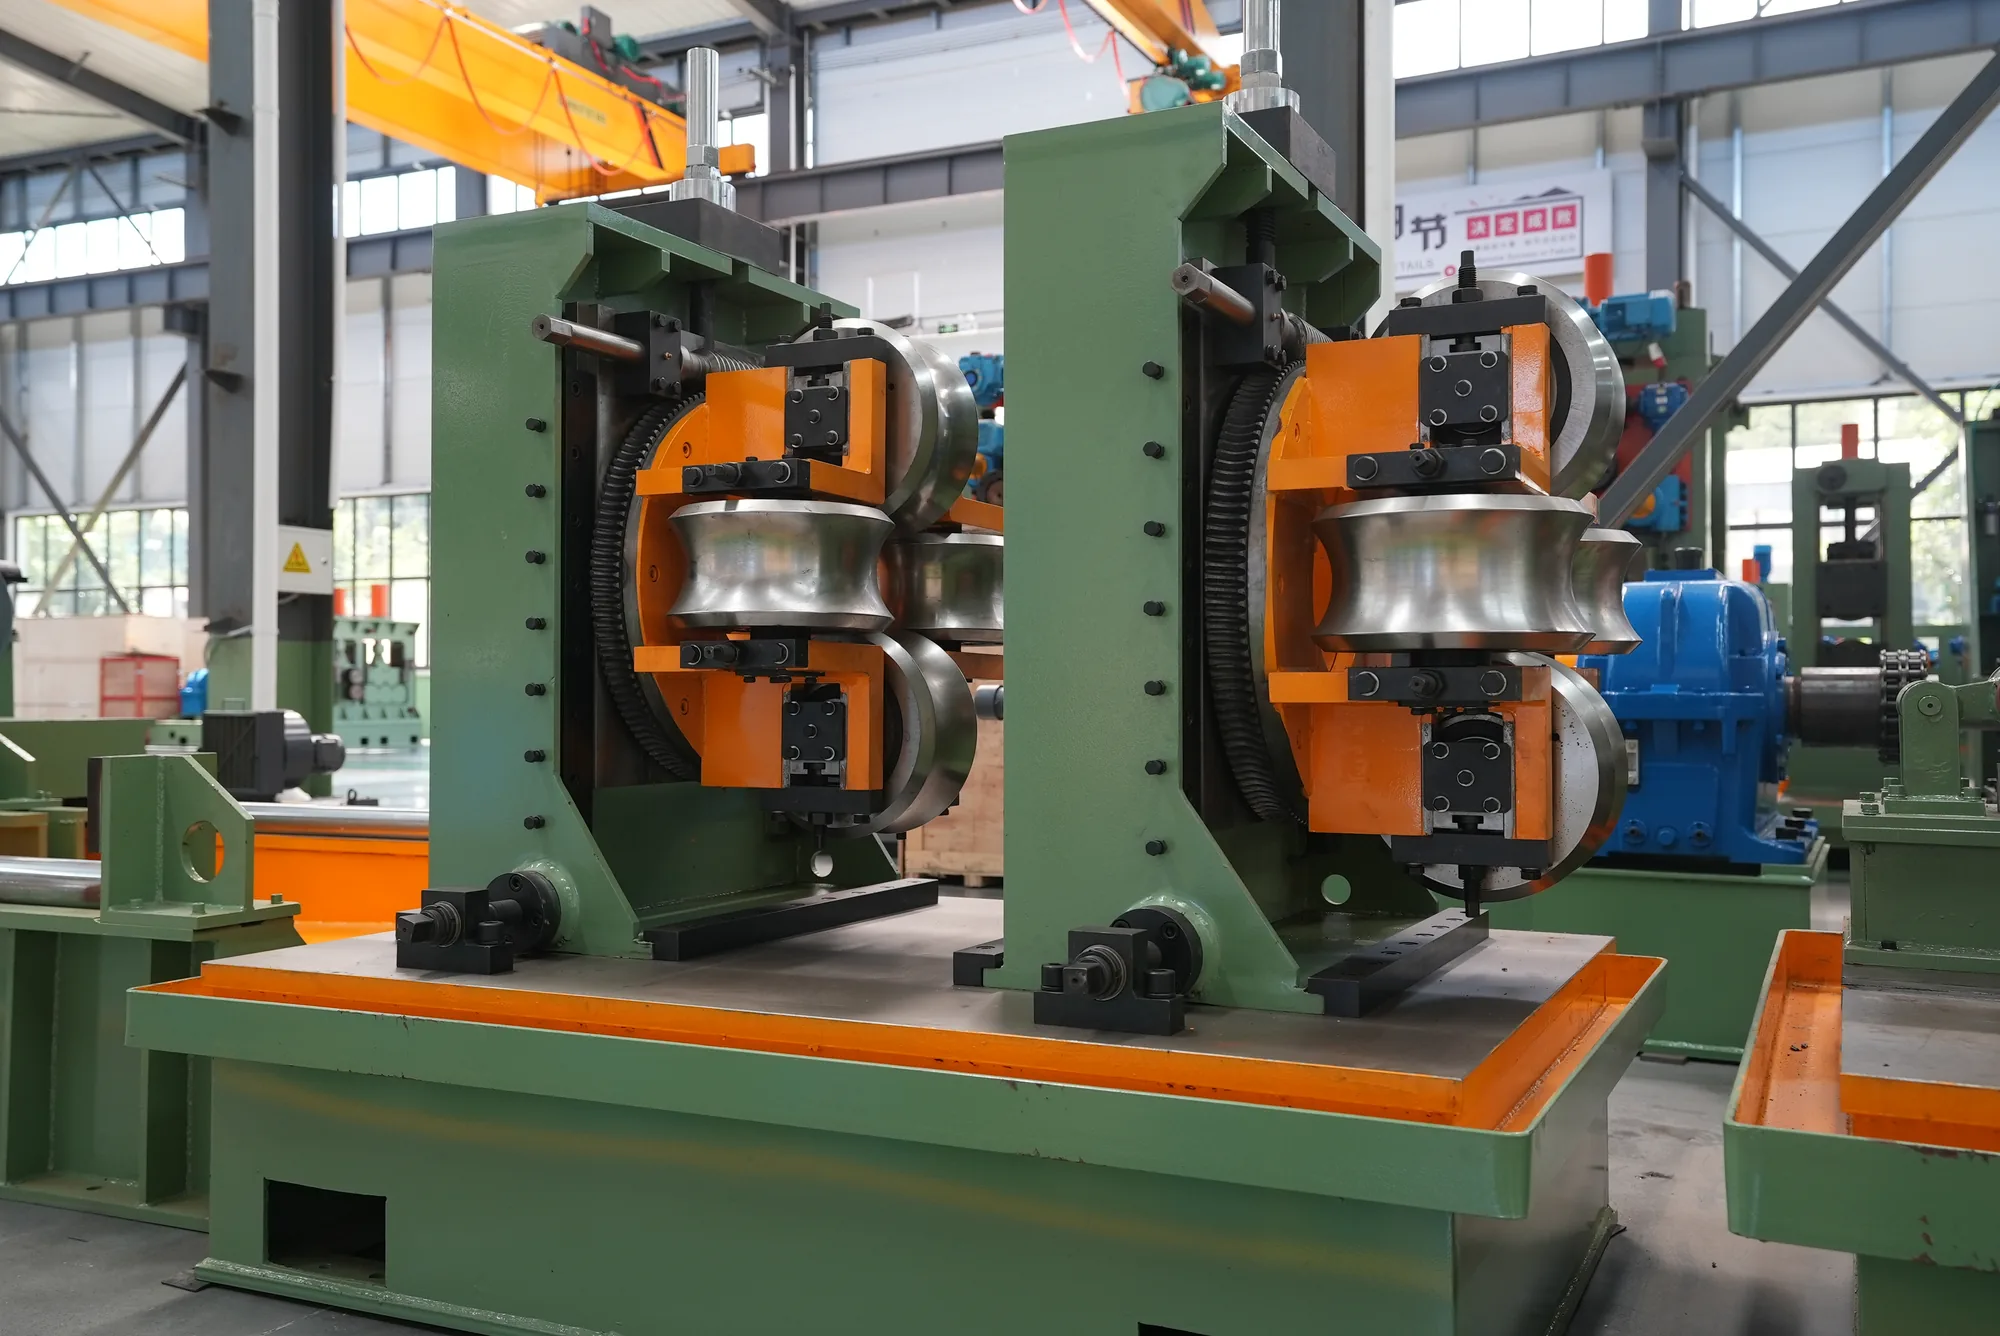
The process is the same one that runs the whole family: continuous uncoiling, roll forming, high-frequency induction welding, sizing and cutting, producing straight-seam welded pipe from coil. From HG219 up, the lines use FFX forming, a variant of W forming: the rolls of the open forming section are shared across sizes instead of being changed, which keeps roll cost down on mills where every roll is heavy and expensive.
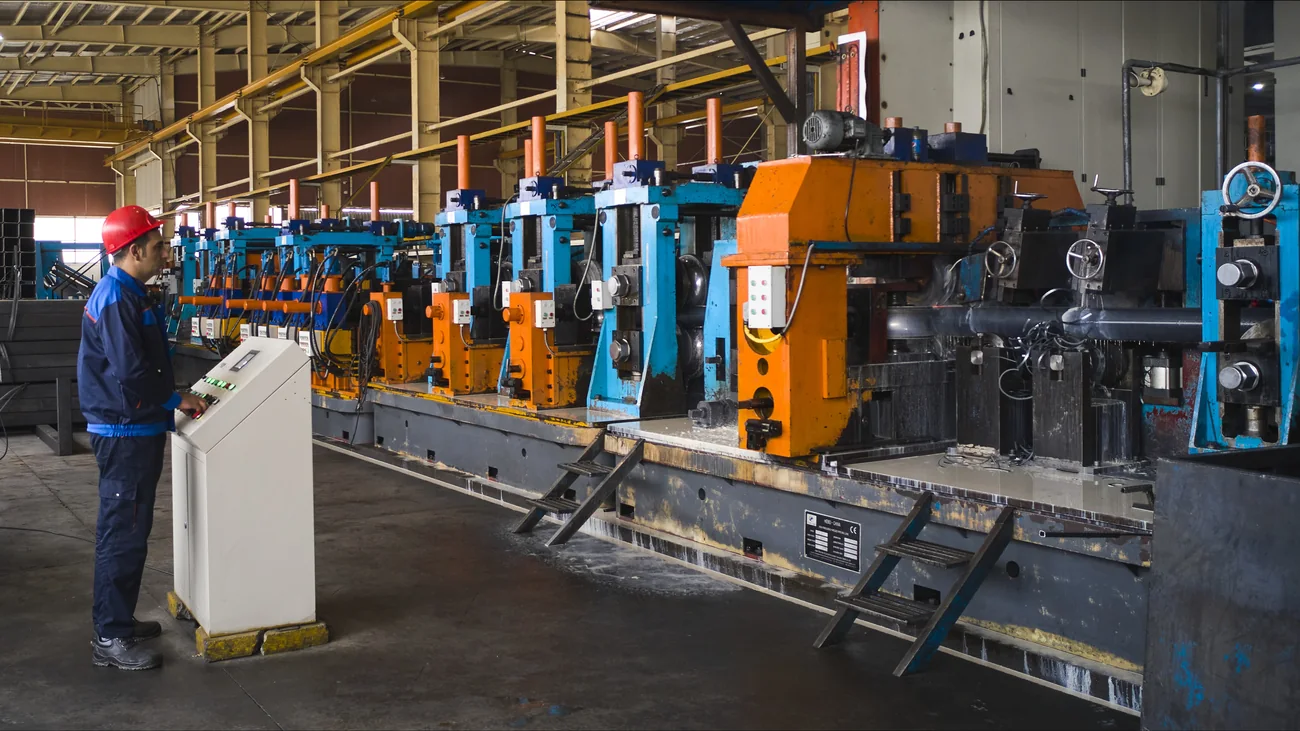
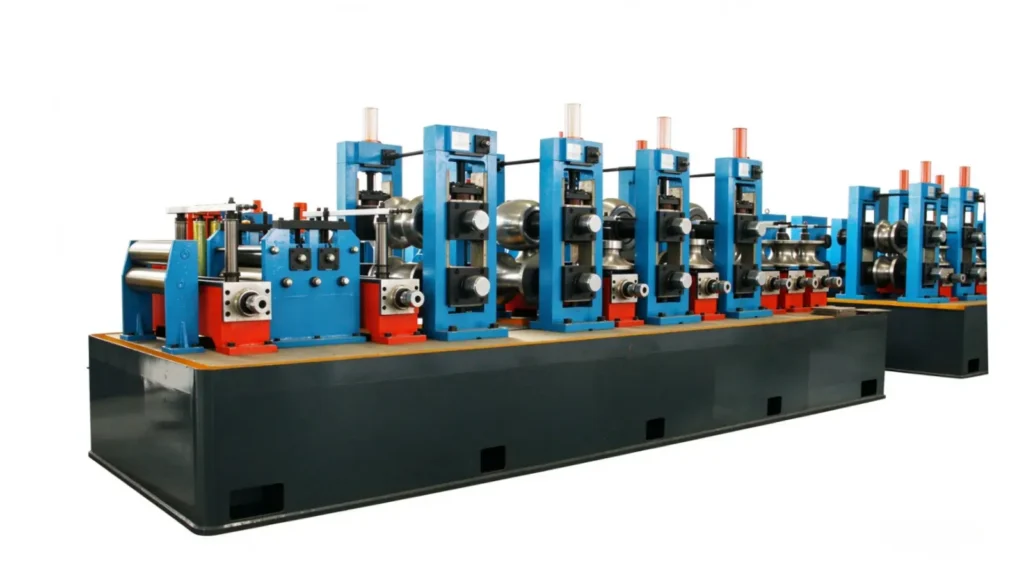 HG165 Tube Mill Line for Φ60–165 mm PipeThe sixth of the twelve model steps — Φ60 – Φ165 mm round pipe and 50×50 – 130×130 mm square section, on a 400 kW high-frequency welder.See the line →
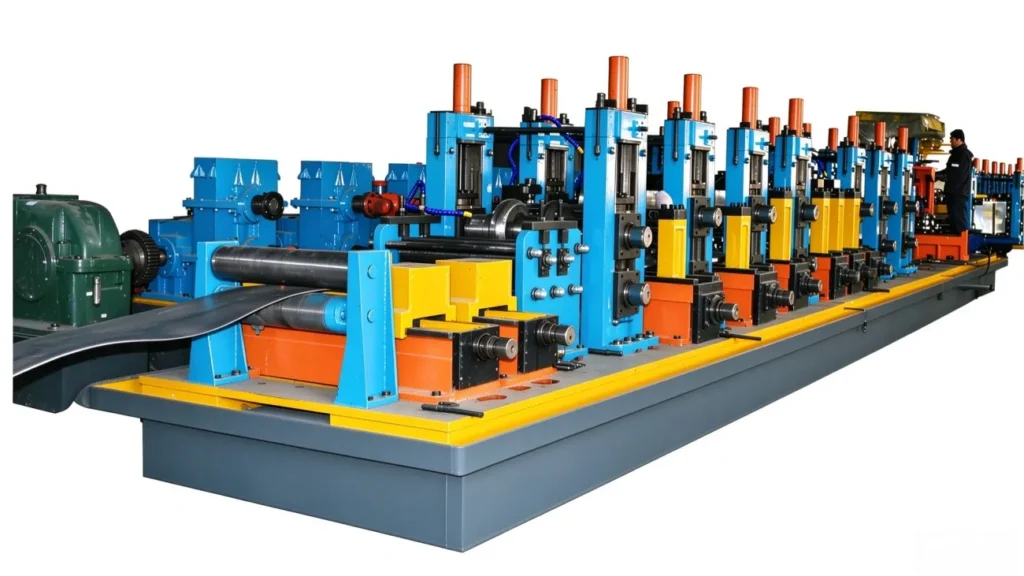 HG219 Tube Mill Line for Φ114–219 mm PipeThe seventh of the twelve model steps — Φ114 – Φ219 mm round pipe and 90×90 – 170×170 mm square section, on a 500 kW high-frequency welder.See the line →
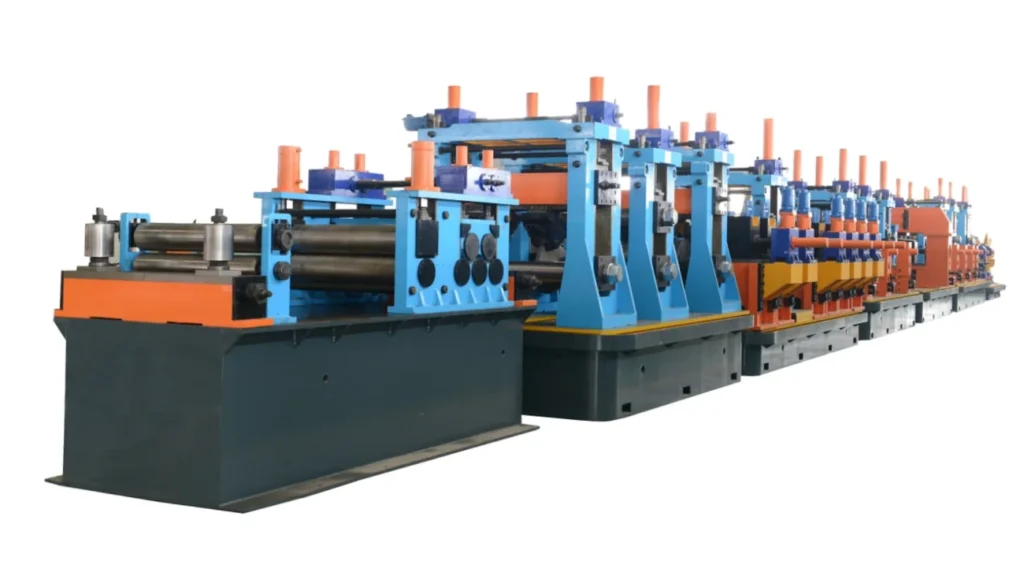 HG273 Tube Mill Line for Φ114–273 mm PipeThe eighth of the twelve model steps — Φ114 – Φ273 mm round pipe and 90×90 – 215×215 mm square section, on a 600 kW high-frequency welder.See the line →
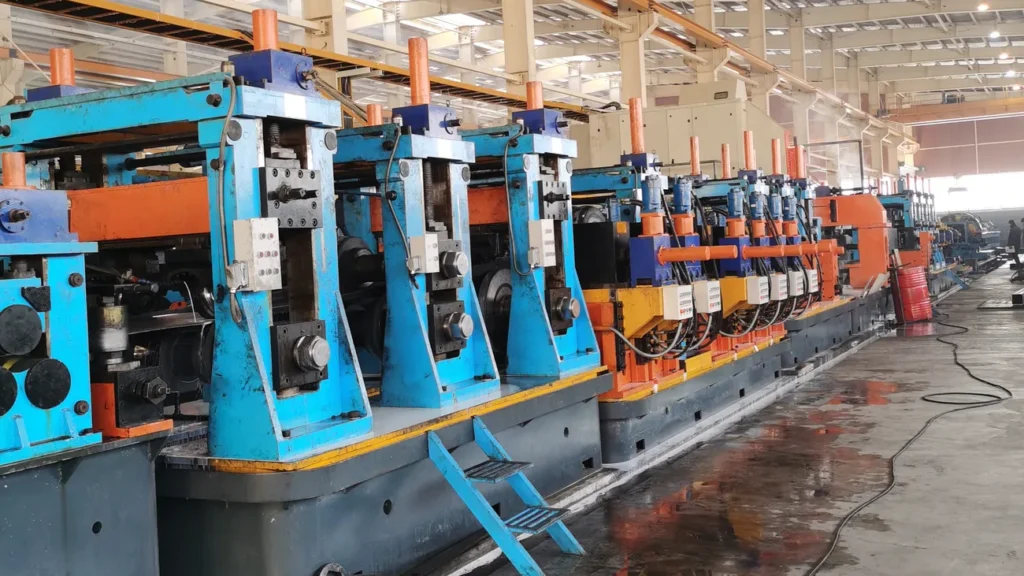 HG325 Tube Mill Line for Φ165–325 mm PipeThe ninth of the twelve model steps — Φ165 – Φ325 mm round pipe and 130×130 – 255×255 mm square section, on a 600 kW high-frequency welder.See the line →
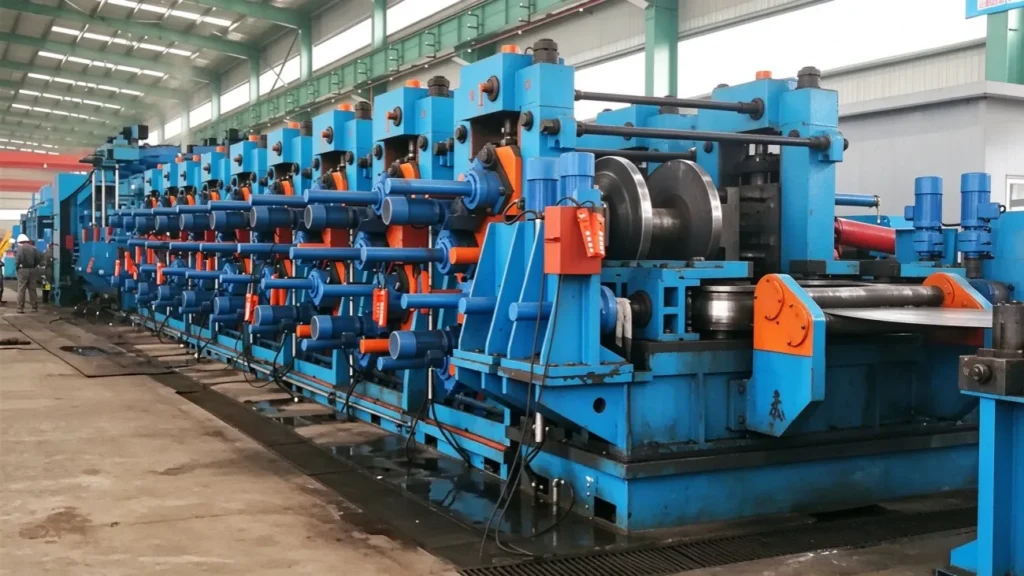 HG426 Tube Mill Line for Φ165–426 mm PipeThe tenth of the twelve model steps — Φ165 – Φ426 mm round pipe and 130×130 – 330×330 mm square section, on a 800 kW high-frequency welder.See the line →
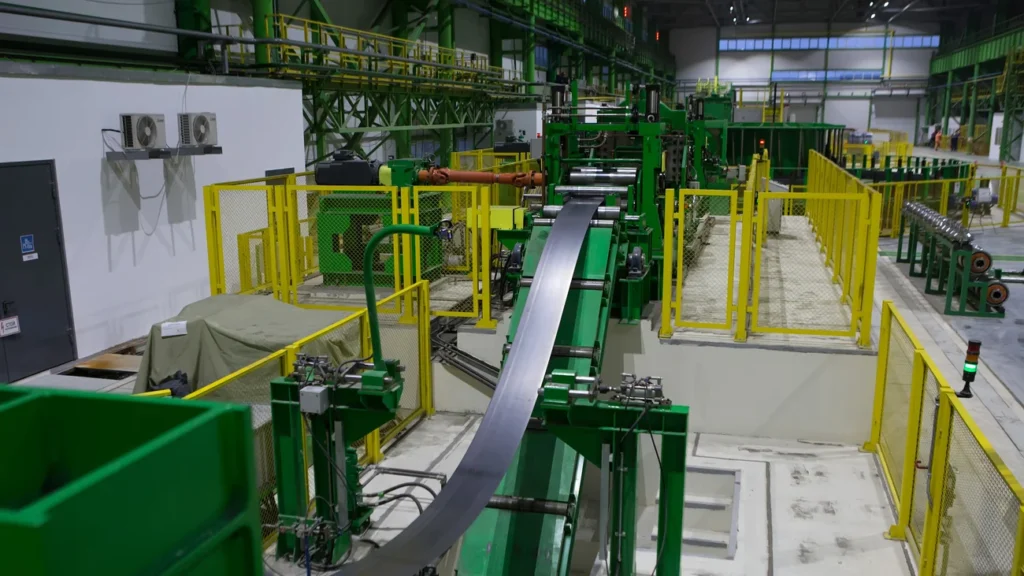 HG508 Tube Mill Line for Φ219–508 mm PipeThe eleventh of the twelve model steps — Φ219 – Φ508 mm round pipe and 170×170 – 400×400 mm square section, on a 1000 kW high-frequency welder.See the line →
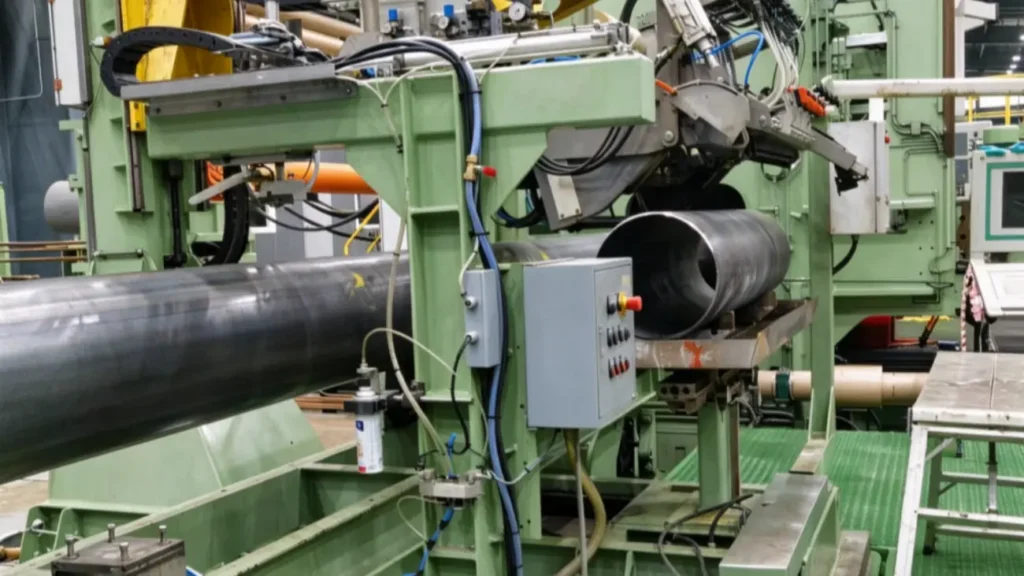 HG630 Tube Mill Line for Φ325–630 mm PipeThe twelfth of the twelve model steps — Φ325 – Φ630 mm round pipe and 250×250 – 500×500 mm square section, on a 1500 kW high-frequency welder.See the line →
Those windows overlap heavily at the lower end — HG219 and HG273 share the same Φ114 start, HG325 and HG426 share Φ165 — so the differentiating figure between adjacent steps is the top of the window, not the bottom.
Large-Diameter HFW Tube Mill — Units and Configuration
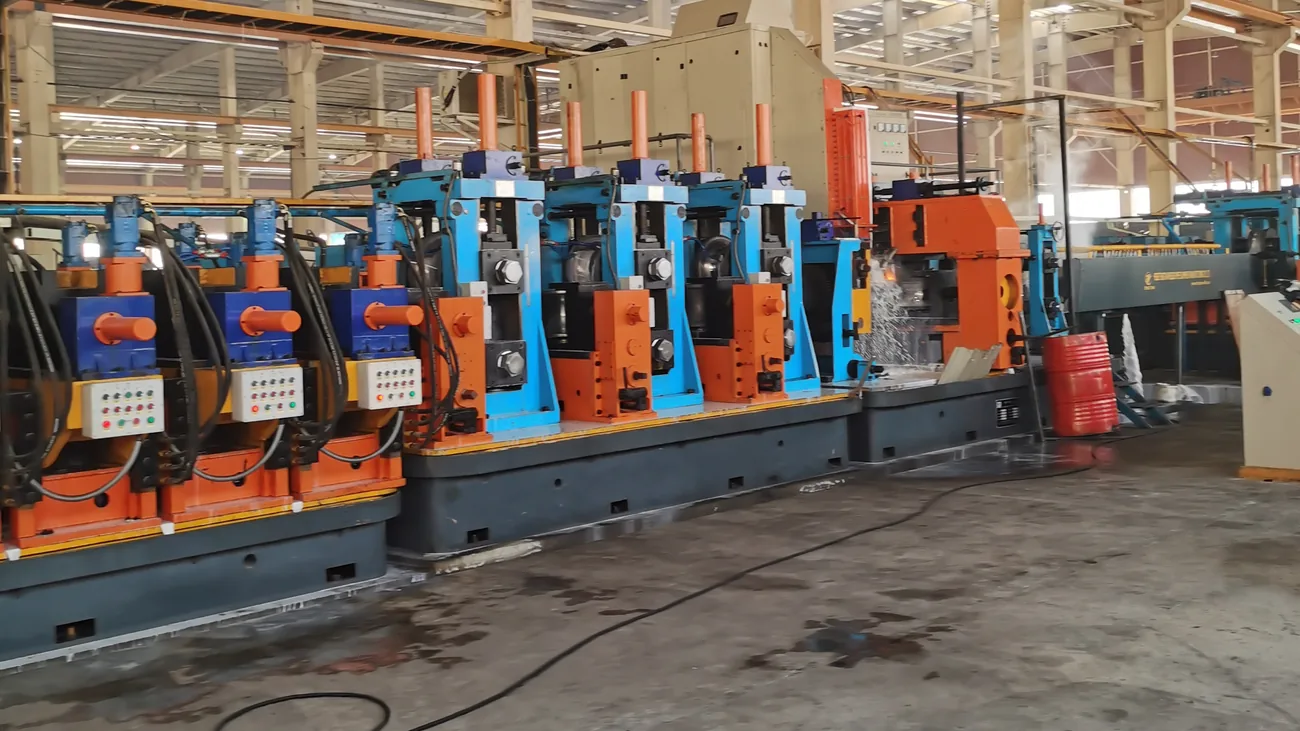
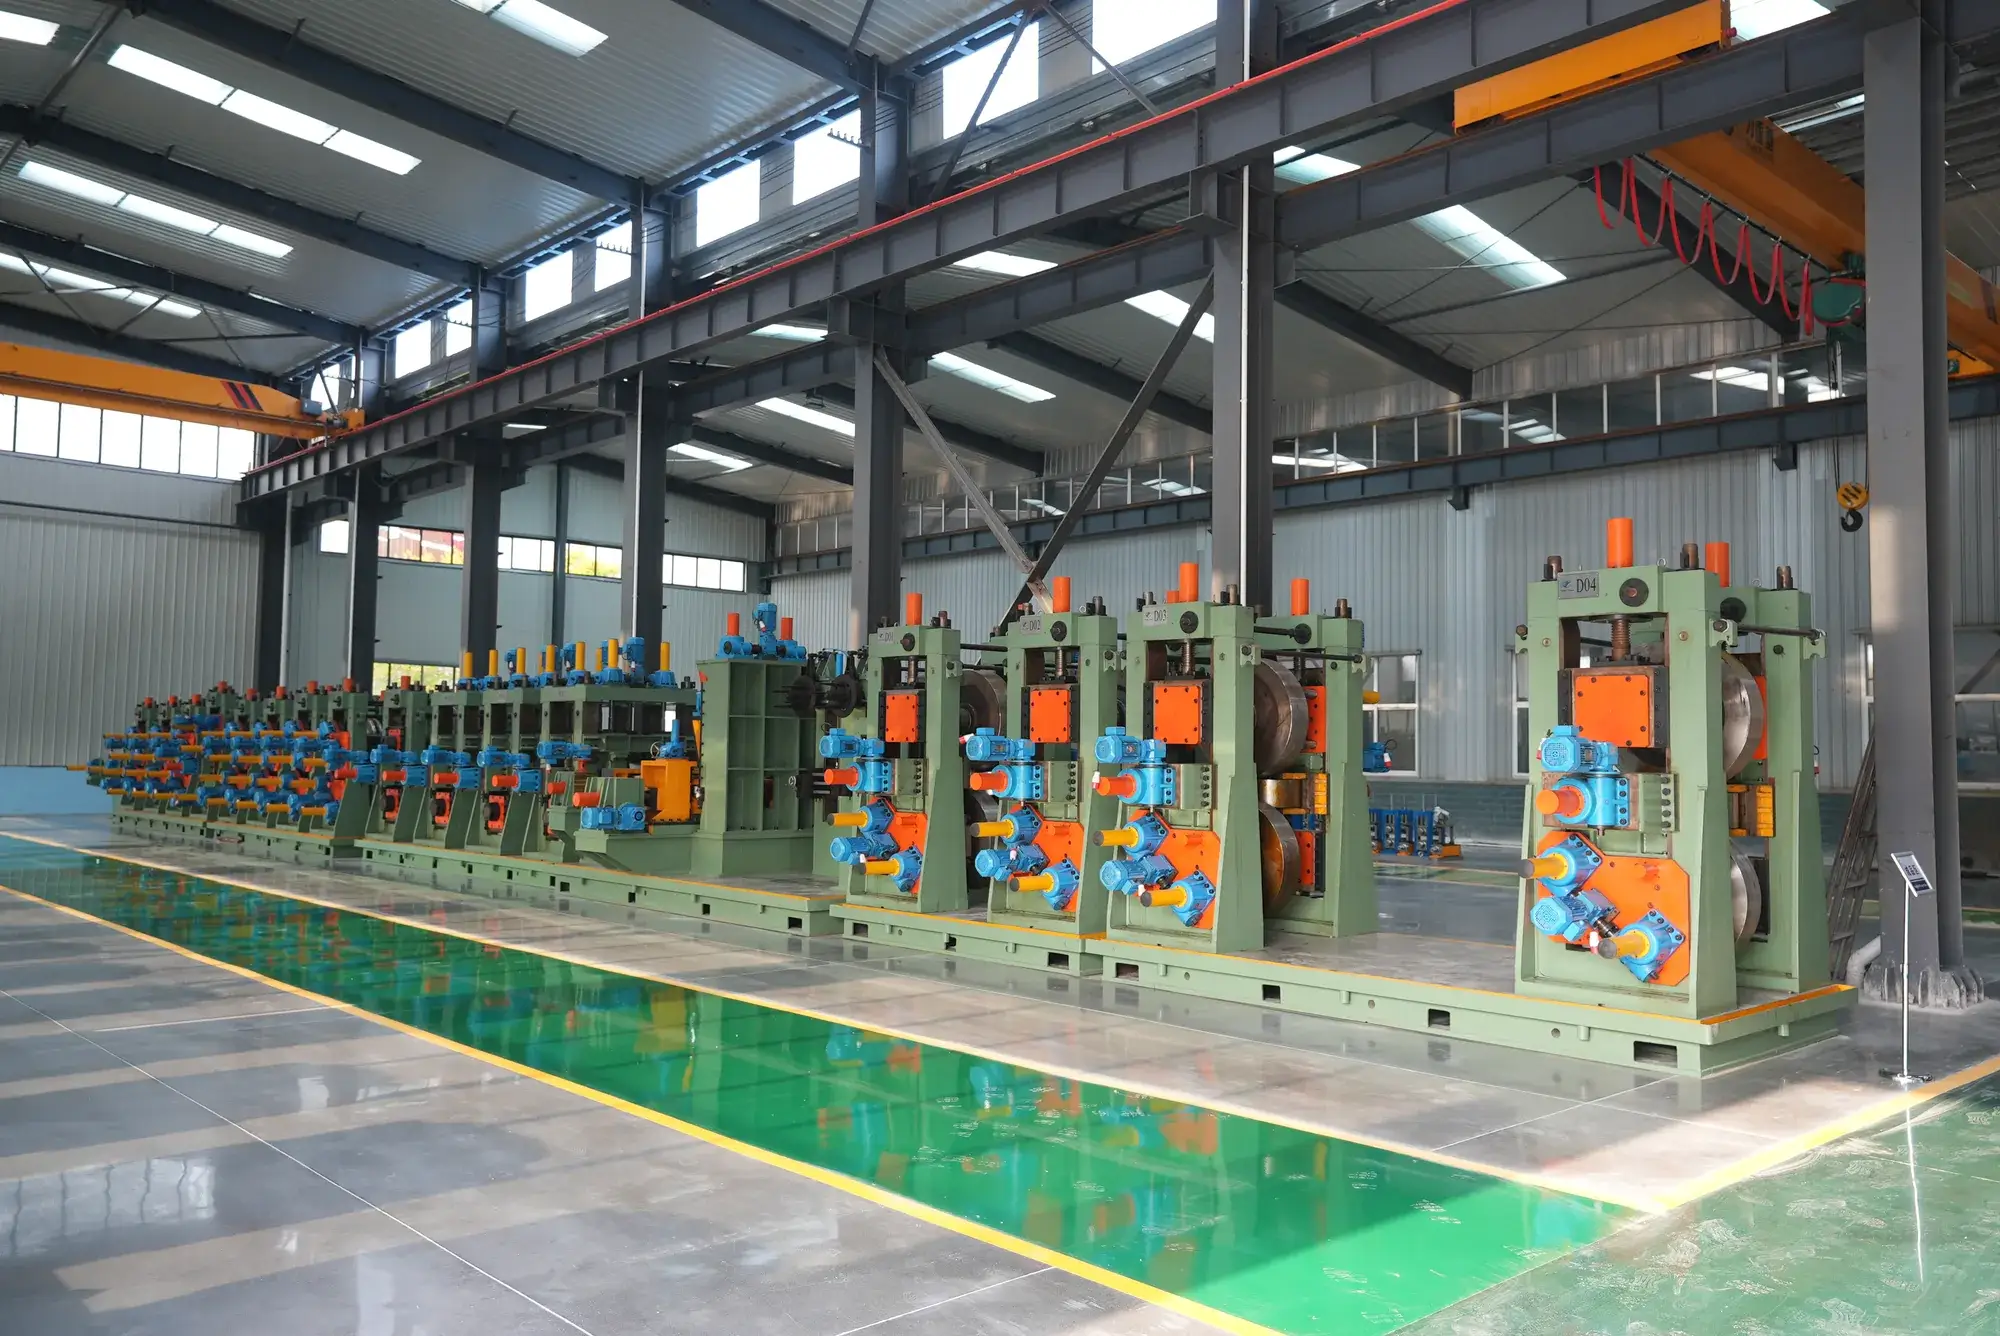
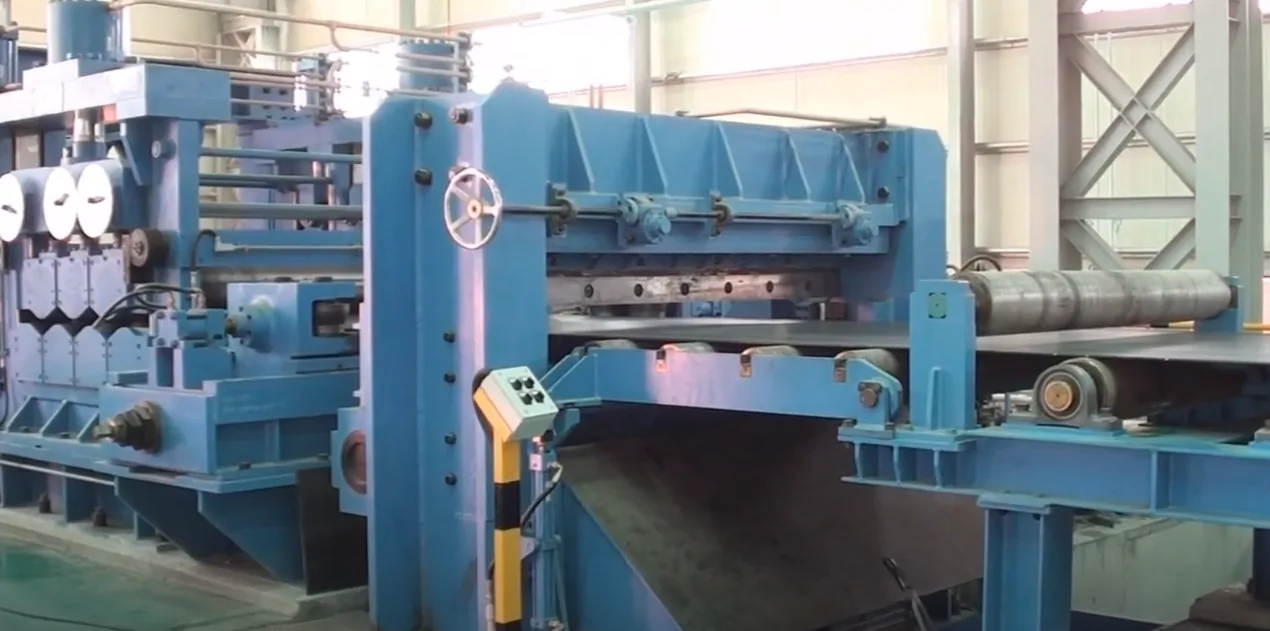
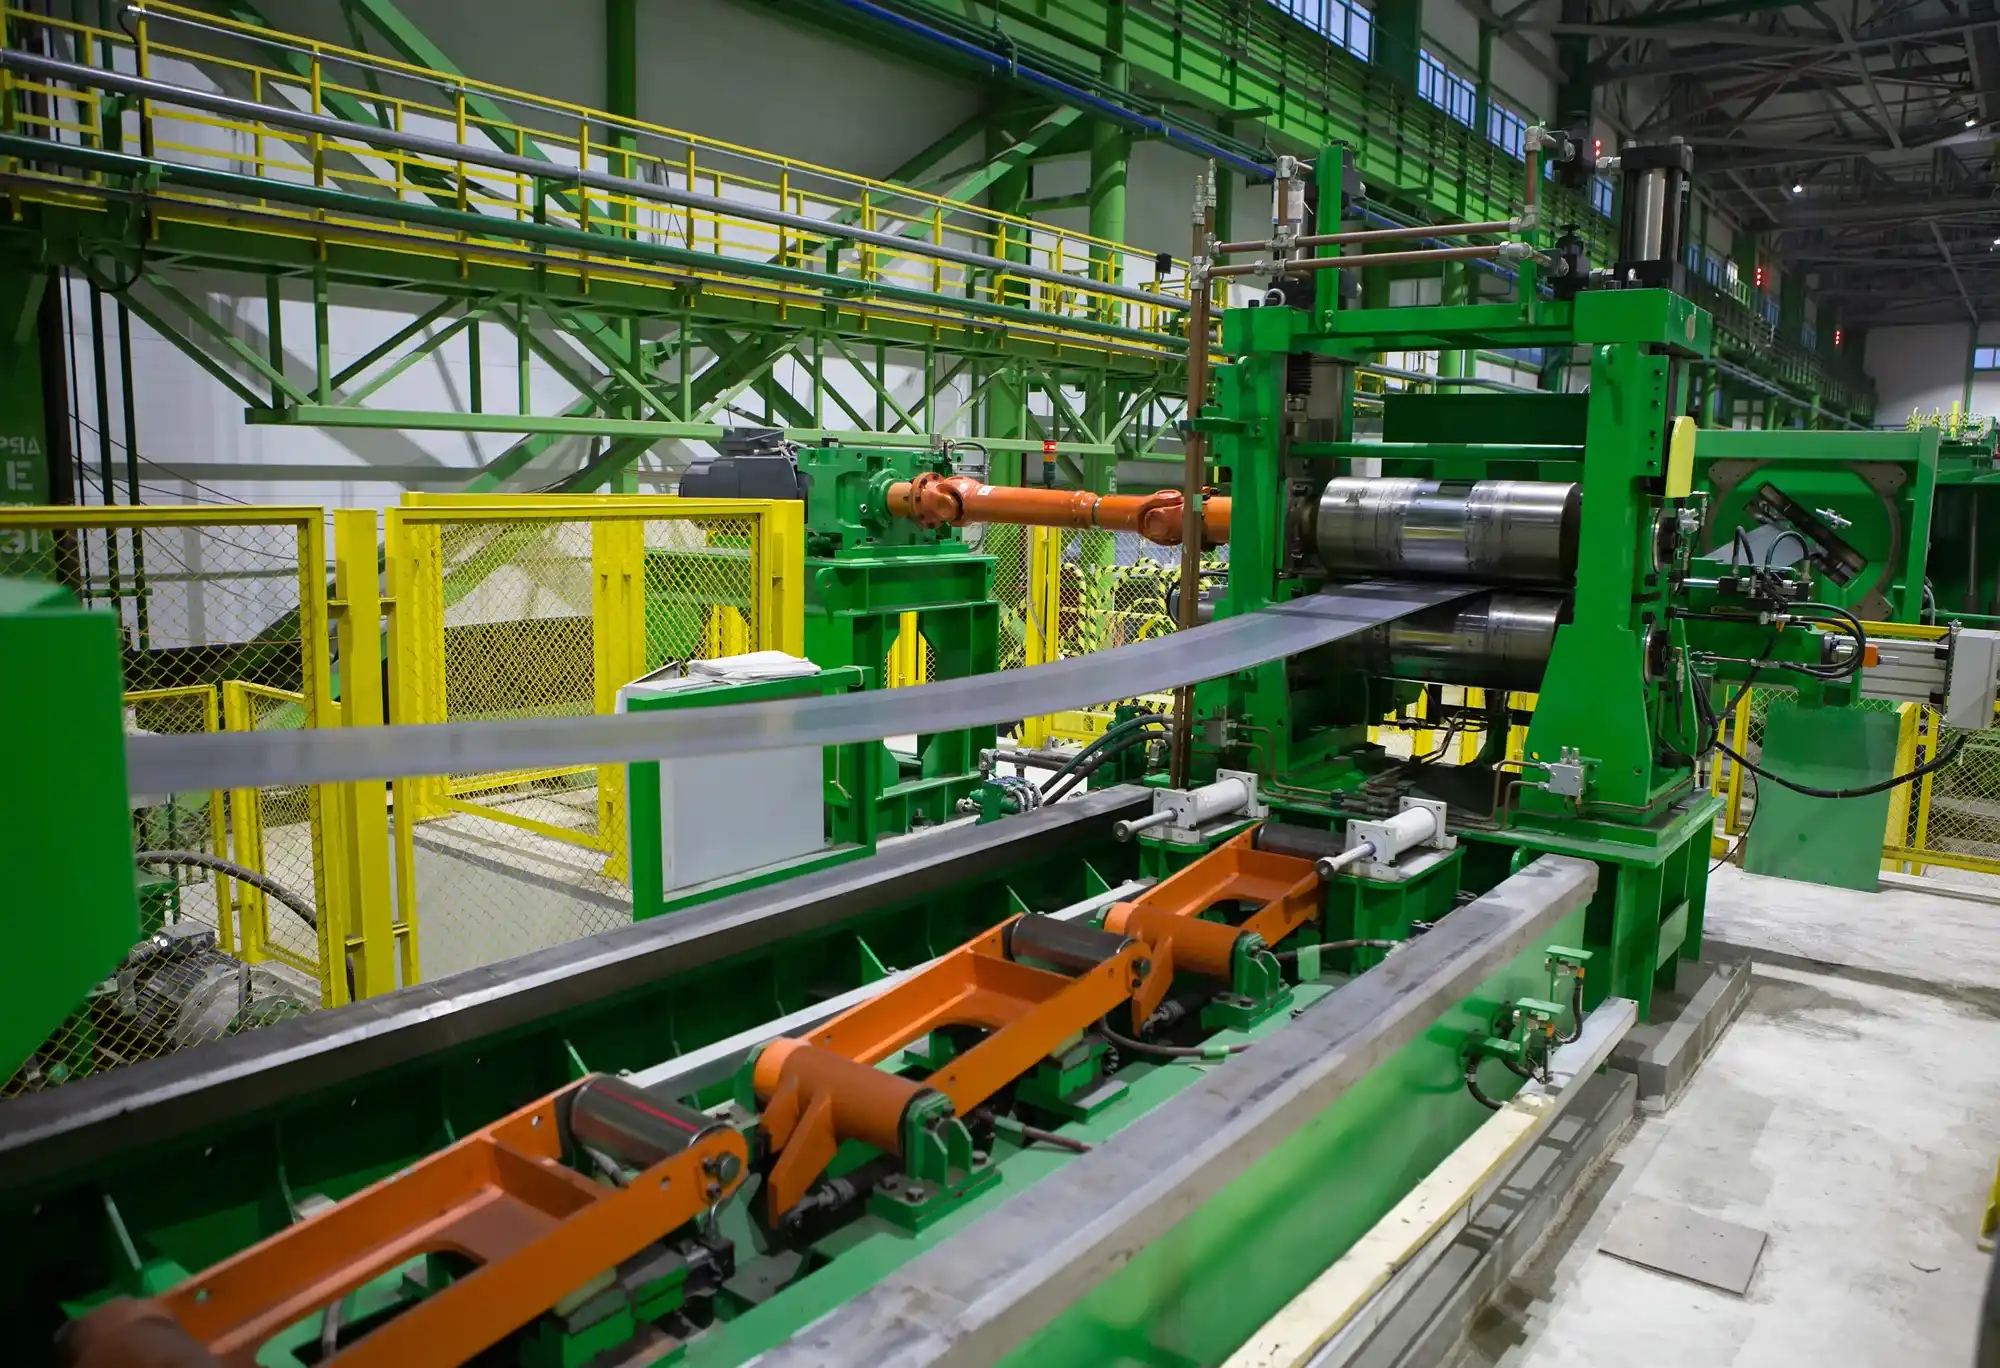
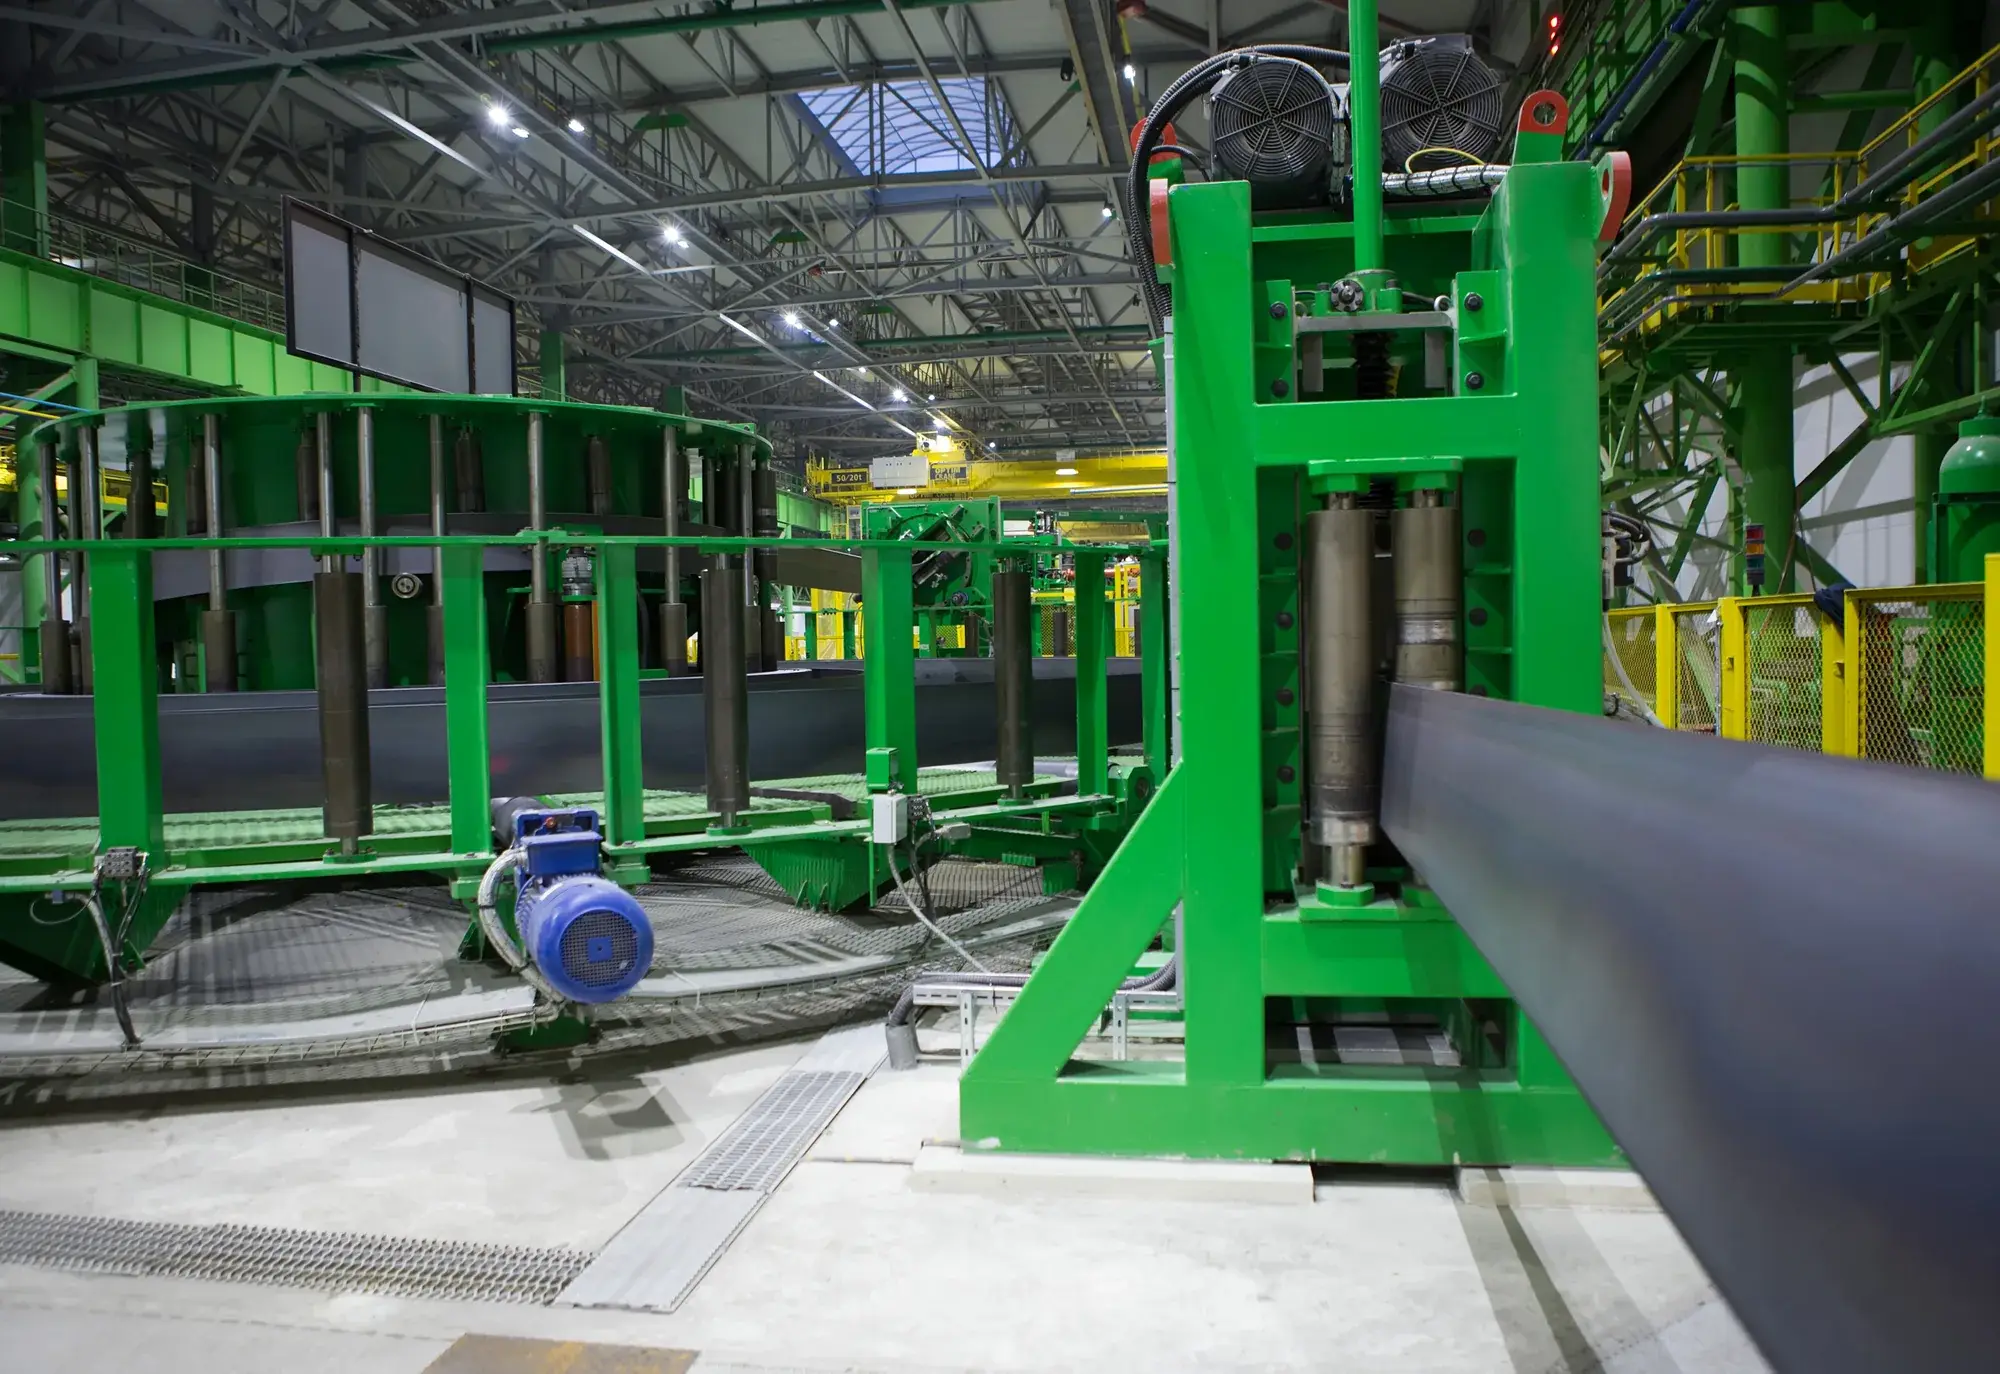
Unit train — the same on every step. Coil car, uncoiler with a pneumatic four-link expanding mandrel, strip-head opener, pinch leveller with five rollers, automatic shear-welder, spiral accumulator, forming and sizing mill, high-frequency welder, flying saw and run-out table, with PLC and variable-frequency control; each model page lists what every unit does.
Welding. High-frequency induction welding across the family.
Section shapes. Round, square and rectangular; most steps produce all three.
Key Parameters: Size Range, Wall Thickness and Welder Power by Model
| Model | Outside diameter | Wall thickness | Square section | HF welder |
|---|---|---|---|---|
| HG165 | Φ60 – 165 mm | 3.0 – 7.0 mm | 50×50 – 130×130 mm | 400 kW |
| HG219 | Φ114 – 219 mm | 4.0 – 8.0 mm | 90×90 – 170×170 mm | 500 kW |
| HG273 | Φ114 – 273 mm | 4.0 – 10.0 mm | 90×90 – 215×215 mm | 600 kW |
| HG325 | Φ165 – 325 mm | 4.0 – 10.0 mm | 130×130 – 255×255 mm | 600 kW |
| HG426 | Φ165 – 426 mm | 4.0 – 10.0 mm | 130×130 – 330×330 mm | 800 kW |
| HG508 | Φ219 – 508 mm | 4.0 – 16.0 mm | 170×170 – 400×400 mm | 1000 kW |
| HG630 | Φ325 – 630 mm | 4.0 – 16.0 mm | 250×250 – 500×500 mm | 1500 kW |
On a large diameter tube mill, line speed and shift output depend on pipe size, wall and material grade, and are stated with the quotation.
Where This Family Meets the Spiral Line
Above Φ630 mm, pipe is made on one of our spiral submerged-arc welded pipe mills, which run Φ219–820 mm and Φ219–1620 mm and so overlap this family from Φ219 mm up. A spiral mill changes diameter by changing the forming angle rather than the roll set, so one machine covers a wide band, but it welds at 0.5–3 m/min and runs discontinuously; a high-frequency line welds a straight seam continuously. SSAW or HFW: how to choose sets out the full comparison, and the HG508 page covers the band where the two overlap most.
Lines Delivered in This Diameter Band
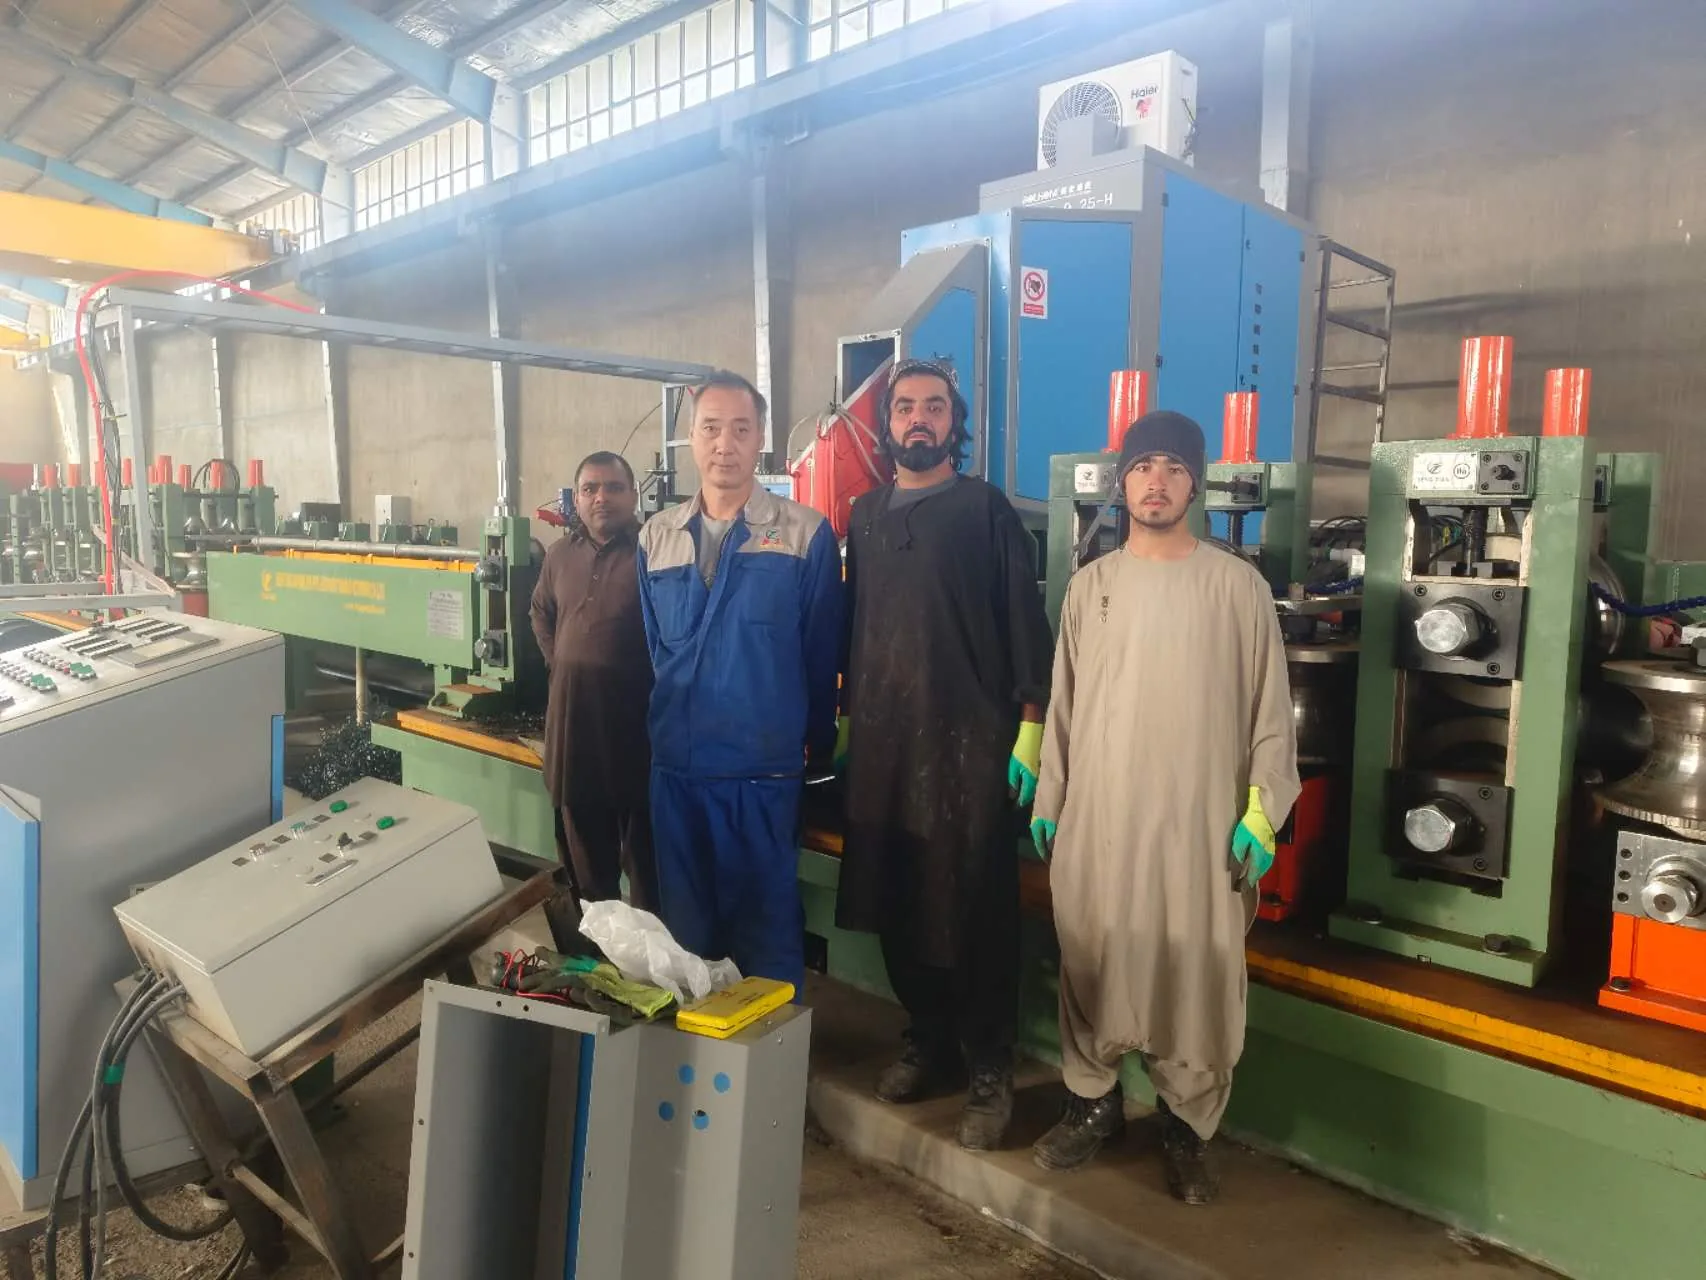
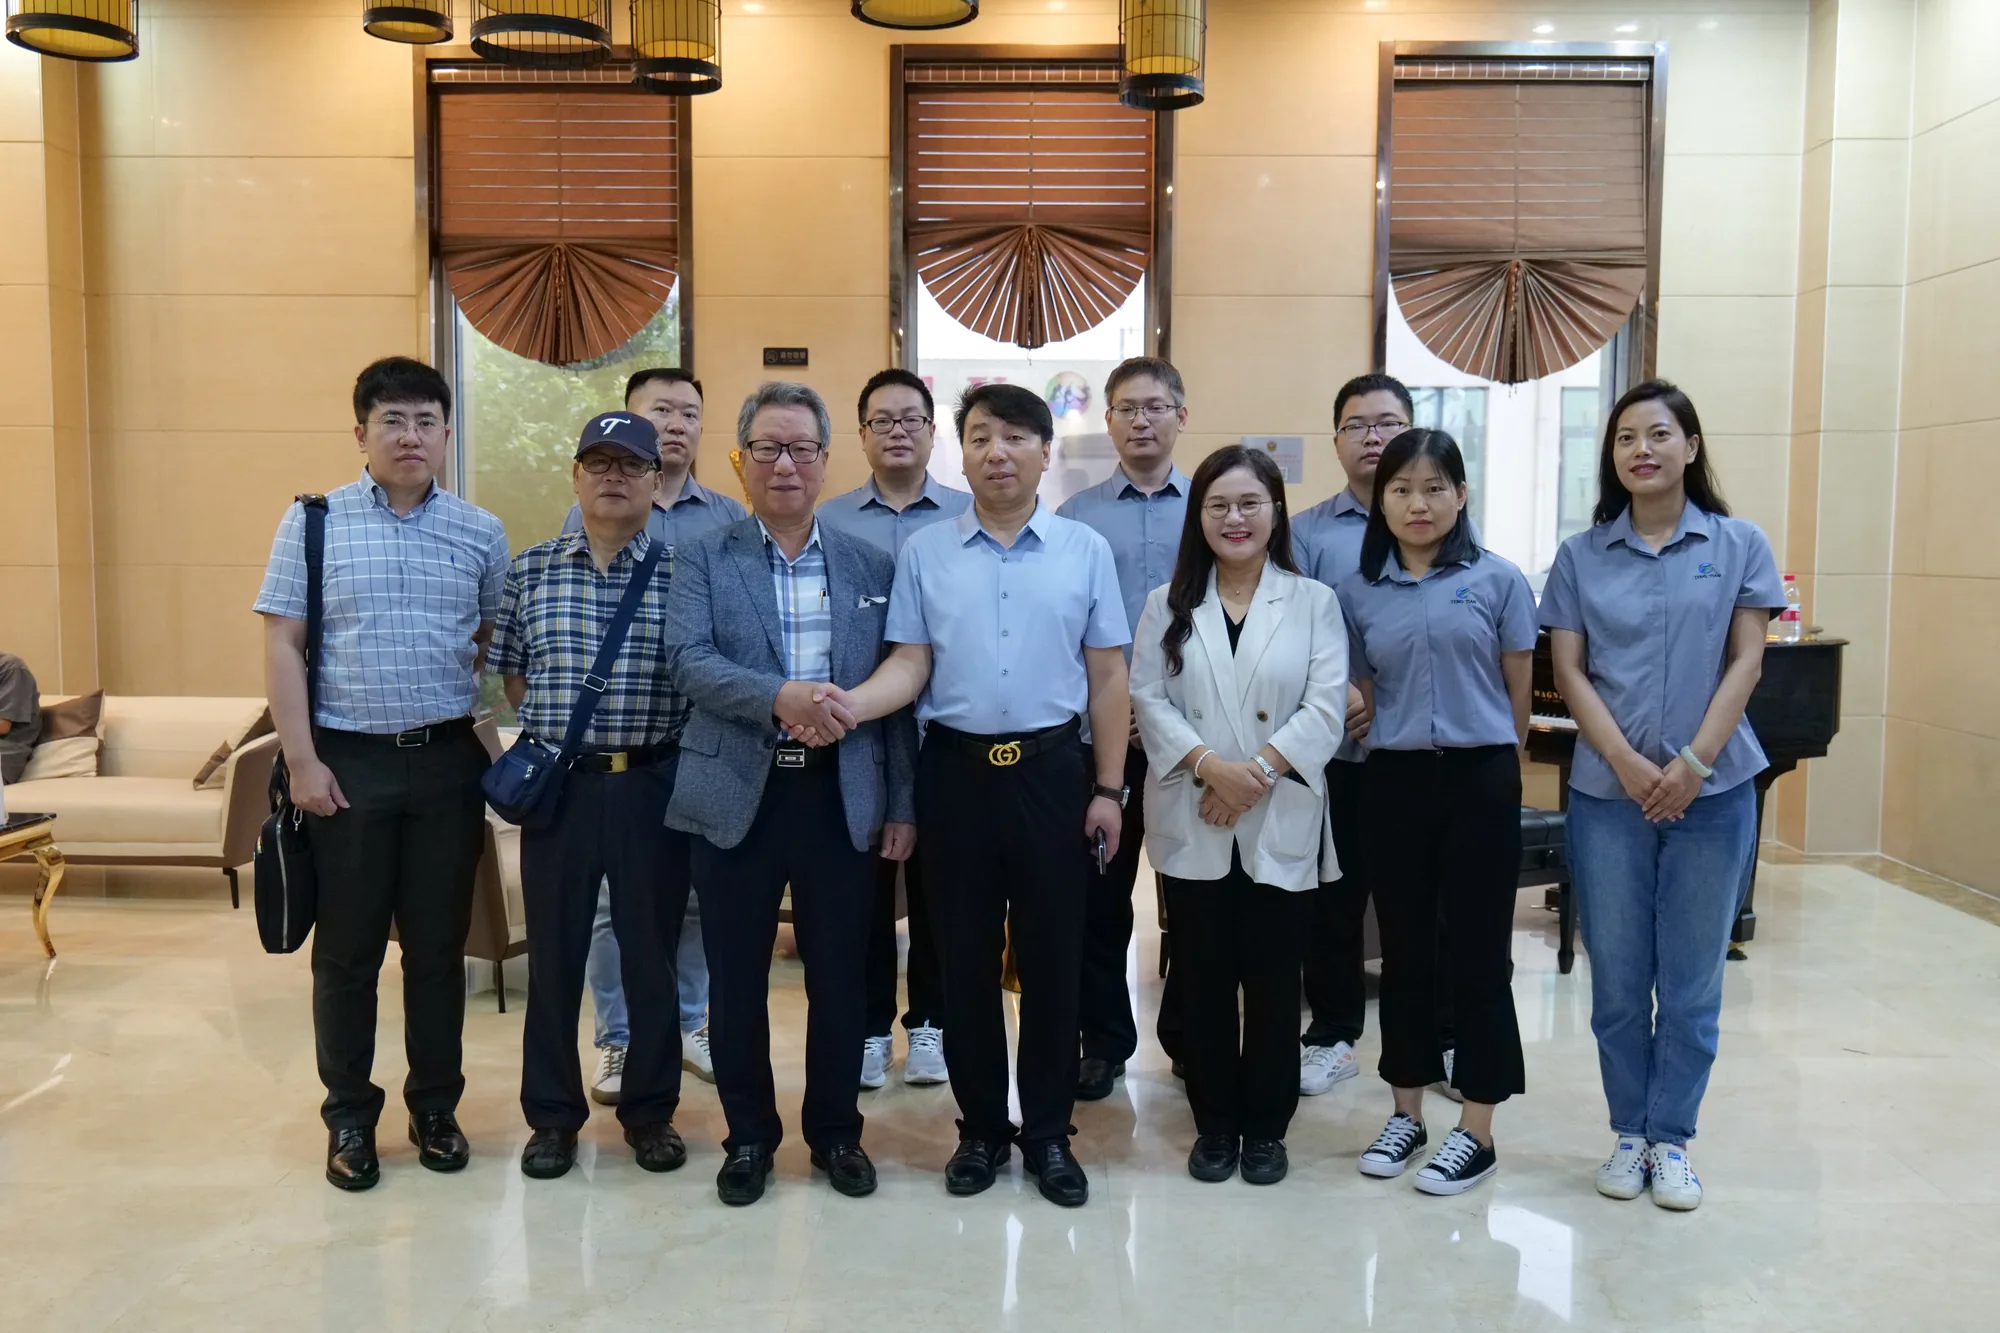
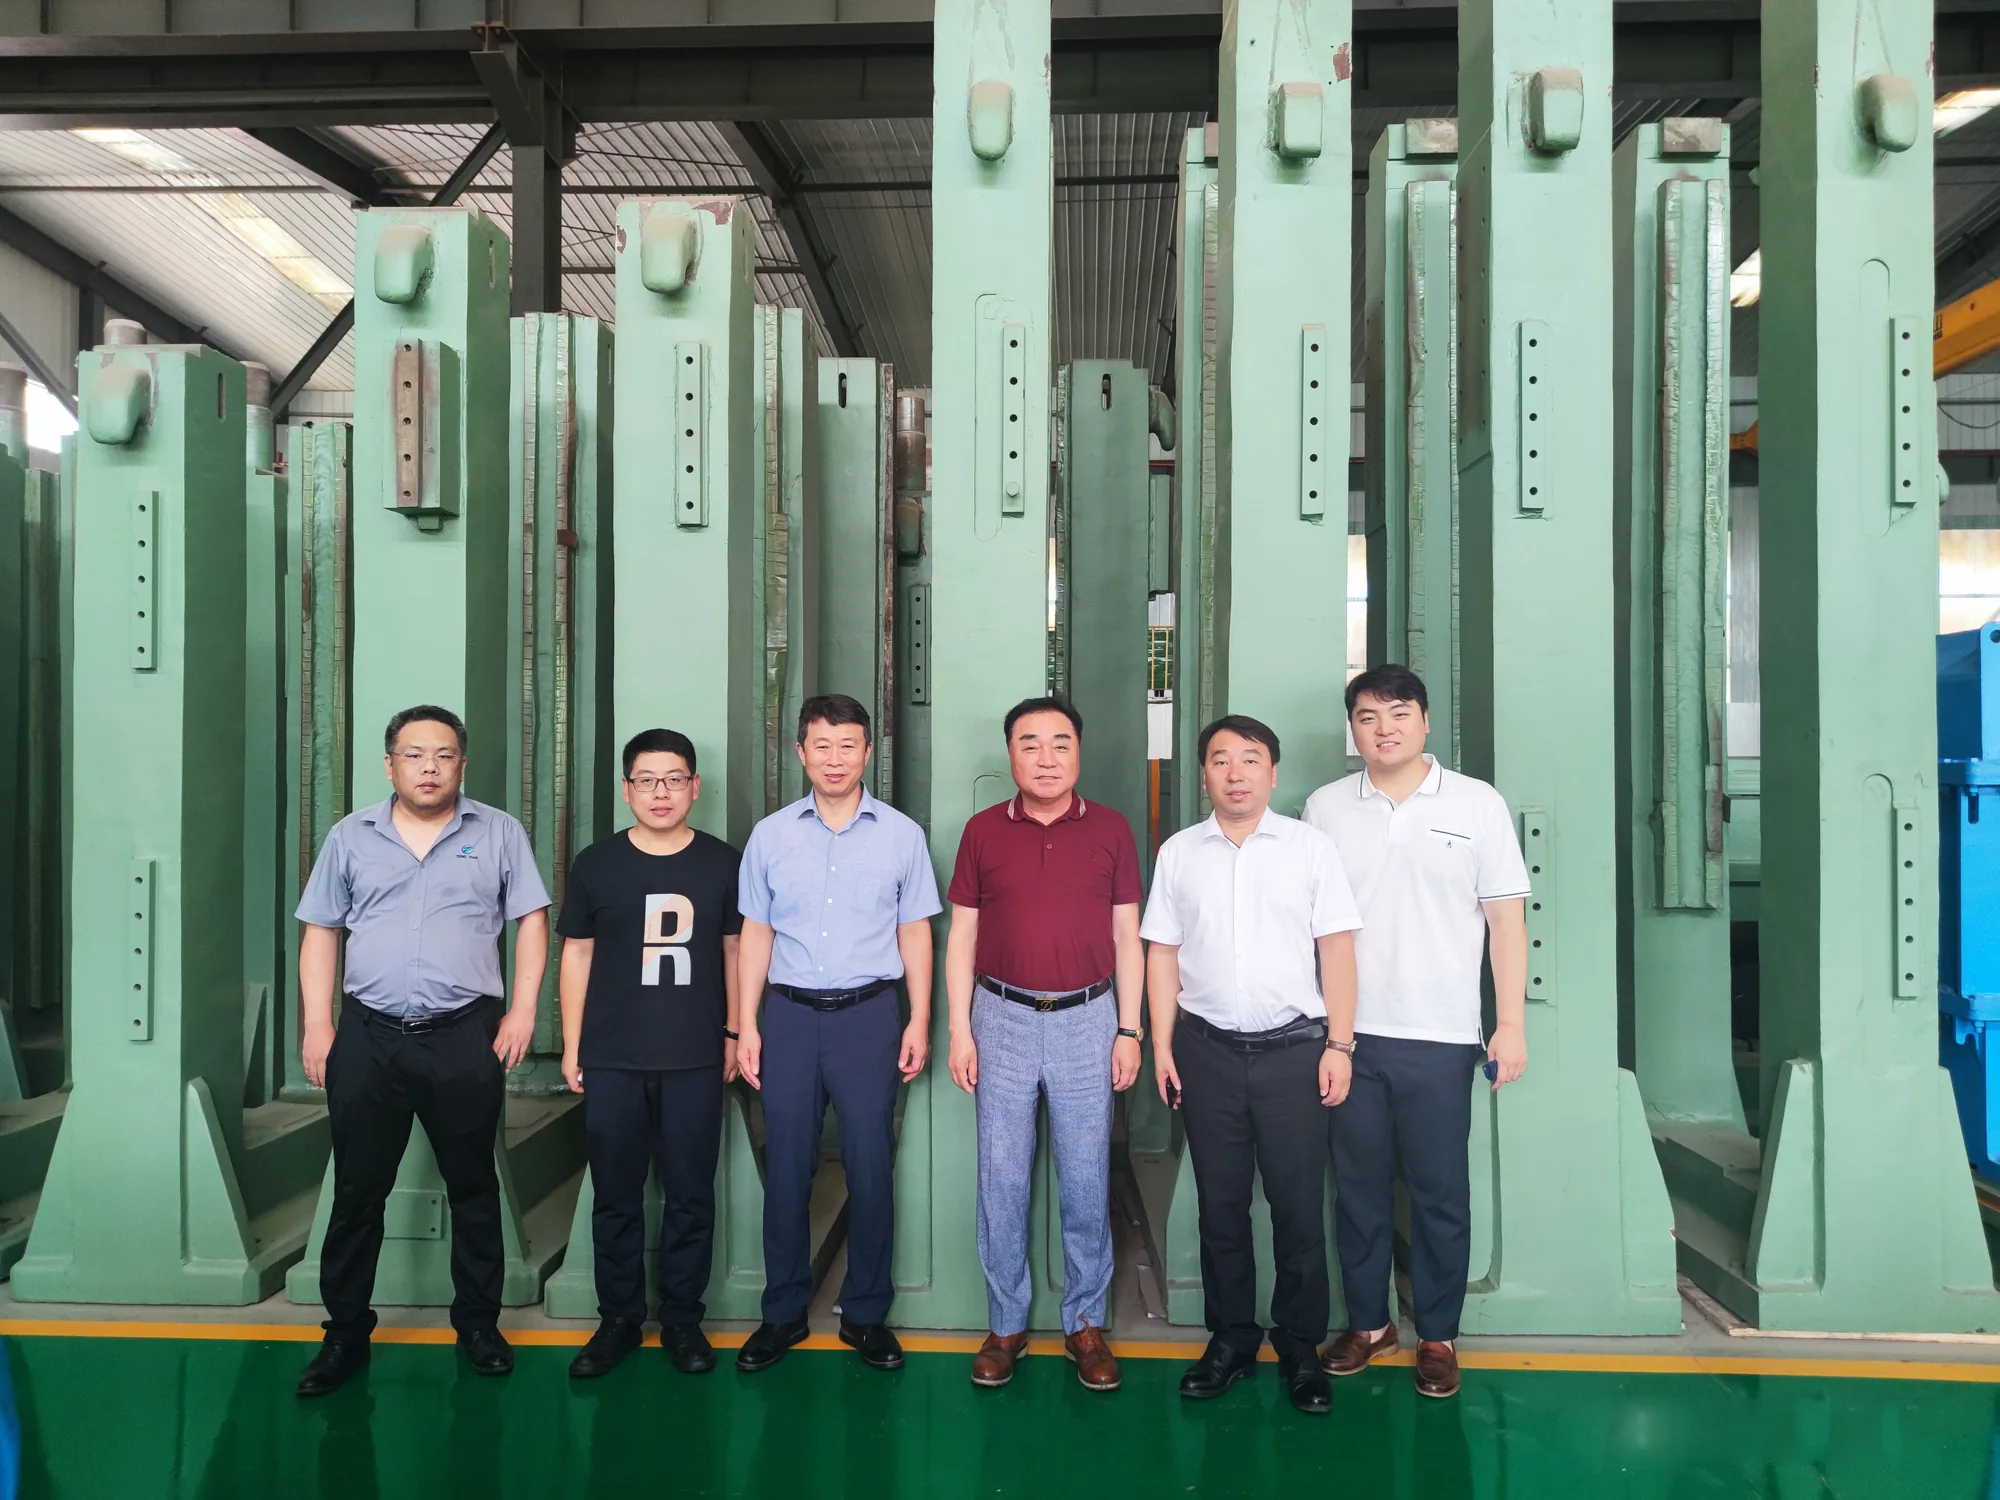
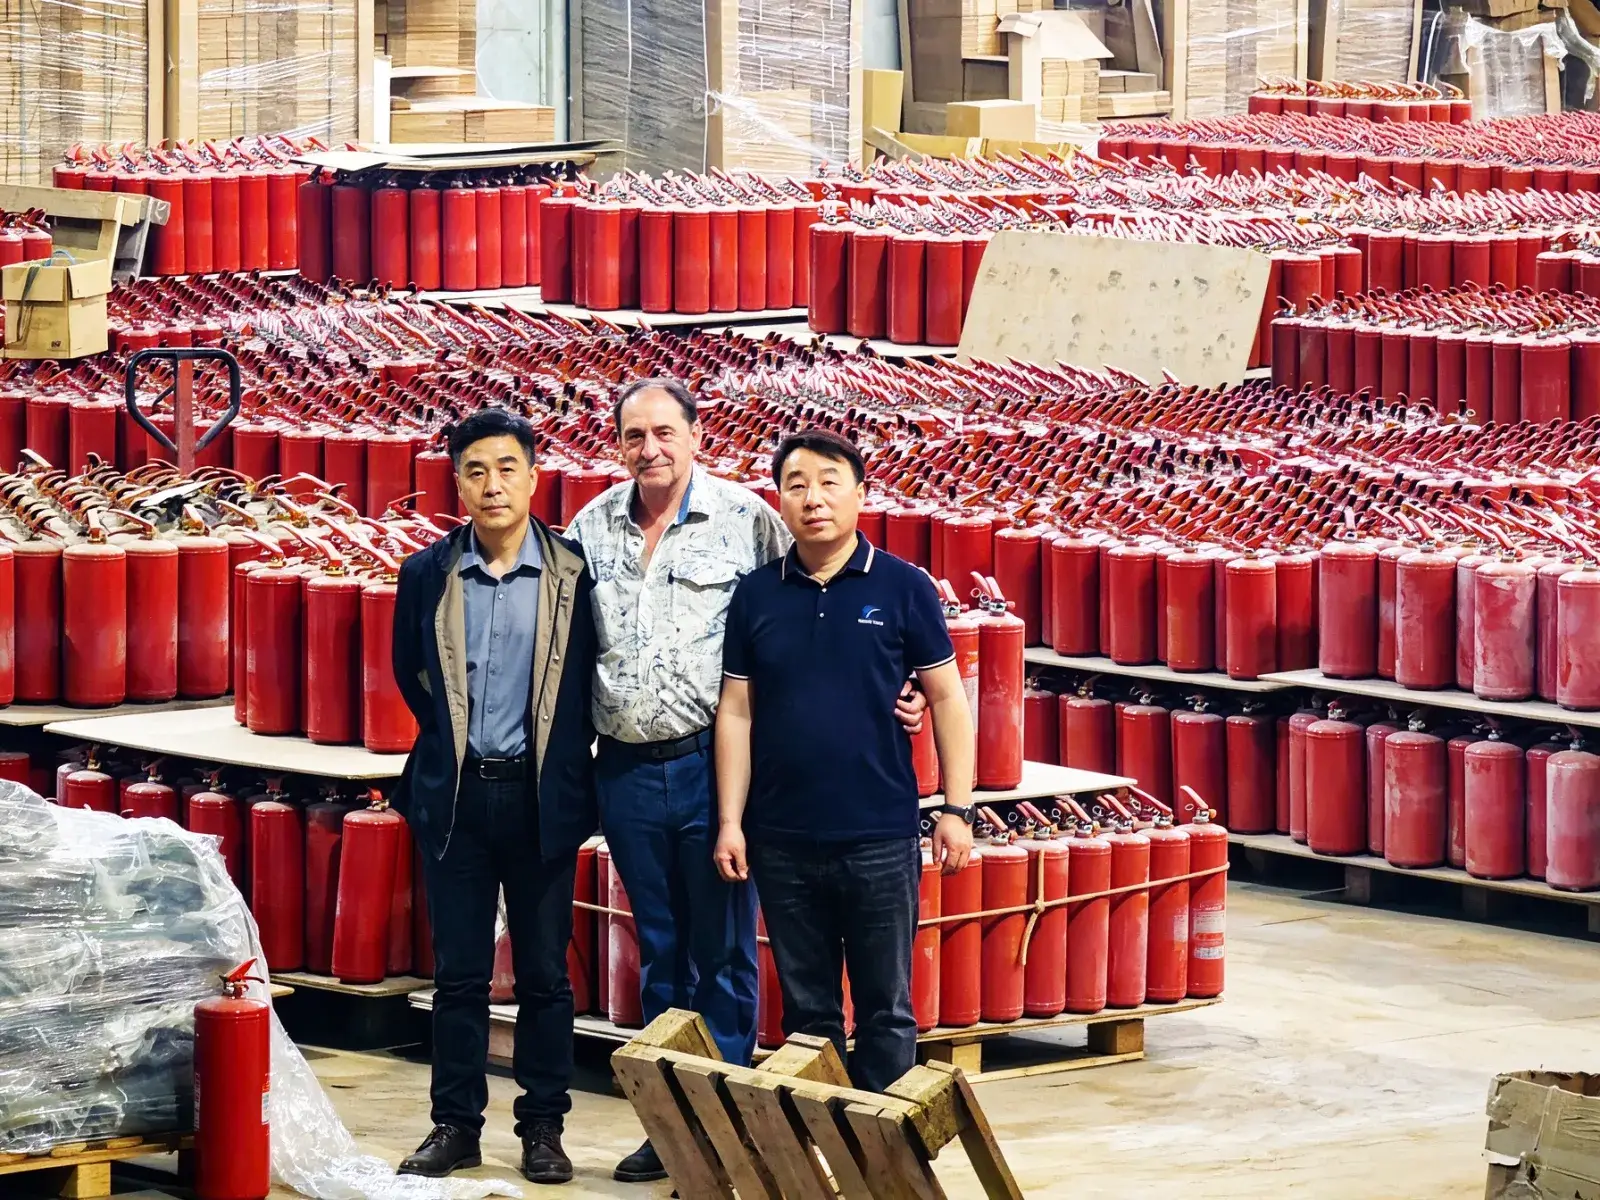
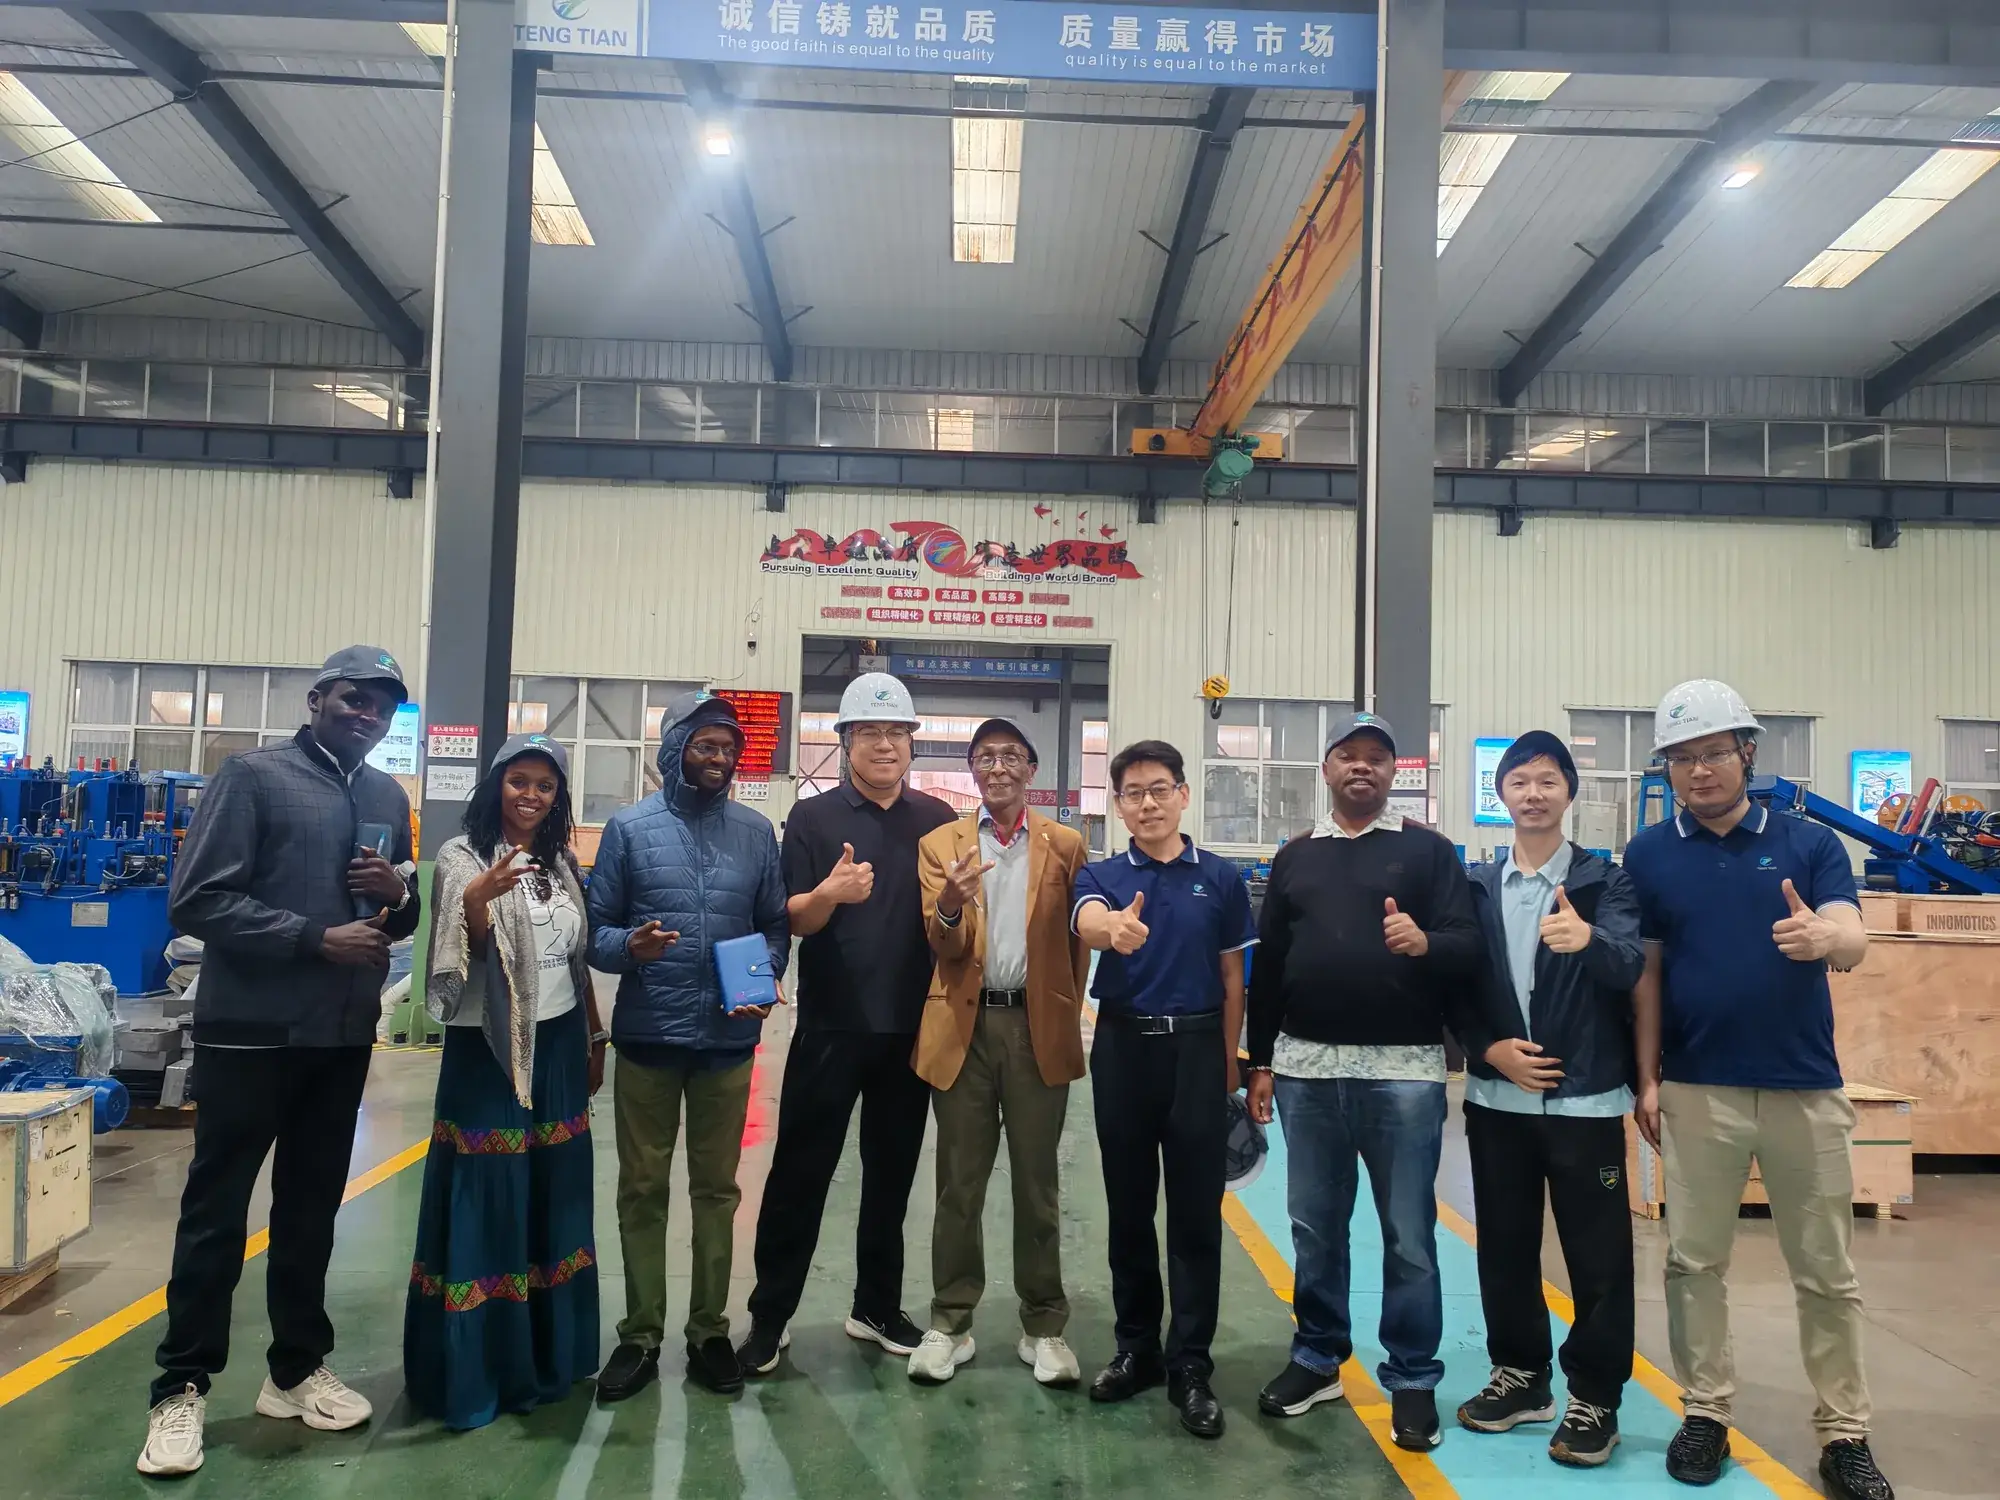
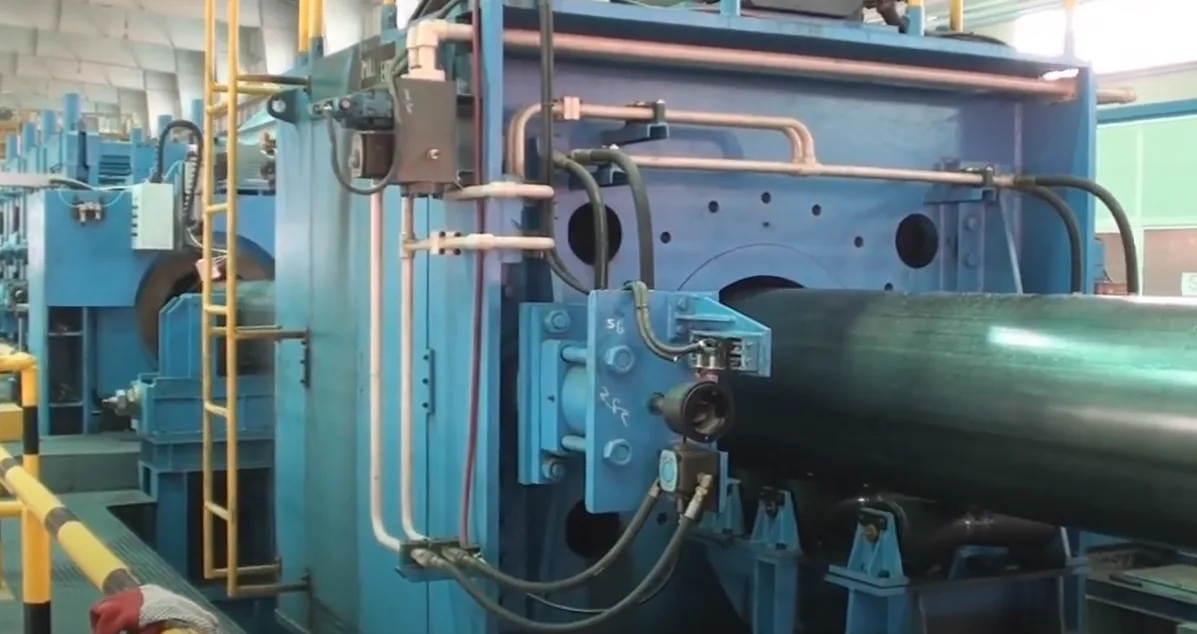
Our lines have gone to 25 countries — most make construction tube, and others run fire-extinguisher tube, furniture tube and other sections. In this diameter band: South Korea (254 × 8 and 200 × 200 × 12), Afghanistan (165 × 5), Thailand (165 × 6), Russia (HG165 × 6), Kyrgyzstan (HG168 × 5), Kenya (150 × 150 × 6), Pakistan and Mexico (127 × 6), Uzbekistan (HG127 × 3), Mexico (HG114 × 4), Egypt (HG89 × 5 and HG76 × 3), Sri Lanka (89 × 5) and India (76 × 3) for construction tube, Malaysia (HG60 × 3) for furniture tube, and Russia (168 × 7) for fire-extinguisher tube. The photographs below come from these deliveries, at customer plants or during customer visits to our works; customer names are withheld, and each card shows the country, the industry and the model or size.
What Decides Weld Quality at Large Diameter
Weld quality is set in the order the strip meets the line — incoming strip grade, thickness tolerance and flatness; forming roll material and heat treatment; high-frequency power and frequency matched to welding speed; squeeze amount and seam alignment; post-weld cooling; sizing and straightening; impeder and induction coil condition — and the list is the same on every step. Weld fusion and dimensional accuracy are on the equipment side; strip quality, incoming thickness tolerance and operating practice are on the buyer’s.
How the Line Stays Continuous
Two of the units exist to keep the line from stopping: the automatic shear and butt welder joins successive coils, and the spiral accumulator stores strip so the forming and welding section keeps running through the join.
The uncoiling and levelling units serve the same end. An expanding-mandrel uncoiler tensions the coil accurately, with unstable tension producing strip wander and loose coil; a five-roller leveller flattens the strip before forming, because residual curvature left at that point reappears later as a wandering seam.
How to Choose the Right Model
Choose by the whole product list, not one size. The seven windows overlap, so the diameter that decides the machine is the largest pipe in the plan — but check where the smallest pipe sits as well, and choose the step that covers the whole list with the least unused range.
Then check the wall. Wall thickness is what separates steps that share a diameter: the HG165 runs 3.0–7.0 mm, the HG219 4.0–8.0 mm, the HG273, HG325 and HG426 4.0–10.0 mm, and the HG508 and HG630 up to 16.0 mm. So a large diameter tube mill for 325mm pipe is the HG325 when nothing in the plan goes above Φ325 mm, and a large diameter tube mill for 426mm pipe is the HG426 with walls up to 10.0 mm, while the HG508 takes over for heavier walls from Φ219 mm up.
Then decide between straight seam and spiral, as set out above, and whether the pipe needs an inspection record. If it does, the line is one of our API line pipe mills: the API 406, API 426 and API 508 lines cover Φ152–406, Φ159–426 and Φ219–508 mm and add medium-frequency annealing, straightening, end facing, hydrostatic testing, and ultrasonic and eddy-current inspection after the weld.
On some of our higher-specification lines, material yield can reach 93 per cent; the yield actually achieved on any line also depends on the buyer’s scheduling and operating practice.
Scope of Supply, Installation and Commissioning
The line is dismantled into units and shipped in containers: heavy frames are braced and secured, while precision parts and wear items travel in wooden cases together with a spare-parts pack. Shipment is within 90 working days of the deposit.
Installation and commissioning are guided on site by our engineers, with online support behind them; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance. Payment terms and the steps that need operator training are set out on each model page.
Certifications: ISO 9001:2015 quality management system; CE marked under the EC Machinery Directive 2006/42/EC.
More from this line
More on this line — specifications, model steps and photographs.
From the Workshop
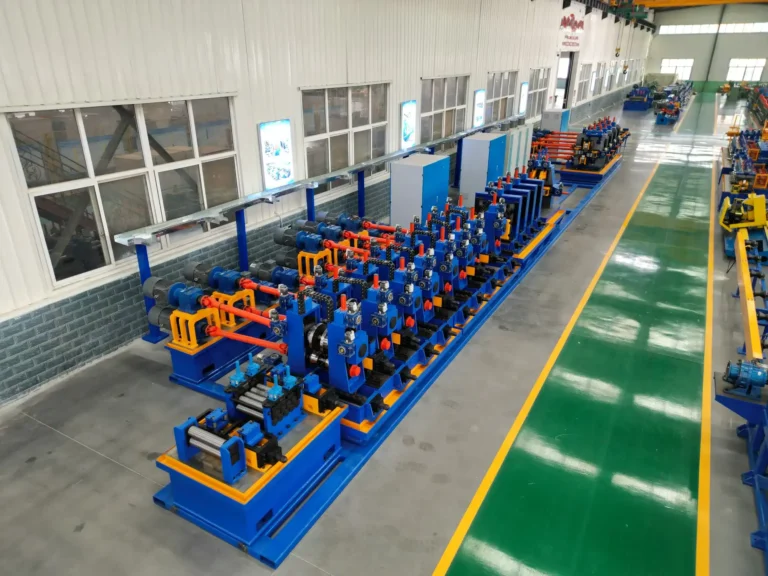 High-Frequency Welded Pipe Mill
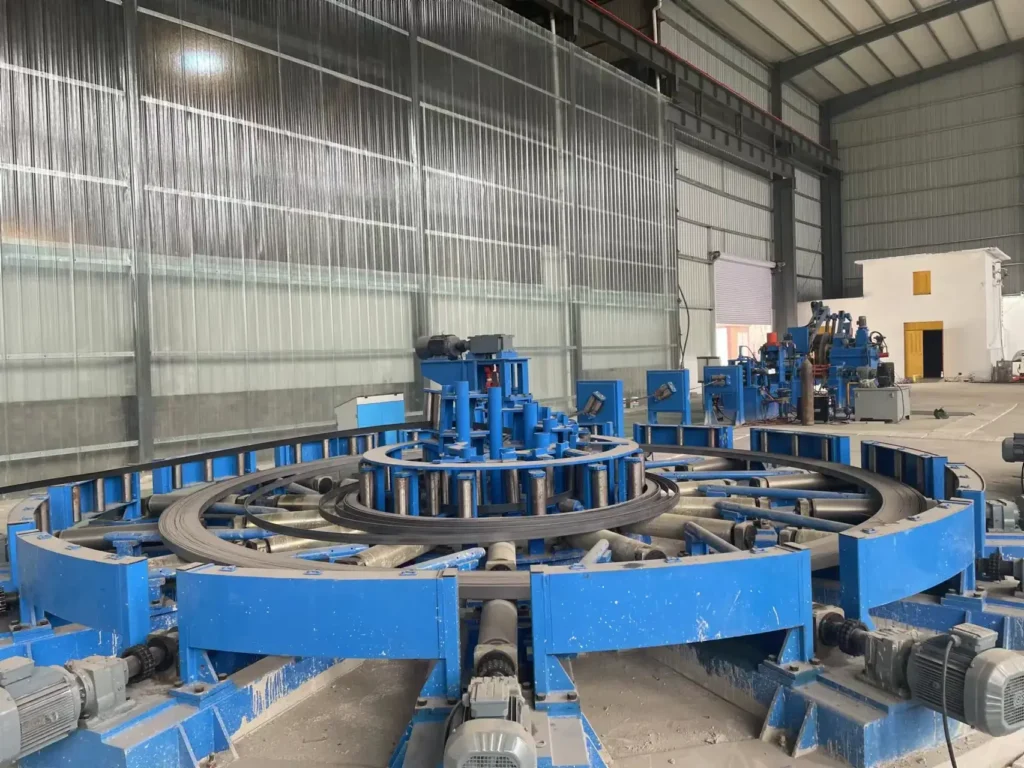 H-Beam Production Line
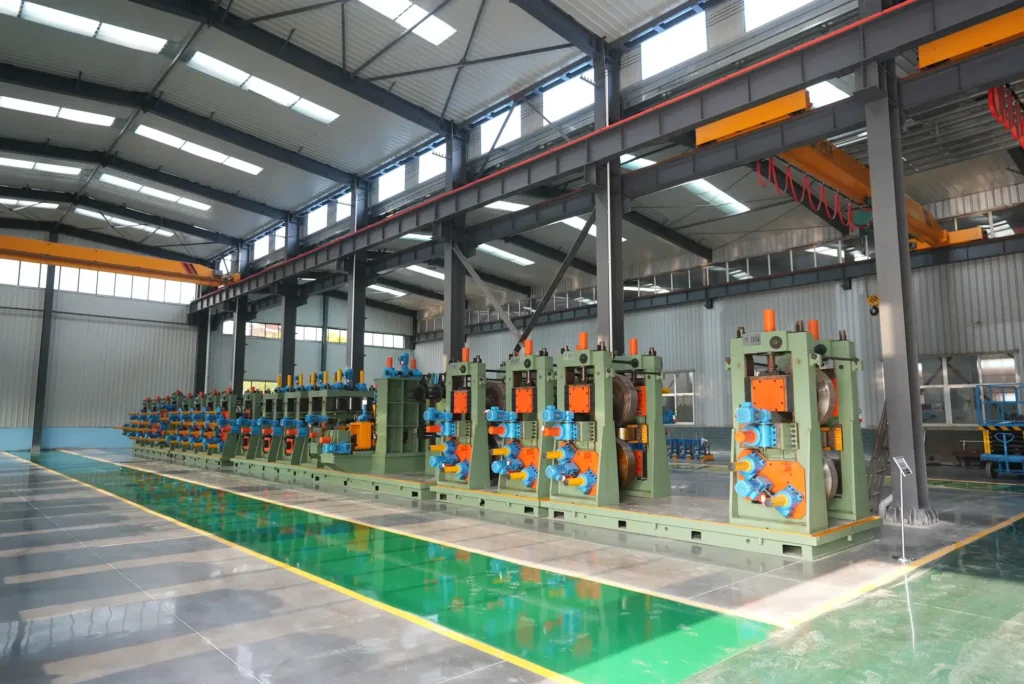 Direct Forming Square Tube Mill
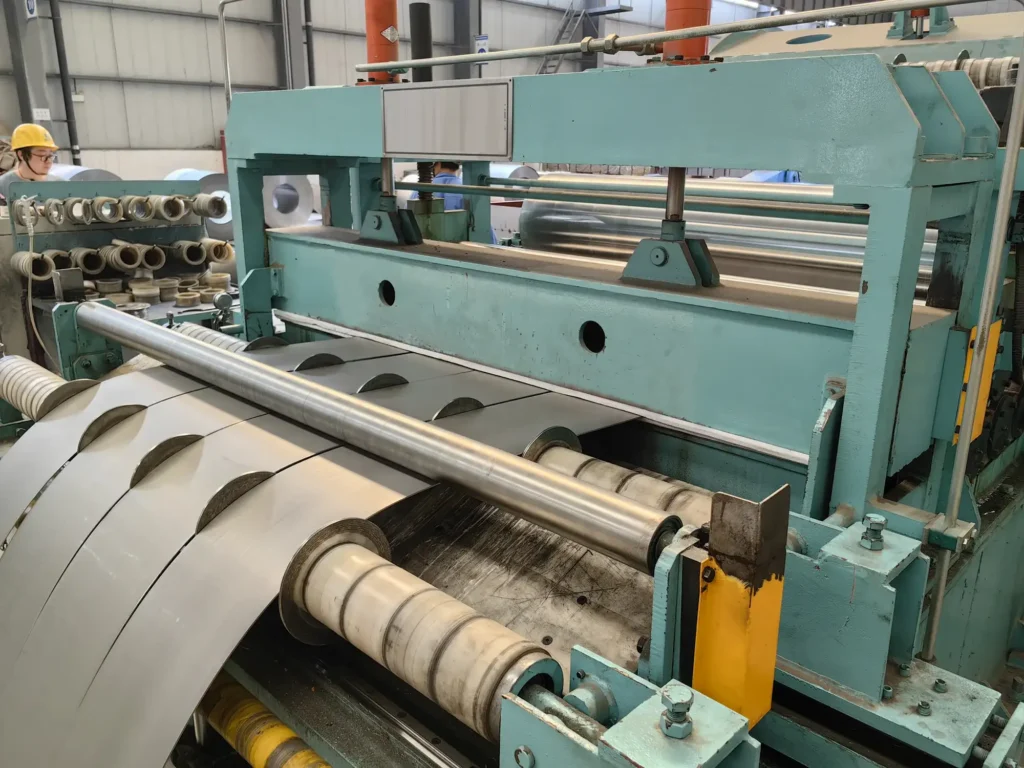 Cut-to-Length Line
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.