
Home › SSAW Spiral Welded Pipe Mill › SSAW or HFW
Both make welded pipe from coil, and Tengtian supplies lines for both.
In This Line
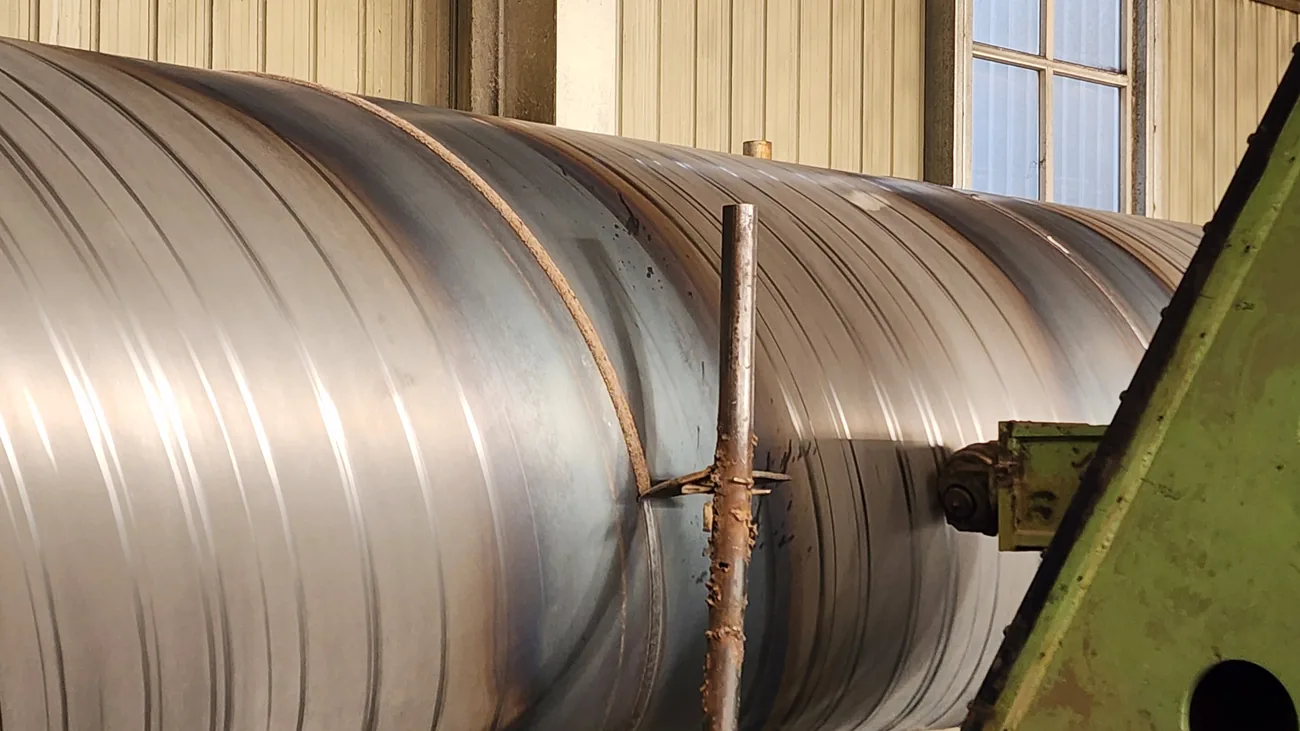
The high-frequency line runs a straight seam continuously up to Φ630 mm. The spiral welded pipe manufacturing process runs a spiral seam, one pipe at a time, from Φ219 to Φ1620 mm and sets the diameter through the forming angle. Between Φ219 and Φ630 both are possible.
Spiral Welded vs Straight Seam Pipe: Where the Two Routes Differ
- Ranges: HFW Φ10–630 mm across twelve classes of tube mill & welded pipe production line; SSAW Φ219–820 × 3–12 mm and Φ219–1620 × 5–16 mm across two classes.
- Diameter-change method: HFW conventional lines change rolls; the spiral line changes the forming angle, at 39° to 80°.
- Production mode: HFW continuous, kept fed by a spiral accumulator; SSAW discontinuous — one pipe cut, then the next.
- Standards by spiral class: GB/T 9711 and GB/T 5037 on Φ820; GB/T 9711 and API 5L on Φ1620.
- Spiral output with its calculation basis: about 62 t per 8-hour shift on Φ820 and about 120 t on Φ1620.
What Is the Difference Between SSAW and HFW
The high-frequency line — HFW, the high-frequency form of ERW — forms strip into a round or square section and closes a straight seam with high-frequency induction heat and squeeze rolls. The spiral line winds strip helically into a large-diameter tube and closes the spiral seam with submerged-arc welding on both the inside and the outside. The seam runs in a different direction, and almost everything else follows from that.
The trade-off, in short: against the high-frequency route, the spiral route substitutes a spiral seam plus submerged arc for a straight seam plus high-frequency welding, and sets the diameter through the forming angle.
That buys one machine a wide diameter span and walls up to 16 mm at large diameter — up to Φ1620 × 16 mm at 7.5 tonnes per pipe — at the cost of a lower welding speed, 0.5 to 3 m/min, and discontinuous production. That profile suits large diameters in small to medium batches.
To change size, the front bridge swings against the rear bridge to a new forming angle 39°–80°, and centre positioning keeps the strip lined up with the forming point.
Both processes are available from the same plant: high-frequency longitudinal and spiral submerged-arc welding, with diameters from Φ10 through to Φ1620 mm, so a buyer does not need a second source when the diameter goes up.
From the other side of the comparison, the high-frequency route is the faster one: higher welding speed, a straight seam, and a fit with structural and ordinary fluid pipe.
The Φ219–630 mm Overlap: When Either Process Will Work
The high-frequency range reaches Φ630 mm at its top class; the spiral range starts at Φ219 mm. Between those two numbers both processes can make the pipe.
Within the overlap, several facts bear on the choice. On the high-frequency side, production is continuous and the accumulator keeps the mill fed through coil changes, so output is a function of running speed rather than of cycle time; the top class, on the large-diameter HFW tube mill, covers Φ325–630 mm.
On the spiral side, production is discontinuous and welding speed is 0.5 to 3 m/min. Both spiral classes start at Φ219 mm — Φ219–820 × 3–12 mm and Φ219–1620 × 5–16 mm — so either one covers the whole overlap band.
Worked Example at Φ426 mm
At Φ426 both routes are open. On the high-frequency side three model steps reach it: HG426 (Φ165–426 mm, wall 4.0–10.0 mm), HG508 (Φ219–508 mm) and HG630 (Φ325–630 mm), both with walls of 4.0–16.0 mm. On the spiral side the limit is the grade: at Φ426 the Φ820 class takes up to 10 mm in Q235, 8 mm in Q355B and 7 mm in L360, and the Φ1620 class up to 9.5 mm in Q235B and 8 mm in Q355C or L360. If the wall you need sits inside both, the choice comes down to section shape, batch size and end use.
Worked Example at Φ820 mm
At Φ820 there is a full example, with its calculation basis. On the Φ820 spiral class, output is set at about 62 tonnes per 8-hour shift, calculated on 1050 mm strip width, 12 mm wall, Φ820 outside diameter and 12 m pipe length — roughly 21 pipes at about 3 tonnes each.
Two-shift annual output on that class is set at 10,000 to 20,000 tonnes.
The comparison at this diameter is not a choice, because Φ820 is above the high-frequency ceiling of Φ630 mm. That constraint is the reason the spiral line exists: a buyer who needs line pipe, water pipe or structural pipe above Φ630 has to move to spiral submerged-arc.
One selection constraint applies at this diameter and is easy to miss: maximum wall thickness is per steel grade, not a single number.
At Φ820 the Φ820 class takes up to 12 mm in Q235, 11.5 mm in Q355B and 10 mm in L360; the Φ1620 class takes up to 12.7 mm in Q235B and 10 mm in Q355C or L360. Grade is therefore chosen before wall.
Decision Rule by Target Diameter and End Use
Diameter is the first rule and the primary selection dimension on both sides. Below Φ219 mm only the high-frequency lines cover the size, and above Φ630 mm only the spiral lines do; the welded pipe guide sets out the full range by process. Between them both lines cover the size, and the choice inside that band is the buyer’s decision.
End use is the second rule, and for the spiral line the end uses are explicit: oil and gas line pipe, low-pressure fluid and urban gas pipe, water supply and drainage pipe, and industrial structural pipe. On the high-frequency side the uses are fluid transport pipe and structural and scaffolding tube.
Section shape is the third rule, and it often settles the matter before diameter does. The high-frequency lines make round, square and rectangular tube; the spiral line makes large-diameter round pipe. A square or rectangular section therefore points to the high-frequency route regardless of the overlap.
Batch shape is the fourth rule and it follows from production mode. The spiral profile suits large diameters in small to medium batches, because production is discontinuous — one pipe cut, then the next — while the high-frequency line runs continuously, with the accumulator carrying it through coil changes.
Standards and Testing on the Spiral Line: GB/T 9711-2017 and API SPEC 5L
The Φ1620 class can be supplied with the full SSAW inspection chain — a 225 kVA X-ray unit, a 1200-tonne hydrostatic tester and offline ultrasonic covering 100% of the weld and at least 35% of the pipe body; the Φ820 class runs X-ray and hydrostatic testing without ultrasonic.
The Φ820 spiral class is built to GB/T 9711 and GB/T 5037; the Φ1620 class is built to GB/T 9711 and API 5L, with GB/T 9711-2017 and API SPEC 5L, 46th edition, named at the inspection stages.
For the machinery itself, no single certification is mandatory in every market: what governs is the destination market’s machinery-safety rules plus the standard the finished pipe has to meet. Tengtian holds CE marking and an ISO 9001 quality system certificate.
Frequently Asked Questions
What actually makes SSAW pipe different from HFW pipe? Seam direction and welding method. The high-frequency route closes a straight seam with induction heat and squeeze rolls and runs continuously; the spiral route winds the strip helically and closes the spiral seam with submerged arc on both faces, running discontinuously at 0.5 to 3 m/min.
The spiral route sets the diameter through the forming angle, at 39° to 80°.
Both lines can make Φ219–630 mm pipe – which one should I buy? Inside that band there is no single right answer — the choice is the buyer’s. Below Φ219 only the high-frequency lines cover the size, above Φ630 only the spiral lines, and inside the band both do. Section shape, batch size and end use are the axes that narrow it further.
How different are the two welds, and does the heat input matter? The high-frequency route heats only the strip edges: skin effect and proximity effect concentrate the current at the open seam, and the heated edges are then forged together by squeeze rolls; the process is classed as solid-state or fusion pressure welding.
The spiral route uses submerged-arc welding on both the inside and the outside of the spiral seam — outer double, inner single on the Φ1620 class.
Which standards do buyers usually test each type of pipe to? By class rather than by process. The Φ820 spiral class is built to GB/T 9711 and GB/T 5037; the Φ1620 class to GB/T 9711 and API 5L, with GB/T 9711-2017 and API SPEC 5L (46th ed.) named at the X-ray and ultrasonic stages.
Which process gives better output for large-diameter pipe above 630 mm? Only one of the two reaches large diameter at all, so the comparison resolves itself. Above Φ630 mm the high-frequency line is out of range.
On the spiral line, output at Φ1620 is set at about 120 tonnes per 8-hour shift, on 1250 mm strip at 16 mm wall making Φ1620 × 12 m pipe — roughly 15 pipes at 7.5 tonnes each.
Can I buy both lines from the same supplier? Yes. The same plant offers both high-frequency longitudinal and spiral submerged-arc welding and covers Φ10 to Φ1620 mm.
From the Workshop
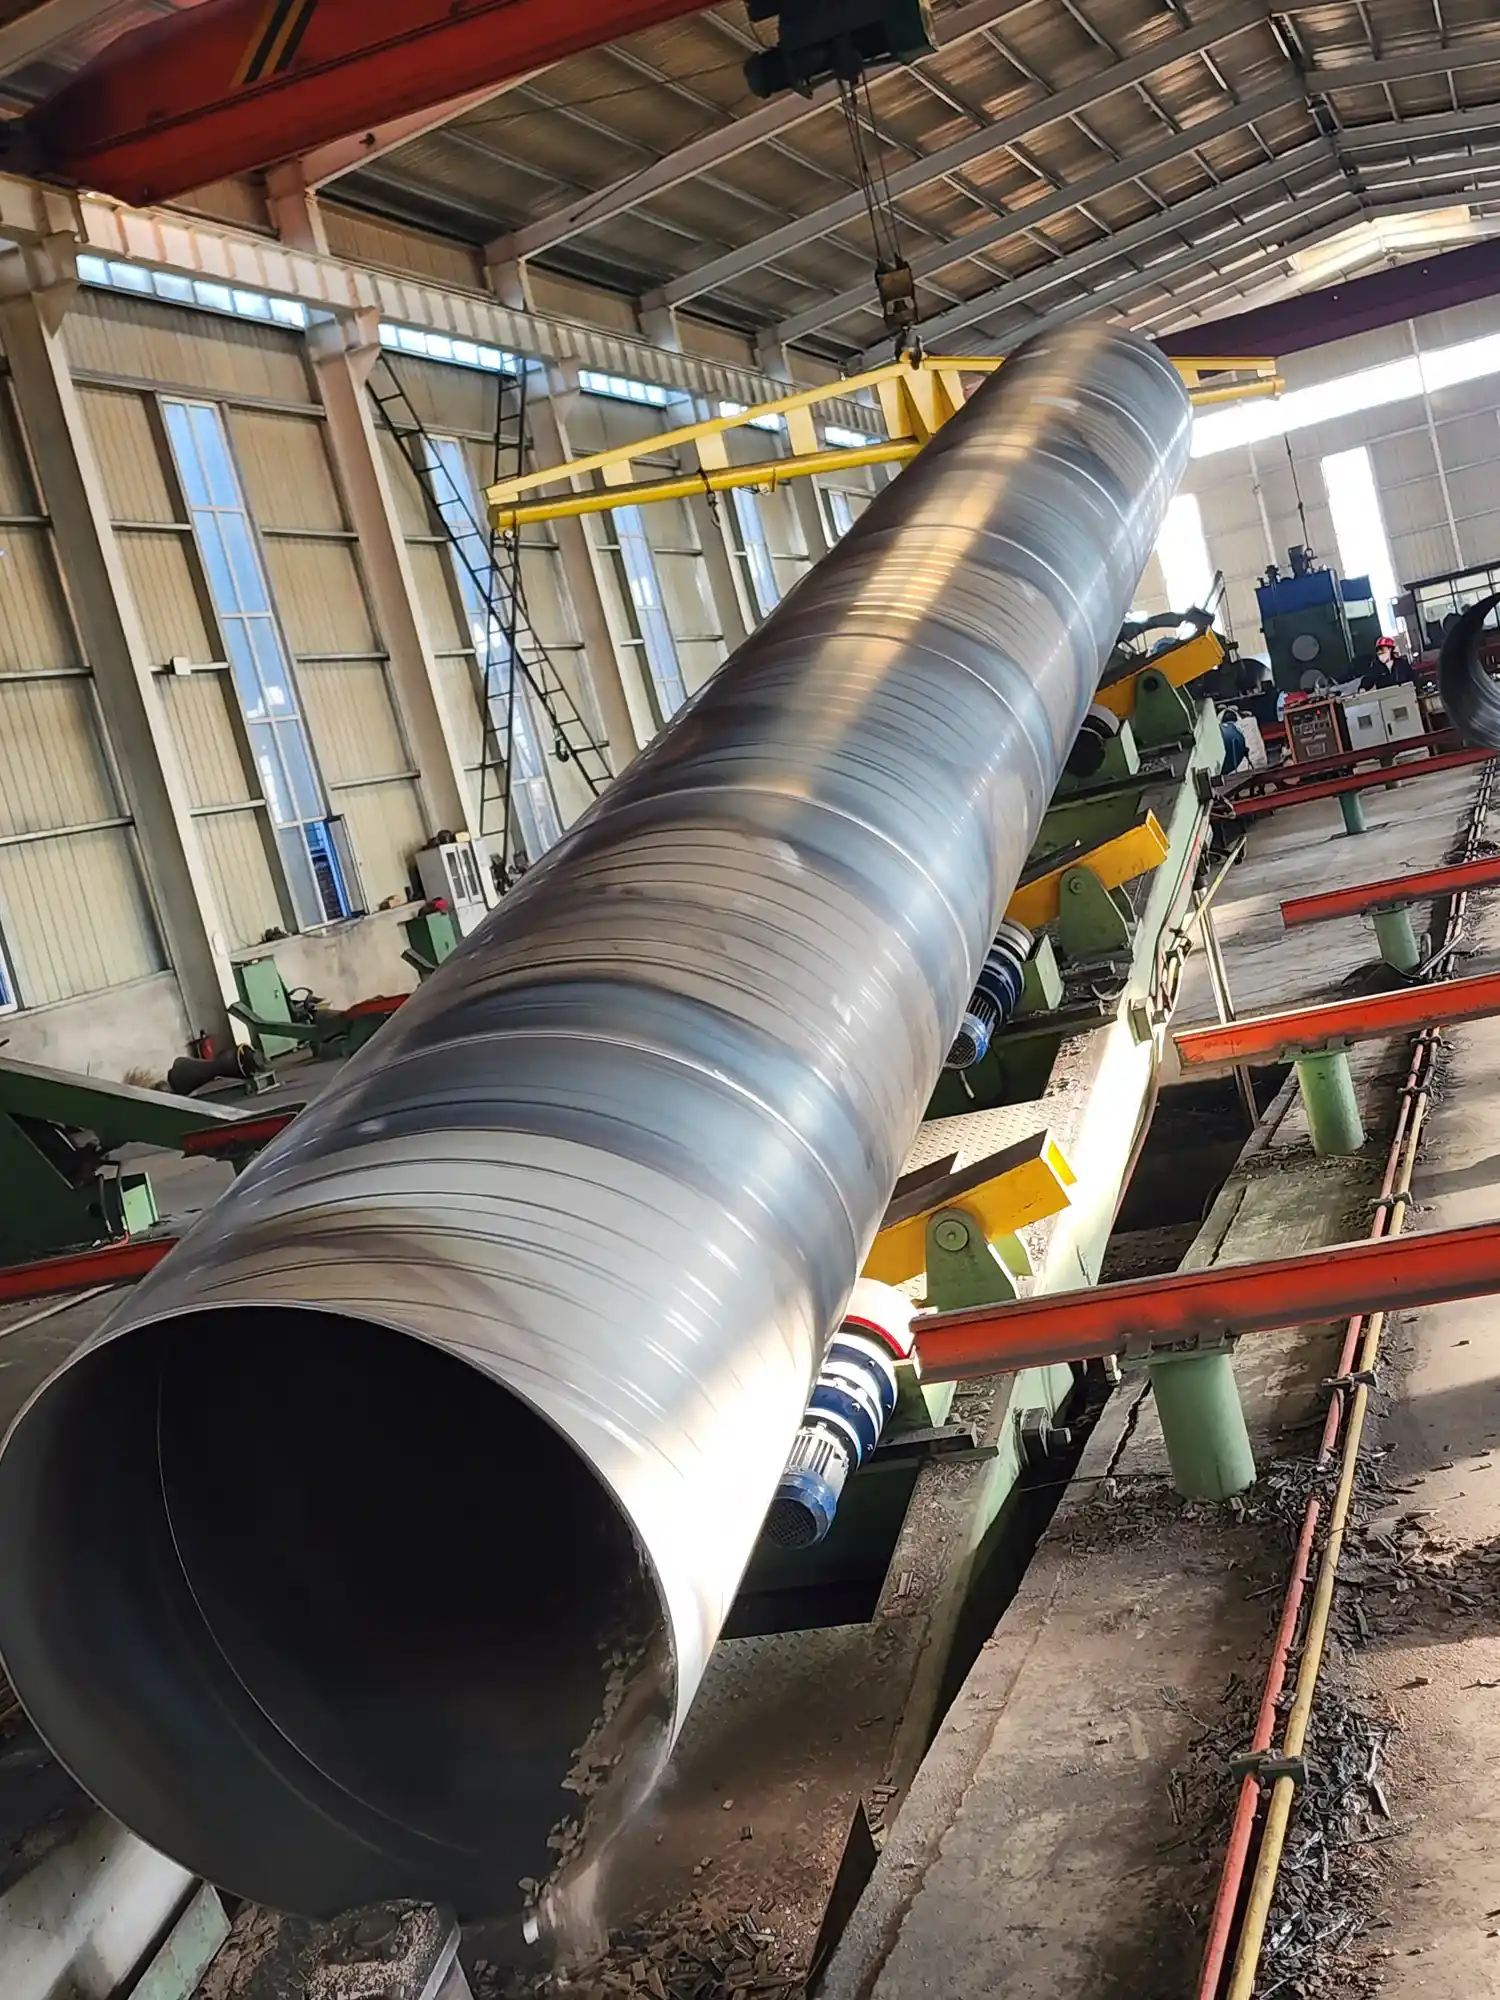
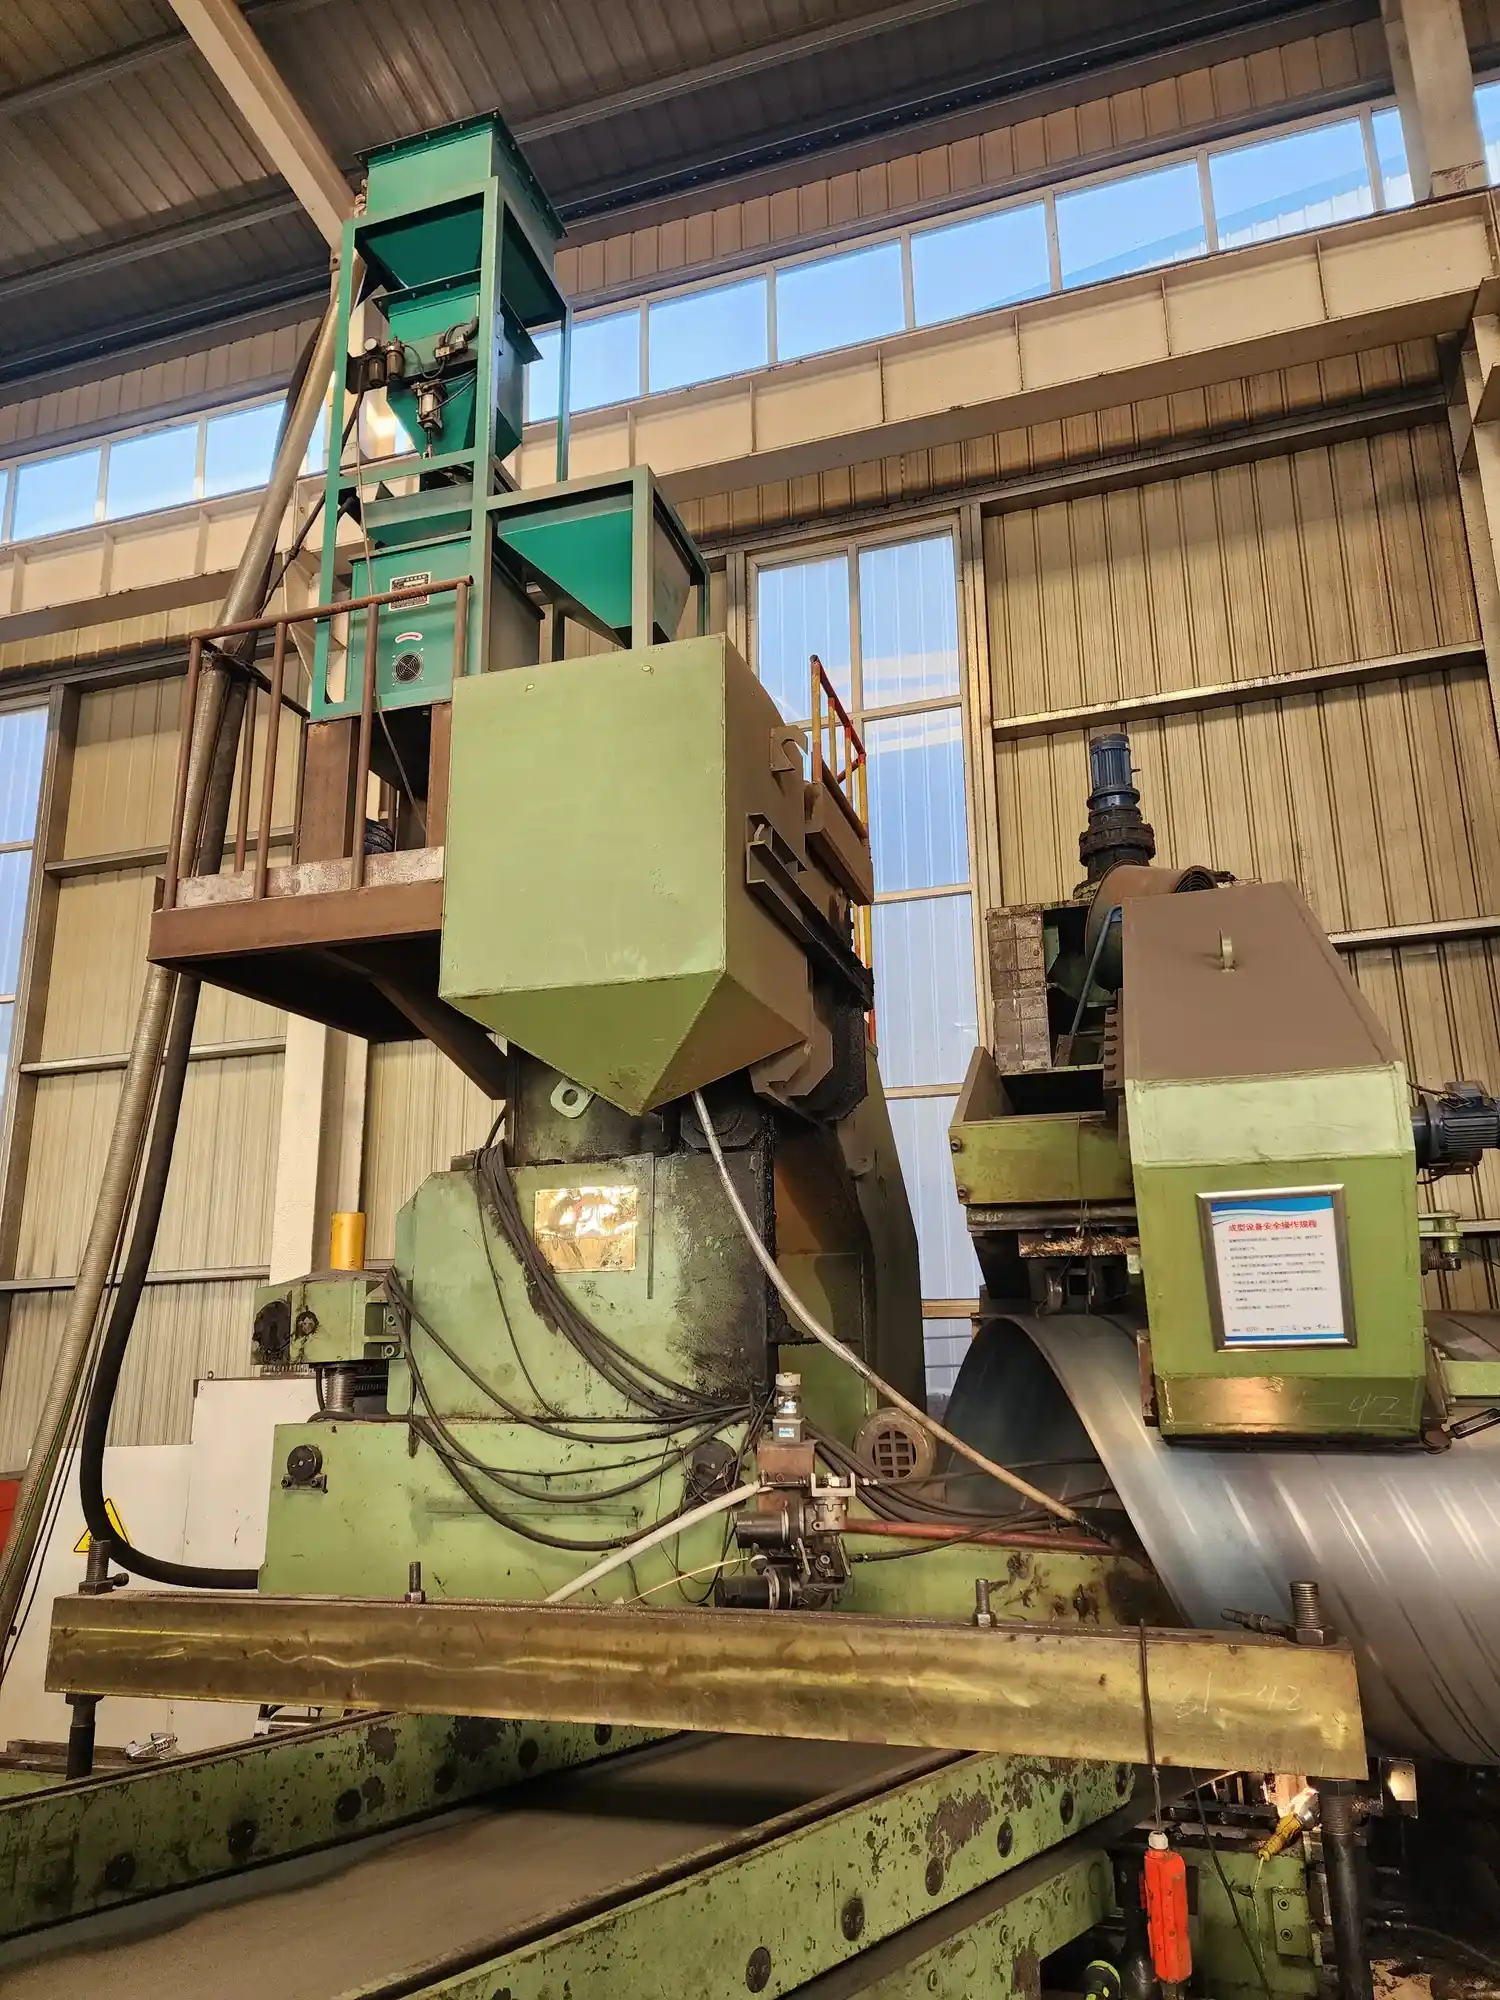
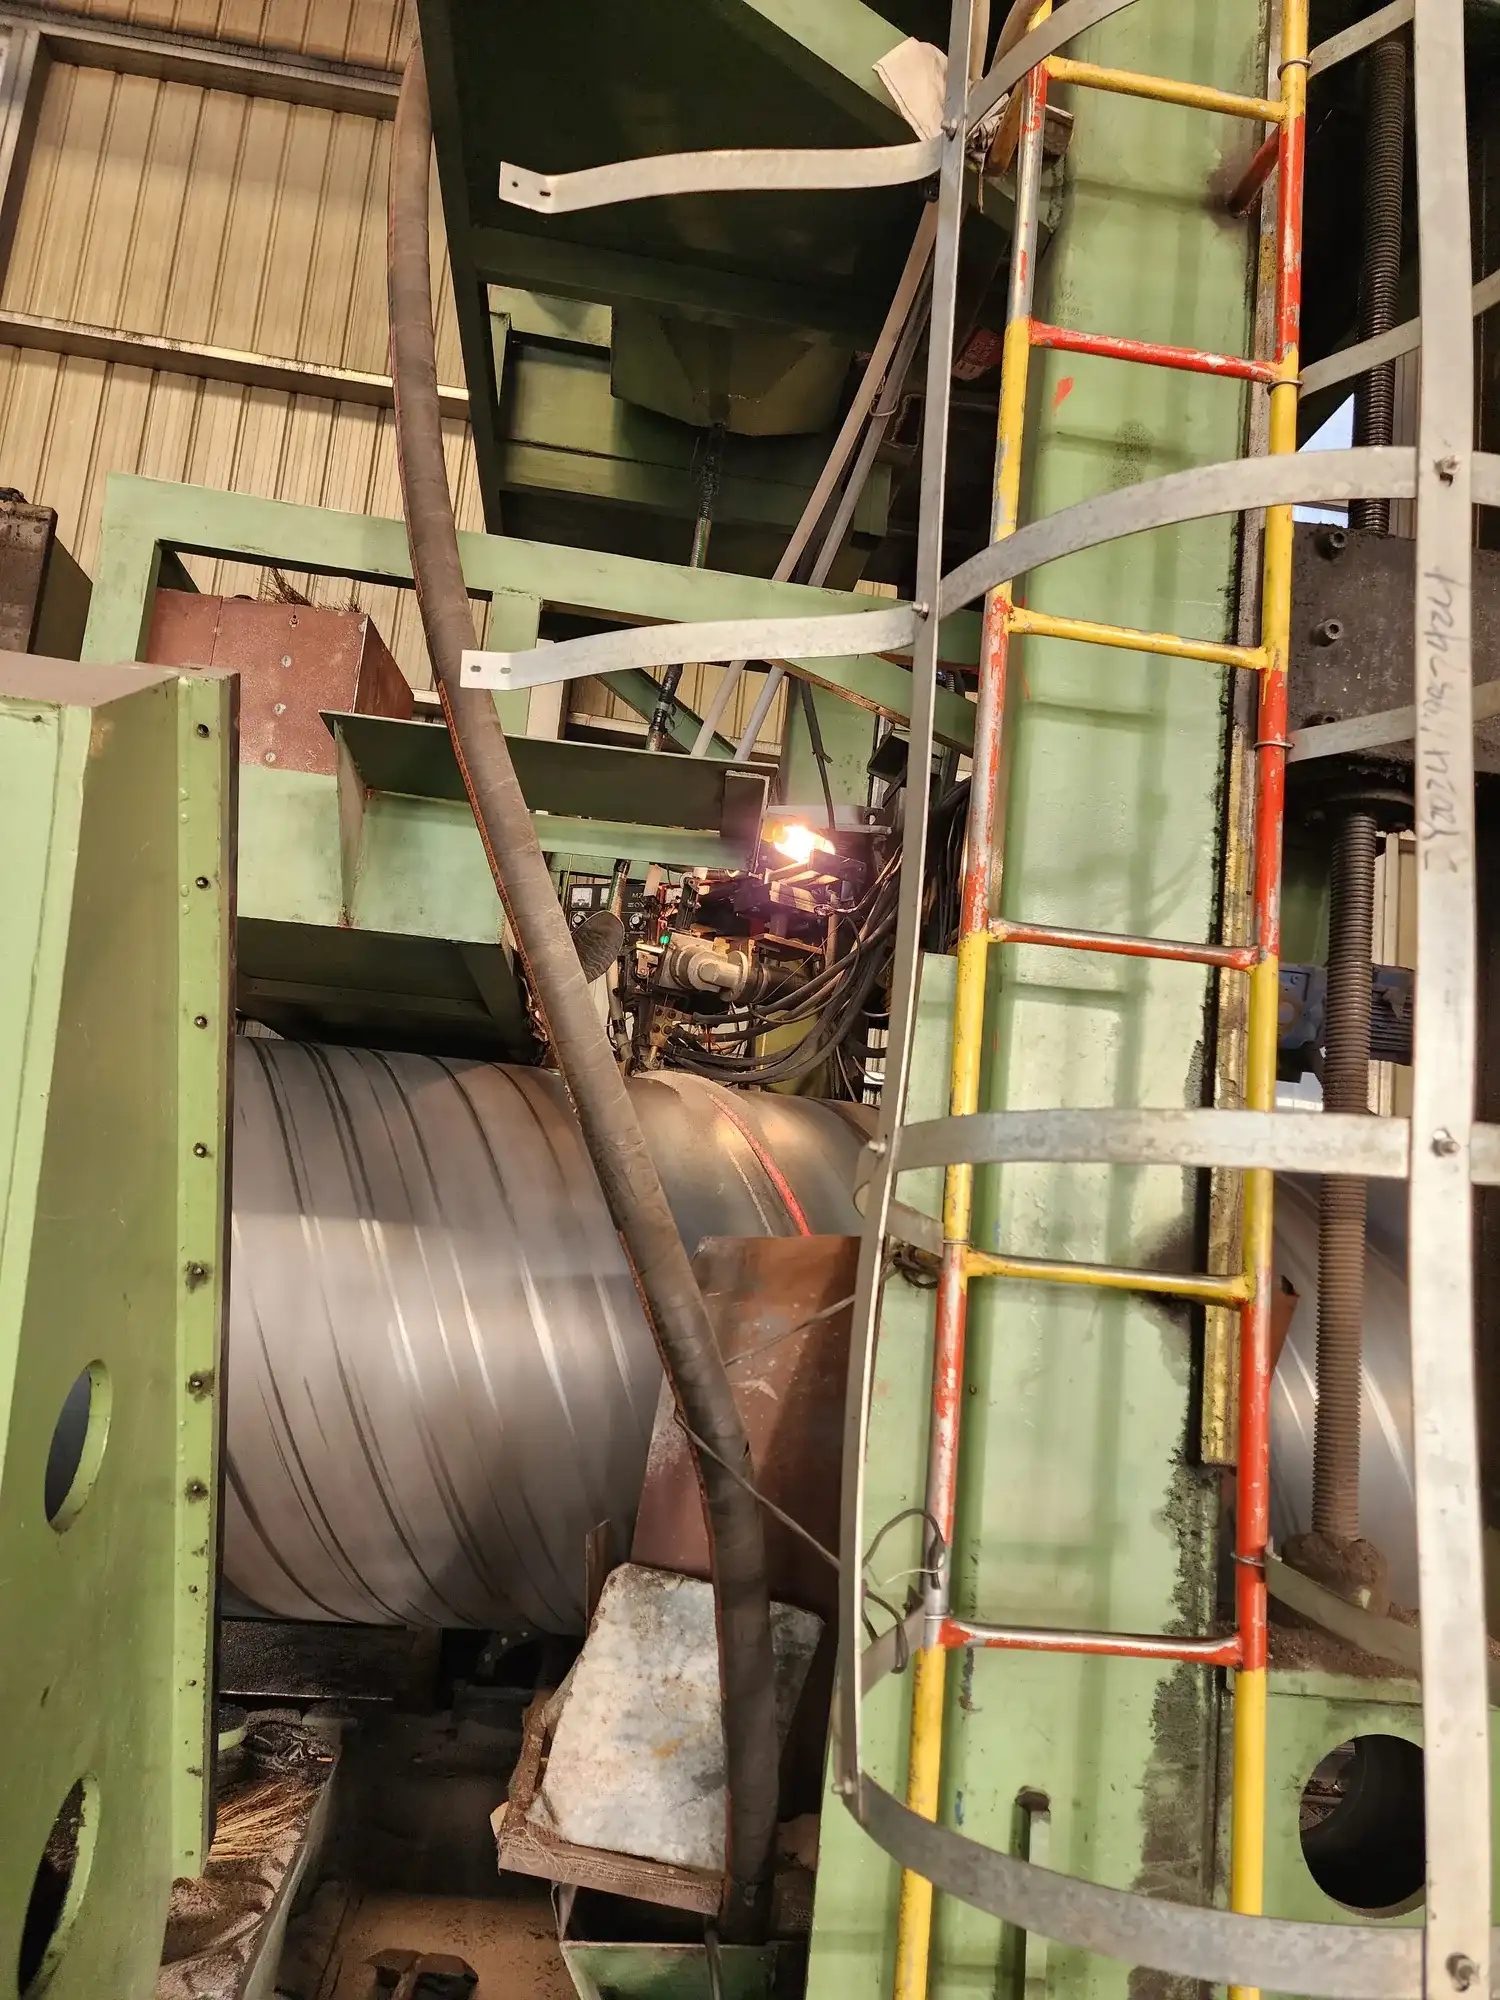
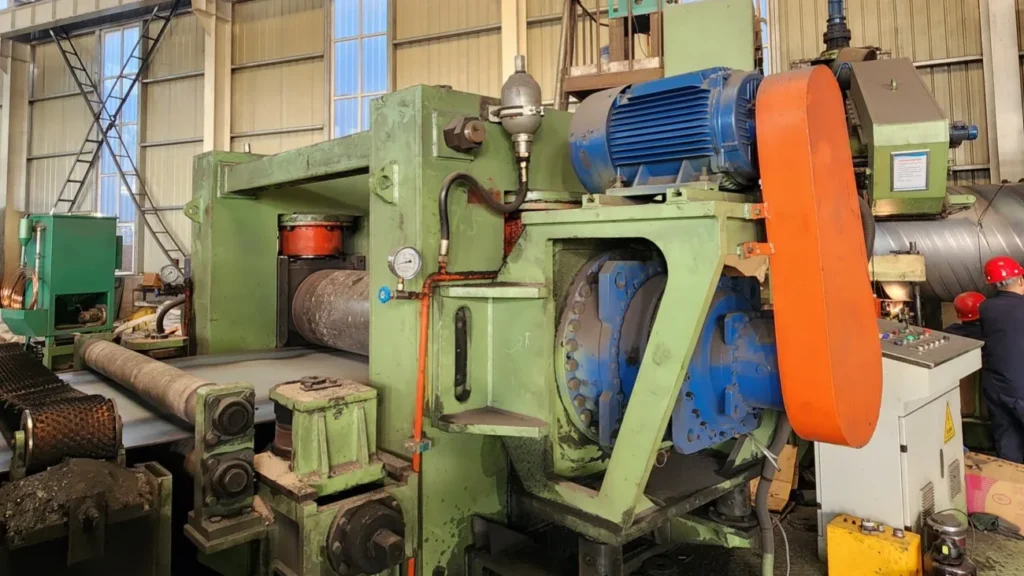 What the Large-Diameter Tier Adds
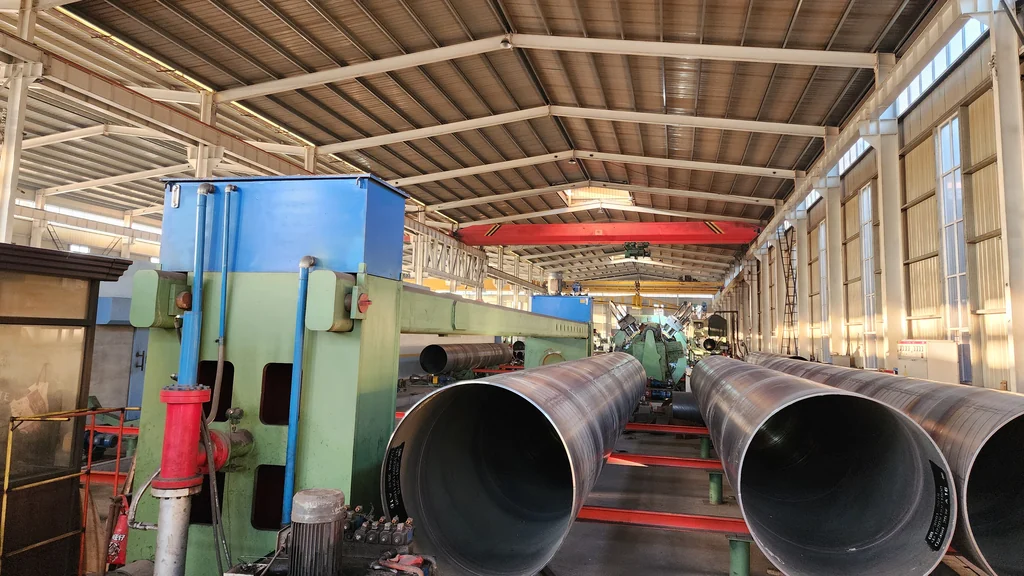 X-Ray, Hydrostatic and Ultrasonic, Station by Station
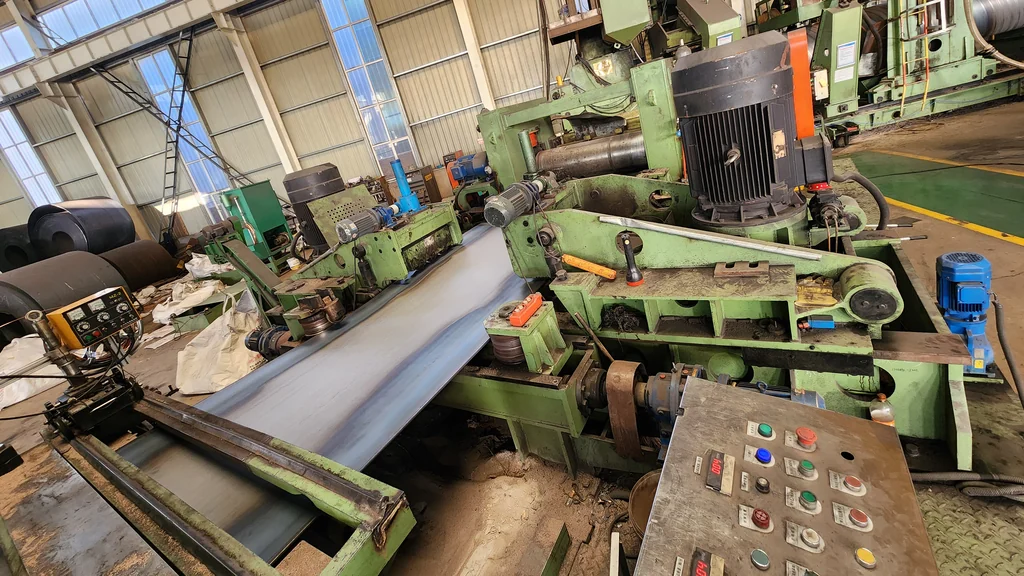 Changing Bore Without Changing Rolls
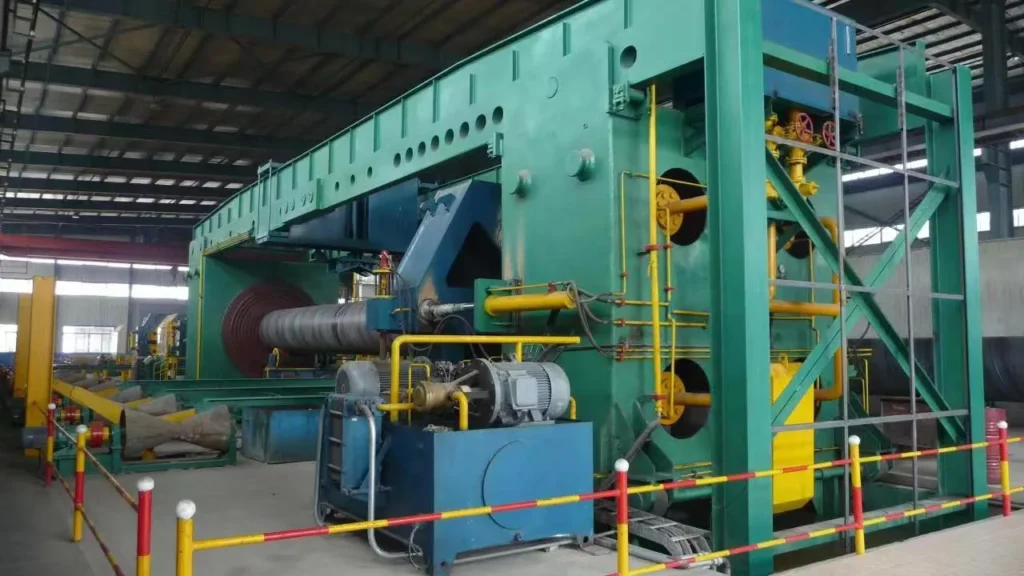 GB/T 9711 for Spiral Welded Line Pipe
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.