
Home › Resources › Welded Pipe Guide › What Is ERW Pipe
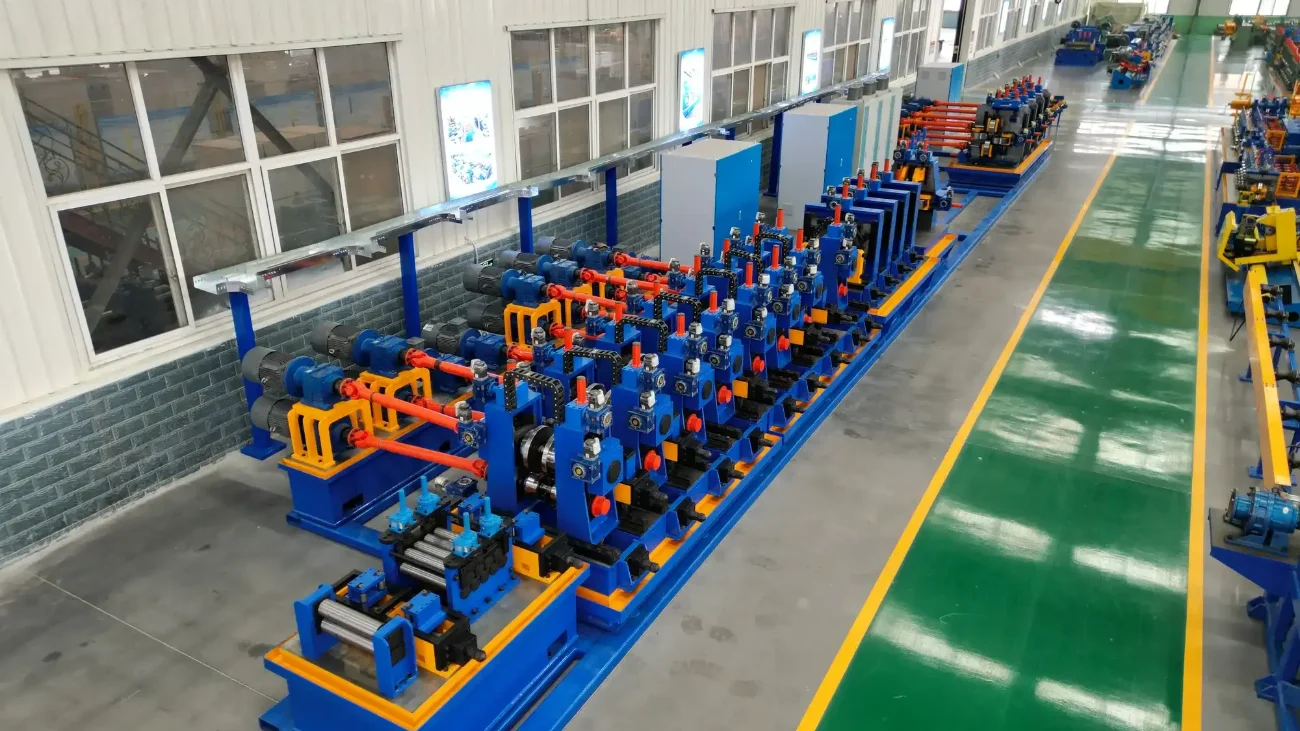
ERW pipe is steel pipe roll-formed from strip and closed along a straight seam by electric resistance welding, with no filler metal added. It goes into fluid transport, construction, structural work and machinery, and it is made on high-frequency tube mills like the ones we build.
What Is ERW Pipe
ERW pipe is welded pipe made by electric resistance welding — the seam is closed by the resistance heat of a current passed through the strip edges, not by adding filler. At Tengtian the process is called HFW, high-frequency welding, and “HFW/ERW” is one name for the same route.
Everything below therefore describes the HFW route, built as the tube mill & welded pipe production line: a continuous forming-welding-sizing installation in which steel coil is uncoiled, formed, high-frequency induction welded, sized and cut, producing longitudinally welded pipe in round, square or rectangular section. Terms used along the way are explained in the tube & pipe mill glossary.
There are twelve size classes, HG32 through HG630, covering Φ10–630 mm outside diameter and 0.5–16 mm wall.
What buyers are buying the line for is just as clear. There are four things: continuous production without stopping, one line covering multiple sizes, stable yield and weld quality, and changeover efficiency.
Those four are what the equipment is designed around, and they explain the accumulator, the twelve size classes and the yield figure.
In one sentence, an ERW line is a complete automated line that turns steel coil continuously into longitudinally welded steel pipe, selected by target diameter, with welder power and unit configuration stepping up with that diameter.
What is meant by ERW pipe
Read strictly, the term names a joining method rather than a product grade. In practice, the current behaves like this. Because of the skin effect and the proximity effect, high-frequency current concentrates at the open edges of the formed shell — in other words, at the seam — and heats that narrow zone quickly to welding temperature.
The join itself is then made by pressure, not by melting a filler into a gap. It is pressure welding: the two heated edges are pressed together by squeeze rolls and forge into a continuous seam.
The downstream products are pipe for fluid transport, construction and structural work, general machinery and household applications — the line’s job being to turn strip into standard longitudinally welded pipe for those markets.
What Is ERW Pipe Explained
A coil car feeds the uncoiler, whose four-bar expanding mandrel grips pneumatically and pays the strip off. The line is best understood as a sequence, and each stage has its own failure mode.
Levelling is the first decisive stage. The head of the coil is flattened, and on HG89 and larger lines a five-roll leveller straightens the strip before it goes on, because strip flatness is the precondition for good forming.
Coil joining and accumulation keep the mill running. An automatic shear cuts off the irregular head and tail and butt-welds the next coil on; a spiral accumulator stores strip between that joint and the mill so the mill keeps being fed while the join is made. Both serve continuous production without stopping.
Forming is where the pipe shape is decided. Rolls progressively bend the flat strip into the round or square open shell, and getting the pass schedule or roll gap wrong has clear consequences: an uneven open seam and a distorted shell, leading to off-centre welding and out-of-tolerance roundness or squareness.
Welding follows immediately, and it is the core quality stage. If power, welding speed and squeeze are mismatched, the result is lack of fusion, cold weld or burn-through, and downstream the pipe fails pressure and NDT acceptance.
Sizing, straightening and cut-off finish the pipe. After cooling, sizing rolls bring the outside diameter to final dimension and give initial straightening; a flying saw then cuts to length automatically at full line speed.
Running the line is five operator stages, and they are worth separating from the equipment stages above because they are where training matters.
Loading and threading comes first: the coil car delivers, the uncoiler tensions, and an operator guides the strip head through the leveller into the mill, with centring, tension and head flattening deciding whether it threads at all.
Joining coils comes second. Before one coil runs out, its tail and the next head are sheared and butt welded, coordinated with the accumulator so the mill never stops; the failure modes are strip breaks that stop the line and scrap pipe at the joint.
Setting the size is third, and there are two behaviours here: a conventional line changes rolls, while the direct-forming square line adjusts servos and does not. What goes wrong is shape drift after a size change and commissioning scrap, and the stage needs a trained changeover crew.
Setting the weld is fourth and needs specialist process training: welder power and welding speed are set, the line is started, and the operator watches the run. Fifth is cut-off and collection, where the flying saw cuts to the set length and the run-out table collects.
What is ERW welding
Three components carry the weld, and they are not equal. The high-frequency welder is core: it supplies the welding energy and governs weld fusion quality and welding speed, and its power steps with diameter — 150 kW on HG32 and 1500 kW on HG630.
The induction coil and the impeder are key rather than core components. Their job is to concentrate the high-frequency current at the seam through the skin and proximity effects, so they act directly on welding thermal efficiency and weld consistency; they are also wear parts with continuing supply.
Control sits underneath both. The PLC and VFD system is core because it holds the tempo and speed of forming, welding, sizing and cut-off together; unstable control produces speed fluctuation, length error and higher downtime.
HFW or Spiral — Which Route for Your Diameter
The short answer is diameter. Within Φ10–630 mm the high-frequency route is the one we build; above Φ630 mm the spiral (SSAW) route takes over, up to Φ1620 mm.
How to Decide: Target Diameter, Application and Volume
The twelve classes are Φ10–32, 16–50.8, 25–76, 32–89, 45–114, 60–165, 114–219, 114–273, 165–325, 165–426, 219–508 and 325–630 mm. Diameter selects the size class, and it is the primary selection dimension.
Application is in two groups. Fluid transport pipe covers oil and gas, municipal water and gas, chemical and heating pipework, and the buyers there need continuous stable output, reliable welds, high yield and coverage across several wall thicknesses and diameters.
Structural and scaffolding tube covers load-bearing construction, scaffolding and general machinery sections, where the concerns are flexible size switching, stable square and rectangular forming, and good straightness and edge appearance.
Automation level is a separate axis rather than a consequence of size: semi-automatic and full PLC automatic are alternatives, with the automatic tube mill as the high-automation class.
Section shape is the second choice and it is usually not exclusive: most HG classes can make round, square and rectangular tube on the same line.
Frequently Asked Questions
What is the practical difference between ERW and spiral welded pipe? The difference between the two welded routes is clear-cut. High-frequency longitudinal welding closes a straight seam with resistance heat and squeeze rolls, runs continuously, and covers Φ10–630 mm.
Spiral submerged-arc welding closes a spiral seam with a submerged arc on both faces, changes diameter by changing the forming angle instead of changing rolls, runs discontinuously at 0.5 to 3 m/min, and covers Φ219–1620 mm.
Which one suits my target diameter and application? There are twelve HG classes, and target diameter is the first thing a buyer picks by. Below Φ630 mm the high-frequency route covers round, square or rectangular section, for fluid transport or structural use.
Above Φ630 mm the high-frequency line is bounded and the spiral route is the one that reaches further.
How do running costs compare between the two routes? Low roll wear, high yield and quick changeover keep long-run running cost under control, and high-end configurations can reach a yield of 93% or more.
Which standards apply to each route? On the high-frequency side, line pipe to API 5L is made on the API configuration of the tube mill. On the spiral side, the Φ820 class is built to GB/T 9711 and GB/T 5037, and the Φ1620 class to GB/T 9711 and API 5L.
Which option ships and commissions faster? Standard lines ship within 90 working days of the deposit, with plant-level customisation scheduled from our own manufacturing base. The term is the same for both welded routes. Commissioning takes two to three engineers on a high-frequency line, with the period set in the quotation, and five personnel — four engineers and an adjustment technician — over forty days on a spiral line.
Can one supplier provide both routes? Yes. The same plant supplies both high-frequency longitudinal and spiral submerged-arc welding, with diameters running from Φ10 to Φ1620 mm, so a buyer does not have to find a second supplier when the diameter goes up. The wider range adds direct-forming square, API, H-beam, slitting, cold-forming and spray lines.
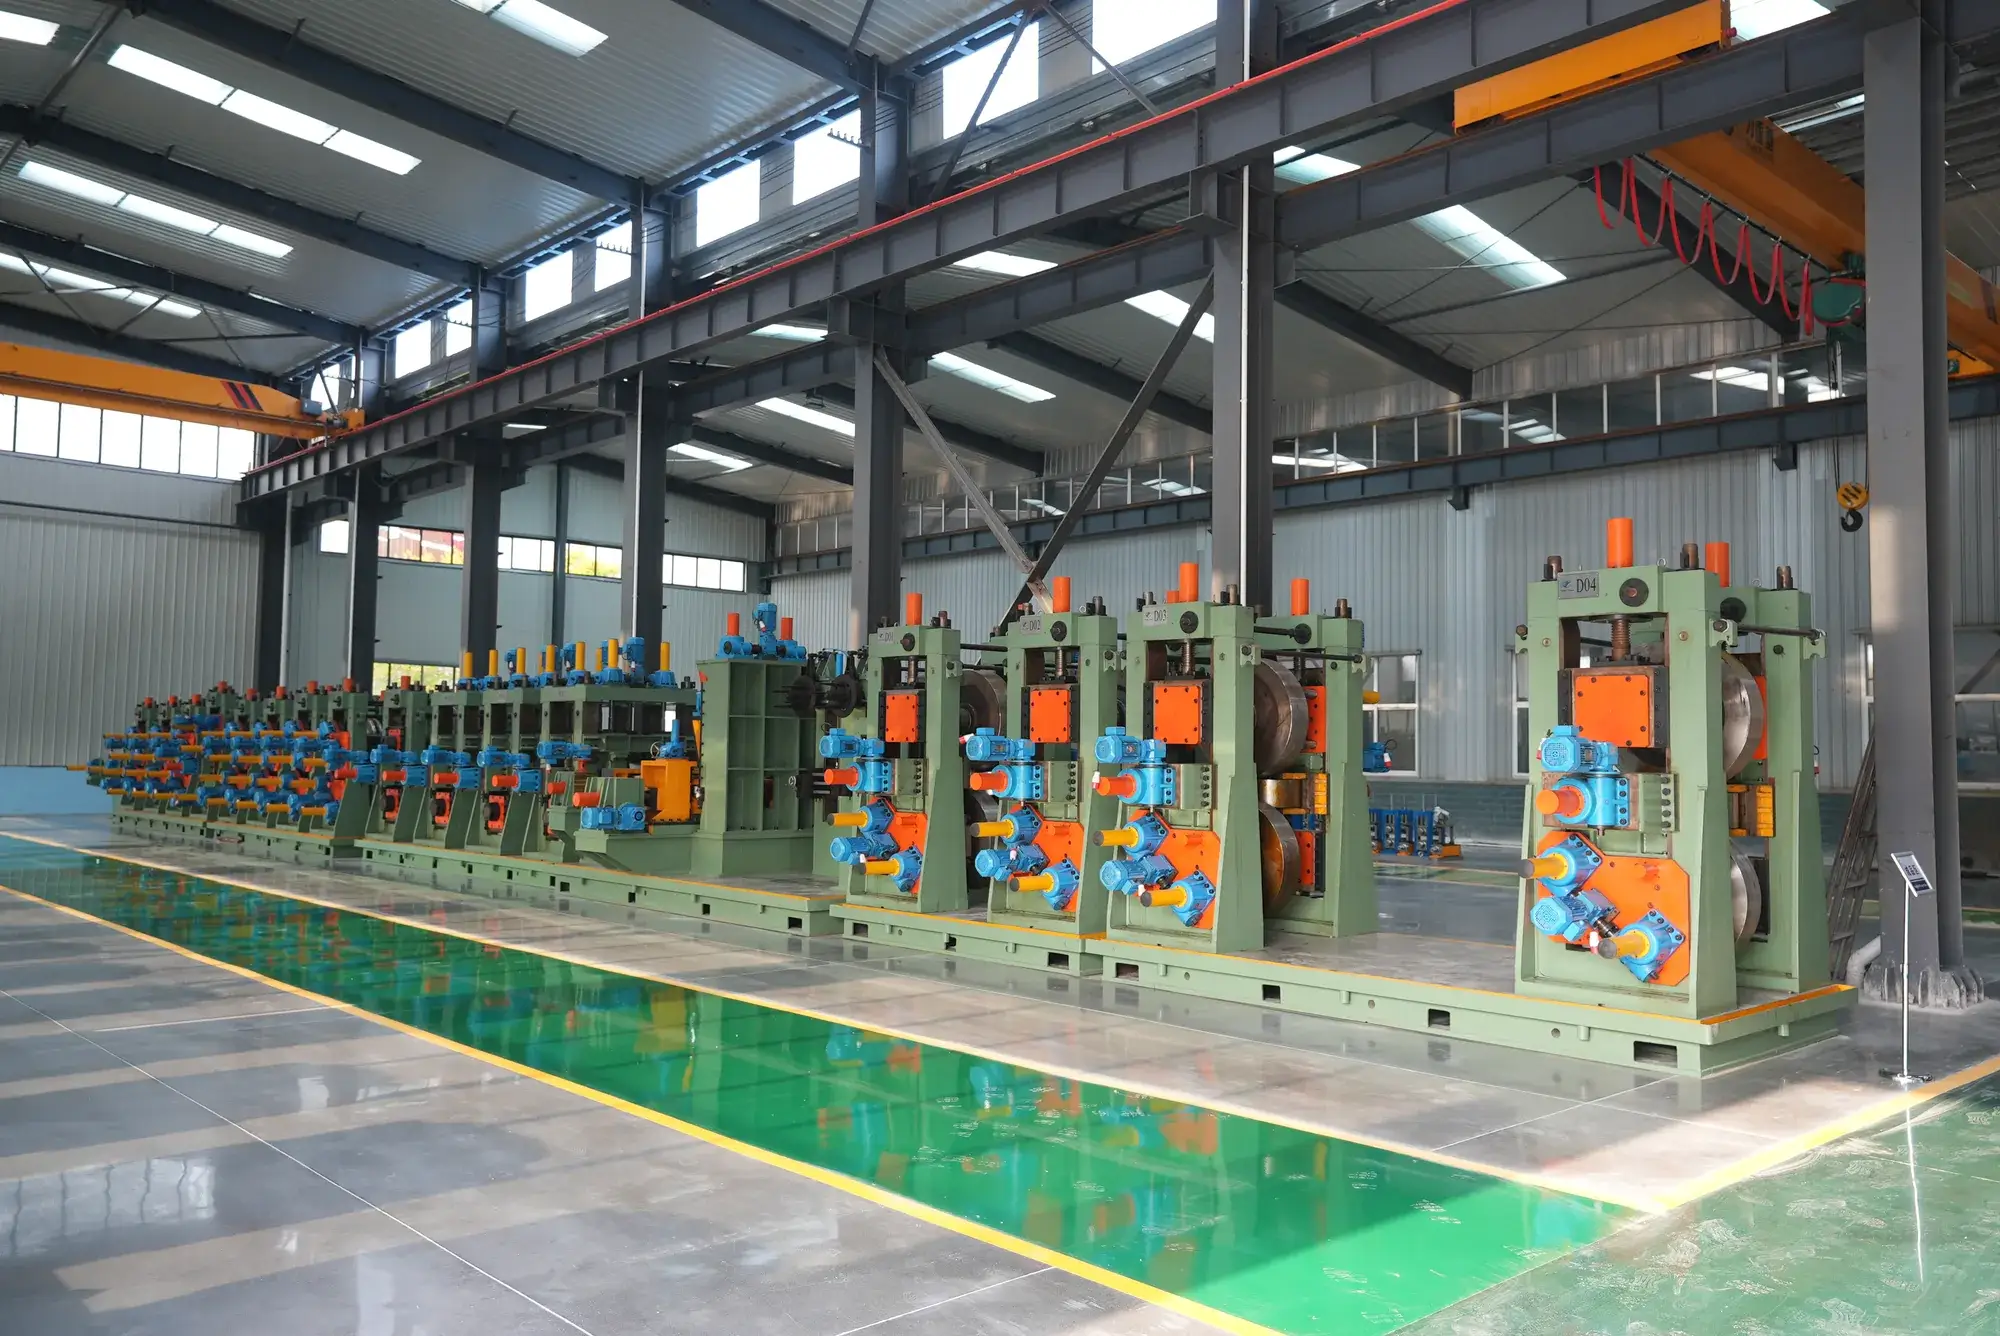
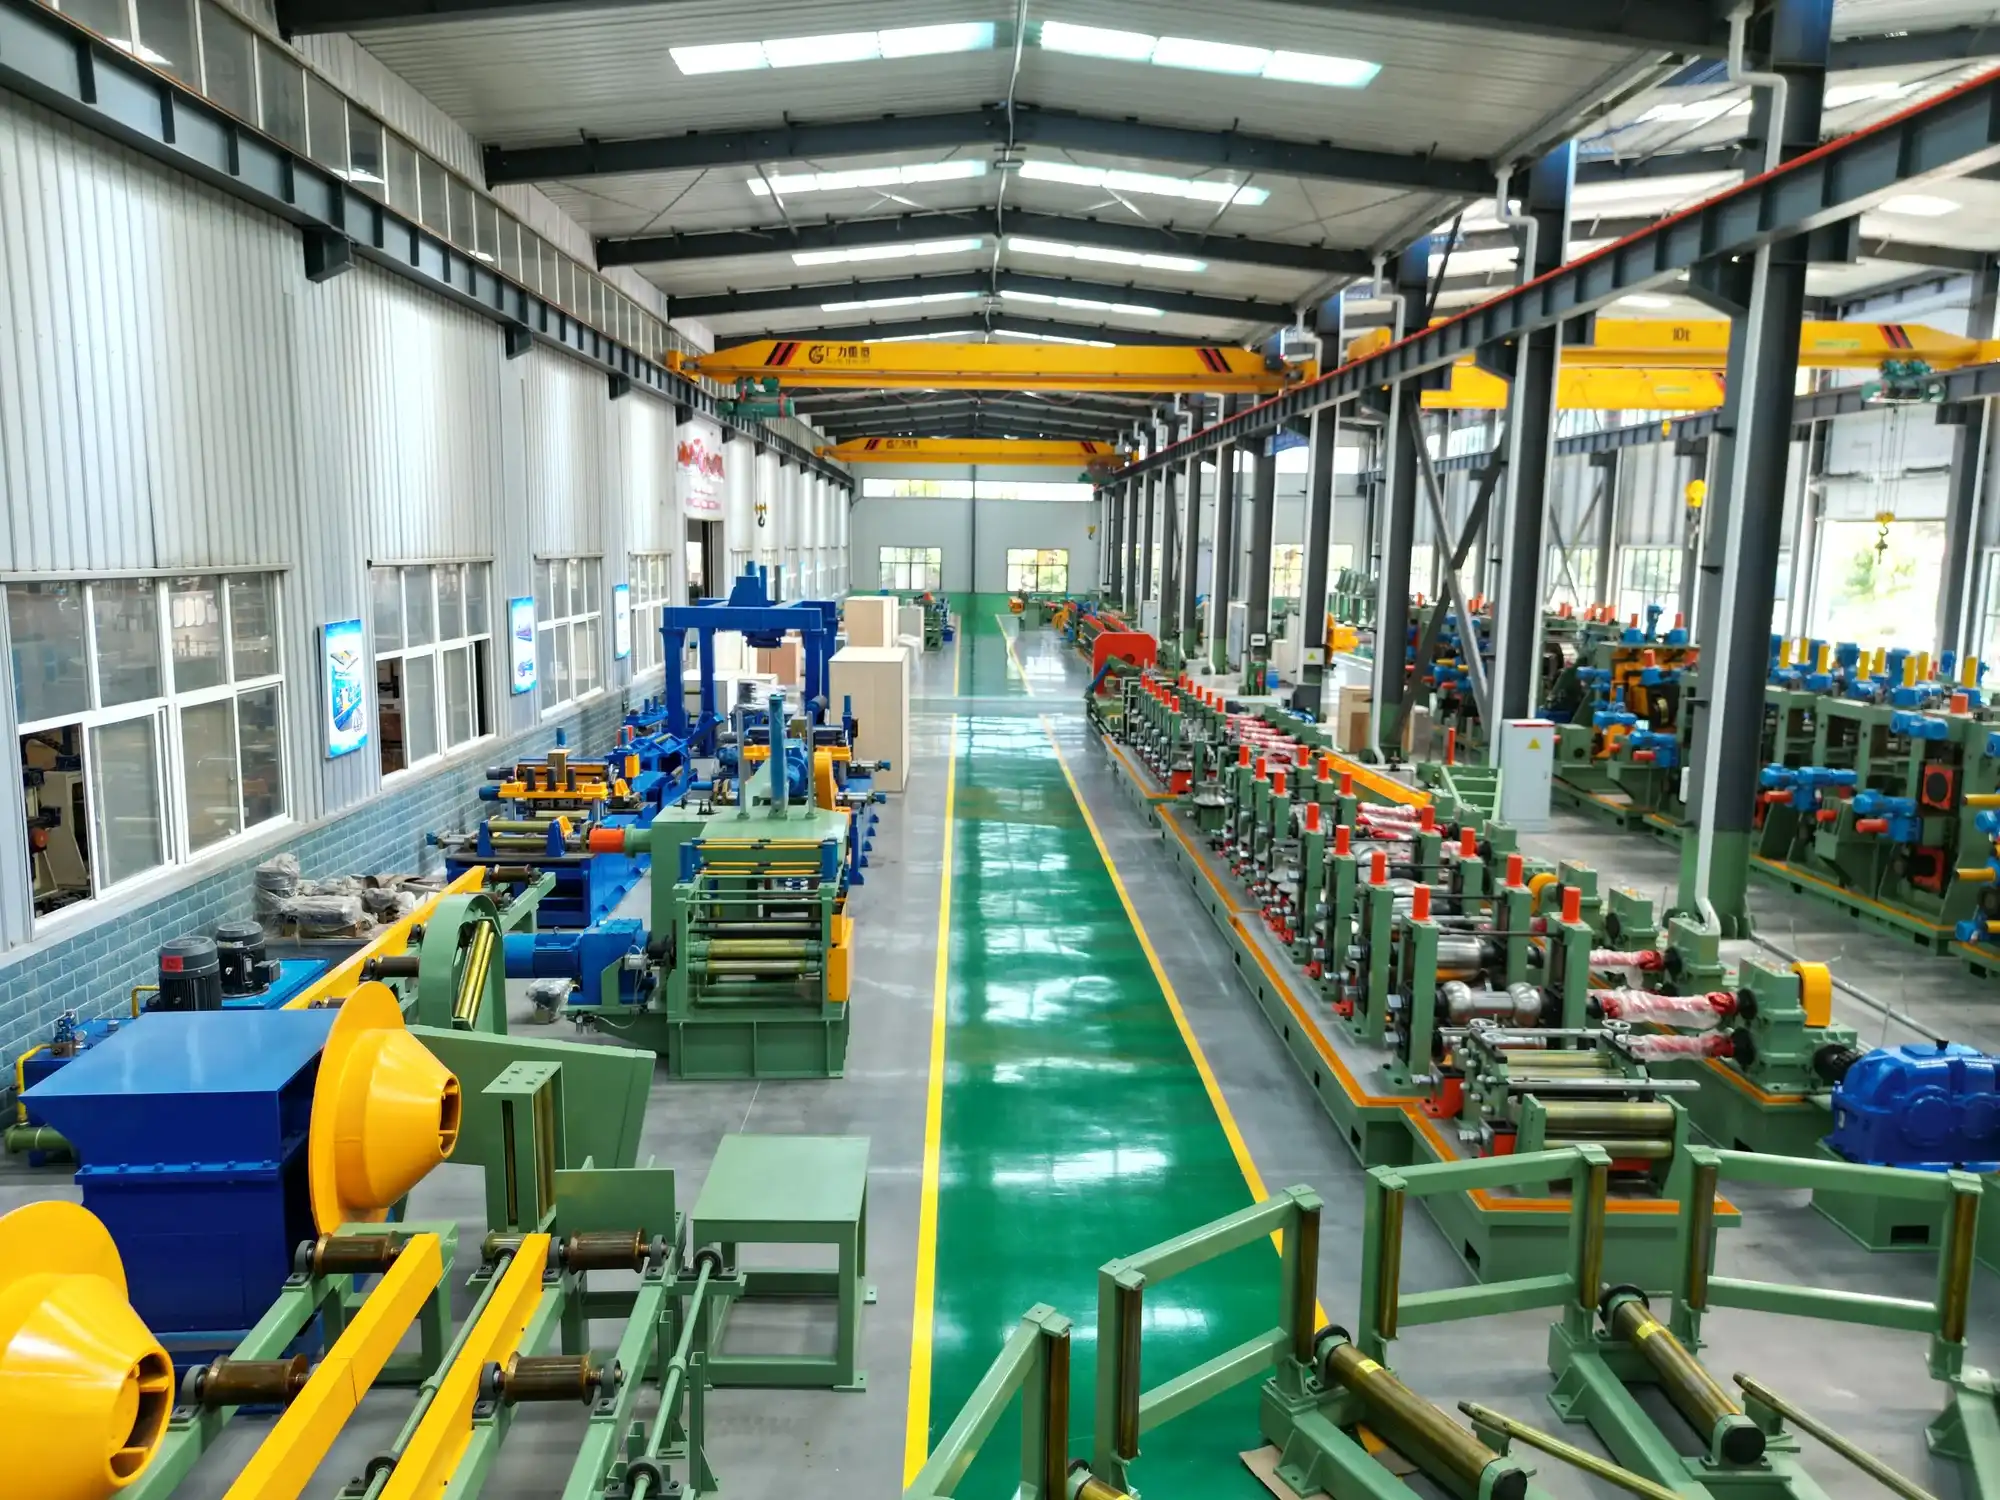
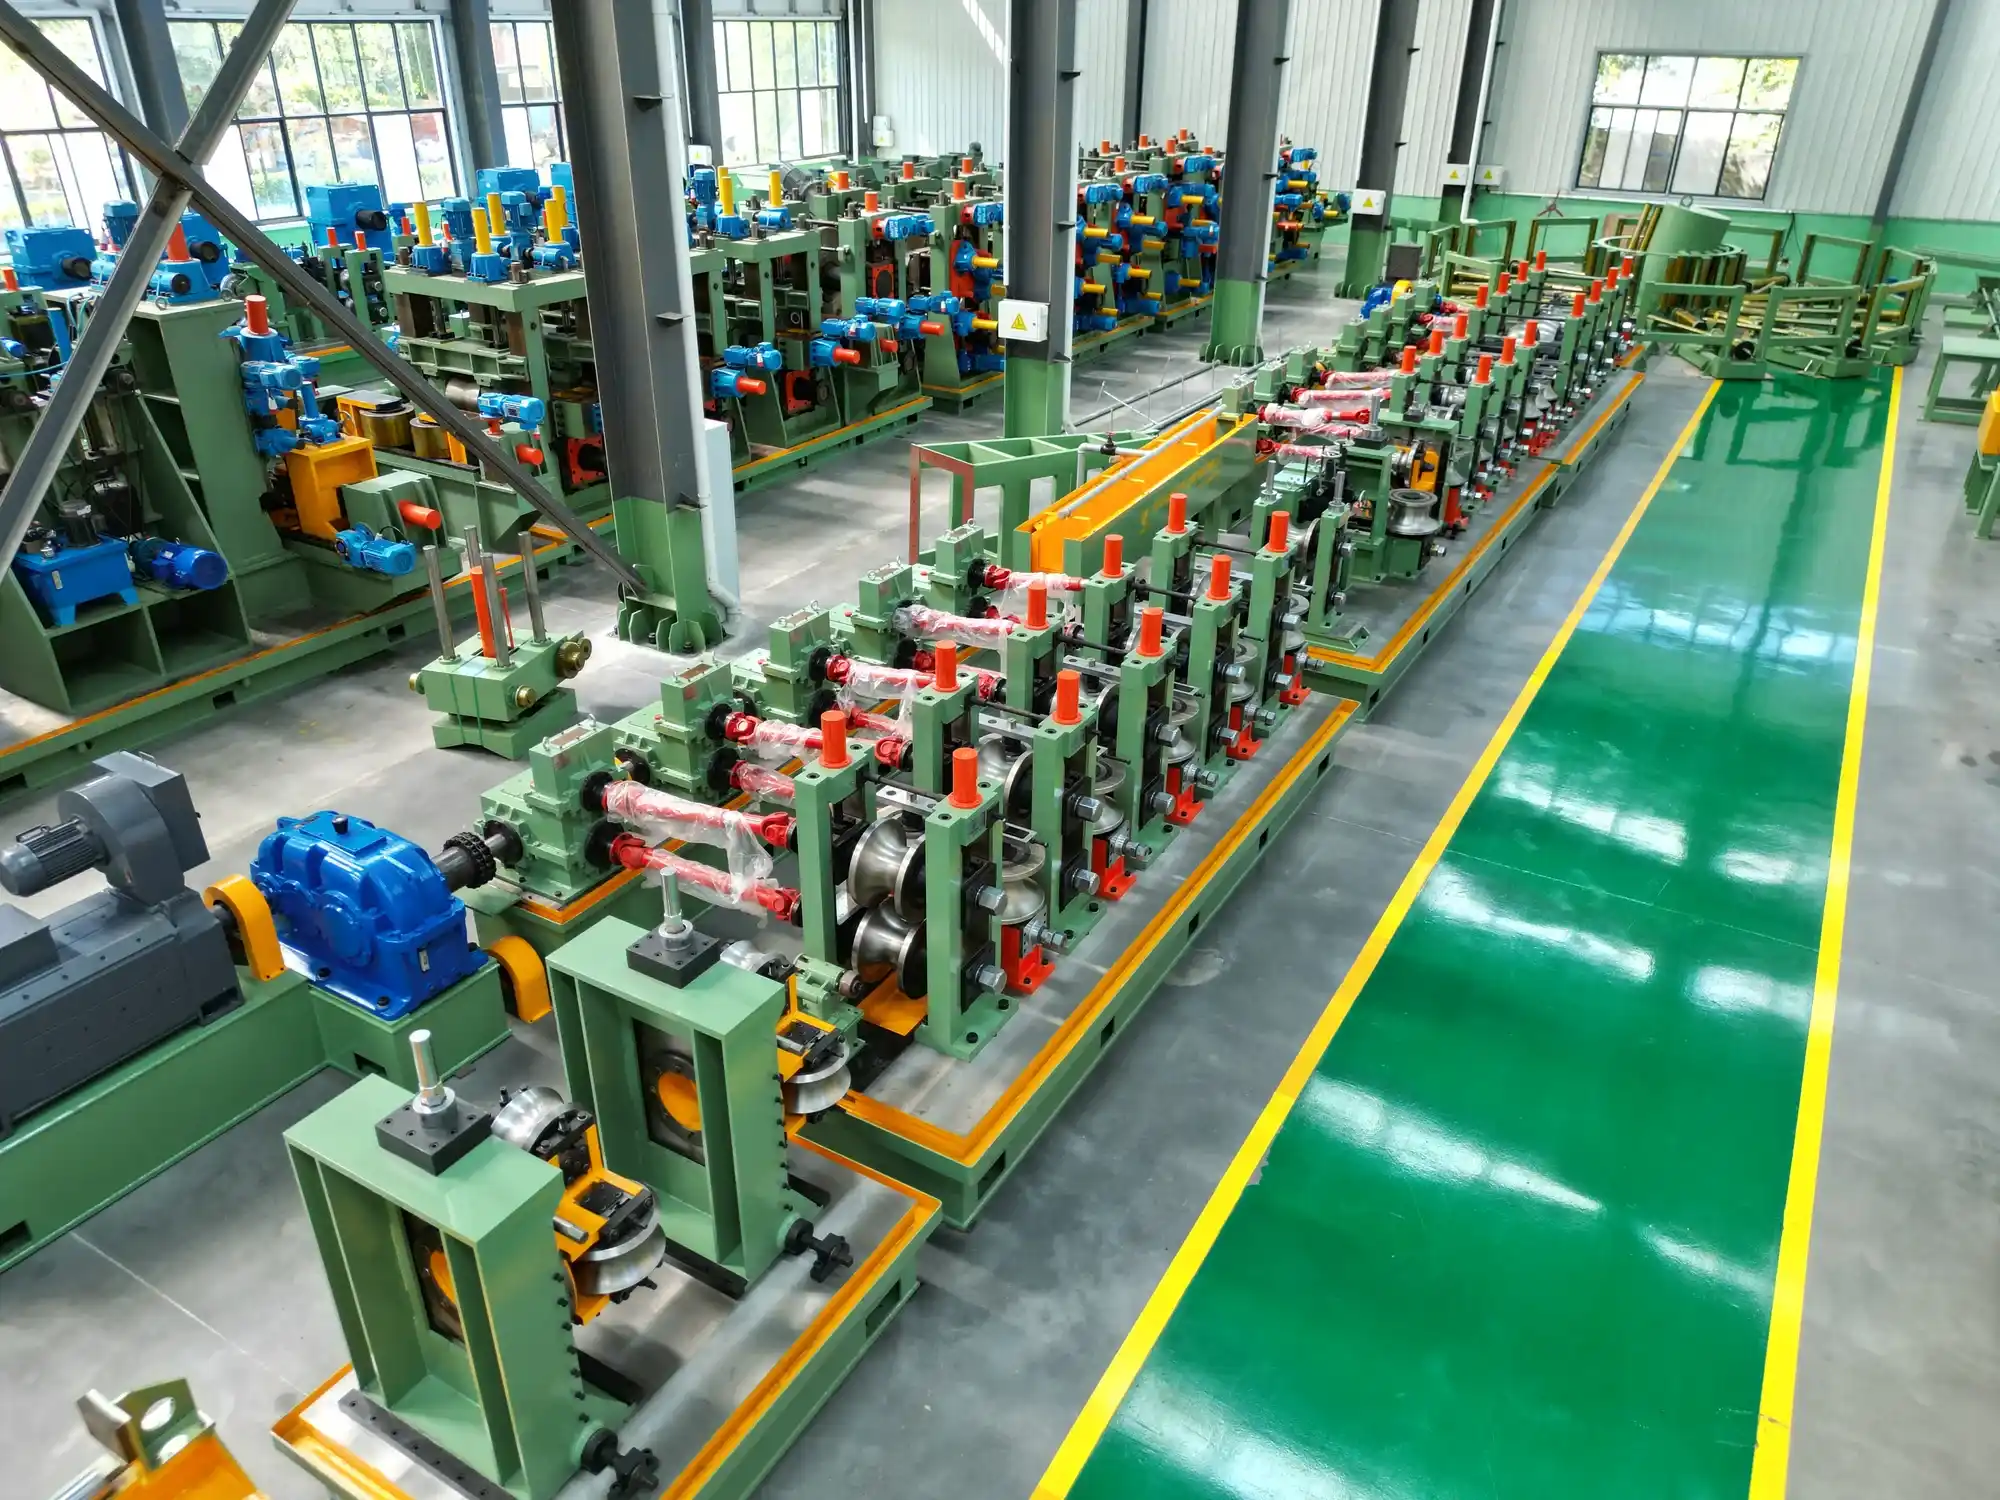
From the Workshop
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.