
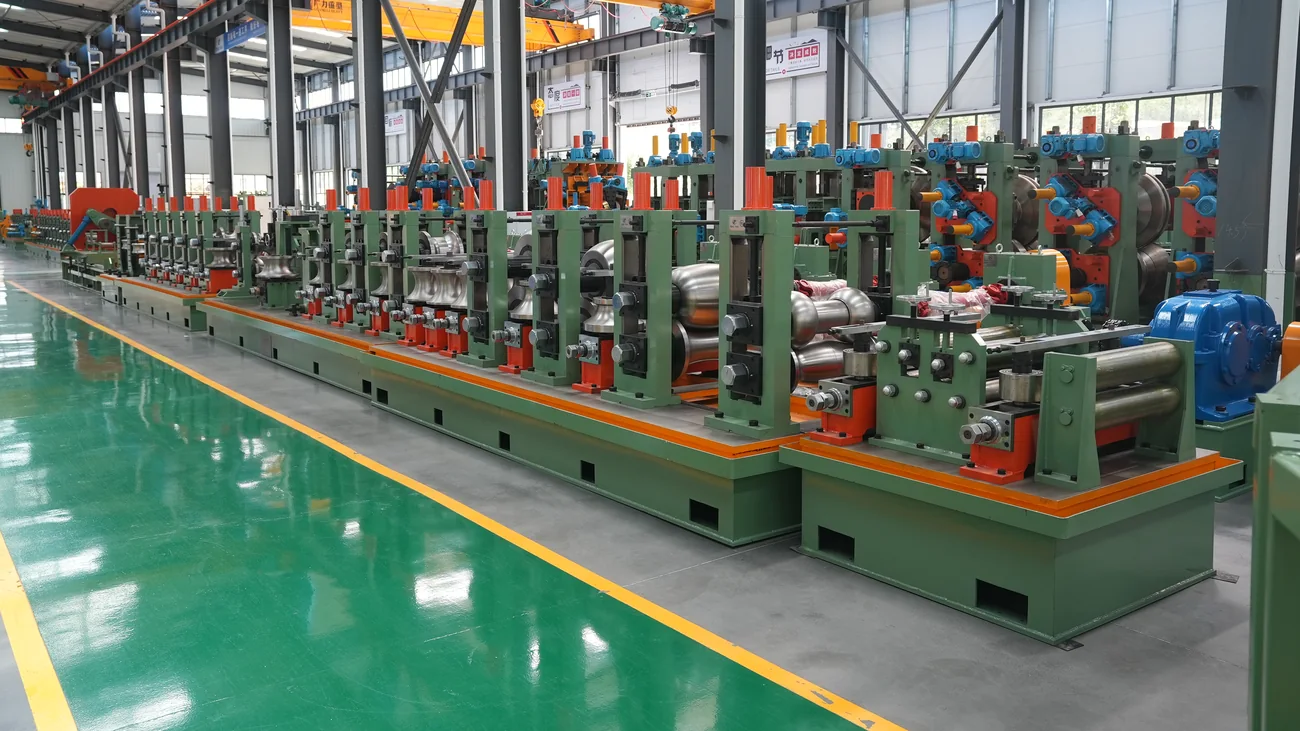
Tengtian’s video library shows 23 production lines running, plus a company film, grouped by how a line runs, how to choose a size and power band, and what inspection looks like. The high-frequency lines in it are set out in full under the tube mill & welded pipe production line.
Watch Three Lines First
Three lines to start with: API line pipe, full-automatic square tube and spiral welded pipe.
What Is in the Library
The library answers three questions, each asked at a different stage of a project:
- Process — how a line runs end to end, from coil entry to pipe cut to length.
- Selection — how to choose a diameter class and a power band once the target product is decided.
- Inspection — what testing and acceptance look like when the finished pipe has a standard to meet, shown in the inspection and test evidence.
 Process VideosCoil entry to finished pipe, stage by stage.Watch the videos →
 Selection VideosMill types and size bands compared side by side.Watch the videos →
 Inspection VideosX-ray, hydrostatic and ultrasonic testing on the line.Watch the videos →
Process Videos — How the Line Runs
On a high-frequency line the strip passes eight stages — uncoiling, levelling on the larger sizes, shear-welding, accumulation, roll forming, high-frequency welding, sizing and straightening, and flying-saw cut-off — and each one can be watched running. A spiral submerged-arc line looks entirely different: the strip is wound helically by three-roll bending at a forming angle of 39°–80° and welded inside and out at 0.5–3 m/min. On direct forming square lines, size is changed by adjusting one combined die set rather than changing rolls, which cuts roll consumption by more than 90%. The stage-by-stage footage is in the tube mill process videos, and the written walk-through is in the welded pipe manufacturing process.
Selection Videos — Choosing Size and Power Band
High-frequency longitudinal mills cover Φ10–630 mm in twelve models, HG32 to HG630, and spiral submerged-arc mills cover Φ219–1620 mm in two classes, so selection starts with the largest outside diameter the plant intends to sell. Welder power is matched to diameter in steps, from 150 kW on the HG32 to 1500 kW on the HG630, with the models in between quoted per project. Between Φ219 and Φ630 mm both routes can make the pipe, and the choice depends on batch size, wall thickness and the standard the finished pipe has to meet. The comparison footage is in the mill selection videos.
Ask an Engineer — Talk to Our After-Sales Team →
Line Videos — 23 Production Lines and a Company Film
 HG32 HFW Pipe Mill — O.D. 10–32 mm
 HG50 HFW Pipe Mill — O.D. 16–50.8 mm
 HG76 HFW Pipe Mill — O.D. 25–76 mm
 HG89 HFW Pipe Mill — O.D. 32–89 mm
 HG114 HFW Pipe Mill — O.D. 45–114 mm
 HG165 HFW Pipe Mill — O.D. 60–165 mm
 HG219 HFW Pipe Mill — O.D. 114–219 mm
 HG273 HFW Pipe Mill — O.D. 114–273 mm
 HG325 HFW Pipe Mill — O.D. 165–325 mm
 HG426 HFW Pipe Mill — O.D. 165–426 mm
 HG508 HFW Pipe Mill — O.D. 219–508 mm
 HG630 HFW Pipe Mill — O.D. 325–630 mm
 SSAW Spiral Welded Pipe Mill — Φ219–1620 mm
 Automatic Tube Mill 150×150 mm — PLC Full-Auto
 Direct Forming Square Tube Mill 120×120 mm
 Direct Forming Square Tube Mill 150×150 mm
 Direct Forming Square Tube Mill 200×200 mm
 Direct Forming Square Tube Mill 400×400 mm
 Auto Spray Paint Line — up to 60 m/min
 Coil Slitting Line — ±0.2 mm Width
 Cut-to-Length Line — Coil to Sheet, up to 32 t
 H-Beam Production Line — GOST R 58966-2020
 API Line Pipe Mill — Φ114–508 mm
 Company Film — Hebei Tengtian
View the full channel on YouTube →
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.