
In This Line
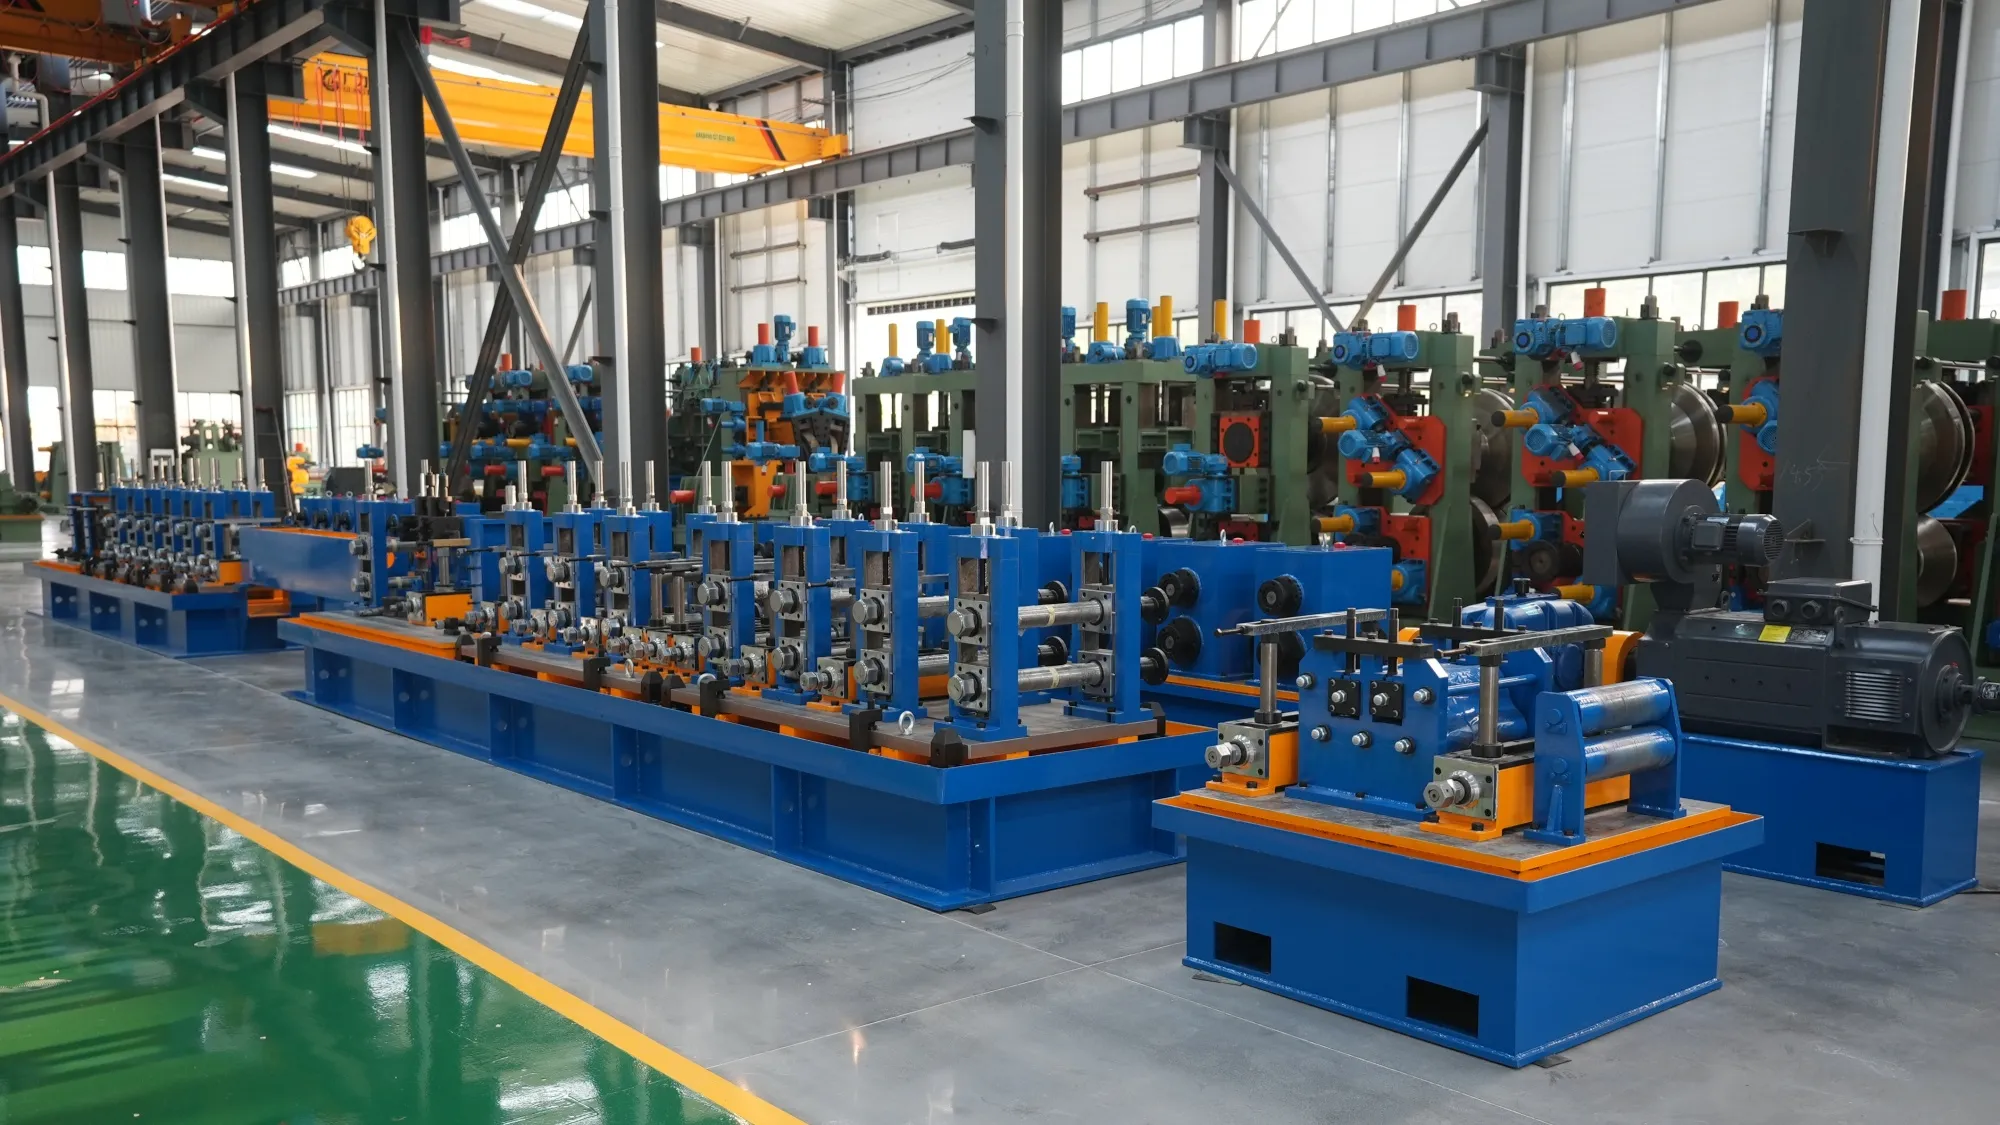
Tengtian’s HG range covers twelve bands from HG32 to HG630, producing Φ10 to Φ630 mm outside diameter at 0.5 to 16 mm wall.
What the Line Is, and What It Can Make
- The line is a continuous forming–welding–sizing set: uncoil, form, HF induction weld, size, cut.
- Twelve bands, HG32 to HG630.
- Output range: Φ10 to Φ630 mm OD, 0.5 to 16 mm wall.
- Welder power is matched to pipe diameter across the range 150 to 1500 kW.
- Forming and sizing rolls are the first determining component of pipe quality.
- Material yield can reach 93% or more on some high-end lines; achieved yield also depends on operating practice.
What Is an ERW Tube Mill
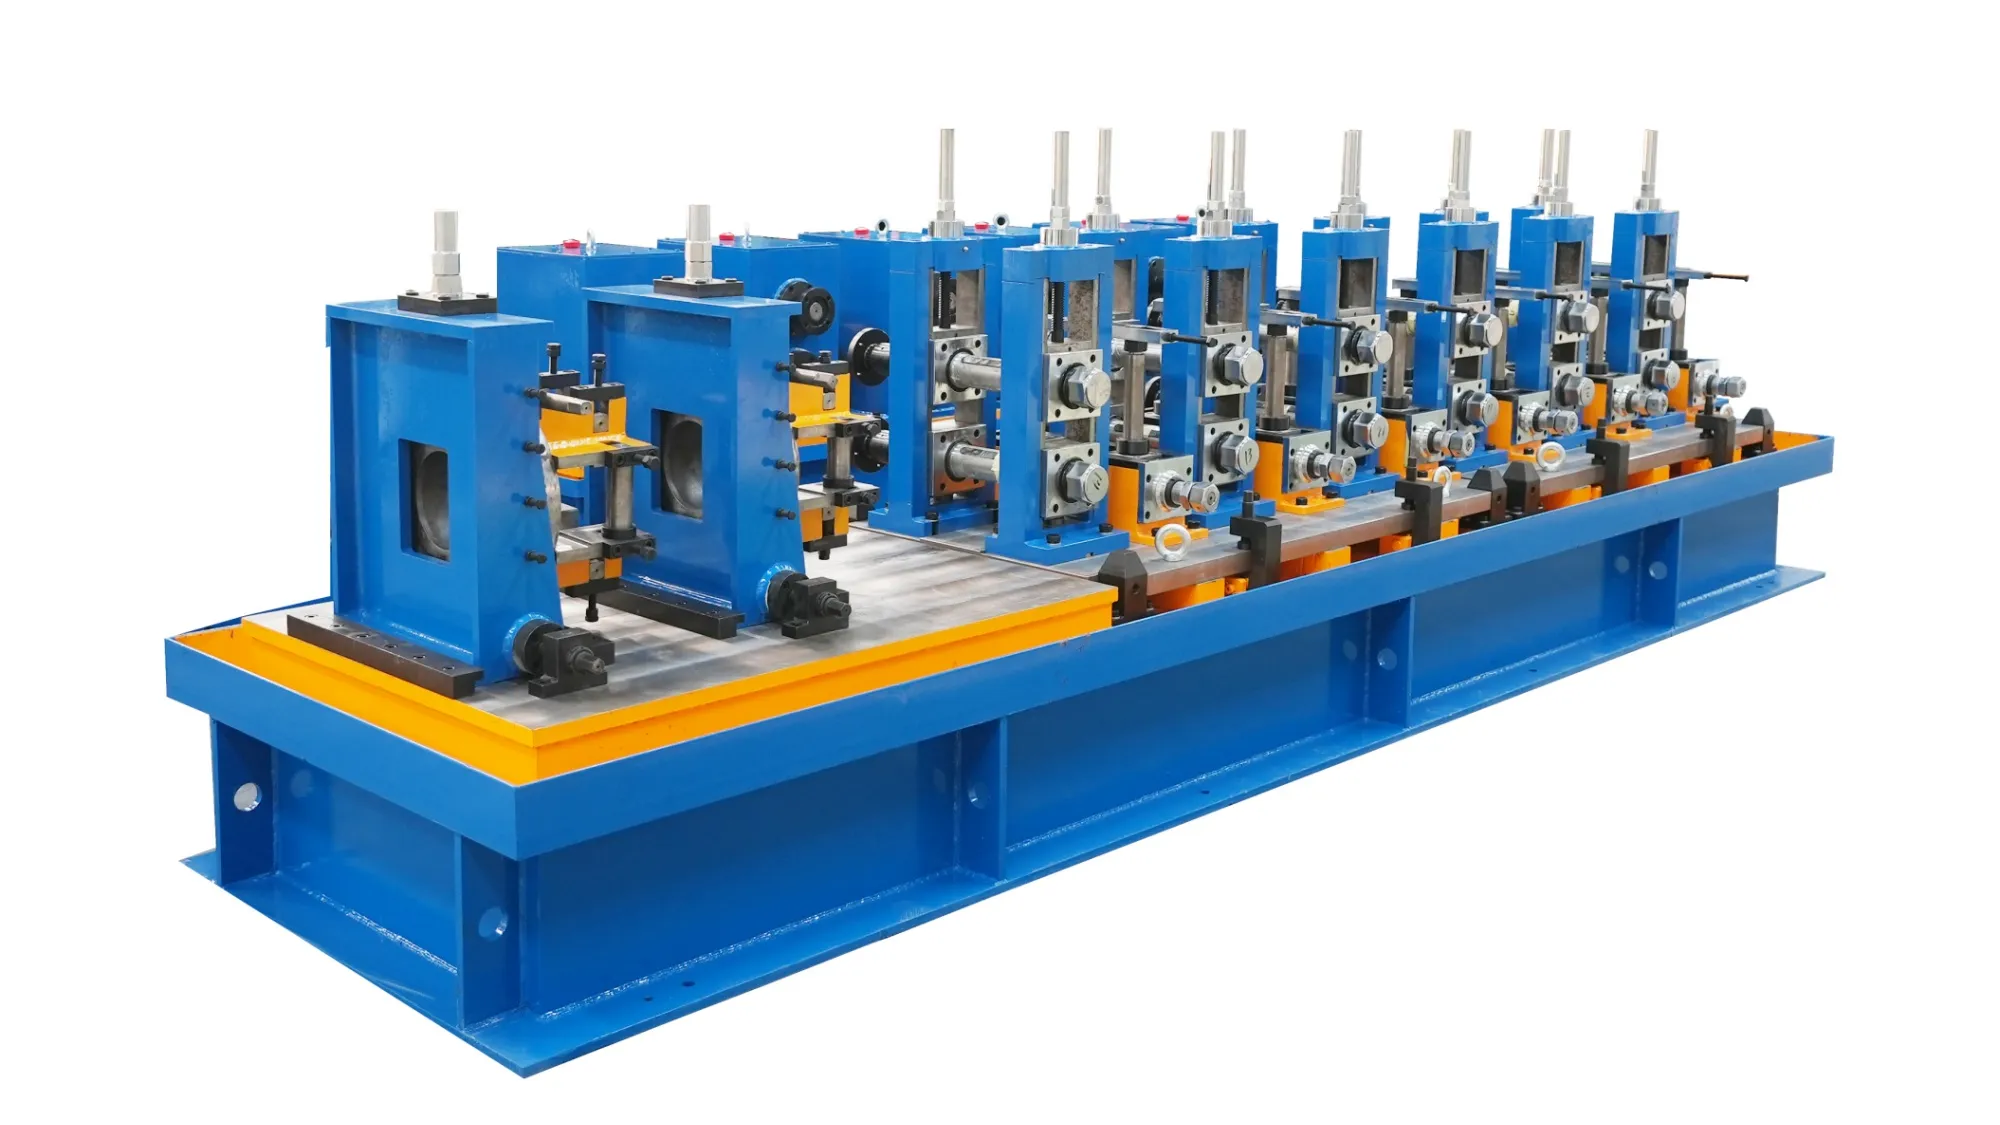
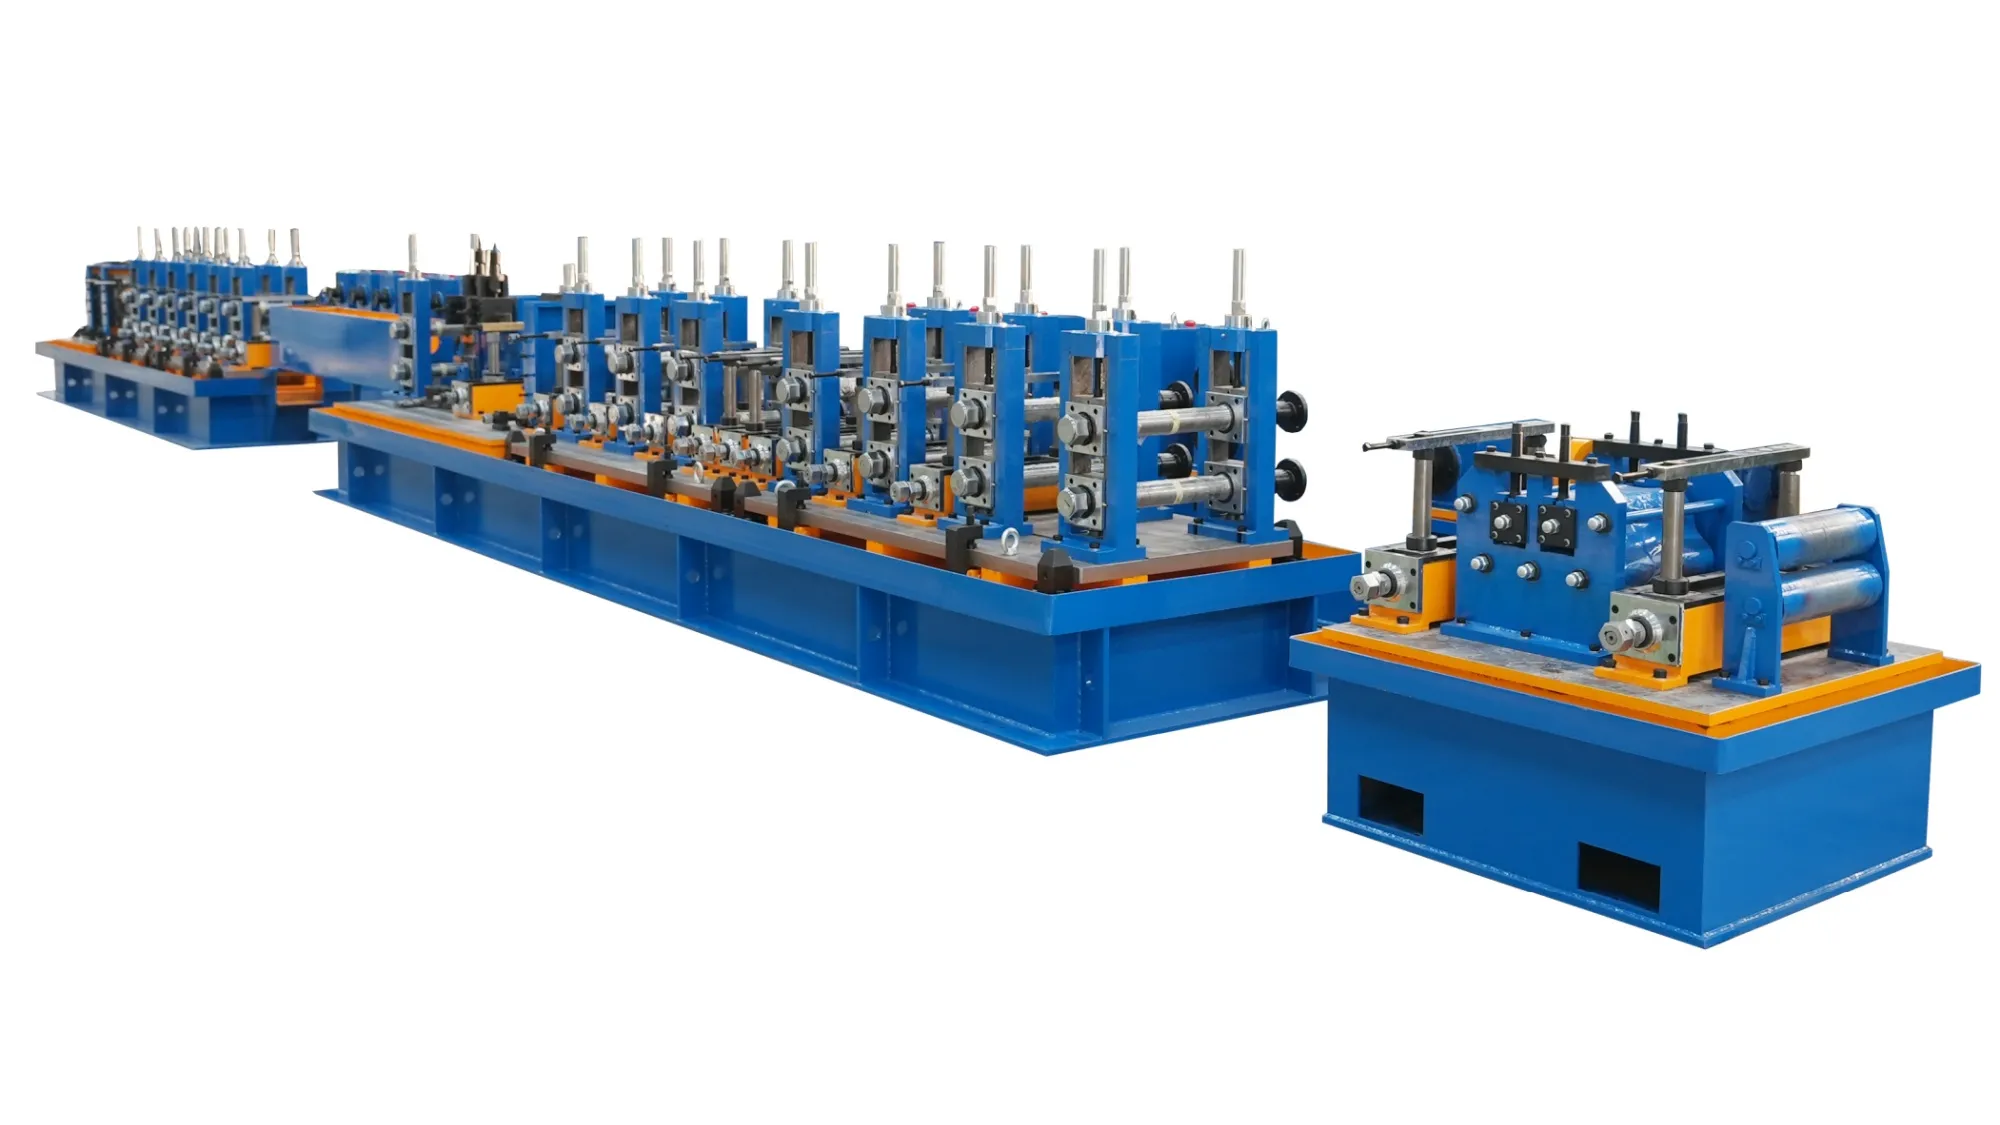
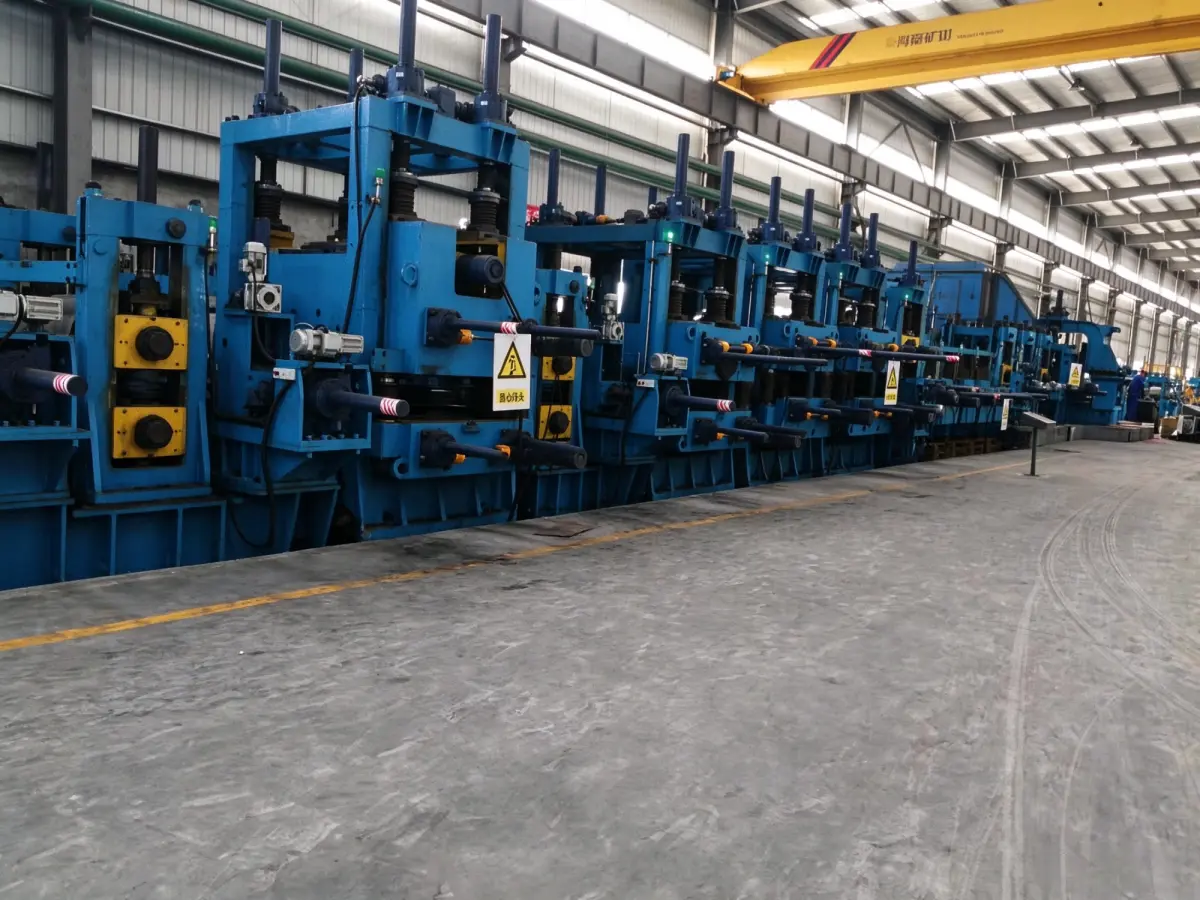
An ERW tube mill — electric resistance welded, and in this range specifically high-frequency induction welded, which is why it is also called an HF tube mill — is a complete continuous set of equipment that converts steel coil into straight-seam welded pipe.
An ERW tube mill is bought for capacity rather than a single product: it gives a downstream pipe mill continuous production capability, converting strip into standard straight-seam welded pipe for fluid transport, building structures, machinery and furniture applications.
What is an ERW tube mill used for
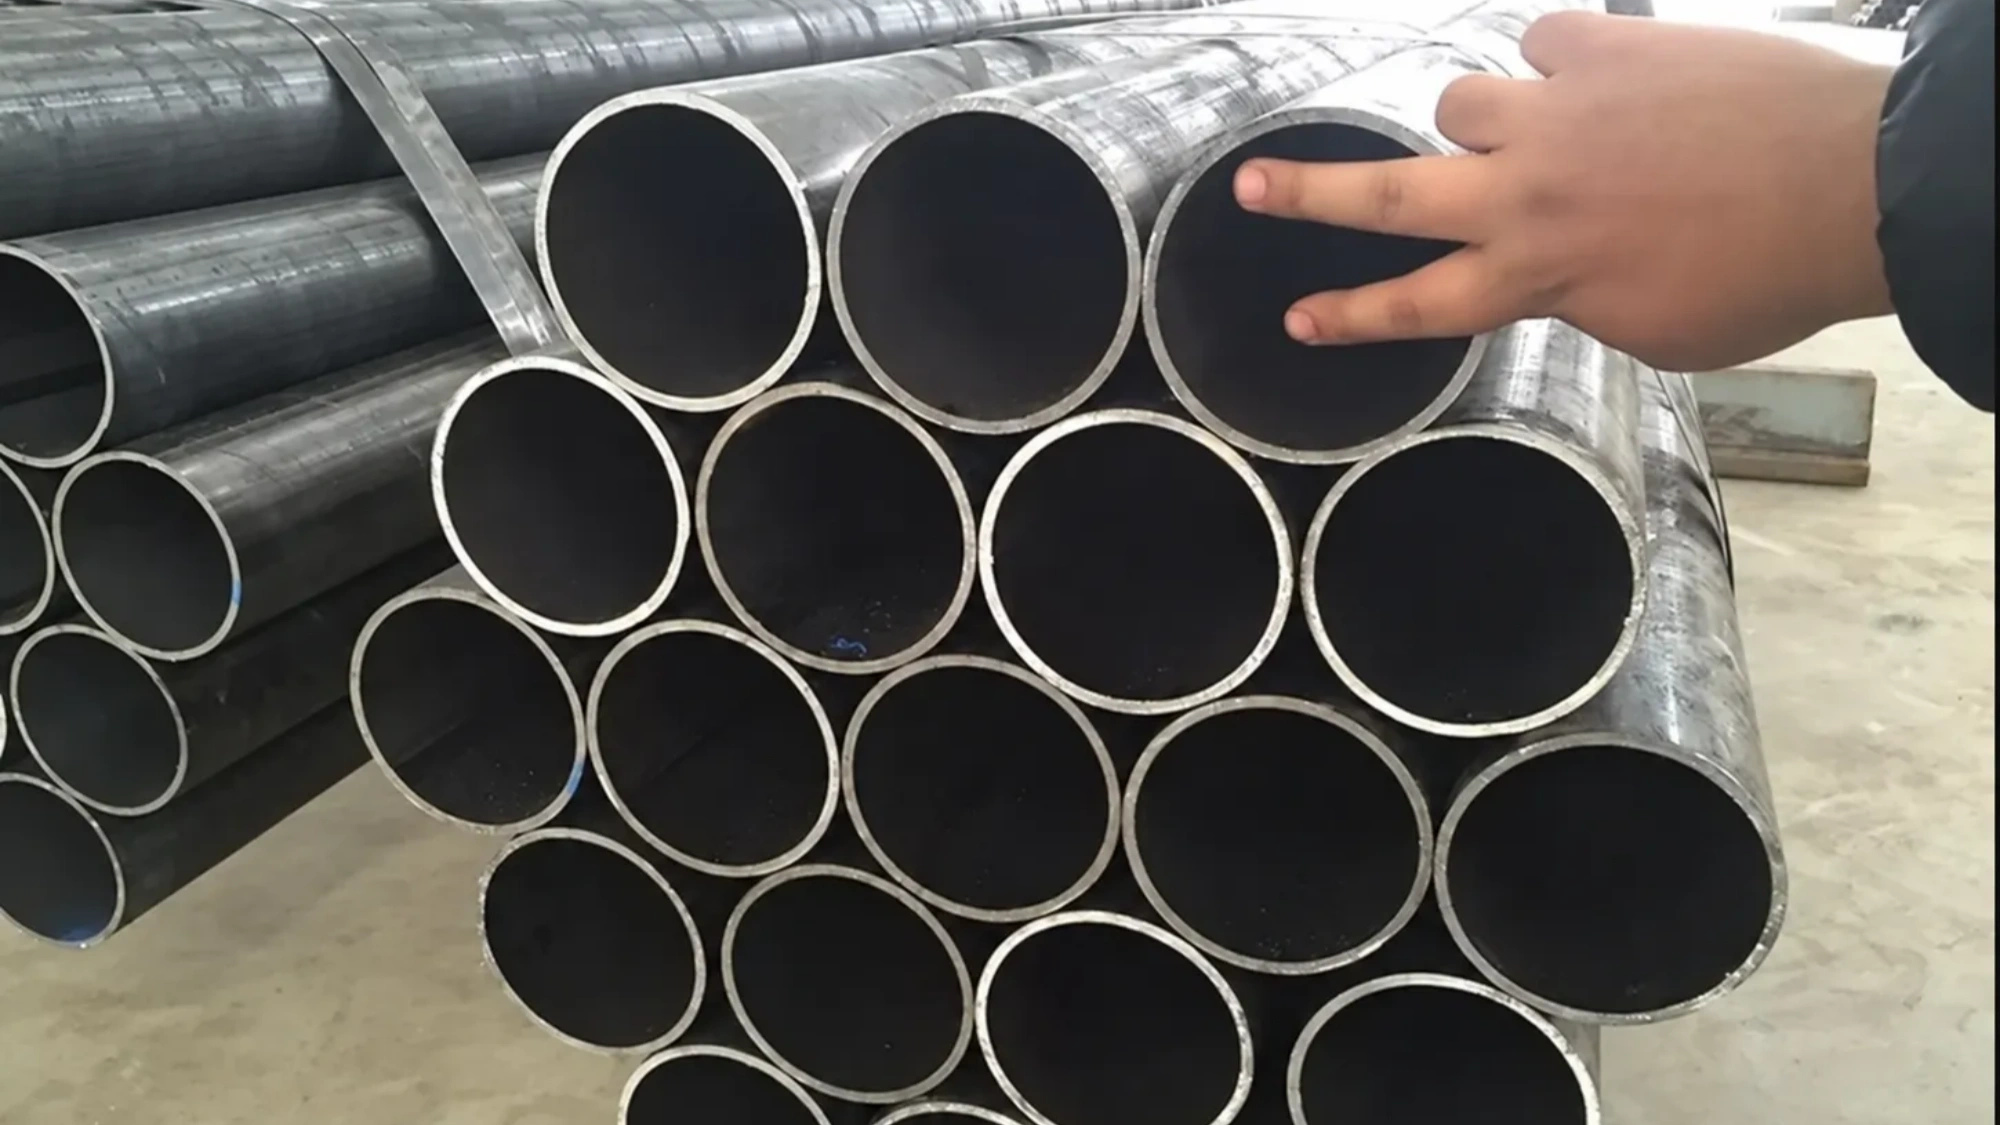
The application that carries the most detail is fluid transport pipe. Pipe mills run the HG line continuously as a carbon steel welded pipe production line for oil and gas transmission, urban water supply and drainage, gas distribution, and chemical and heating pipework.
Pipe mills serving that market need continuous, stable output, reliable weld seams, high material yield, and coverage of multiple wall thicknesses and diameters.
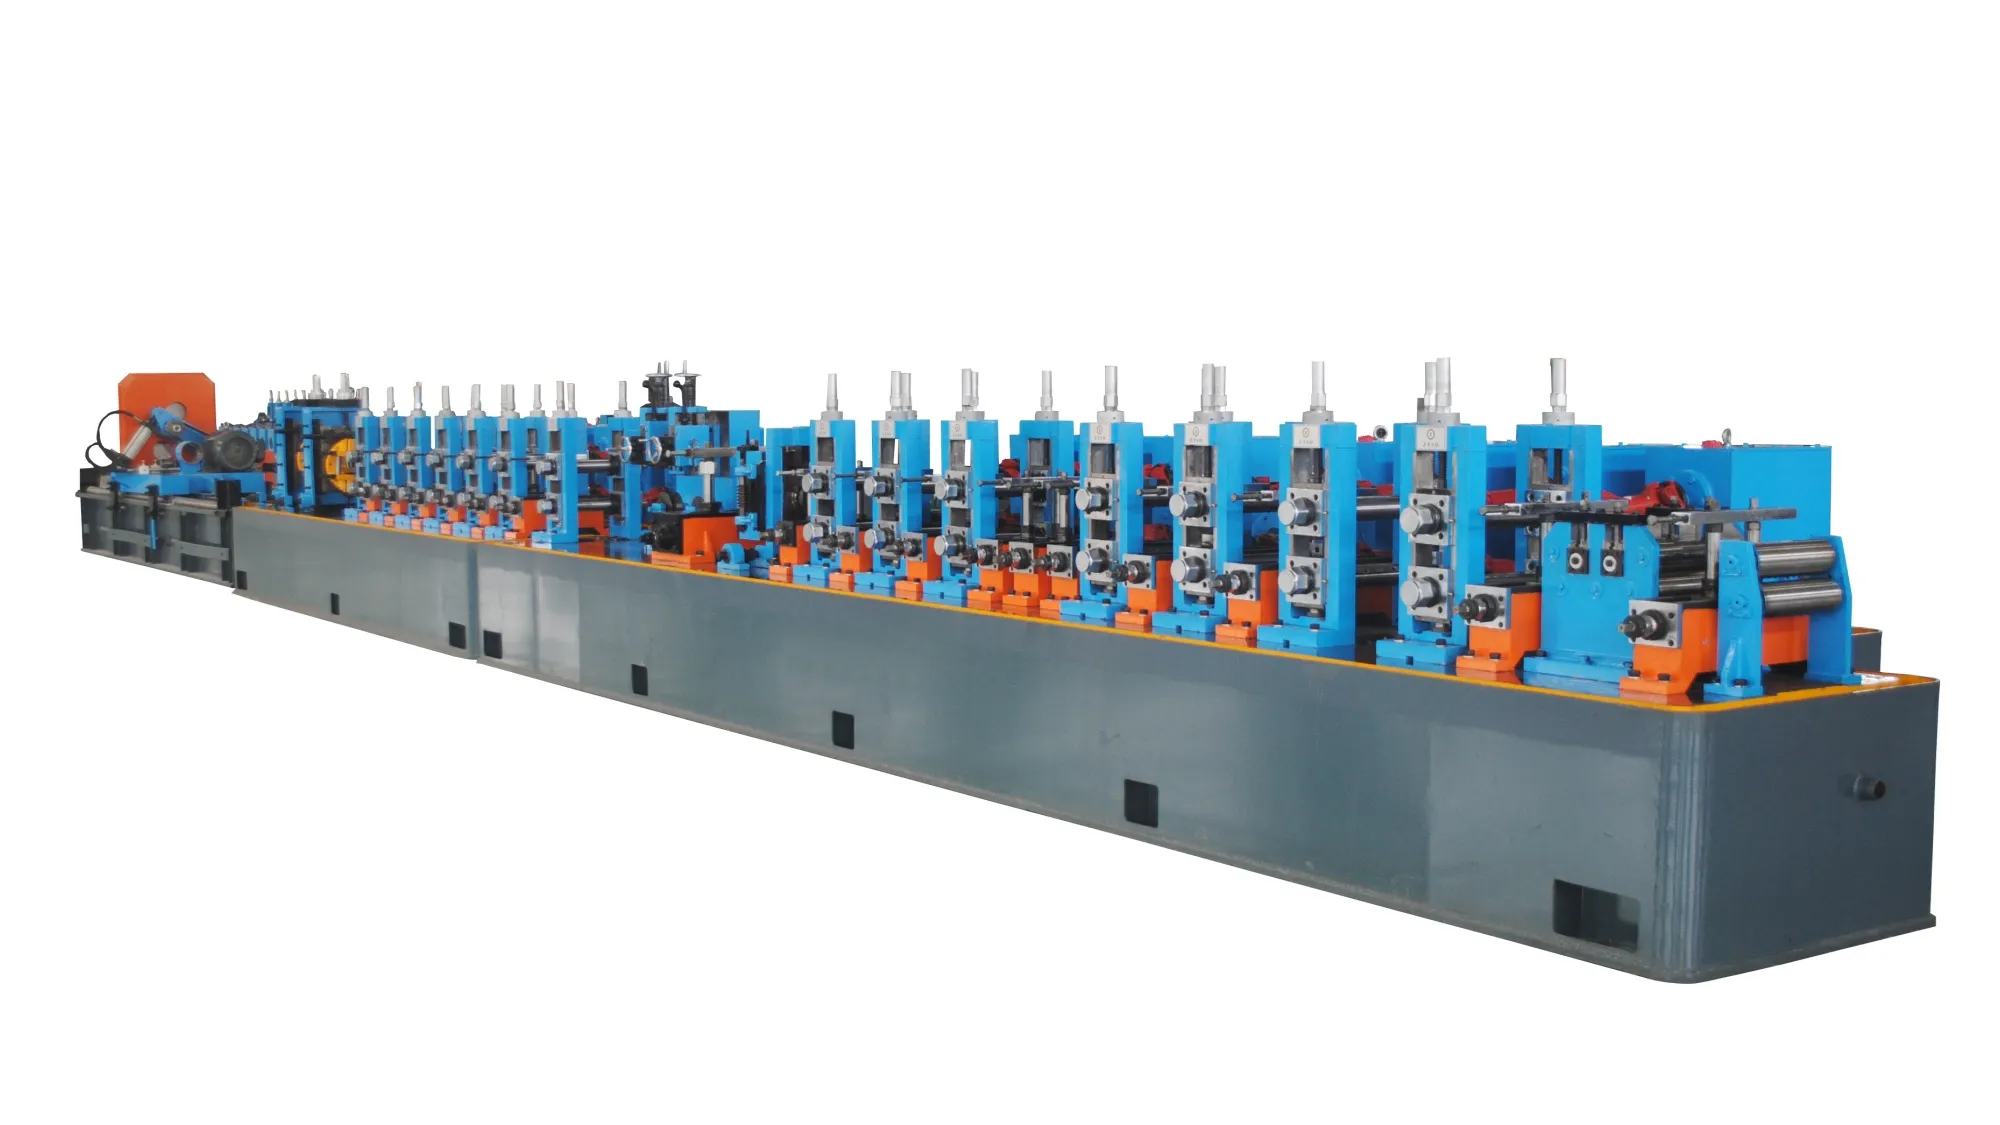
The process chain is uncoiling, roll forming, high-frequency induction welding, sizing, and cutting, producing round or square and rectangular section pipe without adding filler metal.
ERW Tube Mill Bands, Diameter Windows and Welder Power
Selection is driven first by finished pipe diameter, and the twelve bands have these diameter windows: Φ10–32, 16–50.8, 25–76, 32–89, 45–114, 60–165, 114–219, 114–273, 165–325, 165–426, 219–508 and 325–630 mm, corresponding to HG32 through HG630.
Across the whole family the envelope is Φ10 to Φ630 mm outside diameter at 0.5 to 16 mm wall.
Welder power is matched to pipe diameter, from 150 kW on HG32 to 1500 kW on HG630: HG32 150 kW · HG50 200 kW · HG76 250 kW · HG89 300 kW · HG114 300 kW · HG165 400 kW · HG219 500 kW · HG273 600 kW · HG325 600 kW · HG426 800 kW · HG508 1000 kW · HG630 1500 kW.
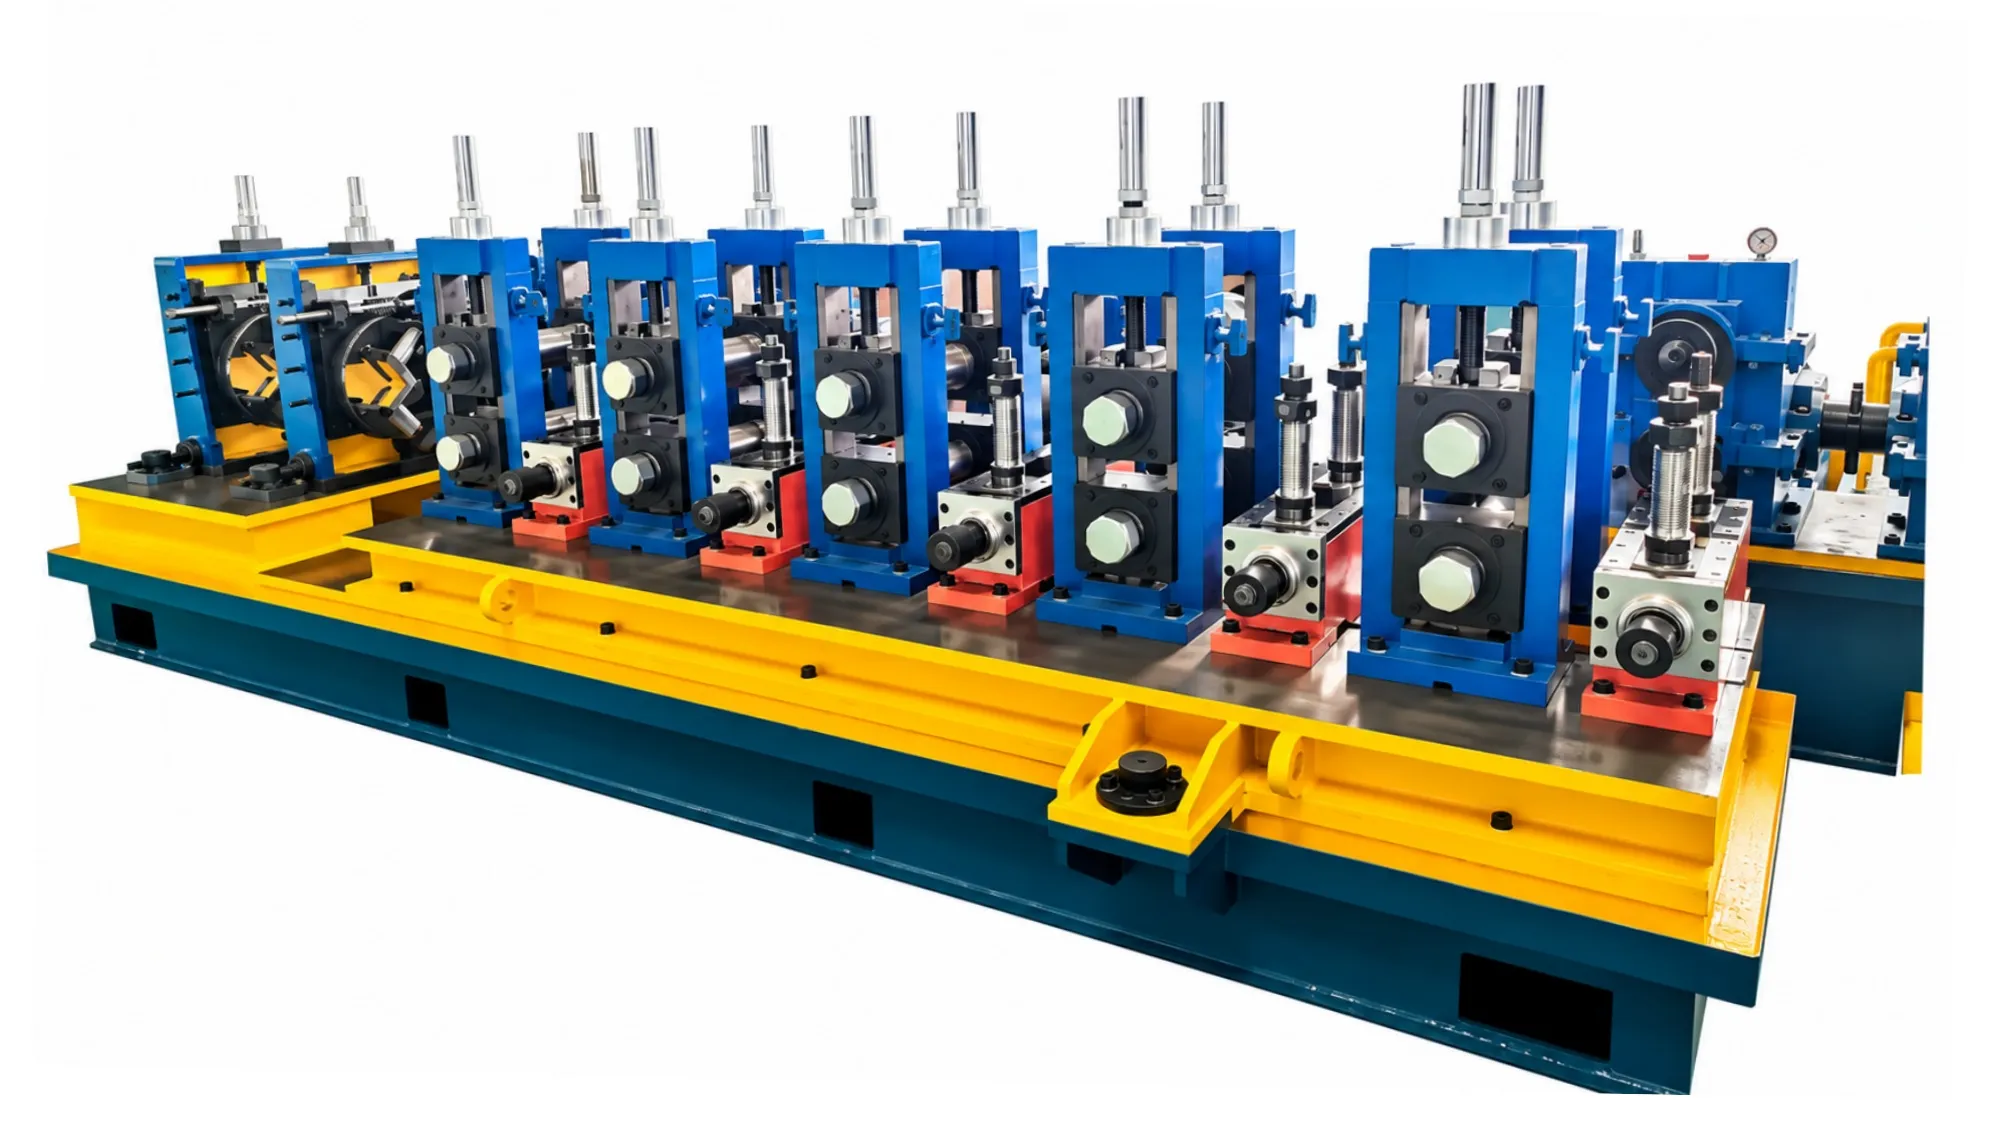
ERW Pipe Mill Line: Rolls, Induction Coil and Impeder
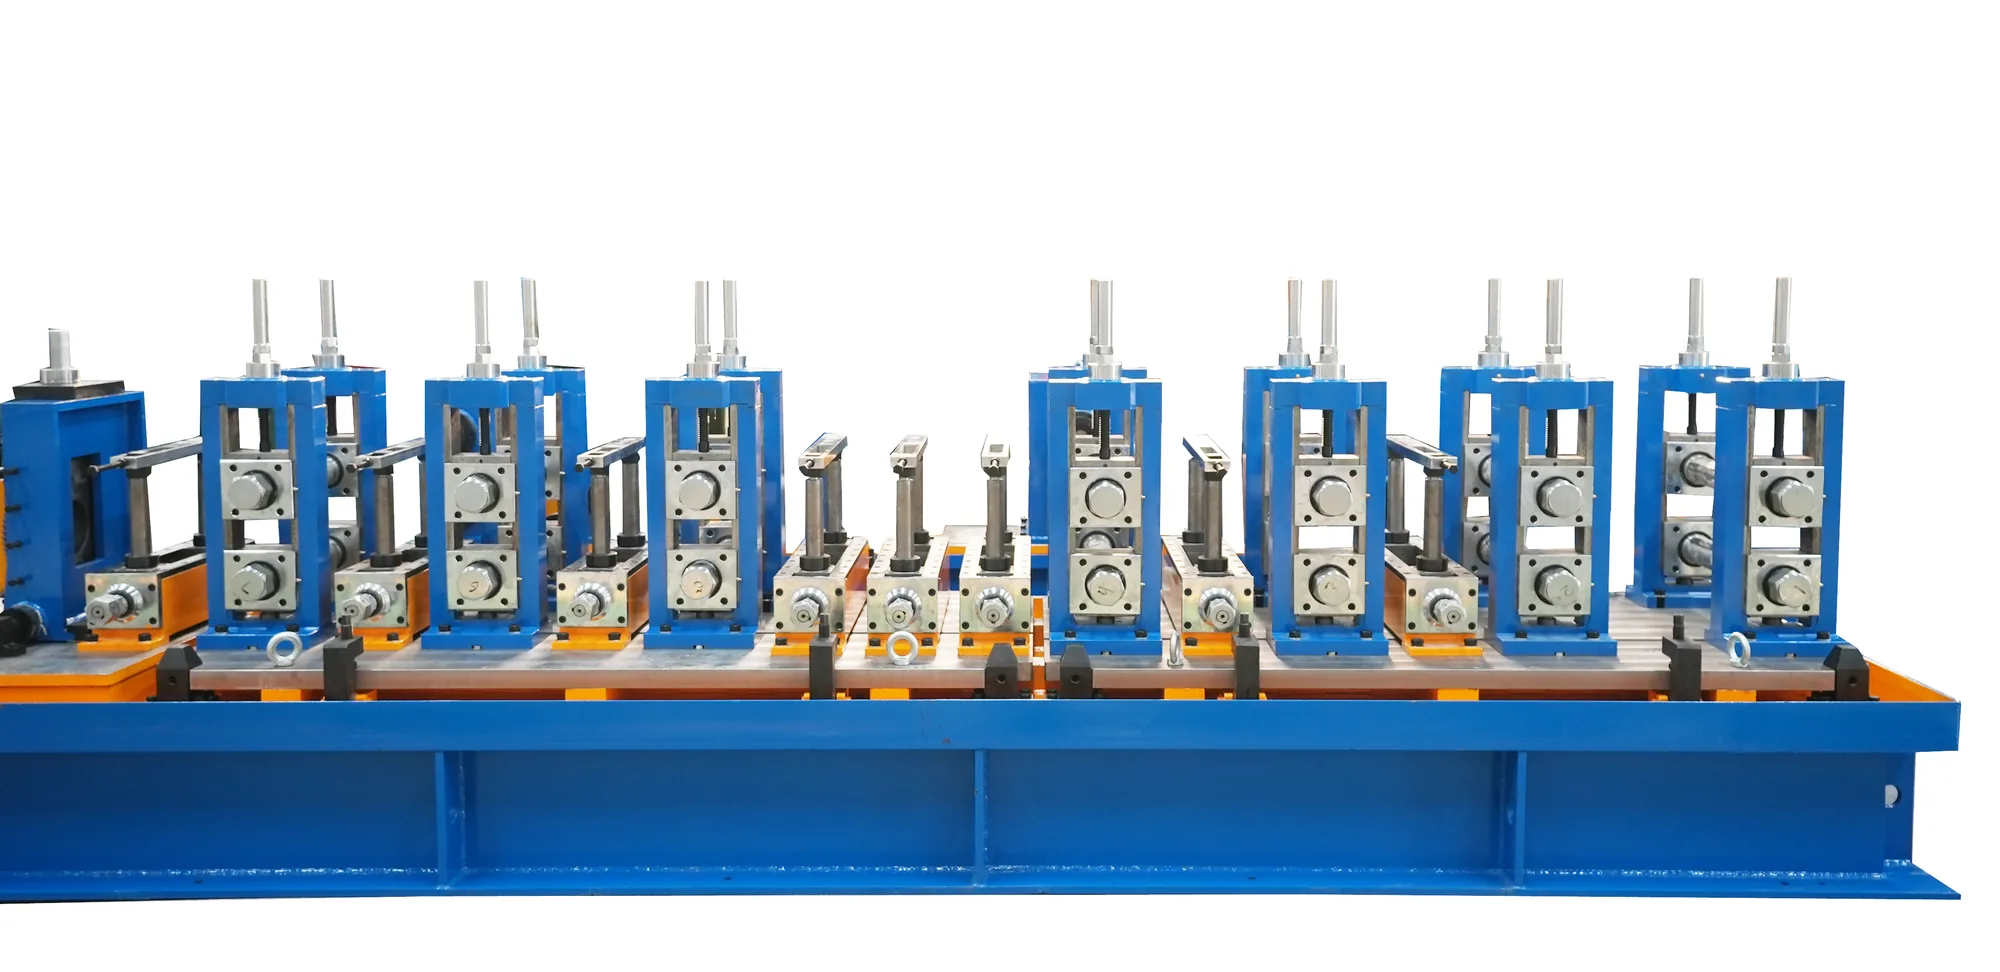
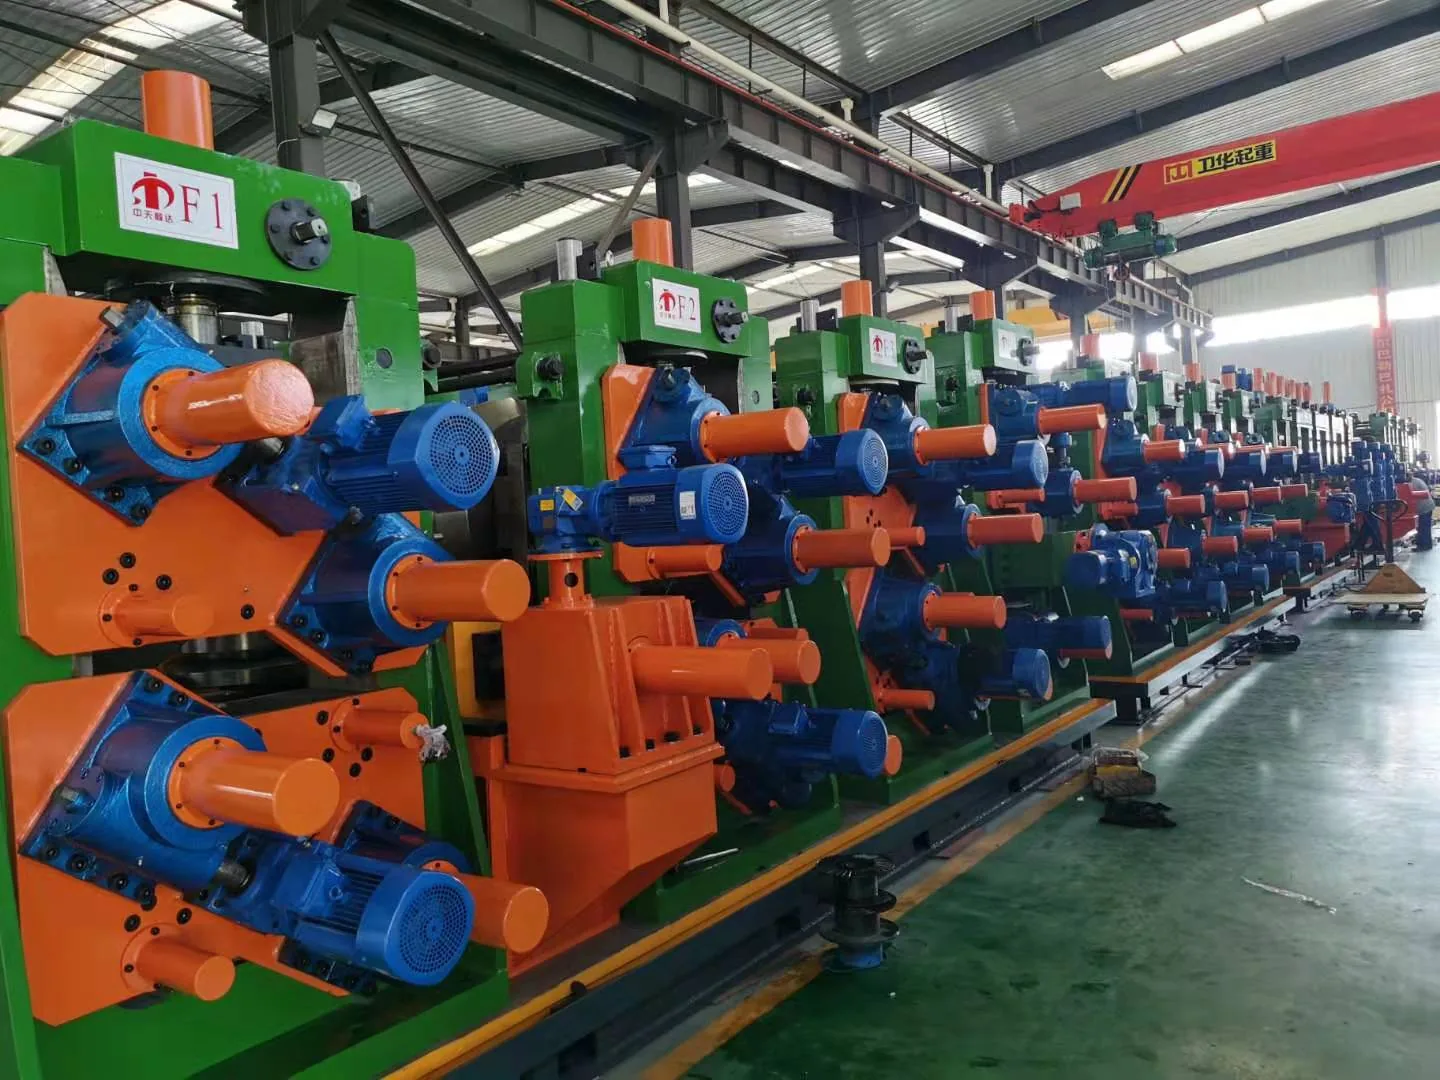
The roll set is the key component for forming and sizing.
The welding side has its own key component. The induction coil and impeder concentrate high-frequency current at the weld seam through skin and proximity effects, and they directly affect welding thermal efficiency and weld quality; when they wear out, welding energy disperses, weld quality fluctuates and energy consumption rises. They are wear parts with continuing supply.
Forming and sizing rolls directly determine pipe shape accuracy, roundness or squareness, corner-line appearance and dimensional consistency, and are the primary determinant of tube quality; the failure mode when roll material or heat treatment falls short is early wear, diameter drift, an uneven corner line and frequent roll dressing at size changes.
Related Standards
Tengtian’s other pipe lines are built to named product standards: for the spiral family, GB/T 9711 on both bands, plus GB/T 5037 on the 820 band and API 5L on the 1620 band; API 5L for the API line pipe family; and GOST R 58966-2020 for the H-beam line.
At enterprise level, Q/GYL TT01-2023 covering HGF150 high-frequency welded pipe equipment was issued on 31 August 2023 and took effect on 15 September 2023.
Step-by-Step Procedure
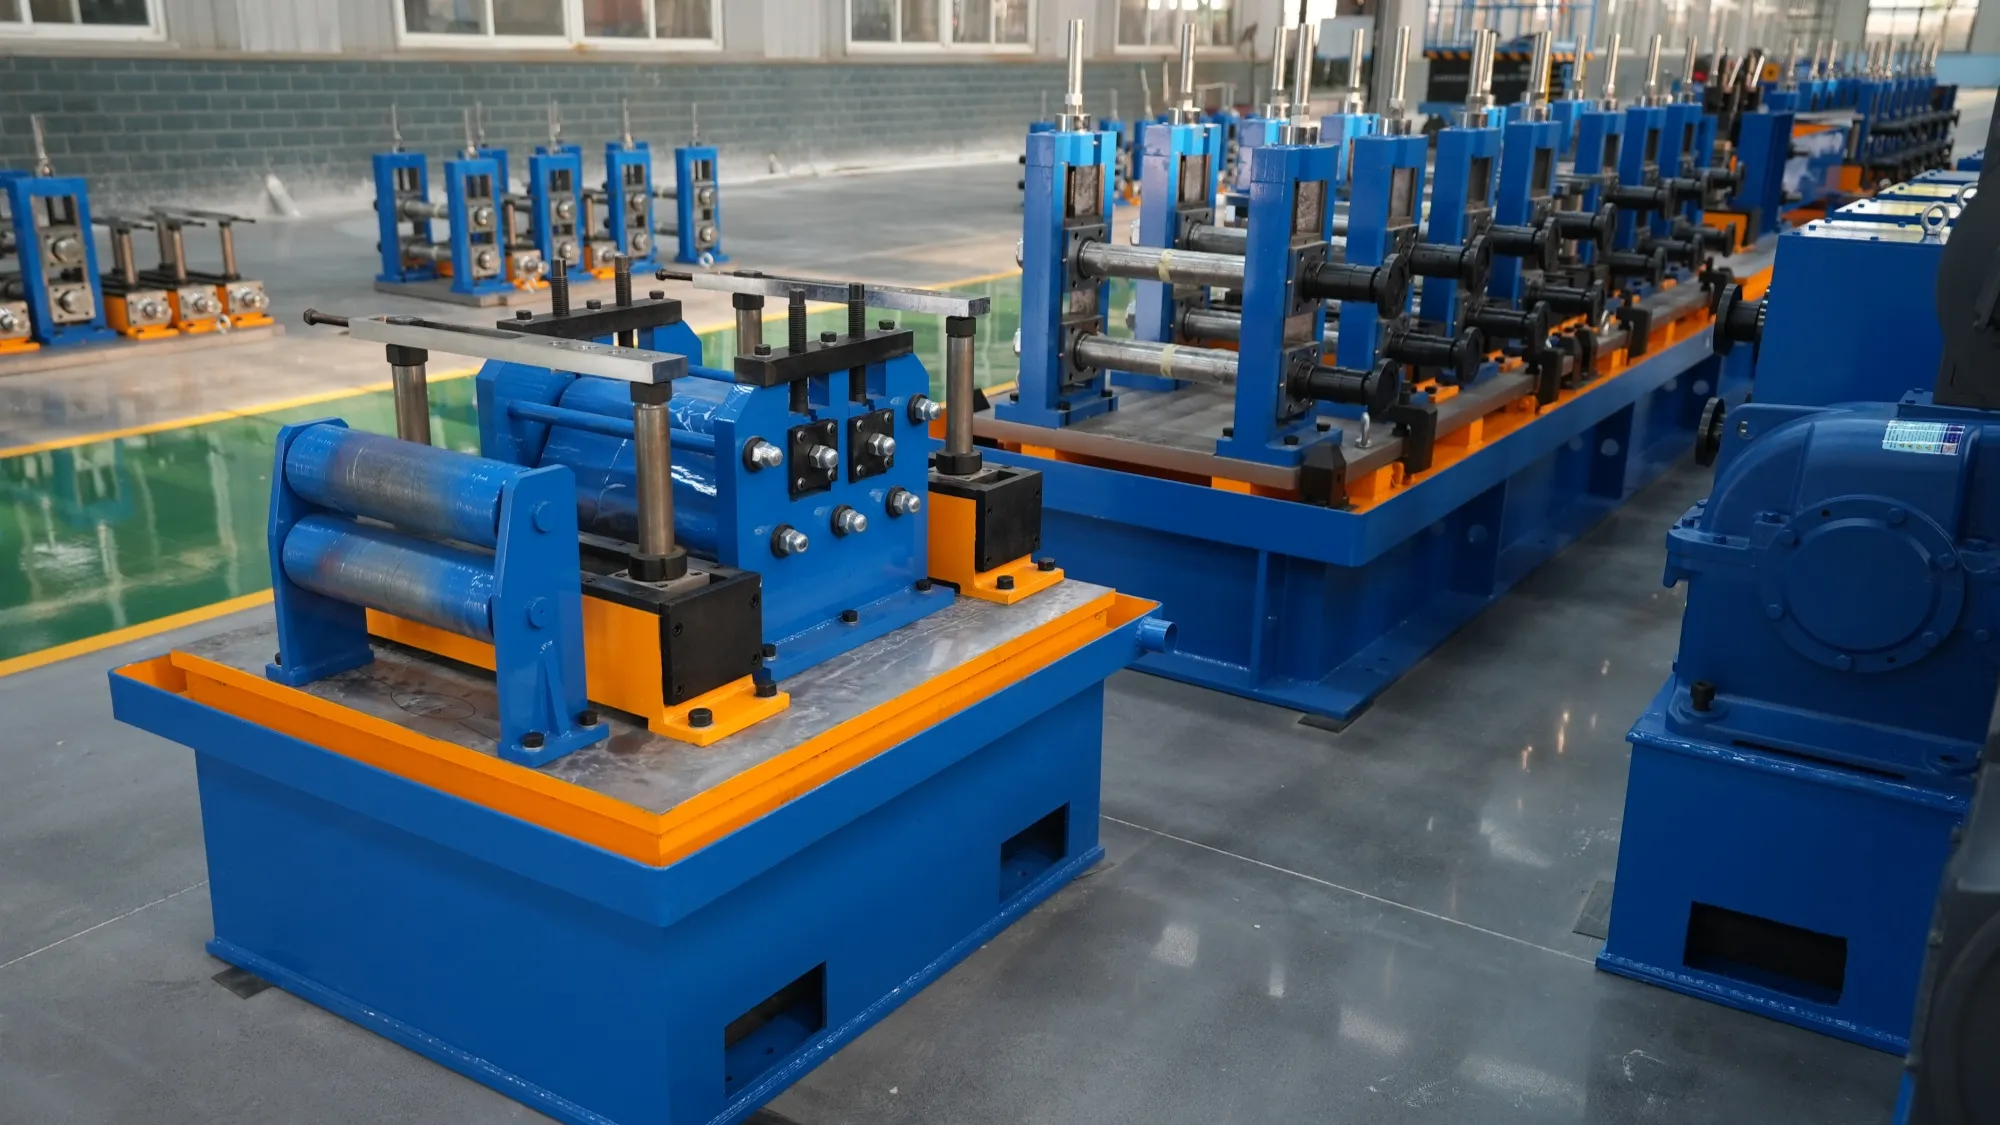
Coil is loaded and uncoiled with an expanding-mandrel uncoiler that tensions the coil pneumatically through a four-bar mandrel; the failure mode at this stage is that unstable tension causes strip wander and loose coil, which then shows up as forming deviation downstream.
On HG89 and above, the head of the strip is flattened and a five-roll leveller straightens it so that it enters the next stage flat.
Rolls then progressively form the strip into the required round or square shape, a stage that is decisive for pipe shape and seam alignment.
Worked Example — Band and Welder Power for Your Diameter
If a buyer’s target is Φ32 mm pipe, the band that carries that diameter is HG32, and the power for that band is 150 kW. At the other end of the range, if the target is Φ630 mm, the band is HG630 and the power is 1500 kW.
The eight process stages
The irregular head and tail are sheared off and the strips butt welded together so that a coil change does not stop the line. A spiral accumulator stores strip between the shear-welder and the mill so that the mill keeps forming while the next coil is prepared. Forming rolls work the strip progressively into the required section.
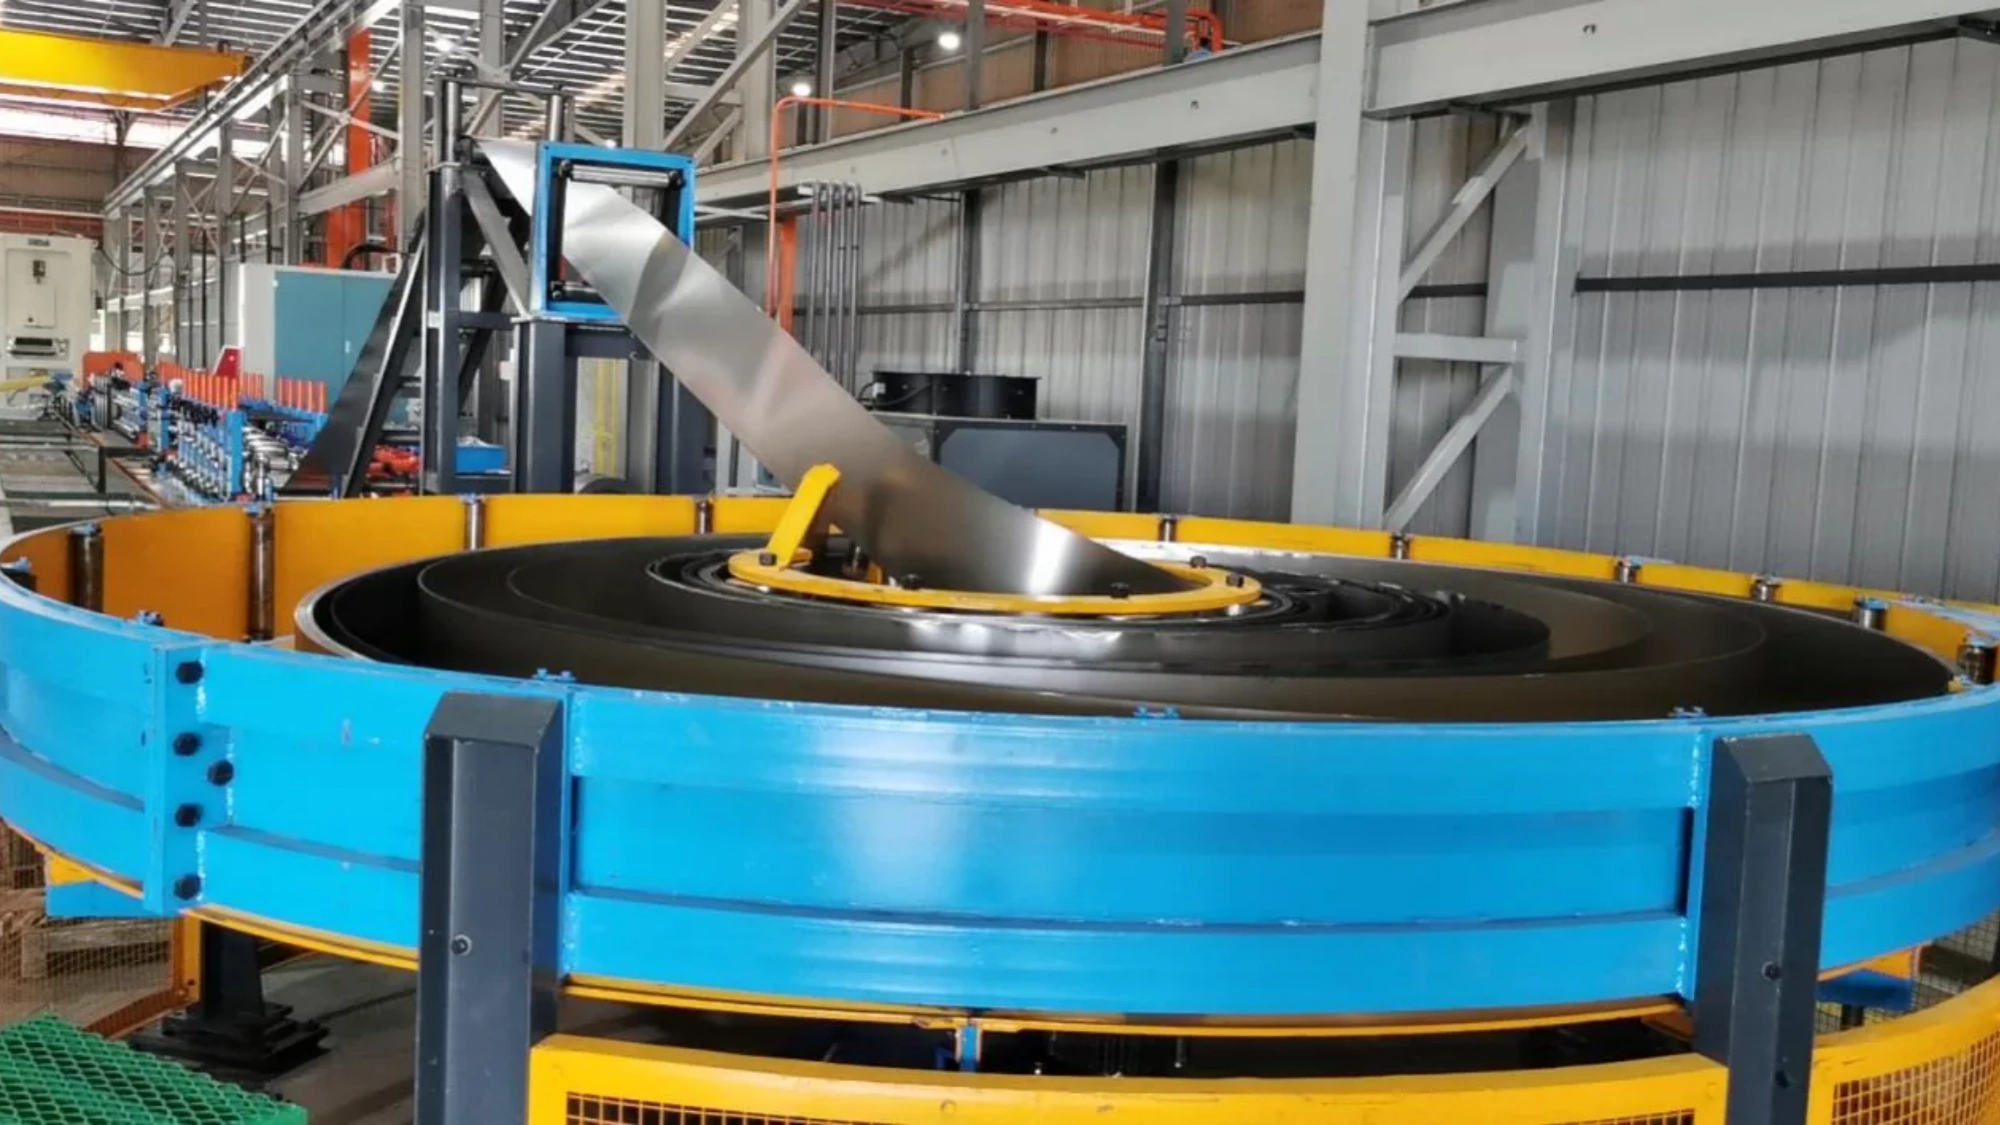
High-frequency current, concentrated at the seam by skin and proximity effects, heats the edges to welding temperature and squeeze rolls press them together. After cooling the tube is sized and straightened to final dimension and straightness. A flying saw cuts it to length automatically while the pipe continues to be delivered at speed.
Each of those stages carries a failure mode, and they are worth reading as a set because together they explain the reasoning behind the line’s specification. Poor accumulator storage or tension control starves or shakes the mill, which shows up as weld-seam fluctuation and downtime.
Mismatched power, weld speed or squeeze amount produces lack of fusion, cold welds or burn-through, which fails pressure and non-destructive testing. Incorrect sizing or straightening adjustment produces out-of-tolerance outside diameter and bend.
The eight units the line is built from
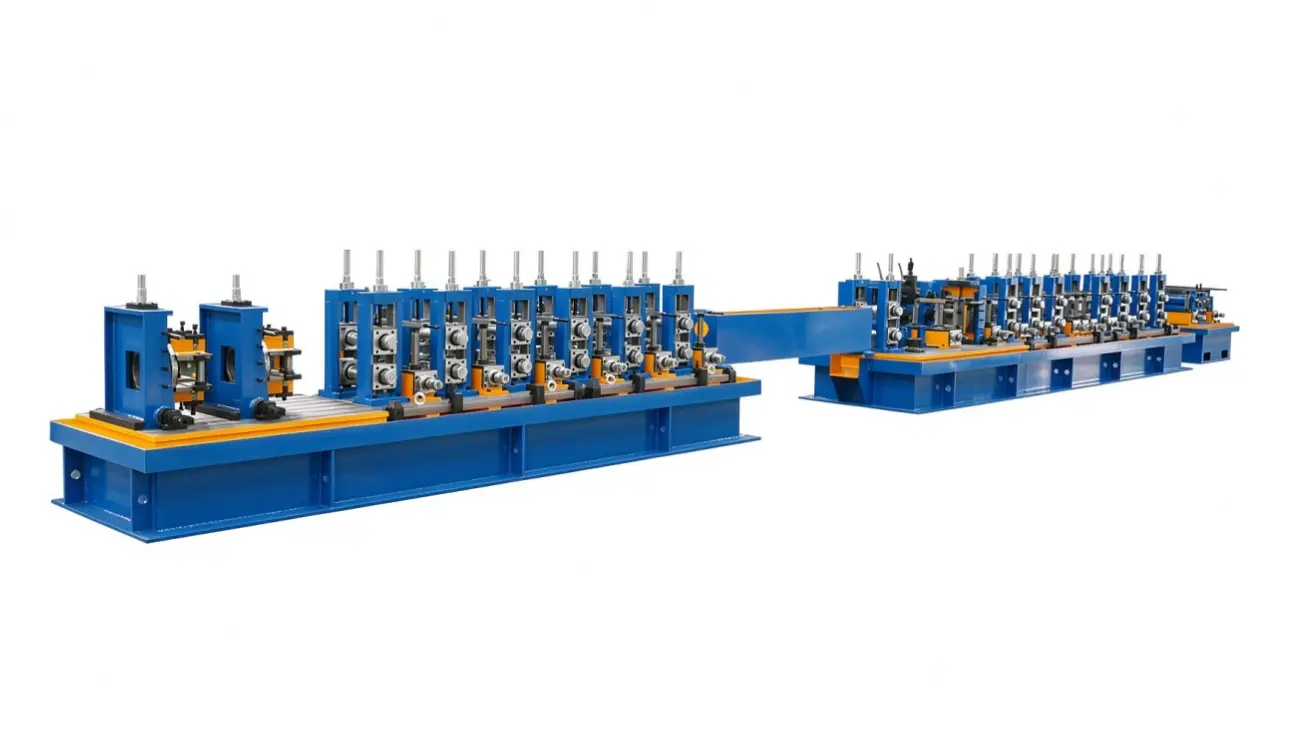
Against those stages a full ERW tube mill machine is built from eight units: an expanding-mandrel uncoiler, a five-roll pinch and levelling machine (HG89 and above), an automatic shear and butt welder, a spiral accumulator, the forming and sizing mill itself, the high-frequency induction welder rated across the 150 to 1500 kW range by band, a flying or cut-to-length saw, and a PLC and variable-frequency drive control system that unifies speed, cycle and cut-length control.
Two of those units are key components rather than merely core ones. The cutting saw determines cut-length accuracy and end-face quality while pipe is delivered continuously at high speed, with blade or length-setting error showing up as length deviation, end burrs and a skewed cut. The induction coil and impeder govern how efficiently welding energy reaches the seam.
What actually decides quality on this line
The key quality factors span raw material, process, equipment, personnel and inspection. Incoming strip is checked for grade, thickness tolerance and flatness, because the consequences of getting it wrong are forming wander, seam inclusions and uneven wall thickness. Roll material and heat treatment govern shape stability.
High-frequency power, frequency and weld speed control seam fusion. Squeeze amount and seam alignment control weld quality, with misalignment, mismatch and burrs as the symptoms. Operator setup and quick roll change reduce scrap on a size change.
That list answers the question of what to look at when comparing lines. Wall thickness, line speed and shift output are confirmed against your pipe size, material grade and cut length at quotation. Send us those three and we will state the figures.
How the line compares with the alternatives
There are two other routes to compare against. Against seamless rolling and UOE or JCOE forming, high-frequency straight-seam welding is lower in investment and running cost, more continuous, and suited to high-volume small and medium diameter production.
Against spiral submerged-arc welding, a straight-seam welded tube mill is faster in welding speed, straight-seam rather than spiral, and suited to structural and conventional fluid pipe.
Beyond diameter there are three more things to decide. Section shape divides round, square and rectangular. Forming technology divides conventional roll forming from direct forming square, in which one combined roll set is adjusted by servo for each size instead of being changed. Automation divides semi-automatic from fully automatic PLC control.
Taken together, a plant building or expanding pipe-making capacity needs production that does not stop, one line that covers several sizes, stable yield and weld quality, and efficient size changes. The spiral accumulator is the specific mechanism that keeps production running through a coil change.
What to ask the factory for
Three questions turn a general enquiry into a quotation. Confirm the band and welder power the ERW mill needs for your target diameter. Ask for the tolerance values behind these quality factors.
And ask what the size-change procedure is on the specific configuration offered — conventional roll change or direct-forming servo adjustment — because that single answer drives both changeover time and long-run tooling cost.
Resource Downloads
From the Workshop
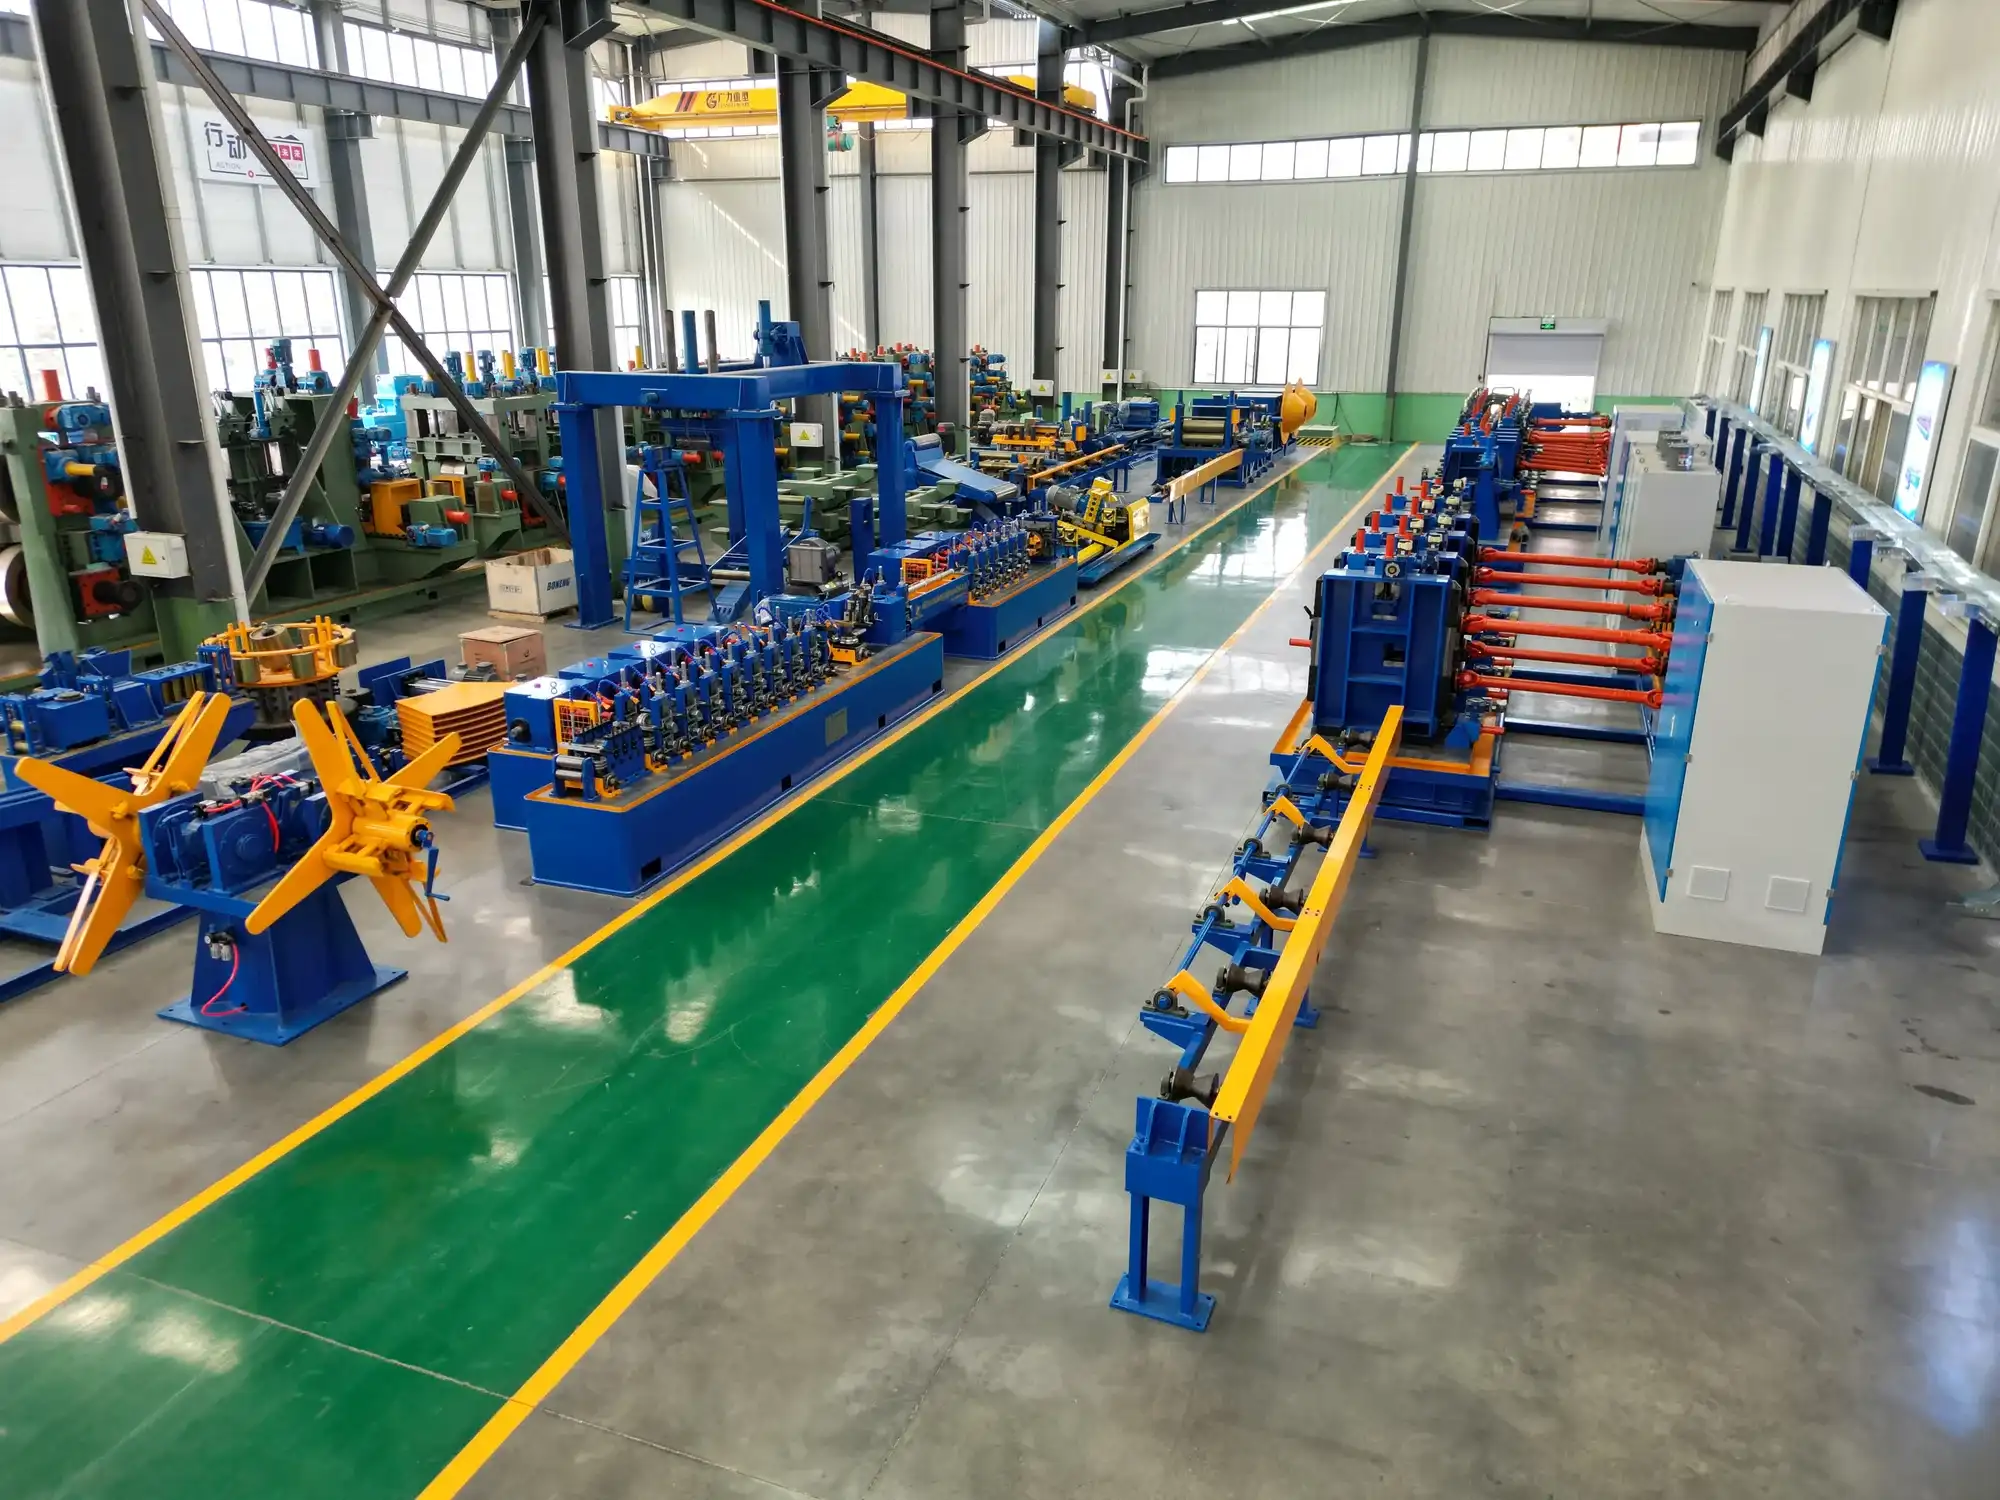
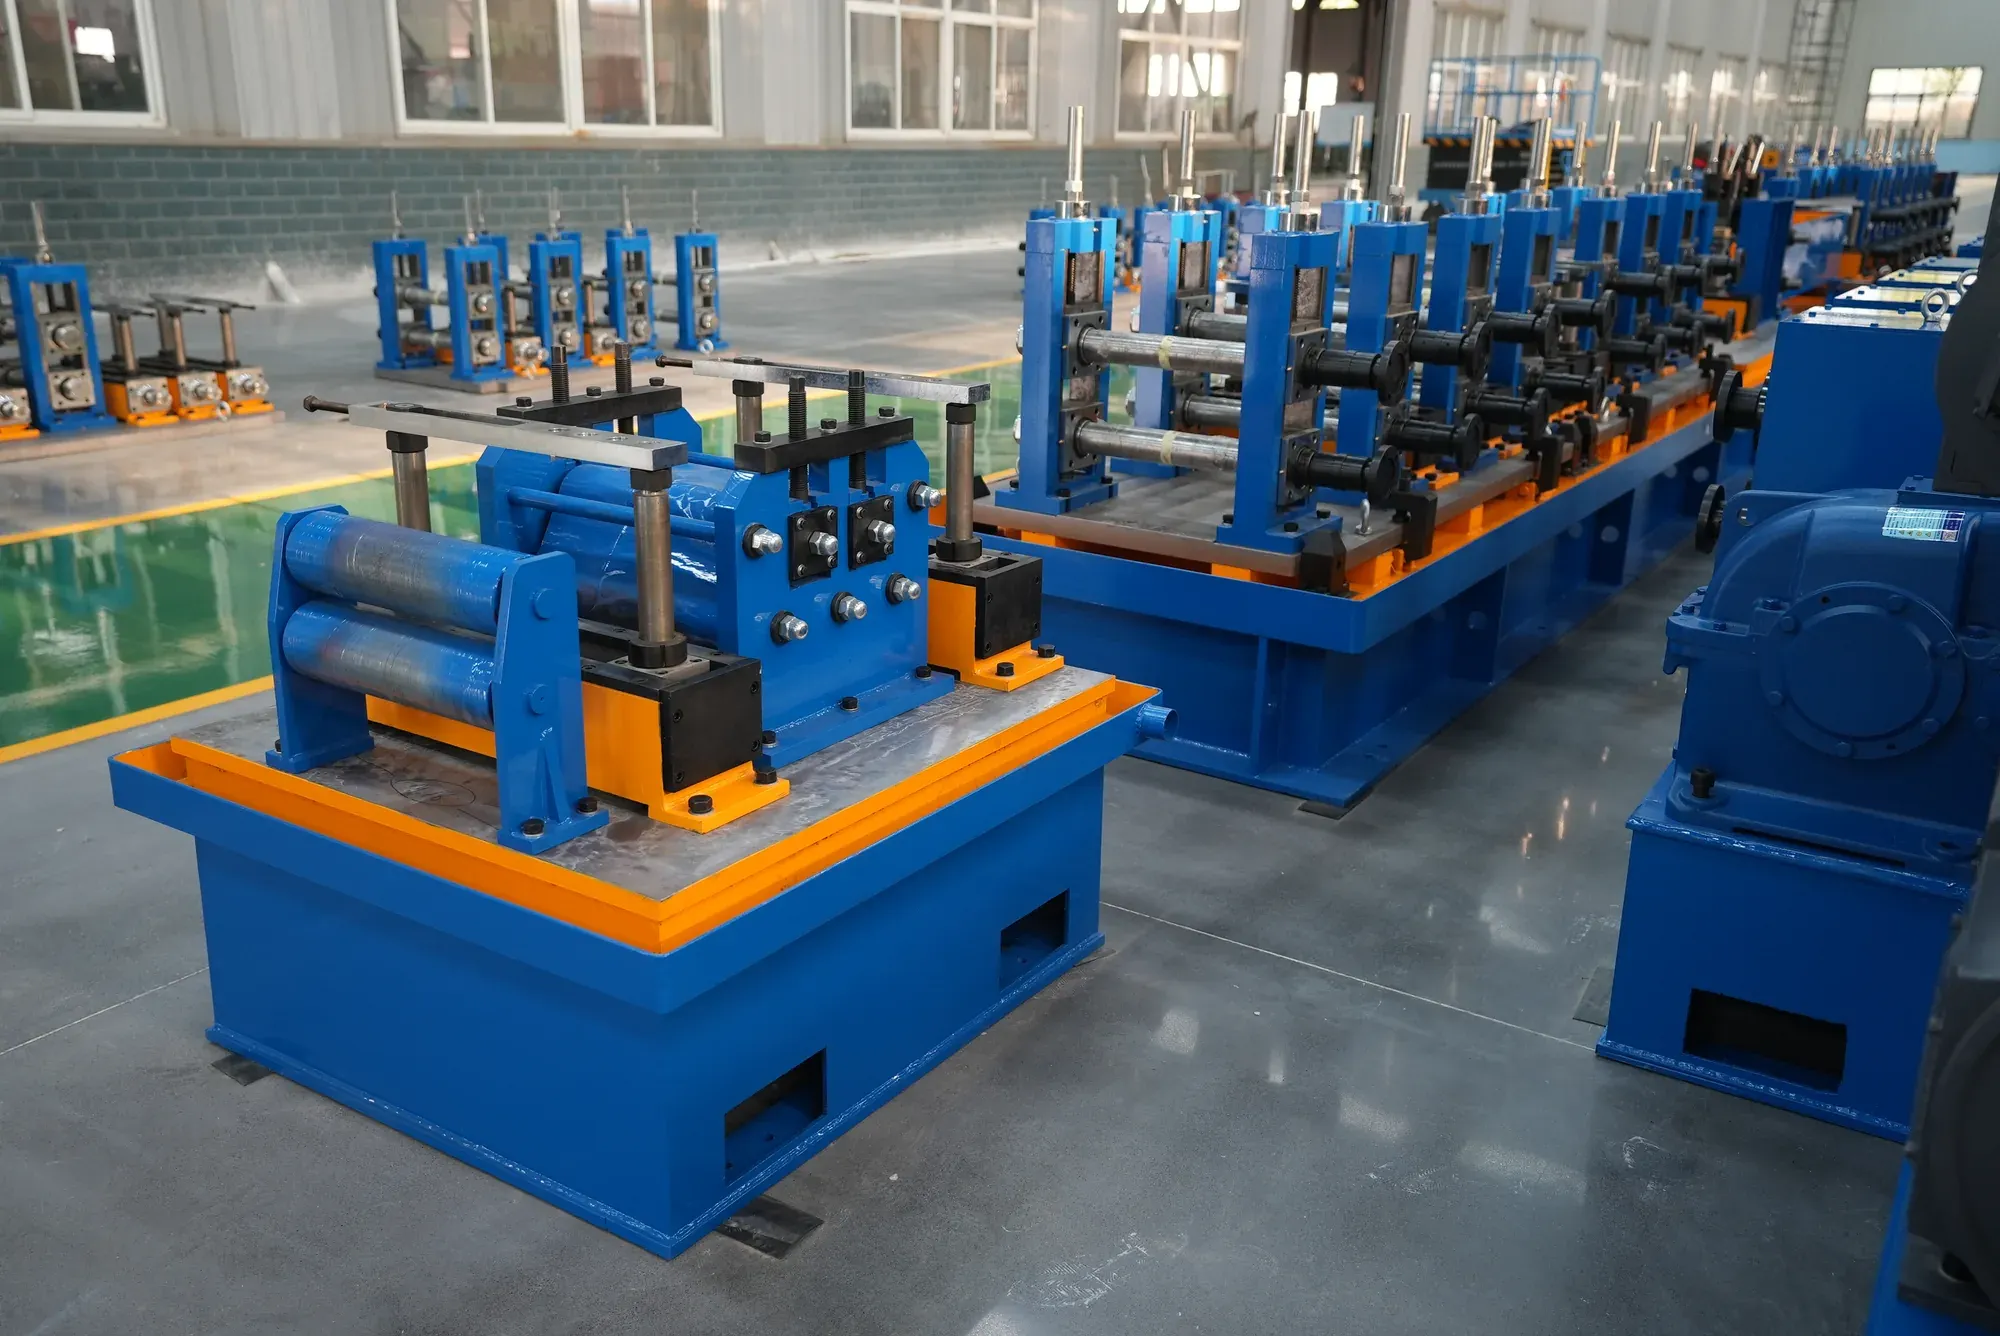
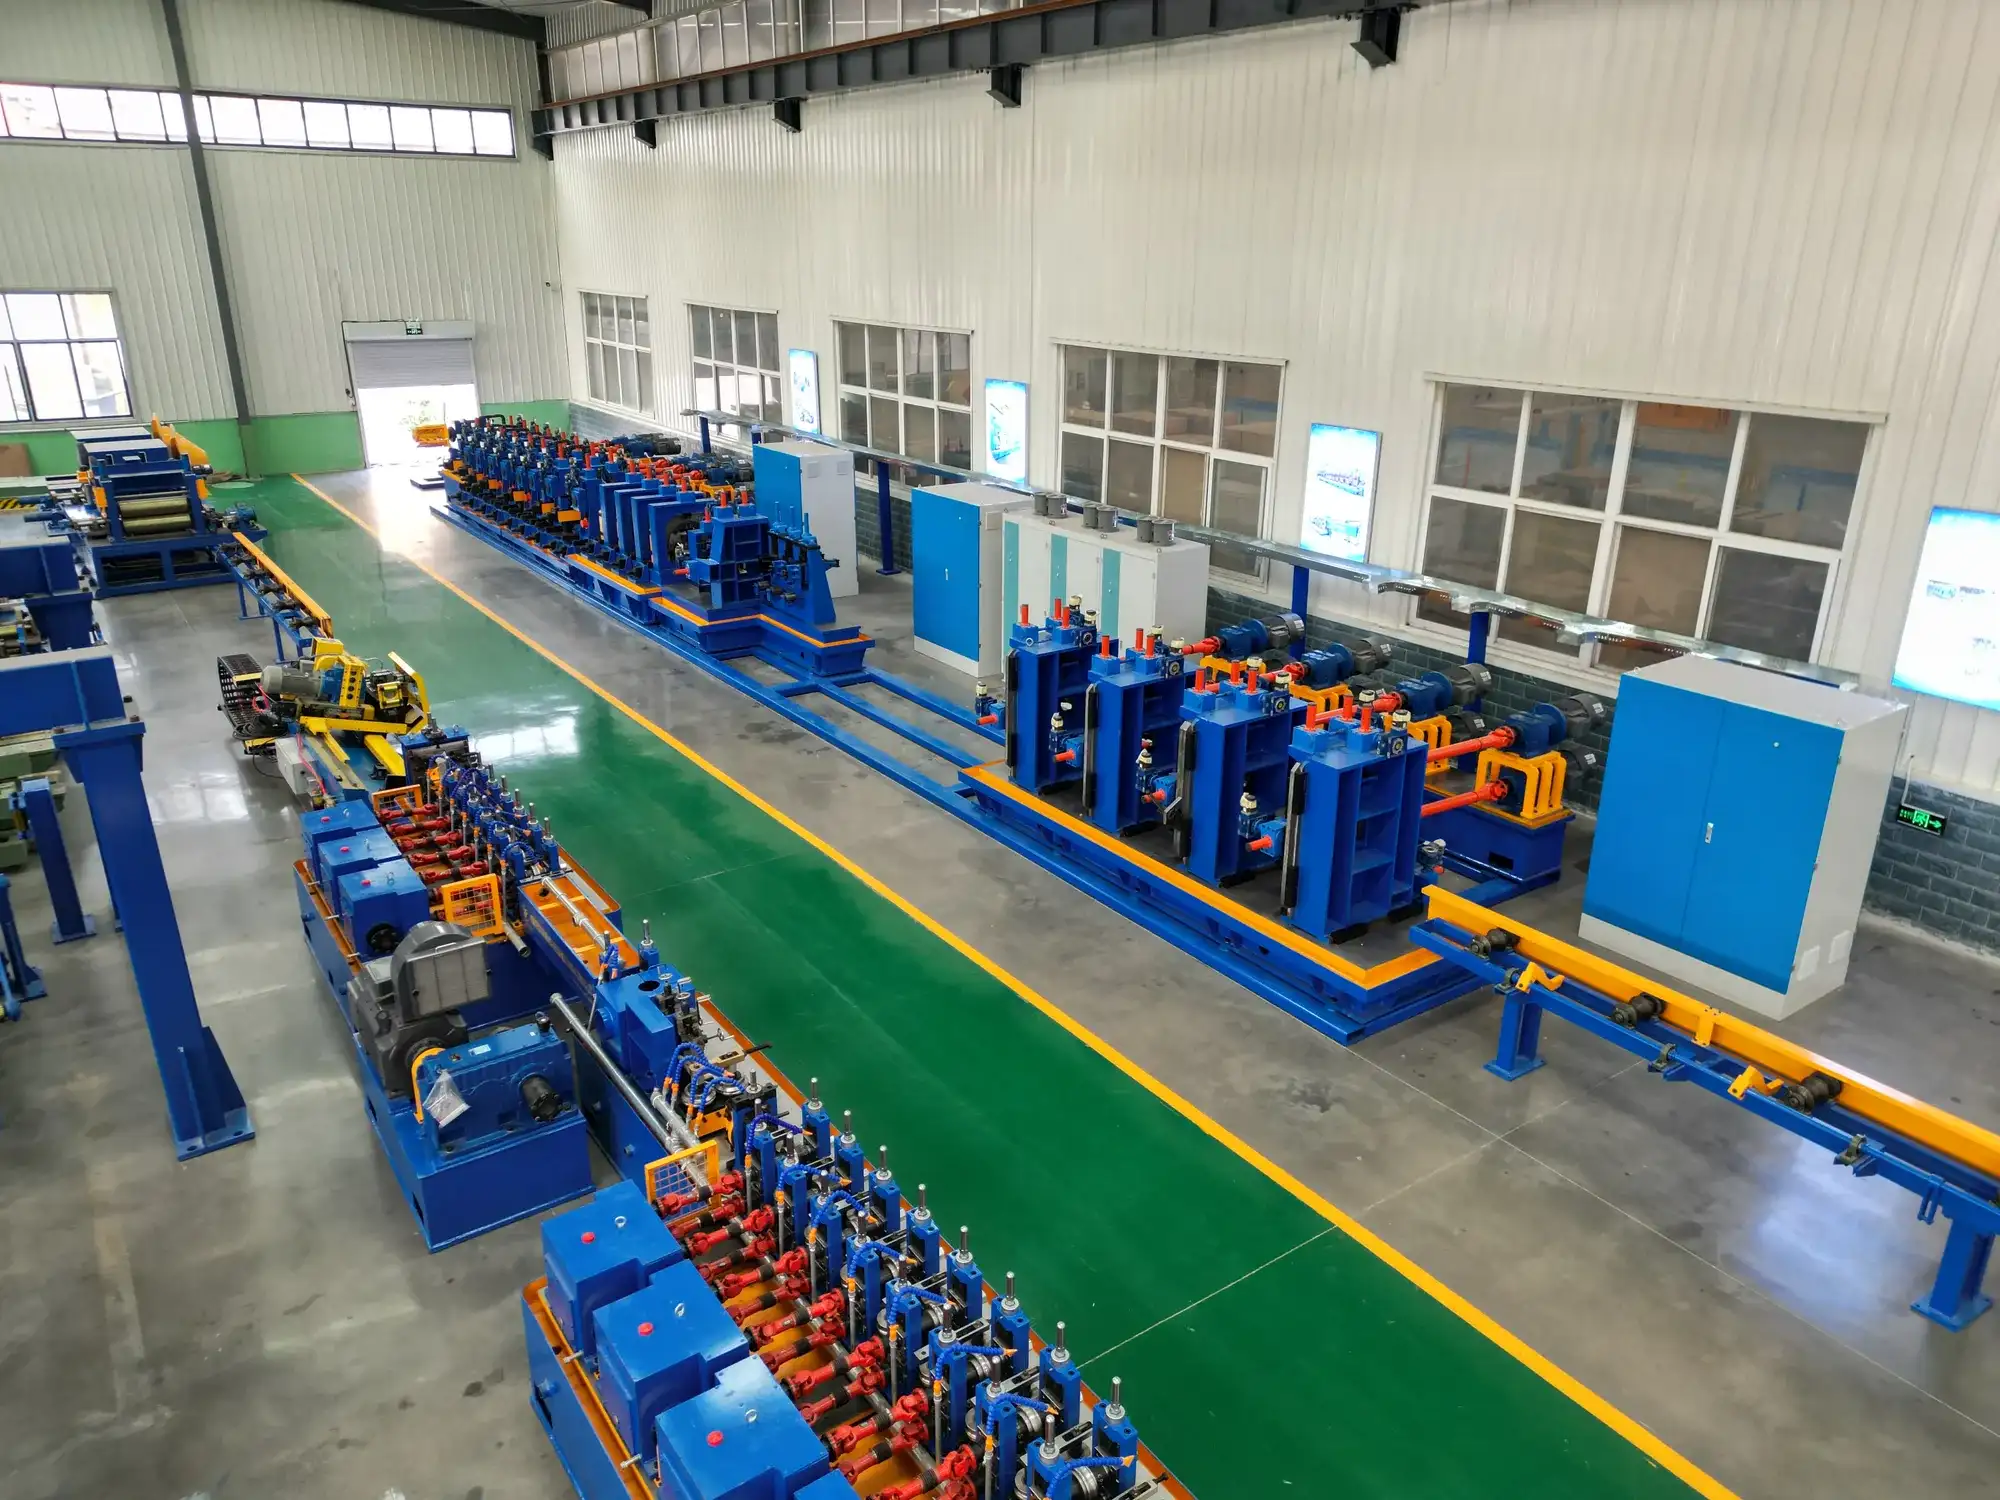
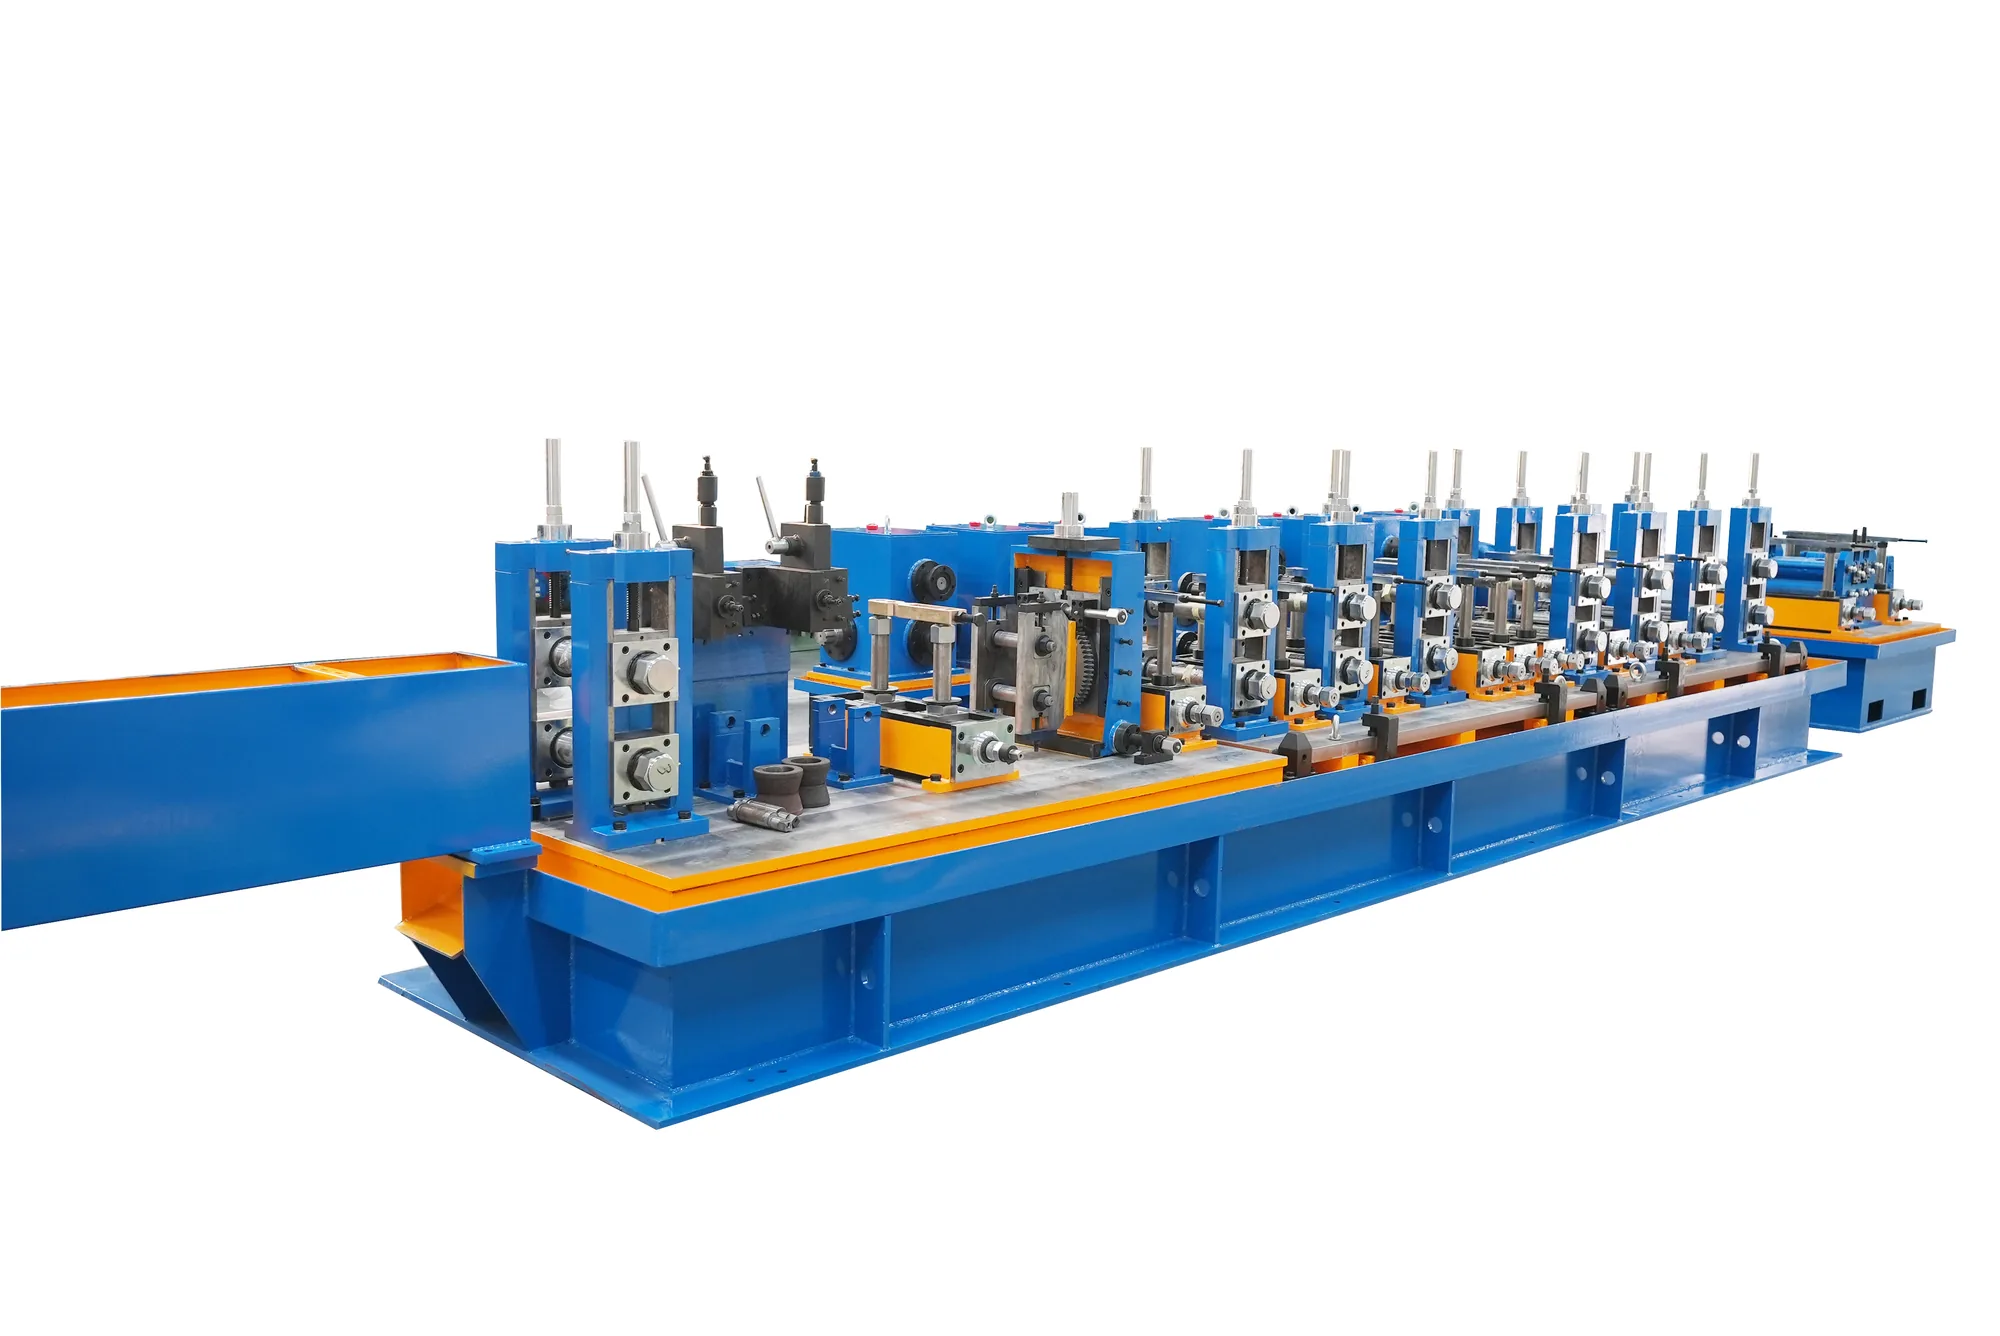
 Tube Mill Machine for Steel Pipe Production
 Tube Mill Output, Material Yield and Roll-Change Cost in the Cold Forming Steel Process
 HGF150 Fully Automatic Square and Rectangular Tube Forming and Welding Equipment
 The API Pipe Mill Inspection Chain
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.