
Home › Direct Forming Square Tube Mill › Roll Saving in Direct Forming
Within each band, direct forming makes every square size from one combined mould set, changing size by servo adjustment instead of by changing rolls.
In This Line
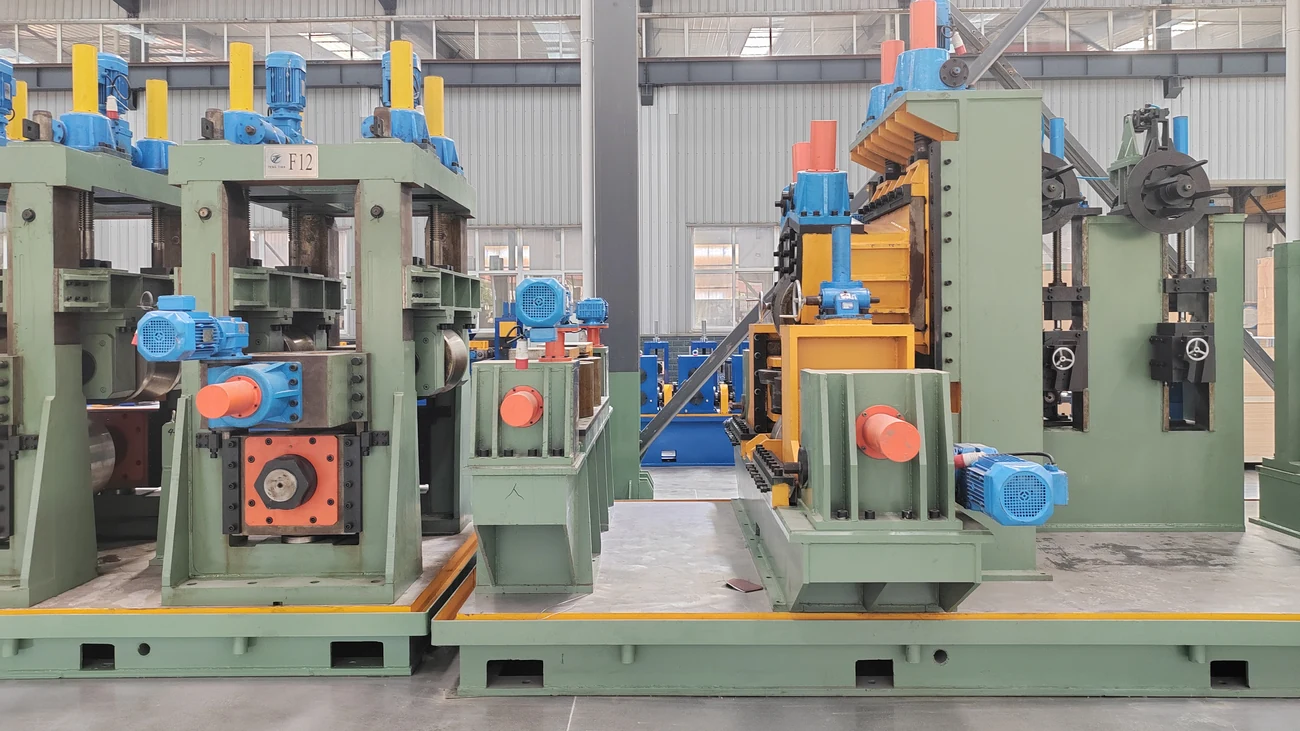
The benefit is a roll saving of more than 90 per cent together with longer roll life, and the mechanism for it is point contact in the combined roll design. There is one exception: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
How the Combined Mould Saves Rolls
- Within each band, one combined mould set produces every square size; a size change is a servo adjustment, not a roll change.
- Roll saving: more than 90 per cent, with longer roll life.
- Mechanism: point contact in the combined roll design lowers roll wear.
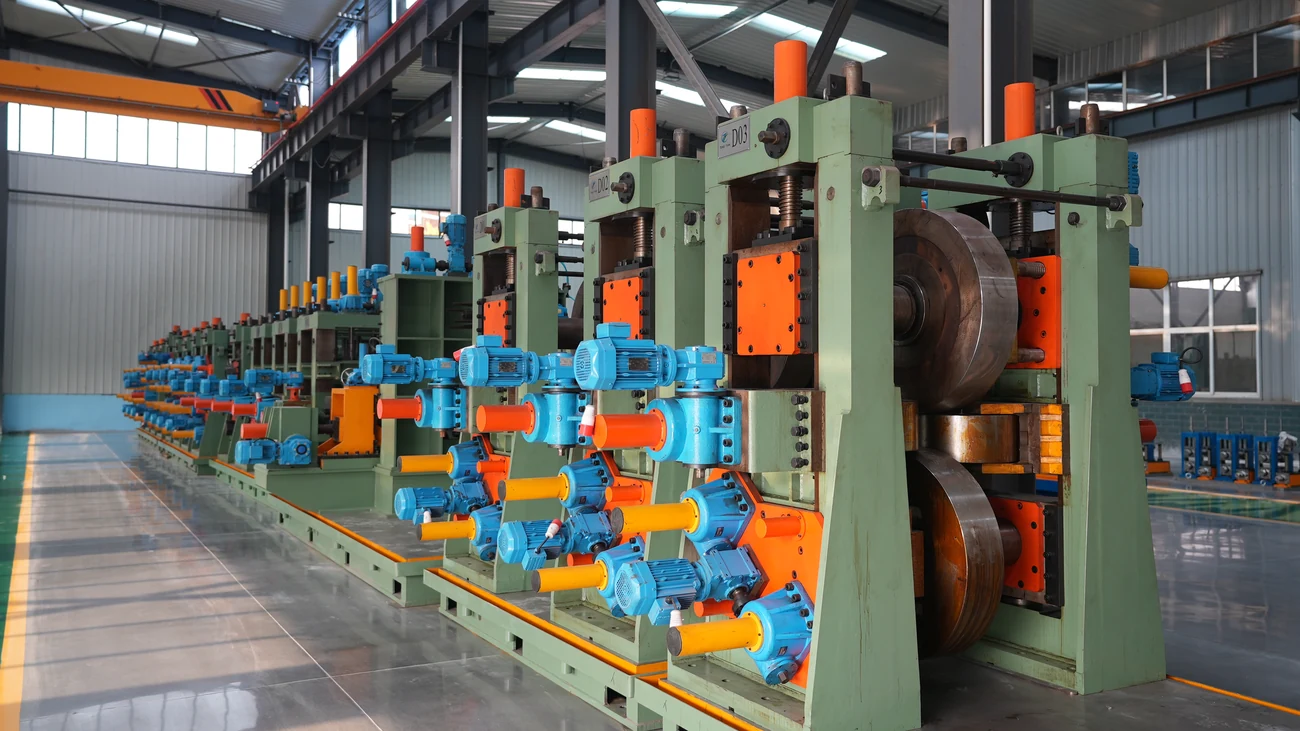
- Size envelope: 30×30 to 500×500 mm across seven bands, wall 1.5 to 20 mm.
- Against the alternative: direct forming vs round-to-square needs fewer forming passes and fewer roll changes.
What Is Roll Saving in Direct Forming
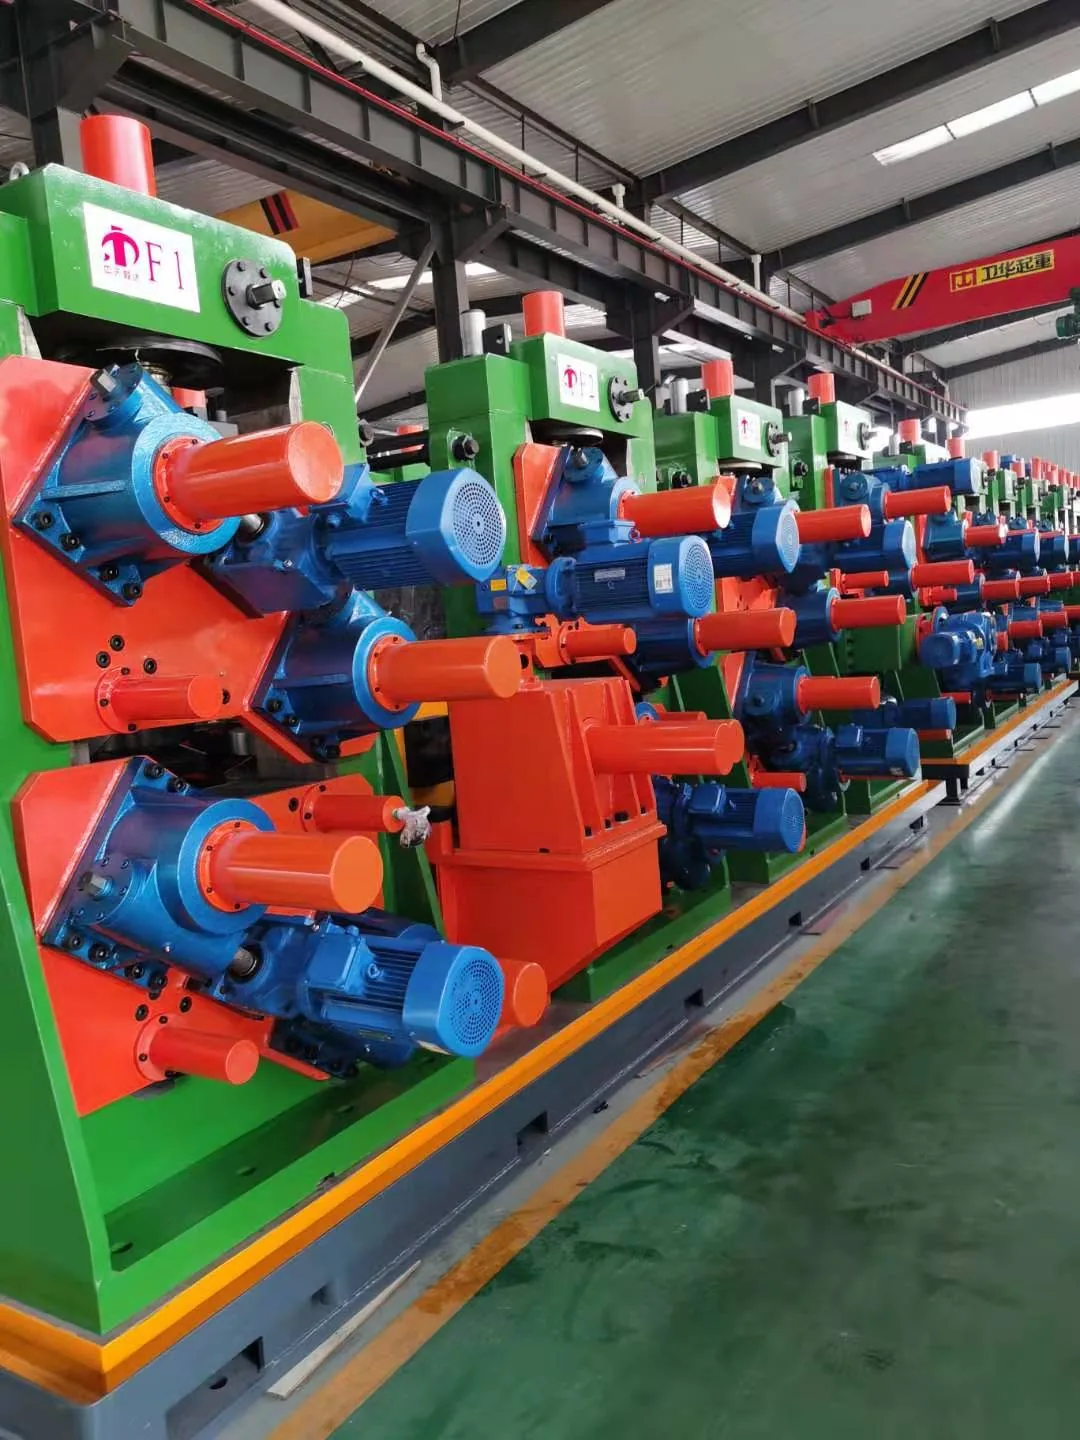
On a roll saving square tube mill, the rolls are not changed at each size change, and that is where the saving of more than 90 per cent comes from.
Roll saving is a comparison, so it matters what it is compared against. A conventional tube mill & welded pipe production line changes its forming rolls when the target size changes; the direct-forming square line does not. Within each band one combined mould set covers the size range, and the change is made by servo adjustment.
The question buyers usually raise
Buyers ask two things: is changing specification troublesome, and how long is the line down for a roll change?
Our answer has three parts: a combined mould with no roll change, a roll saving of more than 90 per cent, and servo adjustment.
Direct forming square tube mill
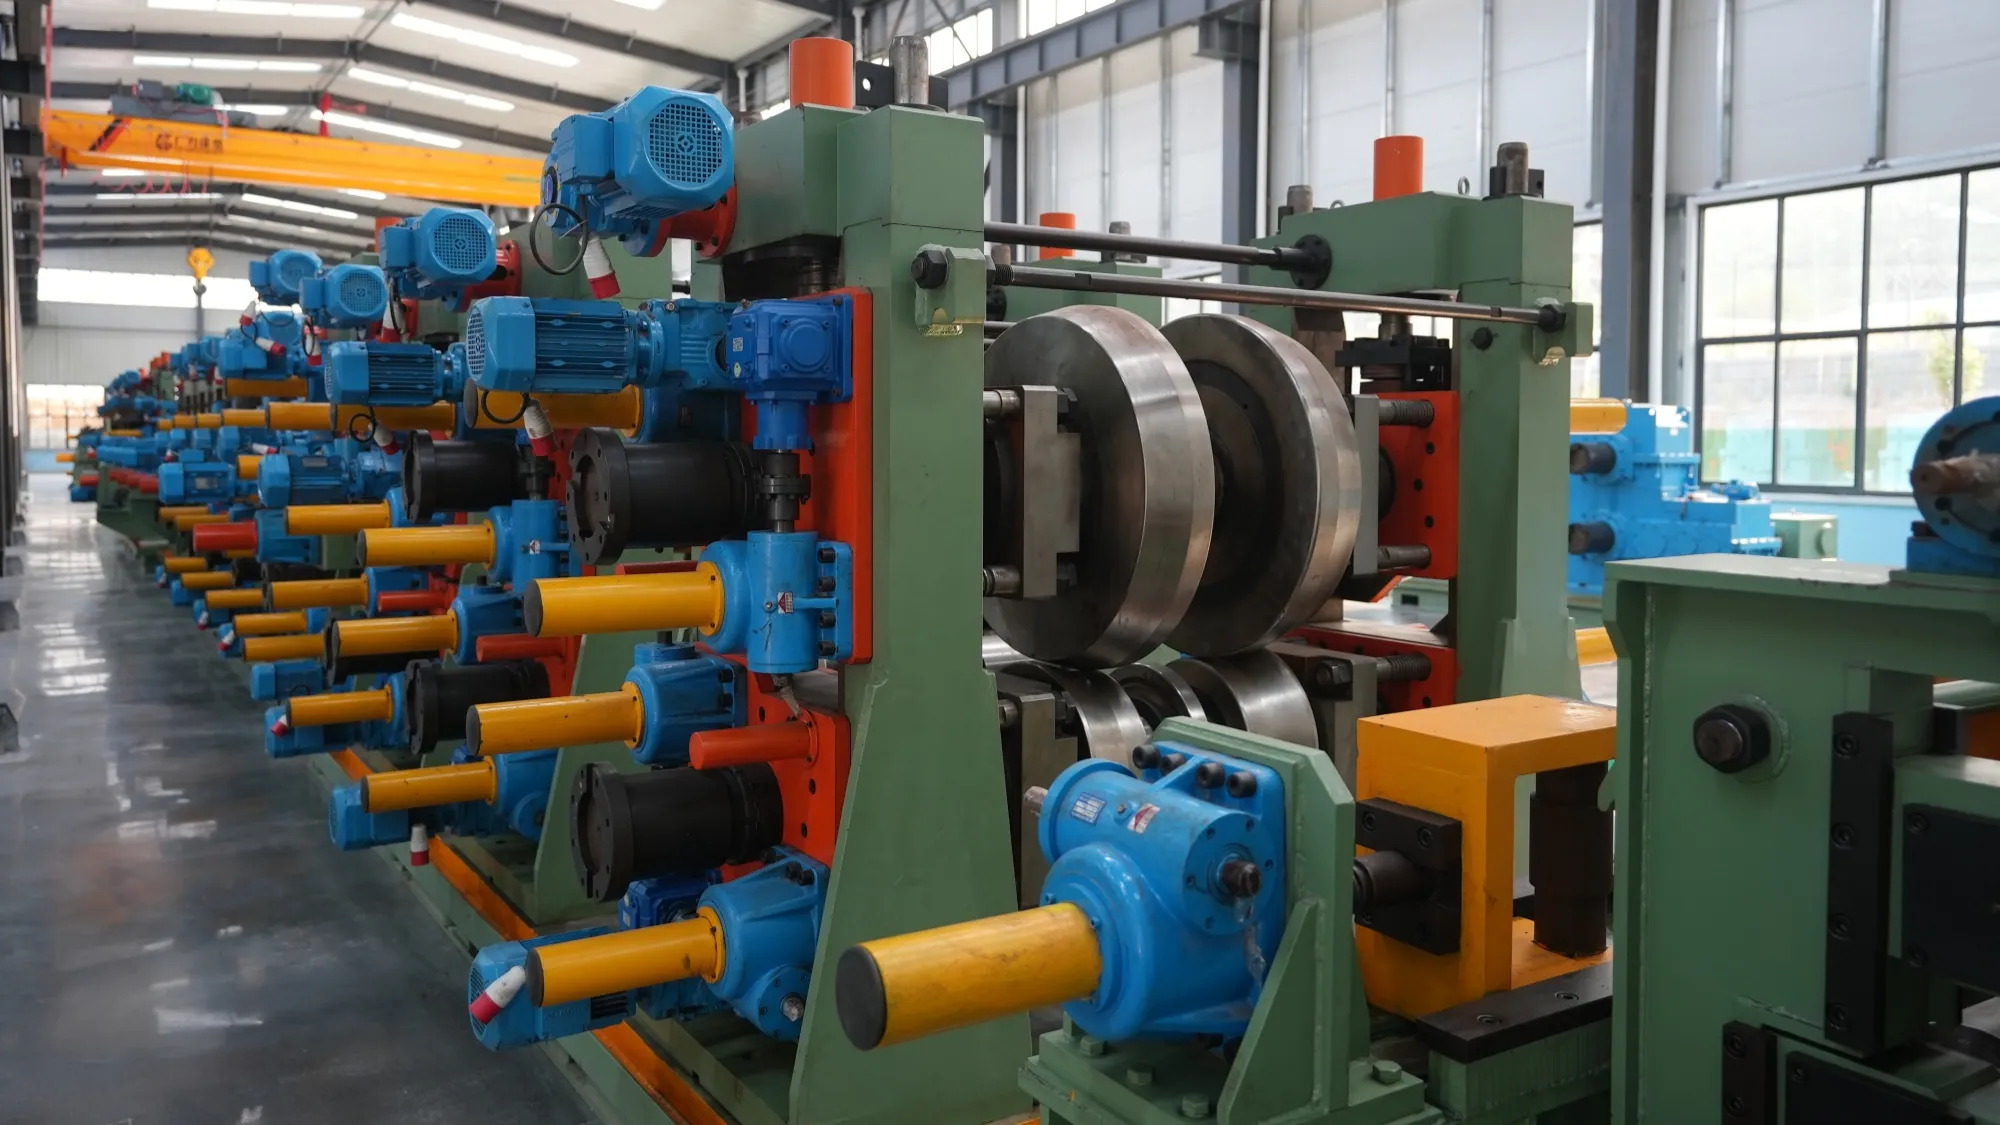
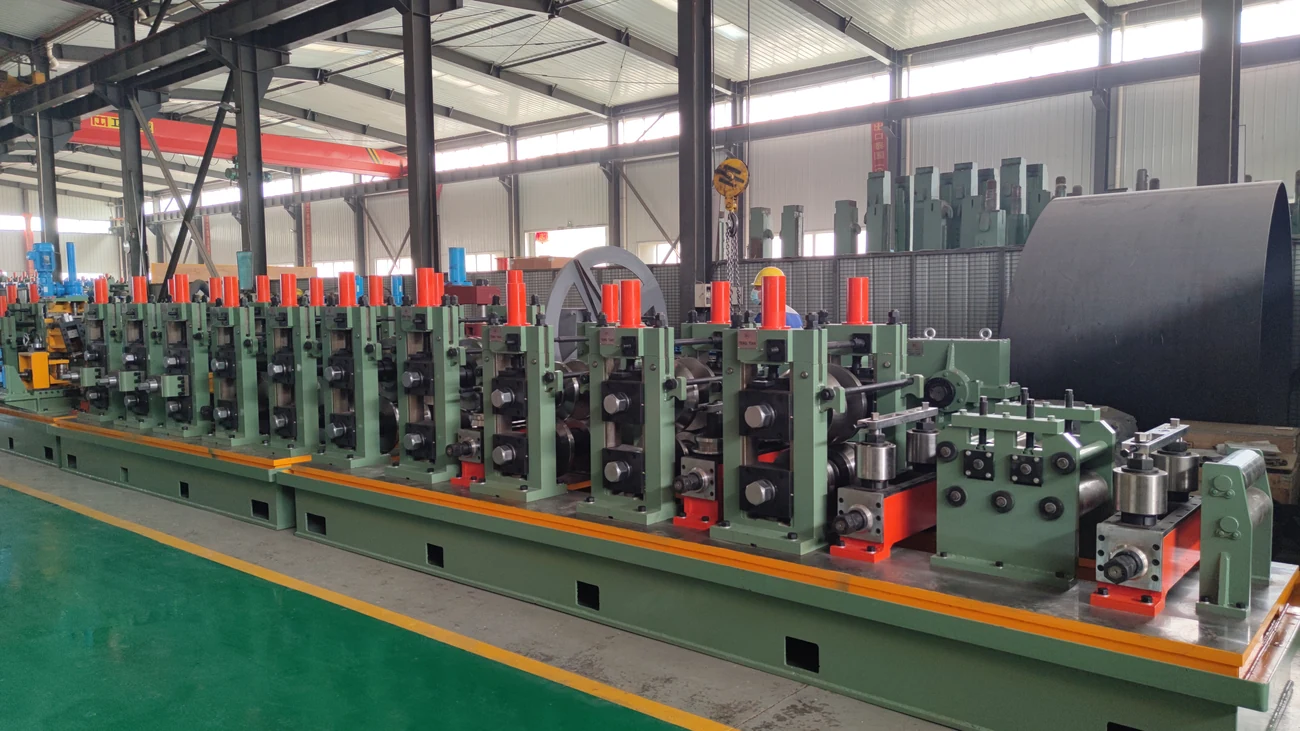
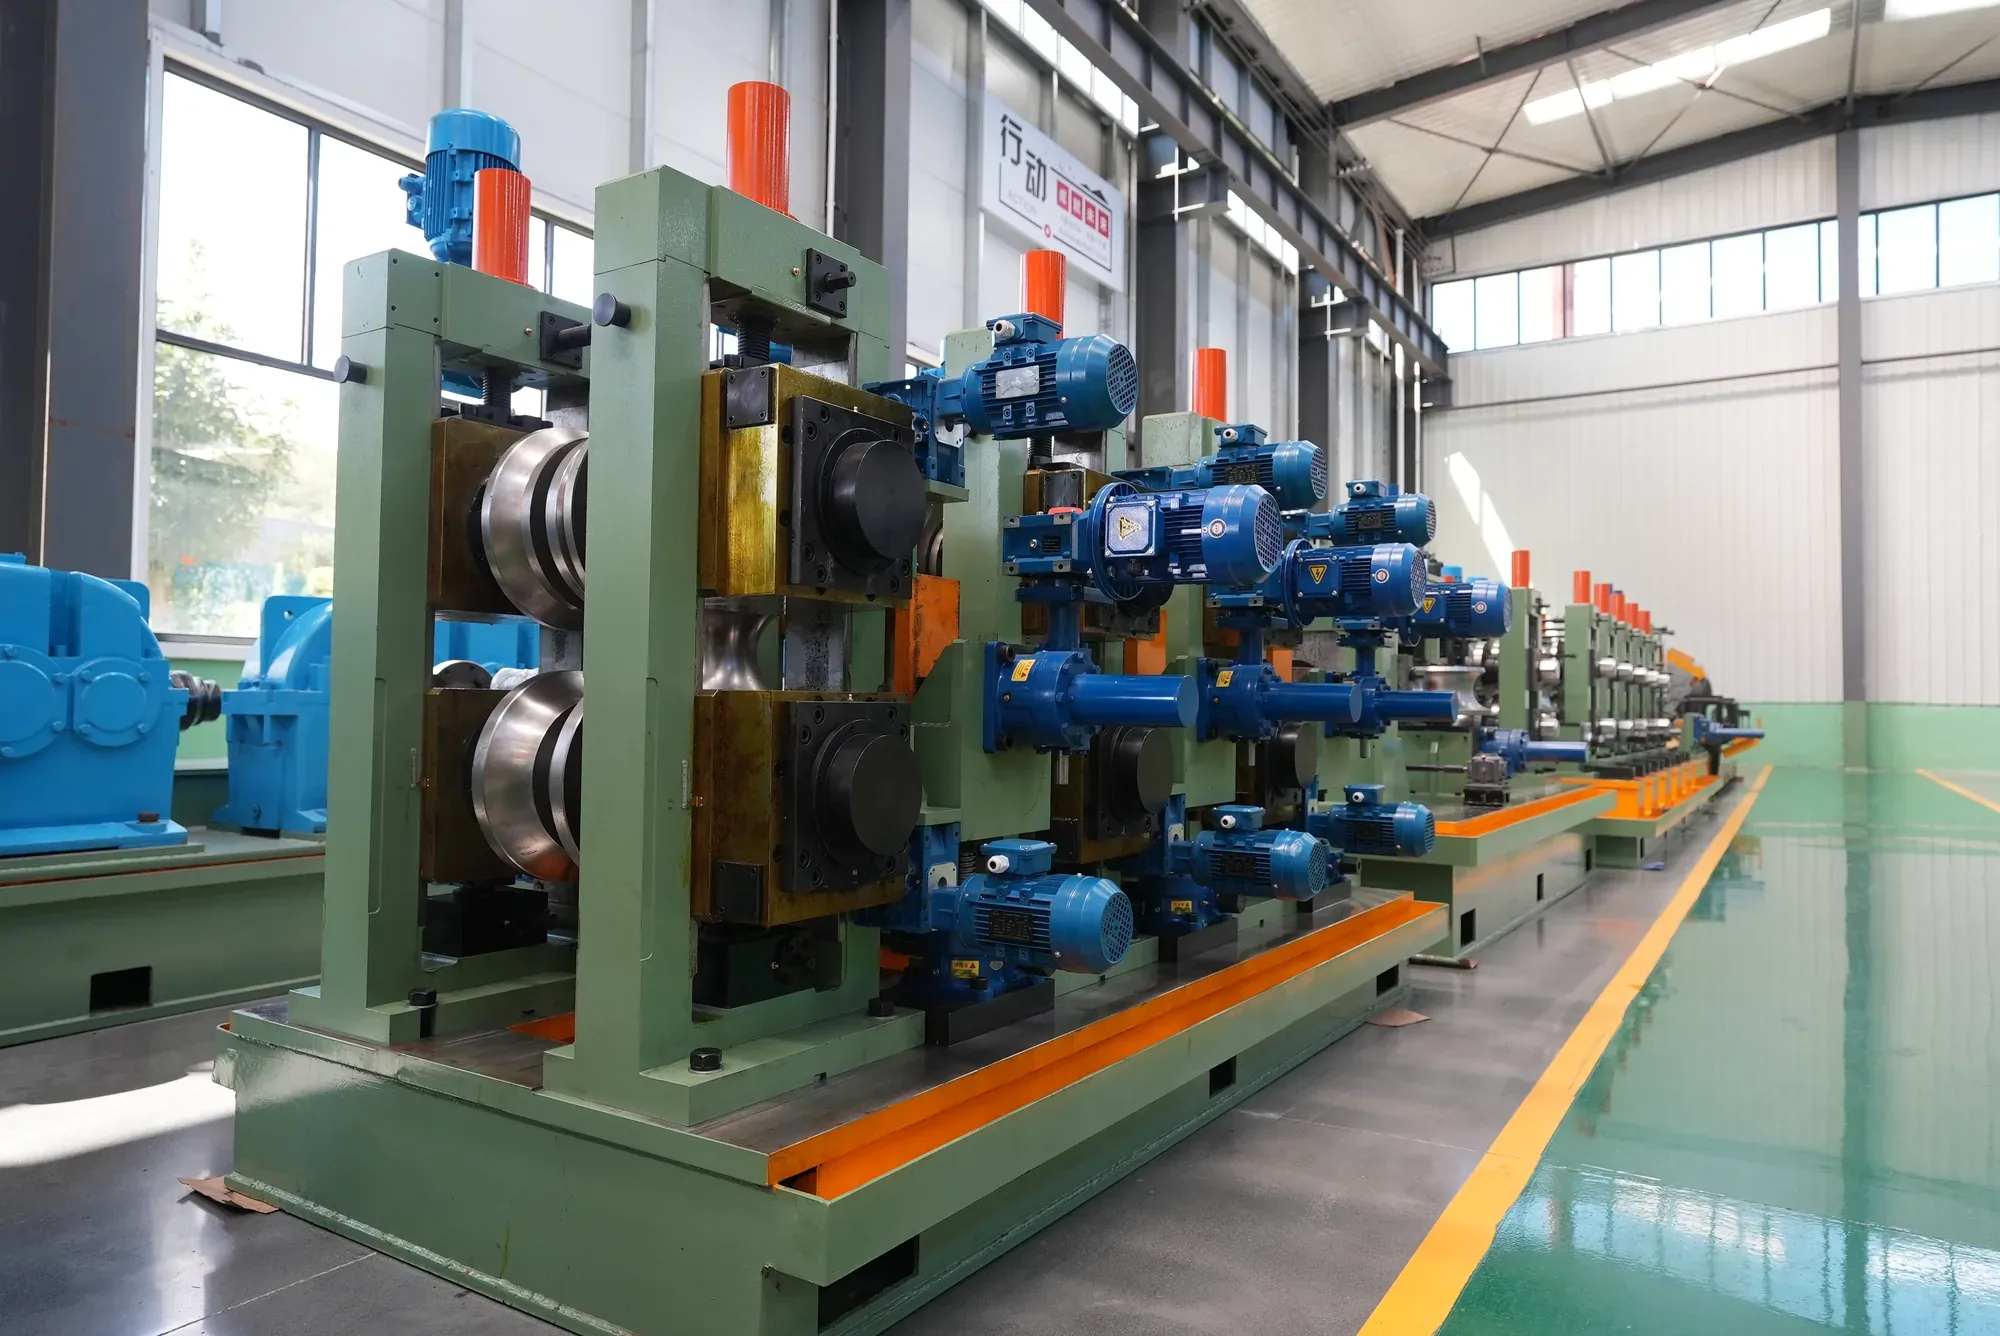
The line itself is a square and rectangular tube line using direct forming square technology: within each band one combined mould set produces every square size, and a size change needs only servo adjustment with no roll change. Across seven bands the finished product runs from 30 by 30 to 500 by 500 mm, wall 1.5 to 20 mm.
Against round-to-square, it needs fewer forming passes and fewer roll changes; the two routes are compared side by side on direct forming vs round-to-square.
The line is aimed at square tube plants that run many sizes and change size often. On a conventional welded line, those plants lose time changing rolls and carry a high roll consumption cost.
Roll Saving in Direct Forming — Method and Measured Values
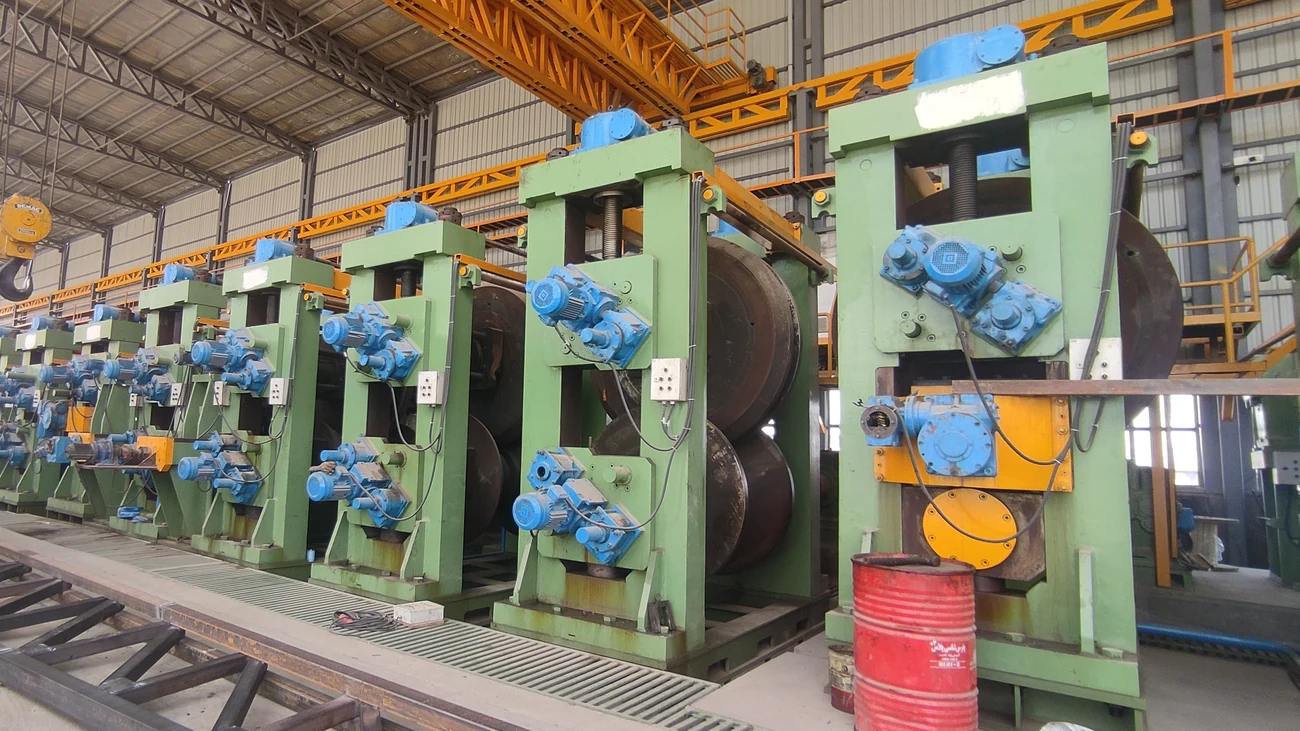
The figure on record is a roll saving of more than 90 per cent, measured against changing rolls at every size change on a conventional line. The method behind it is point contact in the combined roll design, which lowers roll wear, together with one mould set per band instead of one roll set per size; quick die change and servo adjustment mean the rolls also last longer.
Multi size square tube machine
A multi size square tube machine is built for plants that switch frequently across the 30 by 30 to 500 by 500 mm range; the cost of doing that on a conventional line is high roll consumption and long downtime for the roll change, and the requirement is therefore adjustment without a roll change.
Roll saving rate is more than 90 per cent. Tooling life is longer, though not expressed as a figure. Size-change time is not a fixed catalogue figure either.
For running cost, roll consumption goes together with material yield: low roll consumption, high yield and quick changeover are what keep long-term operating cost under control.
Standards and Patents Behind the Roll Saving
The enterprise standard Q/GYL TT01-2023, covering HGF150 high-frequency welded pipe equipment, was issued on 31 August 2023, took effect on 15 September 2023, and is published on the national enterprise-standard information platform as a twelve-page document.
Tengtian holds granted invention and utility model patents on the direct-forming square line and its forming units.
Step-by-Step Procedure
A size change on a direct-forming square line takes four steps.
- Set the target size. Set the line to the new square size within the band it is built for.
- Adjust the forming stands by servo. The combined mould stays in the mill and the servo motors move the rolls to the new size; there is no roll change. (On a conventional line this step is a roll change, followed by resetting roll gap and alignment.) The one exception is 100 × 100 mm, where the upper roll on the final open stand is changed.
- Run the first tubes and check the section. Shape drift after a size change shows up here, before production starts.
- Keep the changeover crew trained. Operator setup and quick die change are what keep scrap low on each size change.
What the 90 Per Cent Means for Your Plant
The 90 per cent is a ratio: it compares one combined mould set per band, adjusted by servo, with a conventional line that changes rolls at every size change. Across the seven bands the line covers 30 by 30 to 500 by 500 mm, wall 1.5 to 20 mm.
To turn the ratio into money or hours for your plant, four inputs are needed: your current roll consumption, the roll price, the time a size change takes on your existing line, and how many size changes you make in a month.
Resource Downloads
 Direct Forming Size Range
 Two Routes to Square Section, Side by Side
 Direct Forming Square Tube Mill
 Welded Pipe Guide
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.