
Home › Direct Forming Square Tube Mill › Direct Forming Size Range
A direct forming square tube making machine covers 30×30 to 500×500 mm across seven bands, with one combined die set per band.
In This Line
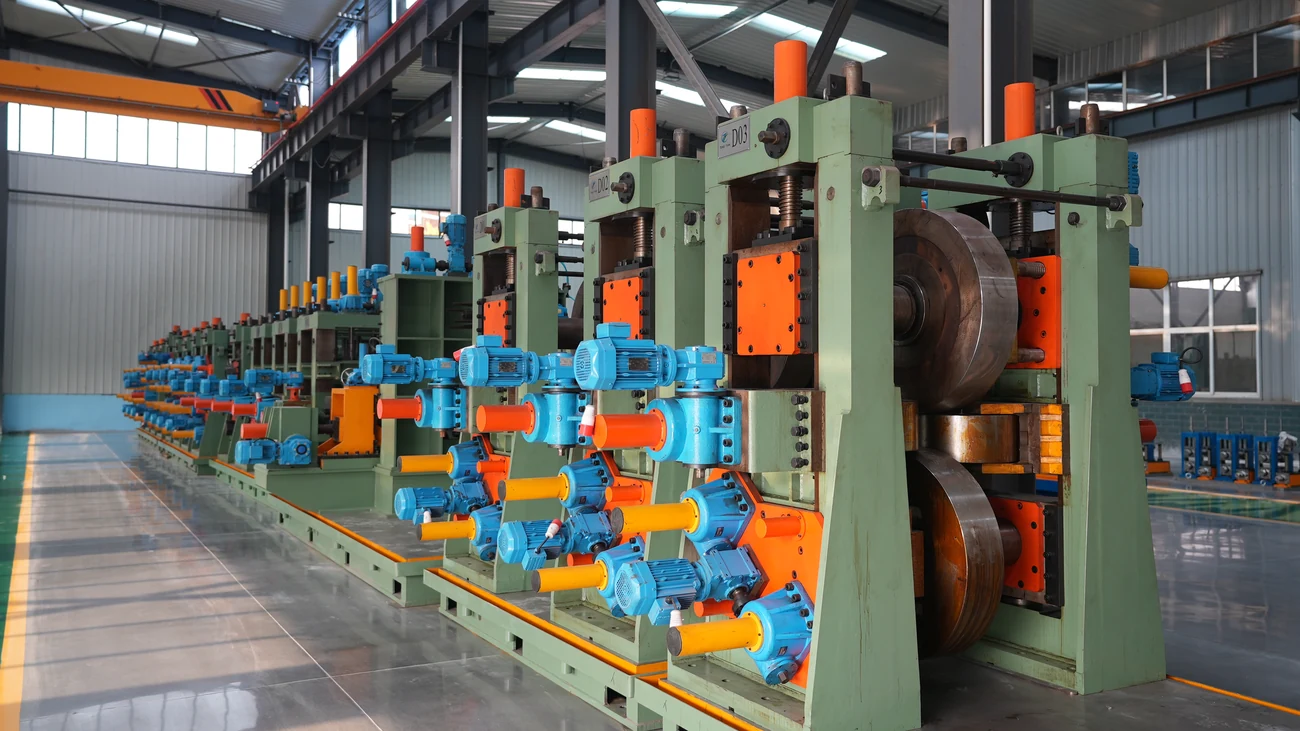
Changing section is a servo adjustment rather than a roll change, and the roll saving is above 90%. There is one exception: making 100 × 100 mm tube needs the upper roll on the final open stand changed.
Technical Specification Table
| Model | Square section (mm) | Wall (mm) | Strip width (mm) | Coil weight (t) | HF welder (kW) |
|---|---|---|---|---|---|
| HG100x100 | 30×30 – 100×100 | 1.5 – 4.0 | 120 – 400 | 4 | 300 |
| HG150x150 | 70×70 – 150×150 | 2.0 – 6.0 | 280 – 600 | 10 | 600 |
| HG200x200 | 100×100 – 200×200 | 2.0 – 6.0 | 400 – 800 | 15 | 600 |
| HG250x250 | 150×150 – 250×250 | 2.0 – 8.0 | 600 – 1000 | 12 | 800 |
| HG300x300 | 150×150 – 300×300 | 5.0 – 13.0 | 600 – 1200 | 25 | 1000 |
| HG400x400 | 150×150 – 400×400 | 5.0 – 14.0 | 600 – 1600 | 26 | 1000 |
| HG500x500 | 200×200 – 500×500 | 10 – 20 | 800 – 2000 | 30 | 2000 |
| Item | All seven models |
|---|---|
| Forming principle | Direct forming square — one combined die set per band, adjusted by servo, no roll change |
| Welding process | High-frequency induction welding |
| Roll saving versus conventional | Above 90% |
| Exception | 100 × 100 mm needs the upper roll on the final open stand changed |
| Strip material | Q195, Q235B, Q355B, galvanized, mild, cold-rolled and hot-rolled |
| Coil ID / OD | 508–610 mm / 1200–2100 mm |
| Application | Structural tube |
Each line is built for one band; the band and the line configuration are confirmed in the quotation.
Line Configuration and Scope of Supply
The welding physics is the same as on any of our high-frequency lines: current concentrates at the open edges through skin and proximity effect, heats them to welding temperature, and squeeze rolls press them together to form the seam under pressure. The difference between this line and a conventional square tube mill sits in one unit, and everything else about the train is shared.
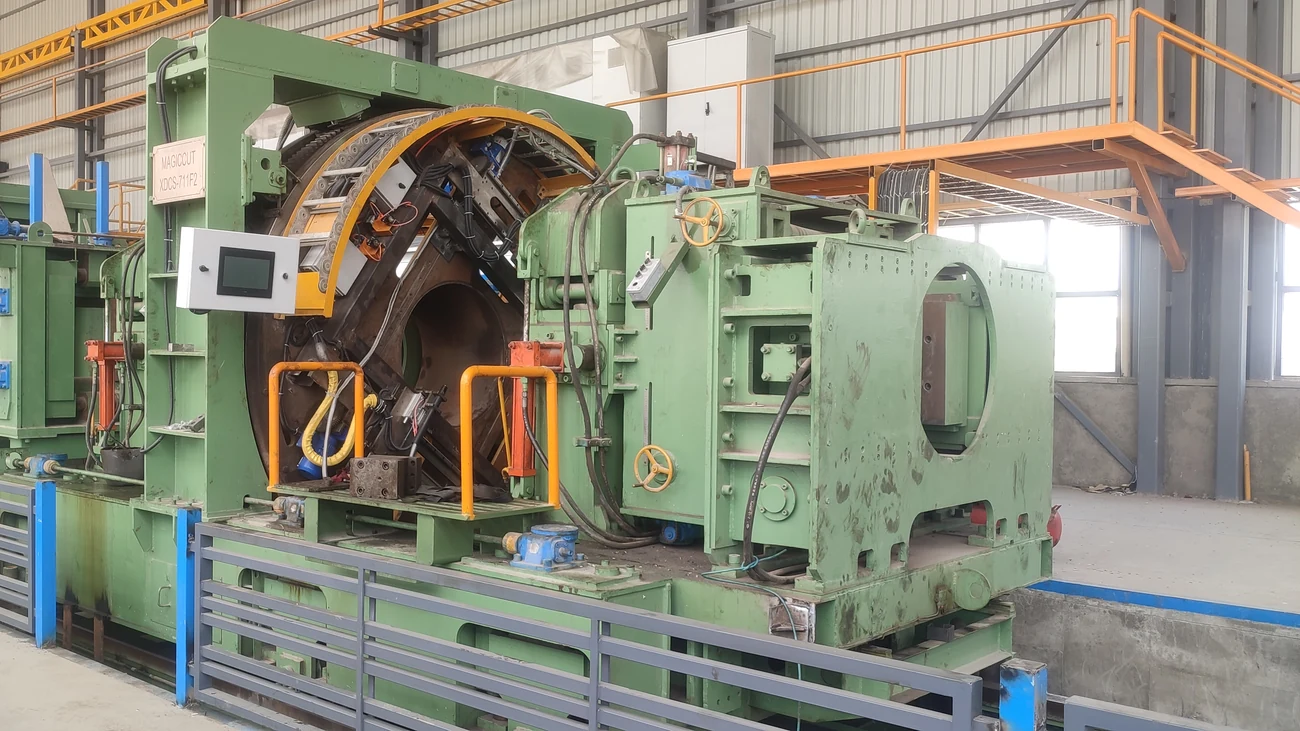
On a direct-forming build, a combined die set forms the square section directly, and the change from one size to the next is made by servo adjustment of that die set rather than by replacing it.
The rest of the line is the standard welded pipe train, from coil loading to cut-to-length:
- Coil car and expanding-mandrel uncoiler, tensioning the coil into the line.
- Five-roller leveller, flattening the strip before forming.
- Automatic shear-welder, joining coil to coil.
- Spiral accumulator, buffering strip so forming continues through a coil change.
- Forming and sizing mill — on this build, the combined die set with servo adjustment.
- High-frequency induction welder, sized to the section range.
- Flying saw, cutting to length at speed.
- PLC and variable-frequency control, tying speed, sequence and cut length together.
No filler metal is used.
On a conventional build, the strip is roll-formed progressively into shape and, if square section is wanted, formed round first and then sized into square; each size needs its own roll set, as on our tube mill & welded pipe production line.
Size Change, Roll Wear and Running Cost
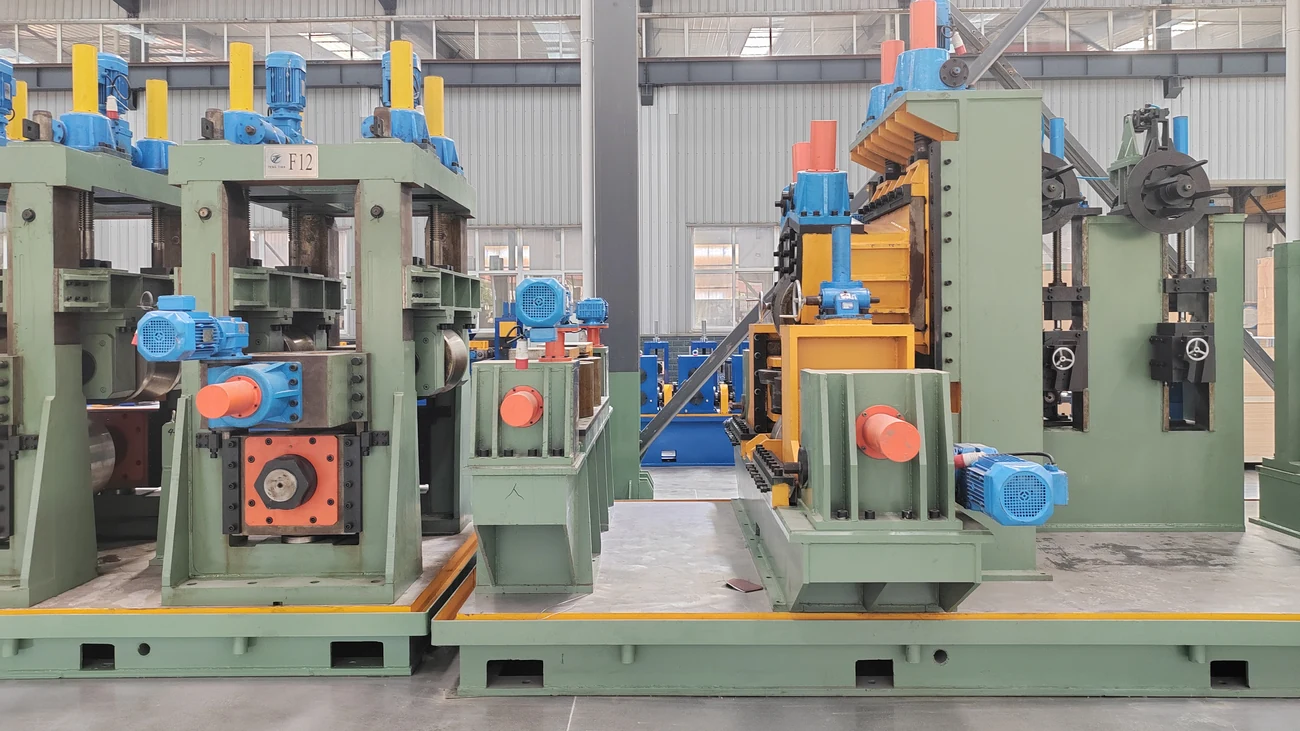
Roll saving is above 90%.
Changing size on a conventional square tube line costs a roll set and the downtime of the roll change; direct forming removes both.
The operator side of a size change still matters: on a conventional build a size change means a roll change, while on a direct-forming build it is a servo adjustment without a roll change. Either way the change crew needs training, and setup practice is what decides how much scrap a size change costs.
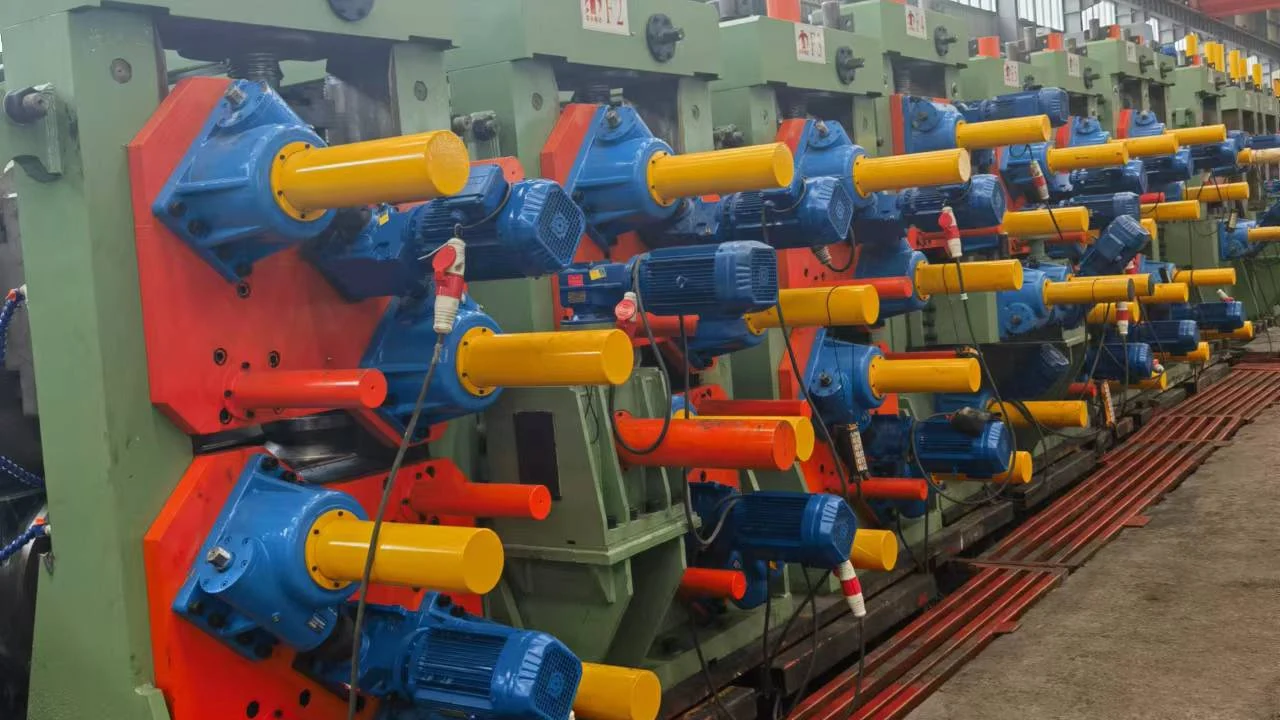
The saving comes from two mechanisms. Contact between the combined die and the strip is point contact rather than line contact, which reduces tooling wear; and because size is changed by servo adjustment, the tooling is not swapped out per size at all.
- The wear items on this line are the usual tube mill items:
- Saw blades and cutting tools, consumed against cutting volume.
- Impeders and induction coils, replaced against welding hours.
- Cooling water and emulsion, and hydraulic oil and grease — specification from us, purchase local.
- Forming tooling as a wear replacement item, backed by in-house CNC machining.
Applications
The line makes structural square and rectangular tube. Sizes already delivered to customers abroad are listed on the Direct Forming Square Tube Mill page.
Where responsibility sits follows the same division as our other welded pipe equipment. The mill controls welding power, seam alignment and squeeze; sizing sets dimensional accuracy; on high-end configurations, material yield can reach 93% or more.
Incoming strip grade, thickness tolerance and flatness stay with the buyer — and on a square section, incoming flatness shows up in corner definition rather than being absorbed.
Delivery, Installation and Training
Standard lines ship within 90 working days of the deposit, with plant-level customisation scheduled from our own manufacturing base.
The line is dismantled into units and shipped in containers: heavy frames are braced and secured, while precision parts and wear items travel in wooden cases together with a spare-parts pack.
Installation and commissioning are guided on site by our engineers, with online support behind them; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance.
Payment is 30% by T/T on signing, 65% by T/T before shipment and 5% after installation and commissioning, or by L/C at sight; prices are quoted ex-works (EXW).
Training on this line has one emphasis that a conventional mill does not. Setting a new size is a servo operation rather than a mechanical one, and the change crew needs dedicated training in size setting and die-change adjustment.
The other four operating steps are as on any of our tube mills: coil loading and threading, and shear-welding a coil join in time with the accumulator, need operator training; setting welder power, welding speed and squeeze needs process-level training; cutting and collecting is routine.
After handover, support is a reply from our after-sales team, online support, on-site dispatch when required, and direct spare-part shipment.
The company is certified to ISO 9001:2015, and the welded pipe equipment is CE marked under the EC Machinery Directive 2006/42/EC. The square tube production line is covered by a granted invention patent. The product standard the finished section is made to depends on the destination market and the buyer’s specification.
Square tube mill machine
Each square tube mill machine in the range is named by its largest section: HG100x100, HG150x150, HG200x200, HG250x250, HG300x300, HG400x400 and HG500x500. Rectangular tube of the same perimeter runs on the same machine, so the model is chosen by the largest square size and the thickest wall in the plan.
Watch This Line Running
Direct Forming Square Tube Mill 120×120 mm — No Roll Change
Direct Forming Square Tube Mill 150×150 mm — No Roll Change
Direct Forming Square Tube Mill 200×200 mm — No Roll Change
Direct Forming Square Tube Mill 400×400 mm — No Roll Change
 Roll Saving in Direct Forming
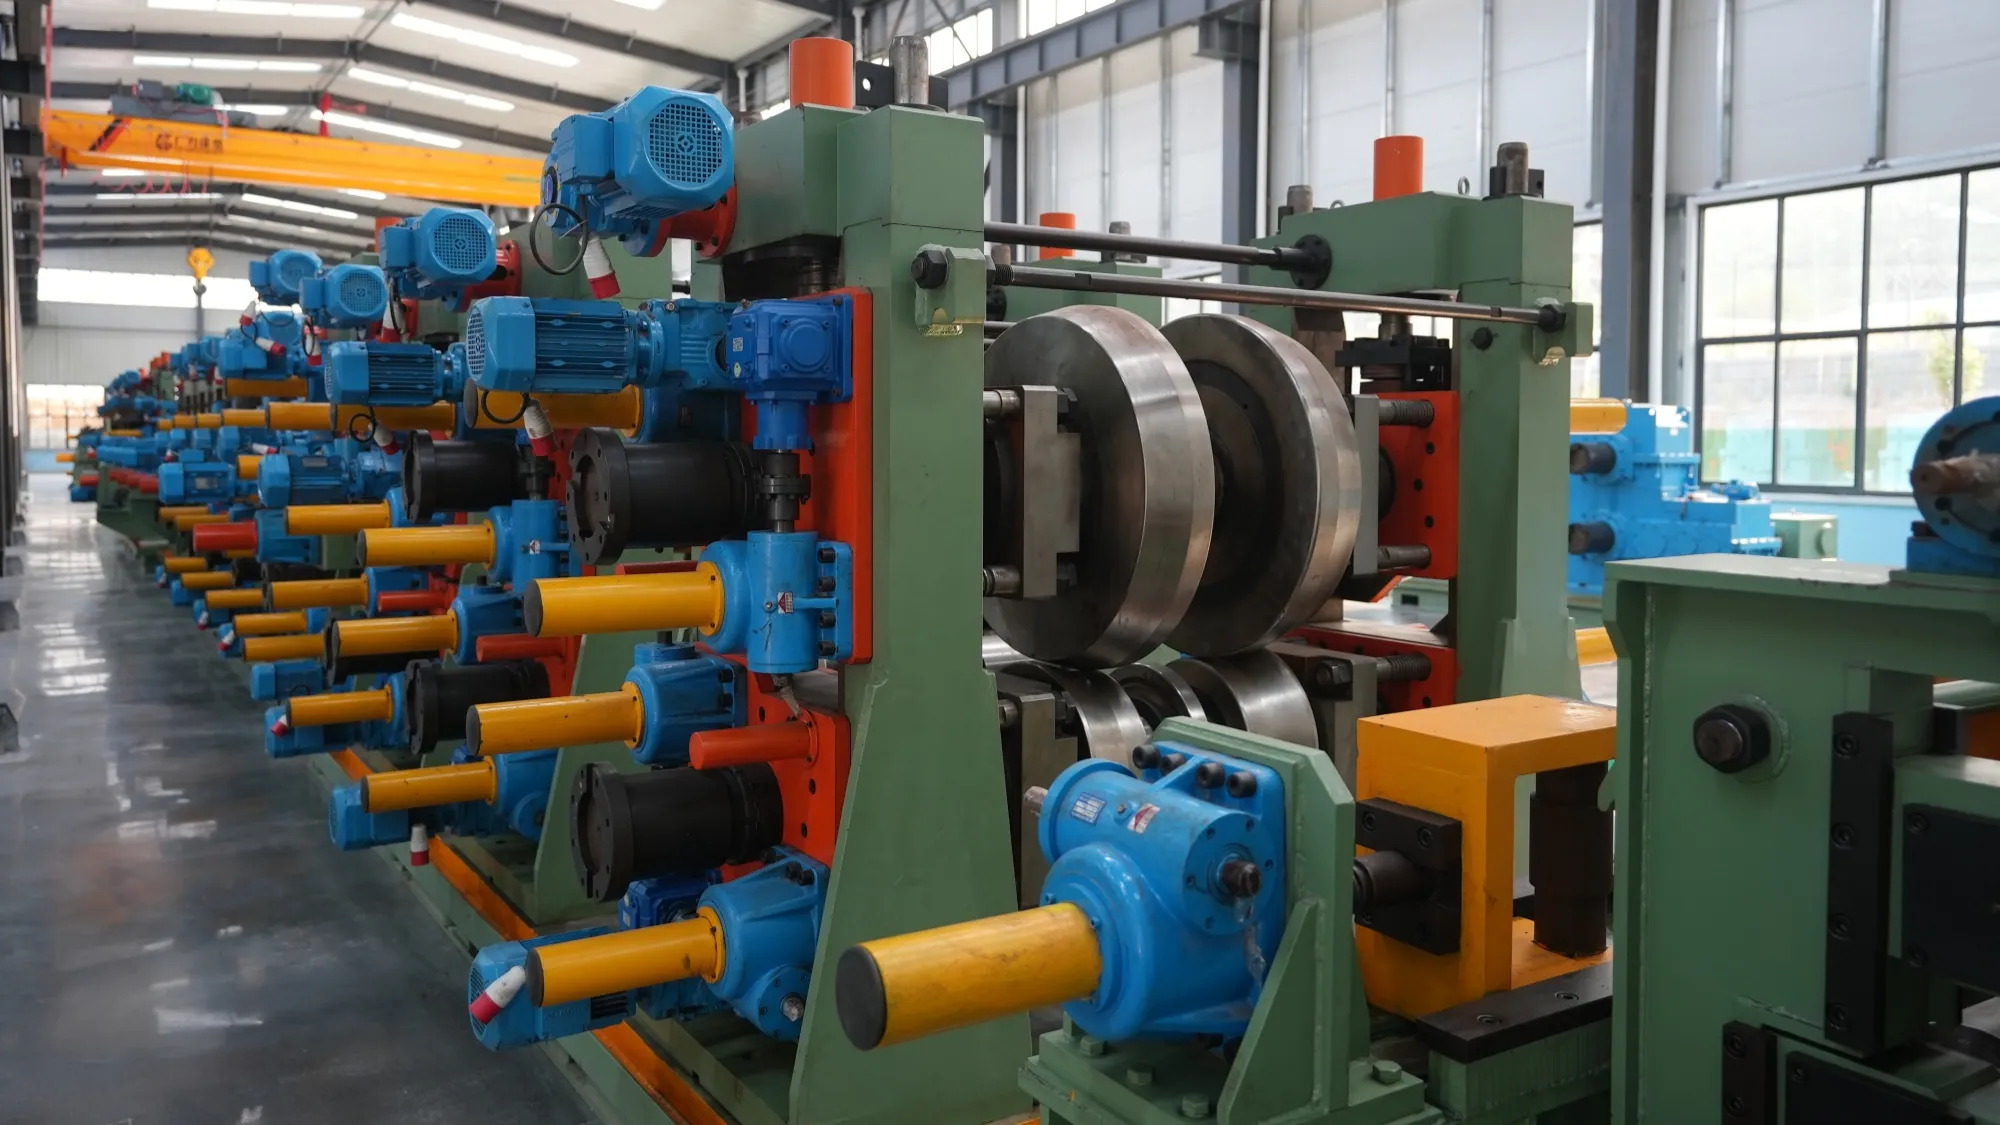 Two Routes to Square Section, Side by Side
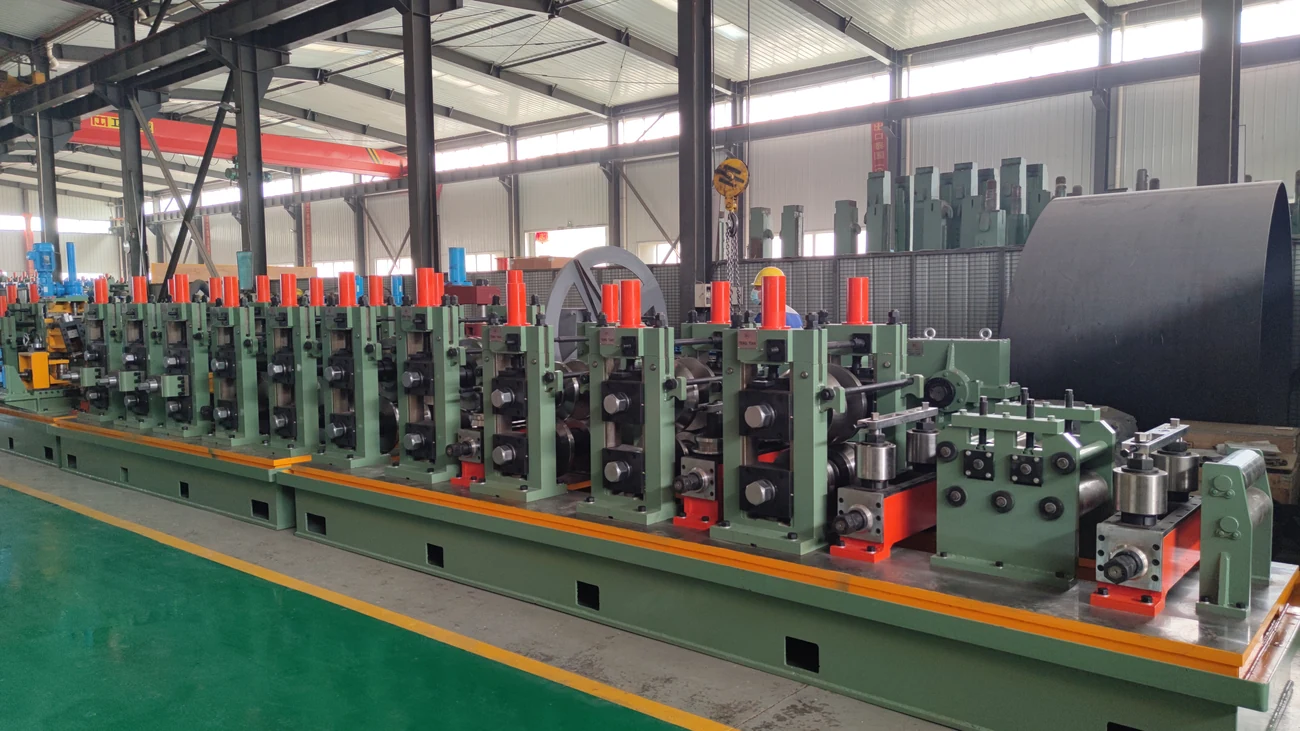 Direct Forming Square Tube Mill
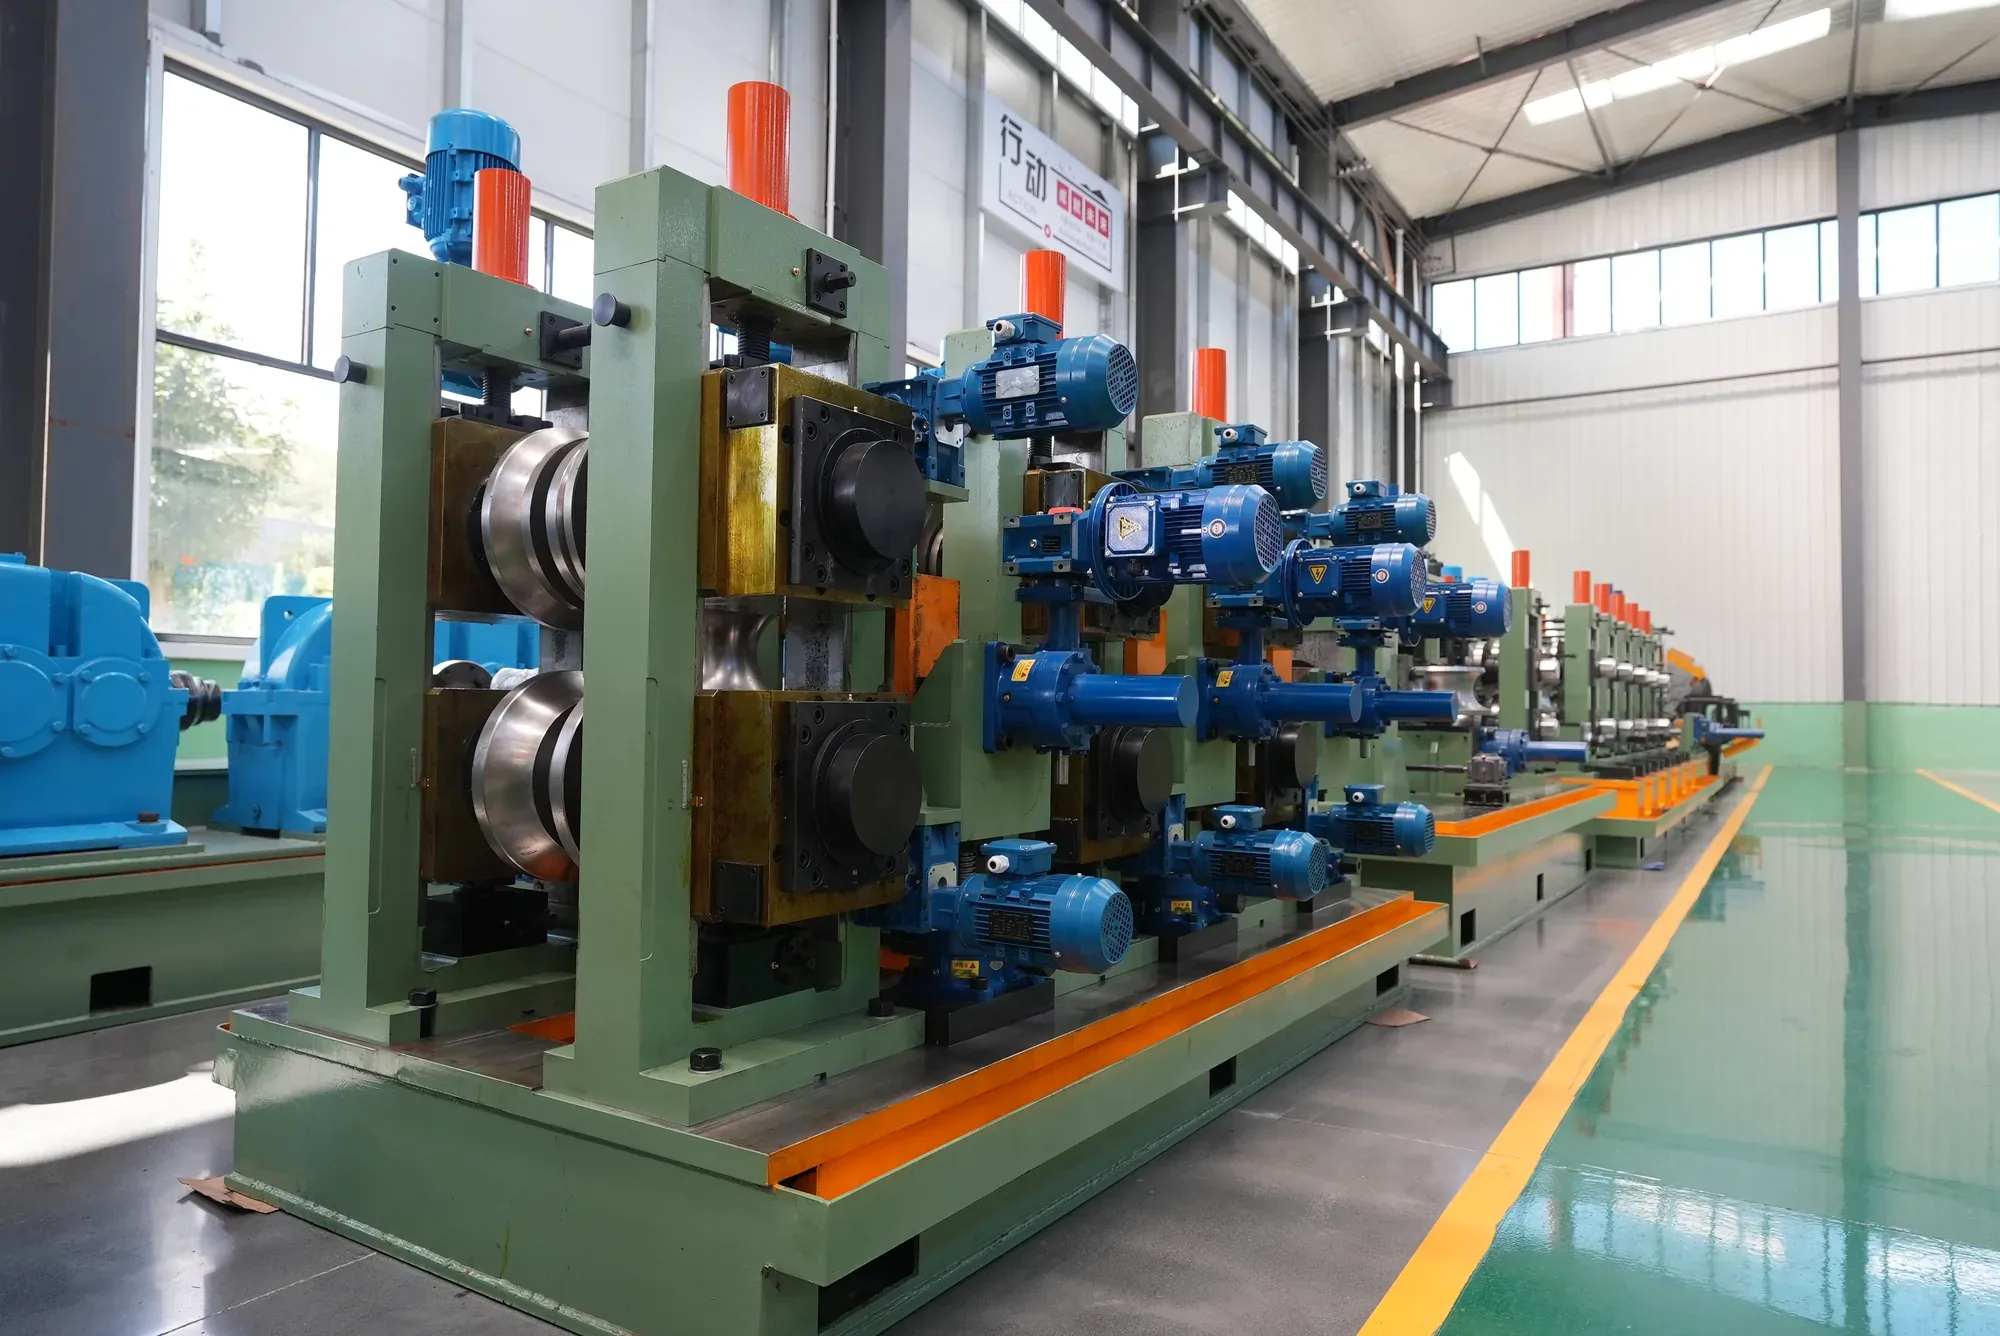 Welded Pipe Guide
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.