
Home › SSAW Spiral Welded Pipe Mill › What the Large-Diameter Tier Adds
In This Line
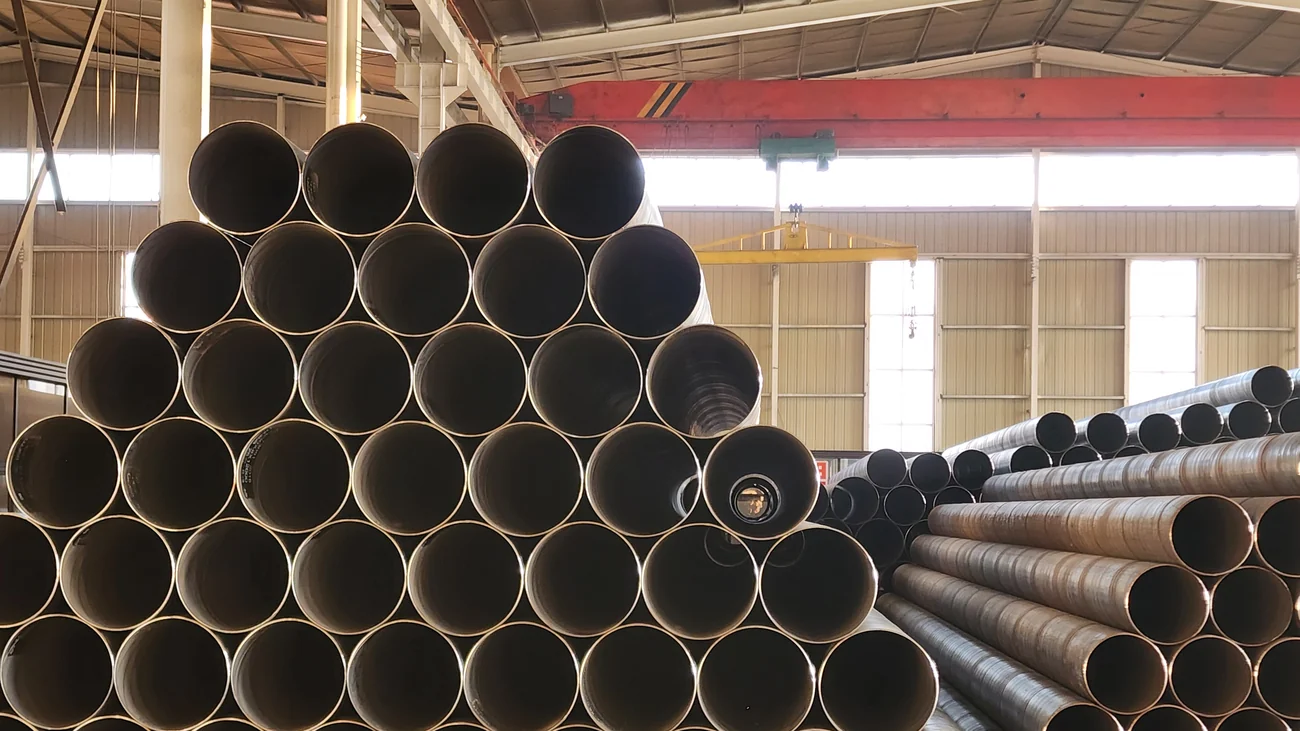
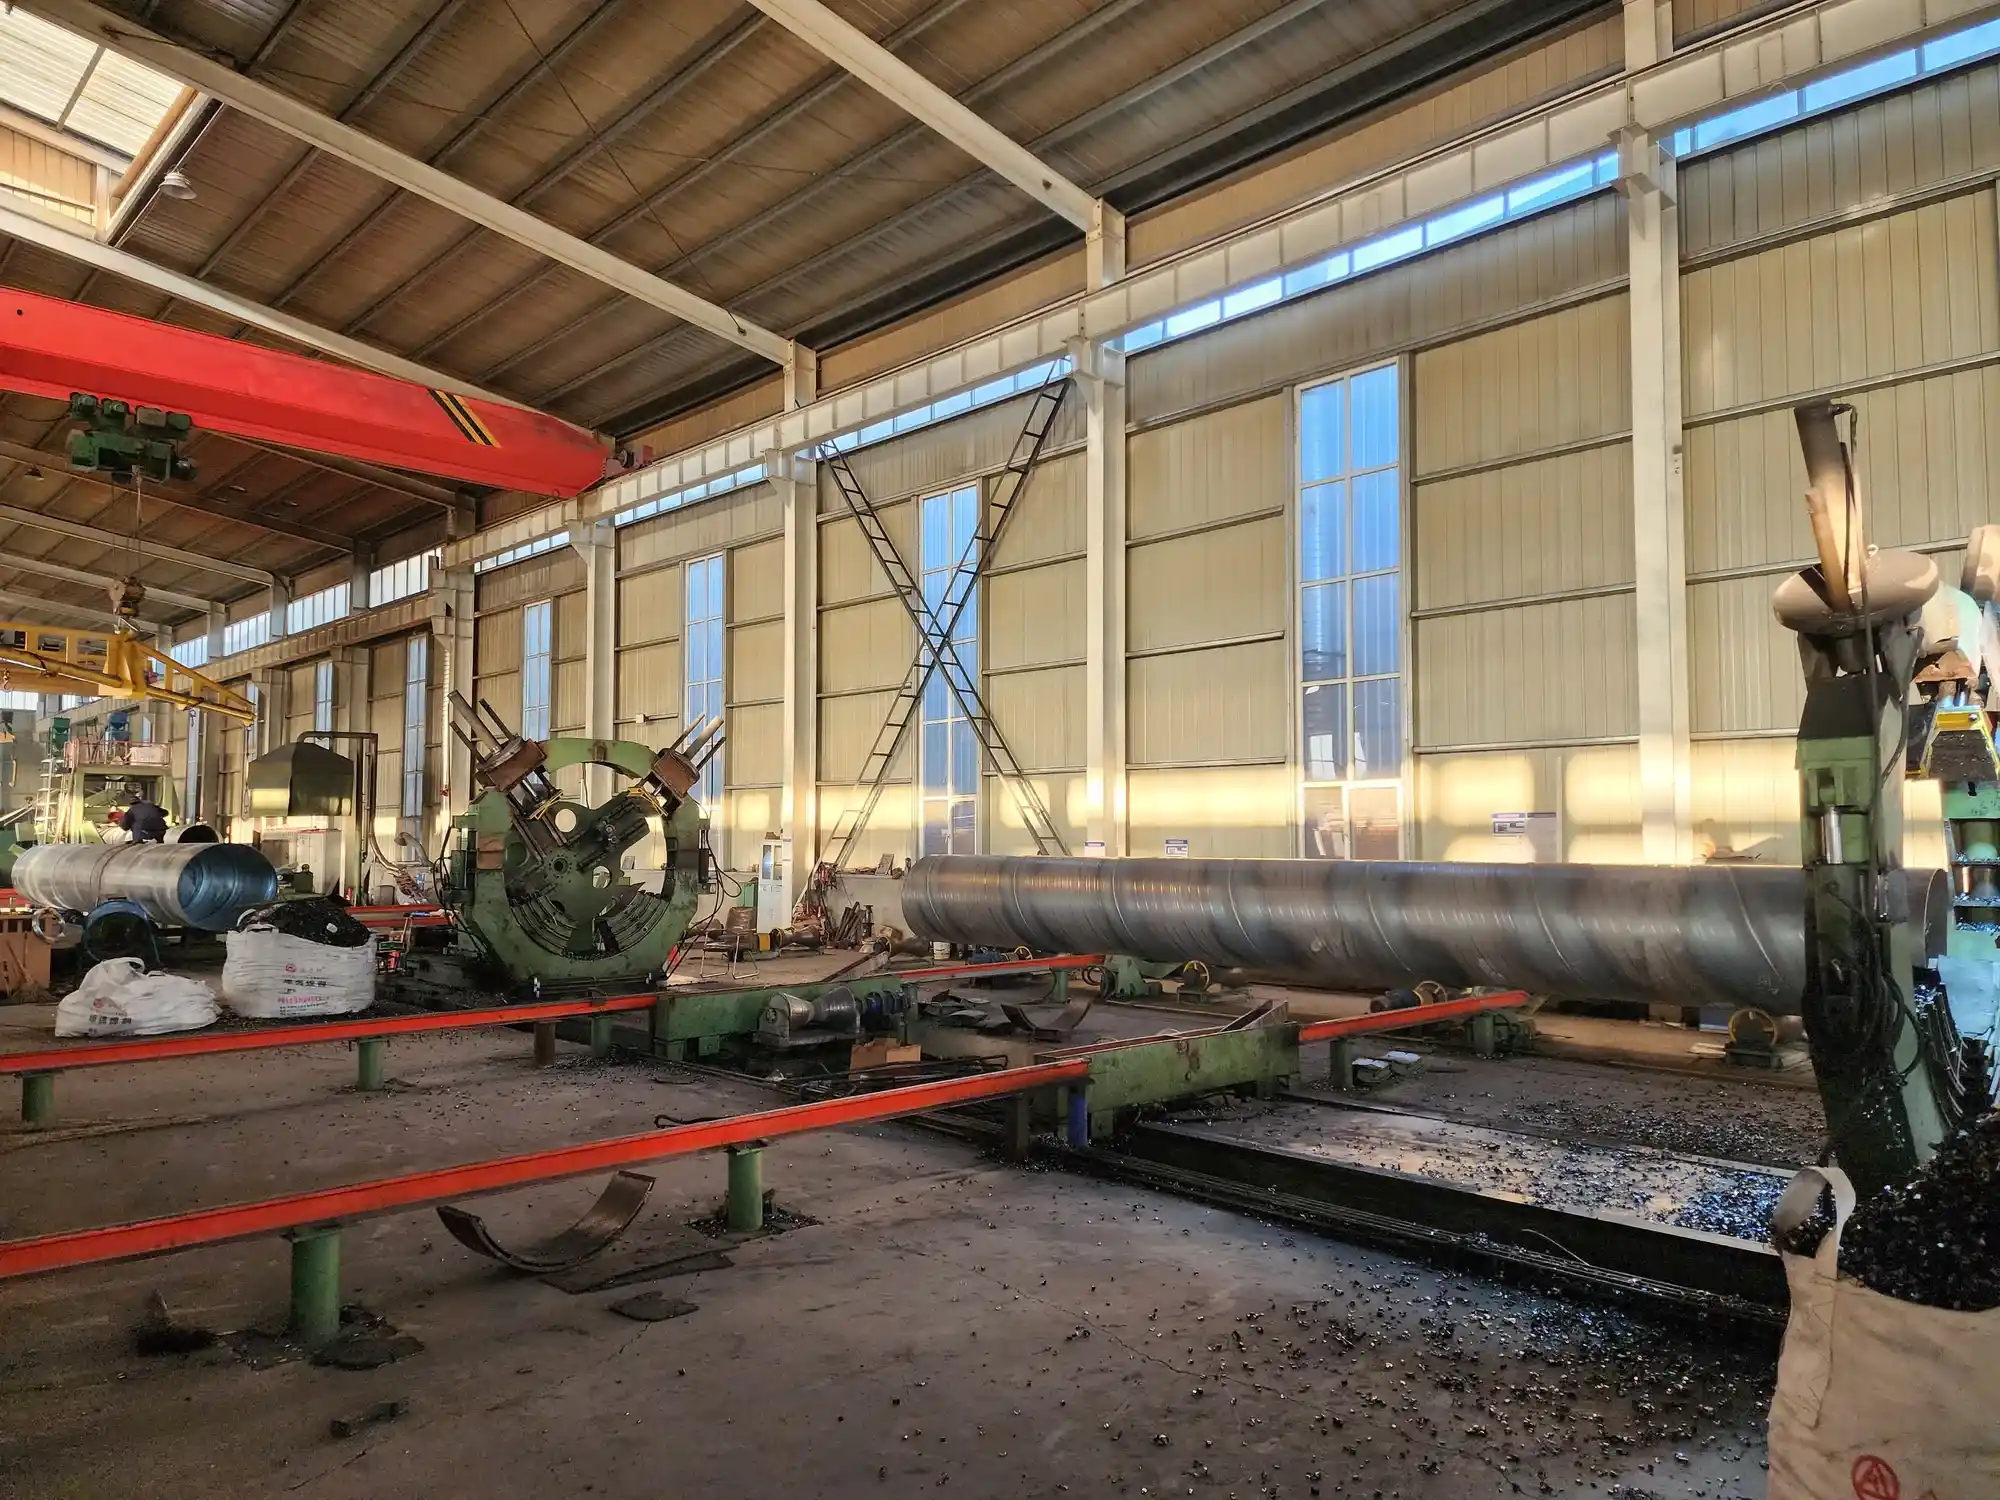
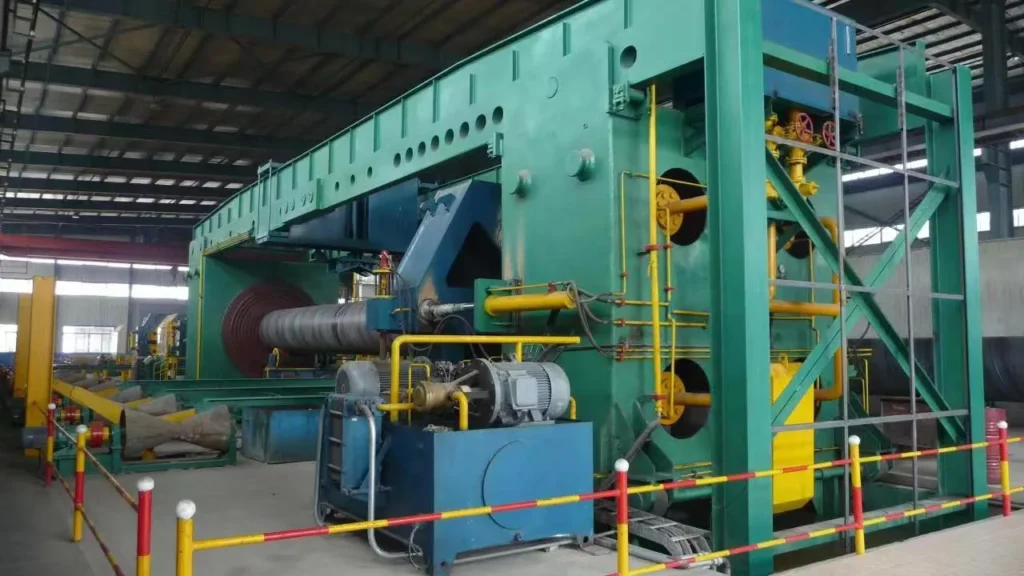
This forward-swinging spiral tube making machine makes Φ219–1620 mm × 5–16 mm pipe in 8–12 m lengths, up to 7.5 t per pipe, welded inside and out by submerged arc.
Technical Specification Table
Forward swinging spiral welding pipe unit
The line is a forward-swinging, centre-located unit that runs intermittently, forming by three-roll bending with external sizing.
| Parameter | Value |
|---|---|
| Pipe outside diameter | Φ219–1620 mm |
| Wall thickness | 5–16 mm |
| Pipe length | 8–12 m |
| Single-pipe weight | up to 7.5 t |
| Machine type | Forward-swinging, centre-located, discontinuous |
| Forming | Three-roll bending, external sizing |
| Forming angle | 39°–80° |
| Maximum pitch | 1900 mm |
| Delivery speed | 0.6–3 m/min |
| Welding speed | 0.5–3 m/min |
| Submerged-arc arrangement | Outer double / inner single |
| Main installed power | 300 kW |
| Welding power source | Lincoln DC-1500 × 2 + AC-1250 |
| Edge preparation | Edge miller, Φ500 cutter, 190 m/min, width 500–1250 mm, 2 × 22 kW |
| Flying cut-off | Plasma LGK-200 |
| Incoming strip width | 500–1250 mm, tolerance within ±5 mm |
| Incoming coil | OD Φ1500–1800 mm, ID Φ508–610 mm, up to 20 t |
| Feed direction | Left or right, confirmed with the buyer |
| Forming rolls (1#–7#) | GCr15, HRC56-60; bearing rollers Φ130 |
| Feed / levelling / pre-bending rolls | 42CrMo, HRC52-58 |
| Operative standards | GB/T 9711, API SPEC 5L |
| Output | ≈ 120 t per 8-hour shift |
| Manufacturing lead time | 150 days |
| Workshop required | 36 × 24 m, 32 t crane, 6.5 m hook height |
| Power / air supply | 220 / 380 V 50 Hz, compressed air 0.6 MPa |
Line Configuration and Scope of Supply
The full nine-stage sequence of the line, from uncoiling to inspection, is set out on the ssaw spiral welded pipe mill page. Against the Φ219–820 mm class, this class adds four things.
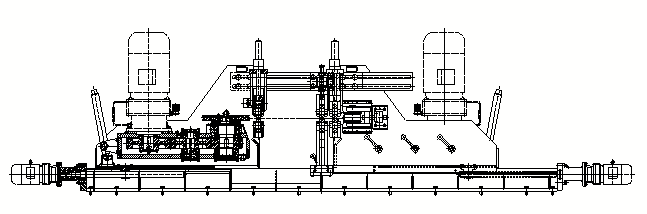
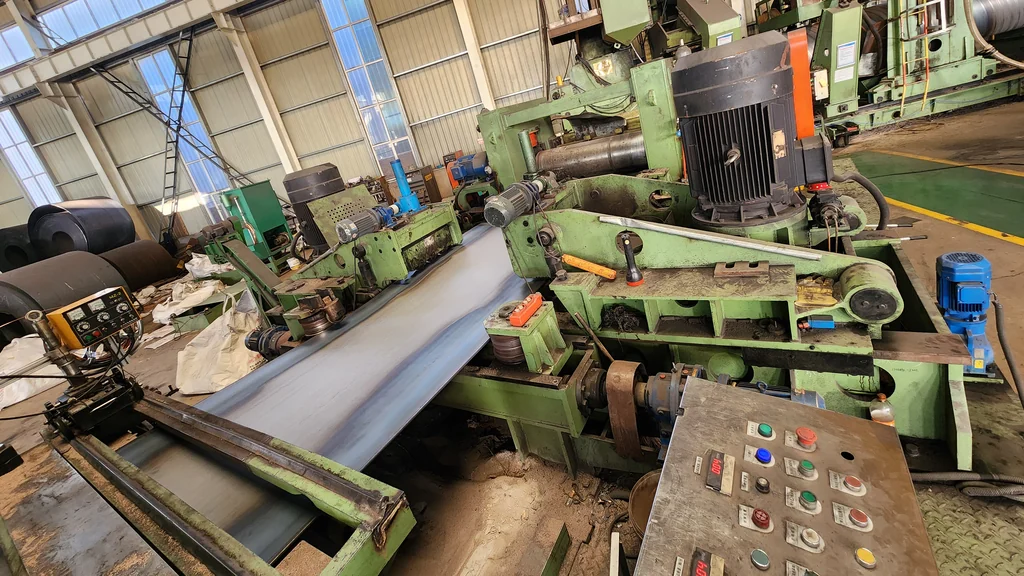
Edge milling instead of a disc shear. The edge milling machine runs a Φ500 cutter at up to 190 m/min across milling widths of 500–1250 mm, driven by two 22 kW motors under variable-frequency speed control, turning in forward milling.
Outer double, inner single submerged-arc welding, powered by Lincoln DC-1500 × 2 and AC-1250 units, instead of outer single, inner single.
Plasma flying cut-off on an LGK-200 instead of an LGK-160.
Off-line ultrasonic inspection in the finishing line, which the smaller class does not carry.
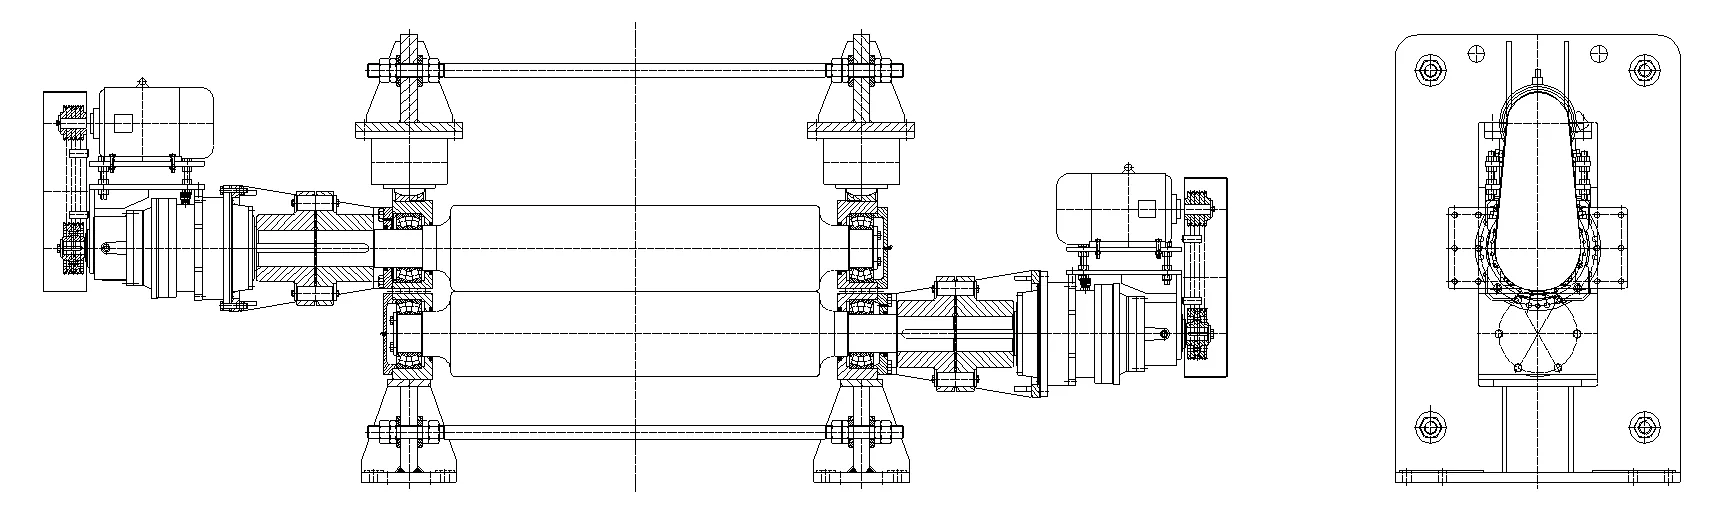
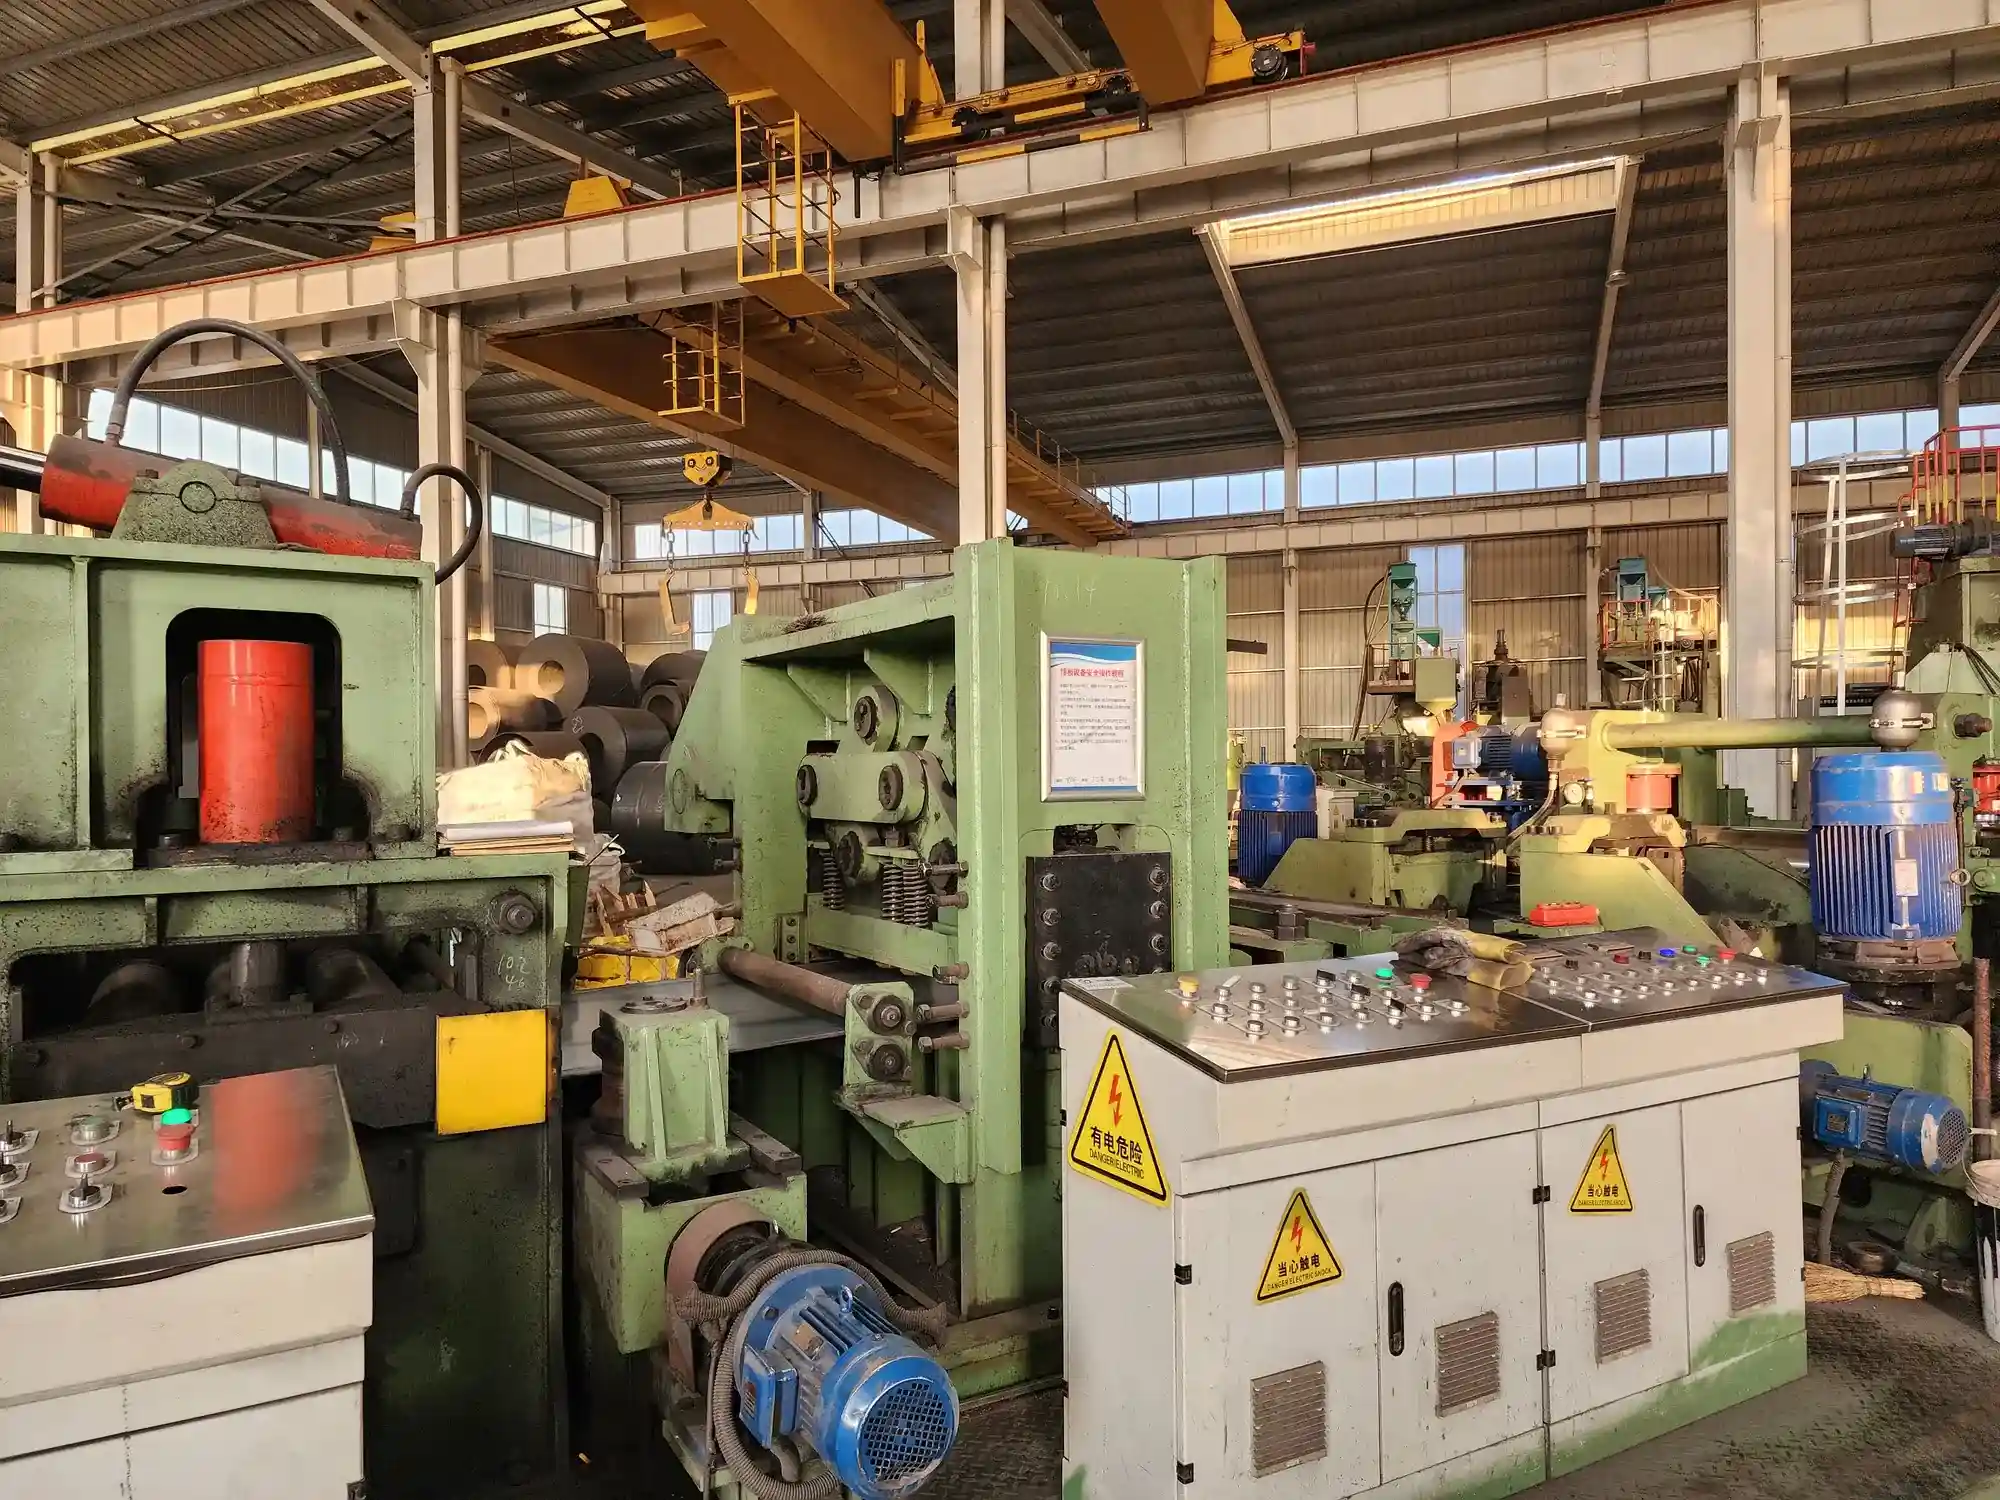
The delivery machine drives the line through a planetary reducer, forged Φ360 42CrMo rolls and two 15 kW drives, and guide plates with 42CrMo pre-bending rolls hardened to HRC52-58 curve the strip edges before forming. Flux is dried and magnetically separated before it covers the weld zone, and recovered afterwards.
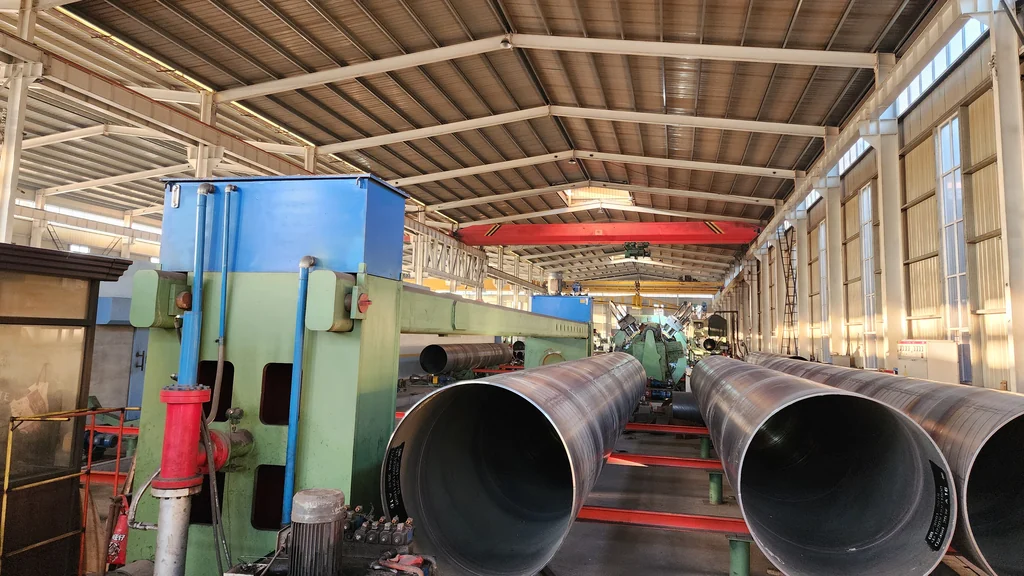
Finishing on this class runs slag removal, weld repair, pipe-end alignment, X-ray, hydrostatic test, off-line ultrasonic and end facing; each station’s rating and the standards it is accepted to are set out in the ssaw inspection chain.
Key bought-in components are listed by brand so they can be priced and checked independently: Lincoln welding power sources, Siemens PLC and motors, Delta drives, Schneider (partly CHINT) electrical components, Jiangsu Guomao cycloidal reducers, Jiangsu Tongli planetary reducers, Harbin or Wafangdian bearings, Beijing Huade hydraulic valves.
Flux drying and magnetic separation, the flux recovery units, the plasma cutter and the Lincoln power sources are listed as procured supporting equipment.
Size Change and Incoming Strip
Diameter is set by the forming angle — the front bridge swings between 39° and 80° — together with the strip width, which must arrive within ±5 mm; how a size change is made is covered in forming angle 39°–80°.
Rolls and key wear parts are machined at the works on its own CNC equipment, which is what makes continuous supply possible years after handover — the practical difference being that a replacement set ordered three years on matches the set delivered with the line, rather than matching whatever an outside shop can quote that quarter.
Applications and Output Examples
Spiral pipe mill for large diameter pipe
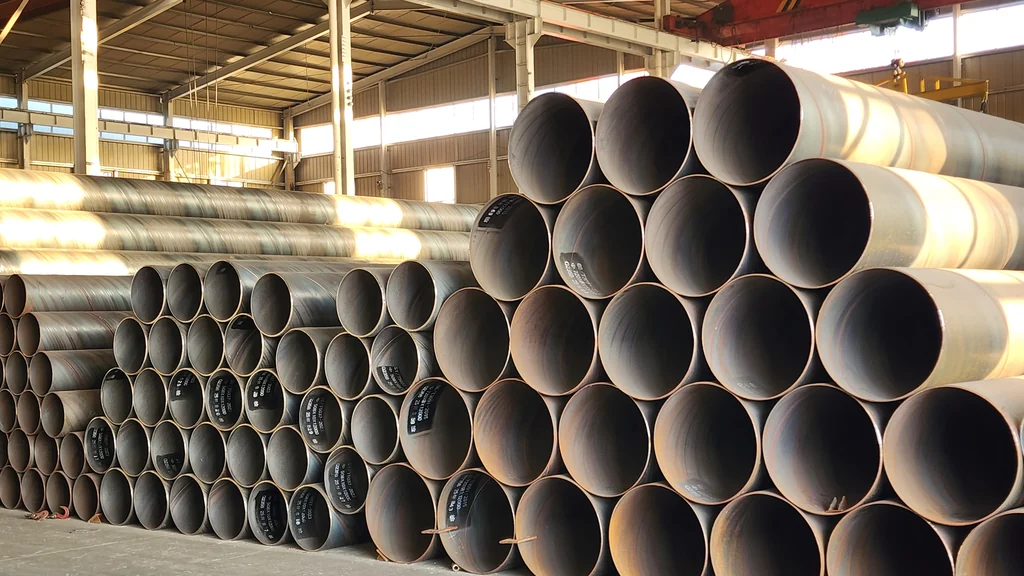
Pipe from this class goes into oil and gas transmission pipelines, low-pressure fluid, urban gas and water supply and drainage pipelines, and industrial structural pipe, made to GB/T 9711 or API SPEC 5L. The pipe production applications page covers these uses in more detail, and for straight-seam pipe up to Φ630 mm see our large-diameter hfw tube mill.
Output is about 120 tonnes per 8-hour shift, calculated on 1250 mm strip, 16 mm wall, Φ1620 mm pipe cut to 12 m — about 15 pipes of 7.5 t each.
Delivery, Installation and Training
Manufacturing lead time for this class is 150 days.
Lines are quoted ex-works (EXW); the buyer books and pays the freight. The finishing line includes 195 sets of test-bay bases, 47 sets of driven roller tables, 45 sets of idle roller tables and 45 suction units.
Installation and commissioning are guided on site by our engineers, with online support behind them; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance. Our engineers also train the operators.
The line is accepted on continuous production of two pipe sizes, four hours on each.
Watch This Line Running
SSAW Spiral Welded Pipe Mill — Φ219–1620 mm
From the Workshop
 SSAW or HFW
 X-Ray, Hydrostatic and Ultrasonic, Station by Station
 Changing Bore Without Changing Rolls
 GB/T 9711 for Spiral Welded Line Pipe
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.