
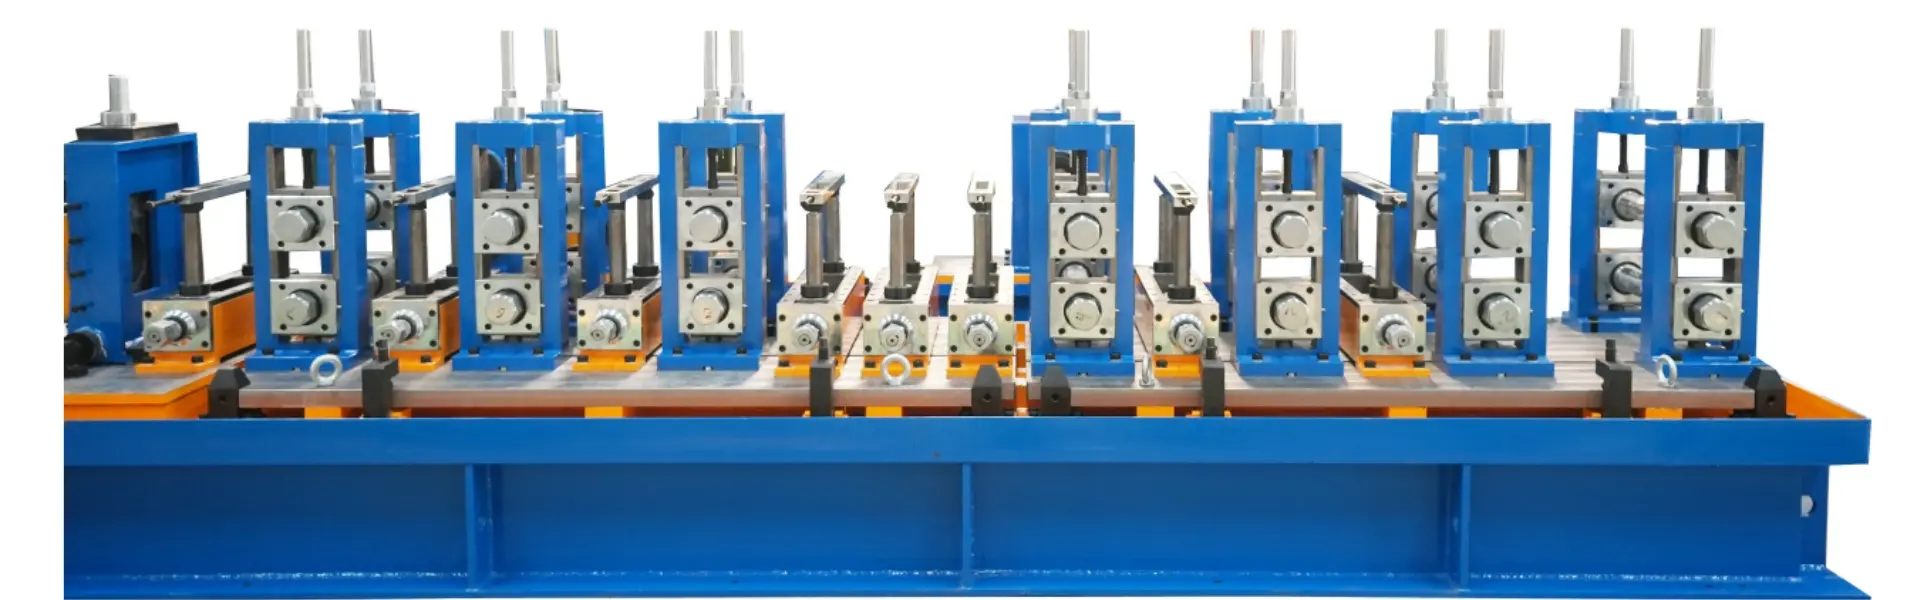
Small Diameter Tube Mill
In This Line
A small diameter tube mill from Tengtian is one of the first five of our twelve HFW diameter steps, HG32 through HG114, covering finished pipe from about Φ10 up to Φ114 mm. Each step is a separate machine size with its own specification, not a setting on one machine.
What Is a Small Diameter Tube Mill?
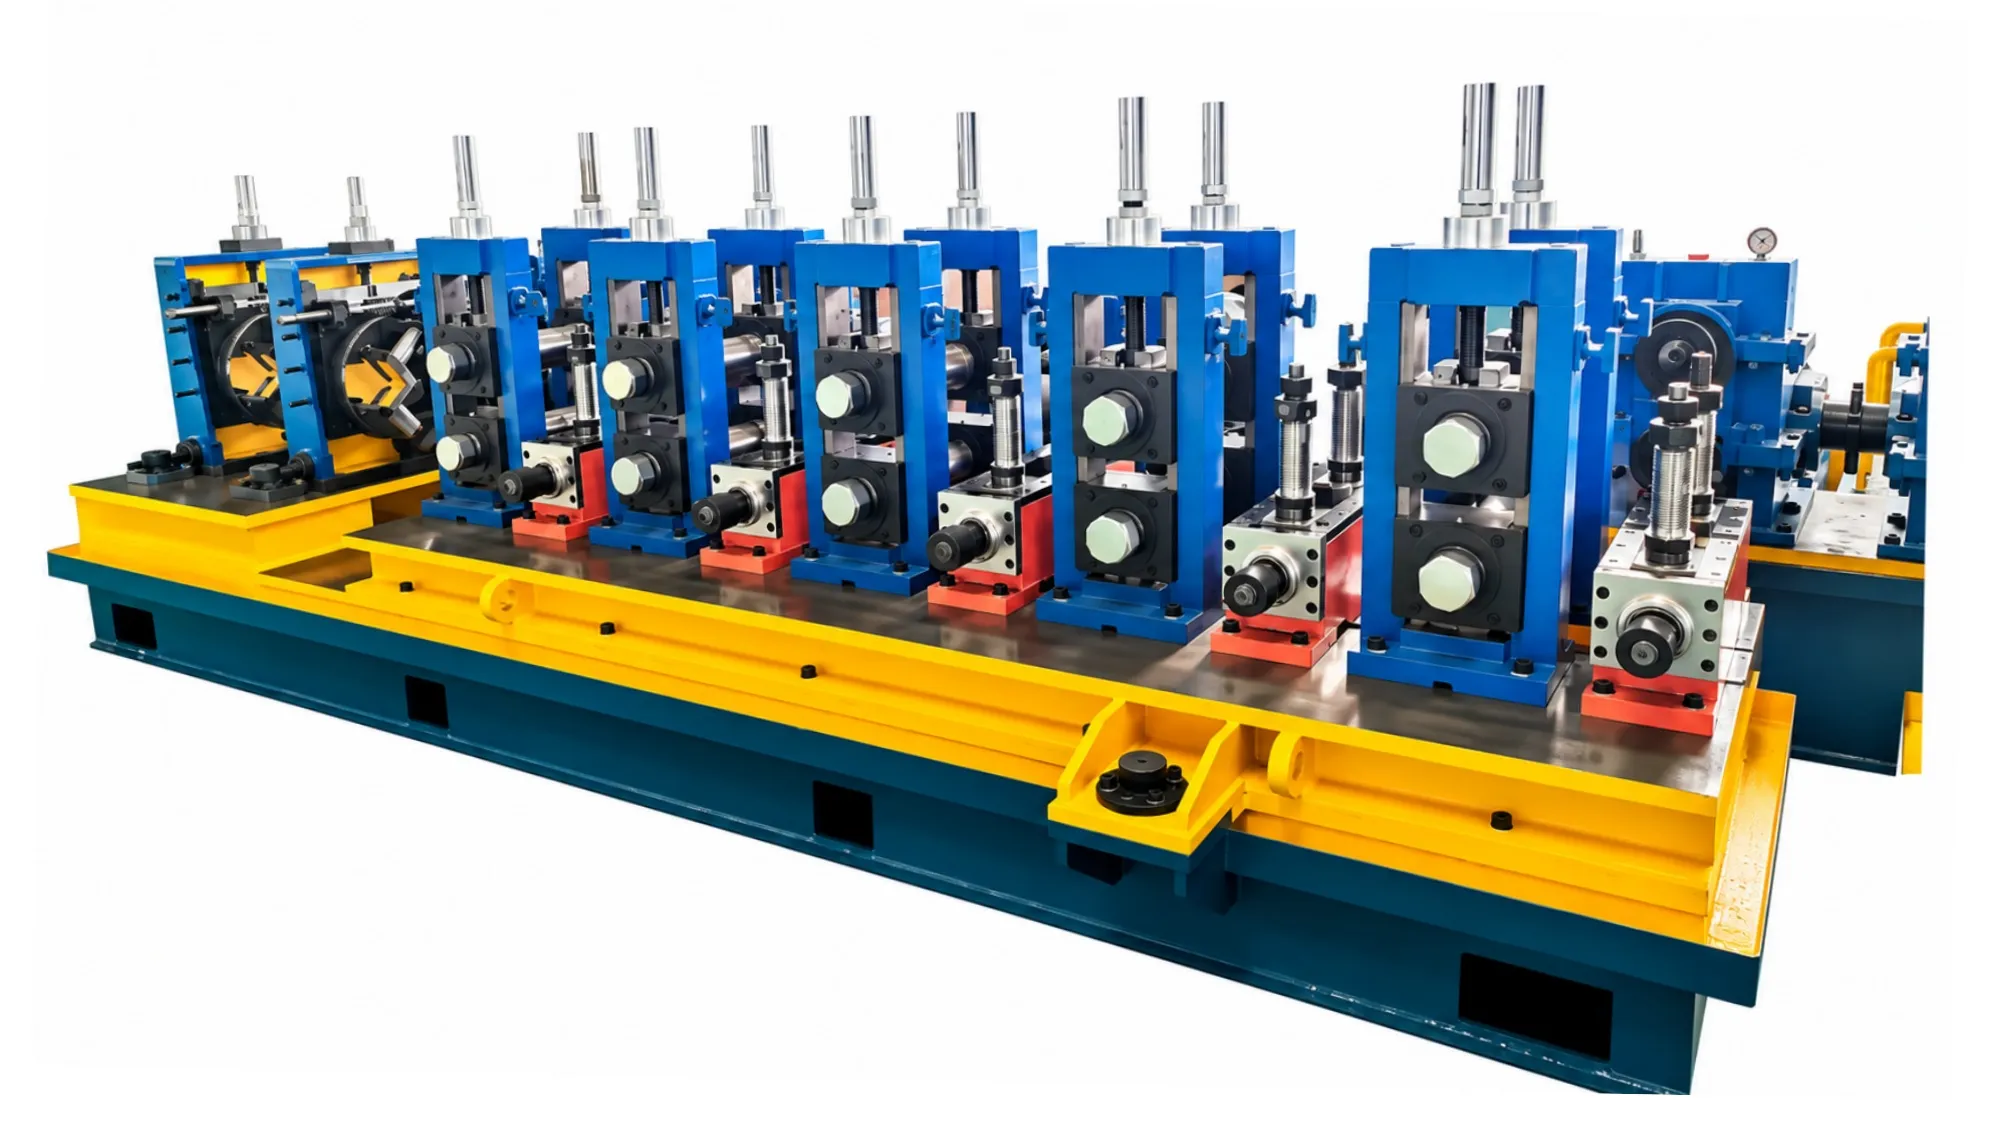
The whole product family runs HG32 to HG630 across twelve steps, finished outside diameter Φ10 to Φ630 mm, wall 0.5 to 16 mm. A high-frequency welded tube mill is a continuous forming, welding and sizing line. Coil goes in; it is uncoiled, roll formed, welded by high-frequency induction, sized and cut, and straight-seam welded pipe — round, square or rectangular — comes out. These mills use W forming, so one line makes both round and square pipe, with a full or half roll set changed between shapes and sizes.
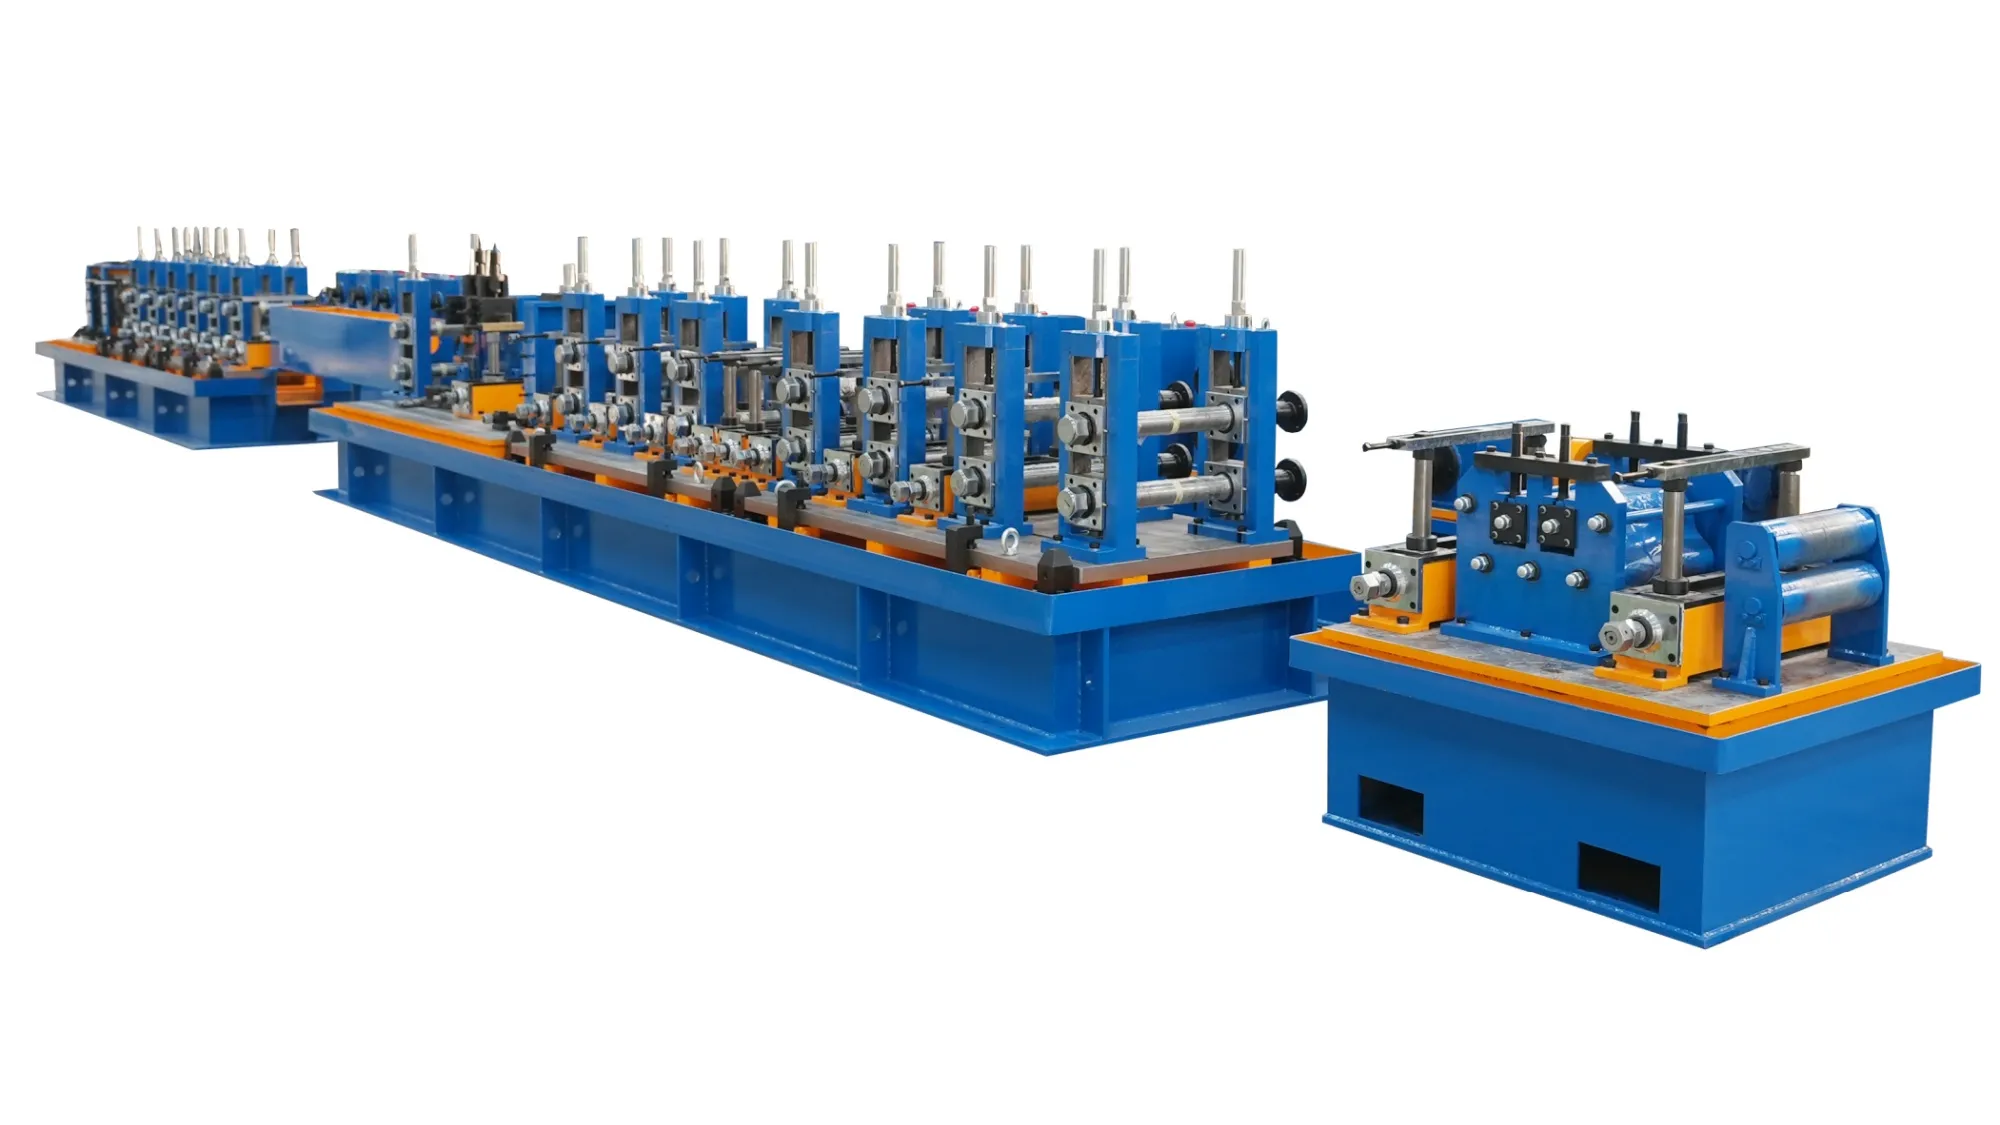
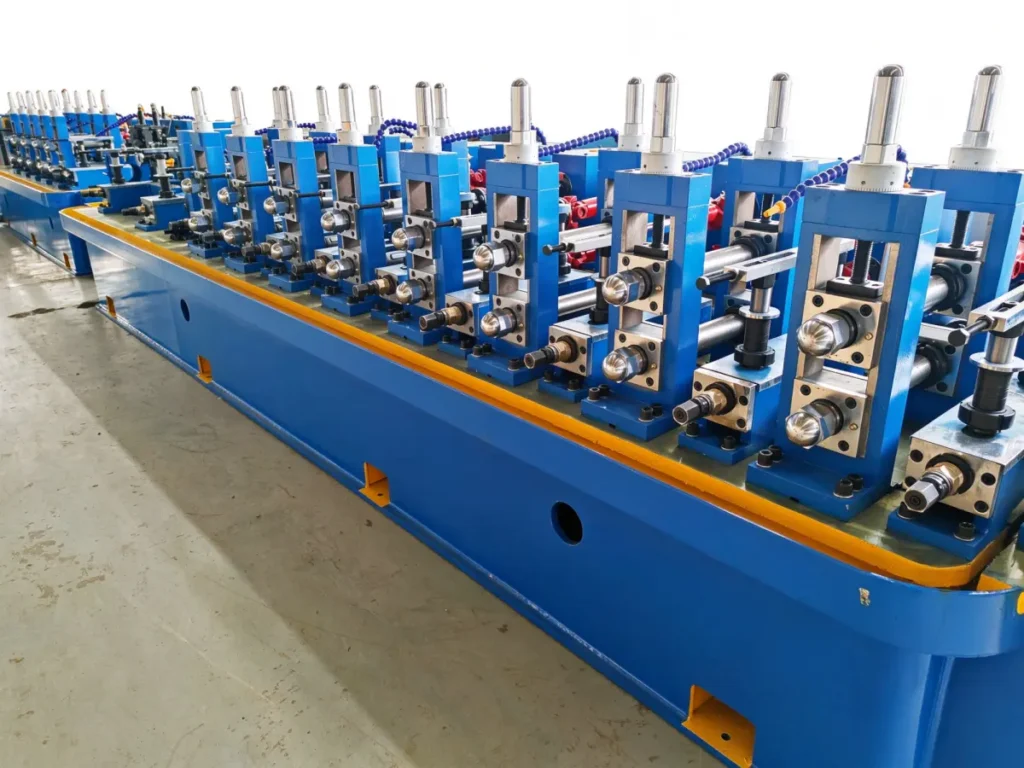 HG32 HFW Tube MillThe first of the twelve model steps and the tube mill for 32mm pipe and below: Φ10 – Φ32 mm round pipe and 10×10 – 25×25 mm square section, on a 150 kW high-frequency welder.See the line →
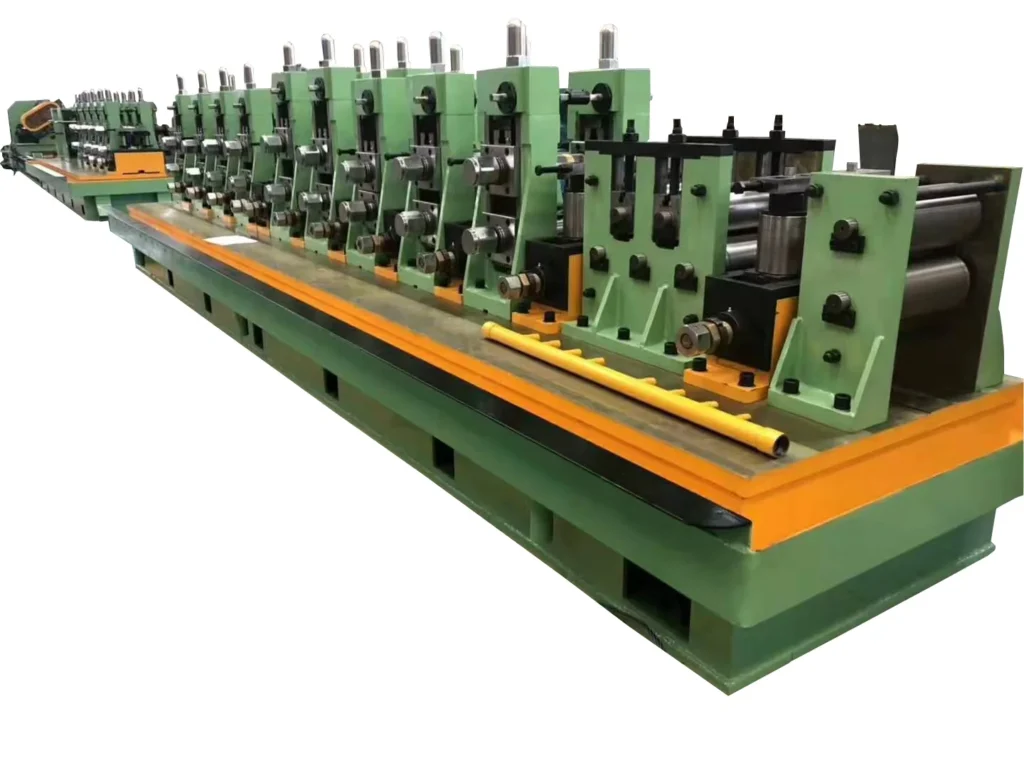 HG50 HFW Tube MillThe second of the twelve model steps, a 16–50.8 mm tube mill: Φ16 – Φ50.8 mm round pipe and 12×12 – 40×40 mm square section, on a 200 kW high-frequency welder.See the line →
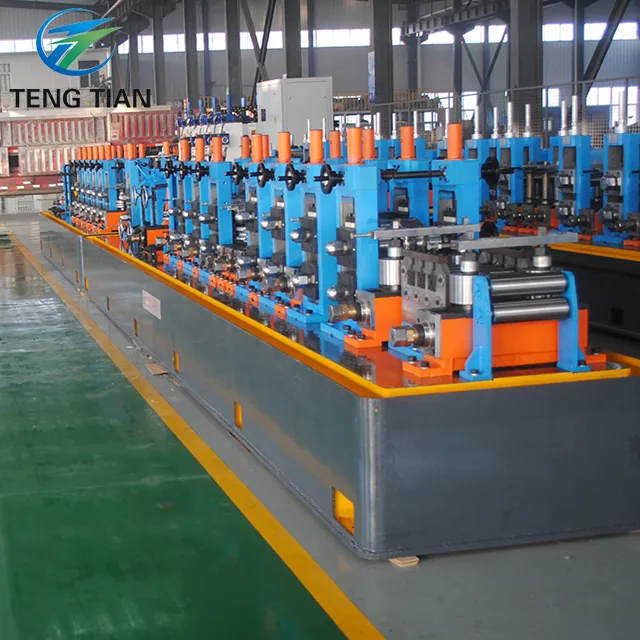 HG76 Tube Mill Line for Φ25–76 mm PipeThe third of the twelve model steps, a 25–76 mm tube mill: Φ25 – Φ76 mm round pipe and 20×20 – 60×60 mm square section, on a 250 kW high-frequency welder.See the line →
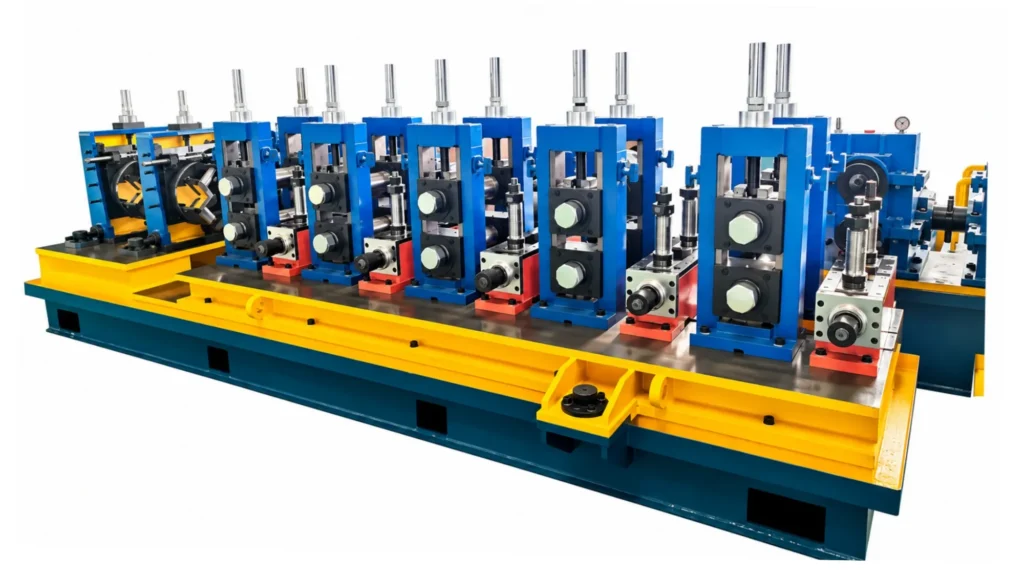 HG89 HFW Tube MillThe fourth of the twelve model steps, a 32–89 mm tube mill: Φ32 – Φ89 mm round pipe and 25×25 – 70×70 mm square section, on a 300 kW high-frequency welder.See the line →
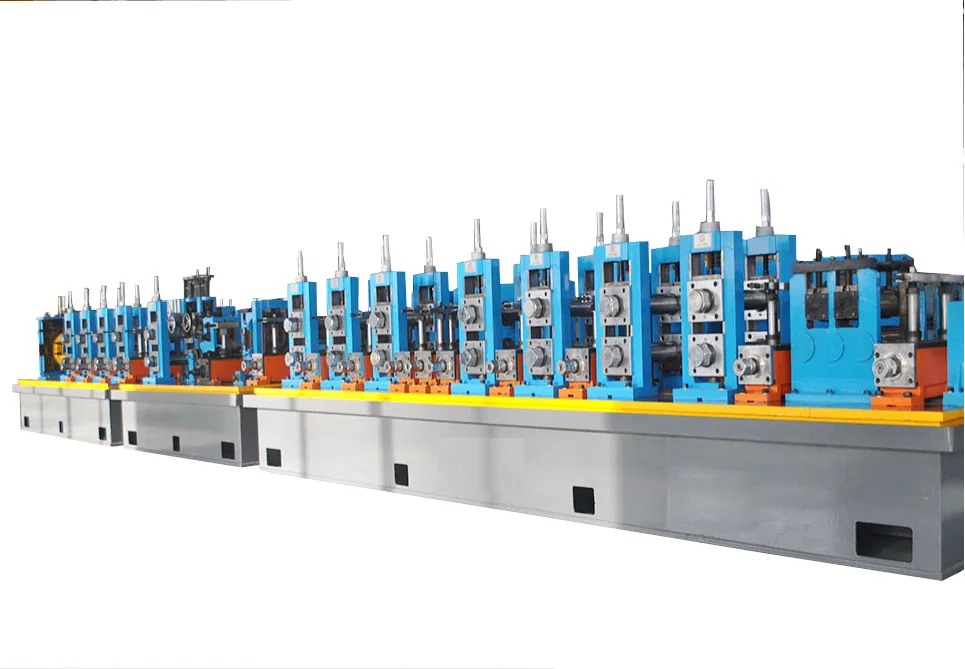 HG114 HFW Tube MillThe fifth of the twelve model steps, a 45–114 mm tube mill: Φ45 – Φ114 mm round pipe and 35×35 – 90×90 mm square section, on a 300 kW high-frequency welder.See the line →
The small-diameter end is the first five of those twelve steps. Their diameter windows are HG32 at Φ10–32 mm, HG50 at Φ16–50.8 mm, HG76 at Φ25–76 mm, HG89 at Φ32–89 mm and HG114 at Φ45–114 mm.
Note that these windows overlap rather than tile. HG76 starts at Φ25 mm, inside the HG50 window, and HG89 starts at Φ32 mm, inside both. Choosing a step is therefore not a matter of finding which band a diameter falls into — several will contain it — but of matching the whole intended product range to one machine.
Line Units, Model Windows and Configuration
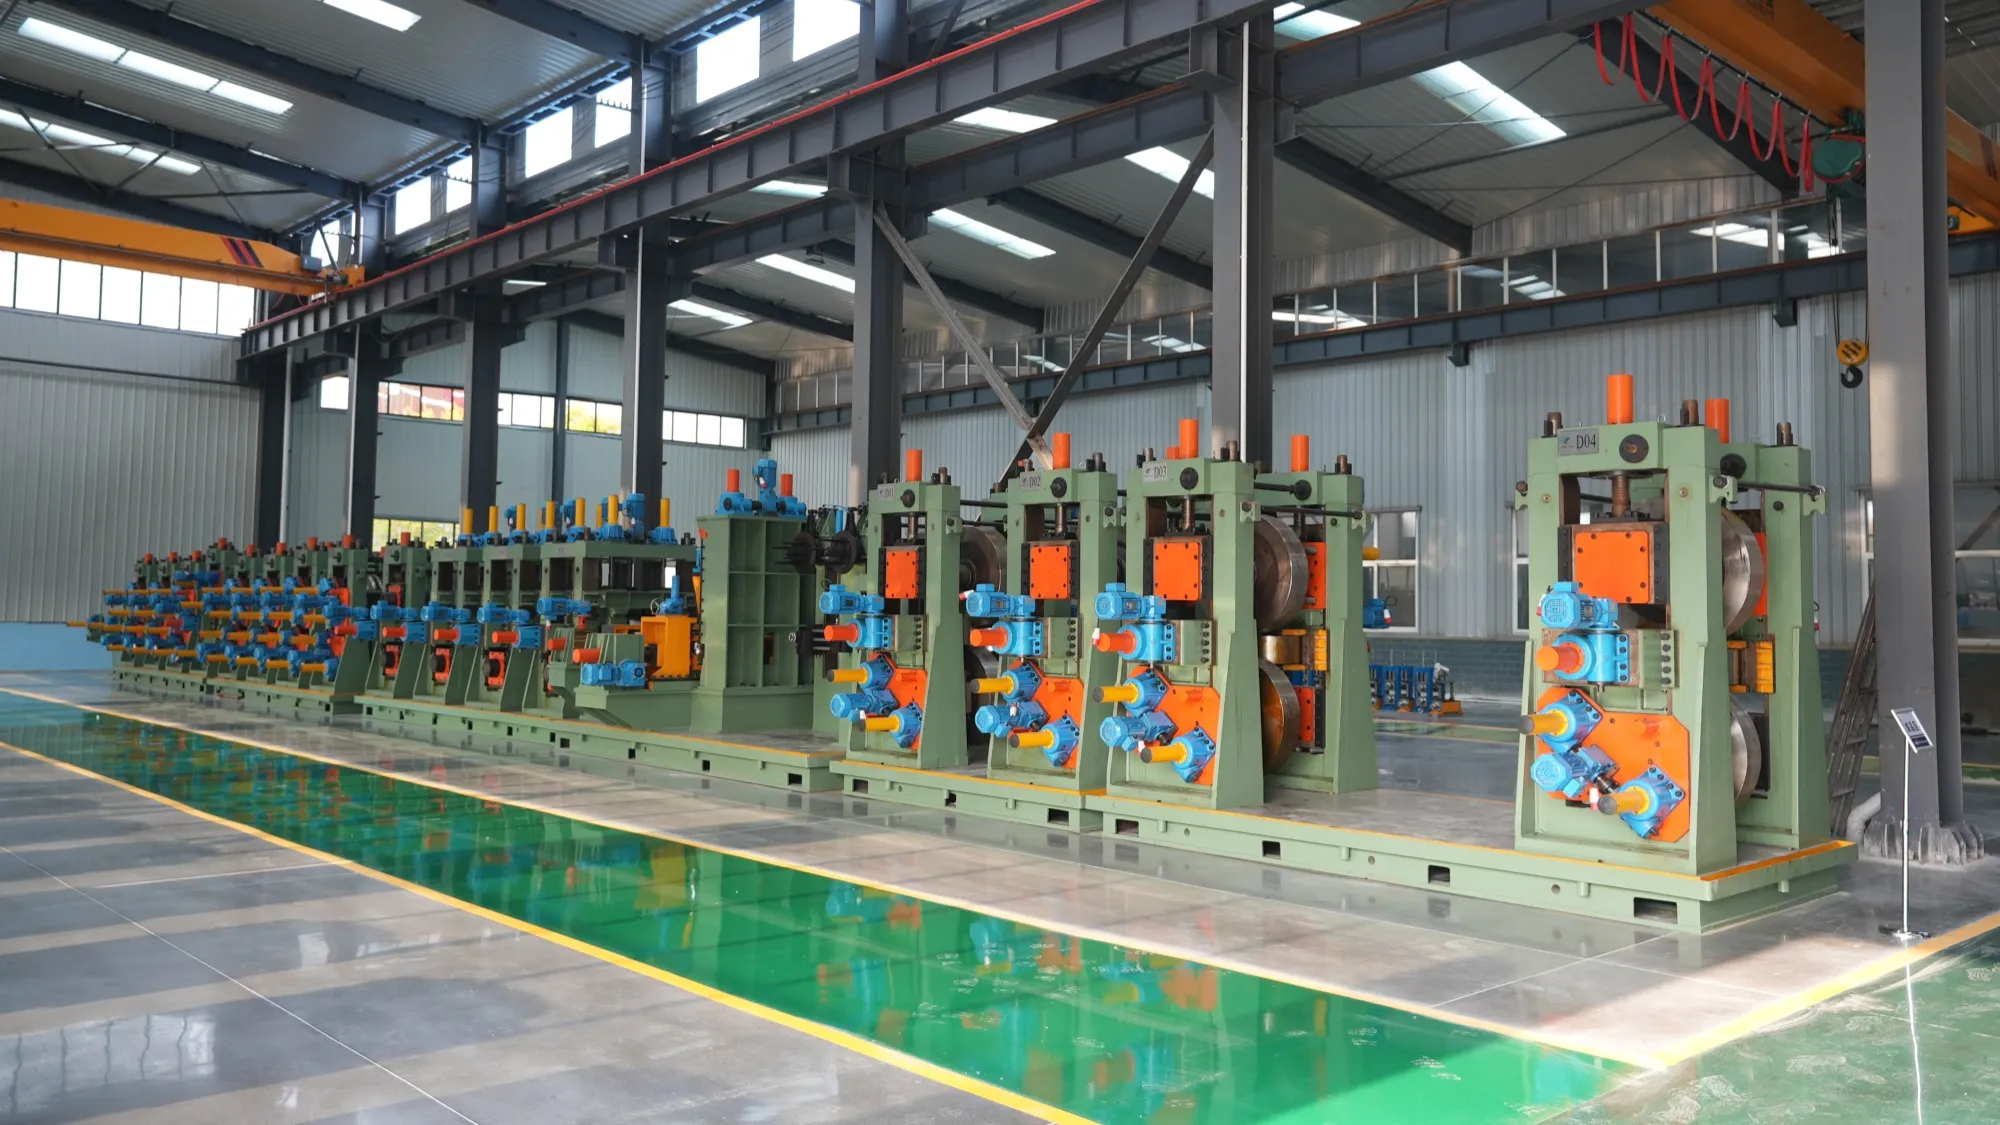
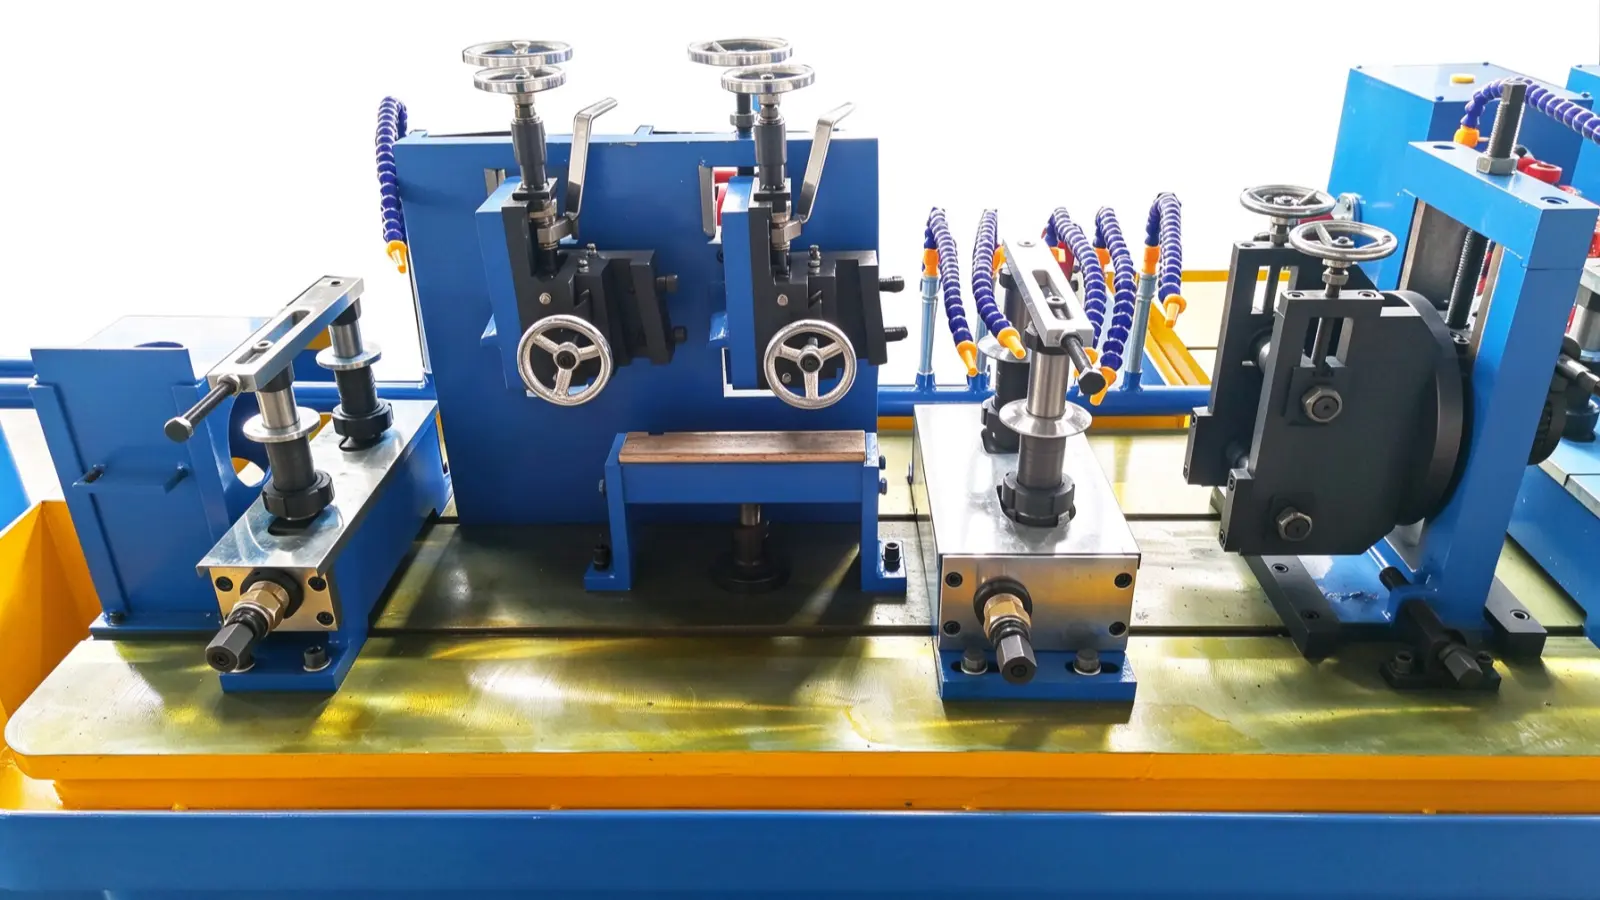
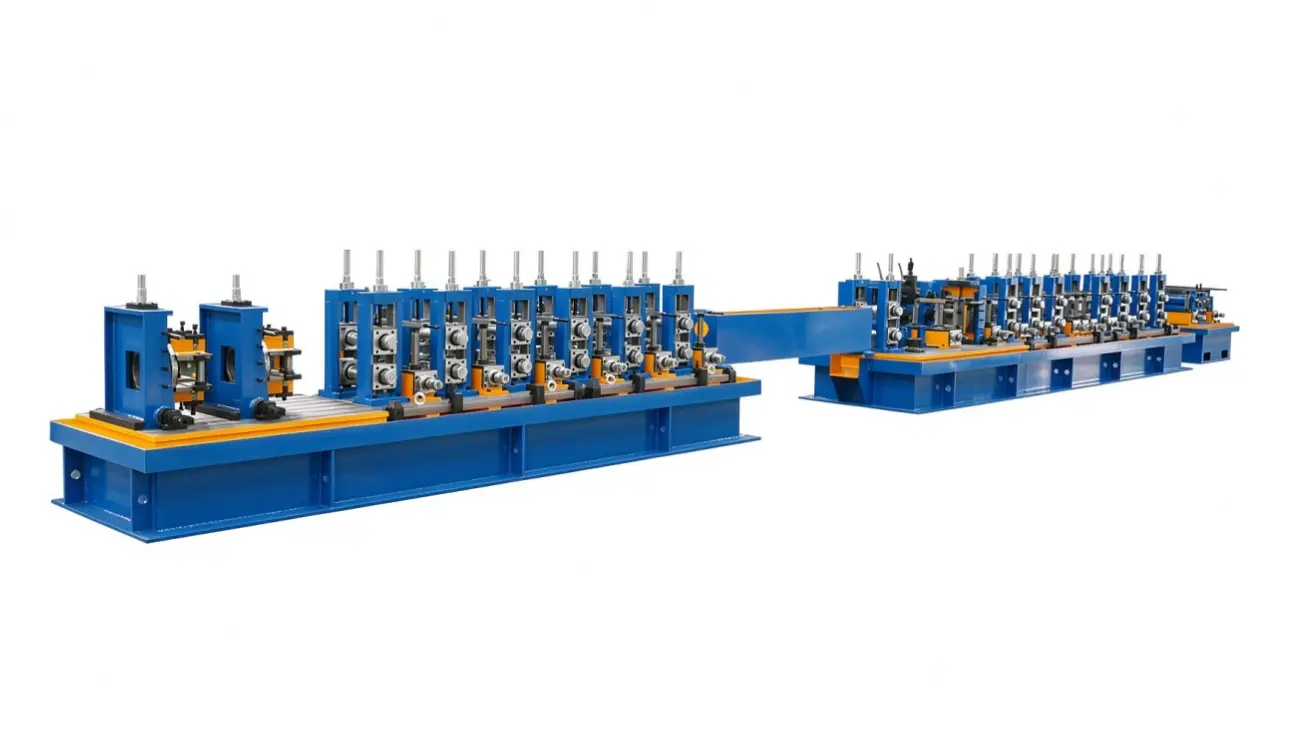
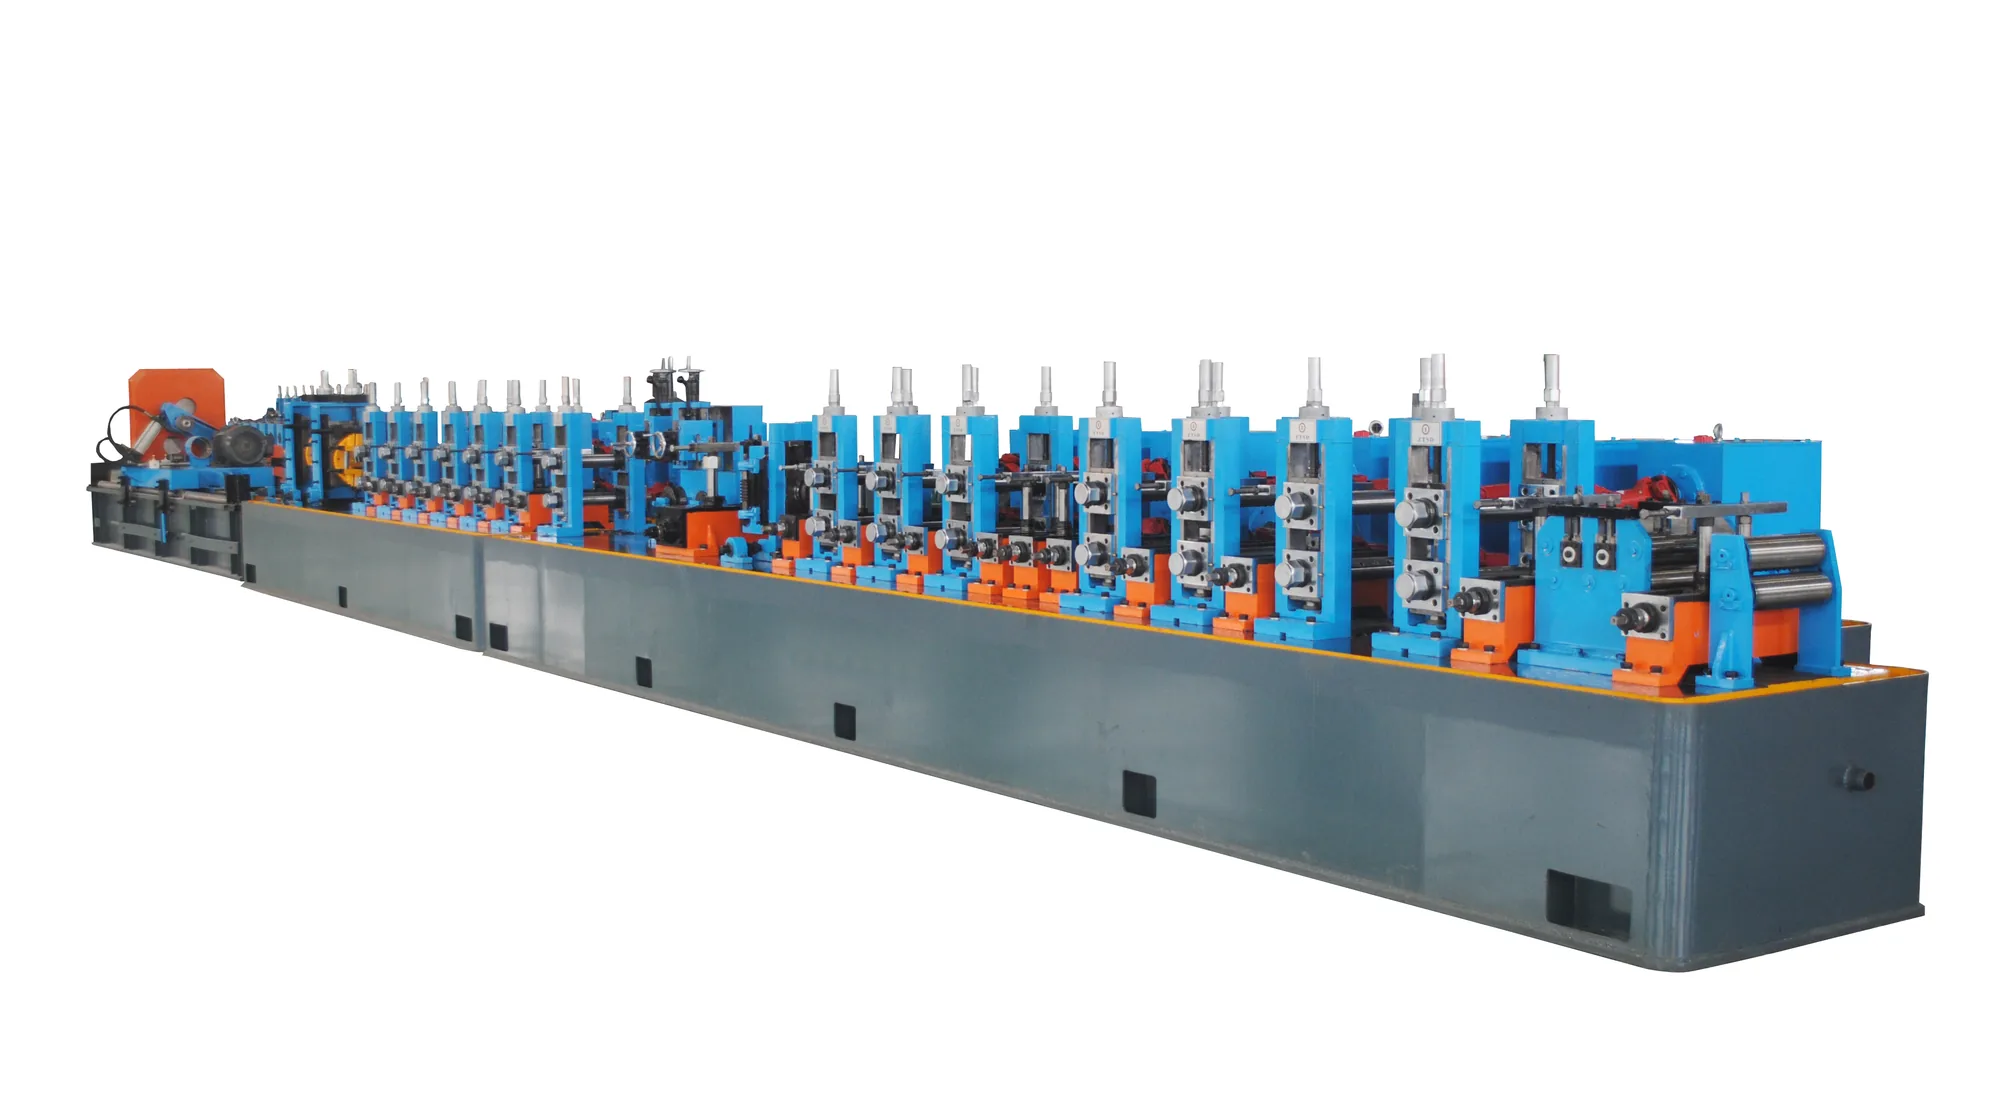
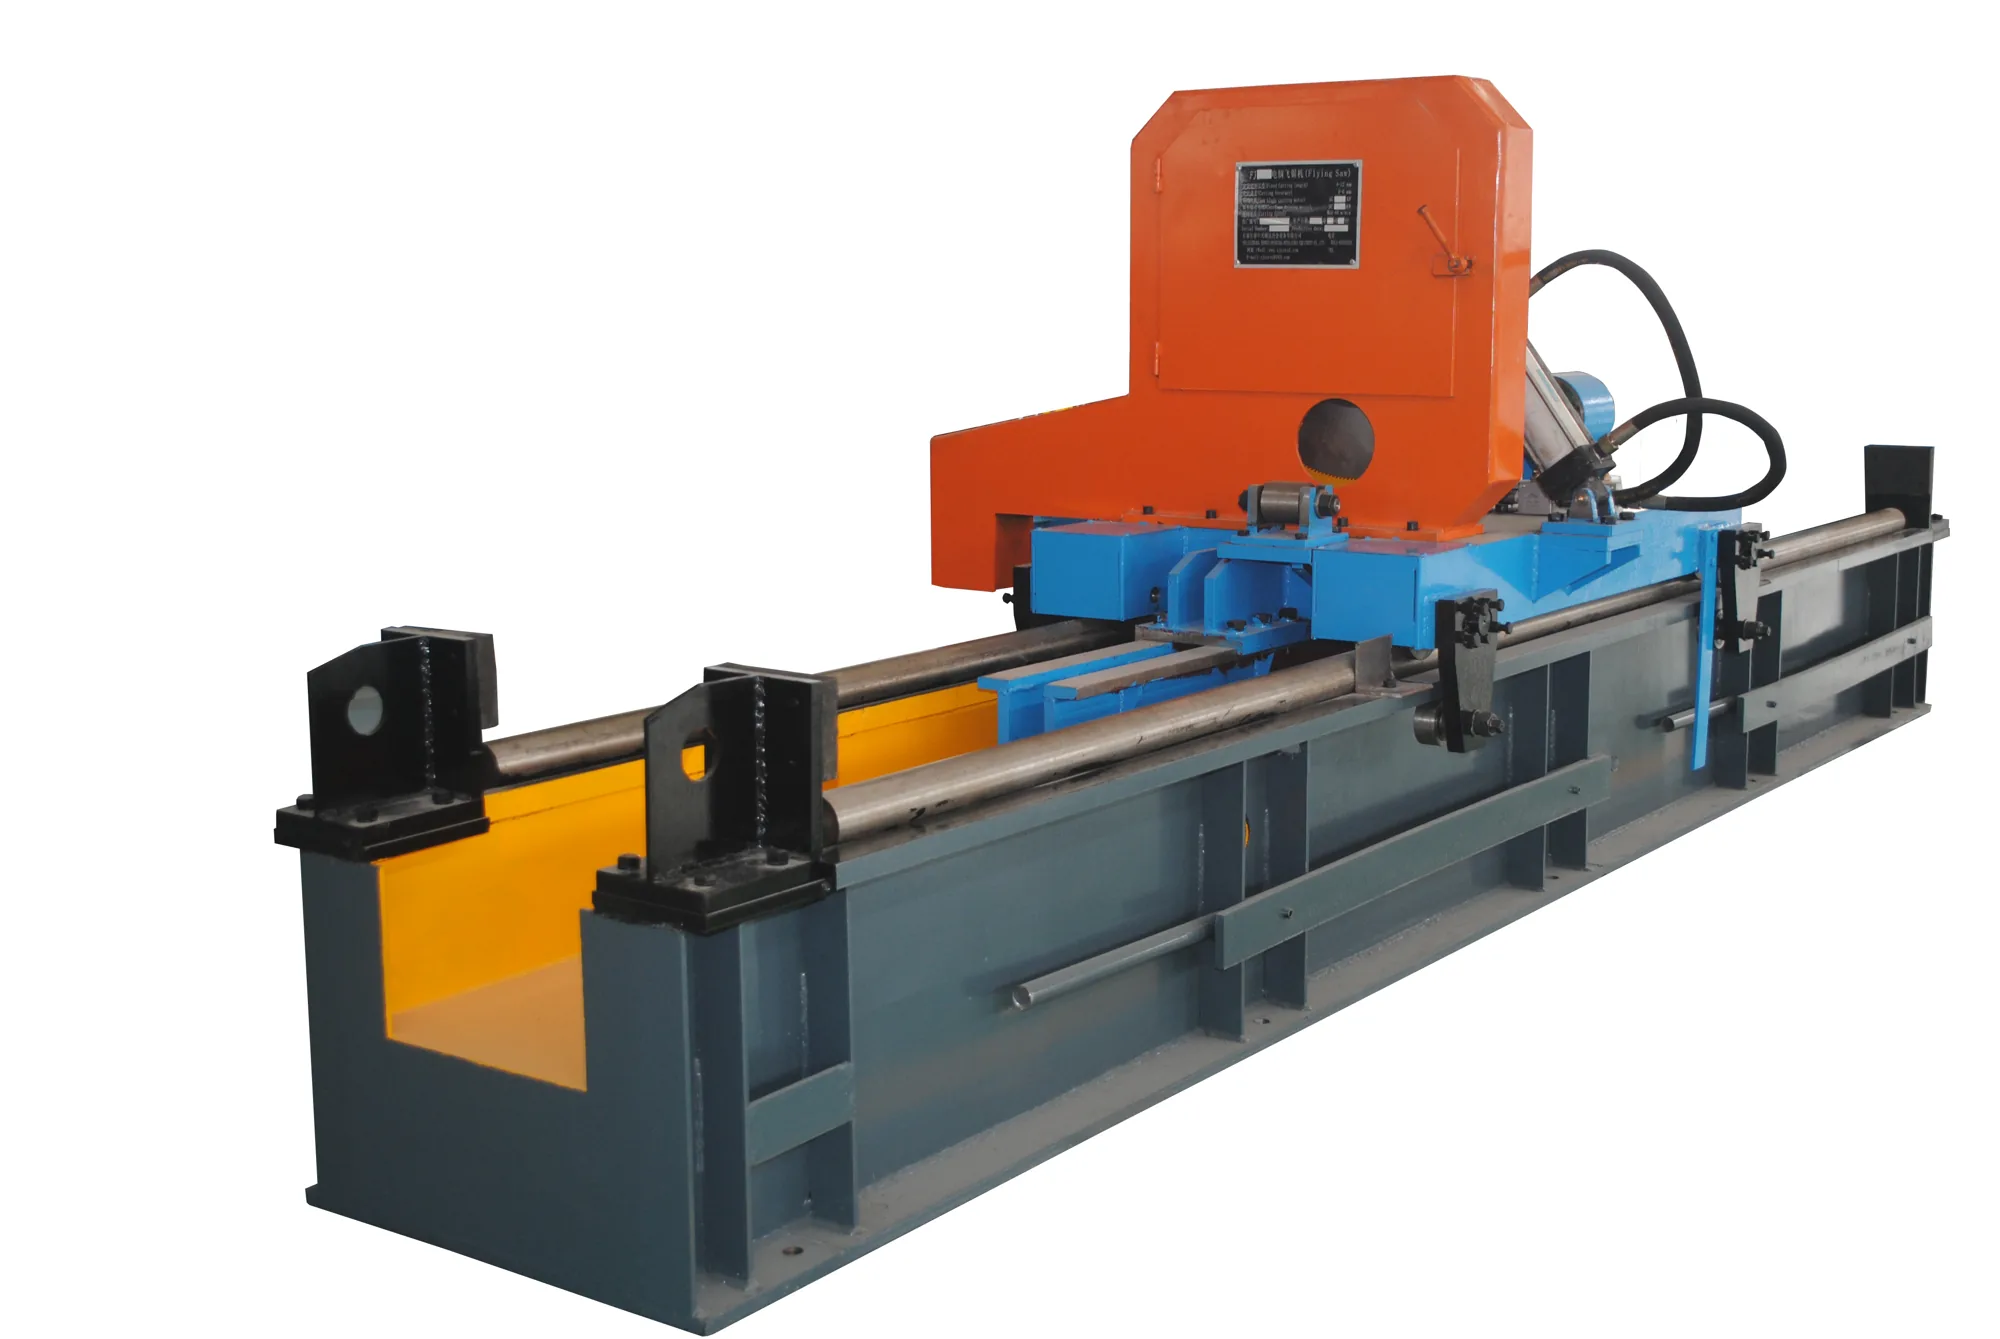
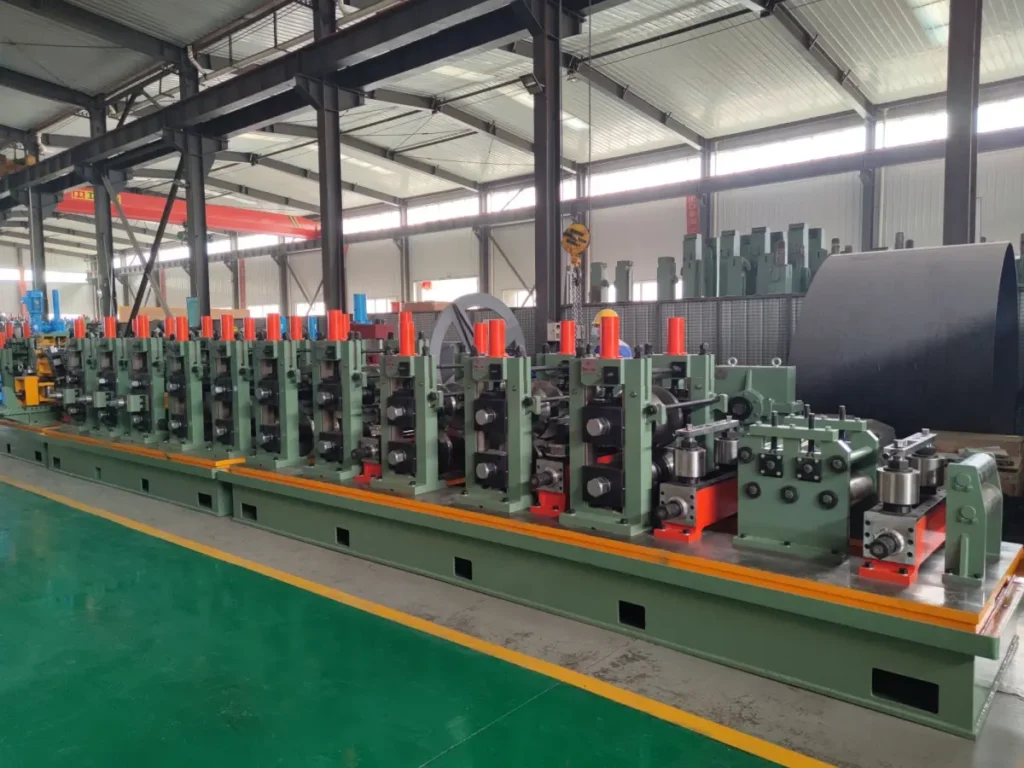
Unit train — eight units on HG89 and HG114; HG32 to HG76 run the same train without the leveller. Expanding-mandrel uncoiler; five-roller leveller (HG89 and HG114); automatic shear and butt welder; spiral accumulator; forming and sizing mill; high-frequency induction welder; flying or cut-off saw; PLC and variable-frequency control system.
The five steps and their windows.
| Model | Finished OD Range |
|---|---|
| HG32 | Φ10–32 mm |
| HG50 | Φ16–50.8 mm |
| HG76 | Φ25–76 mm |
| HG89 | Φ32–89 mm |
| HG114 | Φ45–114 mm |
Forming route. Conventional roll forming, or direct forming square as a separate technology with its own line.
Welding method. High-frequency induction welding across the whole family, using the skin and proximity effects to concentrate current at the strip edges.
Automation. Semi-automatic or fully automatic PLC control, with the fully automatic tube mill as the high-automation variant.
Section shapes. Round, square and rectangular. Most HG steps can produce all three.
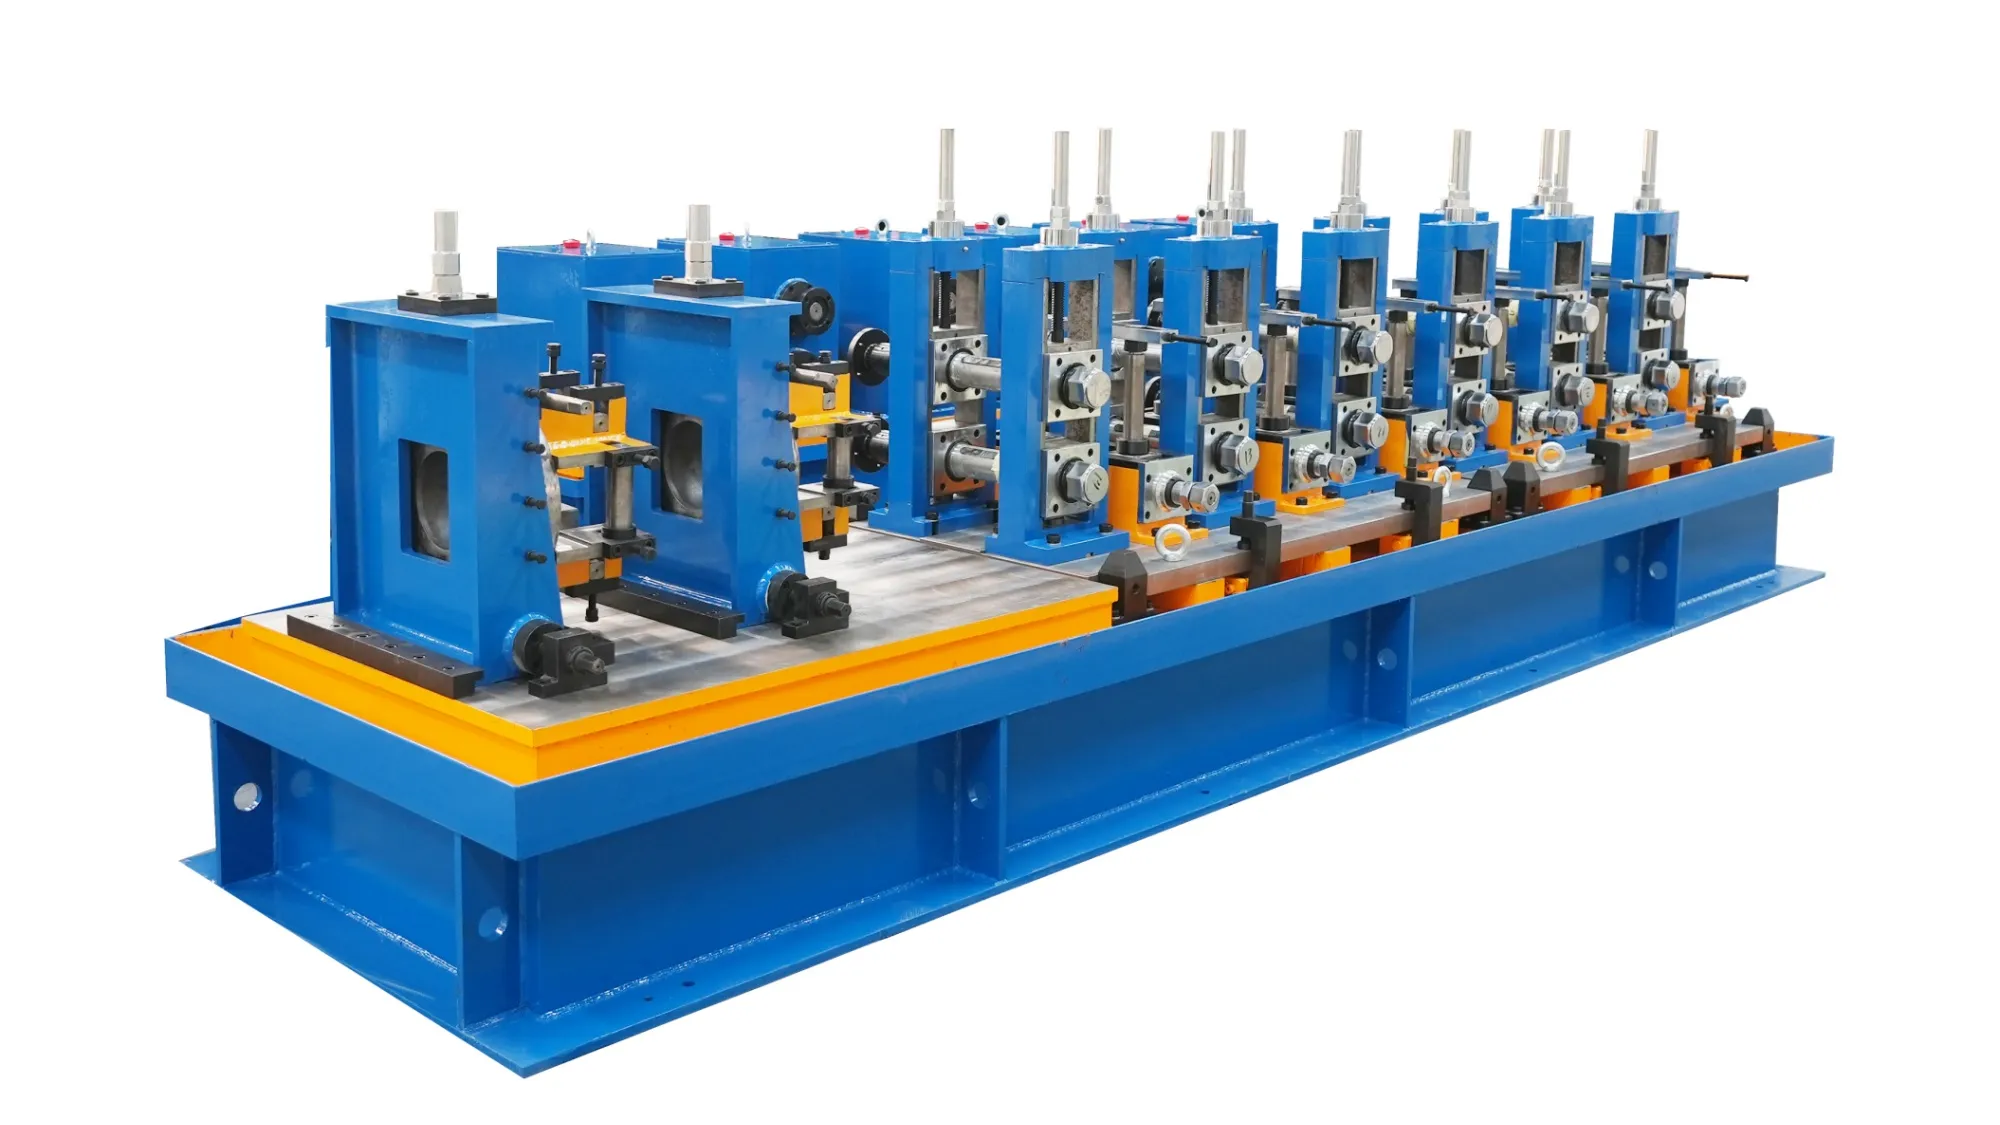
Key Parameters: Size Range, Wall Thickness and Welder Power by Model
| Model | Outside diameter | Wall thickness | Square section | HF welder |
|---|---|---|---|---|
| HG32 | Φ10 – 32 mm | 0.5 – 1.5 mm | 10×10 – 25×25 mm | 150 kW |
| HG50 | Φ16 – 50.8 mm | 0.8 – 2.0 mm | 12×12 – 40×40 mm | 200 kW |
| HG76 | Φ25 – 76 mm | 1.5 – 3.0 mm | 20×20 – 60×60 mm | 250 kW |
| HG89 | Φ32 – 89 mm | 1.0 – 4.0 mm | 25×25 – 70×70 mm | 300 kW |
| HG114 | Φ45 – 114 mm | 1.5 – 5.0 mm | 35×35 – 90×90 mm | 300 kW |
On a small diameter tube mill, line speed and shift output depend on pipe size, wall and material grade, and are stated with the quotation.
How the Line Stays Continuous
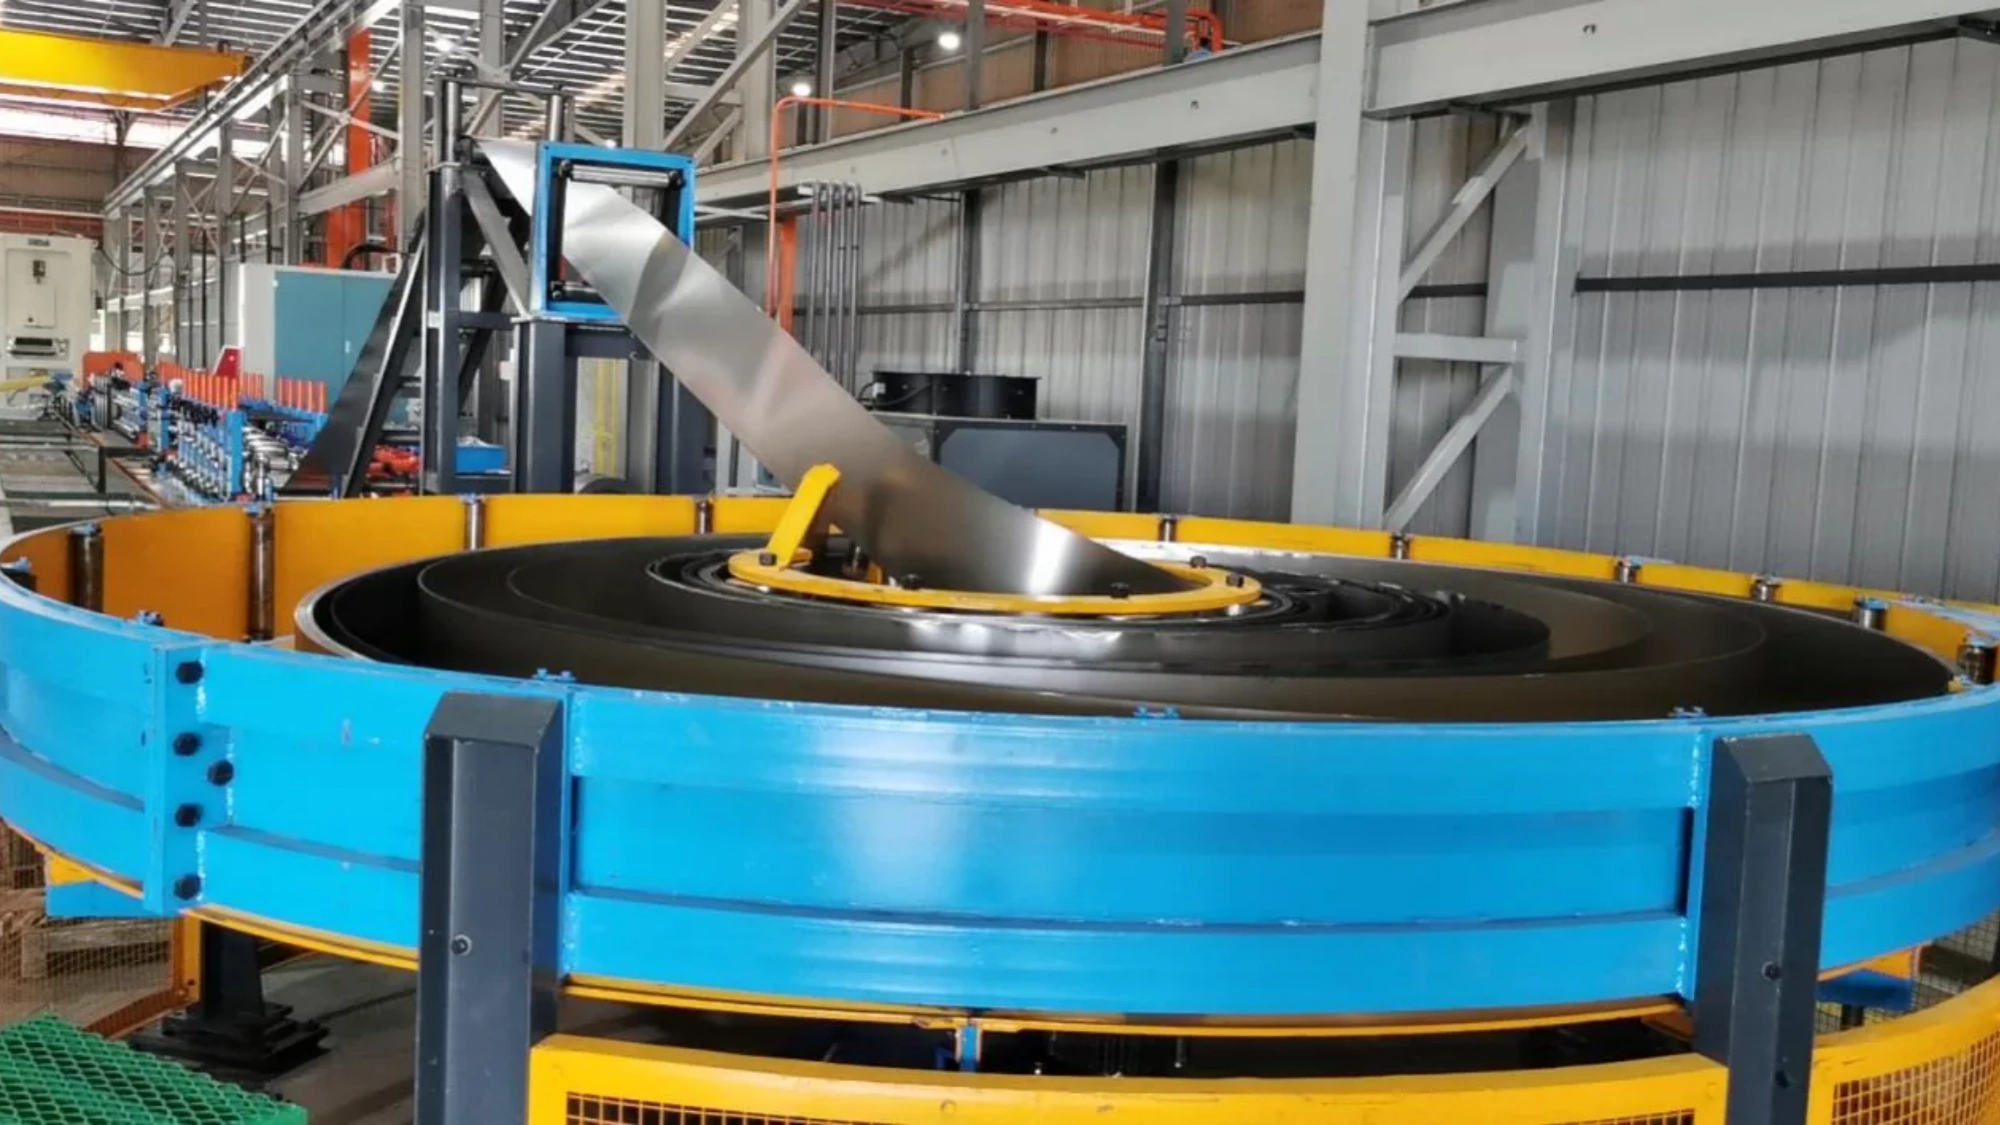
The word continuous in the definition is doing real work, and two of the eight units exist only to protect it. An automatic shear and butt welder cuts the head and tail of successive coils and welds them together, so a coil change does not stop the mill. A spiral accumulator stores strip so that the line’s entry section can pause for that join while the forming and welding section keeps running.
Seen from the operator’s side: before a coil runs out, the head and tail are sheared and butt welded, timed against the accumulator so that the line does not stop, with broken strip and scrap pipe at the joint as the failure mode.
The two remaining entry units serve the same purpose differently. An expanding-mandrel uncoiler tensions the coil accurately, with unstable tension producing strip wander and loose coil; on HG89 and HG114, a five-roller leveller flattens the strip before forming, with poor levelling leaving residual curvature that shows up later as a wandering seam.
What Small-Diameter Pipe Is Made For
Two applications dominate this end of the range, and they ask for different things from the same machine.
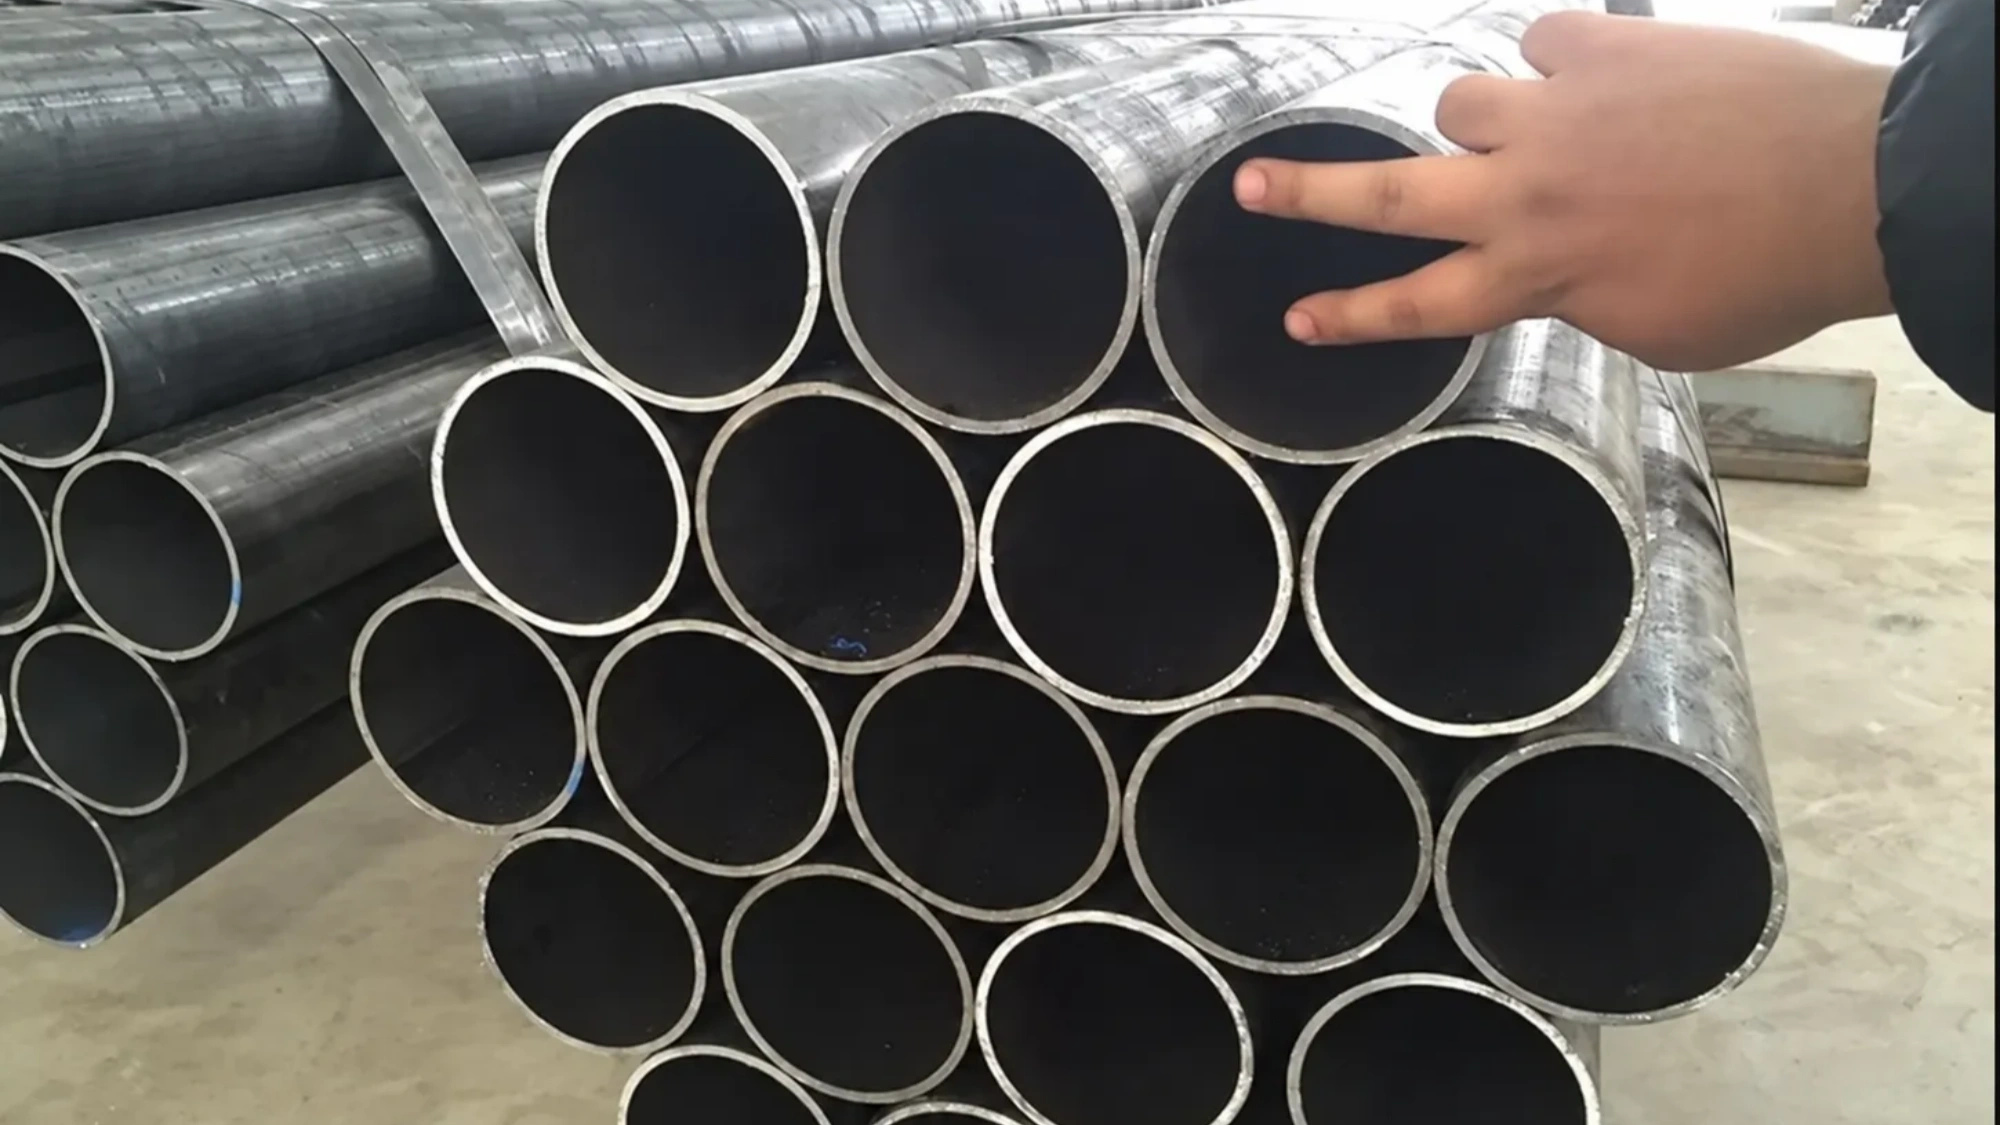
Fluid transport pipe: pipe plants running HG lines continuously to make carbon steel welded pipe for oil and gas transport, municipal water supply, drainage and gas, and chemical and heating pipework. The acceptance criteria are weld pass rate, diameter and wall coverage, non-stop coil changing, and energy and yield.
Structural and scaffolding tube: plants making load-bearing, scaffolding and general mechanical section in square, rectangular and round. Here the criteria shift to corner definition and straightness on square and rectangular section, changeover efficiency, and unit electricity consumption.
Furniture and home tube appears as a third downstream application at the small end, and it is the application where an in-line coating line is often added.
Automation Level Is a Selection Decision
There are two levels: semi-automatic, and fully automatic PLC control — the automatic tube mill is the fully automatic one.
What the control layer governs: PLC and variable-frequency control unify the takt and speed of forming, welding, sizing and cutting, and the consequence of instability is speed fluctuation, cut-length error and higher downtime.
Where acceptance is dimensional rather than structural, as with automotive parts and new-energy profiles, that stability is the specification, and PLC and variable-frequency drive control is what makes the operation repeatable.
Operating Reality After Handover
The line has five operating steps, and three of them require training rather than ordinary skill: coil loading and strip threading, where centring, tension and head flattening decide whether the strip wanders; shear-weld coil joining, where butt-weld parameters and accumulator timing must be coordinated; and setting welding power and speed, where power, weld speed and squeeze have to be matched against each other.
Size setting is the fourth, as roll change on a conventional line versus servo adjustment only on a direct-forming line, with profile drift and trial scrap as the cost of getting it wrong. Cutting and collecting is the fifth and is ordinary operation.
Two support facts follow from that. Operator setup and quick tooling change reduce scrap on a size change, and the condition of the impeder and induction coil directly affects weld energy — which is why those two parts sit on the spares list rather than the maintenance list.
How to Choose the Right Model
A plant making Φ20 to Φ100 mm is not choosing between five steps; it is choosing the one step whose window contains 100. Start from the widest pipe you will actually make, not the average. Because the windows overlap, the binding constraint is the top of your product range.
Then check section shape. Round, square and rectangular are all producible on most steps, but the square and rectangular route has its own dedicated line where frequent size changes are the priority.
Then decide automation level. Semi-automatic and fully automatic PLC are a classification dimension, not an option list, which means it is decided at selection rather than retrofitted.
Then look at what the line is actually responsible for. The split is precise: the mill controls weld power matching, seam alignment and squeeze; the buyer controls strip quality and operation. Dimensional accuracy comes from sizing and straightening on the equipment side, with incoming wall-thickness tolerance on the buyer’s side.
On high-end configurations, material yield can reach 93% or more, with actual yield also depending on the plant’s own operation.
What these lines are bought to fix is worth saying plainly, because it drives the specification: continuous production without stopping to change coils, multi-size coverage on one line, stable yield and weld quality, and changeover efficiency.
Scope of Supply, Installation and Commissioning
The process flow the line delivers, end to end, is uncoiling, shear and butt welding, spiral accumulator, forming and sizing, and flying saw — which is also the shortest accurate description of what a complete line includes.
Commissioning has to cover the same five operating steps described under Operating Reality After Handover, including the three that require training.
Delivery is knocked down in containers with precision parts crated, installation and commissioning guided by our engineers on site, and shipment within 90 working days of the deposit.
Small Diameter Tube Mill Machine: Sizes at a Glance
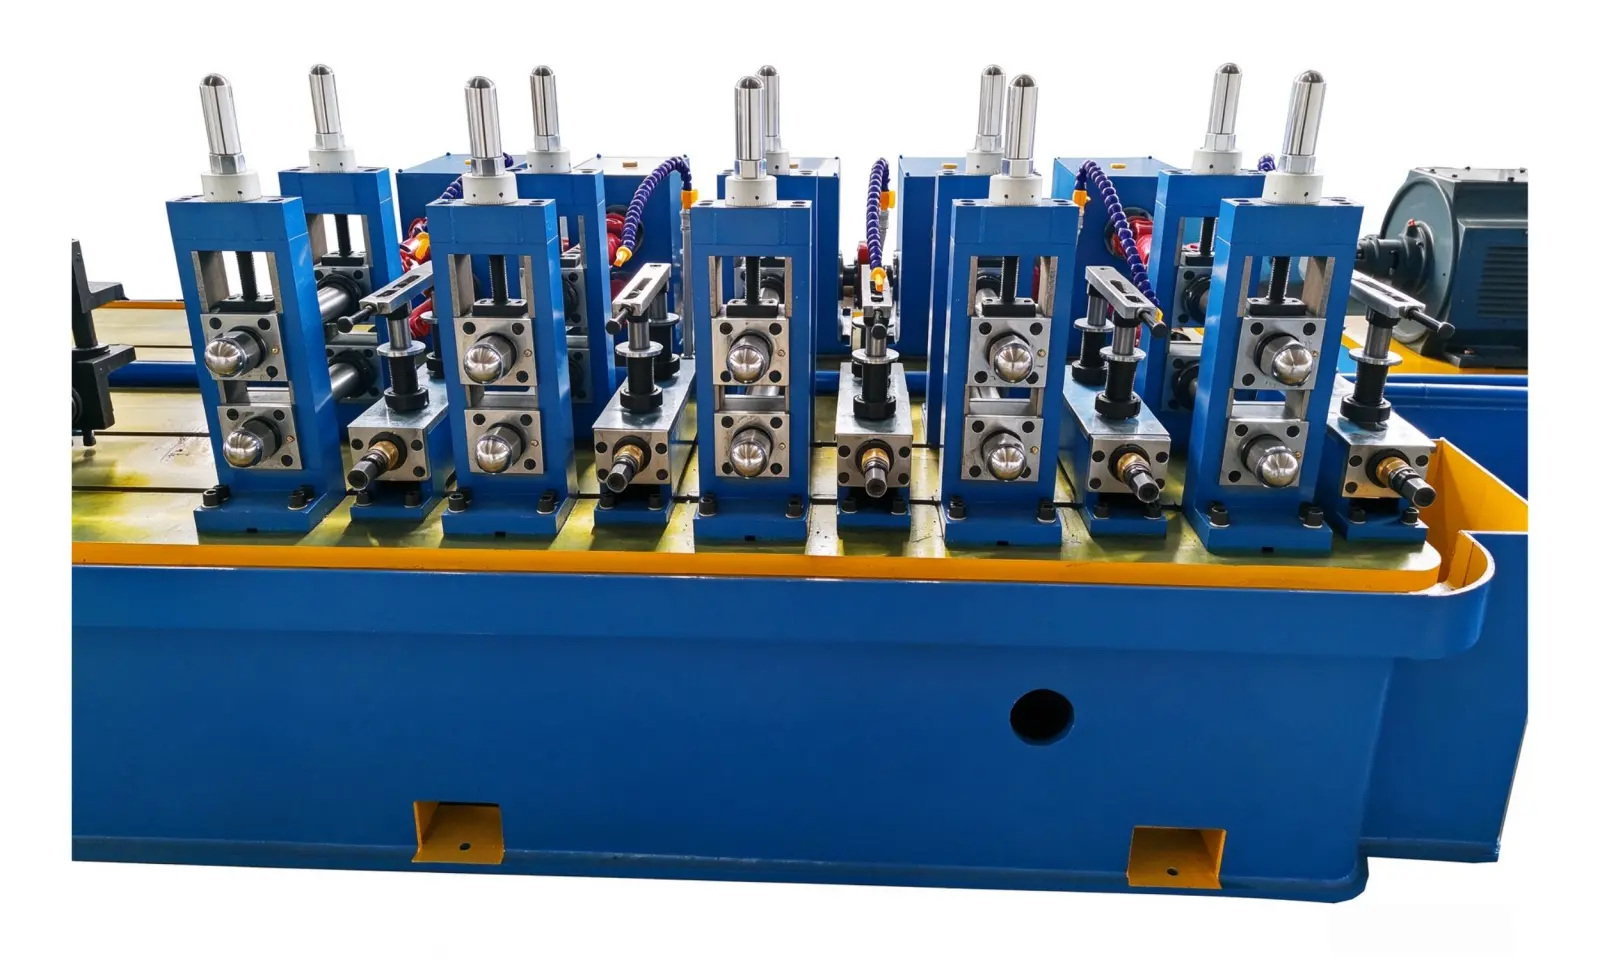
Five small diameter tube mill sizes, HG32 to HG114, cover finished pipe from about Φ10 to Φ114 mm. All are high-frequency induction welded and PLC controlled, and the right size is the one whose window contains the largest diameter in the plant’s product plan.
Tube Mill for 114mm Pipe: HG114 or HG165?
Φ114 mm sits at the top of the HG114 window, which runs Φ45–114 mm. It is also inside the HG165 window, which runs Φ60–165 mm and belongs to the large-diameter range. Which of the two is right depends on the rest of the range, not on the 114 figure alone — and this is exactly the case where choosing by “the band that contains my diameter” gives the wrong answer.
Lines Delivered in This Diameter Band
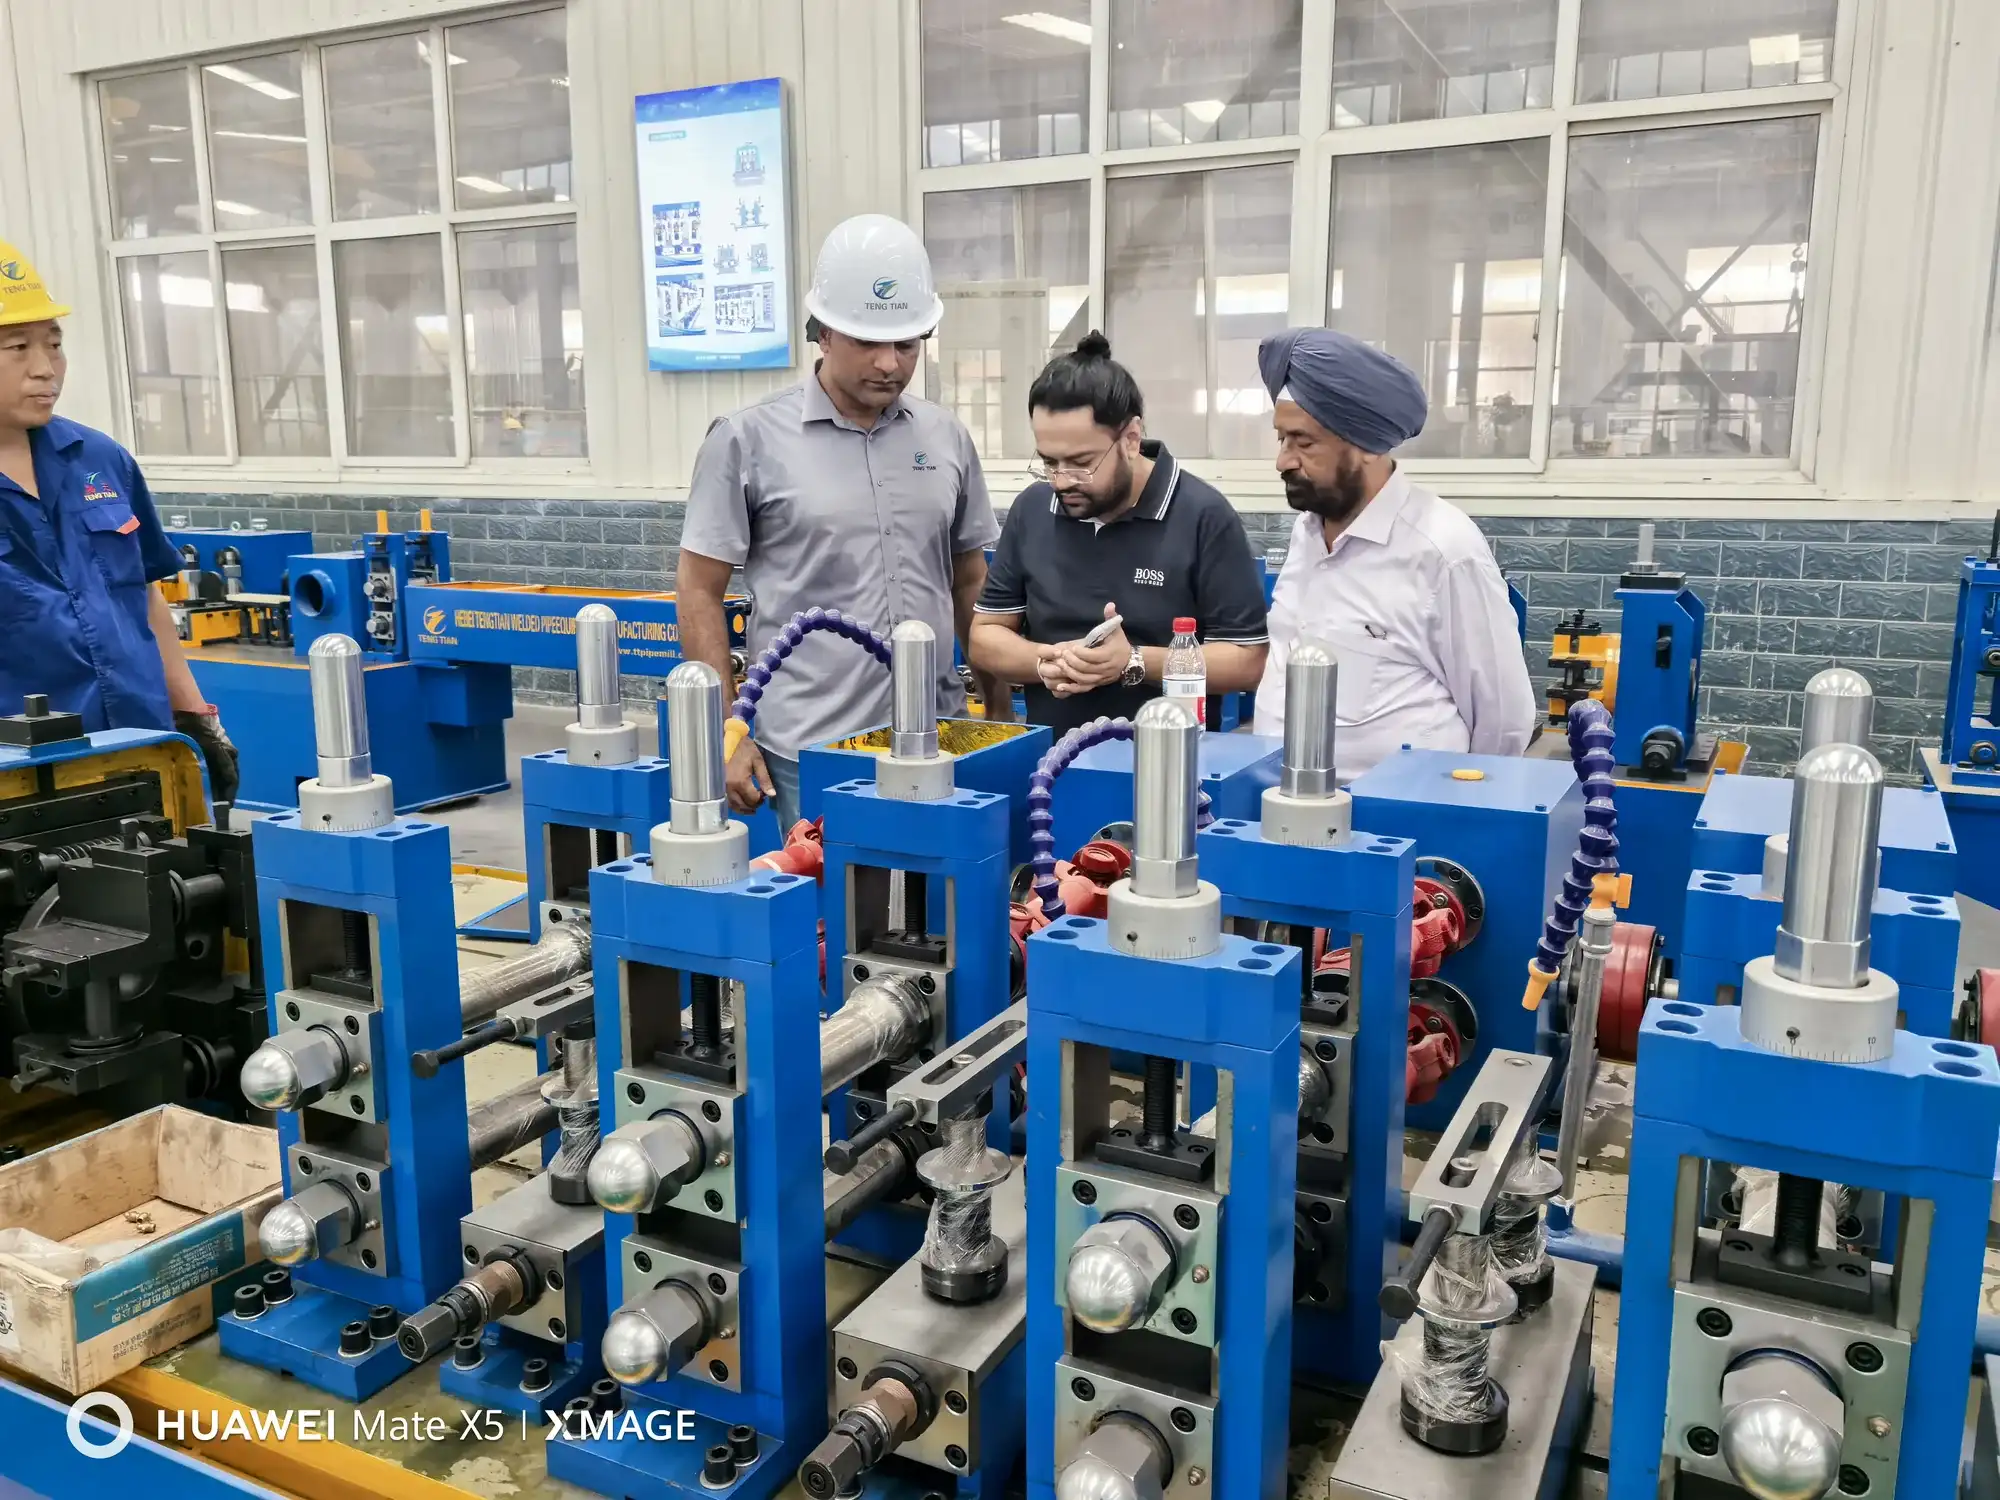
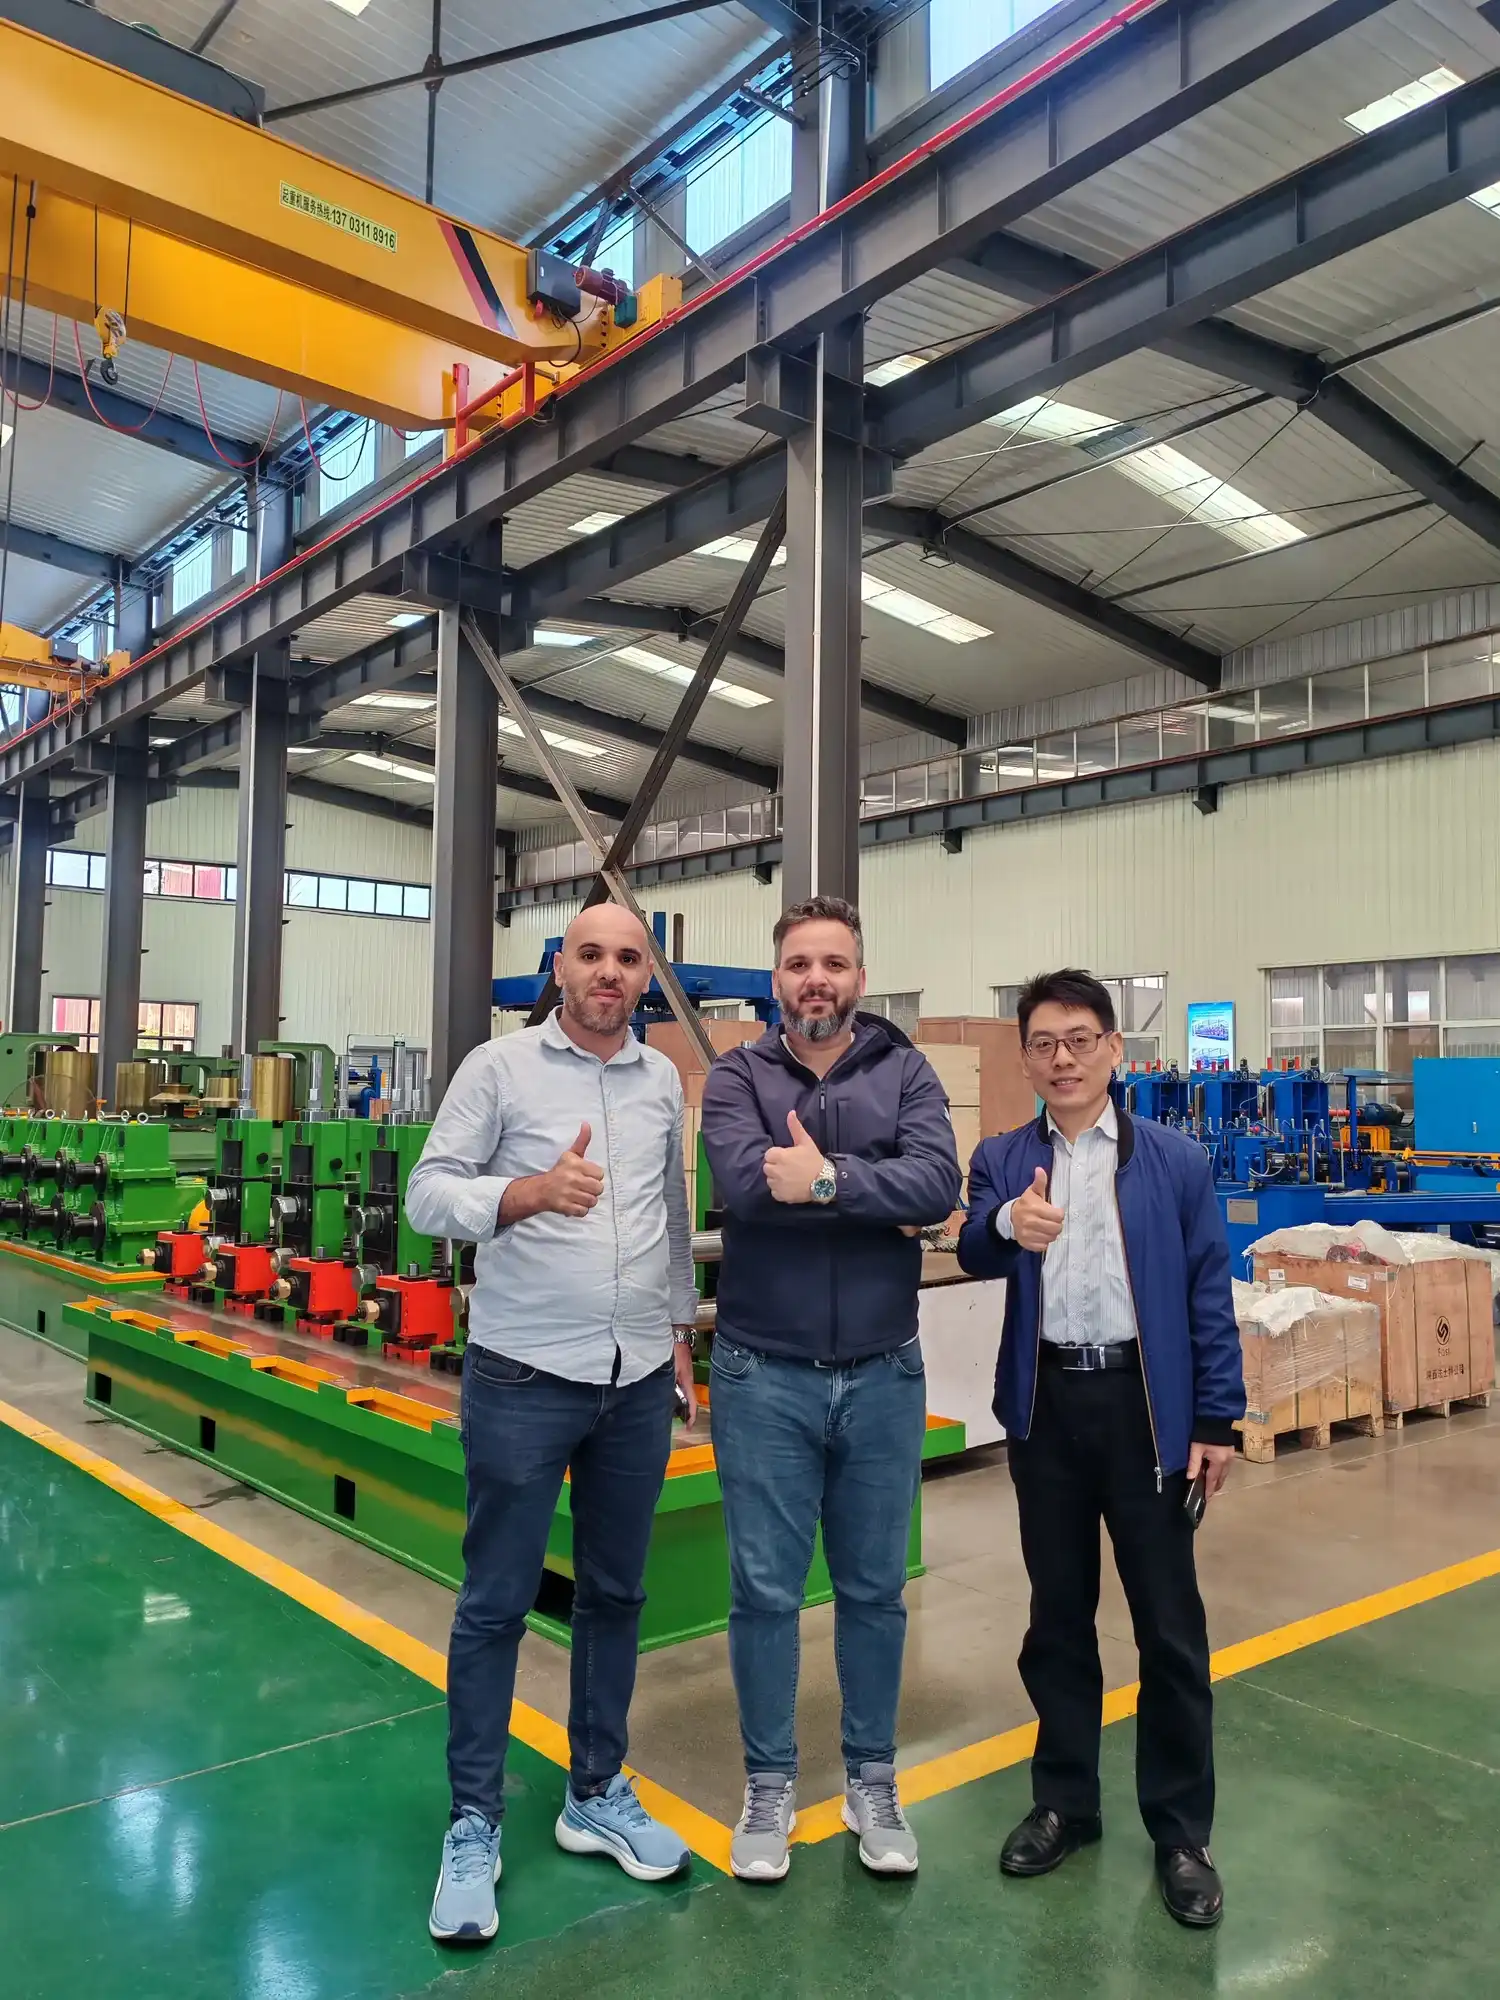
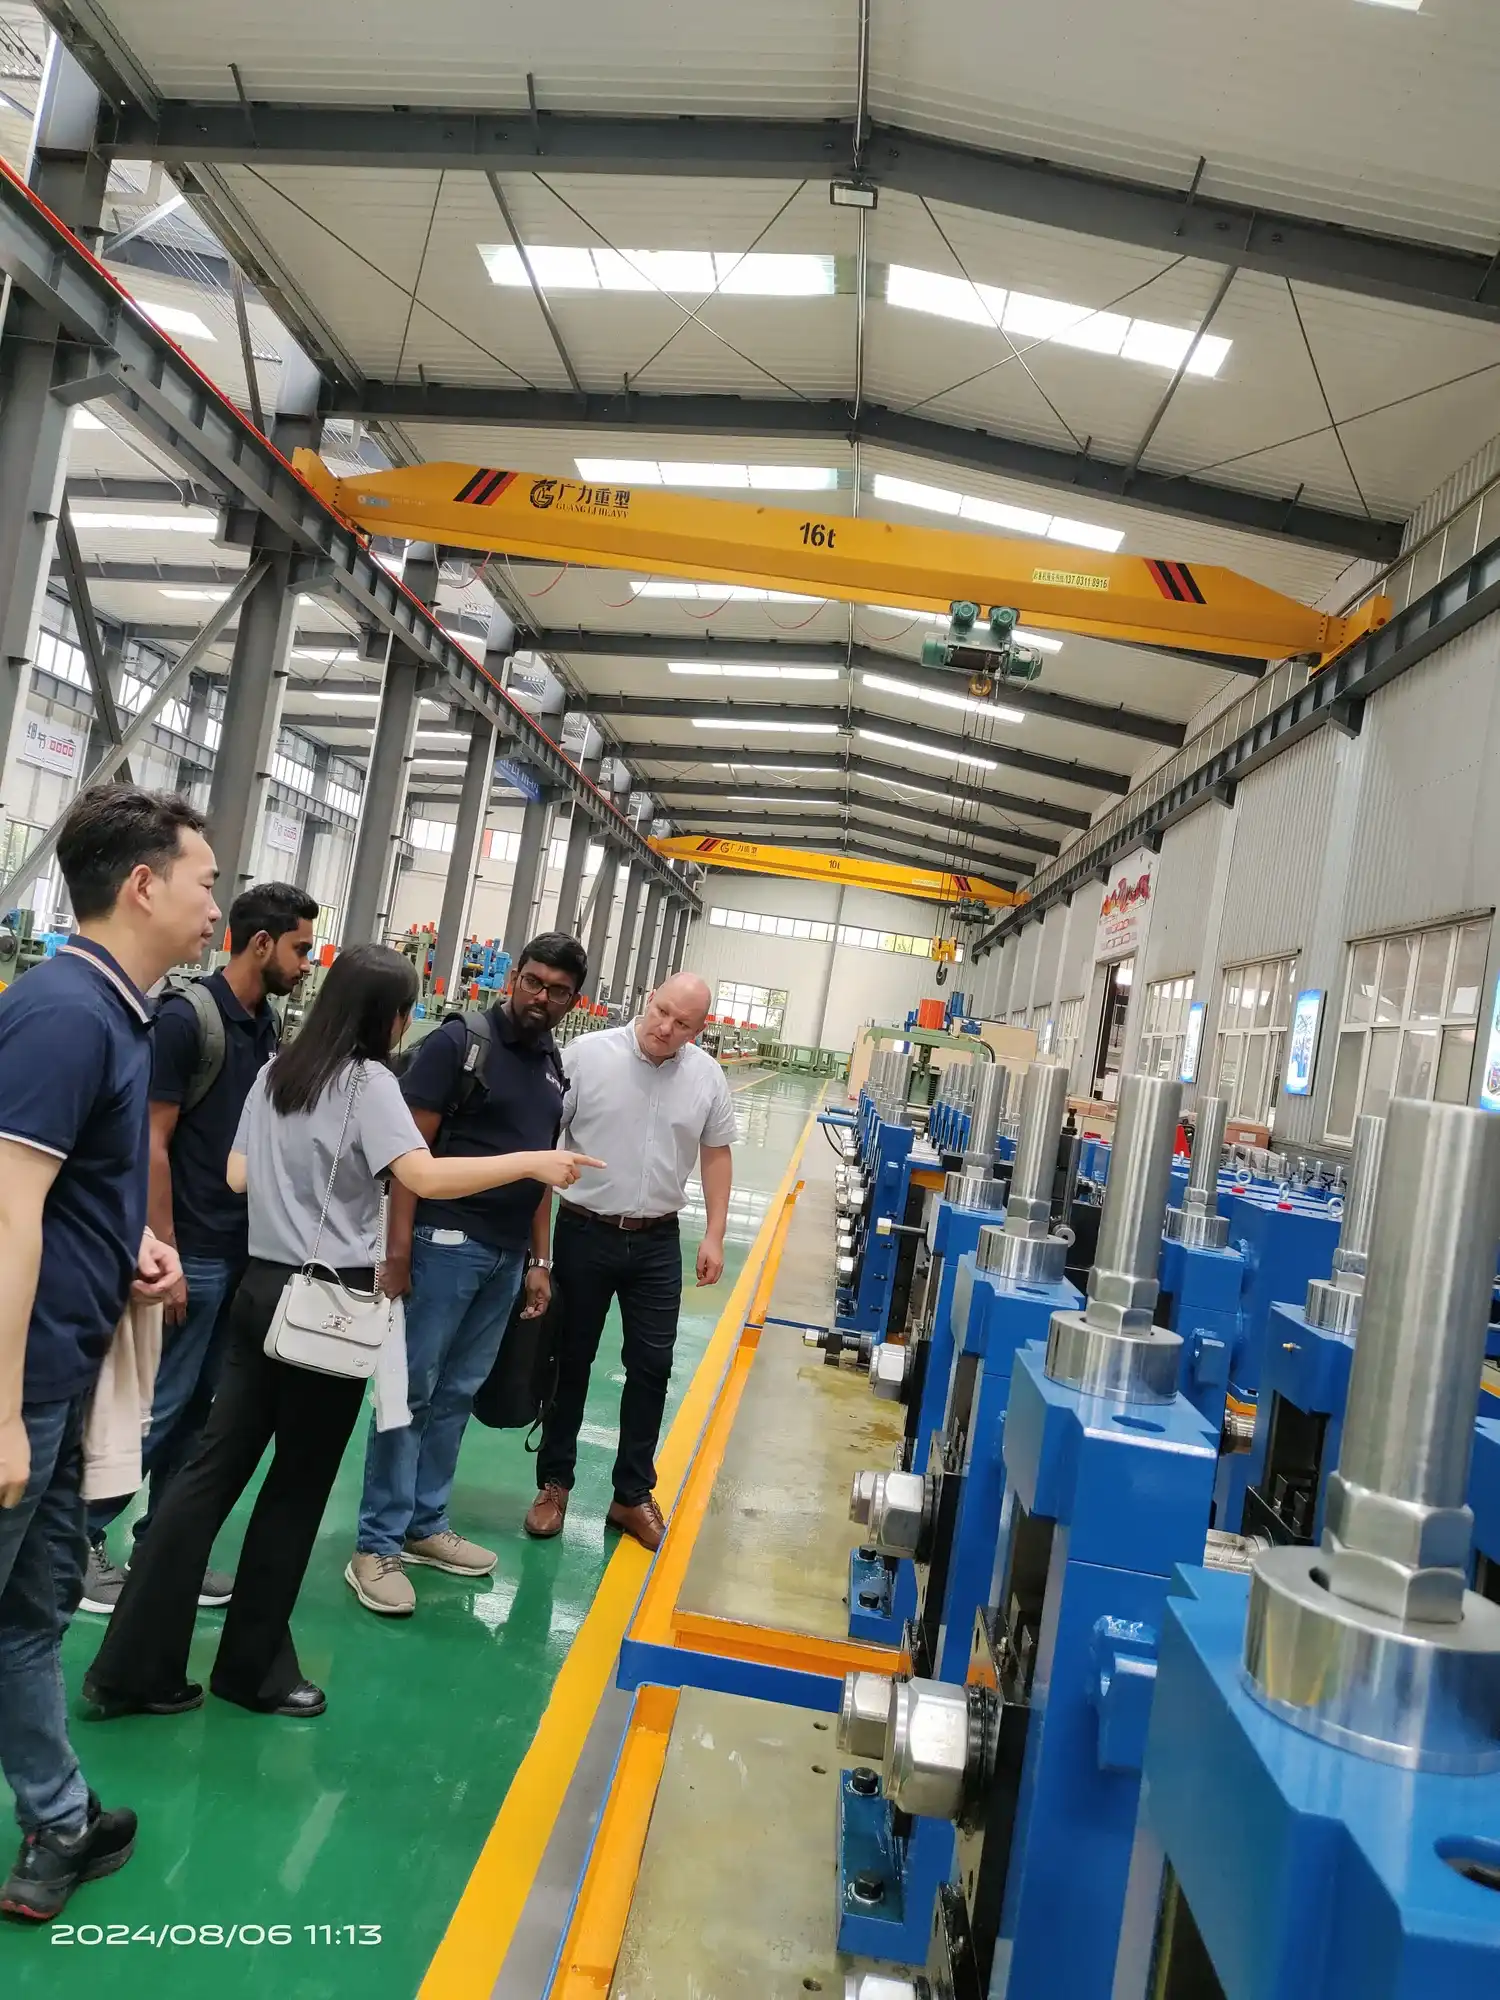
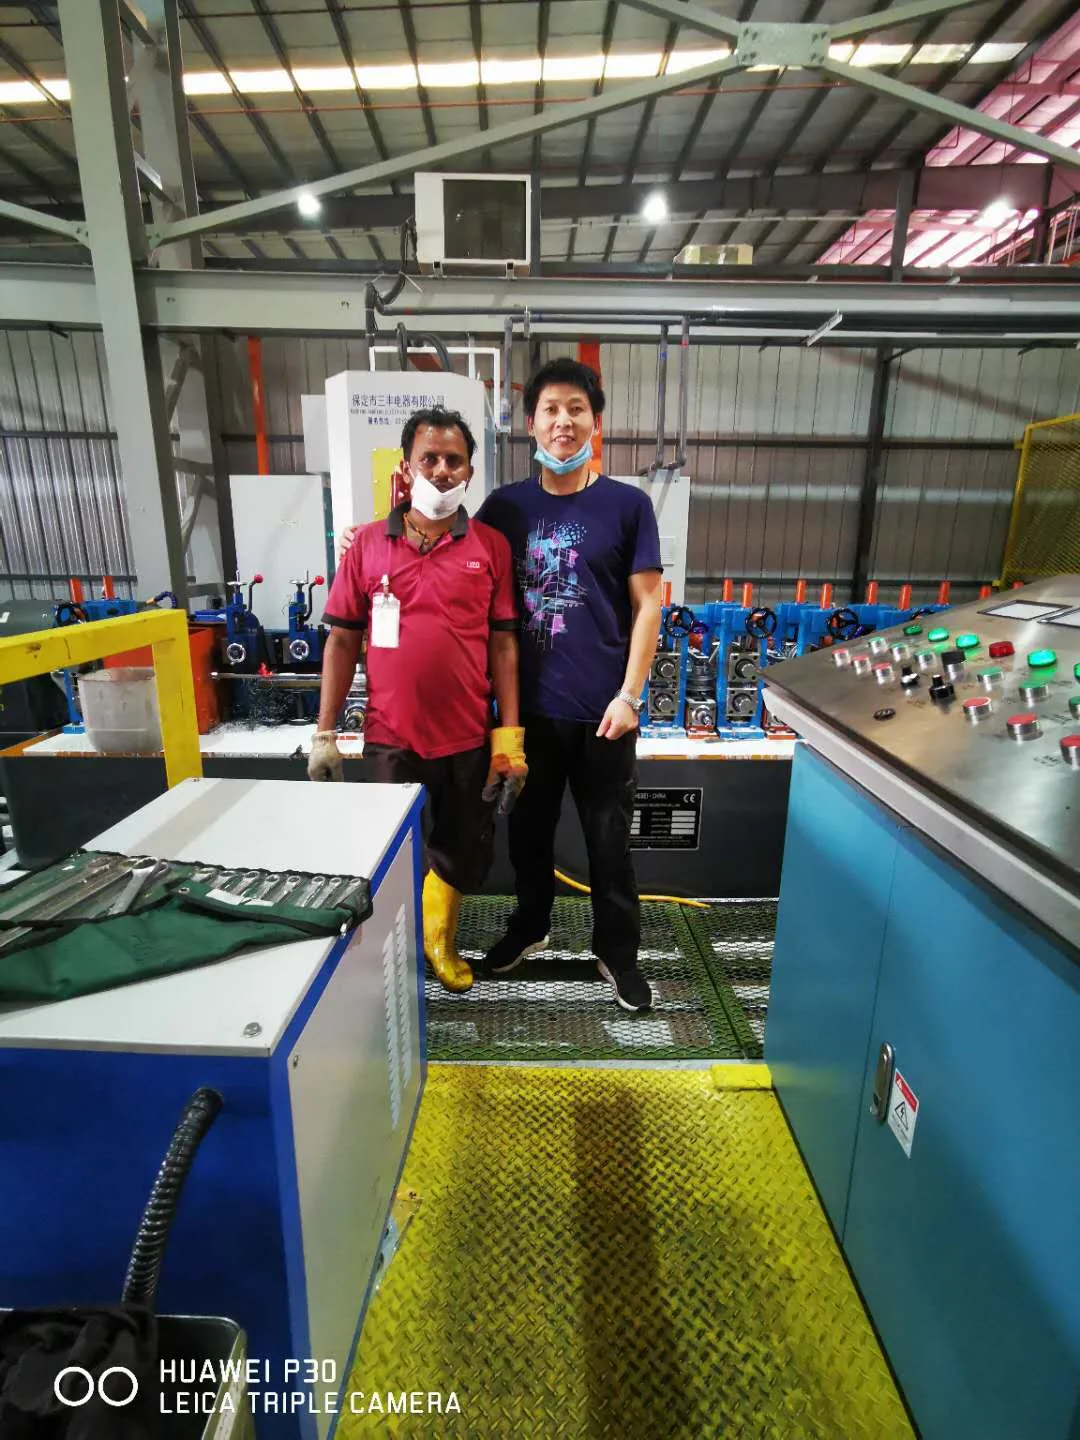
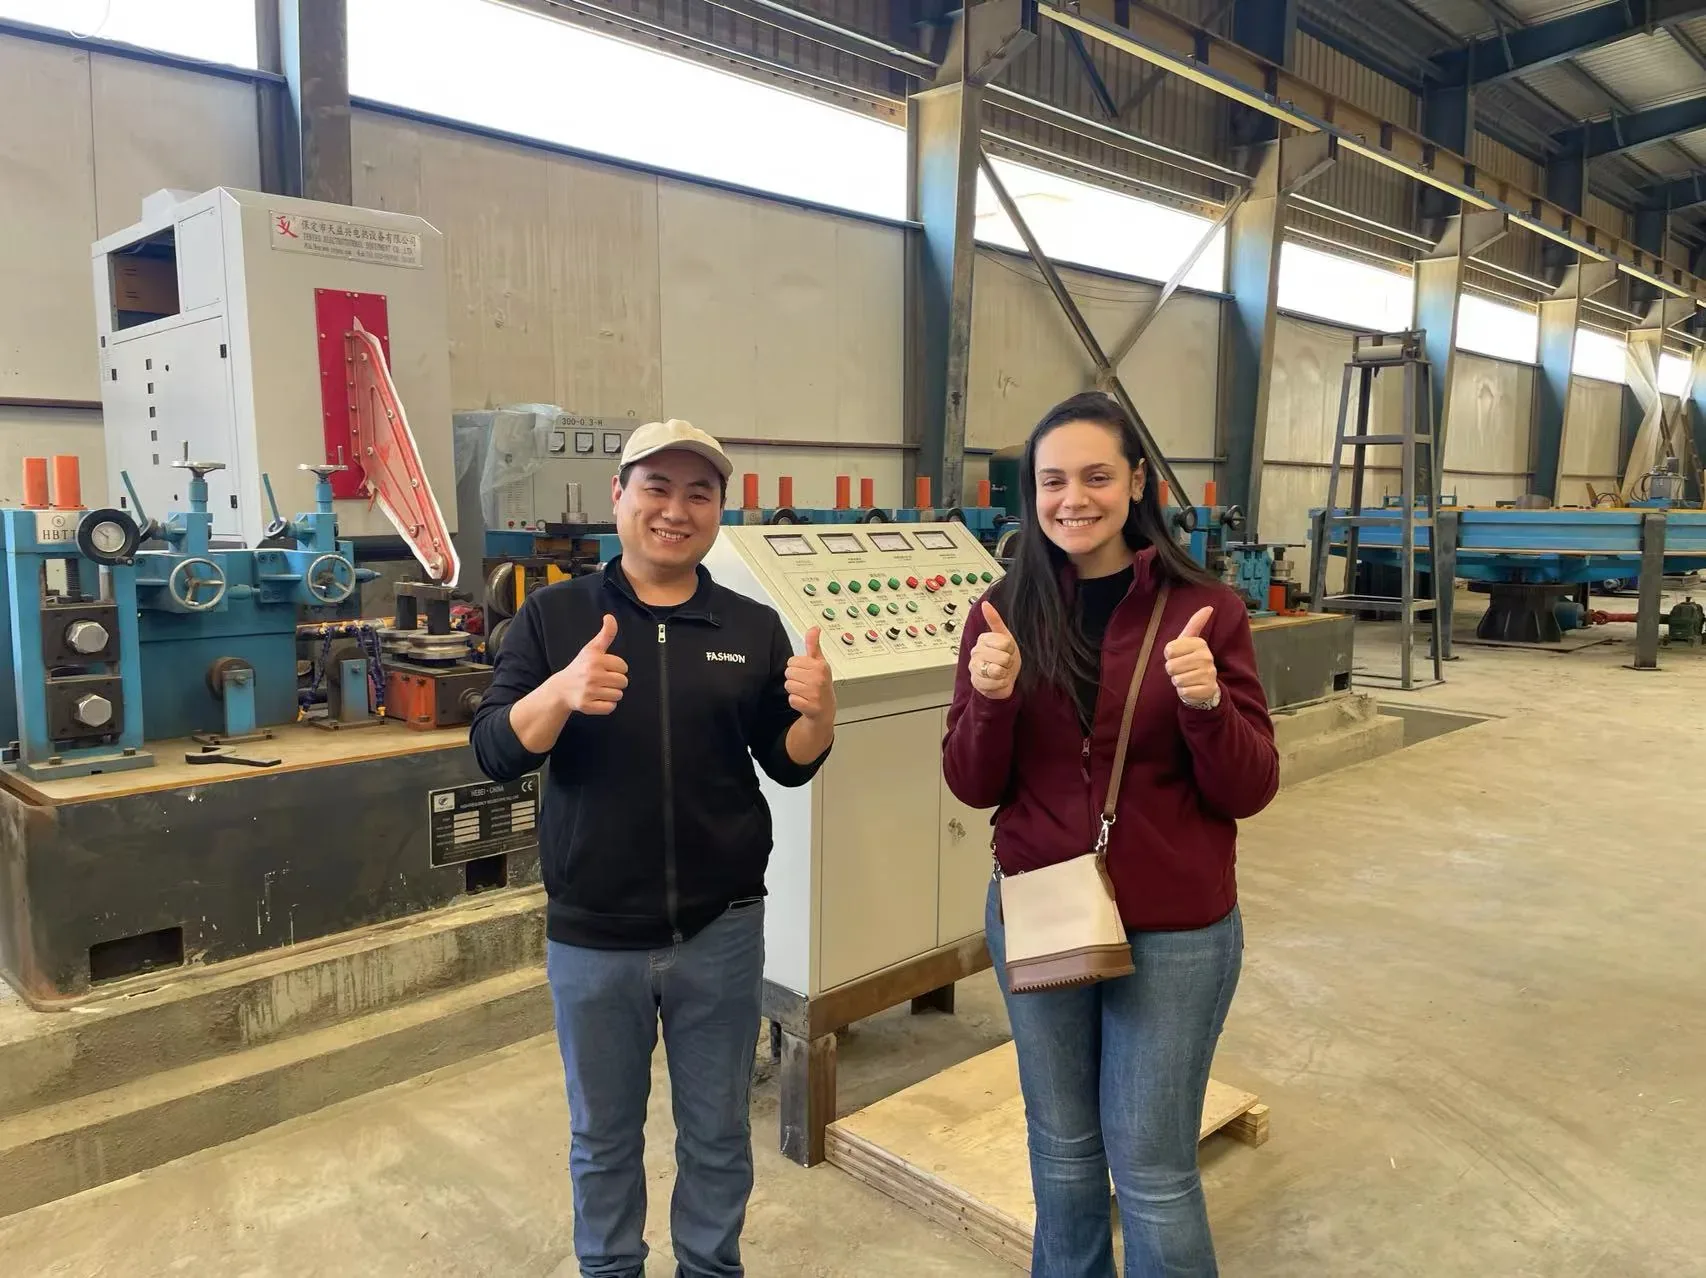
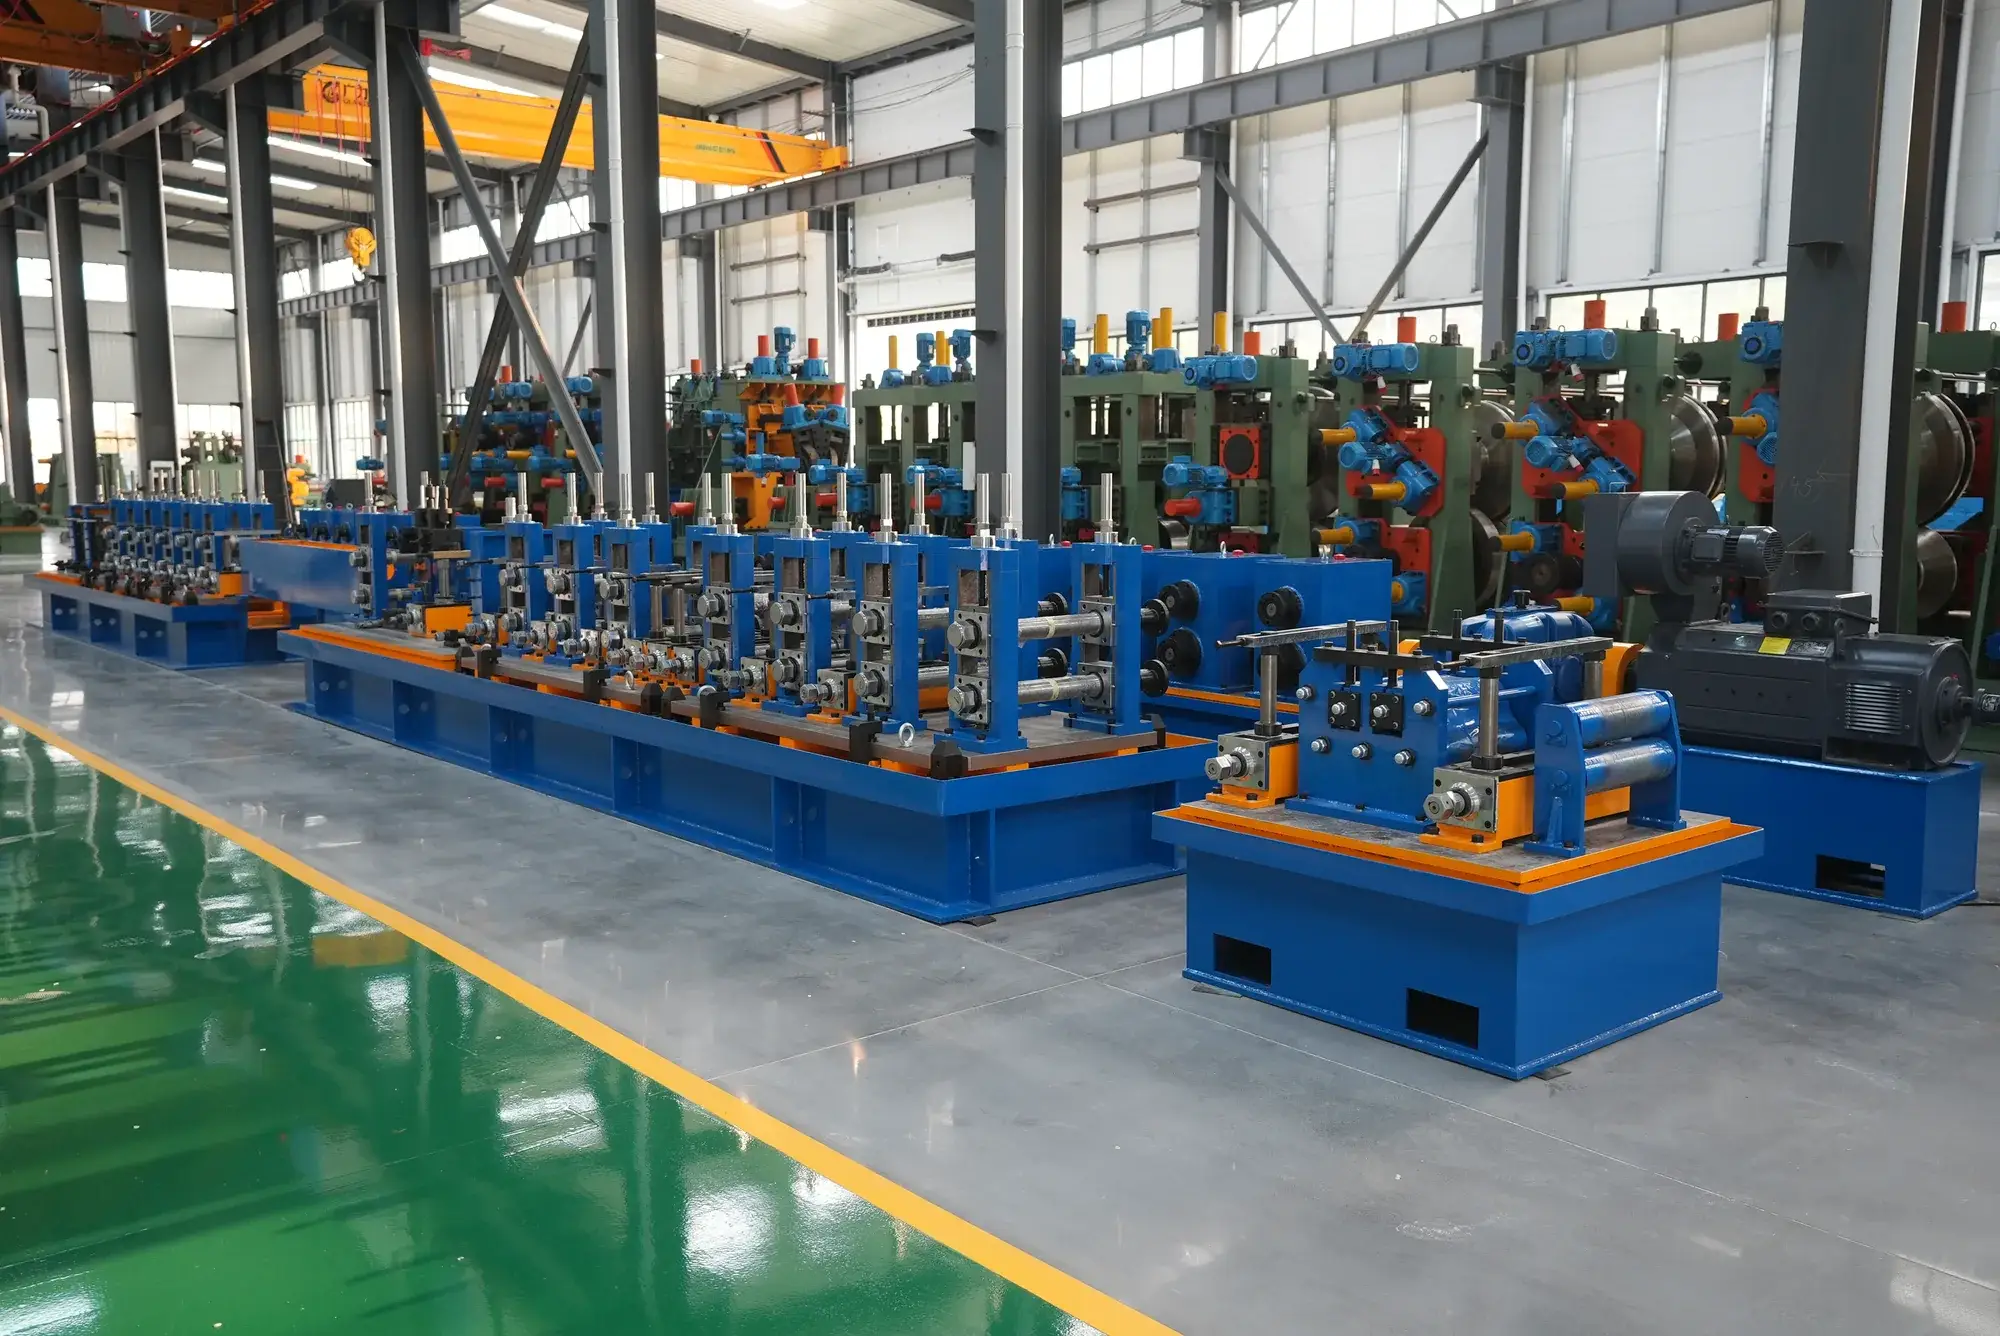
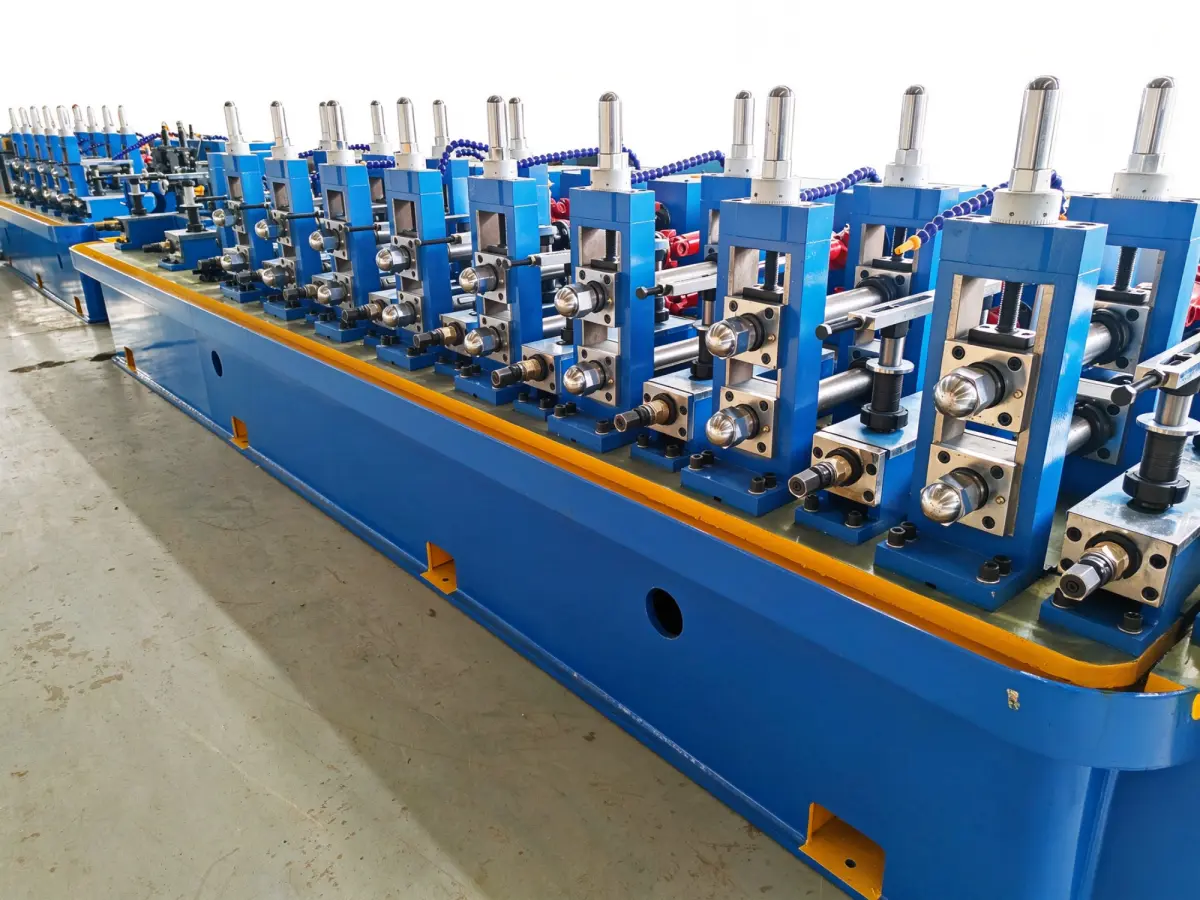
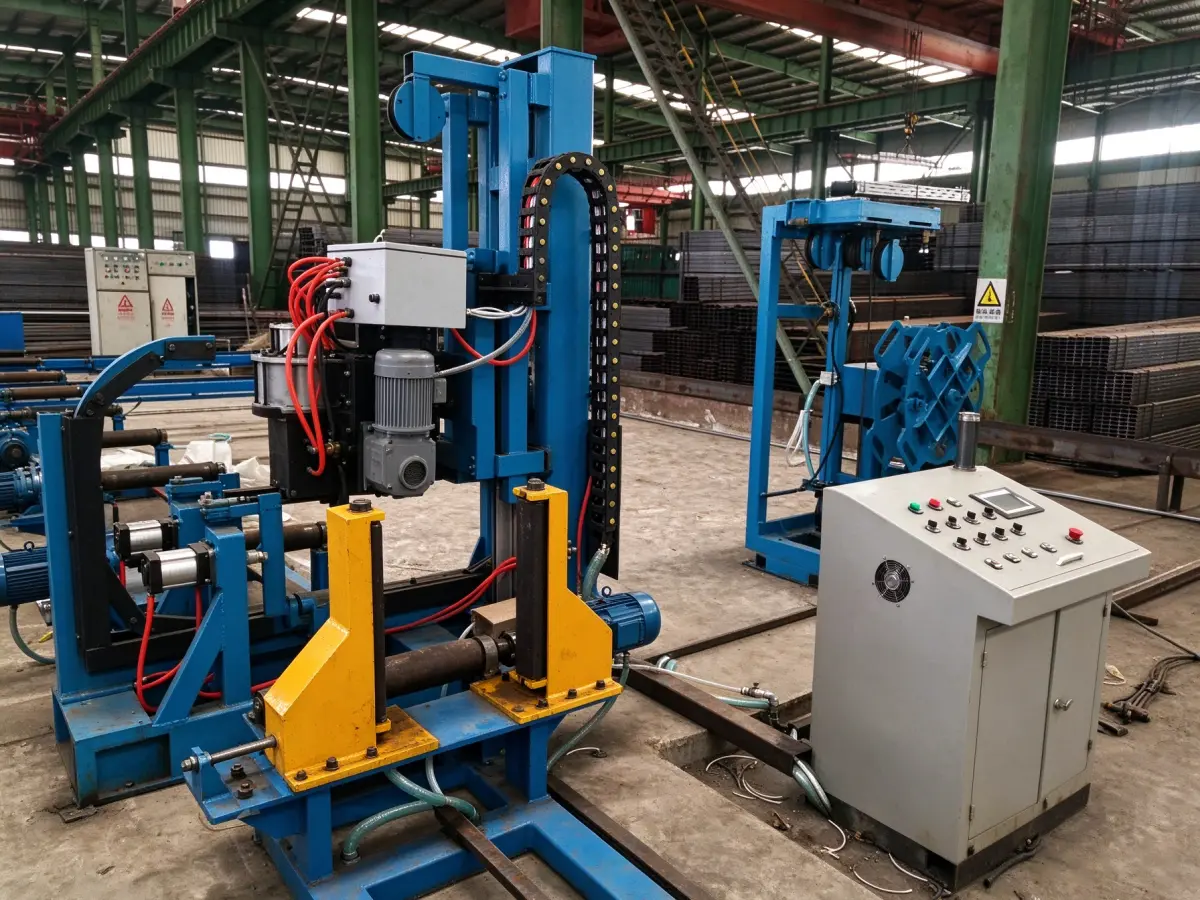
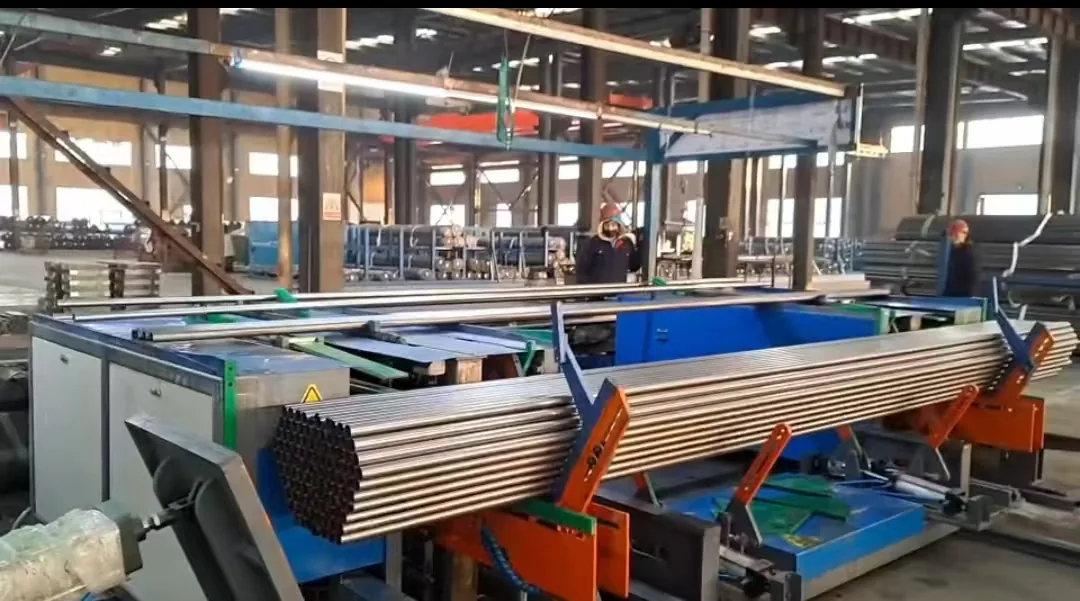
Deliveries in or near this band include Egypt at HG76 × 3 and HG89 × 5, Malaysia at HG60 × 3, Mexico at HG114 × 4, Sri Lanka at 89 × 5, and India at 76 × 3. The photographs below come from these deliveries, at customer plants or during customer visits to our works; customer names are withheld, and each card shows the country, the industry and the model or size.
From the Workshop
 Steel Coil Slitting Line
 Roll Forming Machine
 Purlin Machine Lines
 Pipe Production Applications
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.