
Home › Tube Mill › Small-Diameter Tube Mill › HG50
The second of the twelve model steps — Φ16 – Φ50.8 mm round pipe and 12×12 – 40×40 mm square section, on a 200 kW high-frequency welder.
Model Steps
In This Line
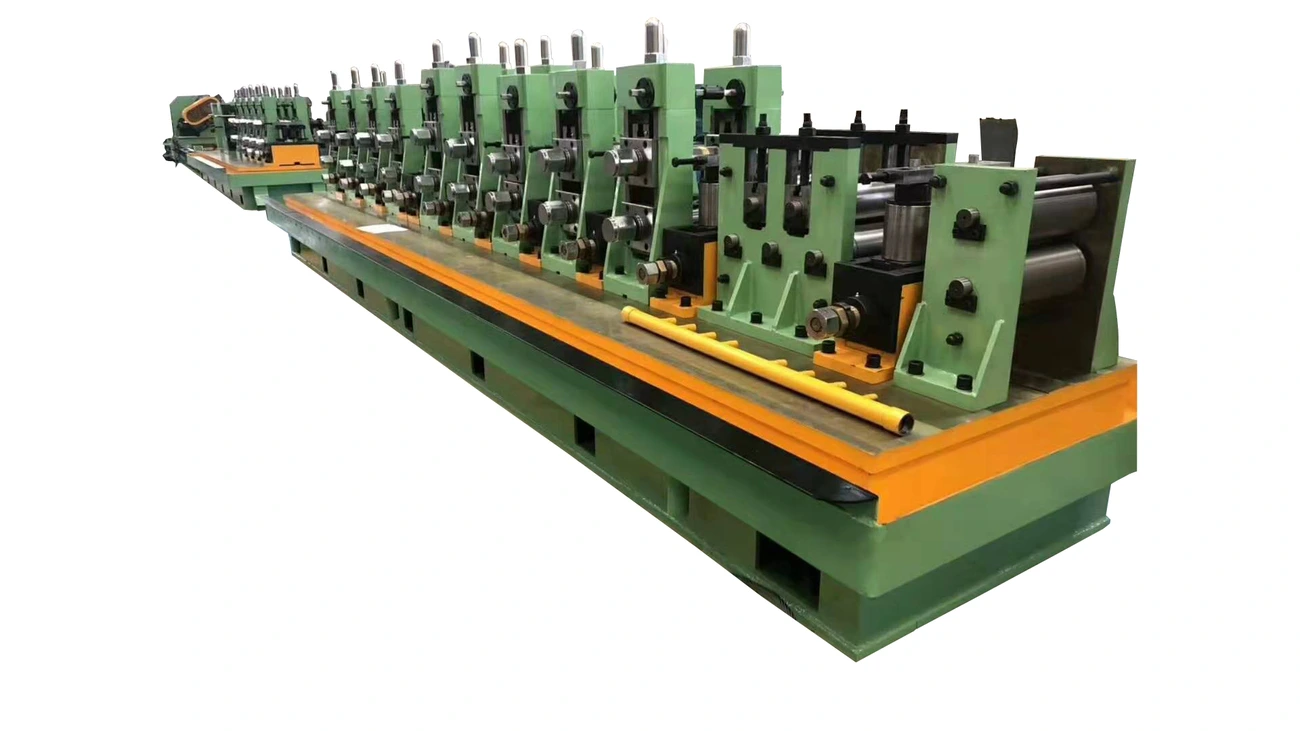
The HG50 tube mill is a Φ16–50.8 mm tube mill for round pipe with 0.8–2.0 mm wall, square pipe from 12×12 to 40×40 mm and 30×50 mm rectangular pipe, welded by a 200 kW high-frequency welder. For thin-wall tube in this size range it is the line to compare first: the larger HG76 starts at 1.5 mm wall.
Line Specification — HG50×2.0
| Round tube outside diameter | Φ16 – Φ50.8 mm |
|---|---|
| Wall thickness | 0.8 – 2.0 mm |
| High-frequency welder | 200 kW |
| Square / rectangular tube | Square 12×12 – 40×40 mm; rectangular 30×50 mm; wall 0.8 – 2.0 mm |
Watch This Line Running
HG50 High-Frequency Welded Pipe Mill — O.D. 16-50.8 mm
HG50 Tube Mill Specifications
- Outside diameter range: Φ16–50.8 mm.
- Wall thickness: 0.8–2.0 mm for round, square and rectangular pipe.
- Section shapes: round; square from 12×12 to 40×40 mm; rectangular 30×50 mm.
- Forming: conventional roll forming.
- Welding: high-frequency induction, with a 200 kW welder.
- Automation: semi-automatic or full PLC control.
Line speed and shift output depend on wall thickness, steel grade and cut length, so we confirm both at quotation once you send us your pipe size, material grade and cut length.
What a Tube Mill for 50mm Pipe Includes
As a tube mill for 50mm pipe, the HG50 line is built from the following units, from coil entry to finished pipe:
- Uncoiler with a pneumatic four-link expanding mandrel.
- Automatic shear-welder, joining strip end to strip end so the line keeps running between coils.
- Spiral accumulator, storing strip while the next coil is prepared.
- Forming and sizing mill.
- 200 kW high-frequency welder.
- Flying saw, cutting to length while pipe is delivered continuously.
- Run-out table, carrying the finished pipe to the collecting table.
- PLC and variable-frequency control tying speed and cut length together.
Wear Parts and Consumables
Impeders and induction coils concentrate weld energy at the seam and wear with welding hours; saw blades wear with cutting volume. Both are wear parts we keep supplying. Forming and sizing rolls are replaced as they wear and are machined on our own CNC equipment.
Size Change, Roll Wear and Yield
On the Φ16–50.8 mm tube mill, a size change means changing the roll set. Roll material and heat treatment decide how often that set has to be reworked: under-specified rolls wear early, drift on diameter and need frequent regrinding.
After a size change, PLC and variable-frequency drive control keep line speed and cut length repeatable from batch to batch, instead of leaving them to the operator.
On some of our higher-specification lines, material yield can reach 93 per cent; the yield actually achieved on any line also depends on the buyer’s scheduling and operating practice.
Where the Φ16–50.8 mm Tube Mill Sits in the Series
HG50 is the second of twelve models. The HG32 below it (Φ10–32 mm) overlaps its smaller sizes, and the HG76 above it (Φ25–76 mm) covers its sizes from Φ25 mm up but starts at 1.5 mm wall. If much of your tube is thinner than 1.5 mm, the HG50 is the size to look at; if your wall is mostly 1.5 mm and up and larger diameters are coming, compare it with the HG76 before choosing a Φ16–50.8 mm tube mill.
Delivery, installation and support
The line is dismantled into units and shipped in containers: heavy frames are braced and secured, while precision parts and wear items travel in wooden cases together with a spare-parts pack. Shipment is within 90 working days of the deposit.
Installation and commissioning are guided on site by our engineers, with online support behind them; the buyer provides the installation crew and covers the engineers’ travel, lodging and daily allowance. Our after-sales team handles enquiries.
Payment is staged — 30% by T/T on signing, 65% by T/T before shipment and 5% after installation and commissioning — or made by L/C at sight; prices are quoted ex-works (EXW).
Where Our Lines Are Running
Our lines have gone to 25 countries — most make construction tube, and others run fire-extinguisher tube, furniture tube and other sections.
Weld and Size Quality on This Line
Three stages set quality rather than keep the line running: forming, where strip condition decides how cleanly the tube closes; welding, where power, seam alignment and squeeze decide fusion; and sizing with straightening, where final dimension and straightness are set. Uncoiling, shear-welding, accumulating and cutting keep the line continuous.
Weld fusion is on the equipment side — power matching, seam alignment and squeeze control — while strip quality and operating practice are on the buyer’s. Dimensional accuracy divides the same way: sizing and straightening on the equipment side, incoming strip thickness tolerance on the buyer’s.
What to send with an enquiry
Outside diameter, wall thickness, section shape and target output, plus the standard the finished pipe is made to. Welder power comes with the size range: on the HG50 tube mill it is 200 kW.
Line Photos from the Works
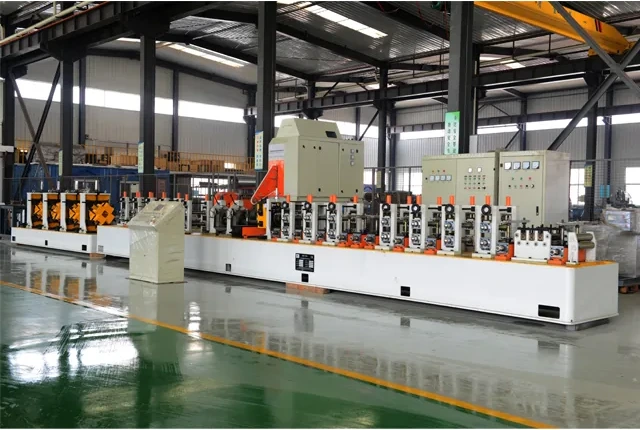
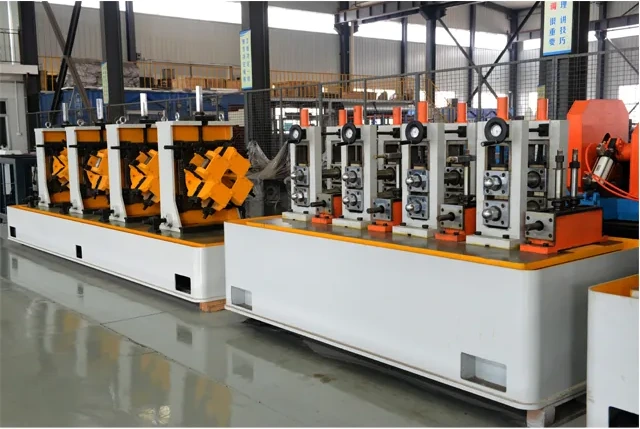
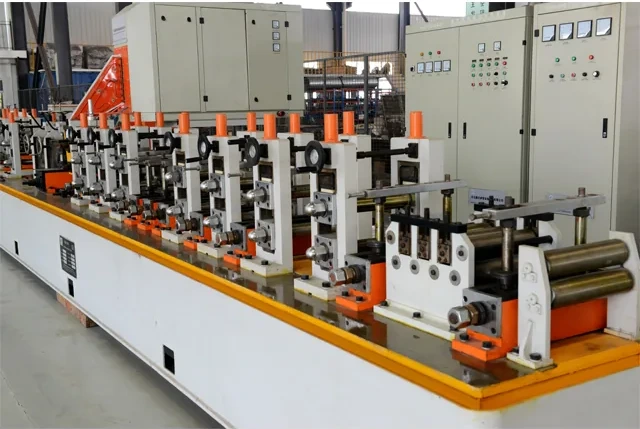
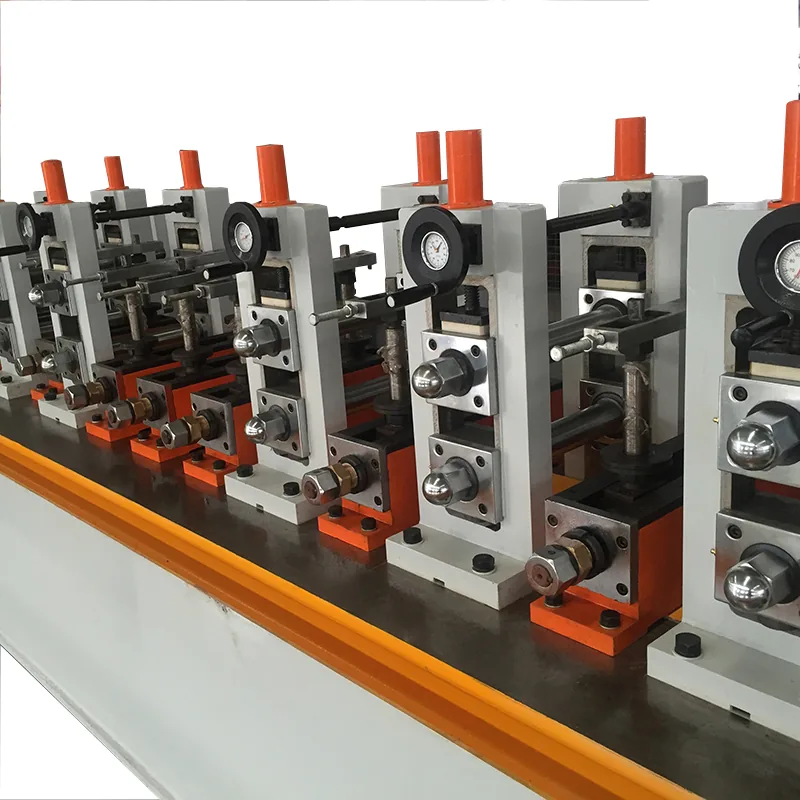
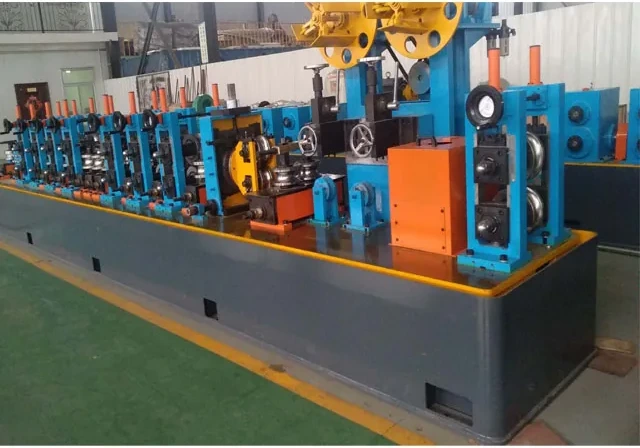
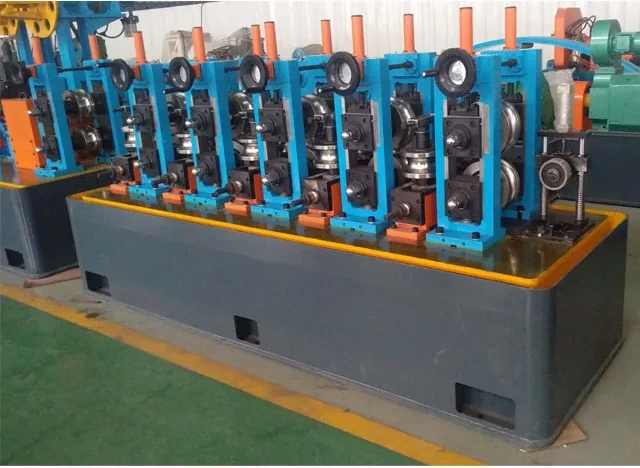
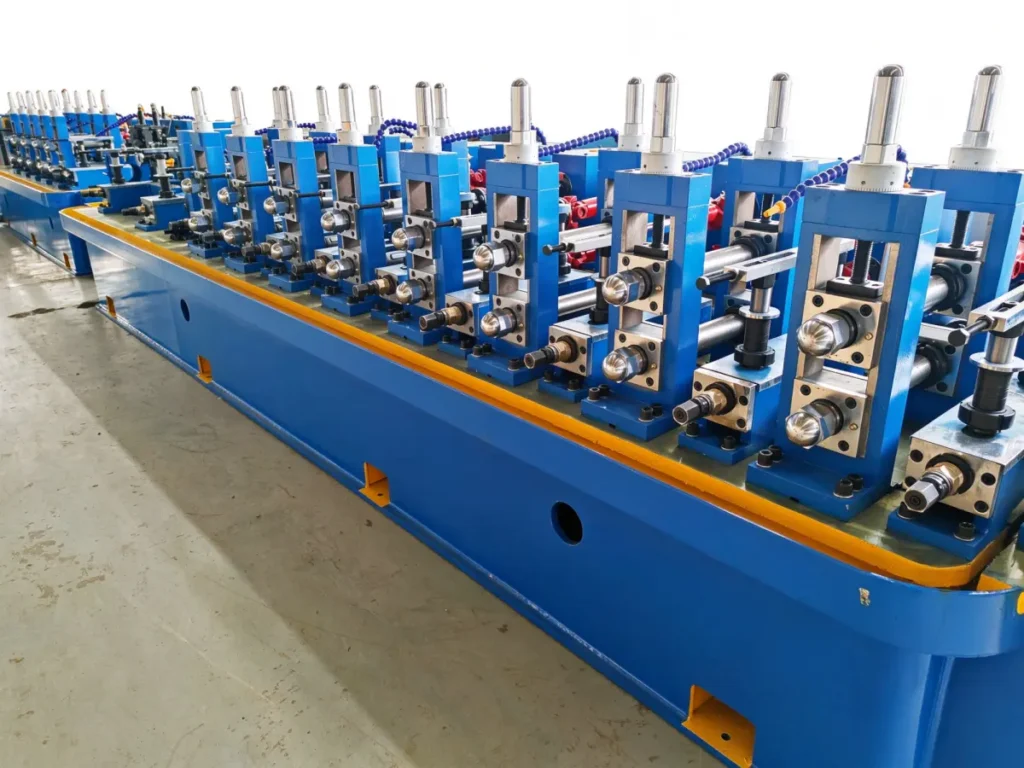
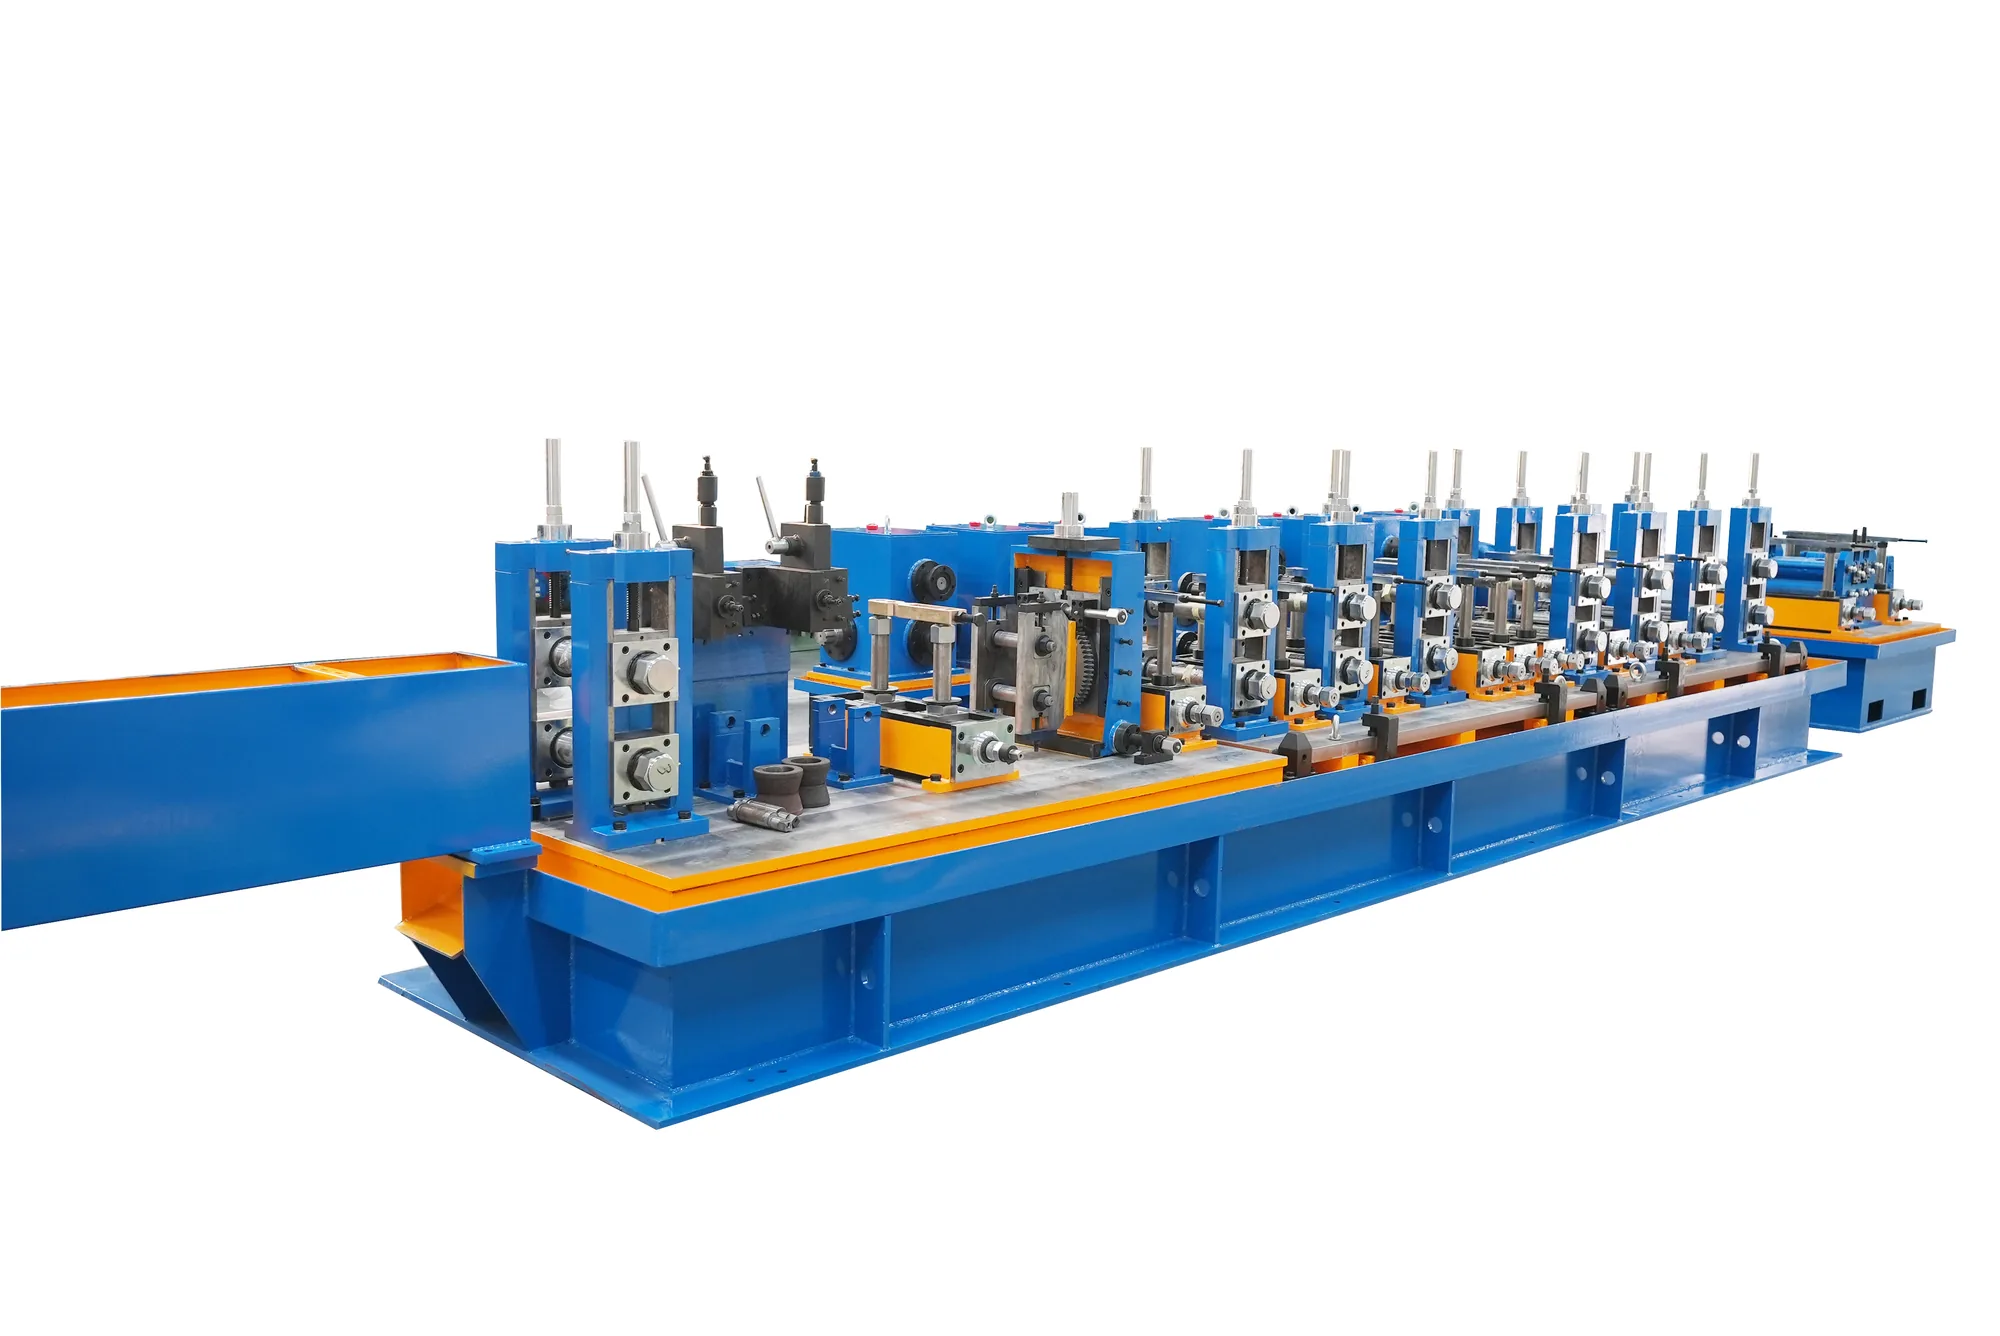
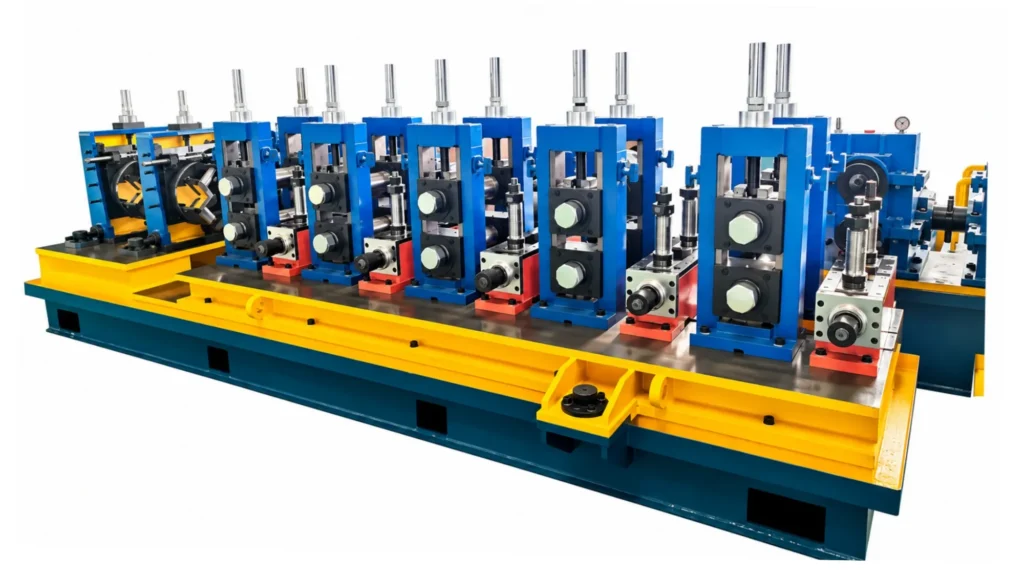
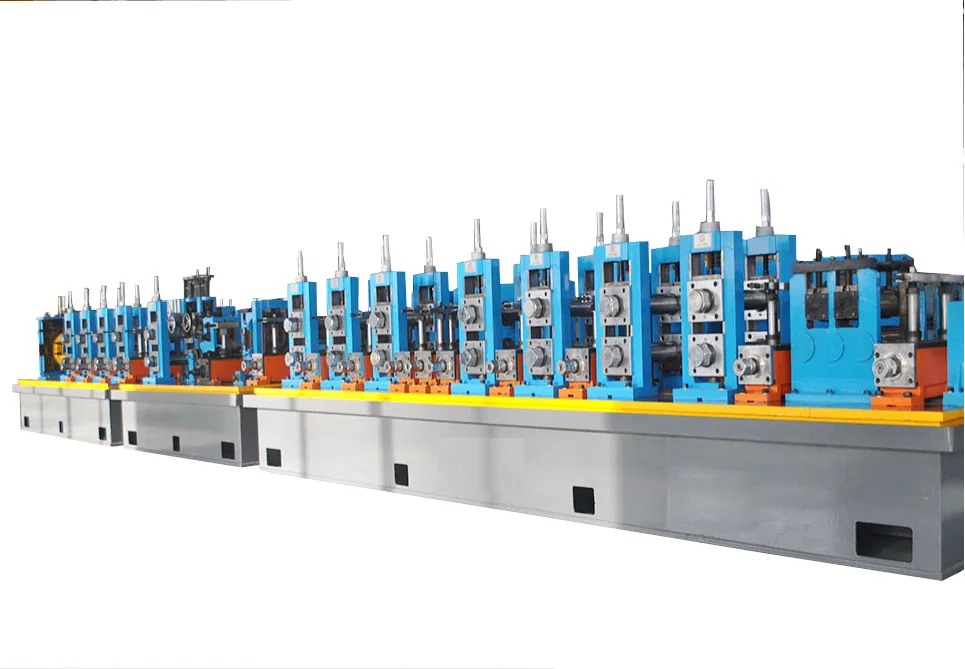
Six photographs of the HG50 tube mill. Click any photo for the full-size image.
 HG32
 HG76
 HG89
 HG114
Send Your Enquiry
Tell us the pipe outside-diameter range, the wall thickness and the output you need. An engineer reads every enquiry — it does not land in a general sales inbox.